
스테인리스강용 U 드릴: 더 나은 공구 수명과 칩 제어를 위한 7가지 검증된 팁
Short insert life, tangled chips and scratched holes are common reasons customers ask for a different U drill. Before recommending a replacement, confirm the stainless grade, hole size and current body and inserts. “Stainless steel” alone is not enough to select a suitable insert combination.
For a replacement, first check whether the existing body and insert stock can still be used. For a new drilling application, confirm the hole requirements, machine setup and coolant supply. The seven tips below explain what to check to improve tool life and chip control.
간단한 답변
For stainless-steel U drilling, check the complete tool system and machining conditions. Review these seven points before a trial or replacement.
Confirm diameter, usable depth and overhang.
Match grade, geometry and cutting position.
Check flow and pressure at the drill.
Use starting data for the tool and alloy.
Watch for wrapping, packing and scratching.
Check alignment, clamping and overhang.
Monitor both inserts before wear damages the body.
목차
Seven tips for better tool life and chip control, followed by troubleshooting and buyer FAQs.
스테인리스강이 드릴링하기 어려운 이유
Stainless steels do not all machine the same way. Confirm the alloy and condition: 304, 316, duplex and hardened grades may need different insert choices and starting data.
Common austenitic grades can work-harden and form long, adhesive chips. Rubbing edges and poor chip evacuation can accelerate wear and damage the hole surface. Check the material, cutting edges and chip path together.
Common stainless-steel drilling problems
열 축적
Stainless steel tends to retain heat near the cutting zone.
Machining Impact
Faster insert wear and more frequent insert changes.
작업 경화
Austenitic stainless steels can work-harden during cutting, making subsequent cutting more difficult.
Machining Impact
More difficult cutting and shorter tool life.
길고 끈적한 칩
Chips do not break as easily as in brittle materials.
Machining Impact
Poor chip evacuation and possible hole scratching.
빌드업 에지
Material may stick to the cutting edge during drilling.
Machining Impact
Edge buildup, less predictable cutting and poorer hole quality.
진동 감도
Stainless steel drilling is less forgiving of unstable setups.
Machining Impact
Poor hole finish and variation between holes.
U 드릴은 스테인리스 스틸에 좋은가요?
예, a 스테인리스 스틸용 U 드릴 은 특히 반복 생산 시 중간 직경 이상의 구멍에 효율적이고 경제적인 선택이 될 수 있습니다.
For repeat purchasing, the useful features of an indexable U drill include:
- Replace worn inserts while retaining a serviceable drill body
- Specify the insert grade and geometry for the actual stainless material
- Record the approved body and insert combination for repeat orders
Check the available diameter range, usable depth and hole capability of the exact drill series before comparing it with other drilling methods.
Before promising longer tool life, check the insert geometry, coolant delivery, machine rigidity, clamping and cutting data. A replacement body alone may not resolve the customer’s machining problem.
Already have a model? Review My Current Model
팁 1: 올바른 U 드릴 직경과 깊이 선택하기
Confirm the required diameter and actual drilling depth with the end user, then check the usable depth on the body drawing. A diameter and a “3D” or “5D” description alone do not identify the complete tool.
드릴 바디가 필요 이상으로 길면 강성이 떨어지고 진동이 증가할 수 있습니다. 스테인리스강 드릴링에서 이는 종종 불안정한 절삭, 인서트 수명 단축 및 구멍 품질 저하로 이어집니다. 많은 표준 애플리케이션의 경우 더 짧고 견고한 설정이 더 안전한 선택입니다.
Before recommending a body, confirm:
- 구멍 지름
- 구멍 깊이
- 기계 스핀들 상태
- 공작물 클램핑 안정성
- 냉각수 가용성
If you need to confirm the drill-body series, usable depth, machine interface and insert compatibility before ordering, start with our U Drill Selection Guide.

팁 2: 스테인리스 스틸에 적합한 인서트 선택하기
When a customer reports short insert life, identify which insert position is affected before recommending a different grade or geometry.
스테인리스 스틸 드릴링 시 인서트는 내마모성과 인성 사이의 균형이 잘 맞아야 합니다. 절삭날이 너무 약하면 너무 일찍 부서질 수 있습니다. 너무 무디면 절삭 열이 빠르게 상승하여 칩 제어가 악화될 수 있습니다.
Before ordering inserts, confirm:
- The full insert code for each position
- The grade and chipbreaker recommended for the stainless material
- Compatibility with the drill body, pocket and screw
- The required quantity for each insert specification
Check the center and peripheral inserts separately. Their cutting speeds and loads differ, and the body’s approved combination may specify different grades or chipbreakers.
To compare common WC and SP systems before selecting a replacement, see our WC 타입과 SP 타입 U 드릴 비교.
Browse our U-드릴 인서트 to identify the family, then confirm the full code and grade against your body model.


팁 3: 가능하면 내부 냉각수 사용
Coolant is one of the most important factors in stainless steel drilling. Stainless steel tends to retain heat near the cutting zone, and chip evacuation is often more difficult than in short-chipping materials. Internal coolant is generally preferred because it helps reduce heat, improves chip evacuation, and lowers the risk of chip jamming. Dry drilling is generally not recommended for stainless steel. Confirm adequate coolant flow and pressure at the tool; a high pump-pressure rating alone does not establish sufficient delivery.
Effective internal coolant can help with:
- Heat removal at the cutting zone
- Chip removal from the hole
- Lubrication to reduce material adhesion
If internal coolant is unavailable, confirm the selected tool’s requirements before use. External coolant may be suitable for shallow holes with reliable chip evacuation, where the tool supplier permits it. Reducing cutting speed alone does not establish suitability. See Sandvik Coromant’s coolant guidance for general principles.
If the customer is unsure about coolant capacity, ask for the machine’s through-tool coolant details and a description of delivery at the drill. Share these with the tool supplier before confirming suitability.
팁 4: 절단 속도 및 이송 속도 최적화하기
Obtain starting cutting speed and feed for the exact body, insert combination and stainless grade. Include these recommendations with the trial tools.
사용 시 스테인리스 스틸용 U 드릴, 과도한 절삭 속도는 종종 열을 증가시키고 인서트 마모를 가속화합니다. 반면에 이송이 너무 낮으면 절삭 대신 마찰이 발생하여 공작물이 경화되고 공구 수명이 단축될 수 있습니다.
Inspect the chips, both cutting edges and hole quality during the trial. Change one setting at a time within the supplier’s recommended range so the results can be compared.
Record the following during the trial:
- 칩 모양
- 절단 소리
- 마모 패턴 삽입
- 구멍 표면 마감
- 기계 부하
- 냉각수 성능
Keep the speed, feed and coolant conditions with the completed-hole count and the reason each insert was indexed or replaced. A claim such as “the insert only lasted 20 holes” is difficult to assess without those details.
When drilling stainless steel, parameter adjustment should not focus on speed alone. Evaluate chip shape, coolant delivery, wear on both inserts and setup rigidity together. Sandvik Coromant’s indexable-drill troubleshooting guidance gives separate checks for wear, chip jamming and unstable hole quality.
Cutting-data reference: formulas and depth checks
Use the recommended cutting data for the selected body and inserts. Check that it covers the actual stainless grade, hole depth and coolant conditions.
- vc = 절단 속도(m/min)
- D = 드릴 직경(mm)
- fn = 회전당 이송량(mm/회전)
- n = 스핀들 속도(rpm)
- vf = 이송 속도(mm/min)
Check the drilling depth
| 드릴링 깊이 | 추천 시작 전략 |
|---|---|
| 최대 3×D | Use the selected series’ starting data and verify coolant delivery and chip formation |
| 3×D 이상 | Prioritize through-tool coolant and verify the series’ depth capability; review geometry and cutting data if chips do not evacuate reliably |
홀 깊이가 깊어질수록 칩 배출이 더 어려워지고 공정 안정성이 더 민감해집니다. 내부 절삭유는 깊은 홀과 스테인리스강과 같이 칩이 오래 남는 소재에 특히 중요합니다. 주요 툴링 공급업체의 지침에 따르면, 특히 약 5mm 이상 드릴링할 때 관통 절삭유를 강조합니다. 3 × 드릴 직경.
For a series-specific example, see Walter’s D4120 cutting-data reference (PDF). Its values apply to the specified Walter system; request starting data for the drill body, inserts and stainless grade you plan to order.
팁 5: 칩 제어에 집중하기
Check chip evacuation during the trial before approving the tool for repeat supply. If chips wrap around the tool or pack in the hole, collect photos before recommending another insert.
스테인리스 스틸의 경우 칩이 길고 끈적거리는 경향이 있습니다. 제대로 파손되지 않거나 원활하게 배출되지 않으면 구멍 벽이 긁히거나 인서트가 손상되고 절단 열이 증가하여 결국 고장의 원인이 될 수 있습니다.
A long chip formed as the drill first enters the material is not, by itself, evidence of poor chip control. Focus on persistent wrapping, chip packing, hole-wall scoring or irregular machine load during drilling.
Checks to discuss with the end user:
- 스테인리스 스틸 가공용으로 설계된 인서트 사용
- 절삭유가 절삭 영역에 효과적으로 도달하는지 확인합니다.
- 불안정한 커팅 매개변수 방지
- 칩이 비정상적으로 보이면 중지하고 검사하기
- 엄격하고 안정적인 머신 설정 유지
Inspect chips from both insert positions; they may have different shapes. Wrapping or packed chips are an early warning to check the process. Confirm any peck cycle against the selected drill’s application guidance rather than adding repeated retracts automatically.
팁 6: 진동 및 런아웃 줄이기
If a customer reports chipping or inconsistent hole quality, ask about the holder, overhang, alignment and workpiece clamping as well as the tool specification.
약간의 진동도 인서트 마모, 거친 홀 표면, 조기 모서리 칩핑을 유발할 수 있습니다. 또한 과도한 런아웃은 인서트에 고르지 않은 하중을 가하고 공정 일관성을 떨어뜨릴 수 있습니다.
Checks to reduce vibration and runout:
- 도구 오버행 최소화
- 안정적인 홀더 및 클램핑 시스템 사용
- 스핀들 상태 확인
- 공작물을 올바르게 고정하기
- 약한 설정에서 지나치게 공격적인 커팅 조건 피하기
Identify whether the drill rotates in a machining centre or remains stationary on a lathe. Include the setup type and measured alignment or runout, where available, with any report of inconsistent hole size.
팁 7: 인서트 마모 모니터링 및 제때 교체하기
Agree on when the end user will index or replace the inserts during the trial. Continuing with heavily worn edges can affect hole quality, chip control and the condition of the drill body.
Signs that an edge needs inspection:
- 엣지 치핑
- 과도한 측면 마모
- 표면 마감 불량
- 비정상적인 절단음
- 칩 모양 변경
- 기계 부하 증가
Record wear and indexing separately for the center and peripheral inserts, and check seats and screws during replacement. Timely indexing or replacement helps protect the drill body and hole quality.
스테인리스 스틸에 U 드릴을 사용할 때 흔히 발생하는 문제
Use the table to decide what information to request when a customer reports a problem. Send the body and insert codes, photos of both used inserts and chips, and the actual cutting conditions to the supplier for review.
| 문제 | 가능한 원인 | 제안 솔루션 |
|---|---|---|
| 빌드업 에지 | Adhesion associated with cutting conditions, unsuitable edge geometry or inadequate lubrication | Identify the affected insert position and inspect adhesion and coolant delivery. Review geometry and cutting speed within the supplier’s range; lowering speed is not a universal remedy. |
| 칩 배출 불량 | 긴 칩, 불충분한 절삭유 압력 또는 불안정한 절삭 조건 | Review feed and chip control. Check coolant flow, direction and pressure. |
| 짧은 공구 수명 | 높은 절단 온도, 진동 또는 잘못된 인서트 선택 | Review cutting speed and setup rigidity, then coolant effectiveness and insert choice. |
| 거친 구멍 표면 | 구멍 내부의 마모, 진동 또는 칩 스크래치 삽입 | Check runout and feed stability, then insert wear and chip scratching. |
| 일관성 없는 홀 품질 | 공구 런아웃, 불안정한 클램핑 또는 고르지 않은 인서트 마모 | 클램핑 안정성 향상, 런아웃 제어 및 마모된 인서트 적시 교체 |
Before You Order
Before placing the order, confirm the drill body and both insert specifications against the stainless grade, hole requirement and available coolant supply.
Use the trial result to agree on hole quality and tool life. Keep the approved tool configuration and test conditions with the order record. For test planning and feedback records, see our 절삭 공구 시험 주문 안내서.
구매자 자주 묻는 질문
What information do you need to quote a U drill for stainless steel?
Send the stainless grade, hole diameter and depth, quantity and destination. For a replacement, include the body model and photos of both insert labels. State whether you need bodies, inserts or complete sets. Add machine and coolant details where available.
Can you suggest an alternative to the U drill our customer already uses?
Yes. Send the existing brand, full body and insert codes, or a catalogue page and clear photos. We can compare the specifications. Pocket fit, insert pairing, usable depth and application suitability need confirmation before approving a replacement.
Can we keep our current drill body and change only the inserts?
That may be possible if the body and pockets are serviceable and a compatible insert configuration suits the stainless material. Send the complete body model and insert codes for both positions. A similar shape alone does not establish compatibility.
Can we place a small trial order before buying larger quantities?
Yes. Send the proposed body and matching insert quantities so we can confirm the MOQ for each item. Samples are generally charged, with freight paid by the buyer. Agree on the hole-quality and tool-life checks before the end user tests the tools.
Are the drill bodies and matching inserts available from stock?
Availability depends on the body model, insert specification and quantity. Some standard items are stocked; others need production. Send the full list so we can check both the bodies and matching inserts and confirm the dispatch date with the quotation.
Our customer reports short insert life or chip problems. What should we send?
Start with the body and insert codes, photos of both used inserts and chips, and the number of holes completed. Add the material grade, hardness, hole size, machine, speed, feed and coolant conditions where known. These help us review the likely cause.
How can we keep repeat orders consistent with the approved trial?
We retain confirmed specifications and order records for repeat supply. Reference the approved order and identify the body model, insert codes, grades and chipbreakers for both positions. Confirm any proposed substitution before ordering. Keep the trial conditions with your customer’s approval record.
For payment, shipping and other order questions, see our 구매자 자주 묻는 질문.
관련 U-Drill 가이드
 U Drill Selection Guide
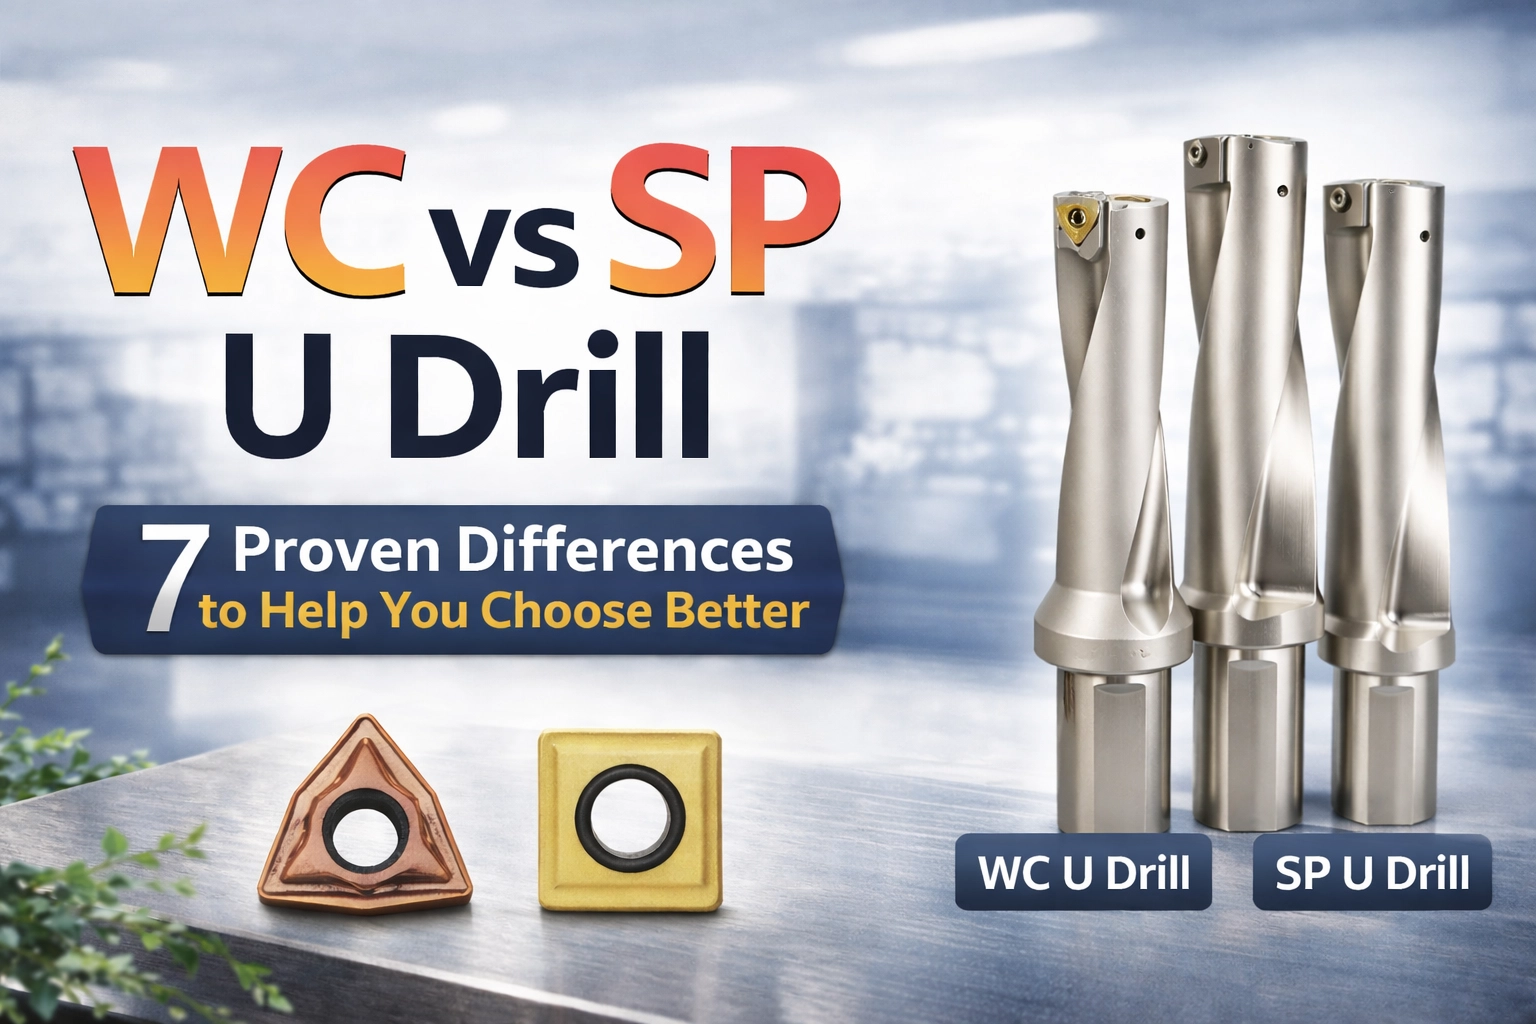 WC형 대 SP형 U 드릴
Send Your U-Drill Requirements
Start with your current model or clear tool photos and quantities. We can review a replacement or help check a new application.
Replacing a tool
Body model, both insert labels or photos, quantity and the current issue.
Selecting for a new application
Stainless grade, hole diameter and depth, machine and coolant details.
Tell us whether you need bodies, inserts or complete sets.