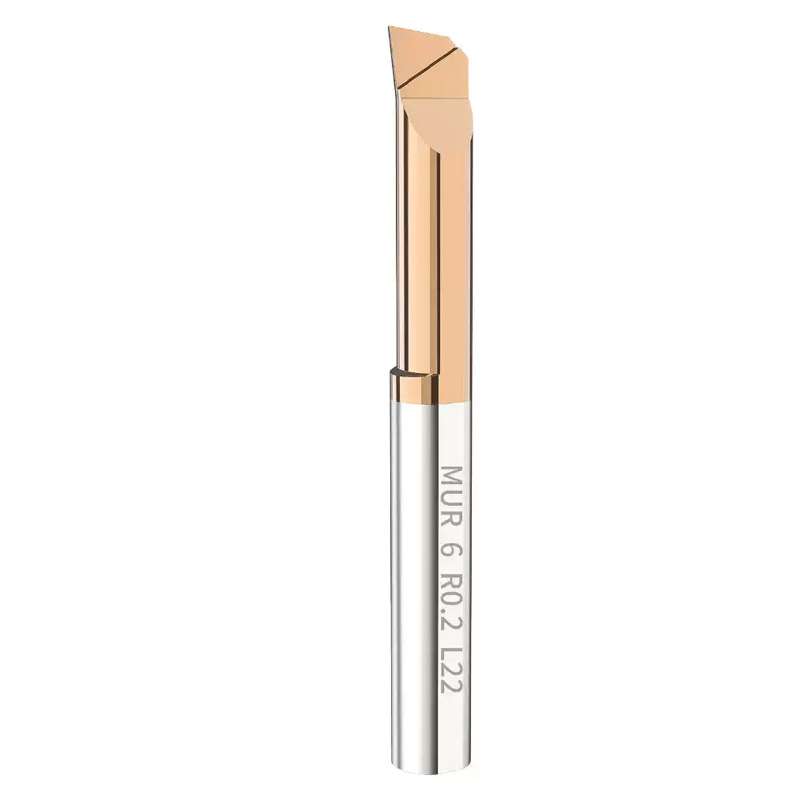
MIR Series 29 Degree Solid Carbide Micro Internal ACME Threading Bars for Small Bore Machining
Kualitas yang Konsisten
Geometri yang konsisten pada setiap pesanan berulang.
Pesanan Fleksibel
Tersedia dalam jumlah kecil dan berbagai ukuran.
Dukungan OEM
Penandaan khusus, label, dan kemasan.
Standar & Khusus
Ukuran standar dan konfigurasi khusus.
MIR 29° Micro Internal ACME Threading Bar
MIR Series 29° solid carbide micro internal threading bars are designed for precision turning of compatible ACME internal threads in small and restricted bores. The right-hand cutting configuration and TPI-specific geometry support compact power-screw, lead-screw and motion-transmission components.
Standard models cover 5 to 16 TPI, cutting diameters from Ø3.9 to Ø11.9 mm and clearance lengths from 15 to 50 mm. The integral fine-grain carbide body provides the rigidity required for controlled 29° flank geometry, repeatable thread depth and stable CNC production.
Ikhtisar Produk
Fitur Utama Produk

Pemilihan Aplikasi & Alat
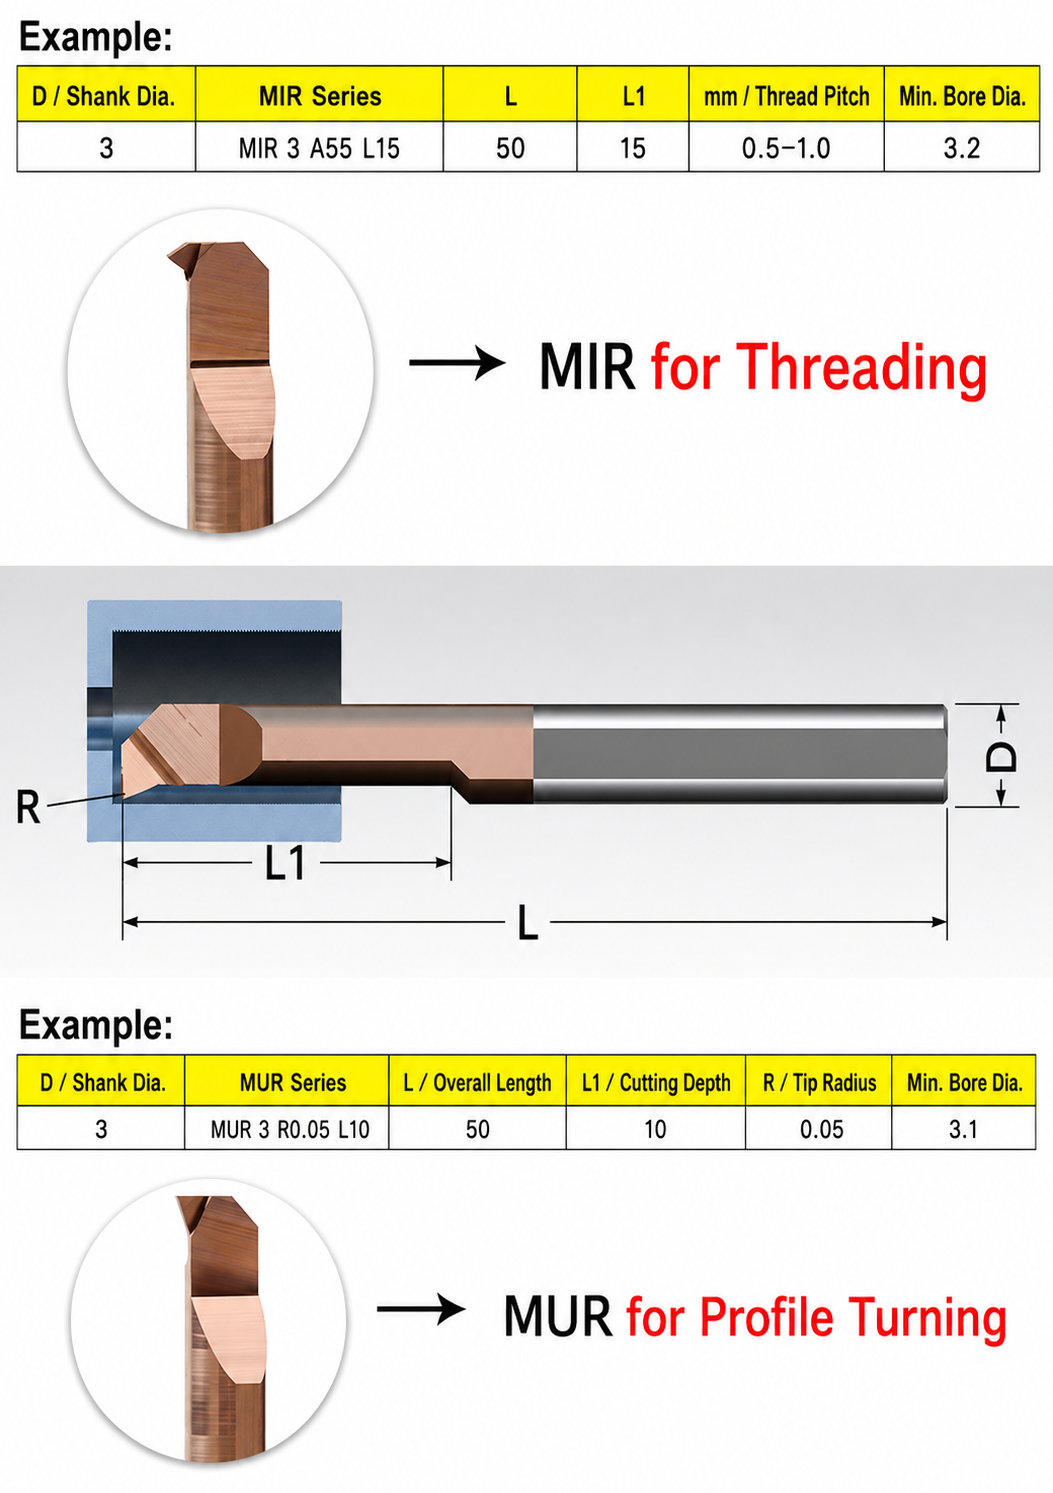
Confirm the ACME Thread FormThis page covers A29 models for compatible ACME internal threads. Confirm nominal diameter, TPI, thread class, hand and whether General Purpose, Centralizing or another ACME form is required.
Match the Threads per InchSelect the TPI-specific model shown in the size table. A 16-TPI tool must not be substituted for a 14-, 12-, 10-, 8-, 6- or 5-TPI model.
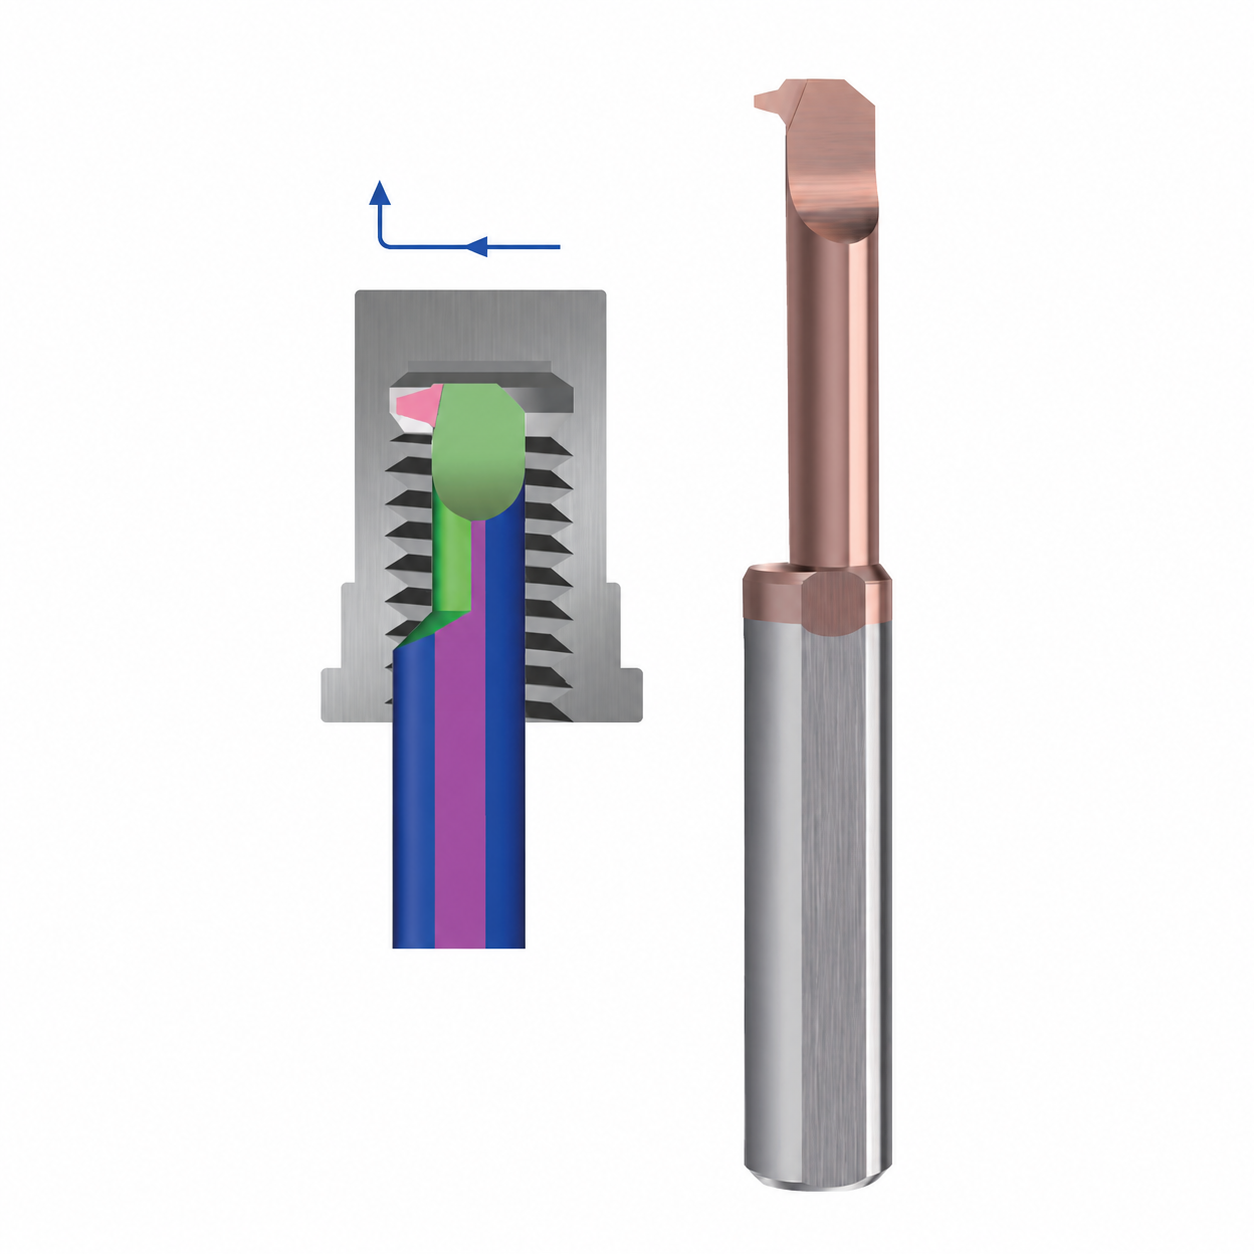
Check Bore and Tool ClearanceVerify that the cutting head, neck, shank and programmed retraction path clear the bore and internal shoulder throughout the complete cycle.
Gunakan Jangkauan Praktis TerpendekChoose the shortest L1 that reaches the full thread length to improve rigidity and reduce vibration during multi-pass threading.
The application image is series-level. For this product, select only the MIR 29° ACME internal threading configuration.
Aplikasi Umum
| Aplikasi | Catatan Penggunaan |
|---|---|
| 29° ACME Internal Threads | Precision machining of compatible imperial ACME internal thread profiles. |
| Lead-Screw Nuts | Internal threads for components used to convert rotary motion into linear movement. |
| Actuators and Clamping Mechanisms | Suitable for compact positioning, adjustment and load-transmission components. |
| Custom Precision Components | For drawing-based parts requiring a verified 29° ACME internal thread form. |
Keunggulan Pengolahan Lubang Kecil

The compact cutting head and integral carbide body provide the rigidity needed for confined internal threading. Correct center height, controlled runout, a suitable infeed strategy and reliable chip evacuation help maintain the broad 29° ACME profile.
- Improved access inside restricted bores
- Reduced deflection during higher-load thread passes
- Controlled 29° ACME flank geometry
- TPI-specific standard model selection
- Suitable for CNC lathes and turning centers
Alat Internal Mikro Standar & Khusus
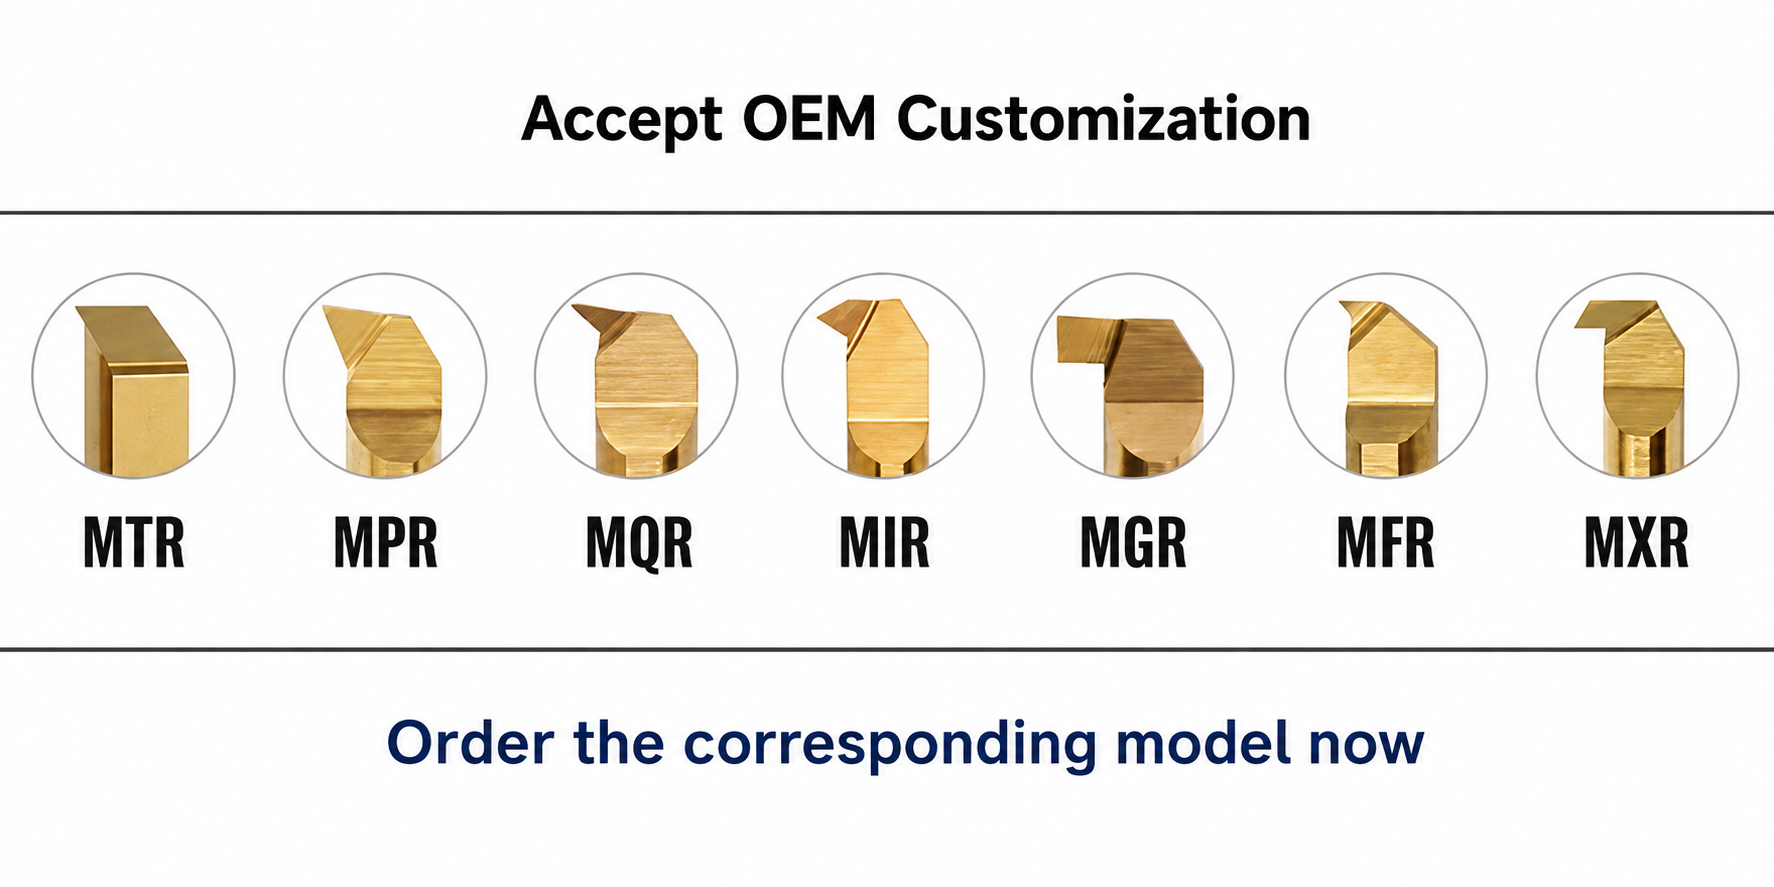
When a standard MIR A29 model does not match the nominal thread diameter, TPI, bore clearance, thread depth or working reach, custom solid carbide internal threading tools can be evaluated according to the component drawing.
Foto dan Video Produk

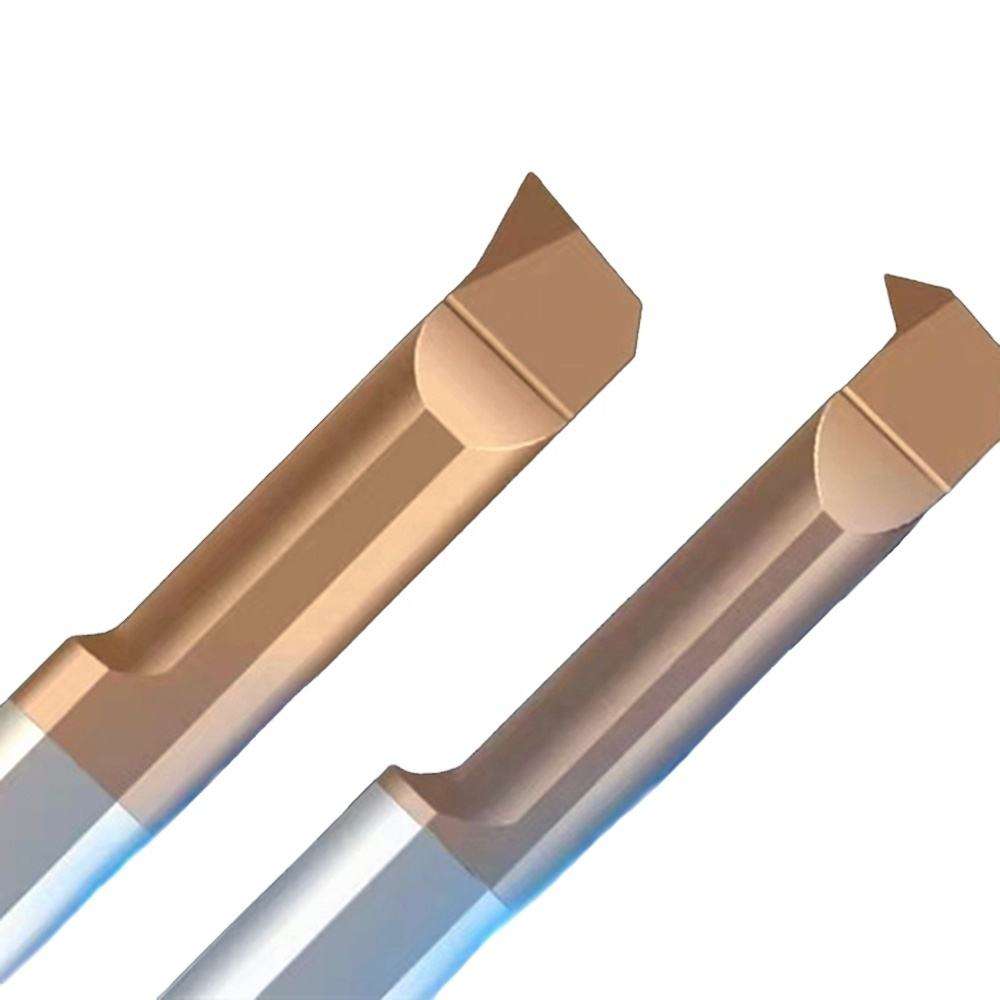
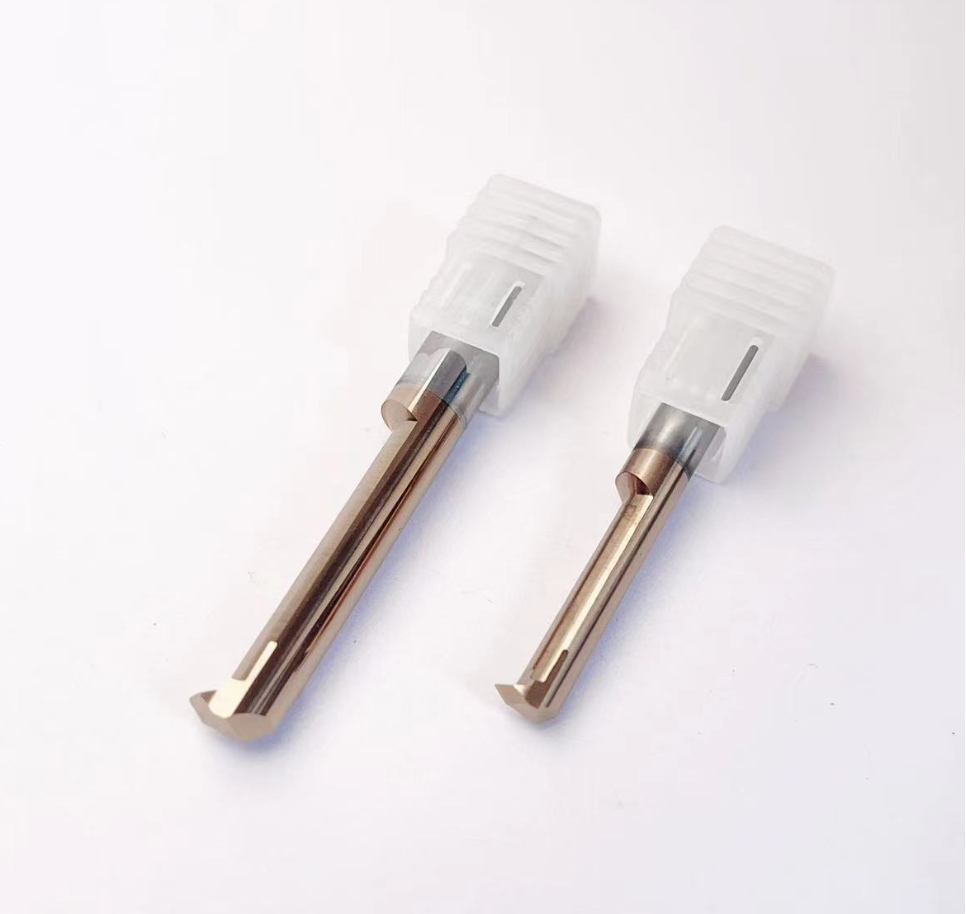

Series-level product video. Confirm the MIR A29 geometry, ACME TPI and model dimensions before ordering.
Custom MIR ACME Threading Bars
Custom ACME thread diameter, TPI, thread class, bore-clearance geometry, working length, shank diameter, carbide grade, coating, laser marking and private-label packaging are available according to drawings and order requirements.
Panduan Penamaan dan Pemilihan Alat
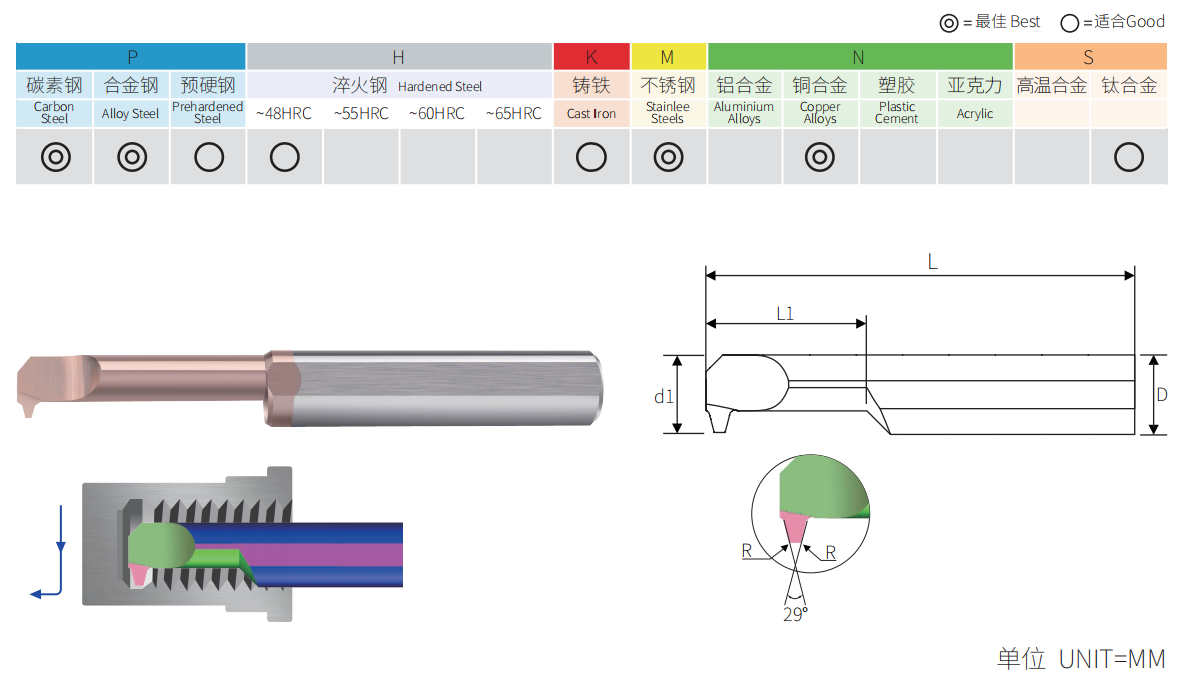
Select the suitable MIR 29° micro internal ACME threading bar according to threads per inch, cutting diameter, clearance length, shank diameter, overall length and required ACME thread form.
| Kode | Deskripsi | Contoh |
|---|---|---|
| MIR | Batang Ulir Internal Mikro Tangan Kanan | Internal ACME threading |
| 39 / 56 / 66 / 79 / 99 / 119 | Cutting Diameter d1 | Ø3.9 / Ø5.6 / Ø6.6 / Ø7.9 / Ø9.9 / Ø11.9 mm |
| P16 / P14 / P12 / P10 / P8 / P6 / P5 | ACME Threads per Inch | 16 / 14 / 12 / 10 / 8 / 6 / 5 TPI |
| L15 / L20 / L25 / L30 / L35 / L45 / L50 | Clearance Length L1 | 15 / 20 / 25 / 30 / 35 / 45 / 50 mm |
| 04 / 06 / 08 / 10 / 12 | Diameter Batang D | Ø4 / Ø6 / Ø8 / Ø10 / Ø12 mm |
| 50 / 60 / 75 / 100 | Panjang Total L | 50 / 60 / 75 / 100 mm |
| A29 | Thread Profile Angle | 29° included angle |
Dimensi & Ukuran yang Tersedia
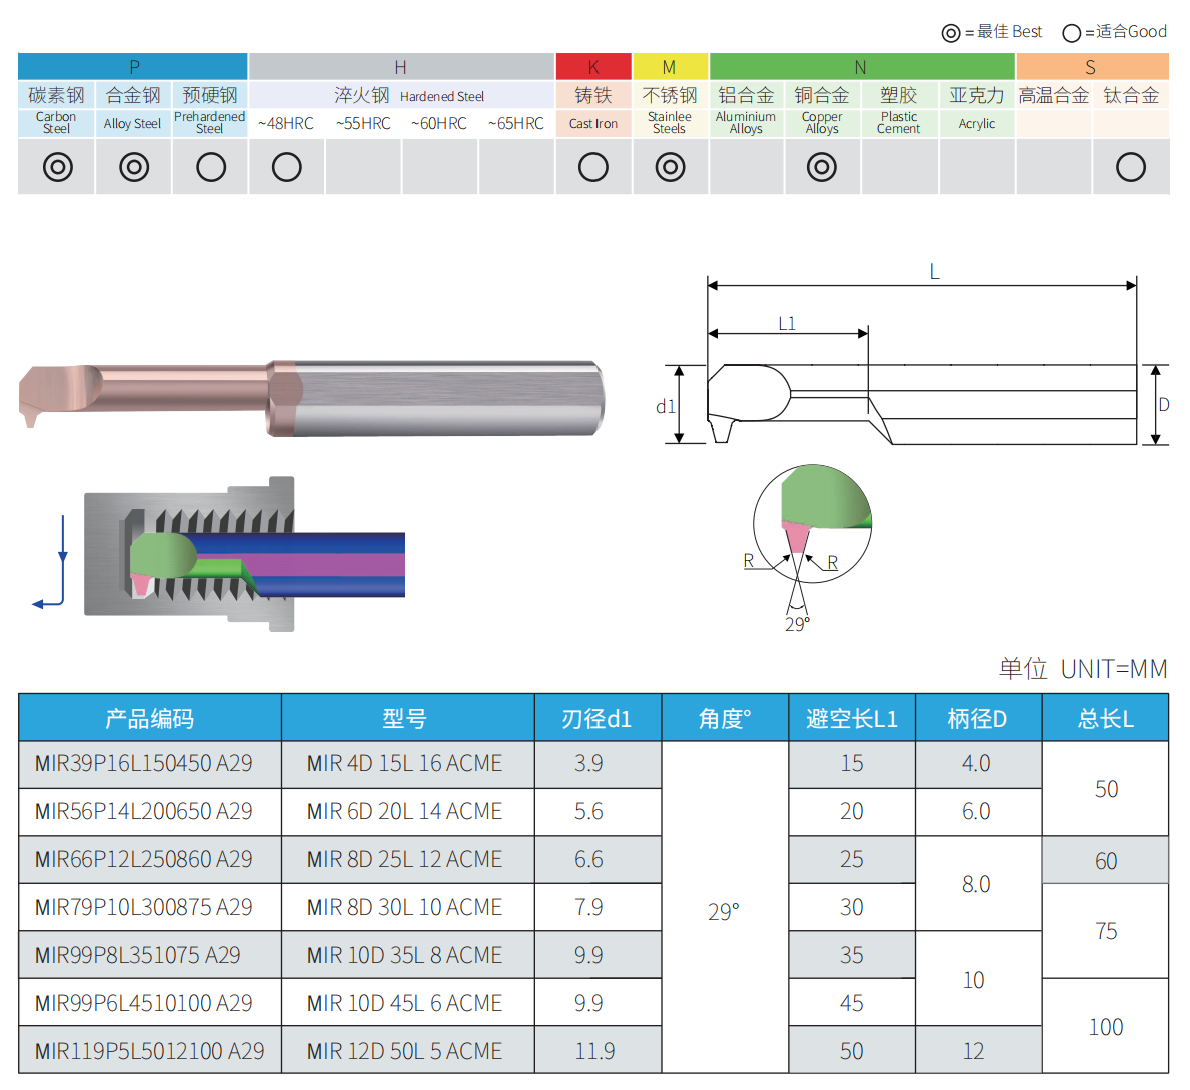
Standard models cover 5–16 TPI, Ø3.9–Ø11.9 mm cutting diameters and 15–50 mm clearance lengths. The cutting diameter d1 is a tool dimension and should not be interpreted as the minimum bore diameter without checking the complete ACME thread and clearance geometry.
Jajaran Model Standar
| Model | TPI | d1 | Sudut | L1 | D | L |
|---|---|---|---|---|---|---|
| MIR 4D 15L 16 ACME | 16 | 3.9 | 29° | 15 | 4 | 50 |
| MIR 6D 20L 14 ACME | 14 | 5.6 | 29° | 20 | 6 | 50 |
| MIR 8D 25L 12 ACME | 12 | 6.6 | 29° | 25 | 8 | 60 |
| MIR 8D 30L 10 ACME | 10 | 7.9 | 29° | 30 | 8 | 75 |
| MIR 10D 35L 8 ACME | 8 | 9.9 | 29° | 35 | 10 | 75 |
| MIR 10D 45L 6 ACME | 6 | 9.9 | 29° | 45 | 10 | 100 |
| MIR 12D 50L 5 ACME | 5 | 11.9 | 29° | 50 | 12 | 100 |
Dimensions are in millimeters except TPI. Confirm the complete ACME designation, nominal diameter, TPI, thread class, hand, thread length and bore clearance before ordering.
Recommended Starting Parameters
Seri Perkakas Internal Mikro Terkait
60° Internal Threading: MIR 60° Series
Right-/Left-Hand Threading: Seri MIR / MIL
Pembuatan Alur Pengurang Tekanan pada Ulir: Seri MDR
Pembuatan Alur Internal: Seri MGR
Kami mendukung para distributor, pemasok perkakas, dan mitra industri dengan solusi OEM dan merek pribadi yang fleksibel untuk produk perkakas mikro internal. Mulai dari penandaan laser dan pengemasan khusus hingga identifikasi produk dan dokumentasi teknis, kami membantu pelanggan membangun lini produk perkakas mereka sendiri dengan dukungan manufaktur yang andal.
Ruang Lingkup Produk OEM
Kami menyediakan solusi manufaktur OEM dan merek pribadi untuk produk perkakas internal mikro, serta mendukung distributor dan pemasok perkakas dengan seri standar, spesifikasi khusus, dan produksi berdasarkan gambar teknis.
Seri MPR dan alat bor berdiameter kecil yang dirancang khusus untuk pemesinan bagian dalam presisi serta aplikasi anti-getaran.
Seri MIR/MIL dengan profil ulir, dimensi, dan persyaratan identifikasi produk yang disesuaikan.
Pembuatan alur internal dan solusi alur khusus untuk komponen presisi berukuran mini.
Tersedia dimensi non-standar, geometri khusus, serta solusi perkakas berdasarkan gambar yang disediakan pelanggan.

Opsi Kustomisasi
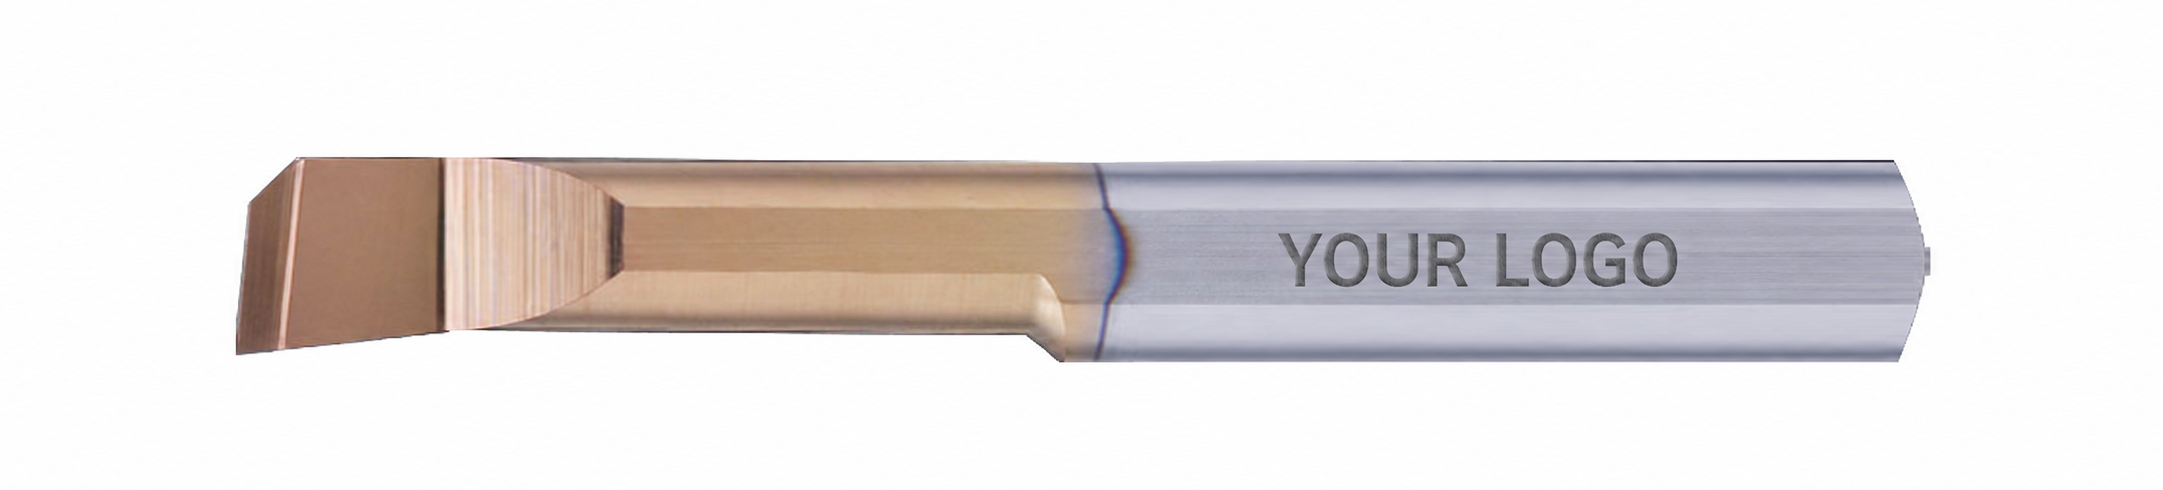
Penandaan Laser & Identifikasi Produk
Logo khusus, nomor model, dan tanda pengenal produk dapat disediakan sesuai dengan persyaratan distributor dan merek.
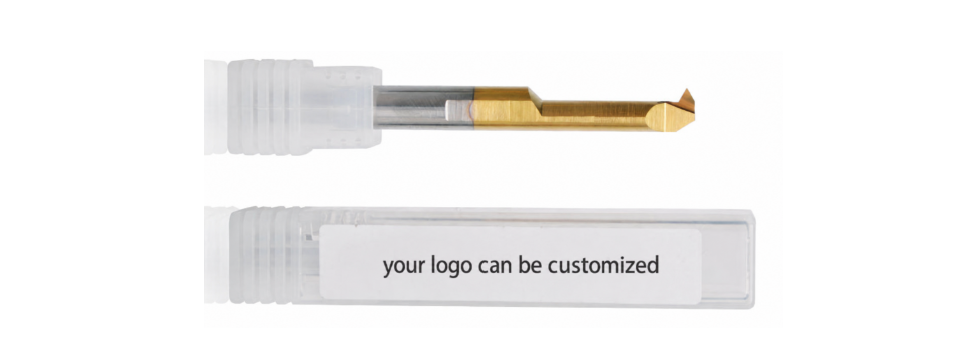
Kemasan Khusus
Kemasan per unit, label, dan informasi produk dapat disesuaikan untuk mendukung saluran penjualan pengecer serta pengembangan merek sendiri.
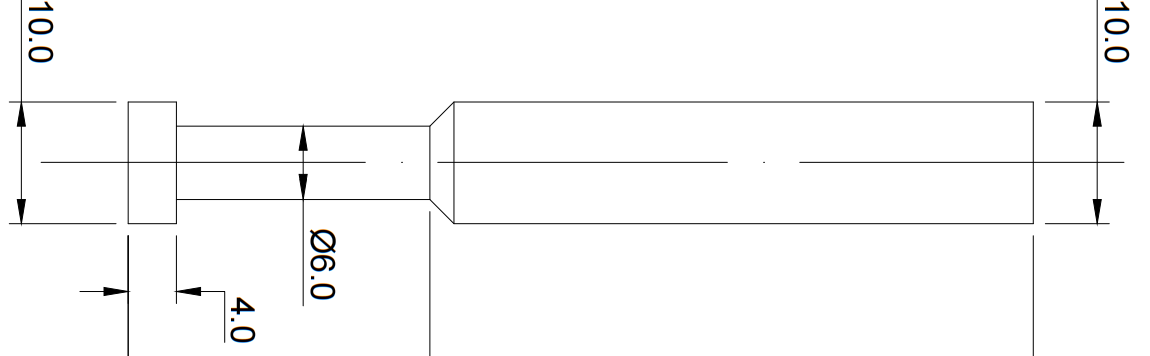
Dokumen Teknis & Dukungan Produk
Menyediakan gambar teknis, spesifikasi, dan informasi produk untuk membantu distributor mempromosikan dan mengelola produk perkakas mereka.
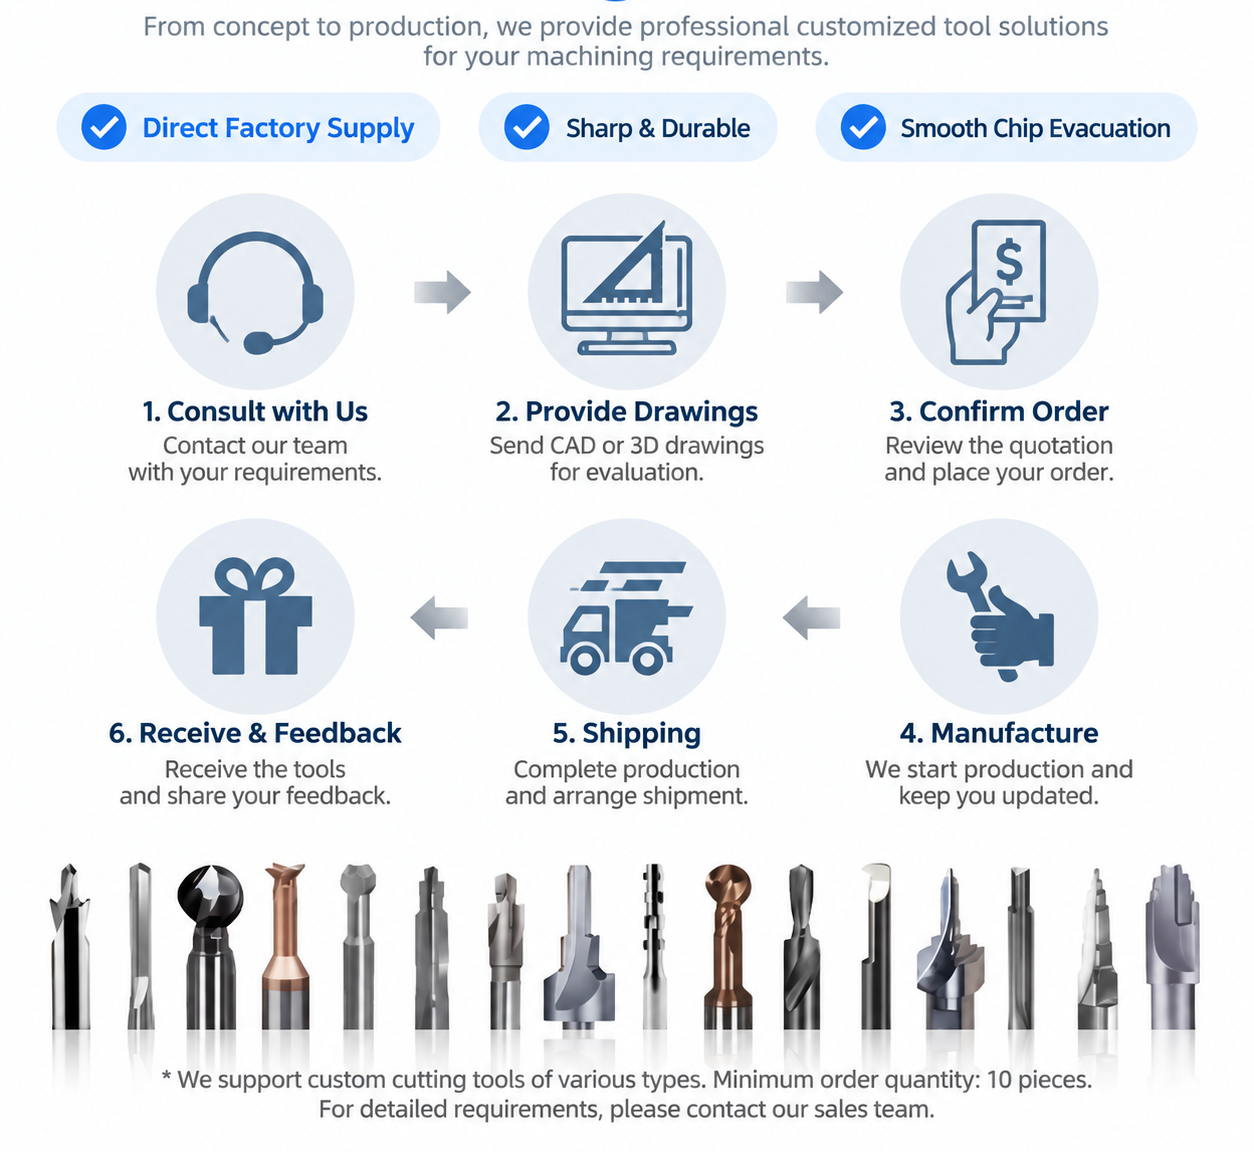
Alur Kerja OEM
Pastikan gambar, spesifikasi, bahan, dan persyaratan pengemasan.
Menyempurnakan desain alat, detail penandaan, dan persyaratan produksi.
Sediakan sampel untuk pengujian dan persetujuan sebelum produksi massal.
Lakukan produksi dan pemeriksaan sesuai dengan persyaratan yang telah disepakati.
Dukungan Merek Pribadi bagi Distributor
Bagi para distributor dan pengecer perkakas, kami menyediakan dukungan merek sendiri yang fleksibel, termasuk penandaan khusus, solusi pengemasan, dan dokumentasi produk, guna membantu membangun rangkaian produk perkakas yang profesional.
Kami menerapkan prosedur pengendalian mutu yang ketat, mulai dari pemeriksaan bahan baku hingga pengiriman akhir. Setiap alat diperiksa untuk memastikan dimensi yang konsisten, kinerja pemotongan yang optimal, dan kualitas yang dapat diandalkan untuk aplikasi pemesinan industri.
Proses Pengendalian Mutu
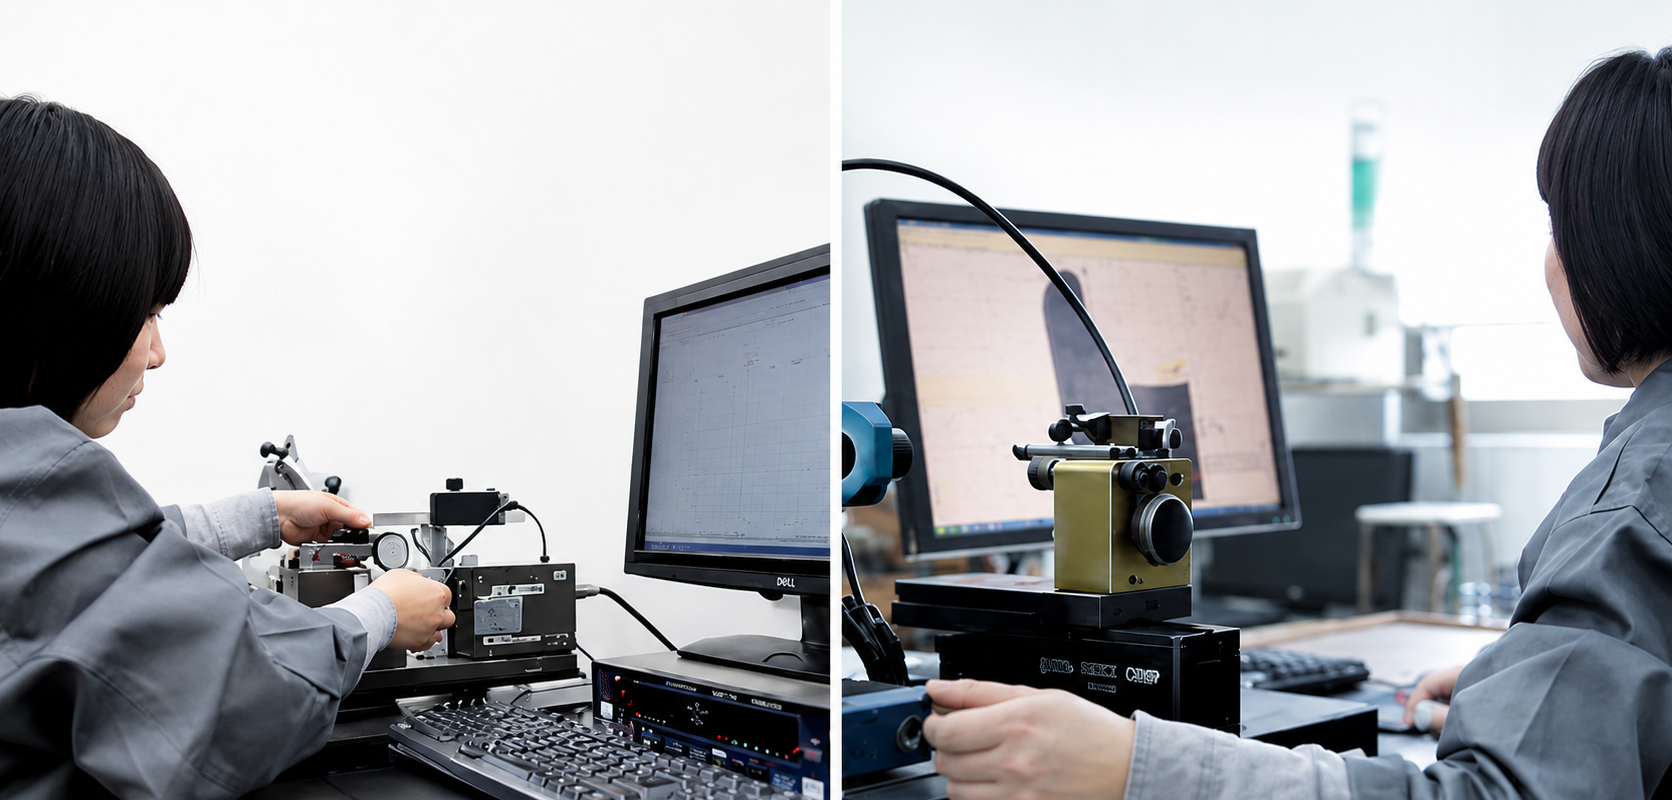
Pastikan kualitas dan konsistensi bahan karbida sebelum proses produksi.
Mengontrol geometri alat, dimensi, dan ketepatan tepi potong selama proses produksi.
Periksa kualitas tepi dan hasil akhir permukaan untuk menjaga kinerja pemotongan yang stabil.
Pastikan spesifikasi produk sebelum pengepakan dan pengiriman.
Standar Pemeriksaan
| Poin Pemeriksaan | Tujuan |
|---|---|
| Pemeriksaan Bahan | Pastikan kualitas karbida dan konsistensi bahannya. |
| Pemeriksaan Dimensi | Pastikan ukuran alat dan persyaratan toleransi. |
| Pemeriksaan Terkini | Periksa geometri tepi dan kualitas permukaan. |
| Pemeriksaan Akhir | Pastikan produk memenuhi spesifikasi yang telah ditetapkan sebelum pengiriman. |
Pengemasan & Perlindungan
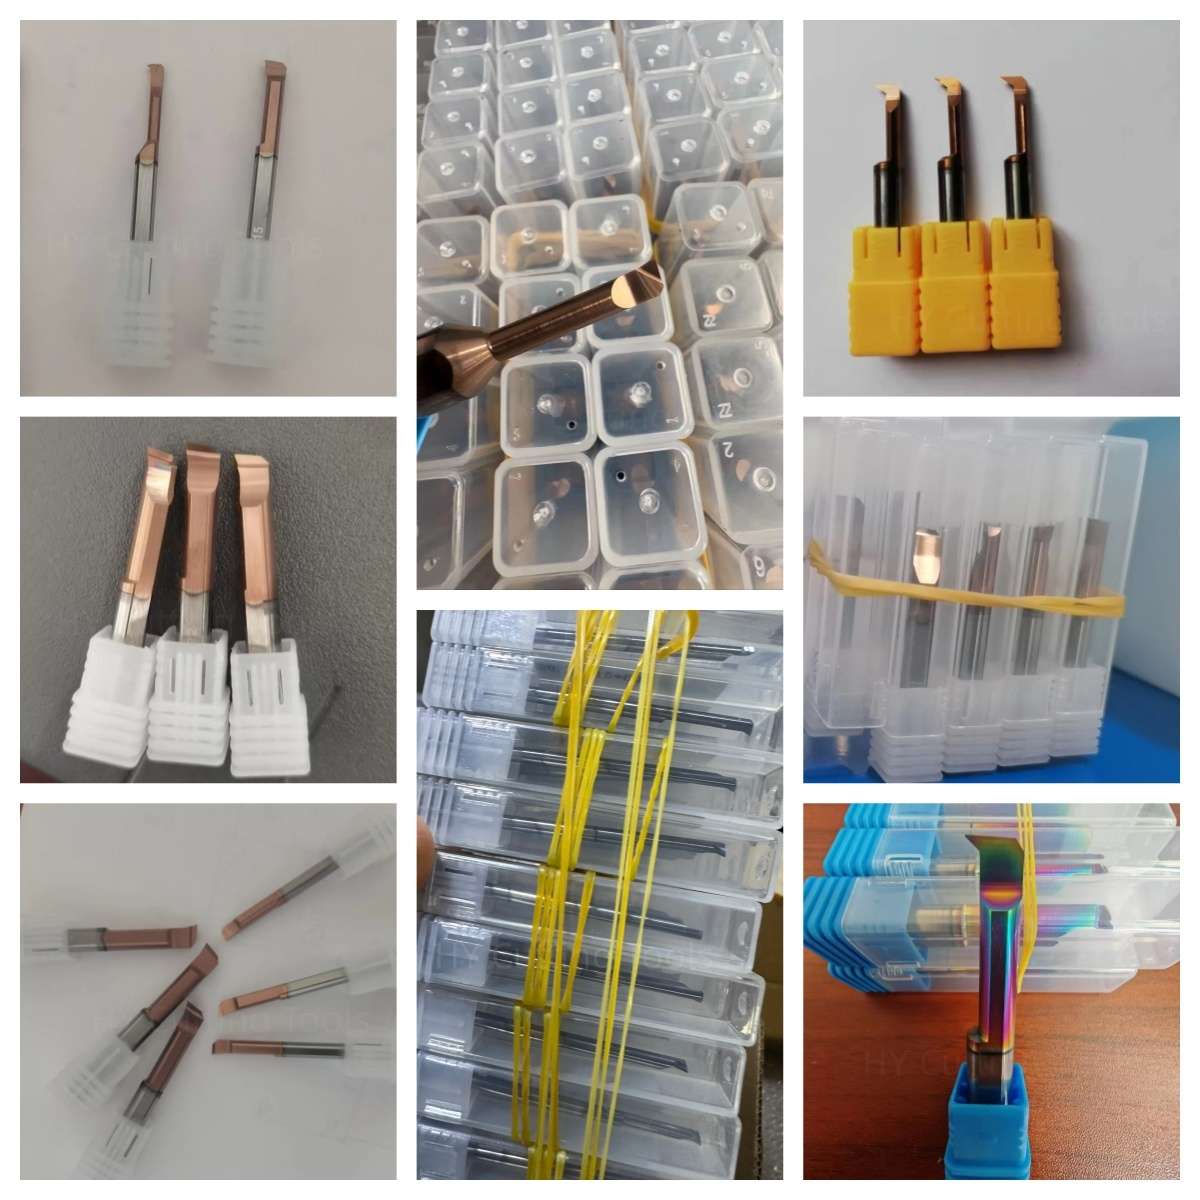

Perlindungan individual dan kemasan ekspor membantu mencegah kerusakan alat selama penyimpanan dan pengangkutan internasional.
- Perlindungan alat secara individual
- Label identifikasi produk
- Dukungan penelusuran batch
- Perlindungan pengiriman ekspor
Alur Kerja Produksi & Pengiriman
Konfirmasi Pesanan
Penjadwalan Produksi
Pemeriksaan Kualitas
Pengemasan
Pengiriman
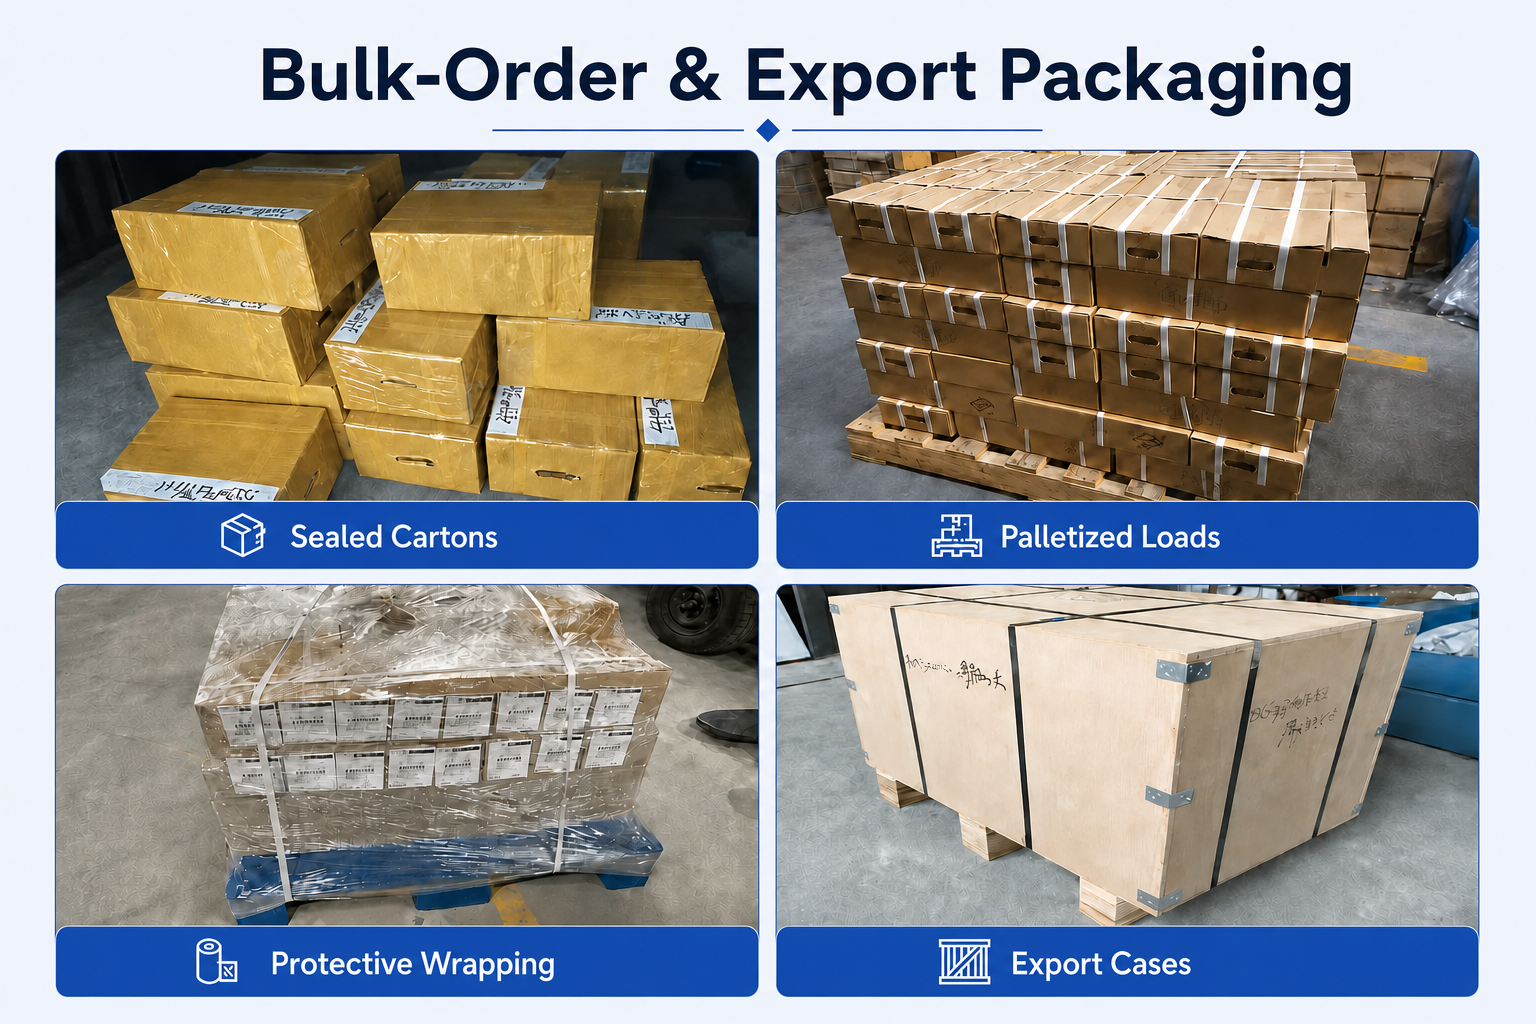

Dukungan Pengiriman
Produk standar biasanya dapat dikirim dalam waktu 1–3 hari kerja setelah konfirmasi pesanan. Produk yang dipesan khusus memerlukan konfirmasi berdasarkan desain cetakan, jumlah, dan persyaratan produksi.
Pertanyaan Umum & Unduhan
Pertanyaan Umum tentang Produk
What are MIR 29° ACME micro internal threading bars used for?
They are solid carbide right-hand tools for machining compatible 29° ACME internal thread profiles in small or restricted bores. Typical components include lead nuts, adjusting nuts, compact actuators, positioning mechanisms and other power-transmission parts.
What does A29 mean in the model designation?
A29 identifies the 29° included cutting profile used for compatible ACME threads. It should not be substituted for a 30° trapezoidal, 55° imperial or 60° metric threading tool.
Which thread sizes are available in the standard series?
The standard range includes 16, 14, 12, 10, 8, 6 and 5 TPI models. Each model is intended for its stated threads-per-inch value, so the required TPI must be confirmed before ordering.
What standard dimensions are available?
Standard models cover cutting diameters d1 from Ø3.9 to Ø11.9 mm, clearance lengths L1 from 15 to 50 mm, shank diameters from Ø4 to Ø12 mm and overall lengths from 50 to 100 mm.
Does cutting diameter d1 equal the minimum bore diameter?
No. The d1 value is a tool dimension. Minimum bore suitability depends on the complete thread geometry, minor diameter, thread depth, entry clearance and tool retraction path, so the component drawing should be checked before selection.
Are these standard tools right-hand or left-hand?
The listed MIR A29 models are right-hand internal threading bars. If the machine layout or toolpath requires a left-hand configuration, submit the drawing and machining direction for a custom-tool review.
Pertanyaan Umum (FAQ) tentang Seleksi & Pendaftaran
How do I select the correct MIR 29° ACME threading bar?
Confirm the complete ACME thread designation, General Purpose or Centralizing form where applicable, nominal diameter, TPI, thread class, hand, required thread length, bore geometry and available clearance. Then select the matching TPI and the shortest practical L1.
Can one tool machine different ACME TPI values?
The standard tools are TPI-specific and should be matched to the required thread. Do not use a 16-TPI model to cut a 14-, 12-, 10-, 8-, 6- or 5-TPI thread.
How should I choose the clearance length L1?
Choose an L1 long enough to reach the full thread and provide safe entry and retraction clearance. Use the shortest practical reach because excessive overhang reduces rigidity and may increase chatter or thread-form error.
How can I improve stability when cutting an internal ACME thread?
Minimize tool overhang, clamp the shank securely, verify center height and runout, and use a multi-pass threading cycle with controlled infeed. Start conservatively and adjust speed, pass depth and the finishing passes according to material, rigidity and thread size.
Is coolant recommended for small-bore ACME threading?
Suitable coolant or air-assisted chip evacuation is recommended when the material and machine permit it. Direct the flow toward the cutting zone and confirm that chips can leave the bore without being recut or packed into the finished thread.
What should be checked before running the CNC threading cycle?
Verify the spindle direction, tool hand, programmed TPI, thread start position, infeed method, final depth, relief or runout space and retract path. A dry run or single-block check is recommended for a new program.
Pertanyaan Umum (FAQ) tentang Pemesanan & OEM
Can you manufacture custom 29° ACME internal threading bars?
Yes. Custom thread diameter, TPI, thread form, cutting diameter, clearance length, shank diameter, overall length, carbide grade, coating and cutting geometry can be reviewed according to drawings or samples.
Informasi apa saja yang diperlukan untuk mendapatkan penawaran harga?
Please provide the standard model or component drawing, complete ACME designation, nominal diameter, TPI, thread class and hand, bore dimensions, thread length, workpiece material, quantity and any coating, marking or packaging requirements.
Can I order mixed models for application testing?
Yes. The standard minimum order quantity is 10 pieces, and mixed-model or sample requirements can be reviewed according to the selected TPI values, sizes and available stock.
Do you provide OEM and private-label service?
Yes. Laser marking, labels, packaging and distributor private-label requirements can be supplied subject to order quantity and artwork confirmation.
What is the lead time for standard and customized tools?
In-stock standard models can usually be dispatched within 1–3 working days after order confirmation. Custom tools require separate lead-time confirmation based on geometry, TPI, coating, quantity and production requirements.
Sumber Daya Teknis
Butuh informasi mengenai ukuran, harga, atau opsi khusus?
Kirimkan kepada kami jenis alat yang dibutuhkan, ukuran, jumlah, bahan benda kerja, serta persyaratan OEM atau khusus apa pun. Kami akan mengonfirmasi spesifikasi yang sesuai, ketersediaan, waktu tunggu, dan rincian penawaran harga.
Gambar, daftar ukuran, dan foto referensi sangat kami harapkan.