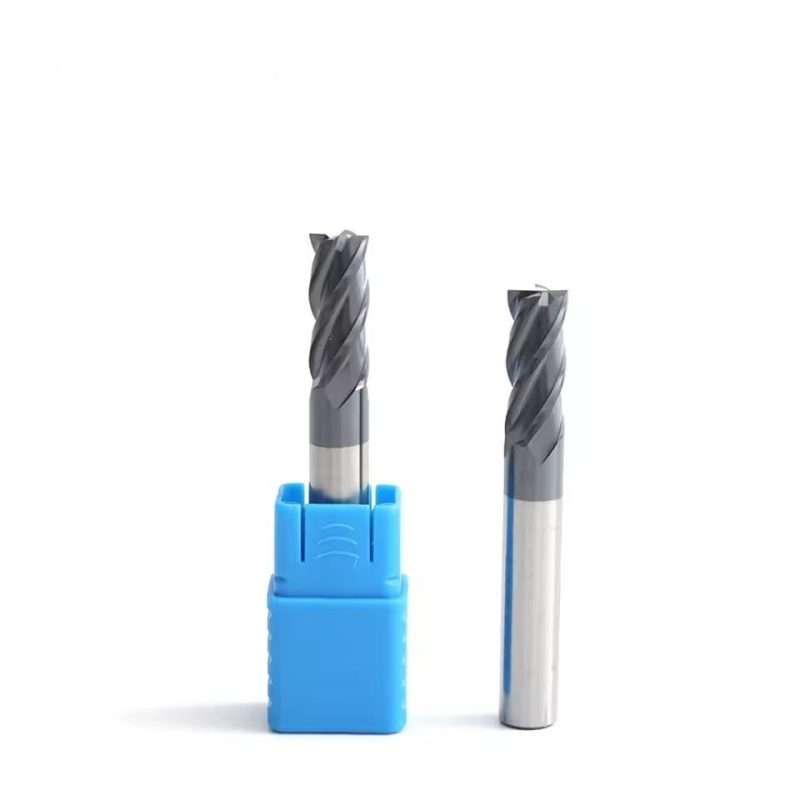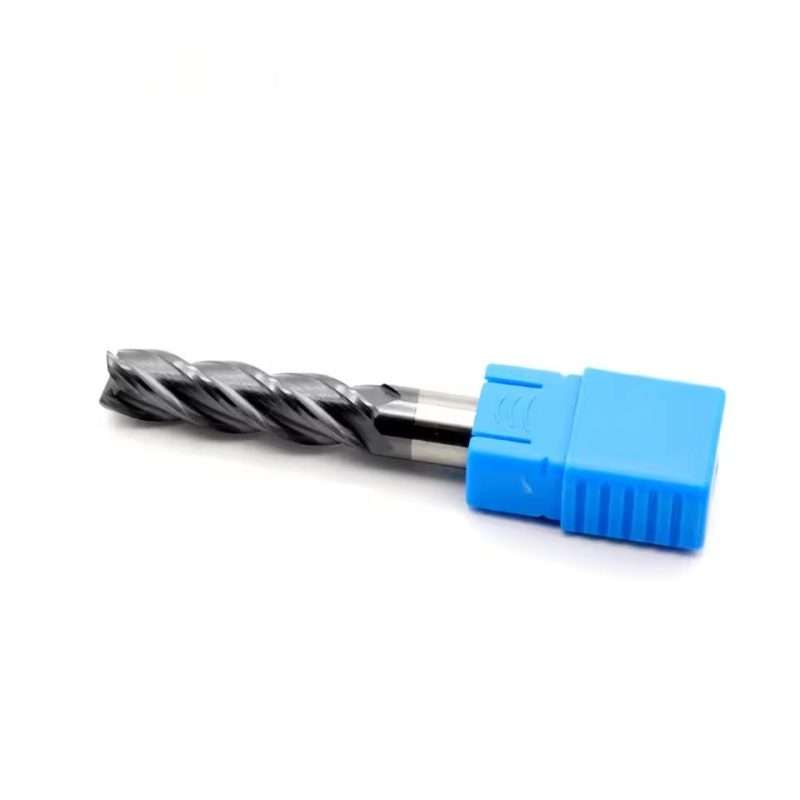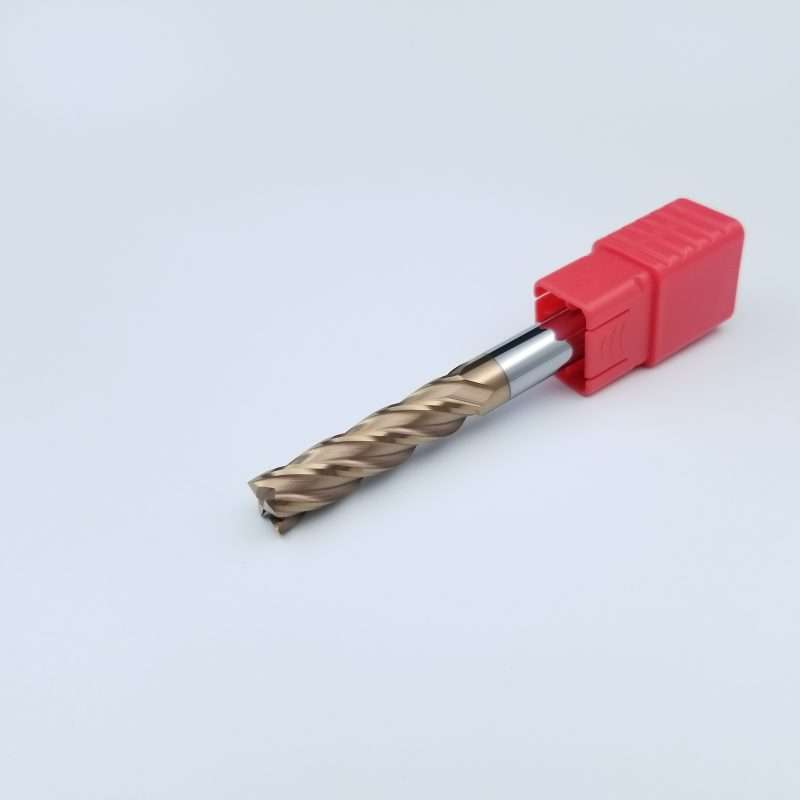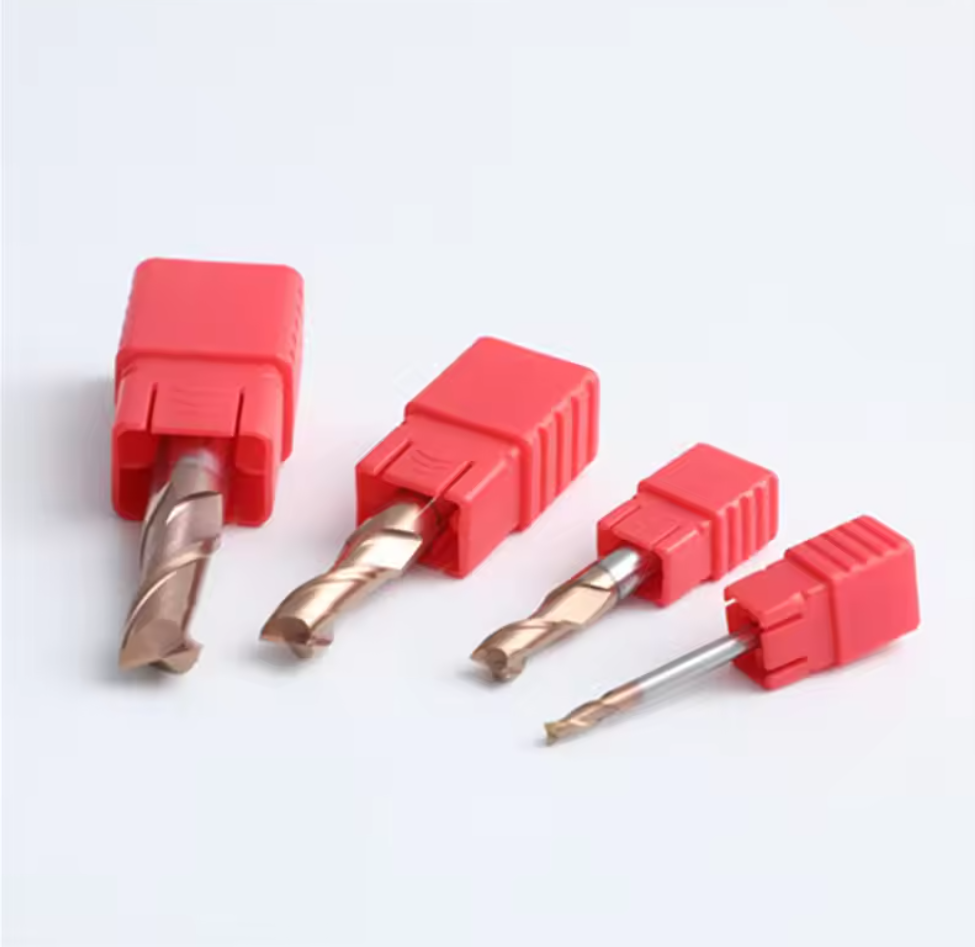
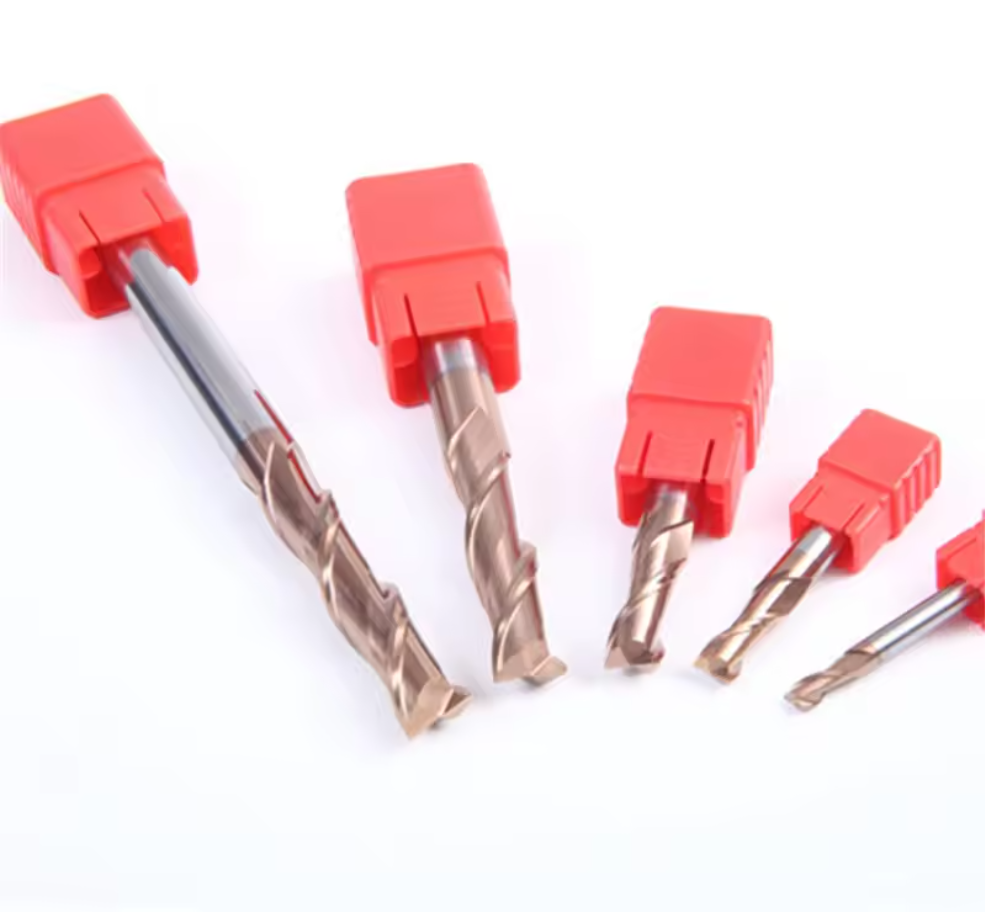

HRC55 Çelik İçin 2 Kanallı Katı Karbür Kare Uçlu Freze
Steel up to HRC55
Stable milling in medium-hard steels.
Efficient Chip Clearance
Wide flutes support smooth chip evacuation.
Stable Cutting
Balanced geometry supports consistent machining.
Coated for Steel
Wear-resistant coating supports reliable tool life.
HRC55 2-Flute Solid Carbide Square End Mill Overview
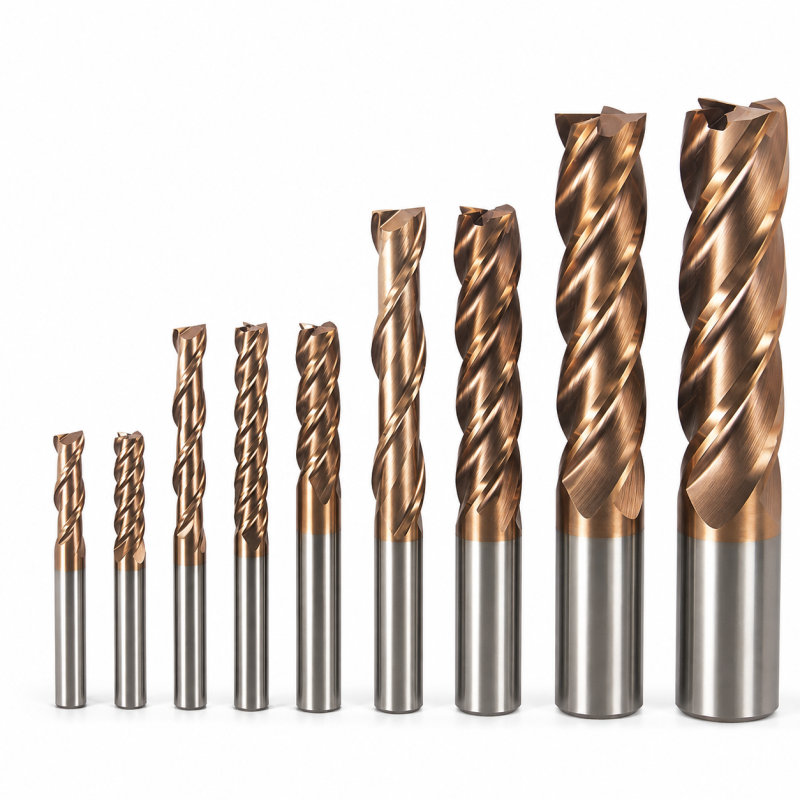
This HRC55-series 2-flute solid carbide square end mill is designed for slotting, side milling, shoulder milling and selected semi-finishing operations in carbon steel, alloy steel and pre-hardened steel. Its square-end geometry supports flat-bottom features and 90° shoulders, while the two-flute configuration provides generous chip space for full-width slotting and stable chip evacuation. Standard cutting diameters range from Ø1 to Ø20 mm, with AlTiN, TiSiN and application-specific coating options available according to the steel grade and machining conditions.
Key Configuration
Square-End Cutting Profile
Designed for flat-bottom slots, pockets and 90° shoulder features.
Two-Flute Chip Space
Generous flute space supports chip evacuation during slotting and side milling.
Steel-Matched Coating
AlTiN, TiSiN or application-specific coatings can be selected according to steel grade and hardness.
Key Product Advantages
Defined Square Features
The square-end profile supports flat-bottom slots and controlled 90° shoulders.
Efficient Chip Evacuation
Two flutes provide chip space for full-width slotting and side-cutting operations.
Precision-Ground Edges
Controlled cutting edges support stable engagement and consistent surface quality.
Steel-Series Configuration
Carbide, edge preparation and coating are configured for confirmed steel conditions.
Milling Operations
The two-flute square-end geometry supports multiple steel-milling operations. Final cutting conditions should be matched to tool diameter, flute length, workpiece hardness and machine rigidity.
RECOMMENDED
RECOMMENDED
RECOMMENDED
SUITABLE
Workpiece Material Compatibility
| MATERIAL GROUP | EXAMPLES | APPLICATION LEVEL |
|---|---|---|
| P Steel | Carbon steel and low-alloy steel | Primary application |
| P Alaşımlı Çelik | Medium-alloy and tool steels | Confirm grade and hardness |
| H Ön Sertleştirilmiş Çelik | Confirmed pre-hardened steel conditions | Application review required |
Product Details & Milling Demonstration
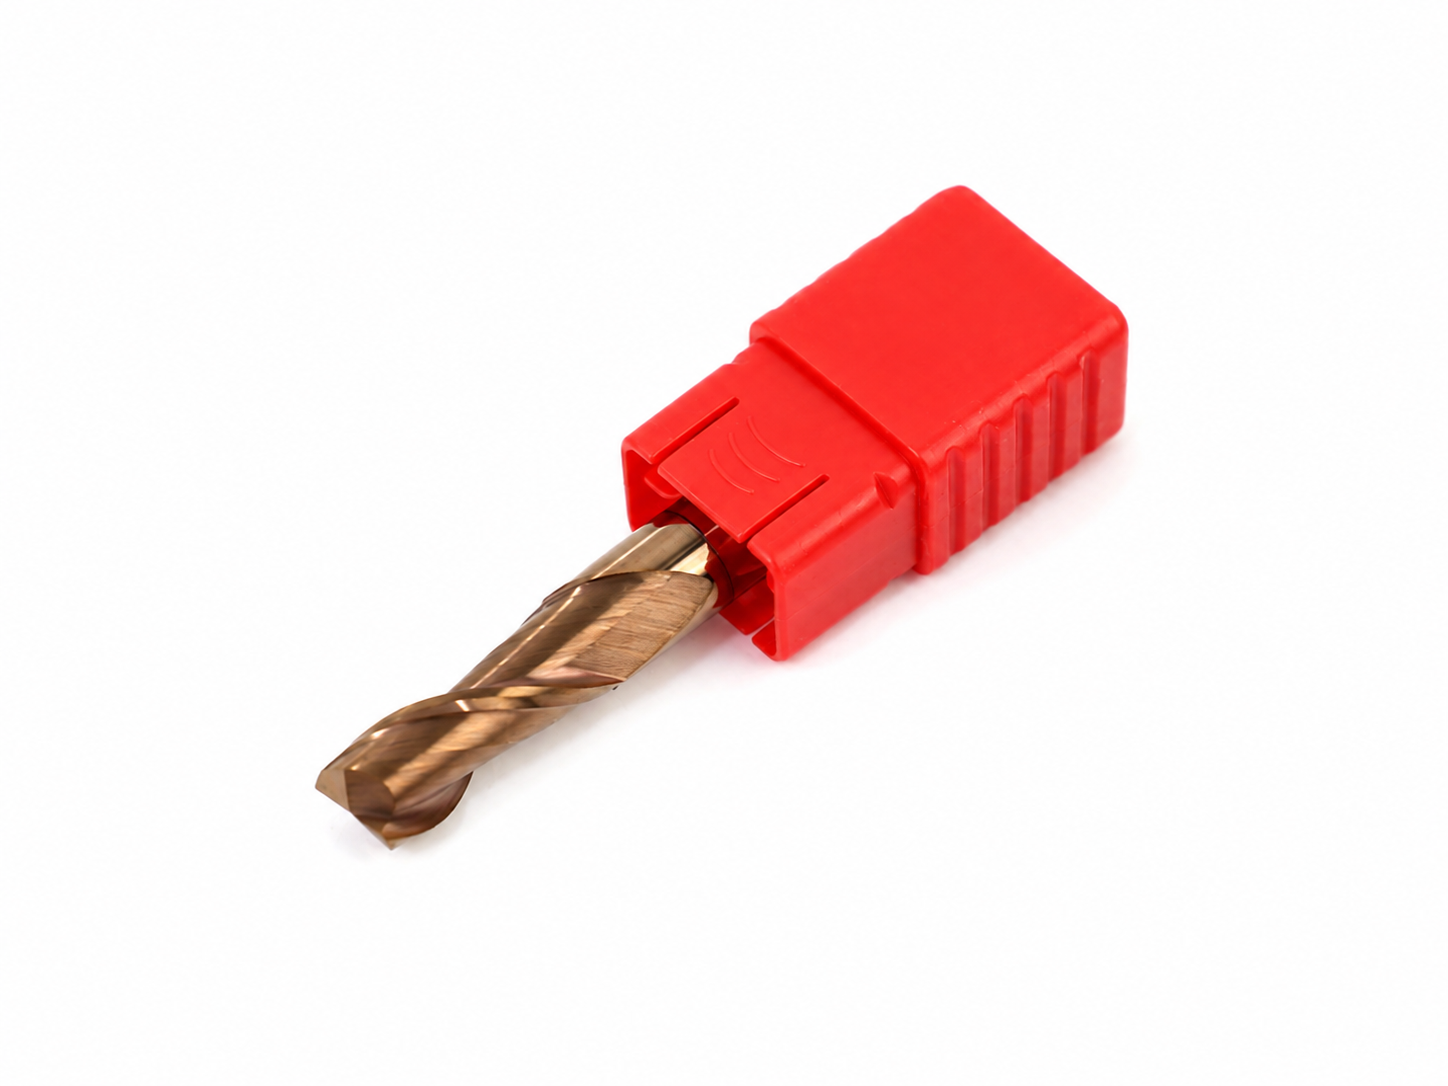
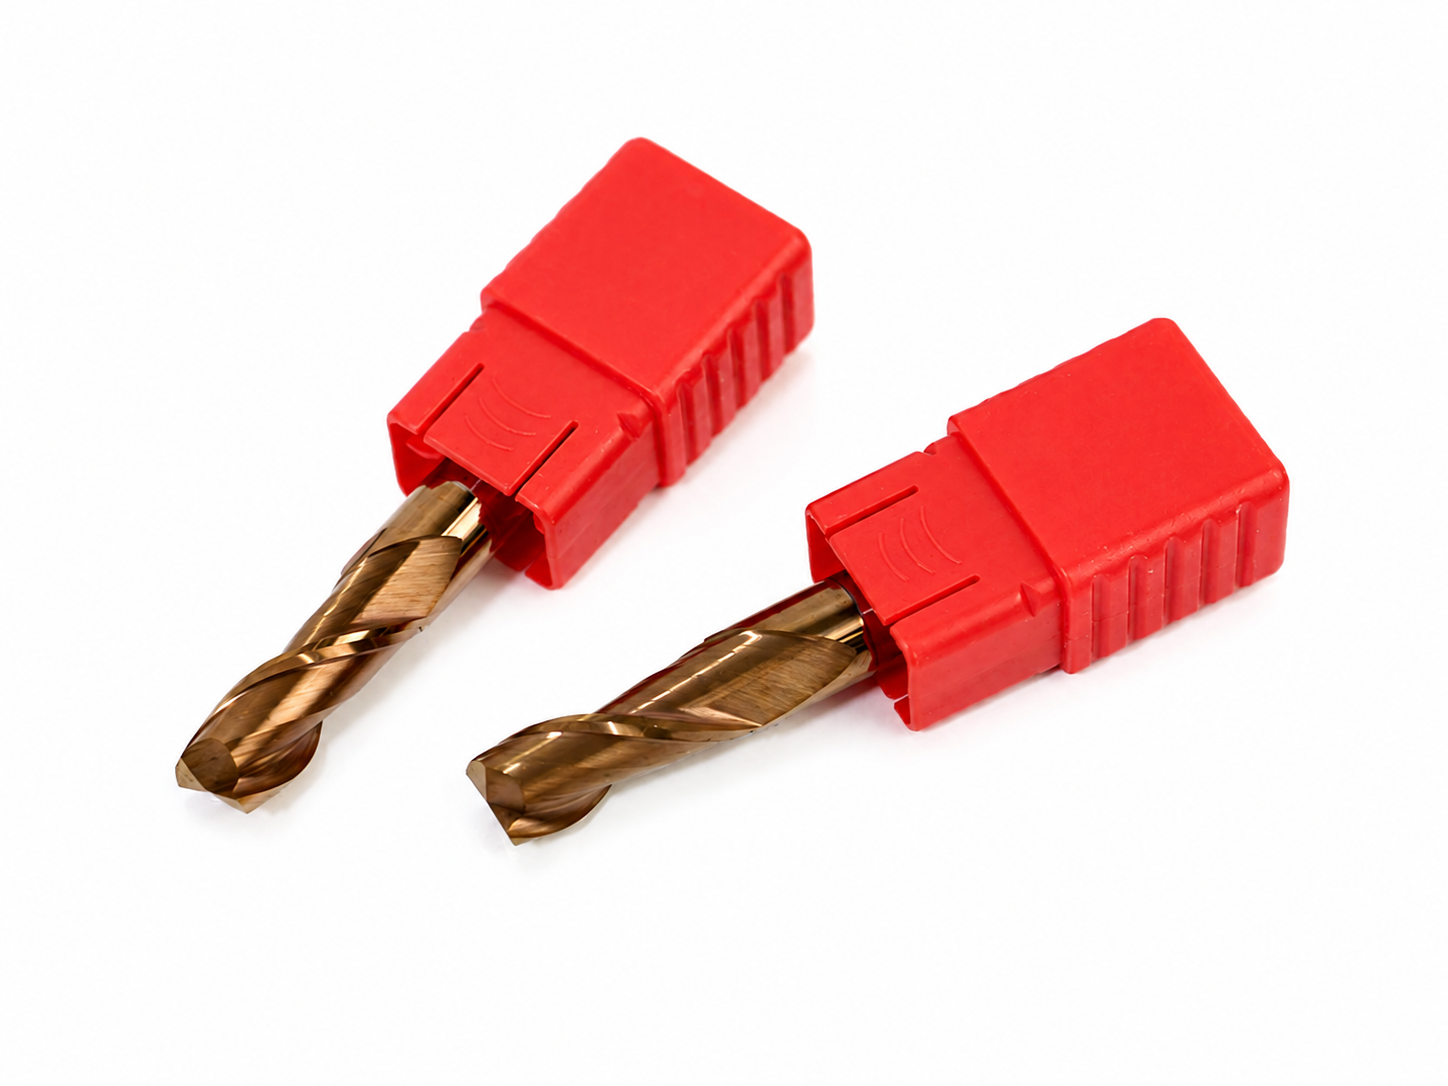
Detailed product views and a machining demonstration of the HRC55 2-flute solid carbide square end mill for steel.
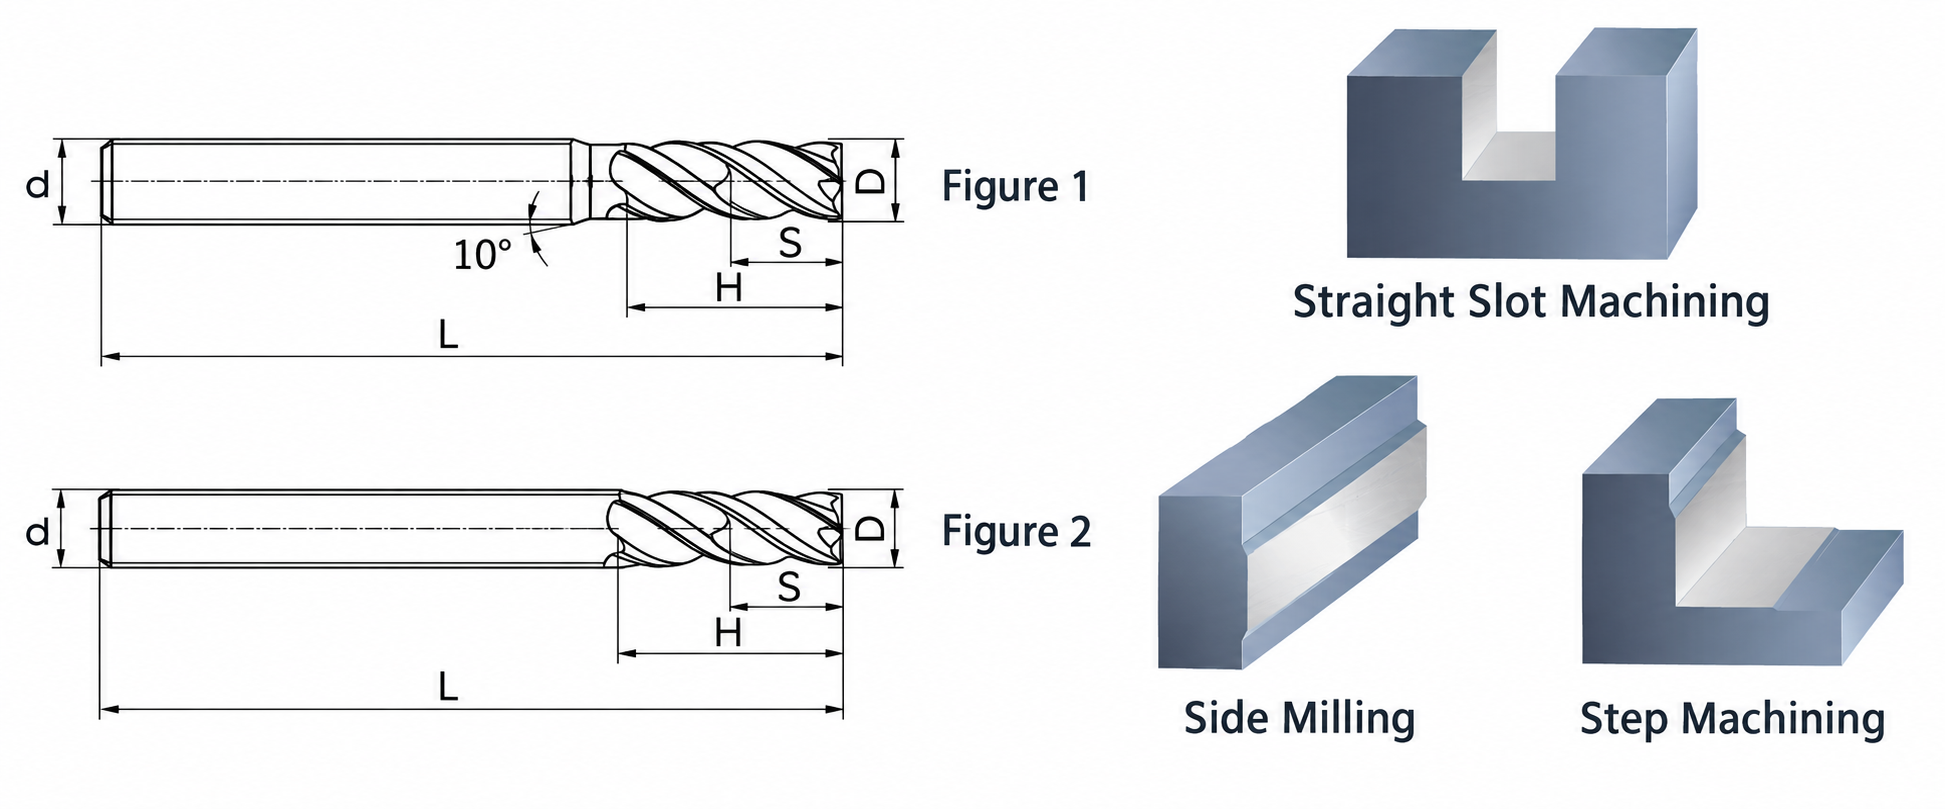
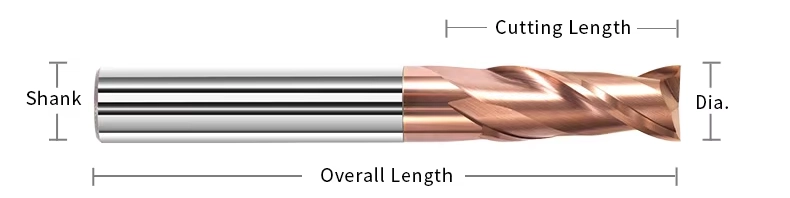
Tool Nomenclature & Dimensions
Reference dimensional nomenclature and standard configurations for the HRC55 2-flute solid carbide square end mill. All listed dimensions are in millimeters.
Technical Configuration
| PARAMETRE | SPECIFICATION |
|---|---|
| Alet Malzemesi | İnce Taneli Katı Karbür |
| Profil Sonu | Square / Flat End |
| Flüt Sayısı | 2 Flüt |
| Helezon Açısı | 35° / 38° |
| Series Positioning | HRC55 Series |
| Kaplama Seçenekleri | AlTiN / TiSiN / Application-Specific Coating |
| Cutting Direction | Sağ El Kesim |
| Çap Aralığı | Ø1–Ø20 mm Standard Range |
| Uzunluk Seçenekleri | Standard / Long Series / Drawing-Based Custom |
| Primary Materials | Carbon Steel / Alloy Steel / Confirmed Pre-Hardened Steel |
| Center Cutting | Confirm by Specific Configuration |
| Coolant Method | Air Blow / Oil Mist / External Coolant According to Application |
Standard Size Matrix
Reference standard sizes retained from the original product information. Custom cutting diameters, flute lengths, shank diameters and overall lengths are available after drawing review.
| SPECIFICATION | DC / d | APMX / ℓ | DCON / D | OAL / L |
|---|---|---|---|---|
| Ø1×3×4D×50L | 1 | 3 | 4 | 50 |
| Ø2×6×4D×50L | 2 | 6 | 4 | 50 |
| Ø3×9×4D×50L | 3 | 9 | 4 | 50 |
| Ø4×12×4D×50L | 4 | 12 | 4 | 50 |
| Ø5×13×5D×50L | 5 | 13 | 5 | 50 |
| Ø6×15×6D×50L | 6 | 15 | 6 | 50 |
| Ø8×20×8D×60L | 8 | 20 | 8 | 60 |
| Ø10×25×10D×75L | 10 | 25 | 10 | 75 |
| Ø12×30×12D×75L | 12 | 30 | 12 | 75 |
| Ø14×45×14D×100L | 14 | 45 | 14 | 100 |
| Ø20×45×20D×100L | 20 | 45 | 20 | 100 |
Recommended Starting Cutting Parameters
The values below are conservative starting references retained from the original product information. Optimize them according to tool diameter, radial engagement, axial depth, holder runout, machine rigidity and coolant conditions.
| WORKPIECE MATERIAL | HARDNESS | VC (m/min) | fz (mm/tooth) | REFERENCE OPERATION |
|---|---|---|---|---|
| Carbon Steel / Alloy Steel | Below 30 HRC | 120-180 | 0.02–0.12 | Slotting / Side Milling / Semi-Finishing |
| Pre-Hardened Steel | 30–45 HRC | 80–120 | 0.02–0.08 | Yarı Son İşlem / Son İşlem |
| Confirmed Harder Steel | 45–55 HRC | 40–70 | 0.01–0.05 | Light Semi-Finishing / Finishing |
Square End Mill Application Guidance
- Slotting: Use reduced cutting parameters compared with side milling because the cutter is engaged across its full diameter.
- Side Milling: Select axial and radial engagement according to the required material-removal rate and surface finish.
- Toolholding: Use a clean, low-runout precision holder and minimize unnecessary overhang.
- Chip Removal: Use air blow, oil mist or suitable external coolant to prevent chip recutting.
- Pocket Entry: Confirm center-cutting and ramping capability before axial plunging or helical entry.
HRC55 2-Flute Square End Mill Customization
Cutting diameter, flute length, overall length, helix angle, square-end geometry, cutting-edge preparation and coating can be configured for steel-milling applications. Standard configurations use a 2-flute design with 35° or 38° helix options, while non-standard dimensions and selected geometry adjustments can be reviewed according to the workpiece grade, hardness, milling operation, tool engagement and required dimensional accuracy.
| PARAMETRE | ÜRETİM KAPASİTELERİ |
|---|---|
| Kesim Çapı | Standard Ø1–Ø20 mm range, with selected intermediate and non-standard diameters reviewed according to the drawing |
| Flüt Sayısı | Standard 2-flute configuration with generous chip space for slotting, side milling and shoulder-milling applications |
| Flüt ve Toplam Uzunluk | Standard, long-series and drawing-defined flute, reach and overall-length configurations |
| Şaft Yapısı | Standart veya çizimde belirtilen şaft çapına ve sıkıştırma uzunluğuna sahip hassas silindirik şaft |
| Helezon Açısı | 35° or 38° standard helix options selected according to the steel grade, chip formation and milling operation |
| Kare Uçlu Geometri | Flat-bottom square-end profile for slots, pockets and 90° shoulders, with center-cutting capability confirmed by specific configuration |
| Kenar Hazırlığı | Application-matched cutting-edge preparation, end-face grinding, gash geometry and corner condition reviewed according to the steel hardness and cutting load |
| Kaplama Seçimi | AlTiN, TiSiN or application-specific coating selected according to the steel grade, hardness, cutting temperature and coolant conditions |
| Freze Uygulaması | Geometry can be reviewed for slotting, side milling, shoulder milling, semi-finishing and selected finishing operations |
| Boyutsal Tolerans | Drawing-defined requirements for cutting diameter, flute length, shank diameter, overall length, runout and square-end geometry |
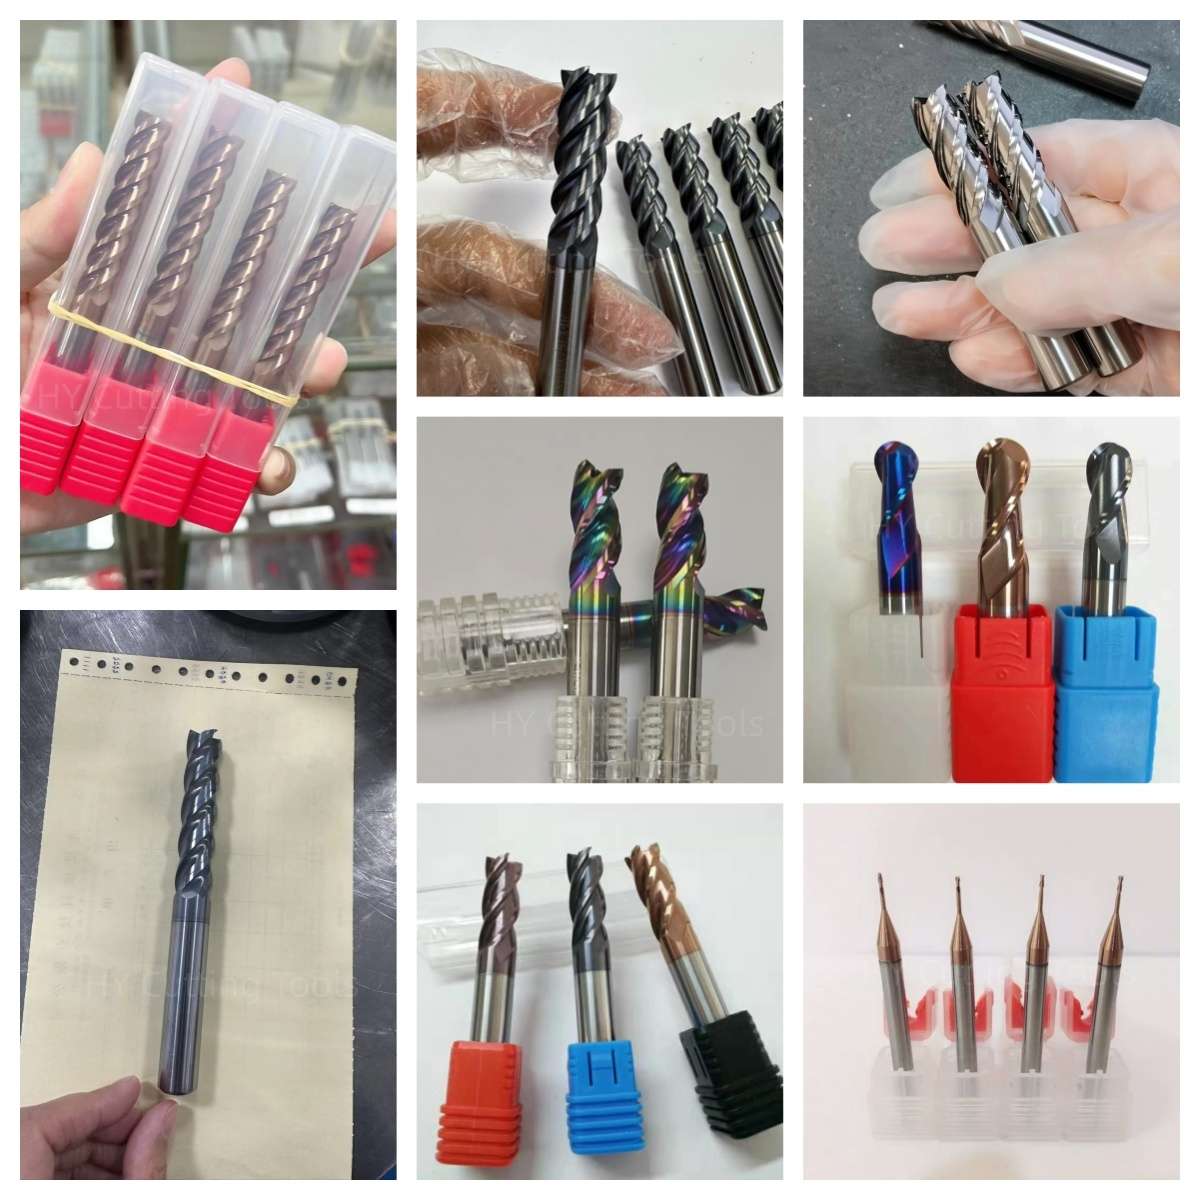
OEM ve Özel Etiket Hizmetleri
Endüstriyel distribütörler, alet markaları ve düzenli üretim yapan müşteriler için OEM üretimi ve özel etiketli tedarik seçenekleri mevcuttur. Lazerle işaretleme, etiket içeriği, koruyucu ambalaj ve kaplama sunumu, onaylanmış ürün spesifikasyonuna ve sipariş gereksinimlerine göre yapılandırılabilir.

Lazer Kazıma
Özel logolar, takım kodları, kesme boyutları, kaplama tanımları ve parti numaraları, mevcut şaft alanına göre işaretlenebilir.
Özel Etiketler ve Ambalajlar
Tek tek koruyucu tüpler, ürün etiketleri, teknik özellik detayları, renkli ambalaj tüpleri ve özel markalı ambalajlar incelenebilir.
Ticari Şartlar
Minimum sipariş miktarı (MOQ), numune değerlendirmesi, özel boyut denemeleri, tekrar siparişler ve planlı tedarik programları, seçilen konfigürasyona göre teyit edilir.
Teknik İş Akışı
Üretim öncesinde standart, özel tasarım ve özel markalı kare uçlu frezelerin gereksinimlerini doğrulamak için yapılandırılmış bir inceleme süreci uygulanmaktadır.
Sorgulama
Malzeme, sertlik, frezeleme işlemi, boyutlar, tolerans ve miktarı belirtiniz.
Mühendislik
Flüt geometrisini, sarmal açısını, kenar hazırlığını, kaplamayı, ap ve ae değerlerini gözden geçirin.
Ticari
Teklifi, minimum sipariş miktarını (MOQ), numune şartlarını, üretim takvimini ve teslimat koşullarını teyit edin.
Üretim
CNC taşlama, uç yüzey şekillendirme, kenar hazırlama, kaplama ve lazerle işaretleme.
Kalite Kontrolü
Çapı, oluk uzunluğunu, şaftı, eksantrikliği, kare uç geometrisini ve kesme kenarlarını kontrol edin.
Kalite, Denetim ve Teslimat
HRC55 2-flute solid carbide square end mills are controlled through material verification, precision grinding, in-process measurement and final inspection. Key dimensions, square-end geometry, cutting-edge condition, coating appearance and product identification are reviewed according to the approved specification or drawing before packing.
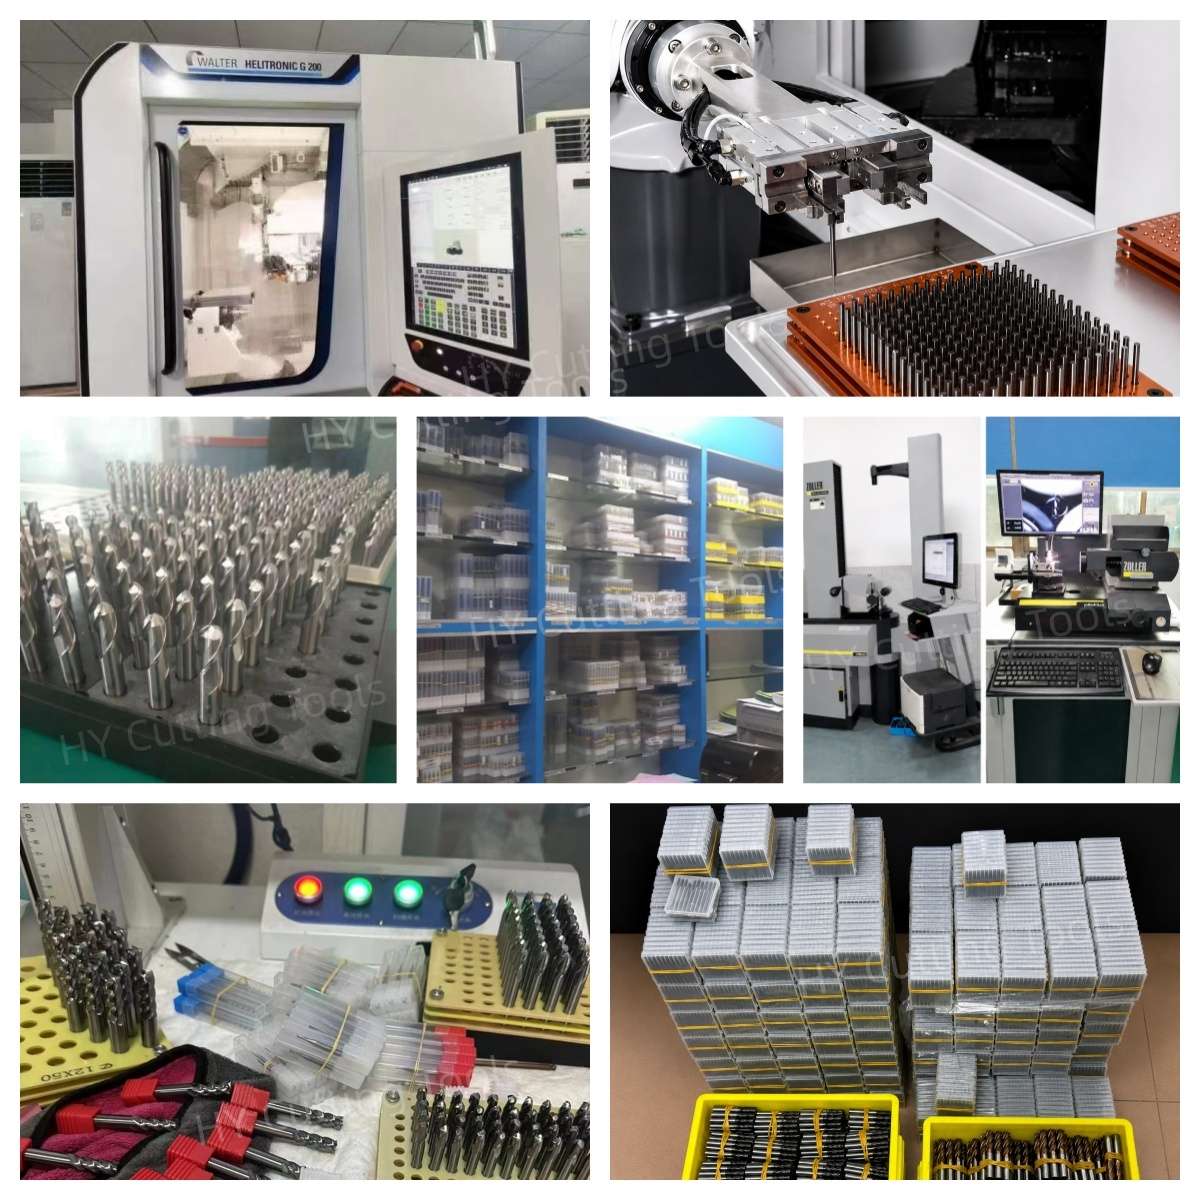
Üç Aşamalı Kalite Kontrolü
Üretim sürecinin çeşitli aşamalarına, boyutsal tutarlılığı sağlamak ve tekrar sipariş kontrolünü desteklemek amacıyla denetim noktaları yerleştirilmiştir.
Gelen Malzeme Kontrolü
Karbür alt tabaka kalitesi, ham parça boyutları ve tedarik edilen malzeme bilgileri, üretim gereksinimleriyle karşılaştırılarak kontrol edilir.
Üretim Sırasında Taşlama Kontrolü
CNC taşlama işlemi sırasında kesme çapı, oluk geometrisi, oluk uzunluğu, kare uç profili ve şaft boyutları izlenir.
Son Alet Kontrolü
Üretimi tamamlanmış takımlar, belirtilen boyutlar, eksantriklik, kesici kenar durumu, kaplama görünümü, işaretleme ve ambalaj tanımlaması açısından incelenir.
Temel Denetim Özellikleri
Denetim gereklilikleri, standart ürün şartnamesine veya onaylanmış özel çizime göre teyit edilir.
| DENETİM KONUSU | KONTROL ODAĞI | ONAY ESASLARI |
|---|---|---|
| Kesme Çapı (DC) | Çap ve boyut tutarlılığı | Standart teknik şartname veya onaylı çizim |
| Flüt Uzunluğu (APMX) | Etkili kesme uzunluğu | Onaylanmış ürün boyutu veya çizim gereksinimi |
| Şaft Çapı (DCON) | Sıkıştırma kesitinin boyutu ve yüzey durumu | Uygun şaft özellikleri |
| Toplam Uzunluk (OAL) | Toplam alet uzunluğu | Standart boyutlu matris veya onaylanmış çizim |
| Radyal Salgı | Kesme bölümü ile şaft arasındaki eşmerkezlilik | Kararlaştırılan denetim şartı |
| Kare Uçlu Geometri | Uç yüz profili, köşe durumu ve merkez kesim şekli | Seçilen araç yapılandırması |
| Flüt ve Heliks Profili | Flüt sayısı, sarmal şekli ve taşlama tutarlılığı | Onaylanmış üretim konfigürasyonu |
| Son Teknoloji ve Kaplama | Kenar durumu, gözle görülür kusurlar ve kaplama görünümü | Uygulamaya özgü üretim gereksinimi |
| İşaretleme ve Tanımlama | Uygun olduğu durumlarda alet kodu, boyutlar ve parti bilgileri | Onaylanmış sipariş ve paketleme özellikleri |
Ölçüm ve Parti İzlenebilirliği
Optik ölçüm sistemleri, takım kontrol ekipmanları ve uygun boyutsal ölçüm aletleri, kontrol edilecek özelliğe göre seçilir.
Optik Ölçüm
Belirtilen kesme özelliklerinin profil ve boyut incelemesi.
Çıkma Kontrolü
Kararlaştırılan ürün gereksinimlerine dayalı eşmerkezlilik incelemesi.
Kenar Denetimi
Uç yüzeyi, köşeler ve kesici kenarın durumuna ilişkin detaylı inceleme.
Parti Tanımlama
Tekrarlanan tedarik için gerekli olan yerlerde sipariş, ürün ve parti bilgileri birbiriyle ilişkilendirilmiştir.
Koruyucu Ambalajlama Süreci
Hazır uçlu frezeler, kesici kenarlar arasındaki teması azaltmak ve depolama ile nakliye sırasında ürünün net bir şekilde tanımlanmasını sağlamak amacıyla korunmaktadır.

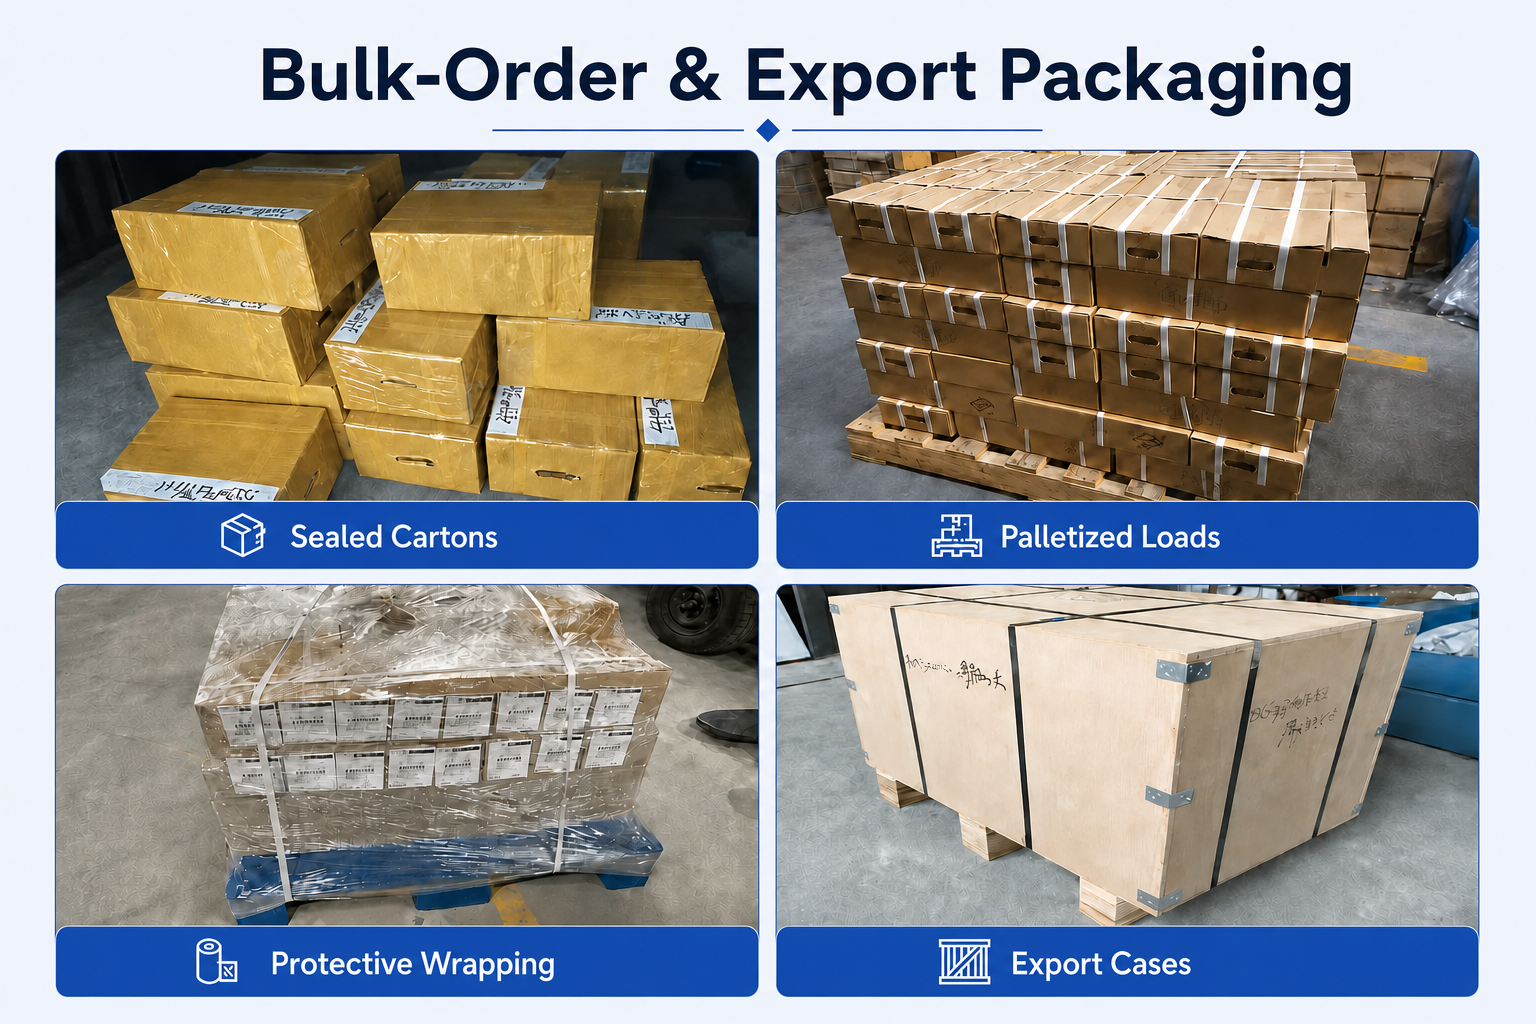
Toplu Sipariş ve İhracat Ambalajı
Toplu sevkiyatlar, sipariş miktarına, sevkiyat ağırlığına ve kararlaştırılan nakliye şartlarına göre, takviyeli karton kutular, koruyucu ambalaj, paletli yükleme veya ihracat kasaları kullanılarak düzenlenebilir.
Teslimat Koordinasyonu
Üretimin tamamlanması, paketleme yöntemi ve sevkiyat düzenlemeleri, onaylanan siparişe göre teyit edilir. Kargo, hava, deniz veya müşteri tarafından belirlenen nakliye seçenekleri, sevkiyatın boyutuna ve varış noktasına göre değerlendirilebilir. Nihai teslim süresi, ürün özellikleri, miktar ve paketleme gereklilikleri onaylandıktan sonra teyit edilir.
Sık Sorulan Sorular ve İndirmeler
Review common product, application and ordering questions for the HRC55 2-flute solid carbide square end mill, then access the current end mill catalog and starting cutting-data guide.
Ürün ve Uygulama SSS'leri
Selection and application guidance for steel milling.
What materials is this HRC55 square end mill designed to machine?
It is primarily configured for carbon steel, alloy steel and confirmed pre-hardened steel applications. The exact coating and cutting parameters should be selected according to the workpiece grade, hardness, machining operation and machine rigidity.
Does HRC55 mean that every tool can machine steel at exactly 55 HRC?
HRC55 describes the product-series positioning and its upper target range under selected machining conditions. Actual suitability depends on the steel grade, operation, tool diameter, cutting data, holder condition, machine rigidity and coolant strategy. Application details should be reviewed before machining near the upper hardness range.
What operations are suitable for the 2-flute square-end design?
The square-end geometry is suitable for slotting, side milling, shoulder milling, pocketing and selected semi-finishing operations. Its flat end supports flat-bottom features and 90° shoulders, while the two-flute design provides additional chip space.
Why choose two flutes instead of four flutes for steel milling?
Two flutes provide larger flute space, which can support chip evacuation during slotting and higher-engagement cutting. Four-flute tools may provide more cutting edges for selected side-milling or finishing operations, but the correct choice depends on radial engagement, axial depth, chip control and the required surface condition.
Can this end mill perform full-width slotting and plunge cutting?
The two-flute configuration is suitable for full-width slotting when cutting parameters and chip evacuation are correctly controlled. Plunge capability depends on the specific center-cutting geometry, so center-cutting availability should be confirmed for the selected size or custom configuration.
Which coating should be selected for steel machining?
AlTiN, TiSiN or another application-specific coating may be selected according to the steel grade, hardness, cutting temperature and machining conditions. The coating should be matched with the carbide substrate and edge preparation rather than selected by color alone.
Sipariş ve Özelleştirme ile İlgili Sık Sorulan Sorular
Information for distributors, tooling brands and customers requesting standard or drawing-based configurations.
Hangi standart boyutlar mevcuttur?
The reference series covers selected cutting diameters from Ø1 to Ø20 mm with standard and long-series configurations. Final availability should be confirmed by cutting diameter, flute length, shank diameter, overall length, helix angle and coating.
Standart dışı boyutlarda veya geometride ürünler üretilebilir mi?
Yes. Selected cutting diameters, flute lengths, overall lengths, shank configurations, helix angles, edge preparation and coatings can be reviewed according to the drawing and machining application. Custom dimensions and tolerances are confirmed before production.
OEM etiketleme ve özel markalı ambalajlama seçenekleri mevcut mu?
Laser marking, tool codes, custom labels, protective tubes and private-label packaging can be reviewed according to the available marking area, order quantity and confirmed packaging specification.
Doğru bir fiyat teklifi için hangi bilgiler gereklidir?
Please provide the workpiece material and hardness, cutting diameter, flute length, shank diameter, overall length, machining operation, axial and radial engagement, coating preference, tolerance requirements and order quantity. A tool drawing or component drawing is recommended for custom projects.
Teknik Dosyalar
Access current product-range information and starting cutting references for solid carbide end mill selection.
Solid Carbide End Mills Catalog
Product families, hardness series, flute options and reference sizes.
Uçlu Freze Hızları ve İlerleme Hızları Kılavuzu
Starting cutting speeds, chip loads, engagement guidance and adjustment notes.
Cutting data are starting references only. Adjust the values according to the exact tool diameter, flute count, workpiece hardness, engagement, overhang, holder condition and machine rigidity.
Boyut veya Uygulama İncelemesi mi Gerekiyor?
Send the workpiece grade, hardness, required dimensions, machining operation and quantity for configuration and quotation review.
Ölçüler, fiyatlar veya özel seçenekler mi arıyorsunuz?
Gerekli takım türünü, boyutlarını, miktarlarını, iş parçası malzemesini ve varsa OEM veya özel gereksinimleri bize iletin. Uygun teknik özellikleri, stok durumunu, teslim süresini ve fiyat teklifi ayrıntılarını size teyit edeceğiz.
Çizimler, boyut listeleri ve referans fotoğraflar memnuniyetle kabul edilir.