
U Matkap Seçim Kılavuzu: Sipariş Öncesi 9 Kontrol Noktası
A request for a “Ø25, 3D U drill” is enough to start a quotation, but it does not identify the complete tool. The shank, usable depth, insert system and coolant connection still need checking. An overlooked difference can leave the buyer with a body that does not fit the machine or inserts already in stock.
This U drill selection guide explains nine checks for buyers, tooling resellers and technical purchasers. Use it to compare a replacement, prepare a new-application inquiry and agree on a trial. If you only have a current model, purchasing list or clear photos, send those first; the remaining details can be confirmed during the review.
U Drill Selection Guide: 30-Second Review
Use these checks to identify the missing information. Do not select a model from one row alone.
| Kontrol et | Onayla | Main risk if missed |
|---|---|---|
| 1. Drilling method | Diameter, tolerance, depth and production volume | Using an indexable drill where another method fits better |
| 2. Hole and component | Through/blind, entry, exit, intersections and wall strength | Uneven loading, burrs or an incomplete depth allowance |
| 3. Diameter and L/D | Usable depth and the shortest suitable body | Insufficient reach or unnecessary deflection |
| 4. Machine and shank | Tool rotation, holder, power, torque and alignment | Wrong interface, body rubbing or unstable hole size |
| 5. Insert system | Complete body, insert, position, screw and pocket data | False compatibility from a similar shape or code |
| 6. Workpiece material | Grade, hardness, condition and matching insert | Poor chip control or premature edge failure |
| 7. Coolant and chips | Internal/external supply, pressure, flow, filtration and chip path | Chip jamming, scoring or body damage |
| 8. Cutting data | Data for the exact body, insert, diameter and condition | Applying a broad material range as a machine setting |
| 9. Replacement approval | Drawing comparison, controlled trial and acceptance criteria | Calling a candidate tool an equivalent before testing |
Tüm sütunları görmek için kaydırın.
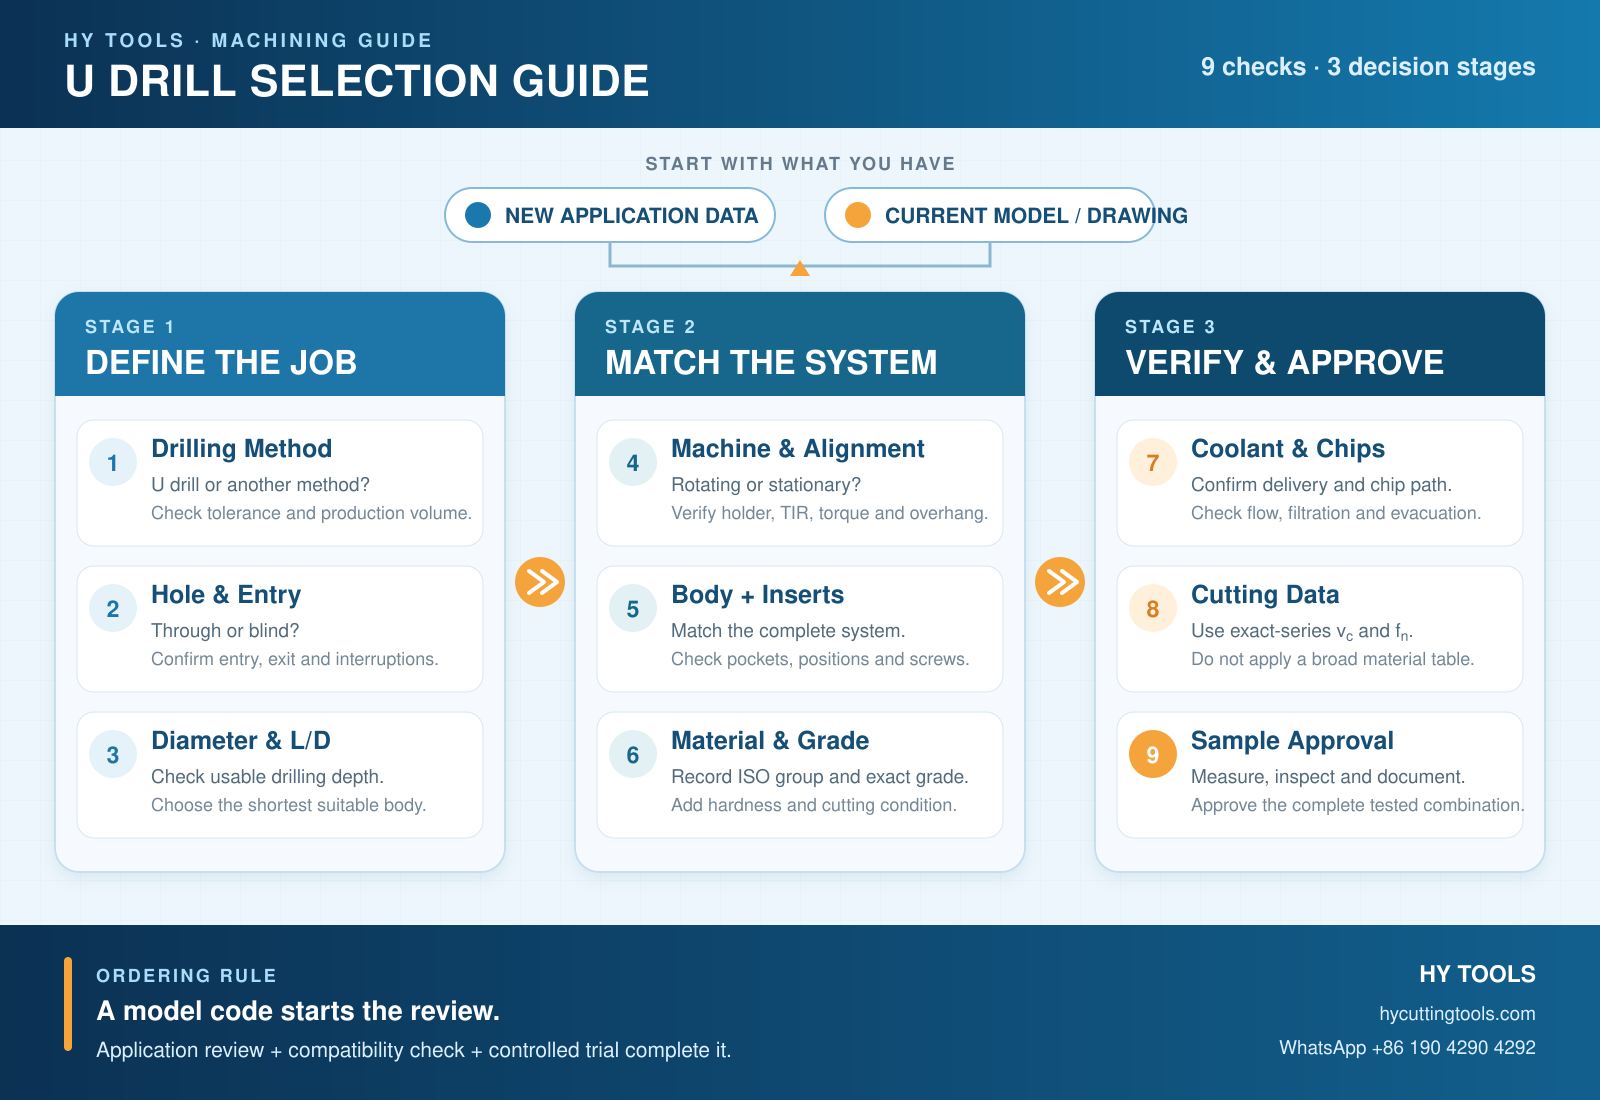
The nine checks can be grouped into three practical decision stages, as summarized below.
What Is a U Drill?
In everyday machining language, “U drill” usually refers to an indexable insert drill used for drilling from solid. Many common designs use a central insert and a peripheral insert. The central insert cuts around the drill axis, while the peripheral insert works at the outside diameter and strongly influences the finished hole wall.
The two positions do not experience the same cutting speed, load or chip formation. Sandvik Coromant’s official drilling guidance shows a characteristic centre chip and a turning-like peripheral chip. Do not assume both pockets use the same grade or geometry unless the system documentation allows it.
Check 1: Decide Whether a U Drill Is the Right Method
Confirm whether the selected drill can produce the required hole before comparing prices. Indexable, exchangeable-tip and solid carbide drills overlap in some applications, but differ in diameter range, hole capability, usable depth and replacement economics.
| Drilling method | Common strength | Verify before choosing |
|---|---|---|
| Endekslenebilir U matkap | Replaceable edges and productive drilling, particularly as diameter increases | Hole capability, machine load, chip evacuation and insert compatibility |
| Exchangeable-tip drill | Replaceable head with drill-specific geometry and size control | Head-body interface, available sizes, permitted depth and runout |
| Solid carbide drill | Useful for small-to-medium diameters, precision and application-specific designs | Diameter, coolant, coating, regrinding policy and usable length |
Tüm sütunları görmek için kaydırın.
No industry-wide rule defines one starting diameter or maximum L/D for every U drill. These limits belong to the exact product family. Confirm hole capability before comparing cost and cycle time.
Check 2: Define the Hole, Component and Entry Condition
A hole described as “Ø25 × 75 mm deep” still leaves important questions. Check the component drawing or confirm the following with the customer:
- Finished hole diameter, tolerance and surface requirement
- Drilled depth, bottom allowance and breakthrough distance
- Through, blind, stepped, pre-drilled or intersecting hole
- Flat, inclined, curved, cast or interrupted entry and exit
- Workpiece grade, hardness, condition and quantity
- Thin walls, weak sections or clamping limits near the hole
Irregular entries create uneven edge engagement. Sandvik’s irregular-surface drilling guidance recommends the shortest suitable drill and application-specific data reductions, with separate guidance for cross holes, inclined surfaces and pre-drilled holes.
Check 3: Match Diameter, L/D and the Shortest Suitable Body
L/D is drilling depth divided by nominal cutting diameter. For a body sold as 3D or 5D, verify the maximum drilling depth on the drawing and allow for the required hole bottom or breakthrough. Check overall length, shank dimensions and flute clearance as well as the nominal depth class.
Choose the shortest body that safely reaches the feature. Extra body length and overhang reduce stiffness and increase sensitivity to alignment, chip evacuation and vibration.

Check 4: Verify the Machine, Shank, Holder and Alignment
On a machining centre, the drill normally rotates. On a lathe, the workpiece may rotate while the drill remains stationary, changing the alignment and troubleshooting path.
| Setup item | What to verify | Possible symptom if missed |
|---|---|---|
| Stationary drill | Parallelism and tool centreline relative to the spindle axis | Oversize, undersize or funnel-shaped hole |
| Rotating drill | Holder, total indicator runout (TIR), spindle and clamping | Uneven wear, poor finish or reduced life |
| Machine capacity | Available torque, power and spindle-speed range | Stalling, excessive load or forced low productivity |
| Shank and interface | Shank diameter/length, flats or orientation, holder and coolant entry | Incorrect clamping, leakage or lost insert orientation |
| Tool overhang | Shortest safe gauge length and a rigid holder | Vibration, deflection or drill-body rubbing |
Tüm sütunları görmek için kaydırın.
For stationary drilling, follow a system-specific alignment procedure. Sandvik’s non-rotating drilling guide explains why centreline alignment, TIR and turret deflection must be checked rather than treated only as a speed-and-feed problem.
Check 5: Confirm the Complete U Drill Insert System
If the aim is to keep the inserts already in stock, compare the complete body and insert system before ordering another body. Record the insert designation, size, geometry or chipbreaker, grade and position, together with pocket and screw details.
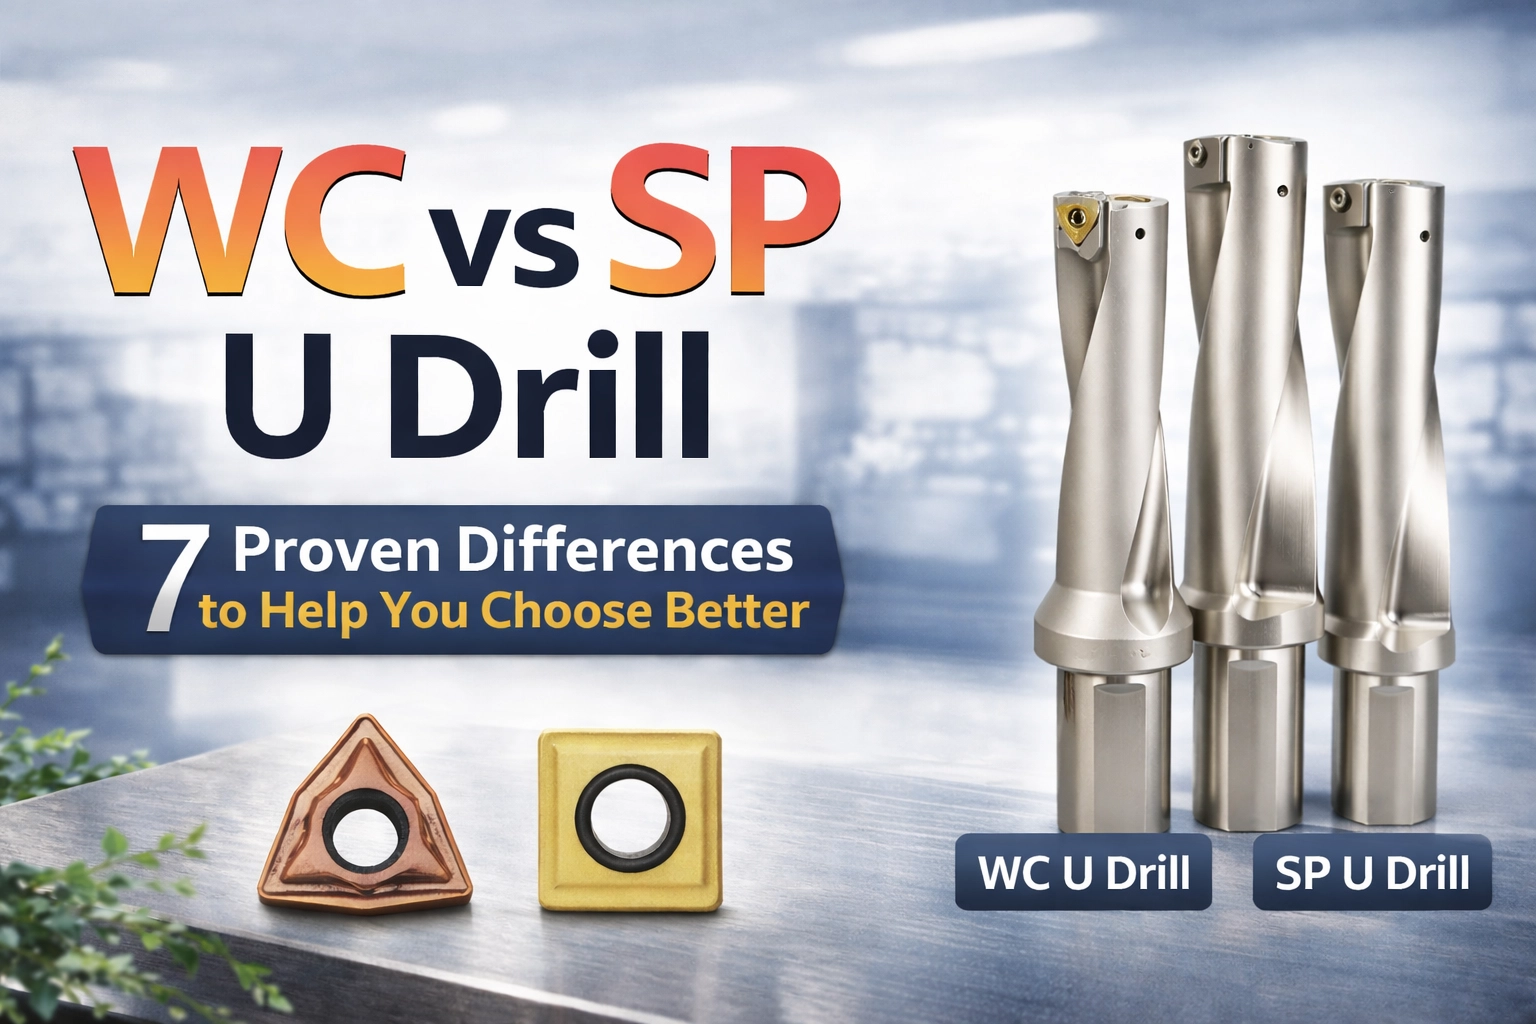
Some suppliers use WC or SP in body codes, while compatible inserts may carry WCMX, WCMT or other designations. These are not universal performance grades, and a similar-looking trigon or square insert does not prove interchangeability. Seat support, thickness, edge preparation, chipbreaker, grade and body design all matter.
To understand the differences between these drill-body systems, read our WC Type vs SP Type U Drill comparison.
| Kontrol et | Evidence to request | Do not assume |
|---|---|---|
| Body system | Complete model and dimensioned catalog page | A similar diameter means the same pocket |
| Insert fit | Full insert code, dimensions and clear pocket photo | The first letters prove interchangeability |
| Position | Central/peripheral assignment in the maker’s data | Both pockets use identical grades or geometries |
| Sıkıştırma | Screw, wrench and tightening specification | A screw that threads into the body is correct |
| Uygulama | Material, hardness, coolant and series cutting data | Shape or edge count alone defines performance |
Tüm sütunları görmek için kaydırın.
 WCMX / WCMT InsertsConfirm the full code, grade and pocket fit.View specifications →
 SPMG / SPGT / SPMT InsertsCheck the insert family, size and cutting position.View specifications →
For other insert families, browse our U-drill inserts and confirm the full insert code, grade and position against the drill body.
Already have a current tool? Send the body model, insert labels and quantities for a compatibility review.
Check 6: Match Insert Geometry and Grade to the Workpiece
Record the material grade, hardness and condition before choosing the insert. “Steel” or “stainless” alone can lead to a recommendation that does not suit the actual workpiece. Include cast or forged surfaces and any interrupted cutting, then check the insert supplier’s application data.
| Material group | Common drilling concern | Verify before selection |
|---|---|---|
| ISO P — steel | Chip formation, edge wear and variable surface condition | Exact grade/hardness, chipbreaker, carbide grade and cutting continuity |
| ISO M — stainless steel | Long chips, adhesion, heat and work hardening | Sharpness, edge strength, coolant delivery and approved grade |
| ISO K — cast iron | Abrasive wear, dust and cast-skin variation | Wear resistance, surface condition and wet/dry guidance for the system |
| ISO N — non-ferrous | Built-up edge, burrs and material adhesion | Sharp or polished geometry, coating/uncoated option and coolant strategy |
| ISO S / H | High heat, hardness or edge-failure risk | Exact alloy/hardness and an application-approved drill and insert combination |
Tüm sütunları görmek için kaydırın.
For stainless steel applications, see our U Drill for Stainless Steel guide for practical checks on chip control, coolant delivery, and insert selection.
Do not identify a coating from colour alone. Similar colours can represent different compositions, substrates and grades. Use the complete grade code and application data.
Check 7: Plan Coolant Delivery and Chip Evacuation
Chip evacuation is part of tool selection. Review chip length, flute space, hole orientation, coolant route, filtration, pressure and available flow.
Sandvik states that internal coolant is preferred to avoid chip jamming, particularly in long-chipping materials and holes deeper than 3×DC. It allows external coolant for shallow holes when chip formation is already good. Seco likewise links poor chip evacuation with incorrect dimensions and bad surface finish in its indexable drill guidance.
Do not make “add a peck cycle” the universal answer. First inspect both chip types, cutting edges, coolant outlets and the exact series guidance. Confirm any pecking strategy for that drill and material.
Check 8: Set U Drill Cutting Data from the Exact Series
Request starting cutting data with the quotation or trial tools. It should identify the body, insert geometry, grade, diameter and material, along with coolant and entry conditions. This gives the end user a defined starting point and makes later feedback easier to compare.
The standard metric calculations are:
Spindle speed: n = (1000 × vc) ÷ (π × Dc)
Feed rate: vf = n × fn
vc = cutting speed (m/min); Dc = drill diameter (mm); fn = feed per revolution (mm/rev).
For drilling, label feed as fn in mm/rev—not milling feed per tooth, fz. During a trial, inspect both chips, listen for interrupted cutting, monitor load, measure the hole and change one variable at a time within the supplier’s range.
Check 9: Review a Replacement Model and Approve the Sample
For a replacement inquiry, a current model or purchasing list can begin the comparison. Confirm the dimensions and application before approving the candidate tool, then record the agreed trial result so the same configuration can be supplied again.
- Identify: record the complete drill body, central/peripheral inserts, screws, shank and coolant connection.
- Compare: place the original and candidate drawings side by side; check every interface and usable dimension.
- Fill the gaps: obtain material, hole, machine, coolant, tolerance and quantity where possible.
- Test: run a controlled sample with agreed cutting data, inspection points and stop criteria.
- Approve: record the accepted body, insert positions, parameters, life criterion and package label.
| Acceptance item | What to record |
|---|---|
| Hole geometry | Diameter at agreed positions, depth and relevant straightness or roundness result |
| Surface and exit | Surface-finish method/result, burr, breakthrough and visible scoring |
| Process stability | Chip form, evacuation, sound, spindle load and coolant condition |
| Aletin durumu | Central/peripheral wear, chipping, screw security and body rub marks |
| Economics | Cycle time, accepted holes per edge and cost per accepted hole |
Tüm sütunları görmek için kaydırın.
Planning a trial with your customer? Our cutting tool trial order guide explains how to agree on test quantities, record machining results and decide whether to move to a larger order.
U Drill Troubleshooting: Check Evidence Before Changing the Insert
The same symptom can have different causes on a rotating drill and a stationary drill. Start with the process evidence rather than immediately changing the insert grade.
| Symptom | Check first | Then review |
|---|---|---|
| Chip jamming | Chip form, coolant flow, filter and blocked outlets | Geometry and cutting data within the maker’s range |
| Oversize, undersize or tapered hole | Rotating/stationary setup, alignment, holder and body rub marks | Central/peripheral edge condition and seat cleanliness |
| Vibration | Overhang, workholding, turret or spindle stability | Cutting speed and application-specific insert geometry |
| Poor finish | Chip scoring, peripheral edge wear and coolant | Feed, stability and any secondary finishing requirement |
| Inconsistent life | Wear pattern on both inserts and coolant repeatability | Material batch, data, insert seats, screws and clamping |
Tüm sütunları görmek için kaydırın.
This sequence is consistent with Sandvik’s indexable drill troubleshooting guide. Use it as a diagnostic order, not as a substitute for the instructions for the selected tool system.
Prepare a Quote-Ready U Drill Inquiry
Use the inquiry paths below. Complete application data is helpful, but do not delay an inquiry just because the end user has not supplied every item.
| Inquiry path | Send these details |
|---|---|
| New application | Material/hardness; hole diameter/depth; through or blind; entry/exit; tolerance/finish; rotating or stationary setup; machine, holder, coolant and quantity |
| Mevcut modelin değiştirilmesi | Brand and complete body/insert codes; catalog page or drawing; tool, pocket and label photos; current issue; quantity; known application data |
| Limited information | Send the current model, purchasing list or clear photos first. Mark unknown fields so they can be confirmed before final approval. |
Tüm sütunları görmek için kaydırın.
Sıkça Sorulan Sorular
What information do you need for a U drill quotation?
Send the model or tool type, sizes, quantity, material or application, and destination. Drawings, photos or existing references help.
Can you compare our current brand or model?
Yes. Send the brand, model or part number and available application details. We can compare key specifications and recommend an alternative or custom option.
Can we place a trial order or request samples?
Yes. Most standard tools start at 10 pcs; confirm the MOQ for the requested items. Samples are generally charged, and the customer pays shipping.
Are standard sizes available from stock?
Some common standard sizes may be stocked; others require production. Send exact models, sizes and quantities to confirm availability.
What should we send if the end user has a machining problem?
Send tool specifications, material and hardness, machine type, RPM, feed, depth and coolant conditions. Add tool life, wear photos or videos, and machining results.
How do you handle repeat orders?
We retain specifications, drawings and order records. Standard repeat orders follow confirmed specifications; custom-tool dimensions and tolerances are reconfirmed before production.
 WC Tipi ve SP Tipi U Matkapların Karşılaştırması
 U Drill for Stainless Steel