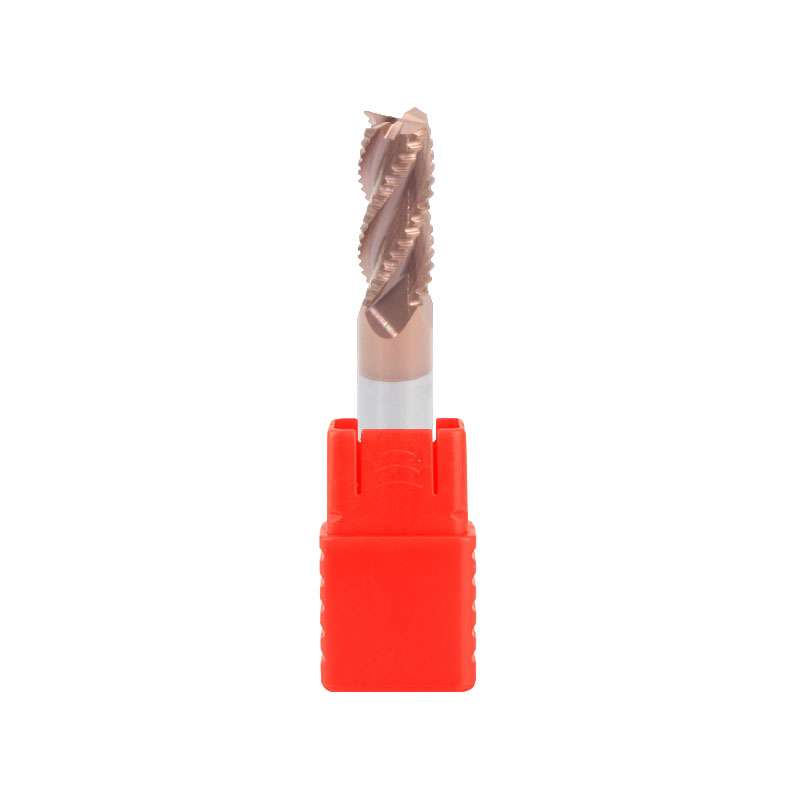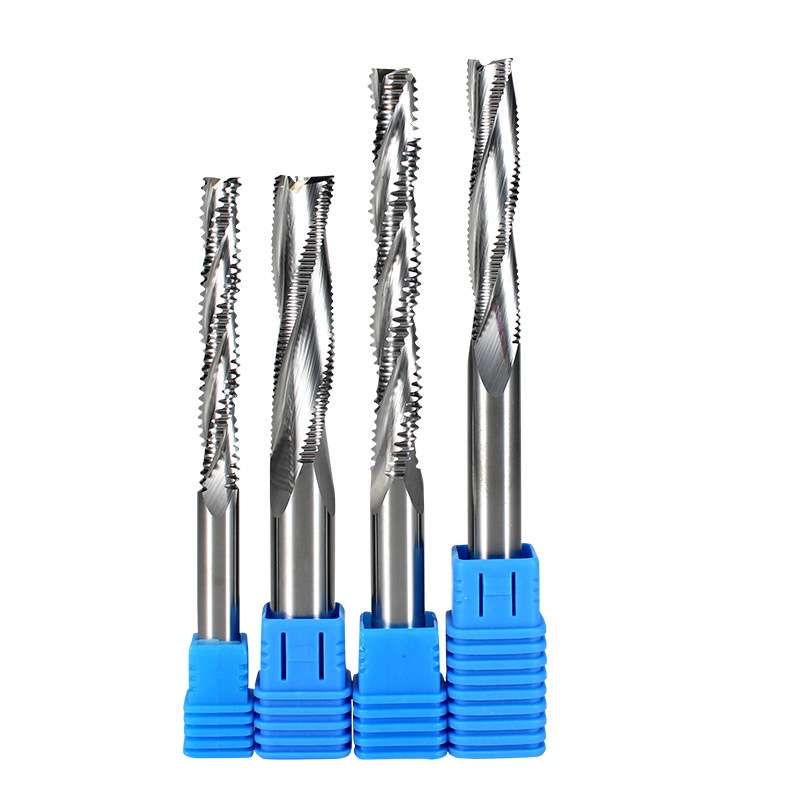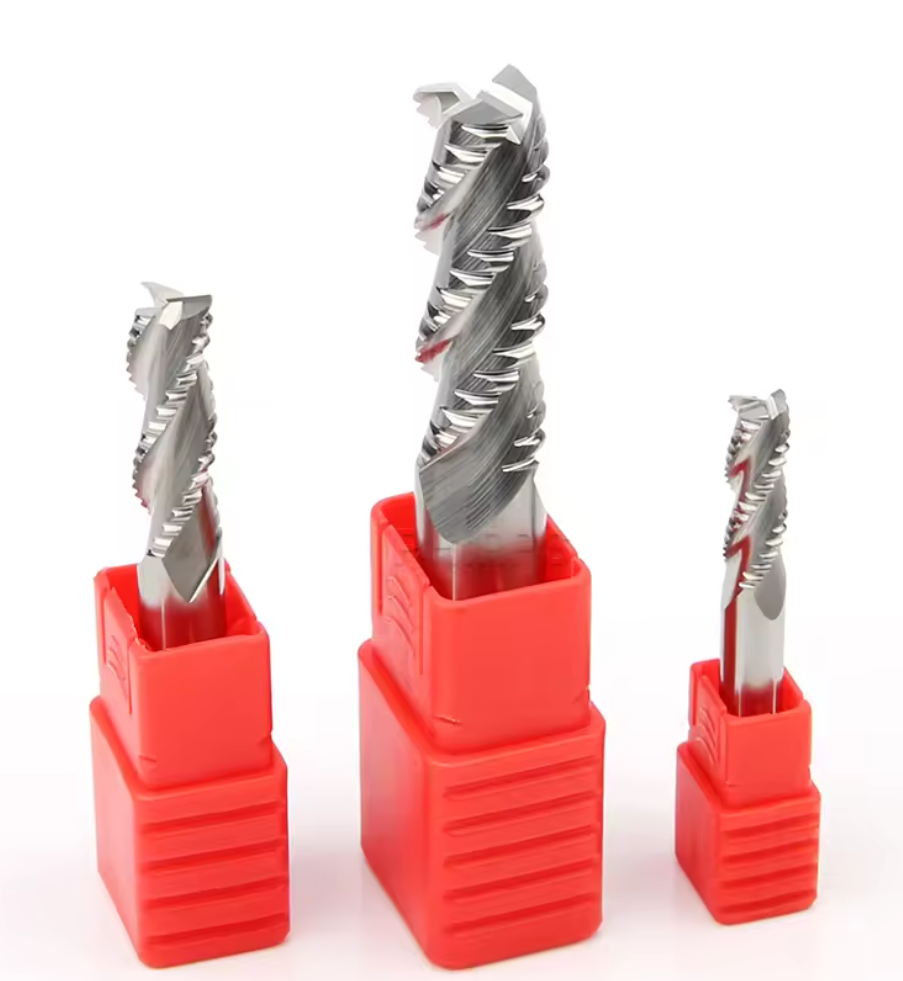
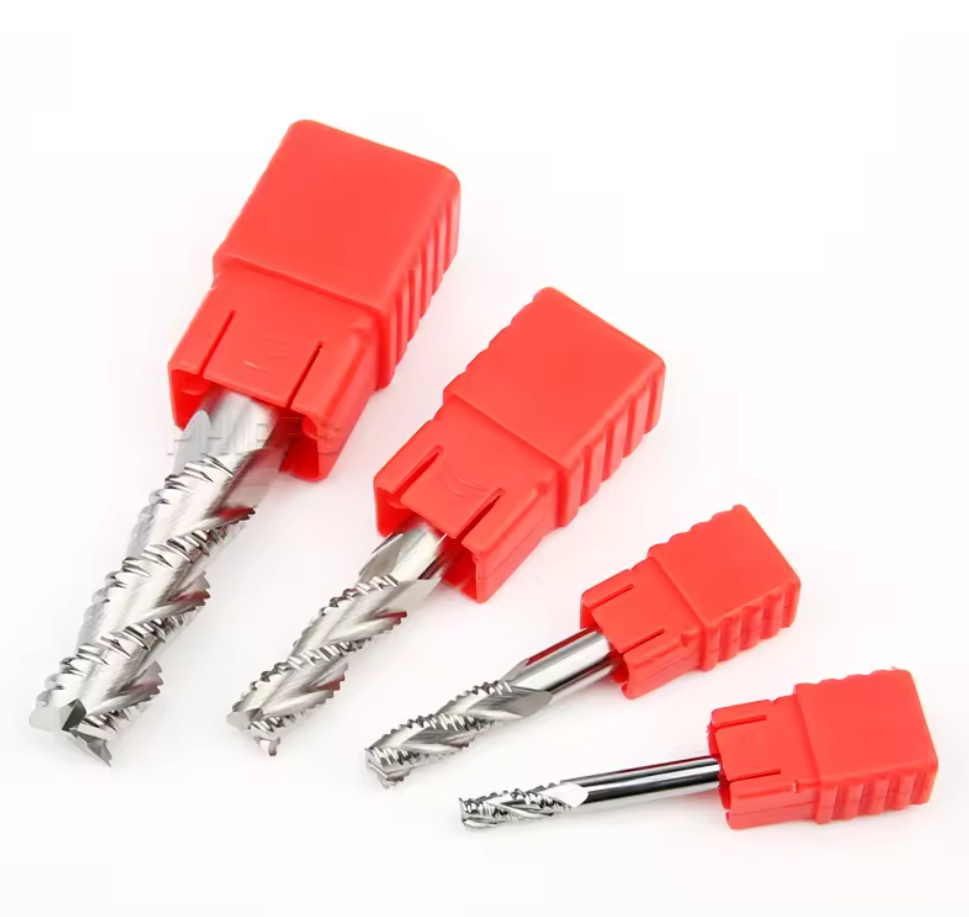
3-Flute Polished Solid Carbide Roughing End Mill for Aluminum
Consistent Quality
Consistent geometry across repeat orders.
Pedidos flexíveis
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
Padrão e personalizado
Standard sizes and custom configurations.
3-Flute Roughing End Mill for Aluminum Overview
This 3-flute polished solid carbide roughing end mill is designed for efficient stock removal in aluminum and selected non-ferrous materials. Its serrated wave-edge geometry divides the cutting load and produces shorter chips during high-engagement machining, while the three-flute construction provides additional chip space compared with conventional four-flute steel-cutting tools. Sharp cutting edges and polished flute surfaces support smooth chip evacuation, reduced aluminum adhesion and stable rough slotting, pocketing, side milling and profiling.
3 Flutes
Wave-Edge Roughing
Mirror Polished
Ligas de alumínio
Aluminum-Roughing Features
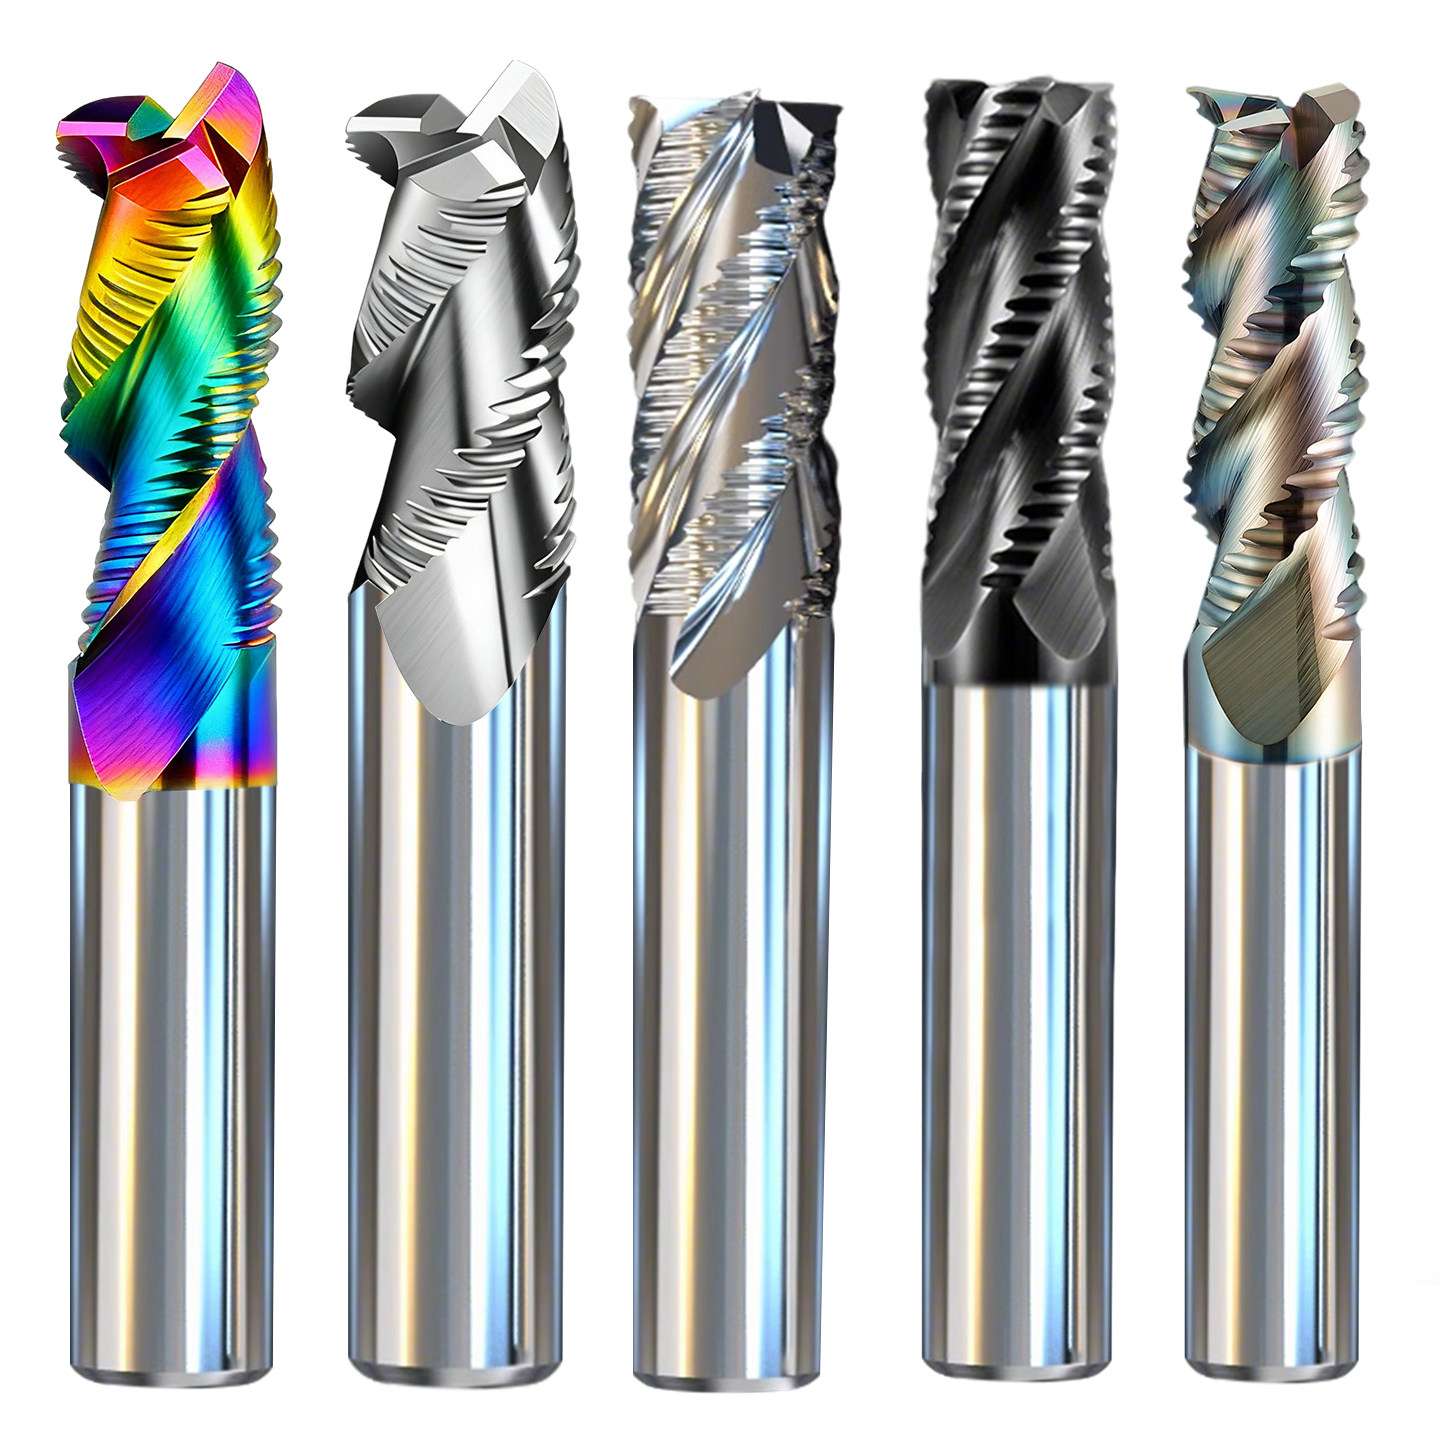
Serrated Wave Edge
The roughing profile divides the removed material into shorter chips and helps control the cutting load during high-engagement machining.
Three-Flute Chip Space
The three-flute construction balances tool-core rigidity, cutting contacts and flute space for evacuating larger aluminum chips.
Polished Flute Surface
Polished flute surfaces reduce friction and support smooth chip flow, helping limit aluminum adhesion and chip recutting.
Sharp Aluminum Geometry
Application-matched rake and relief geometry reduce cutting resistance during rough slotting, pocketing and side milling.
Applications & Materials
Recommended for rough slotting, pocket roughing, side milling, profiling and high-engagement stock removal in aluminum components. The tool can be used on CNC machining centers, milling machines and other suitable production equipment with effective chip evacuation and secure toolholding.
N Aluminum Alloys
N Copper Alloys
N Other Non-Ferrous
Product Details
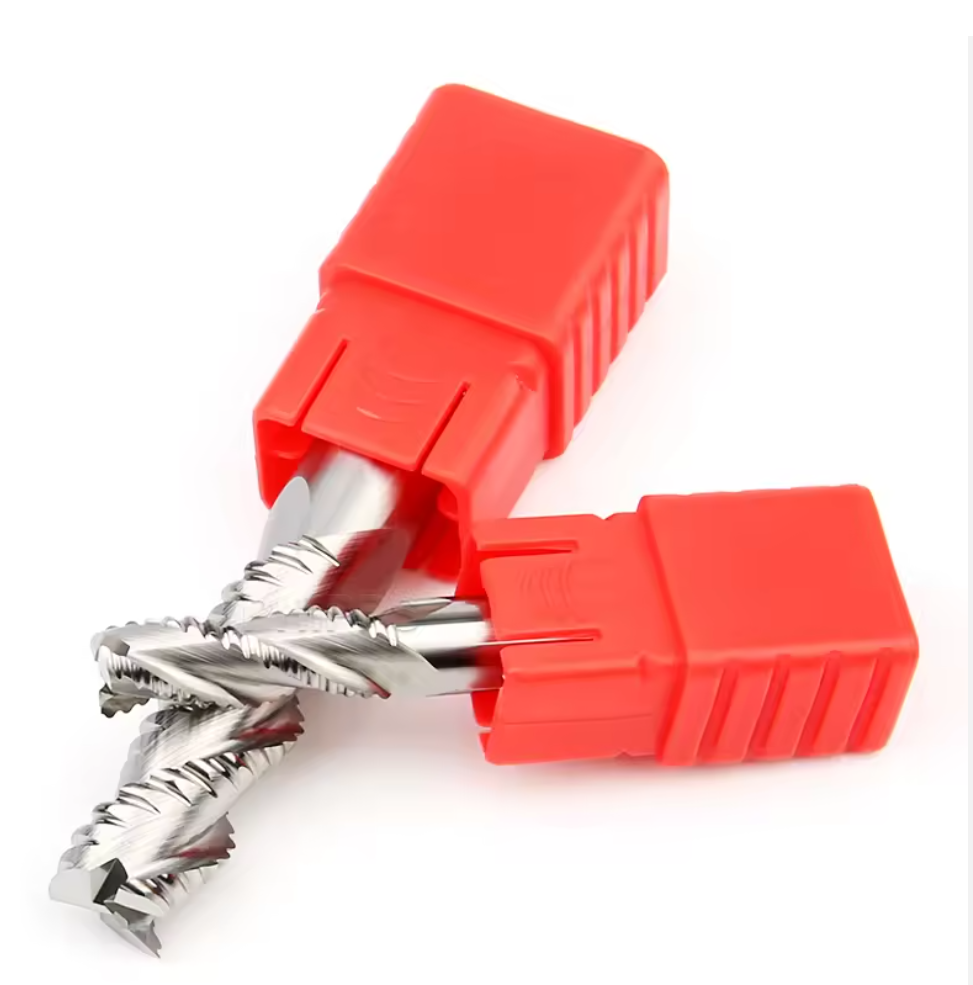
Aluminum Roughing End Mill Specifications
Technical configuration and standard reference sizes for the 3-flute polished solid carbide roughing end mill for aluminum. Dimensions are shown in millimeters. The cutting geometry combines a serrated roughing edge, generous flute space and polished flute surfaces for chip control and efficient stock removal in aluminum and selected non-ferrous materials.
| PARAMETER | STANDARD CONFIGURATION |
|---|---|
| Product Type | Solid carbide roughing end mill for aluminum |
| Cutting Profile | Serrated wave-edge geometry for rough machining and controlled chip formation |
| Substrato | Fine-grain solid carbide selected for cutting-edge sharpness and tool rigidity |
| Contagem de flautas | 3 flutes with additional chip space for aluminum roughing |
| End Profile | Flat / square end for rough slotting, pocketing and shoulder machining |
| Flute Finish | Polished flute surfaces for reduced friction, smoother chip flow and controlled aluminum adhesion |
| Cutting Diameter | Ø1–Ø20 mm reference range |
| Diâmetro da haste | Ø4–Ø20 mm or drawing-defined configuration |
| Comprimento total | 50–100 mm standard reference sizes; extended lengths can be reviewed separately |
| Surface Treatment | Polished uncoated configuration as standard; DLC coating available after application review |
| Materiais adequados | Aluminum, wrought aluminum alloys, cast aluminum and selected copper alloys or other non-ferrous materials |
| Main Applications | Rough slotting, pocket roughing, side milling, profiling and high-engagement stock removal |
| Compatibilidade de máquinas | CNC machining centers and milling machines with effective chip evacuation |
Standard Reference Sizes
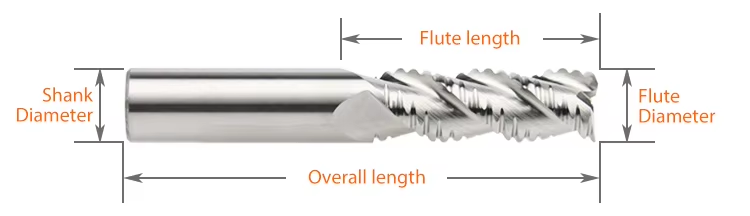
D = cutting diameter, L1 = flute length, d = shank diameter and L = overall length. The original dimensional combinations are retained below. Final availability should be confirmed according to the required diameter, cutting length and order quantity.
| SPECIFICATION | D | L1 | d | L | FLUTES |
|---|---|---|---|---|---|
| D1–D4 × L1 × d4 × 50L | 1-4 | 3 / 6 / 9 / 12 | 4 | 50 | 3 |
| D4 × 16 × d4 × 75L | 4 | 16 | 4 | 75 | 3 |
| D4 × 20 × d4 × 100L | 4 | 20 | 4 | 100 | 3 |
| D6 × 15 × d6 × 50L | 6 | 15 | 6 | 50 | 3 |
| D6 × 24 × d6 × 75L | 6 | 24 | 6 | 75 | 3 |
| D6 × 30 × d6 × 100L | 6 | 30 | 6 | 100 | 3 |
| D8 × 20 × d8 × 60L | 8 | 20 | 8 | 60 | 3 |
| D8 × 25 × d8 × 75L | 8 | 25 | 8 | 75 | 3 |
| D8 × 35 × d8 × 100L | 8 | 35 | 8 | 100 | 3 |
| D10 × 25 × d10 × 75L | 10 | 25 | 10 | 75 | 3 |
| D10 × 40 × d10 × 100L | 10 | 40 | 10 | 100 | 3 |
| D12 × 35 × d12 × 75L | 12 | 35 | 12 | 75 | 3 |
| D12 × 45 × d12 × 100L | 12 | 45 | 12 | 100 | 3 |
| D14 × 45 × d14 × 100L | 14 | 45 | 14 | 100 | 3 |
| D16 × 45 × d16 × 100L | 16 | 45 | 16 | 100 | 3 |
| D18 × 45 × d18 × 100L | 18 | 45 | 18 | 100 | 3 |
| D20 × 45 × d20 × 100L | 20 | 45 | 20 | 100 | 3 |
Aluminum Cutting Configuration
The carbide substrate, three-flute geometry and polished flute surface work together to provide sharp cutting and sufficient chip space for aluminum roughing.
| CONFIGURATION | APPLICATION FUNCTION |
|---|---|
| Fine-Grain Carbide | Provides tool rigidity and supports a sharp cutting edge during high-engagement aluminum machining |
| Three-Flute Geometry | Balances cutting-edge count, tool-core strength and flute space for evacuating larger aluminum chips |
| Serrated Roughing Edge | Produces shorter chips and distributes the cutting load during rough slotting, pocketing and profiling |
| Polished Flute Surface | Supports smooth chip flow and helps limit friction, aluminum adhesion and chip recutting |
Surface Treatment Options
Surface treatment should be selected according to the aluminum grade, silicon content, cutting engagement, coolant method and required production volume.
| SURFACE TREATMENT | SELECTION GUIDANCE |
|---|---|
| Polished Uncoated | Standard choice for maintaining a sharp cutting edge, reducing friction and supporting smooth chip evacuation in common aluminum alloys |
| DLC-Coated Option | Available after technical review when lower friction, reduced material adhesion or additional wear resistance is required |
| Other Coatings | Alternative coatings should be confirmed according to the exact non-ferrous material and must not reduce the required cutting-edge sharpness |
Polished uncoated geometry is the standard positioning for this product. DLC coating is an optional configuration rather than the default specification.
Aluminum Roughing End Mill Customization
Cutting diameter, serrated roughing-tooth profile, flute length, shank diameter, overall length, helix angle, cutting-edge geometry and surface treatment can be configured for aluminum-roughing applications. The standard design combines three flutes with polished chip channels and sharp cutting edges for controlled chip formation and efficient chip evacuation. Standard, long-flute, extended-length and drawing-defined configurations can be reviewed according to the aluminum grade, machining depth, tool engagement, spindle capability and required production efficiency.
| PARAMETER | MANUFACTURING CAPABILITIES |
|---|---|
| Cutting Diameter | Reference cutting diameters from Ø1–Ø20 mm, with intermediate and drawing-defined non-standard diameters available after technical review |
| Contagem de flautas | Standard 3-flute construction balancing tool-core rigidity, cutting contacts and flute space for aluminum chip evacuation |
| Roughing-Tooth Profile | Serrated wave-edge pitch and tooth profile can be adjusted according to the cutting diameter, required chip size, cutting load and remaining finishing allowance |
| Comprimento da flauta | Standard, long-flute and drawing-defined cutting lengths can be reviewed according to the axial depth, workpiece geometry and required machining reach |
| Comprimento total | Reference overall lengths of 50, 60, 75 and 100 mm, with selected extended-length configurations available for deep or less accessible features |
| Configuração da haste | Precision cylindrical shanks from Ø4–Ø20 mm, with custom shank diameter, reduced-neck geometry and clamping length reviewed according to the holder and tool overhang |
| Helix Geometry | Application-matched helix geometry selected according to the aluminum grade, cutting engagement, chip formation and required balance between edge strength and chip evacuation |
| Geometria da extremidade | Flat square-end geometry for rough slotting, pocketing and shoulder machining, with center-cutting capability confirmed by the selected configuration |
| Cutting-Edge Geometry | Sharp rake angle, relief geometry, end-face grinding and edge preparation can be matched to the aluminum grade, silicon content and cutting load |
| Flute Polishing | Polished flute surfaces support smooth chip flow and help limit friction, aluminum adhesion and chip recutting during continuous rough machining |
| Surface Treatment | Polished uncoated geometry is the standard configuration; DLC coating can be reviewed for lower friction and additional wear resistance |
| Workpiece Materials | Configurations can be reviewed for wrought aluminum, cast aluminum, aluminum alloys and selected copper alloys or other non-ferrous materials |
| Roughing Applications | Geometry can be configured for rough slotting, pocket roughing, side milling, profiling and high-engagement stock-removal operations |
| Método de resfriamento | Air blast, mist or aluminum-compatible coolant can be selected according to the machining engagement, chip volume and production conditions |
| Dimensional Tolerance | Drawing-defined control of cutting diameter, flute length, shank diameter, overall length, runout and roughing-edge geometry, with critical tolerances confirmed before production |
| OEM & Private Label | Customer logos, tool codes, dimensions, surface identification and batch numbers can be laser marked; custom labels, protective tubes and private-label packaging are also available |
Serviços de OEM e marca própria
OEM manufacturing and private-label supply options are available for industrial distributors, tooling brands and repeat-production customers. Laser identification, label content, protective packaging and coating presentation can be configured according to the approved product specification and order requirements.

Laser Etching
Custom logos, tool codes, cutting dimensions, coating identification and batch numbers can be marked according to the available shank area.
Custom Labels & Packaging
Individual protective tubes, product labels, specification details, colored packaging tubes and private-label packaging can be reviewed.
Commercial Terms
MOQ, sample evaluation, custom-size trials, repeat orders and scheduled supply programs are confirmed according to the selected configuration.
Technical Workflow
A structured review process is used to confirm standard, customized and private-label square end mill requirements before production.
Inquiry
Submit the material, hardness, milling operation, dimensions, tolerance and quantity.
Engineering
Review flute geometry, helix angle, edge preparation, coating, ap and ae.
Commercial
Confirm quotation, MOQ, sample requirements, production schedule and delivery terms.
Production
CNC grinding, end-face formation, edge preparation, coating and laser marking.
Quality Control
Inspect diameter, flute length, shank, runout, square-end geometry and cutting edges.
Quality, Inspection & Delivery
Our solid carbide square end mills are controlled through material verification, precision grinding, in-process measurement and final inspection. Key dimensions, square-end geometry, cutting-edge condition, coating appearance and product identification are reviewed according to the approved specification or drawing before packing.

Three-Stage Quality Control
Inspection checkpoints are arranged around the manufacturing process to support dimensional consistency and repeat-order control.
Incoming Material Control
Carbide substrate grade, blank dimensions and supplied material information are checked against the production requirement.
In-Process Grinding Control
Cutting diameter, flute geometry, flute length, square-end profile and shank dimensions are monitored during CNC grinding.
Final Tool Inspection
Finished tools are reviewed for specified dimensions, runout, cutting-edge condition, coating appearance, marking and packing identification.
Key Inspection Characteristics
Inspection requirements are confirmed according to the standard product specification or the approved custom drawing.
| INSPECTION ITEM | CONTROL FOCUS | CONFIRMATION BASIS |
|---|---|---|
| Cutting Diameter (DC) | Diameter and dimensional consistency | Standard specification or approved drawing |
| Flute Length (APMX) | Effective cutting length | Confirmed product size or drawing requirement |
| Shank Diameter (DCON) | Clamping-section dimension and surface condition | Applicable shank specification |
| Overall Length (OAL) | Total tool length | Standard size matrix or approved drawing |
| Deslocamento radial | Concentricity between cutting section and shank | Agreed inspection requirement |
| Square-End Geometry | End-face profile, corner condition and center-cutting form | Selected tool configuration |
| Flute & Helix Profile | Flute count, helix form and grinding consistency | Approved manufacturing configuration |
| Cutting Edge & Coating | Edge condition, visible defects and coating appearance | Application-specific production requirement |
| Marking & Identification | Tool code, dimensions and batch information where applicable | Confirmed order and packaging specification |
Measurement & Batch Traceability
Optical measuring systems, tool inspection equipment and appropriate dimensional gauges are selected according to the feature being checked.
Optical Measurement
Profile and dimensional review of specified cutting features.
Runout Verification
Concentricity review based on the agreed product requirement.
Edge Inspection
Magnified review of the end face, corners and cutting-edge condition.
Batch Identification
Order, product and batch information are linked where required for repeat supply.
Protective Packaging Process
Finished end mills are protected to reduce contact between cutting edges and to support clear product identification during storage and transportation.

Bulk-Order & Export Packaging
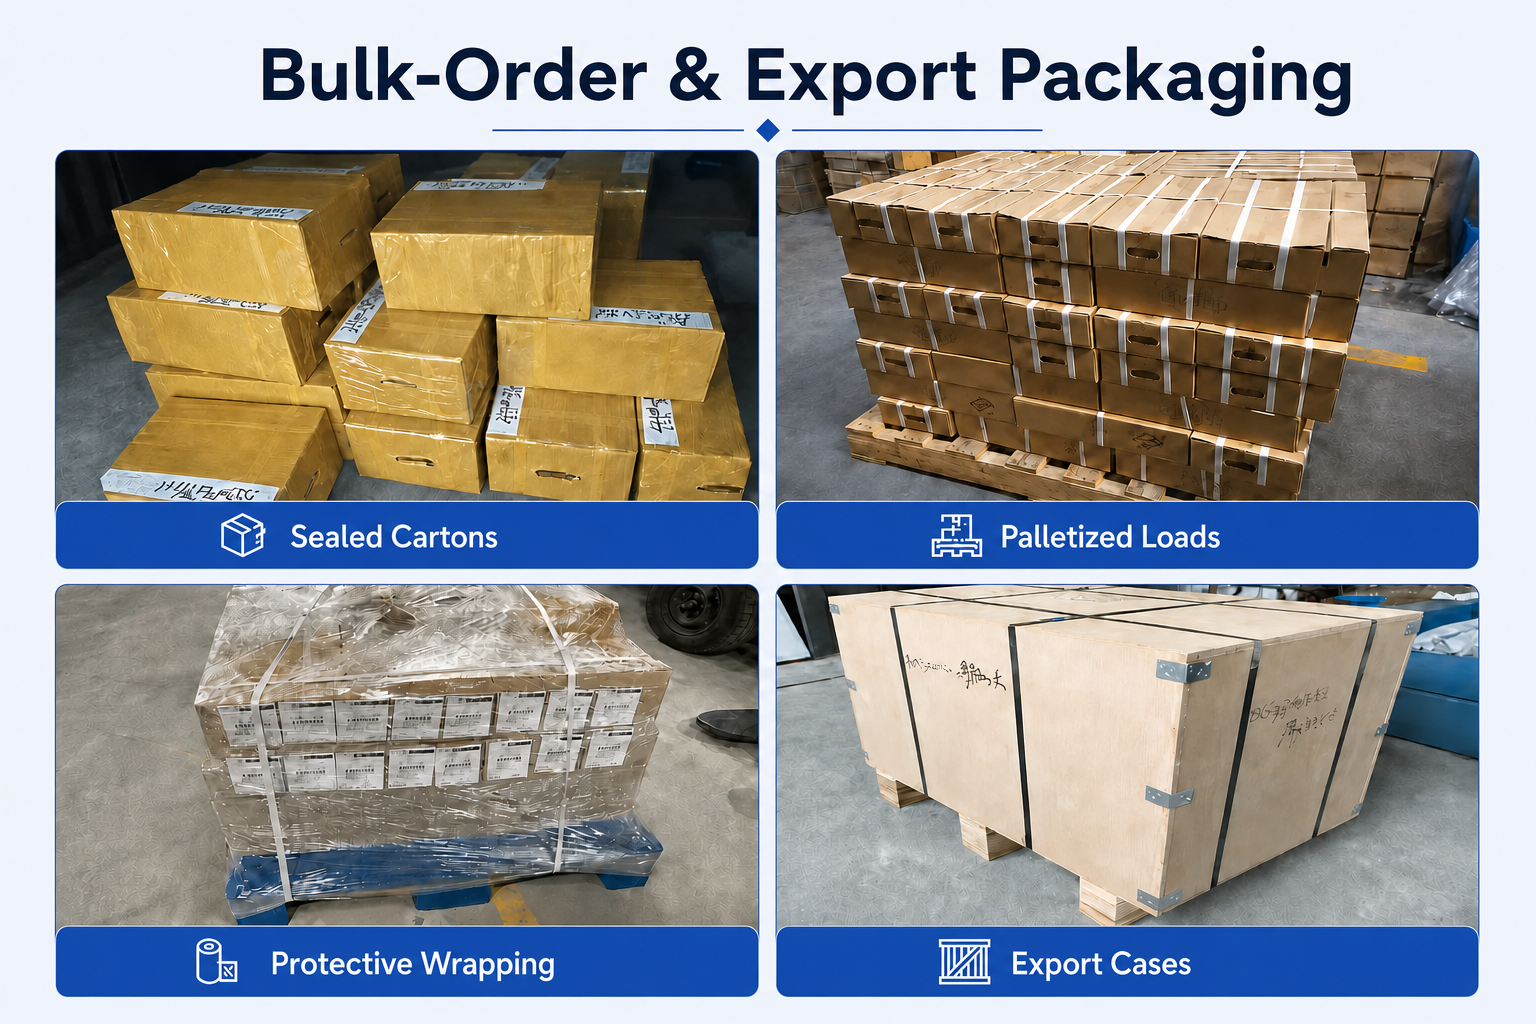
Bulk shipments can be arranged with reinforced cartons, protective wrapping, palletized loading or export cases according to order quantity, shipment weight and agreed transportation requirements.
Delivery Coordination
Production completion, packing method and dispatch arrangements are confirmed according to the approved order. Courier, air, sea or customer-designated shipping options can be reviewed according to shipment size and destination. Final lead time is confirmed after product specifications, quantity and packaging requirements are approved.
FAQ & Downloads
Review common product, application and ordering questions for the 3-flute polished solid carbide roughing end mill for aluminum, then access the current end mill catalog and starting cutting-data guide.
Product & Application FAQs
Selection and application guidance for efficient aluminum roughing.
What materials is this roughing end mill designed to machine?
It is primarily designed for wrought aluminum, cast aluminum and common aluminum alloys. Selected copper alloys and other non-ferrous materials may also be machined after reviewing the material grade, cutting load and required surface condition.
Why does this aluminum roughing end mill use three flutes?
The three-flute construction balances cutting-edge count, tool-core rigidity and flute space. Compared with a four-flute steel-cutting tool, it provides more room for evacuating larger aluminum chips while maintaining multiple cutting contacts for stable rough machining.
What is the purpose of the serrated wave edge?
The serrated wave-edge geometry divides the removed material into shorter chips and interrupts the cutting load. This supports chip control during rough slotting, pocketing, side milling and other high-engagement stock-removal operations.
What are the benefits of the polished flute surface?
Polished flute surfaces reduce friction and provide a smoother path for chip evacuation. This helps limit aluminum adhesion, chip recutting and heat accumulation around the cutting zone during continuous rough machining.
Can this roughing end mill produce the final finished surface?
The serrated cutting profile normally leaves a visible wave pattern on the machined surface. When a smooth final surface or close finished dimension is required, leave suitable finishing stock and complete the operation with a polished smooth-edge finishing end mill.
Can this cutter perform full-width slotting?
It can be used for rough slotting when the axial depth, feed and chip evacuation are properly controlled. For deep full-width slots, reduce the cutting engagement when necessary and use effective air blast, mist or aluminum-compatible coolant to prevent chip packing.
Should I choose polished uncoated or DLC-coated?
Polished uncoated geometry is the standard choice for maintaining a sharp edge and smooth chip flow in common aluminum alloys. DLC coating can be reviewed when lower friction, reduced material adhesion or additional wear resistance is required, particularly for repetitive or abrasive non-ferrous machining.
Is this roughing end mill suitable for steel?
This product is optimized for aluminum and selected non-ferrous materials. For carbon steel, alloy steel or pre-hardened steel, choose a steel-specific roughing end mill with the appropriate carbide grade, edge preparation and heat-resistant coating.
Ordering & Customization FAQs
Information for distributors, tooling brands and customers requesting standard or drawing-based aluminum roughing end mills.
What standard sizes are available?
The reference range covers selected cutting diameters from Ø1–Ø20 mm with standard, long-flute and selected extended-length configurations. Final availability should be confirmed by cutting diameter, flute length, shank diameter, overall length and surface treatment.
Can non-standard dimensions or roughing geometry be manufactured?
Yes. Cutting diameter, flute length, shank diameter, overall length, reduced-neck geometry, roughing-tooth profile, helix geometry, corner radius and surface treatment can be reviewed according to the drawing and machining application.
Can I order samples before placing a bulk order?
Yes. Samples can be reviewed according to the required diameter, flute length, polished or DLC-coated surface and quantity. For a non-standard tool, the approved drawing, tolerance requirements, sample quantity and delivery cost must be confirmed before production.
What is the lead time?
Available standard configurations can normally be shipped within 1–3 working days after order confirmation. Lead time for custom dimensions, special roughing geometry, DLC coating or non-standard production requirements is confirmed according to the drawing, quantity and current production schedule.
Are OEM marking and private-label packaging available?
Yes. Customer logos, tool codes, cutting dimensions, surface-treatment identification and batch numbers can be laser marked according to the available shank area. Custom labels, protective tubes and private-label packaging can also be supplied.
What information is required for an accurate quotation?
Please provide the aluminum grade, silicon content, cutting diameter, flute length, shank diameter, overall length, roughing operation, axial depth ap, radial engagement ae, spindle speed, holder type, air or coolant method, surface-treatment preference, dimensional tolerance and order quantity.
Technical Downloads
Access current product-range information and starting cutting references for solid carbide aluminum roughing end mill selection.
Catálogo de fresas de ponta de metal duro maciço
Aluminum end mill families, flute options, surface treatments and reference sizes.
End Mill Speeds & Feeds Guide
Starting cutting speeds, chip loads, engagement guidance and adjustment notes.
Cutting data are starting references only. Adjust the values according to the exact tool diameter, aluminum grade, flute length, axial and radial engagement, tool overhang, holder condition, spindle capability and chip-evacuation method.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.