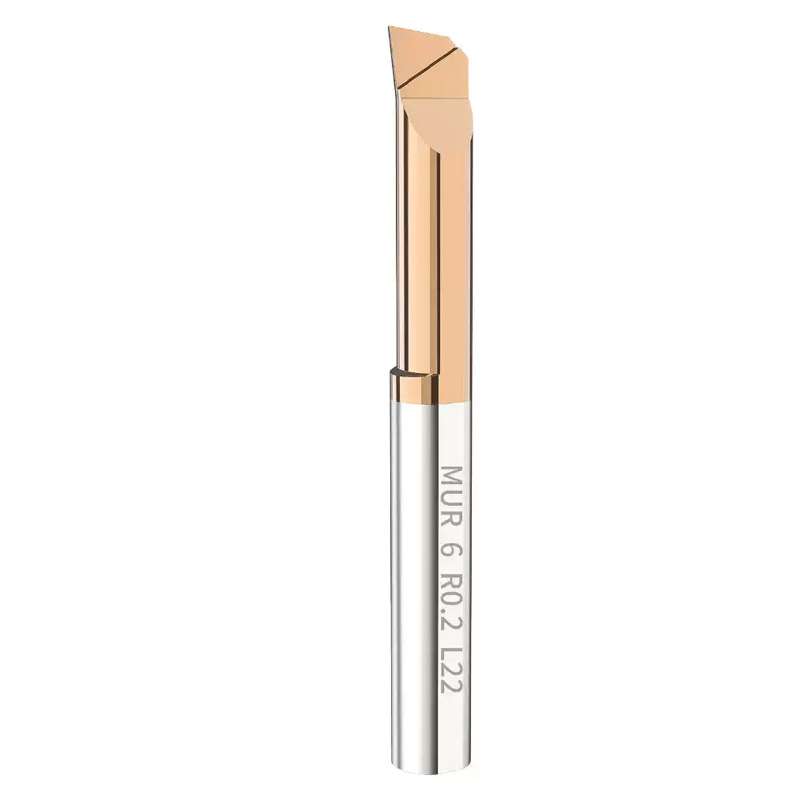
MXR Series Solid Carbide Micro Back Turning Bars for Small Bore Internal Machining
Calidad constante
Consistent geometry across repeat orders.
Pedidos flexibles
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
Herramientas estándar y personalizadas
Standard sizes and custom configurations.
MXR Micro Back Turning Bar Overview
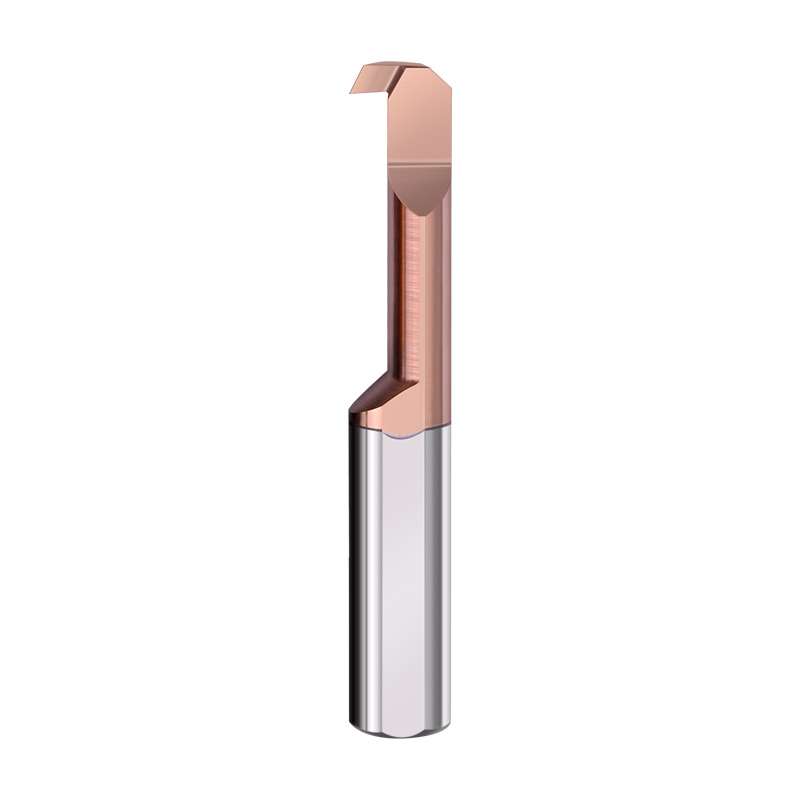
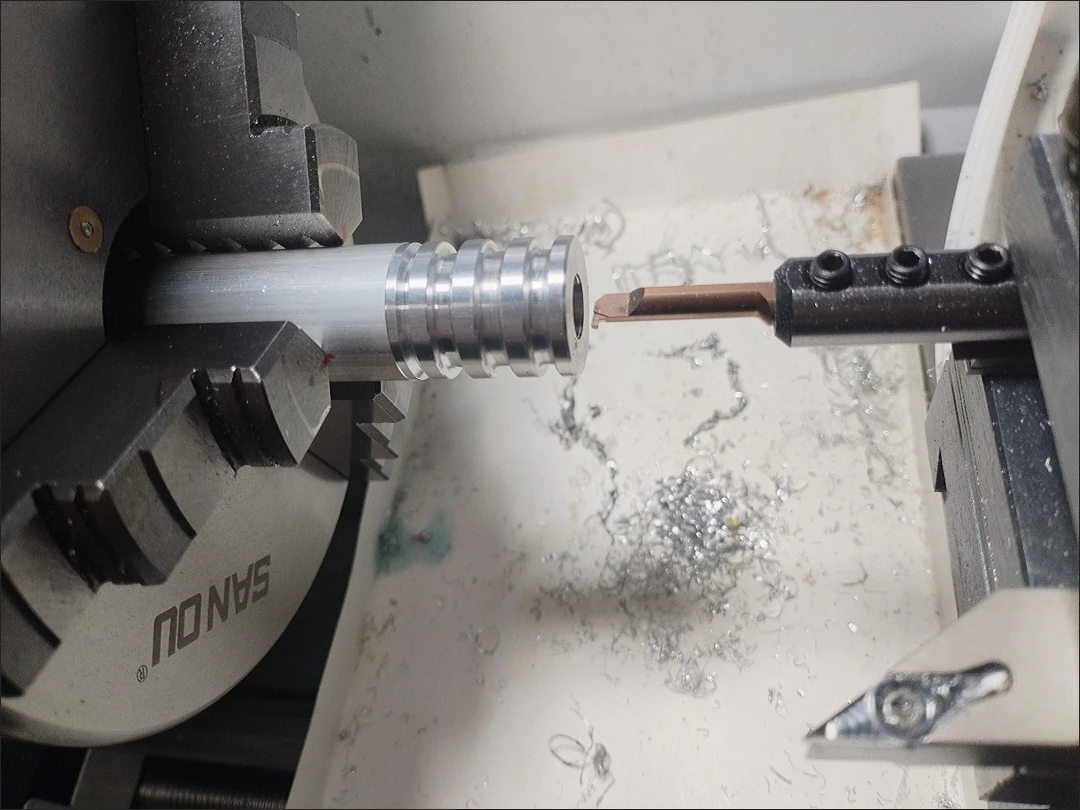
The MXR Series is a precision-ground solid carbide micro back turning bar designed for machining rear faces, internal undercuts and recessed features behind shoulders in small-diameter bores. The tool enters through the bore, passes the internal shoulder and cuts during a controlled reverse-feed movement.
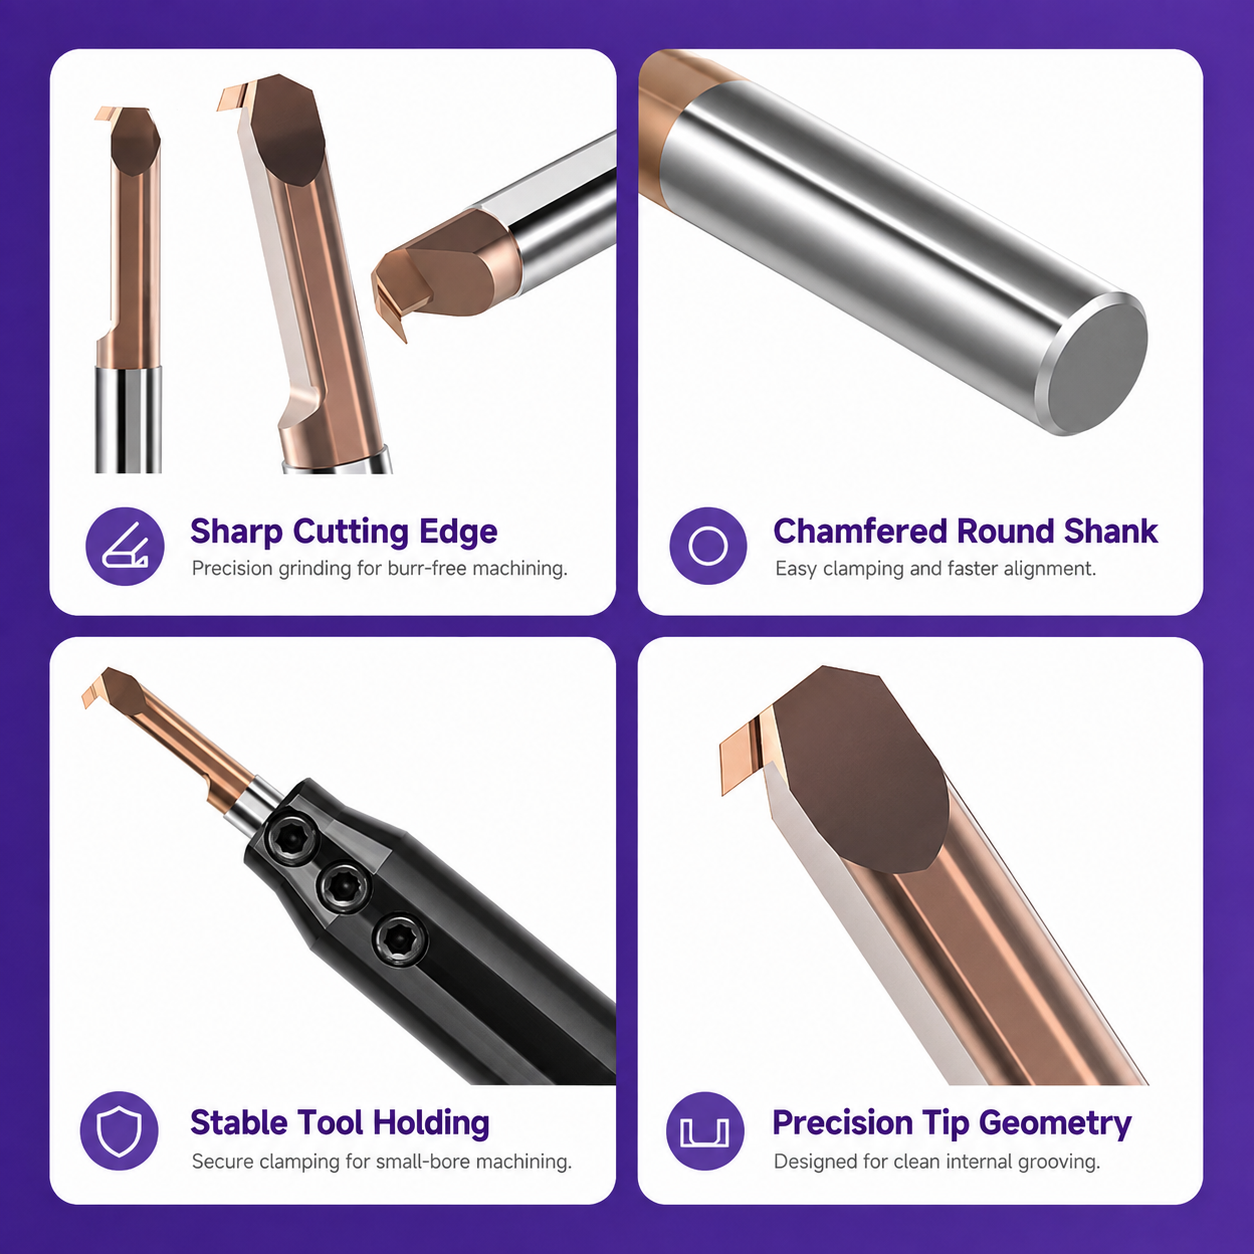
Standard models cover cutting diameters from Ø2.8 to Ø5.9 mm, cutting widths of 1.3 and 1.5 mm, and clearance lengths from 10 to 22 mm. The one-piece carbide construction provides the rigidity and dimensional stability required for restricted-access internal machining.
Key Product Features
Typical Applications
| Aplicación | Machining Purpose |
|---|---|
| Internal Back Turning | Machining a rear-facing internal surface by cutting in the reverse feed direction. |
| Rear Shoulder Finishing | Finishing the back face of an internal shoulder that cannot be reached with a conventional boring bar. |
| Internal Undercutting | Producing controlled relief features and recessed areas behind internal shoulders. |
| Recessed Feature Machining | Machining hidden or restricted internal features after the cutting edge passes through the bore entrance. |
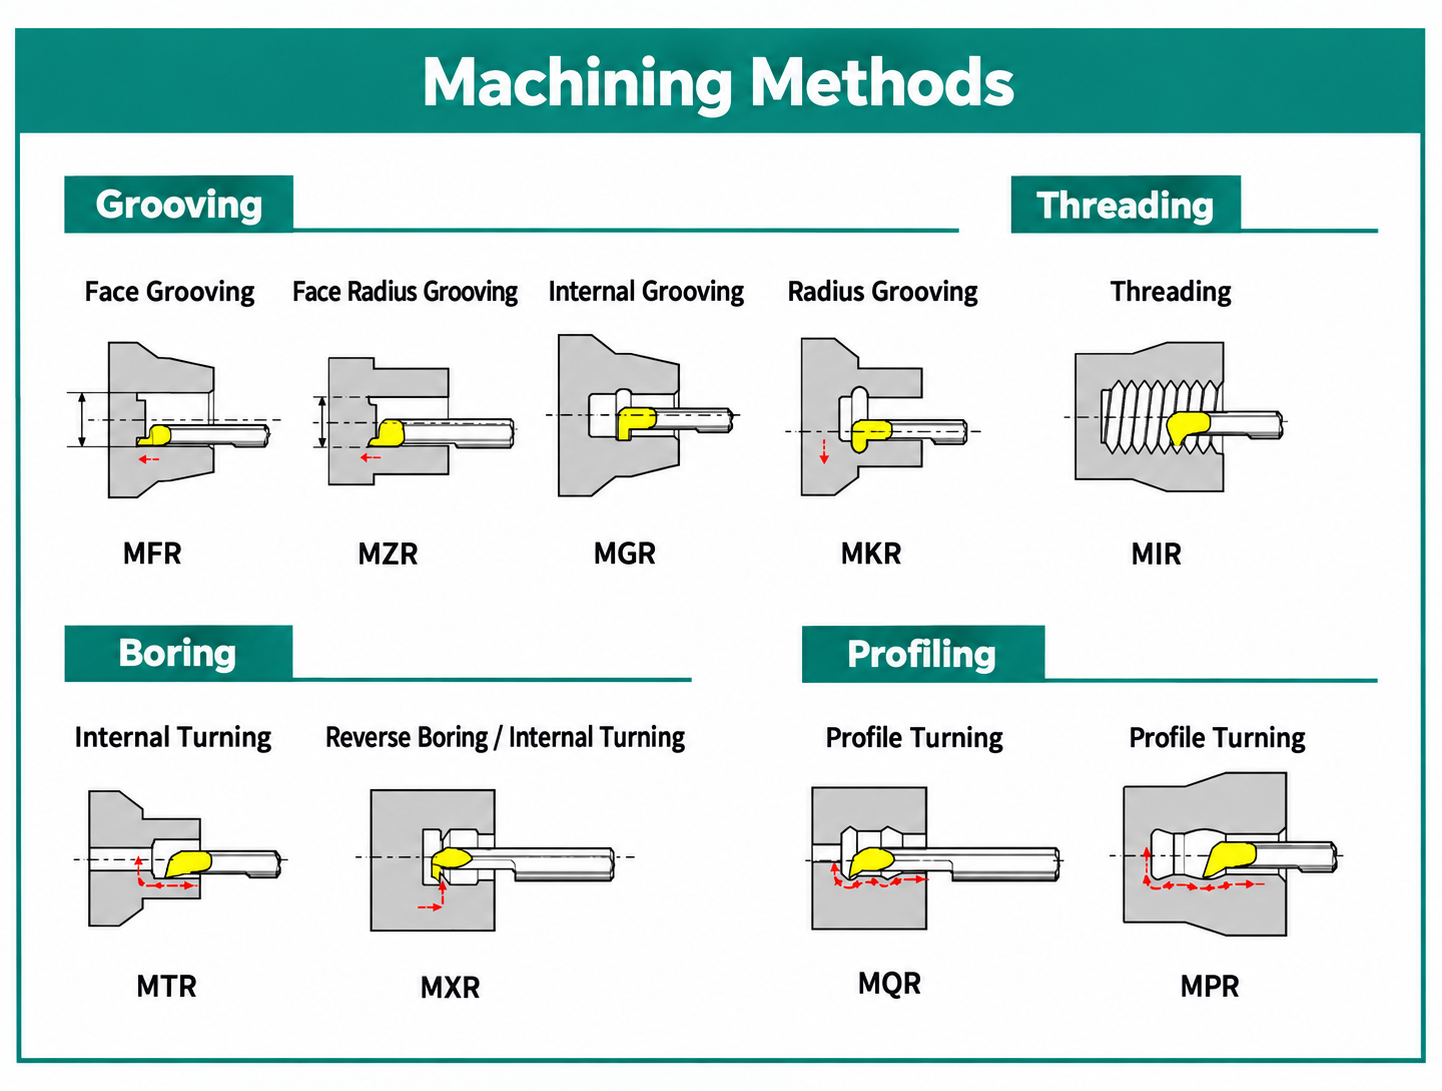
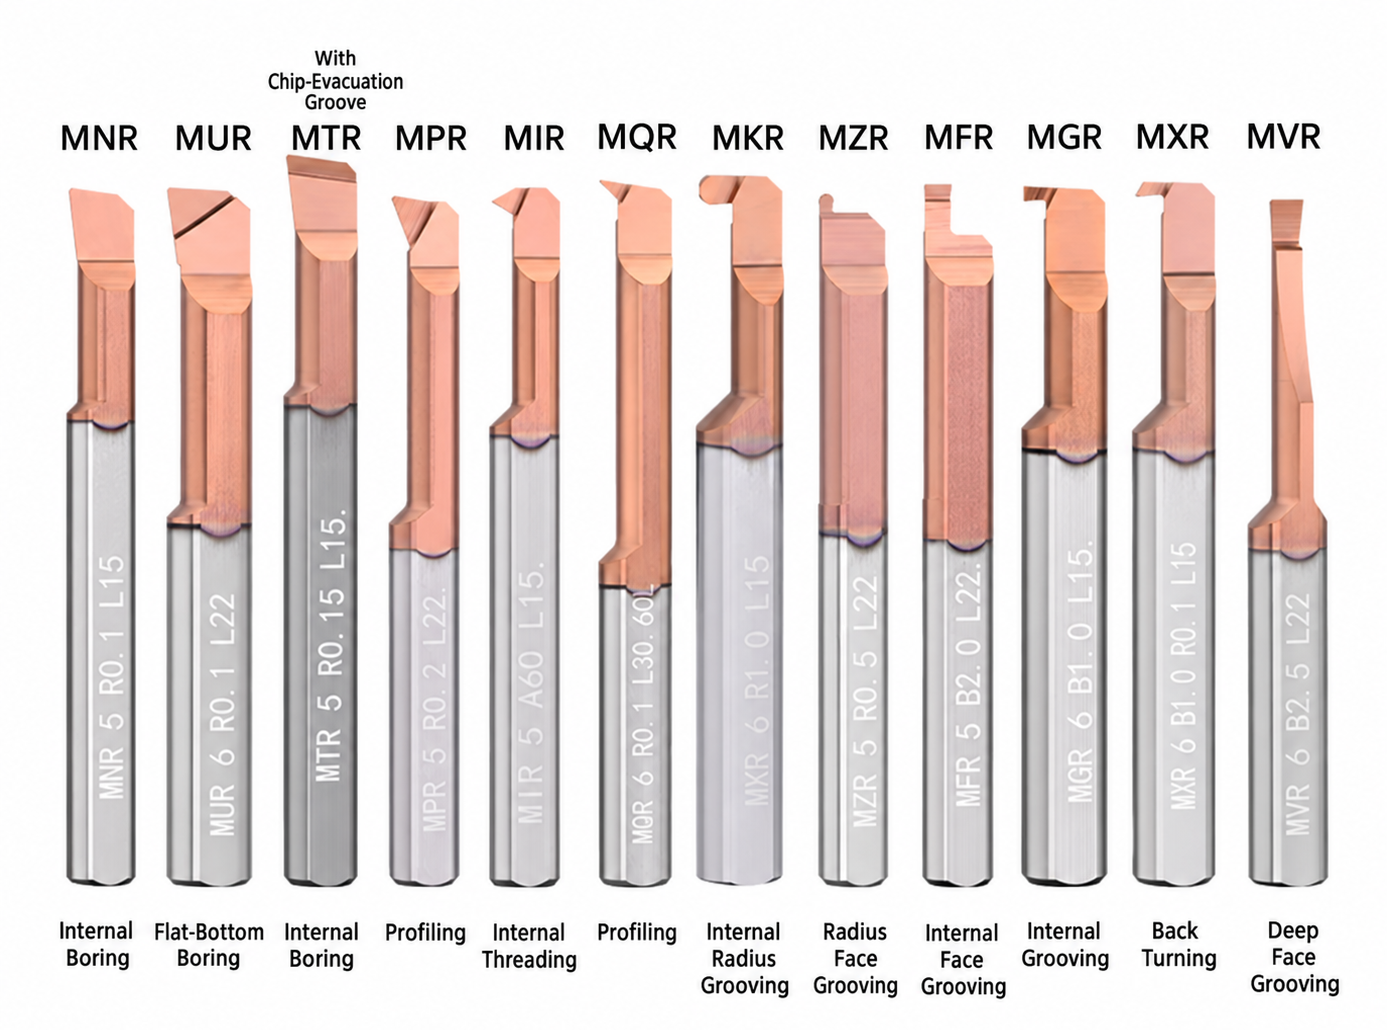
Micro Internal Machining Methods
Recommended Workpiece Materials

Compatibilidad de la máquina
Internal back turning and recessed features.
Miniature and high-volume precision parts.
Repeatable machining of internal rear faces.
Prototype and small-batch internal machining.
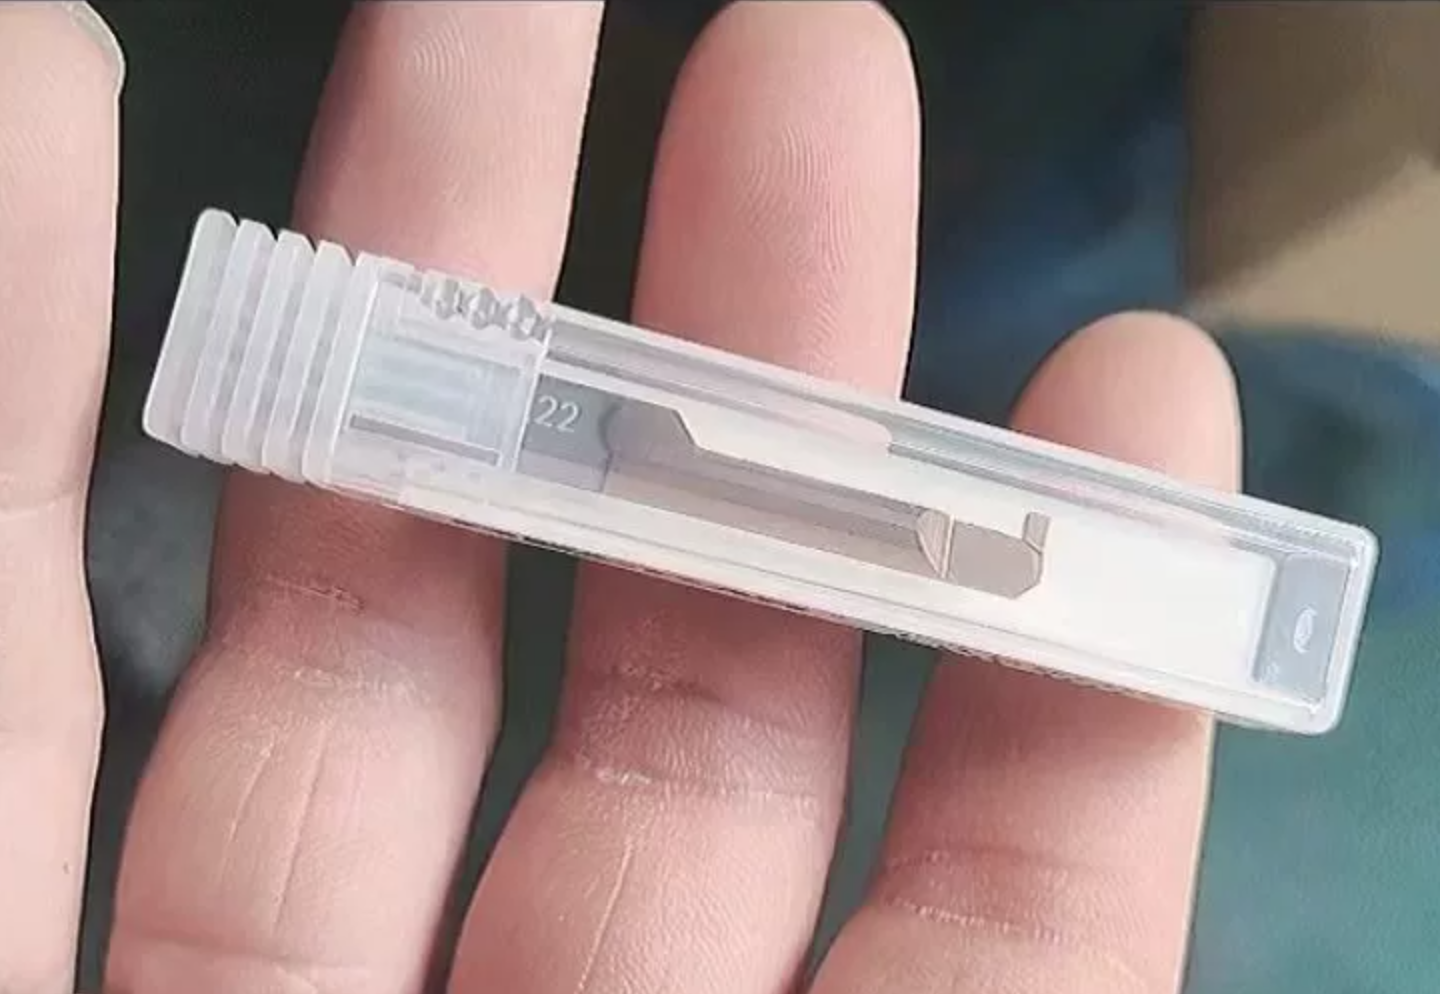
Product Detail Photos

Product Video
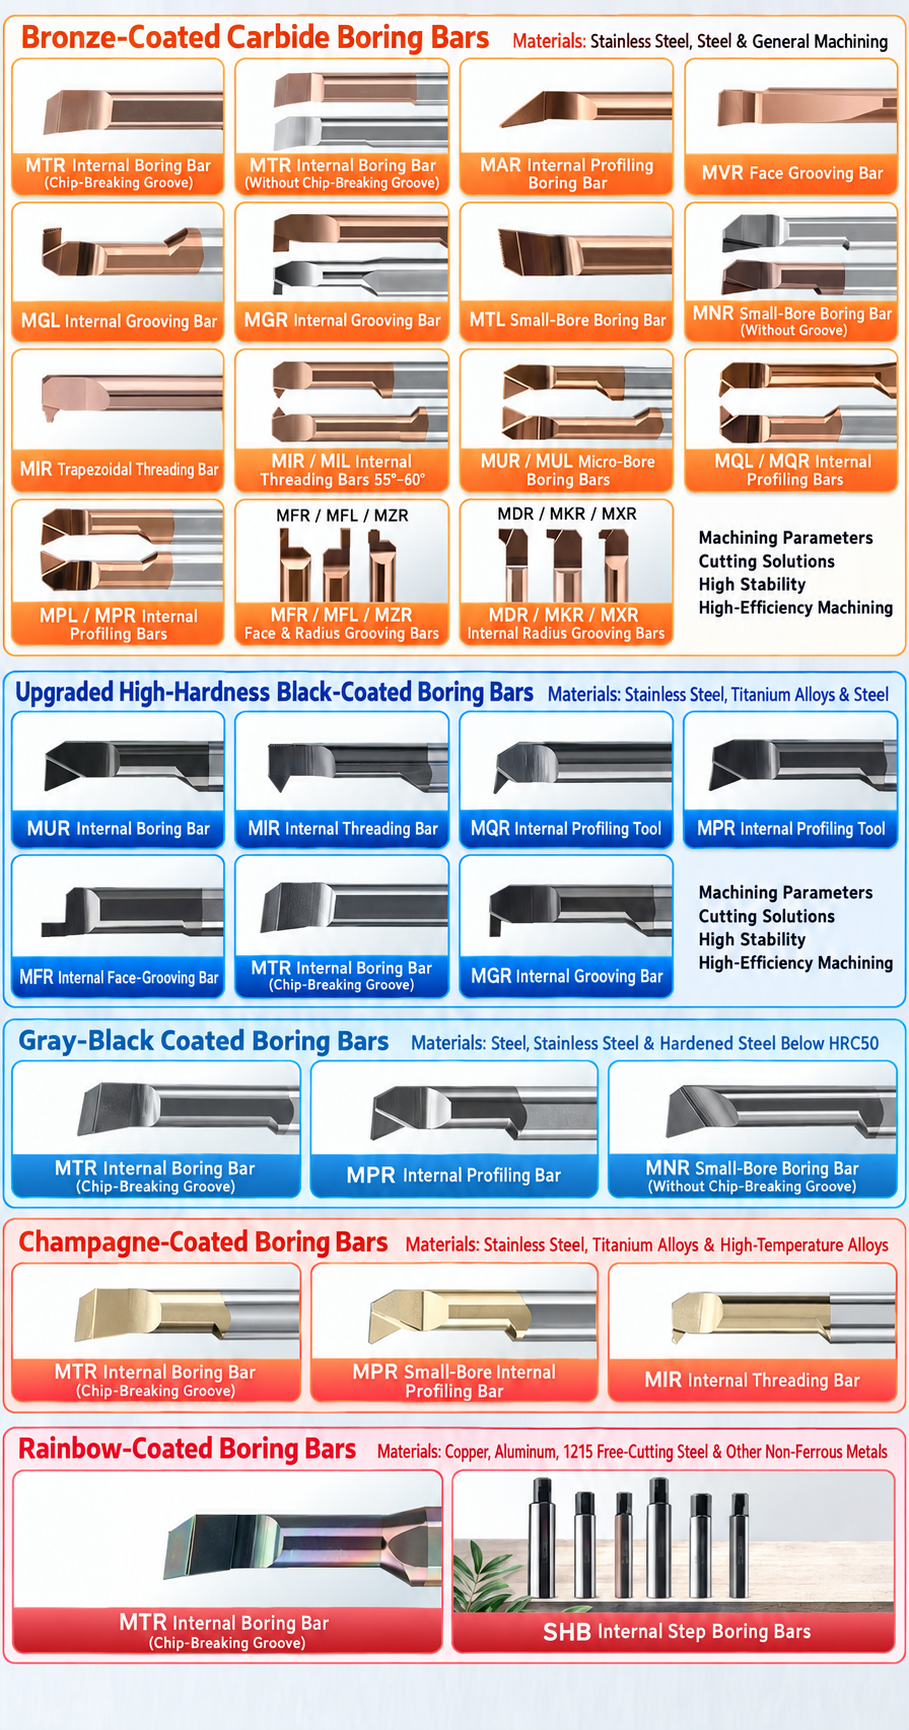
Back-Turning Toolpath
Selection Recommendation
Select the MXR model according to cutting diameter d1, nose radius R, cutting width B, cutting depth Q, clearance length L1 and shank diameter D. Verify that the cutting edge can pass through the bore and move behind the shoulder without collision. Use the shortest practical clearance length to maximize tool rigidity.
MXR Series Specifications
The MXR Series includes solid carbide micro back turning bars for machining internal rear faces, undercuts and recessed features behind shoulders. Standard models cover cutting diameters from Ø2.8 to Ø5.9 mm. All dimensions shown below are in millimeters.
Model Designation
| Código | Meaning | Example Value |
|---|---|---|
| MXR | Tool series | Micro back turning bar |
| 49 | Cutting diameter d1 | Ø4.9 mm |
| R020 | Nose radius R | R0.20 mm |
| L220 | Clearance length L1 | 22 mm |
| 550 | Shank diameter D and overall length L | Ø5 mm shank, 50 mm overall length |
Custom tools and special geometries may use different model coding. Confirm all dimensions on the approved production drawing before ordering.
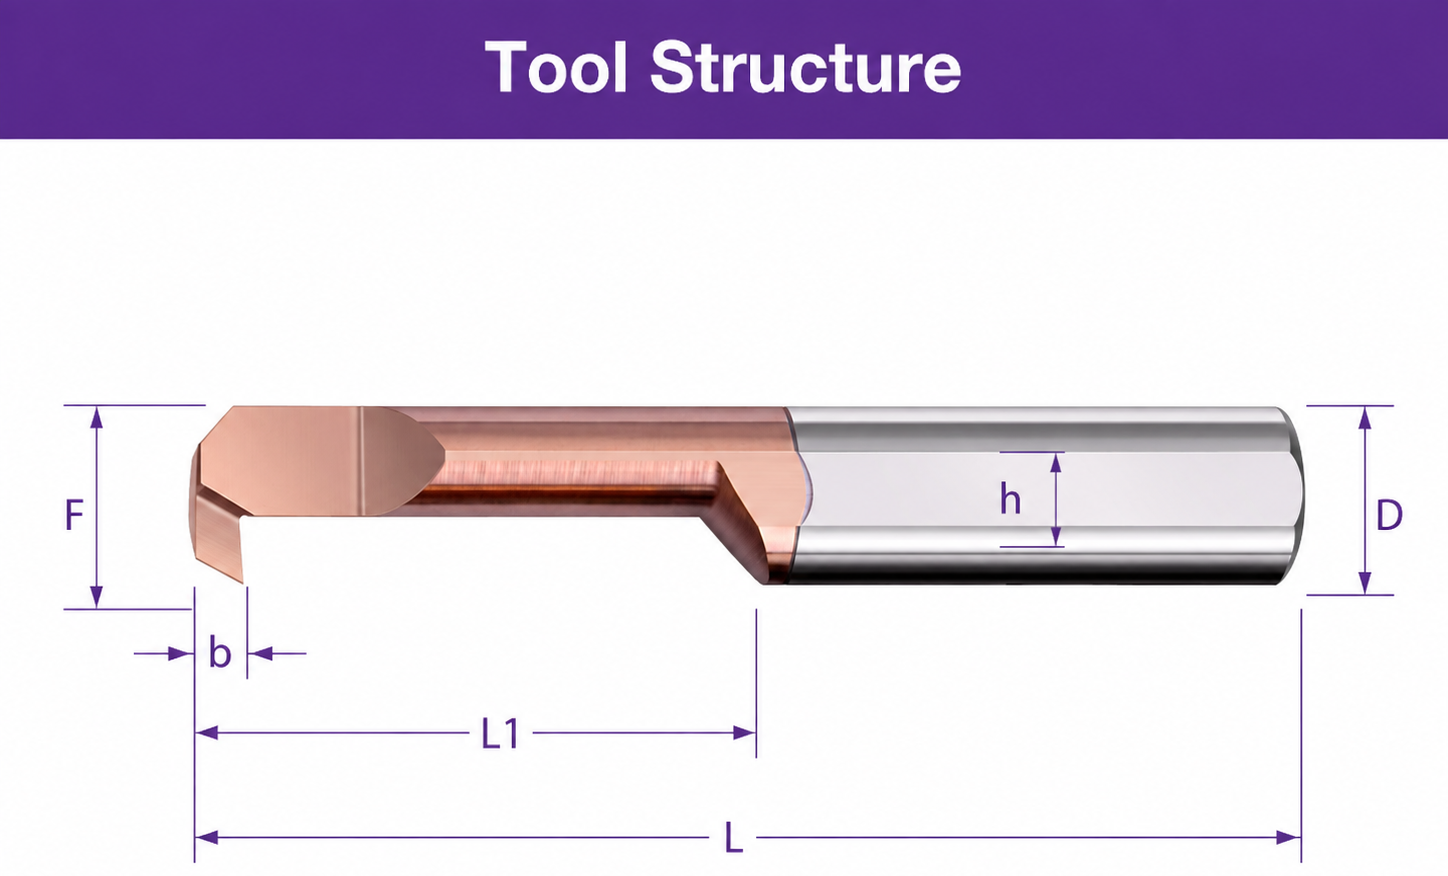
Dimension Definitions
| Symbol | Dimension | Descripción |
|---|---|---|
| d1 | Diámetro de corte | Diameter represented by the cutting edge and used to identify the MXR model size. |
| R | Radio de la nariz | Cutting-edge radius affecting edge strength, profile accuracy and surface finish. |
| B | Cutting Width | Width of the back-turning cutting geometry shown in the technical drawing. |
| Q | Cutting Depth | Catalog depth dimension available for machining the rear feature. |
| L1 | Clearance Length | Reduced-neck length available for reaching behind an internal shoulder. |
| D | Diámetro del vástago | Nominal cylindrical shank diameter used for toolholding. |
| L | Longitud total | Total length from the cutting edge to the end of the carbide shank. |
Dimensions and Standard Sizes
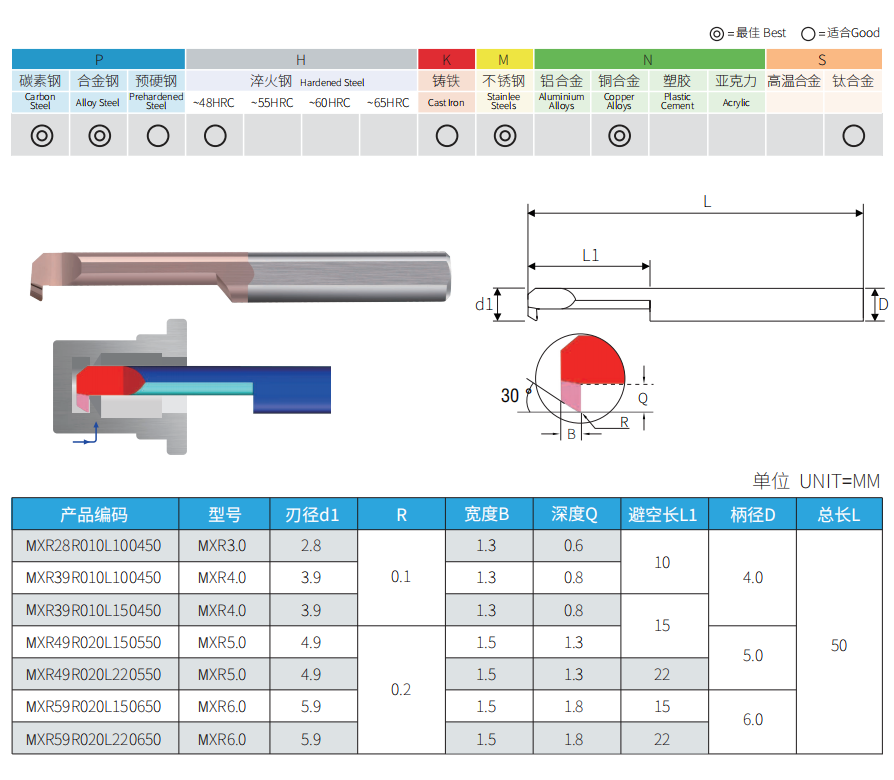
Click the dimension chart to open the full-size image.
Standard Model Range
| Modelo | d1 | R | B | Q | L1 | D | L |
|---|---|---|---|---|---|---|---|
| MXR3.0 | 2.8 | 0.10 | 1.3 | 0.6 | 10 | 4 | 50 |
| MXR4.0 | 3.9 | 0.10 | 1.3 | 0.8 | 10 / 15 | 4 | 50 |
| MXR5.0 | 4.9 | 0.20 | 1.5 | 1.3 | 15 / 22 | 5 | 50 |
| MXR6.0 | 5.9 | 0.20 | 1.5 | 1.8 | 15 / 22 | 6 | 50 |
Specification Range Summary
Selection Guidance
Recommended Starting Conditions
- Set the cutting edge accurately on the spindle centerline.
- Confirm the spindle direction and programmed reverse-feed direction.
- Simulate the complete entry, positioning, cutting and retraction path.
- Do not move the tool radially into cutting position before it has cleared the shoulder.
- Begin with a conservative cutting depth and feed, especially on the 22 mm clearance-length models.
- Use suitable coolant or compressed air to prevent chip accumulation behind the shoulder.
- Reduce the cutting load if vibration, taper or rear-face dimensional variation occurs.
Related Micro Internal Tool Series
Internal Profiling: MUR Series
Complex Profiling: MQR Series
General Internal Boring: MTR Series
Internal Grooving: MGR Series
We support distributors, tooling suppliers and industrial partners with flexible OEM and private label solutions for micro internal tooling products. From laser marking and customized packaging to product identification and technical documentation, we help customers build their own tooling product lines with reliable manufacturing support.
OEM Product Scope
We provide OEM and private label manufacturing solutions for micro internal tooling products, supporting distributors and tooling suppliers with standard series, customized specifications and drawing-based production.
MPR series and customized small-diameter boring tools for precision internal machining and anti-vibration applications.
MIR/MIL series with customized thread profiles, dimensions and product identification requirements.
Internal grooving and special groove solutions for miniature precision components.
Non-standard dimensions, special geometries and customer drawing-based tooling solutions are available.

Customization Options
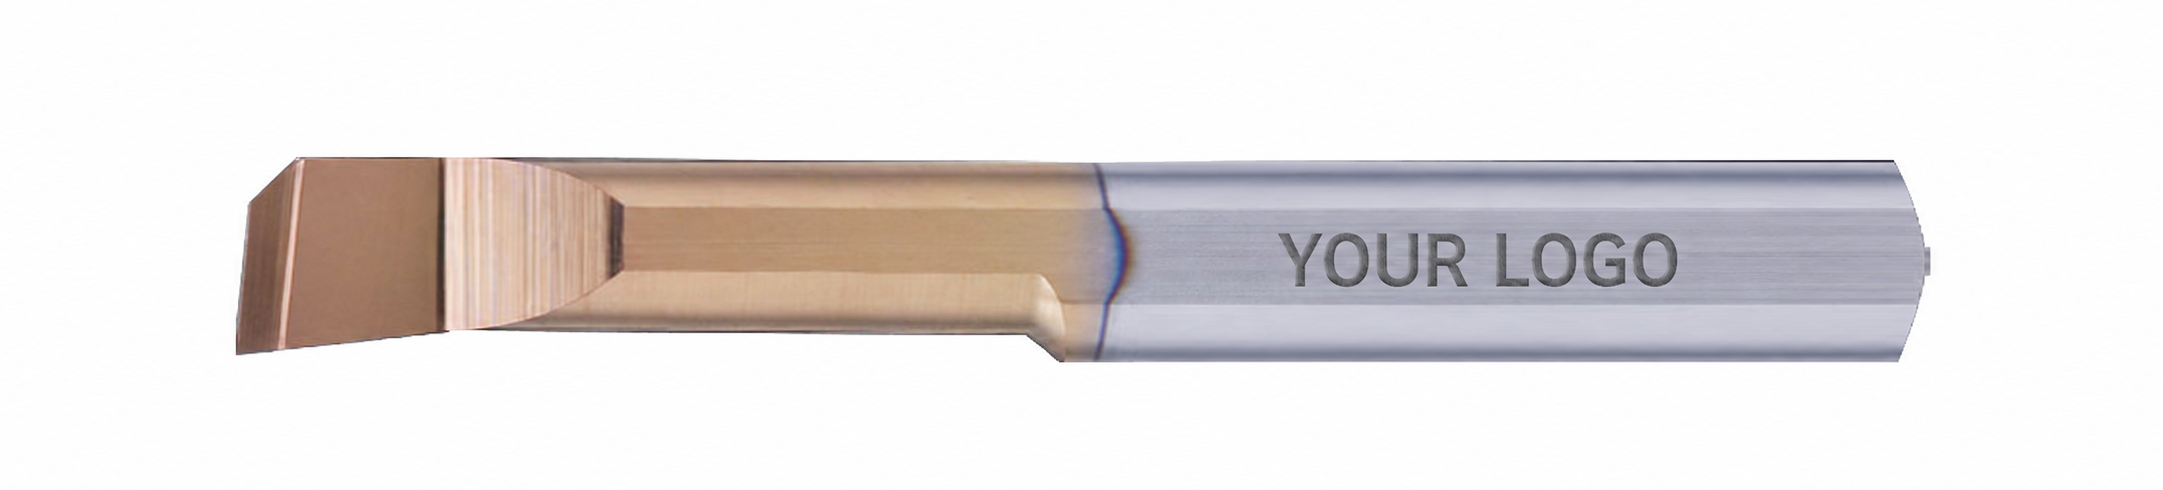
Laser Marking & Product Identification
Custom logo, model number and product identification marking can be provided according to distributor and brand requirements.
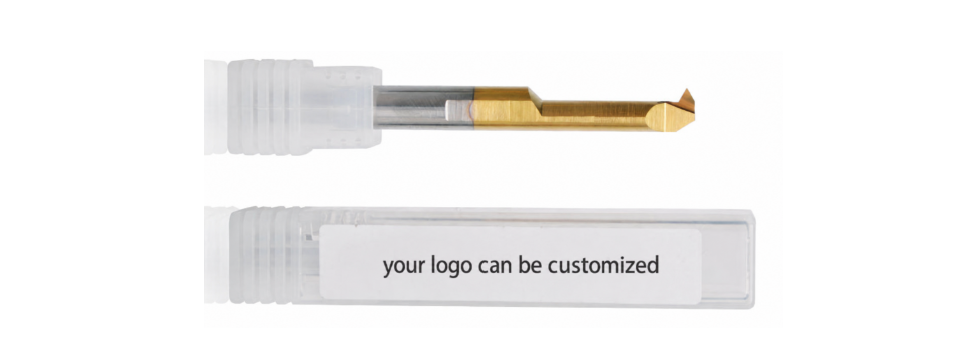
Custom Packaging
Individual packaging, labels and product information can be customized to support reseller sales channels and private brand development.
Technical Documents & Product Support
Support technical drawings, specifications and product information to help distributors promote and manage their tooling products.
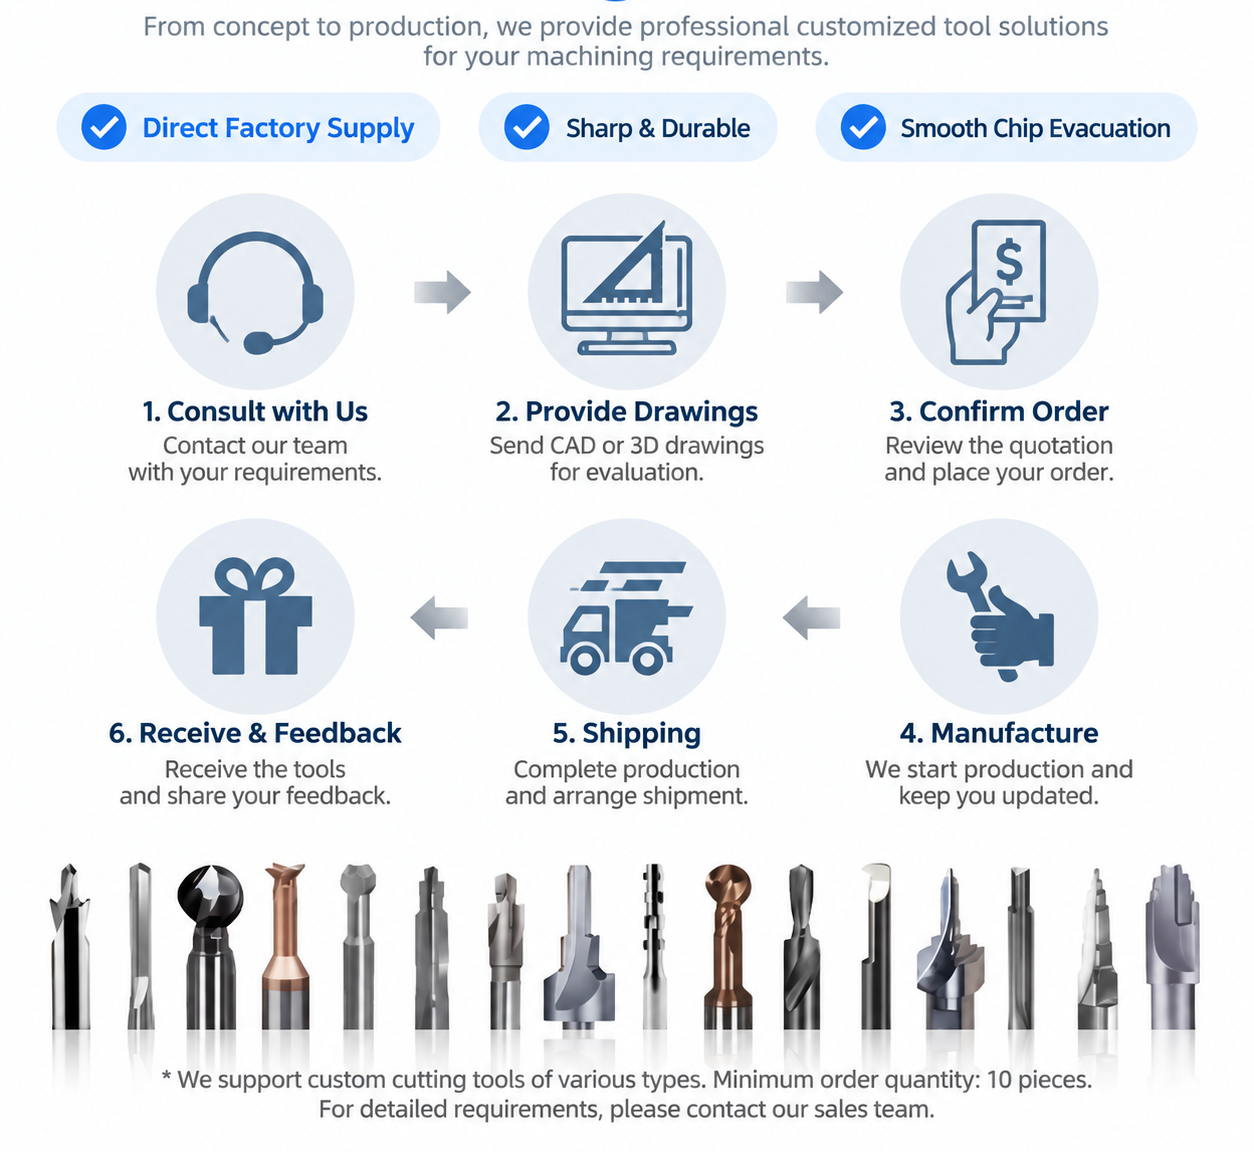
OEM Workflow
Confirm drawings, specifications, materials and packaging requirements.
Finalize tool design, marking details and production requirements.
Provide samples for testing and approval before batch production.
Produce and inspect according to confirmed requirements.
Private Label Support for Distributors
For distributors and tooling resellers, we provide flexible private label support including customized marking, packaging solutions and product documentation to help establish a professional tooling product range.
We follow strict quality control procedures from raw material inspection to final shipment. Each tool is inspected to ensure consistent dimensions, cutting performance and reliable quality for industrial machining applications.
Proceso de control de calidad
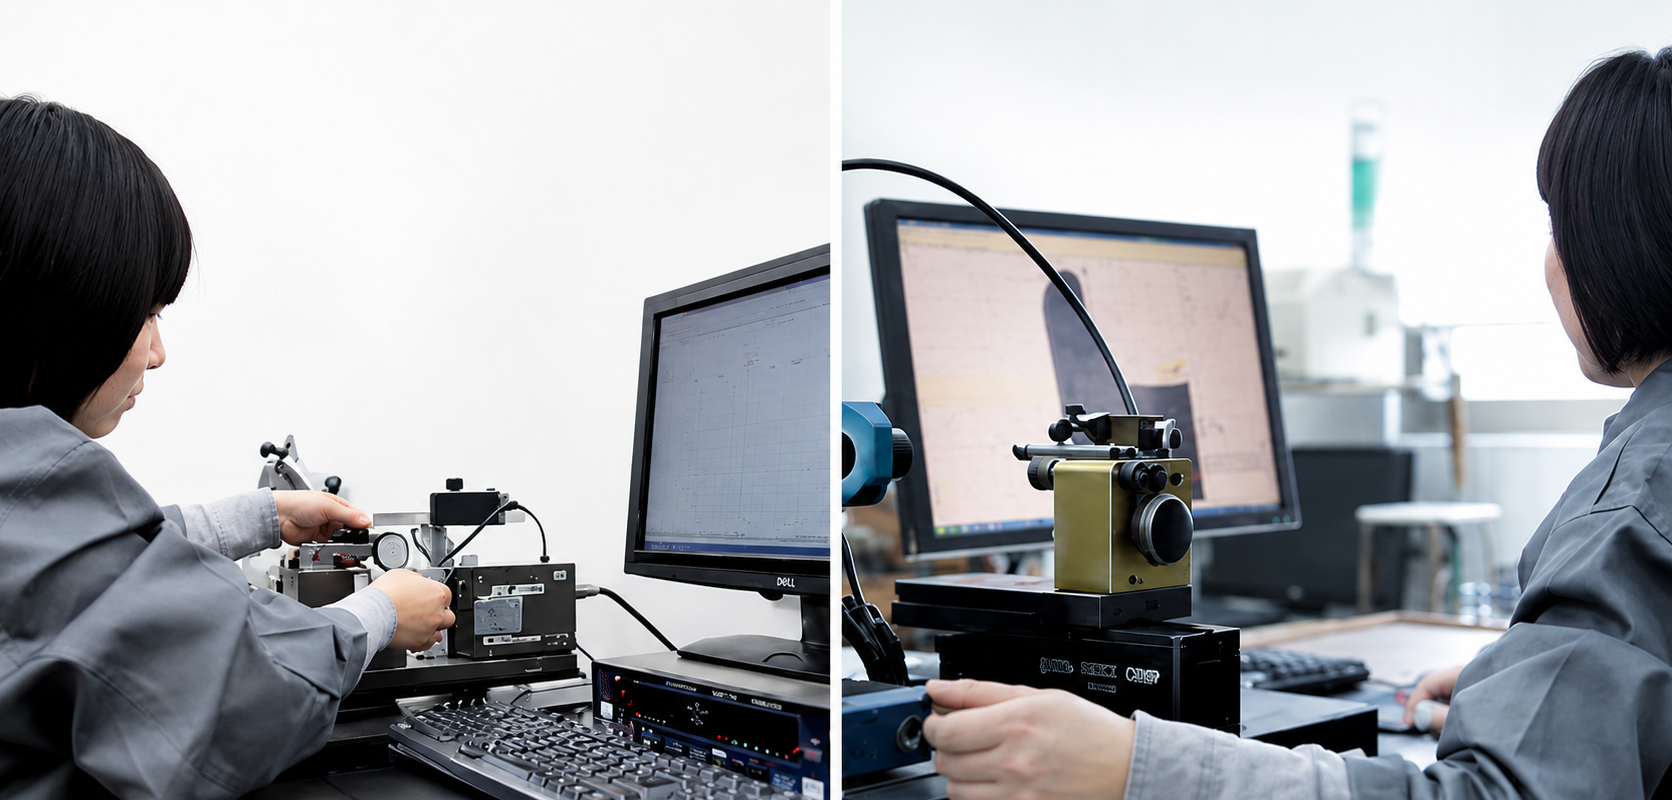
Verify carbide material quality and consistency before production.
Control tool geometry, dimensions and cutting edge accuracy during manufacturing.
Inspect edge quality and surface finish to maintain stable cutting performance.
Confirm product specifications before packing and shipment.
Inspection Standards
| Inspection Item | Purpose |
|---|---|
| Material Inspection | Verify carbide quality and material consistency. |
| Dimension Inspection | Confirm tool size and tolerance requirements. |
| Cutting Edge Inspection | Check edge geometry and surface quality. |
| Final Inspection | Ensure products meet confirmed specifications before delivery. |
Packing & Protection

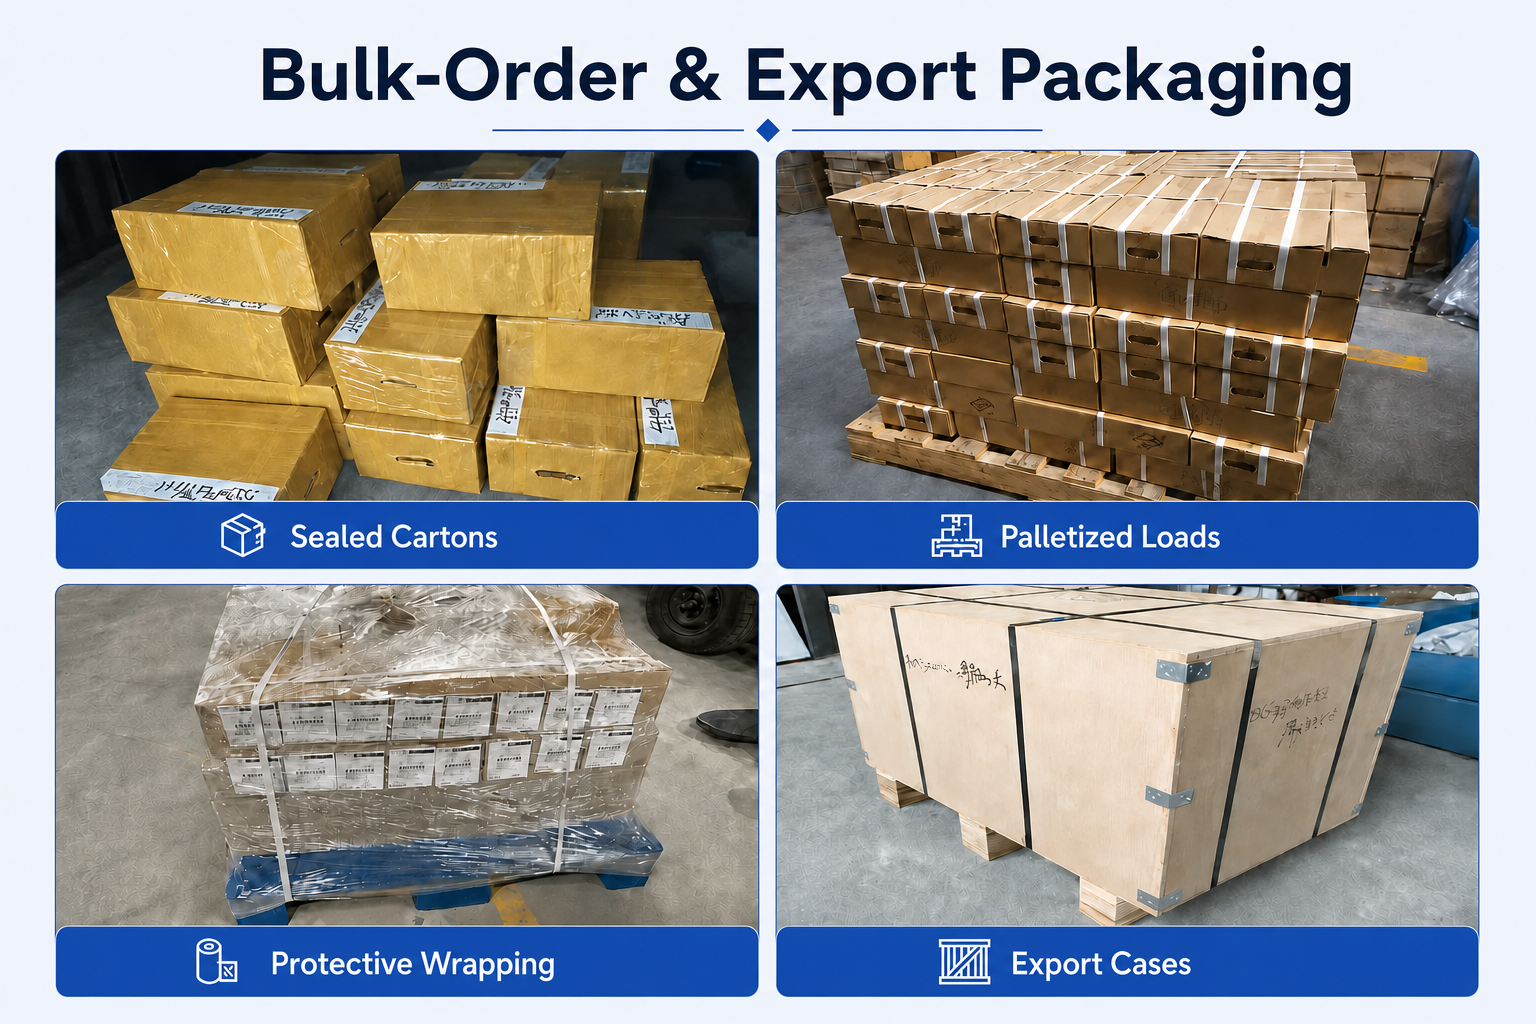
Individual protection and export packaging help prevent tool damage during storage and international transportation.
- Individual tool protection
- Product identification labels
- Batch traceability support
- Export shipment protection
Production & Delivery Workflow
Confirmación del pedido
Production Scheduling
Quality Inspection
Packing
Shipment

Delivery Support
Standard products can usually be shipped within 1–3 working days after order confirmation. Customized products require confirmation according to tool design, quantity and production requirements.
FAQ & Downloads
Product FAQs
What are MXR micro back turning bars used for?
What cutting diameters are available?
What cutting widths and depths are available?
What does the 30° geometry represent?
Selection & Application FAQs
How do I select the correct MXR back turning bar?
How is an MXR tool different from a conventional boring bar?
What materials can be machined with MXR back turning bars?
How can I prevent a collision during back turning?
How can I improve machining stability?
Ordering & OEM FAQs
Can you manufacture custom MXR back turning bars?
Can I order mixed models or trial quantities?
Is OEM marking and private-label packaging available?
What information is required for a quotation?
What is the lead time for MXR back turning bars?
Recursos técnicos
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.