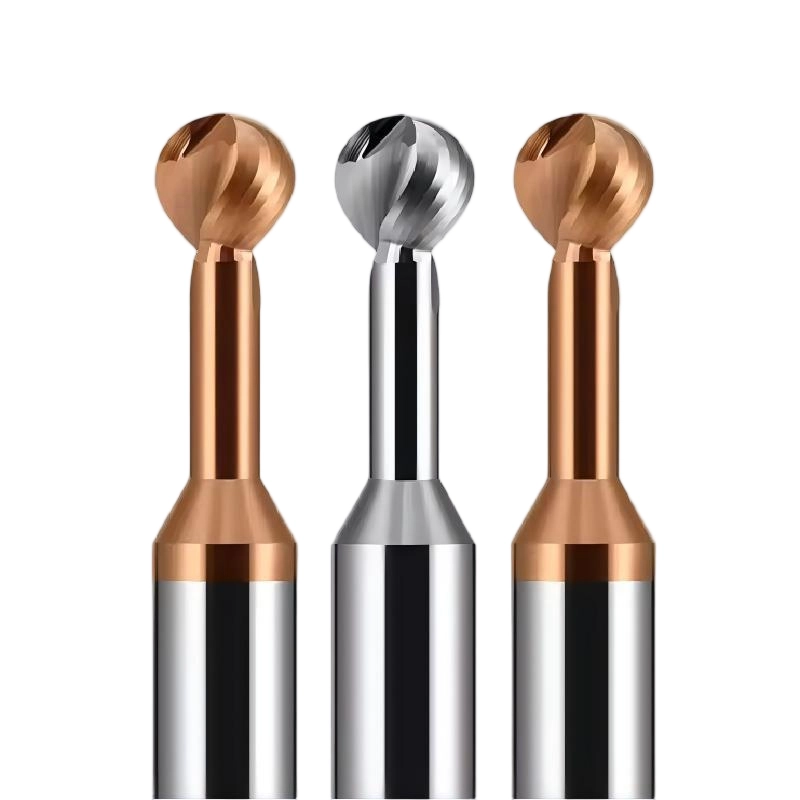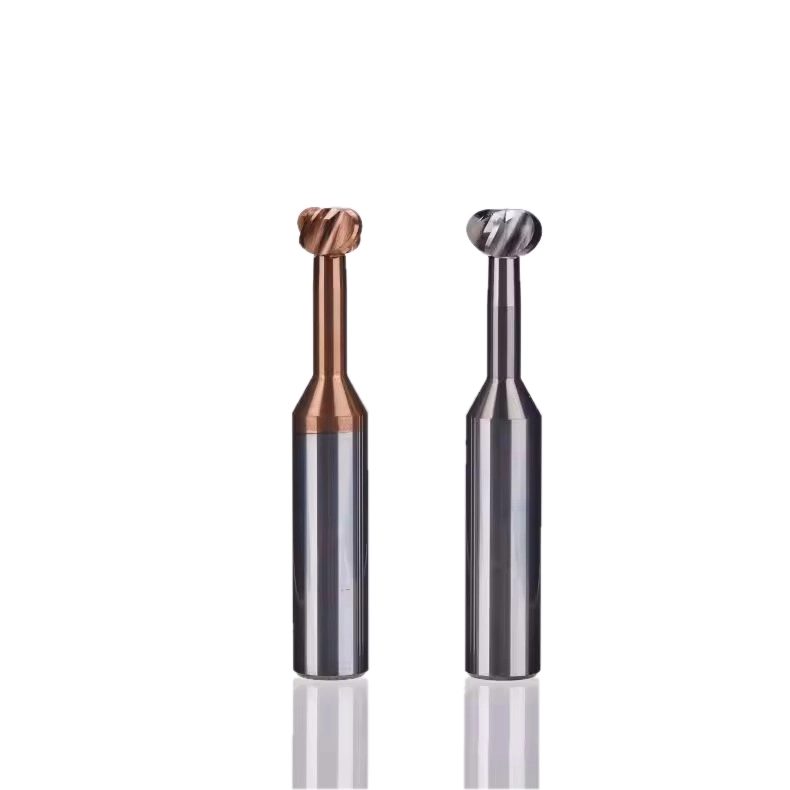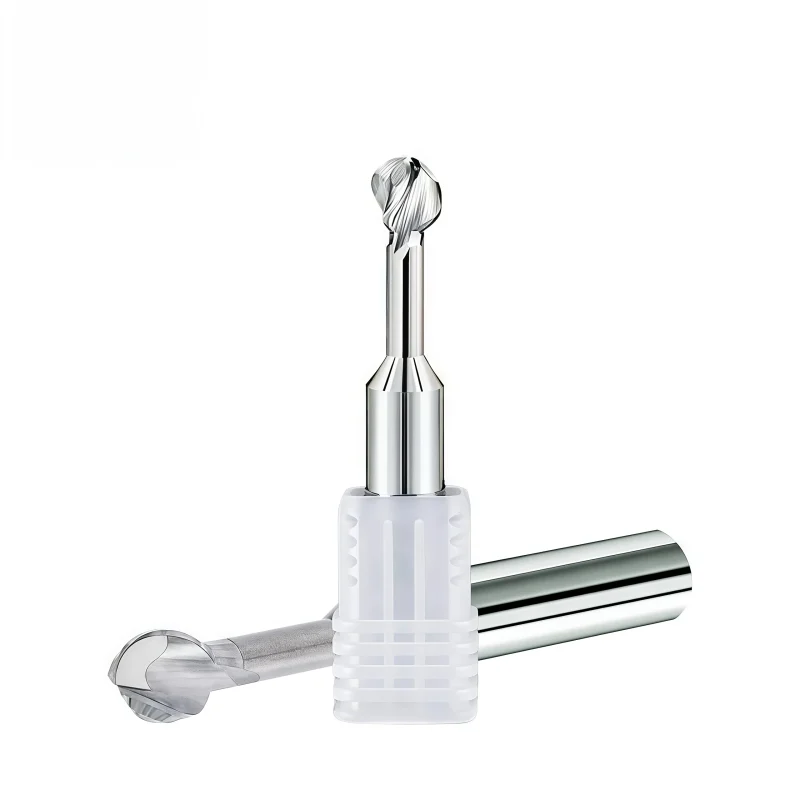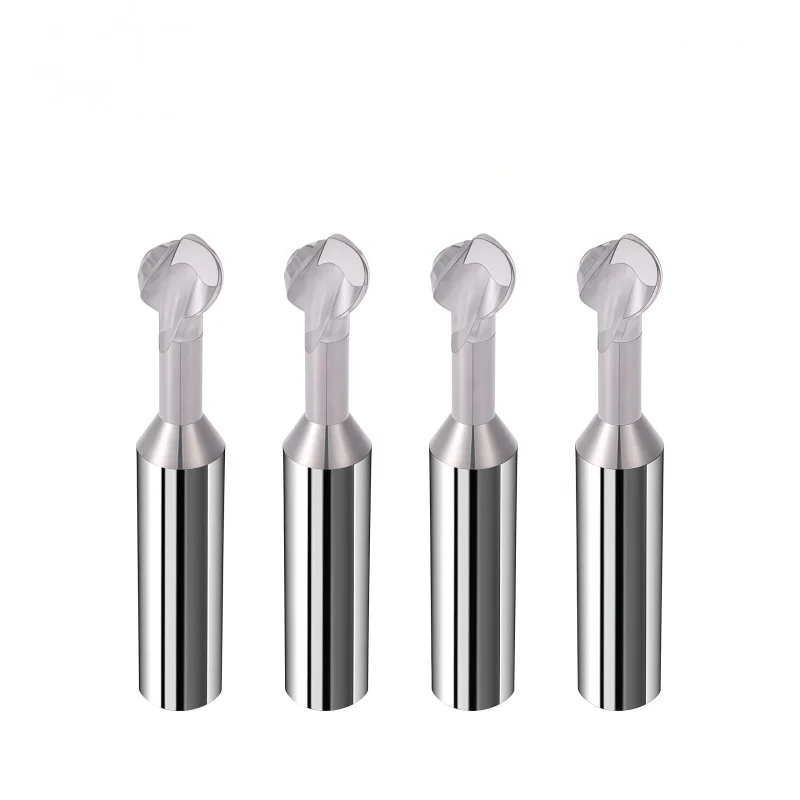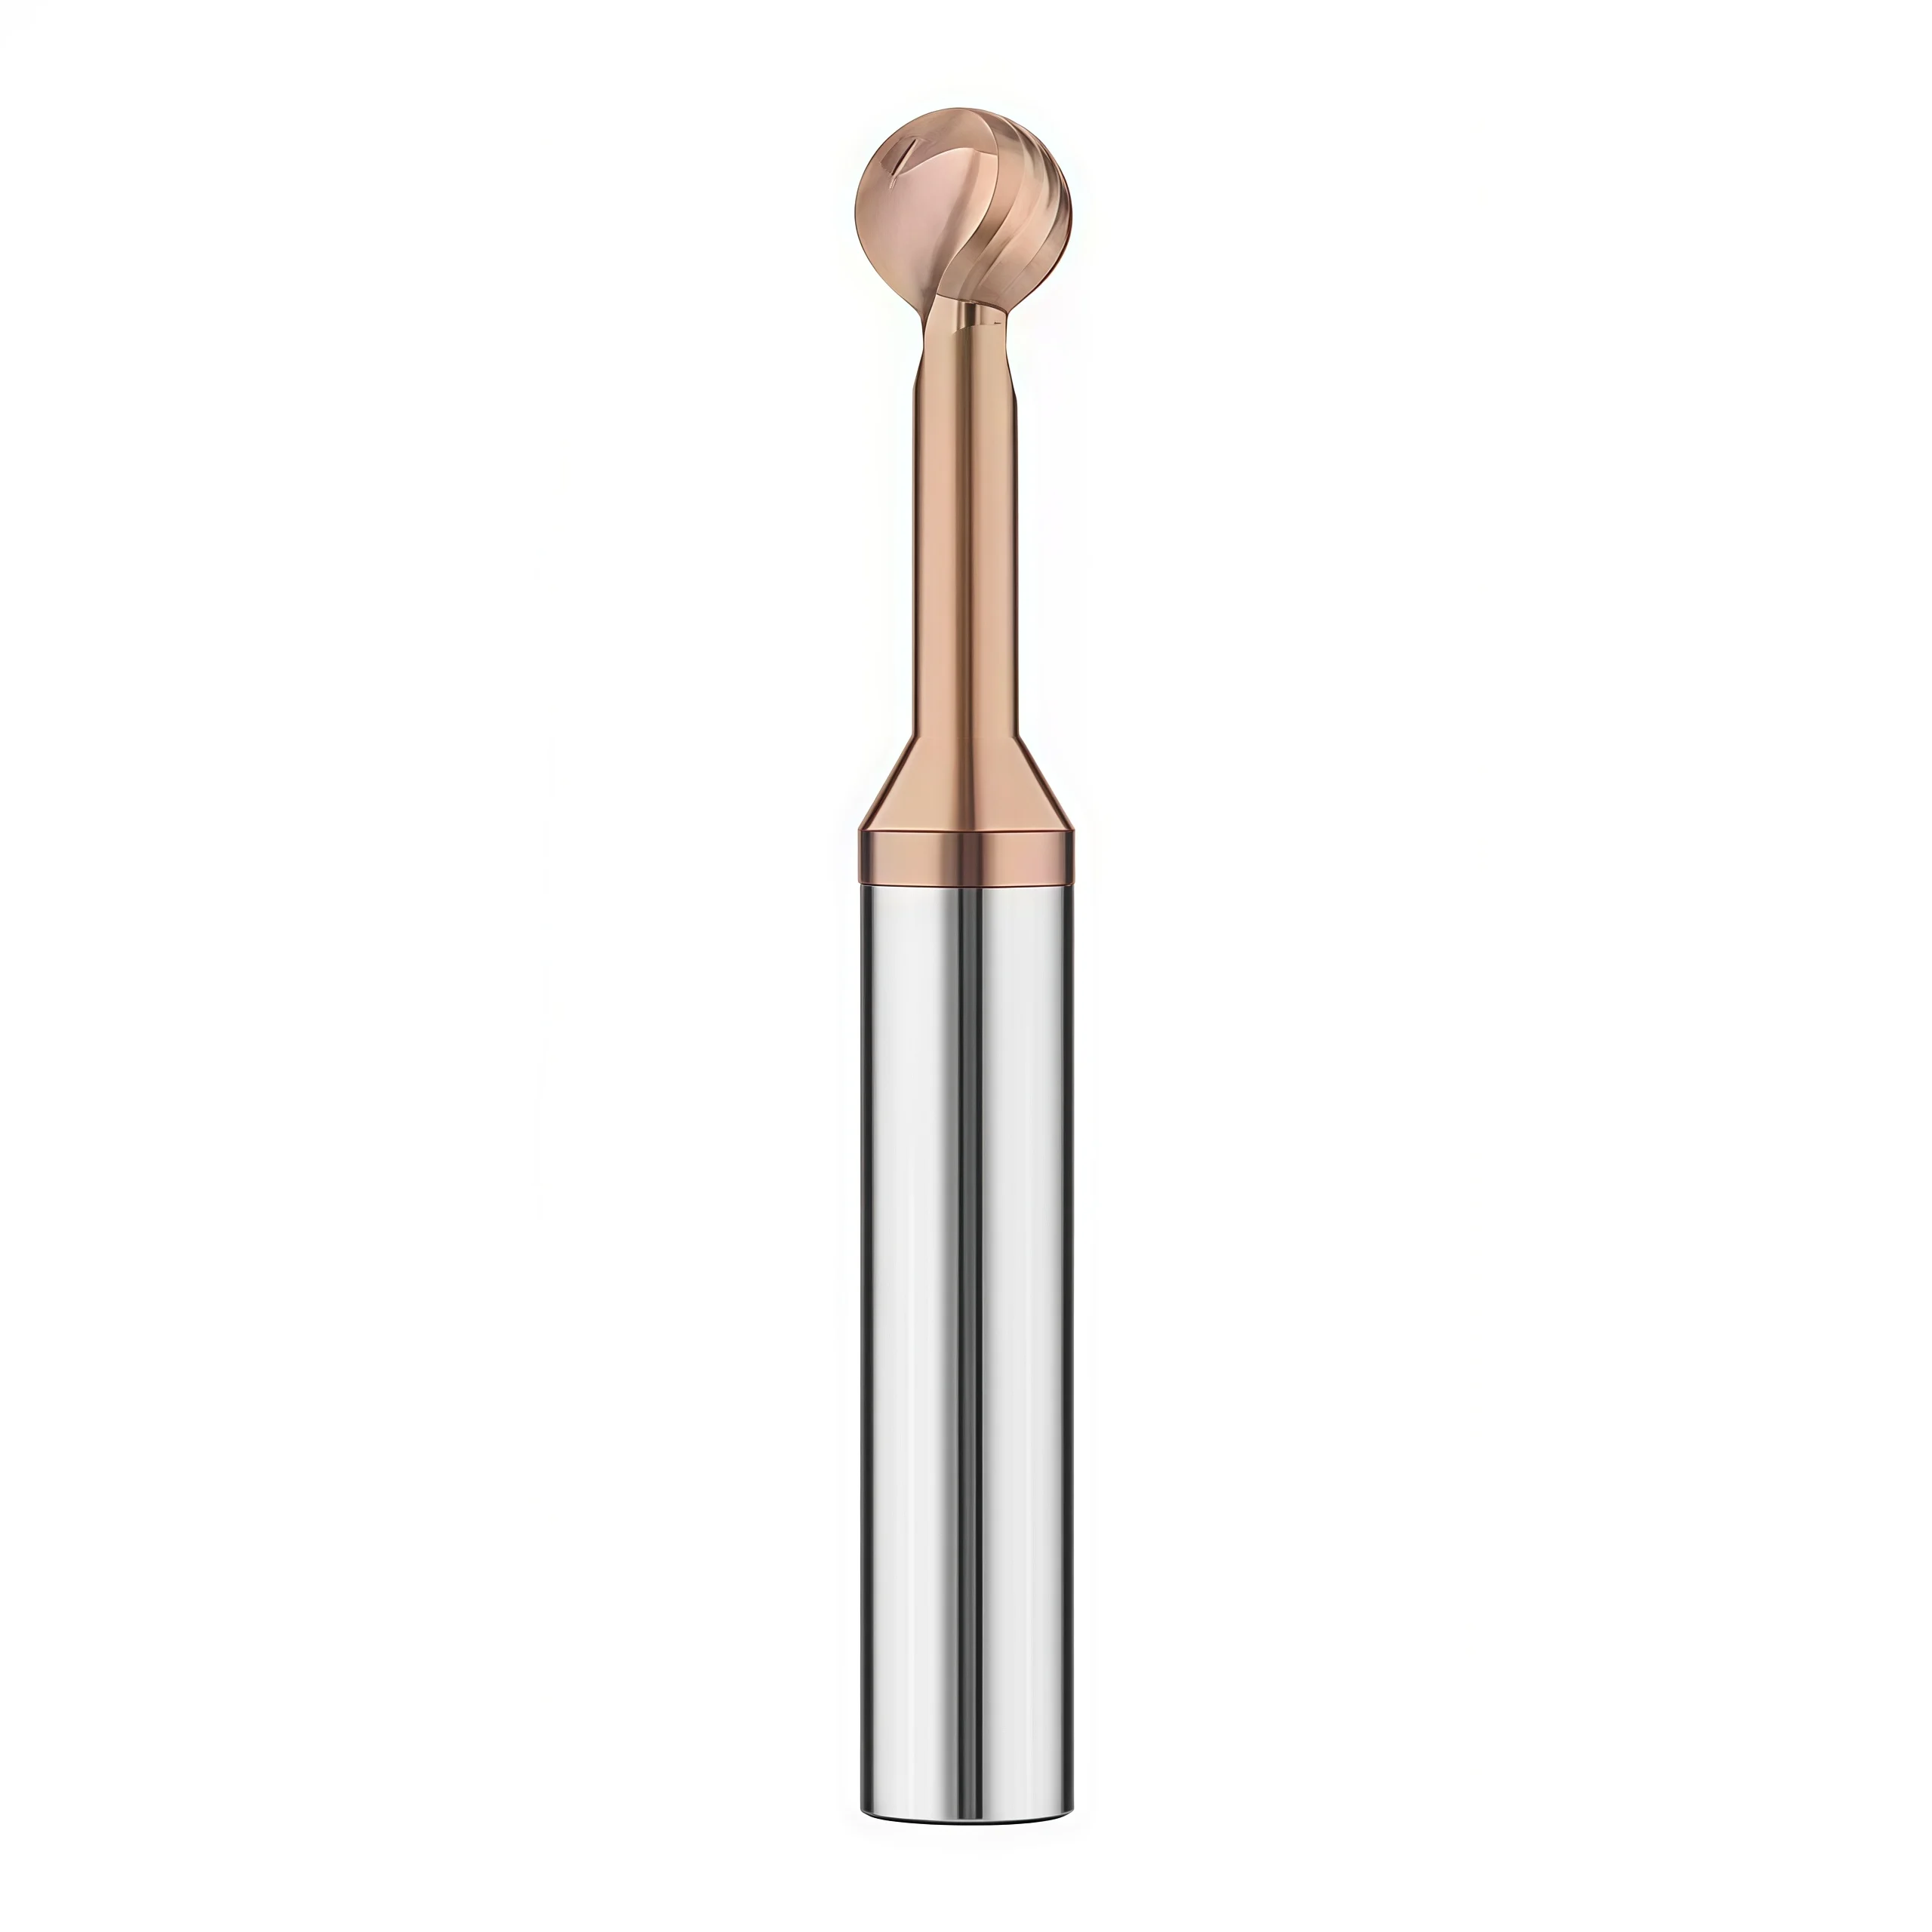
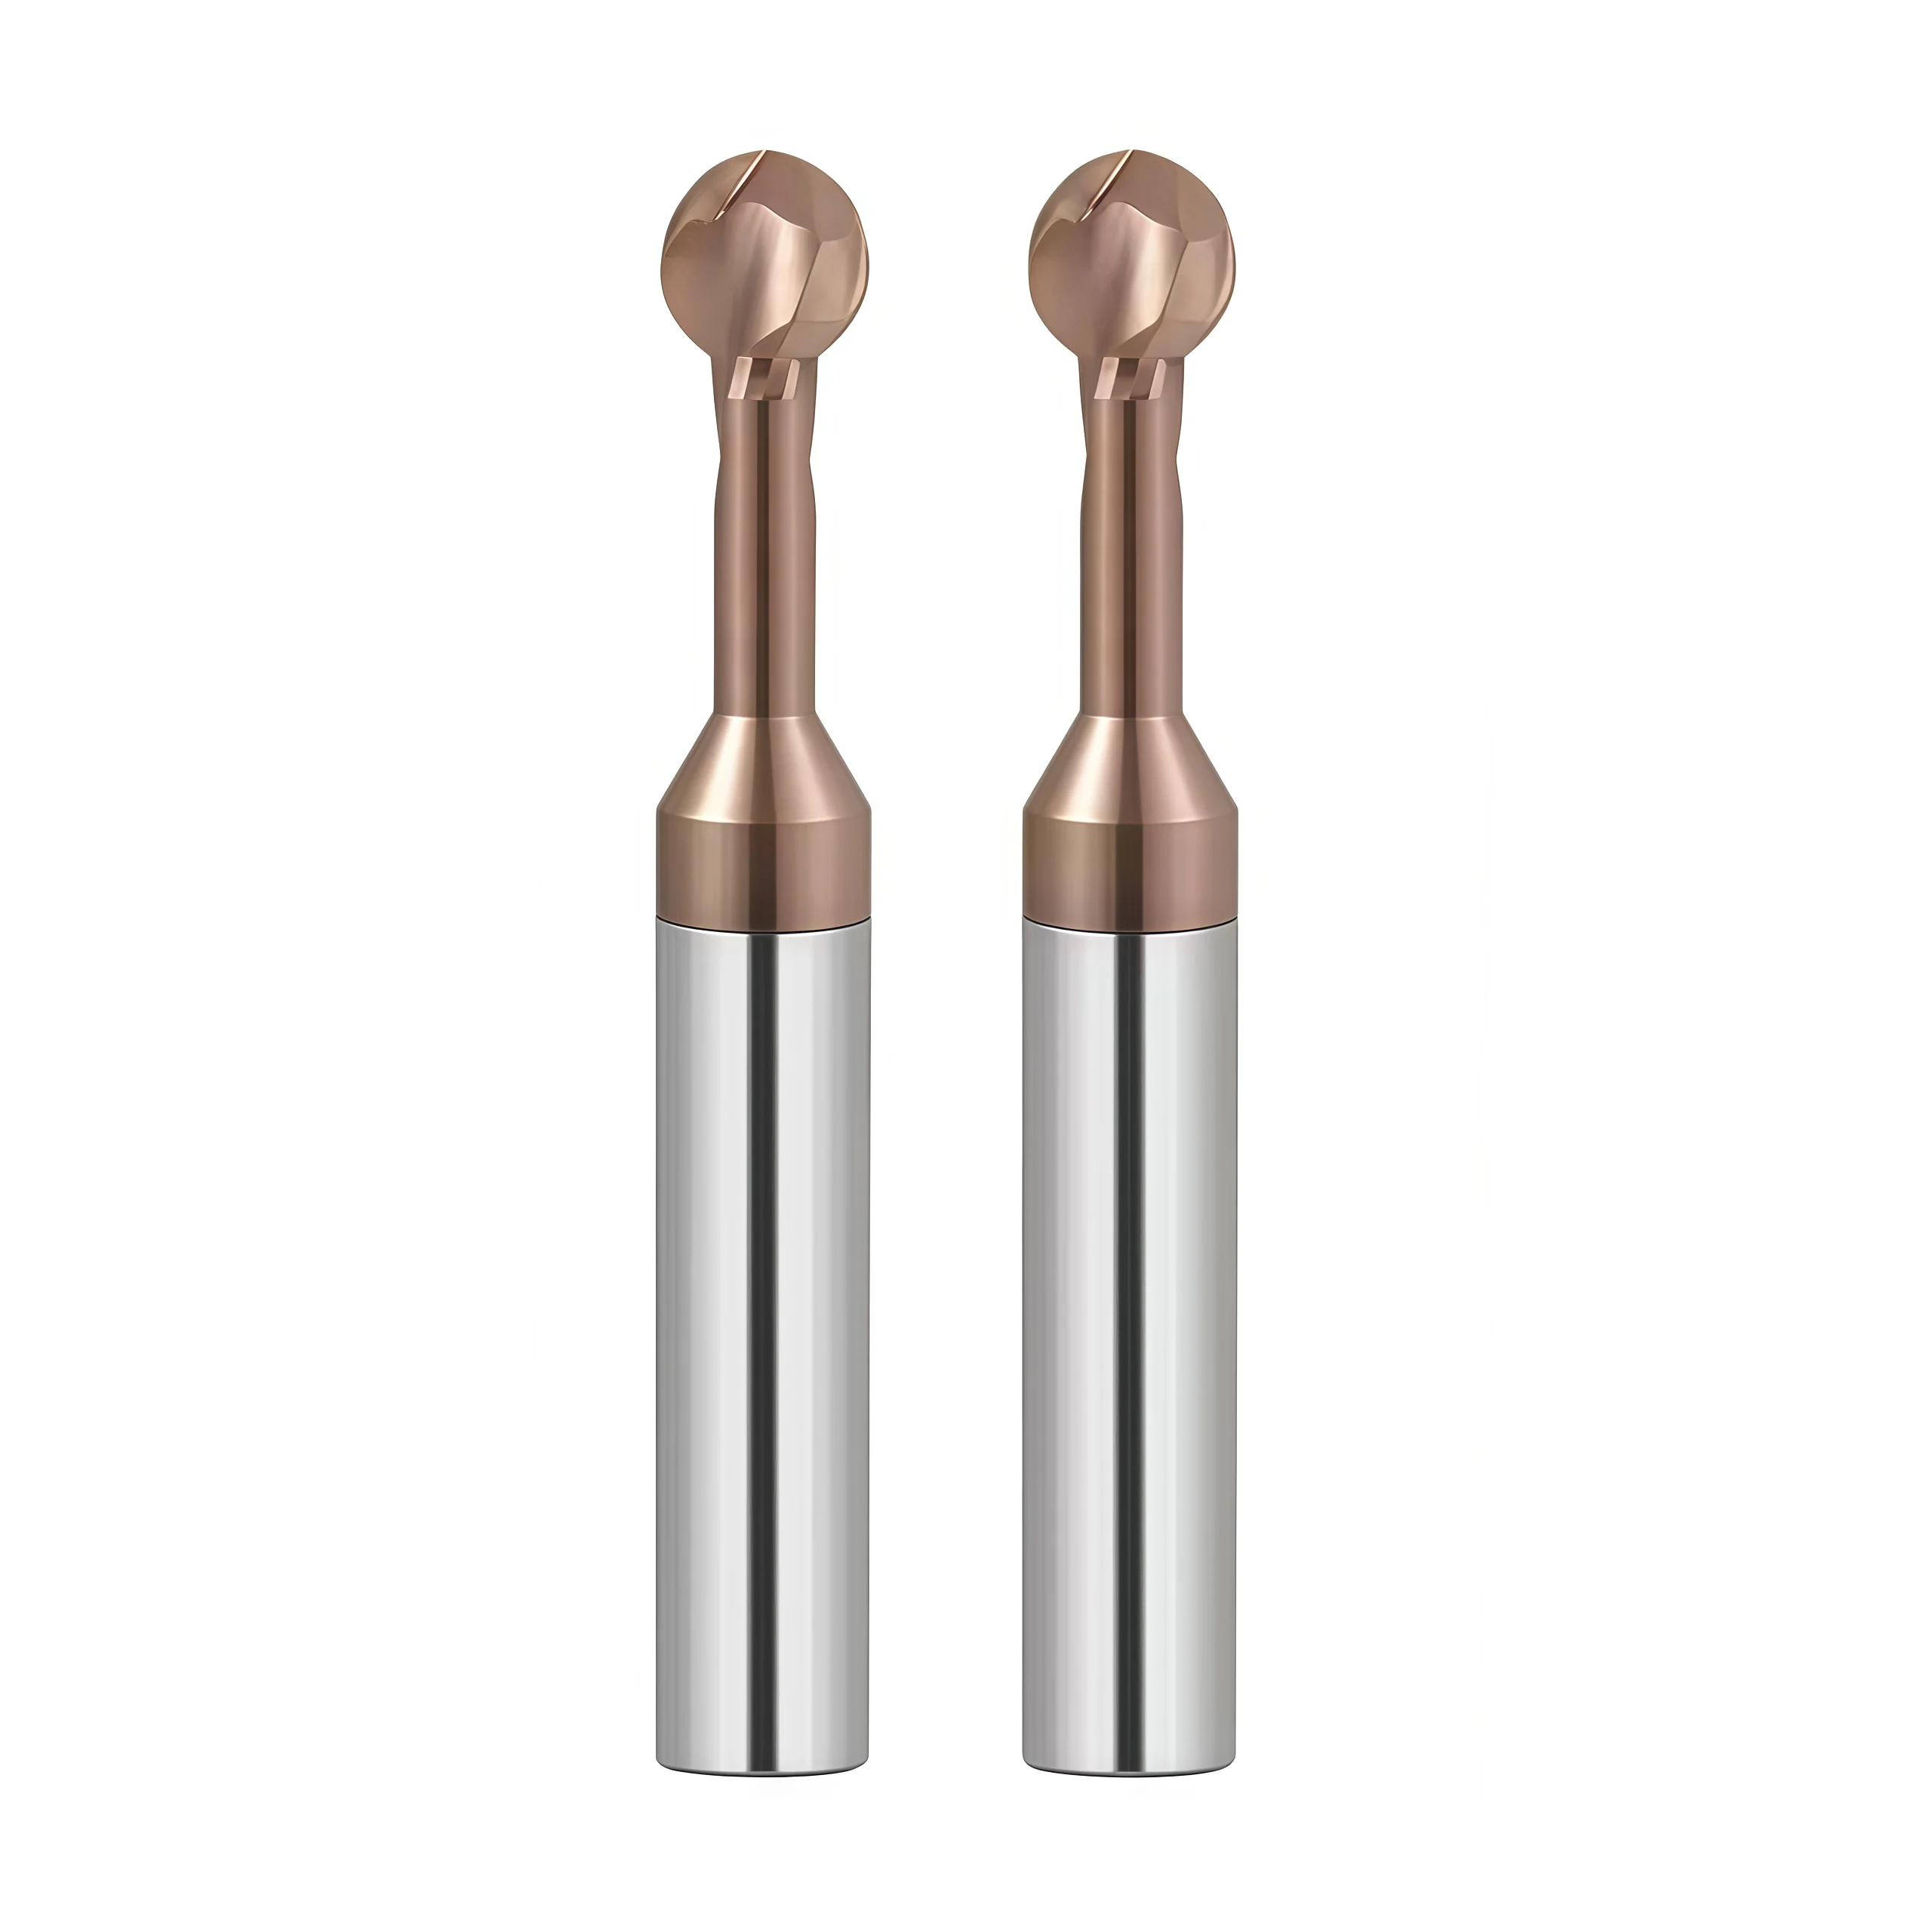
Solid Carbide Lollipop Ball Nose End Mill R1–R10 for T-Slot Milling
Solid carbide lollipop ball nose end mill for radiused T-slot milling, undercutting, backside profiling and recessed 3D machining. The spherical cutting head and relieved-neck geometry provide access behind shoulders and openings where conventional straight end mills cannot reach. Standard R1–R10 configurations cover different profile sizes, undercut depths and access requirements.
- ◆Spherical cutting head for radiused grooves, undercuts and recessed profiles
- ◆Relieved-neck geometry provides clearance for backside and difficult-to-reach machining
- ◆R1–R10 radius series supports small precision features through larger undercut applications
Calidad constante
Consistent geometry across repeat orders.
Pedidos flexibles
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
Herramientas estándar y personalizadas
Standard sizes and custom configurations.
Carbide Lollipop Ball Nose End Mill Overview
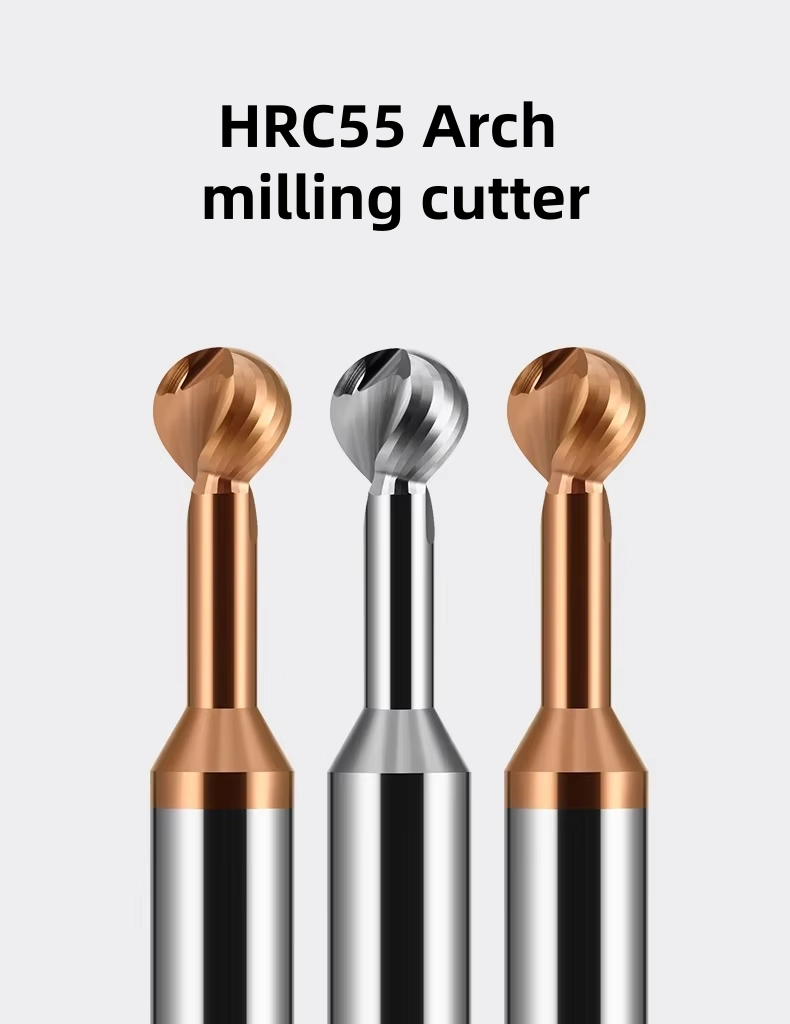
This solid carbide lollipop ball nose end mill is designed for radiused T-slot milling, undercutting, backside-edge machining and recessed 3D profiling where conventional straight end mills cannot reach. The near-spherical cutting head works together with a relieved neck to provide side and backside access after the tool enters through a suitable opening. Standard sizes cover R1–R10, with 2-tooth configurations used for R1–R6 and 3-tooth configurations for R7–R10.
Lollipop Ball Nose
R1–R10
2T / 3T
Carburo sólido
Lollipop Ball Nose Geometry
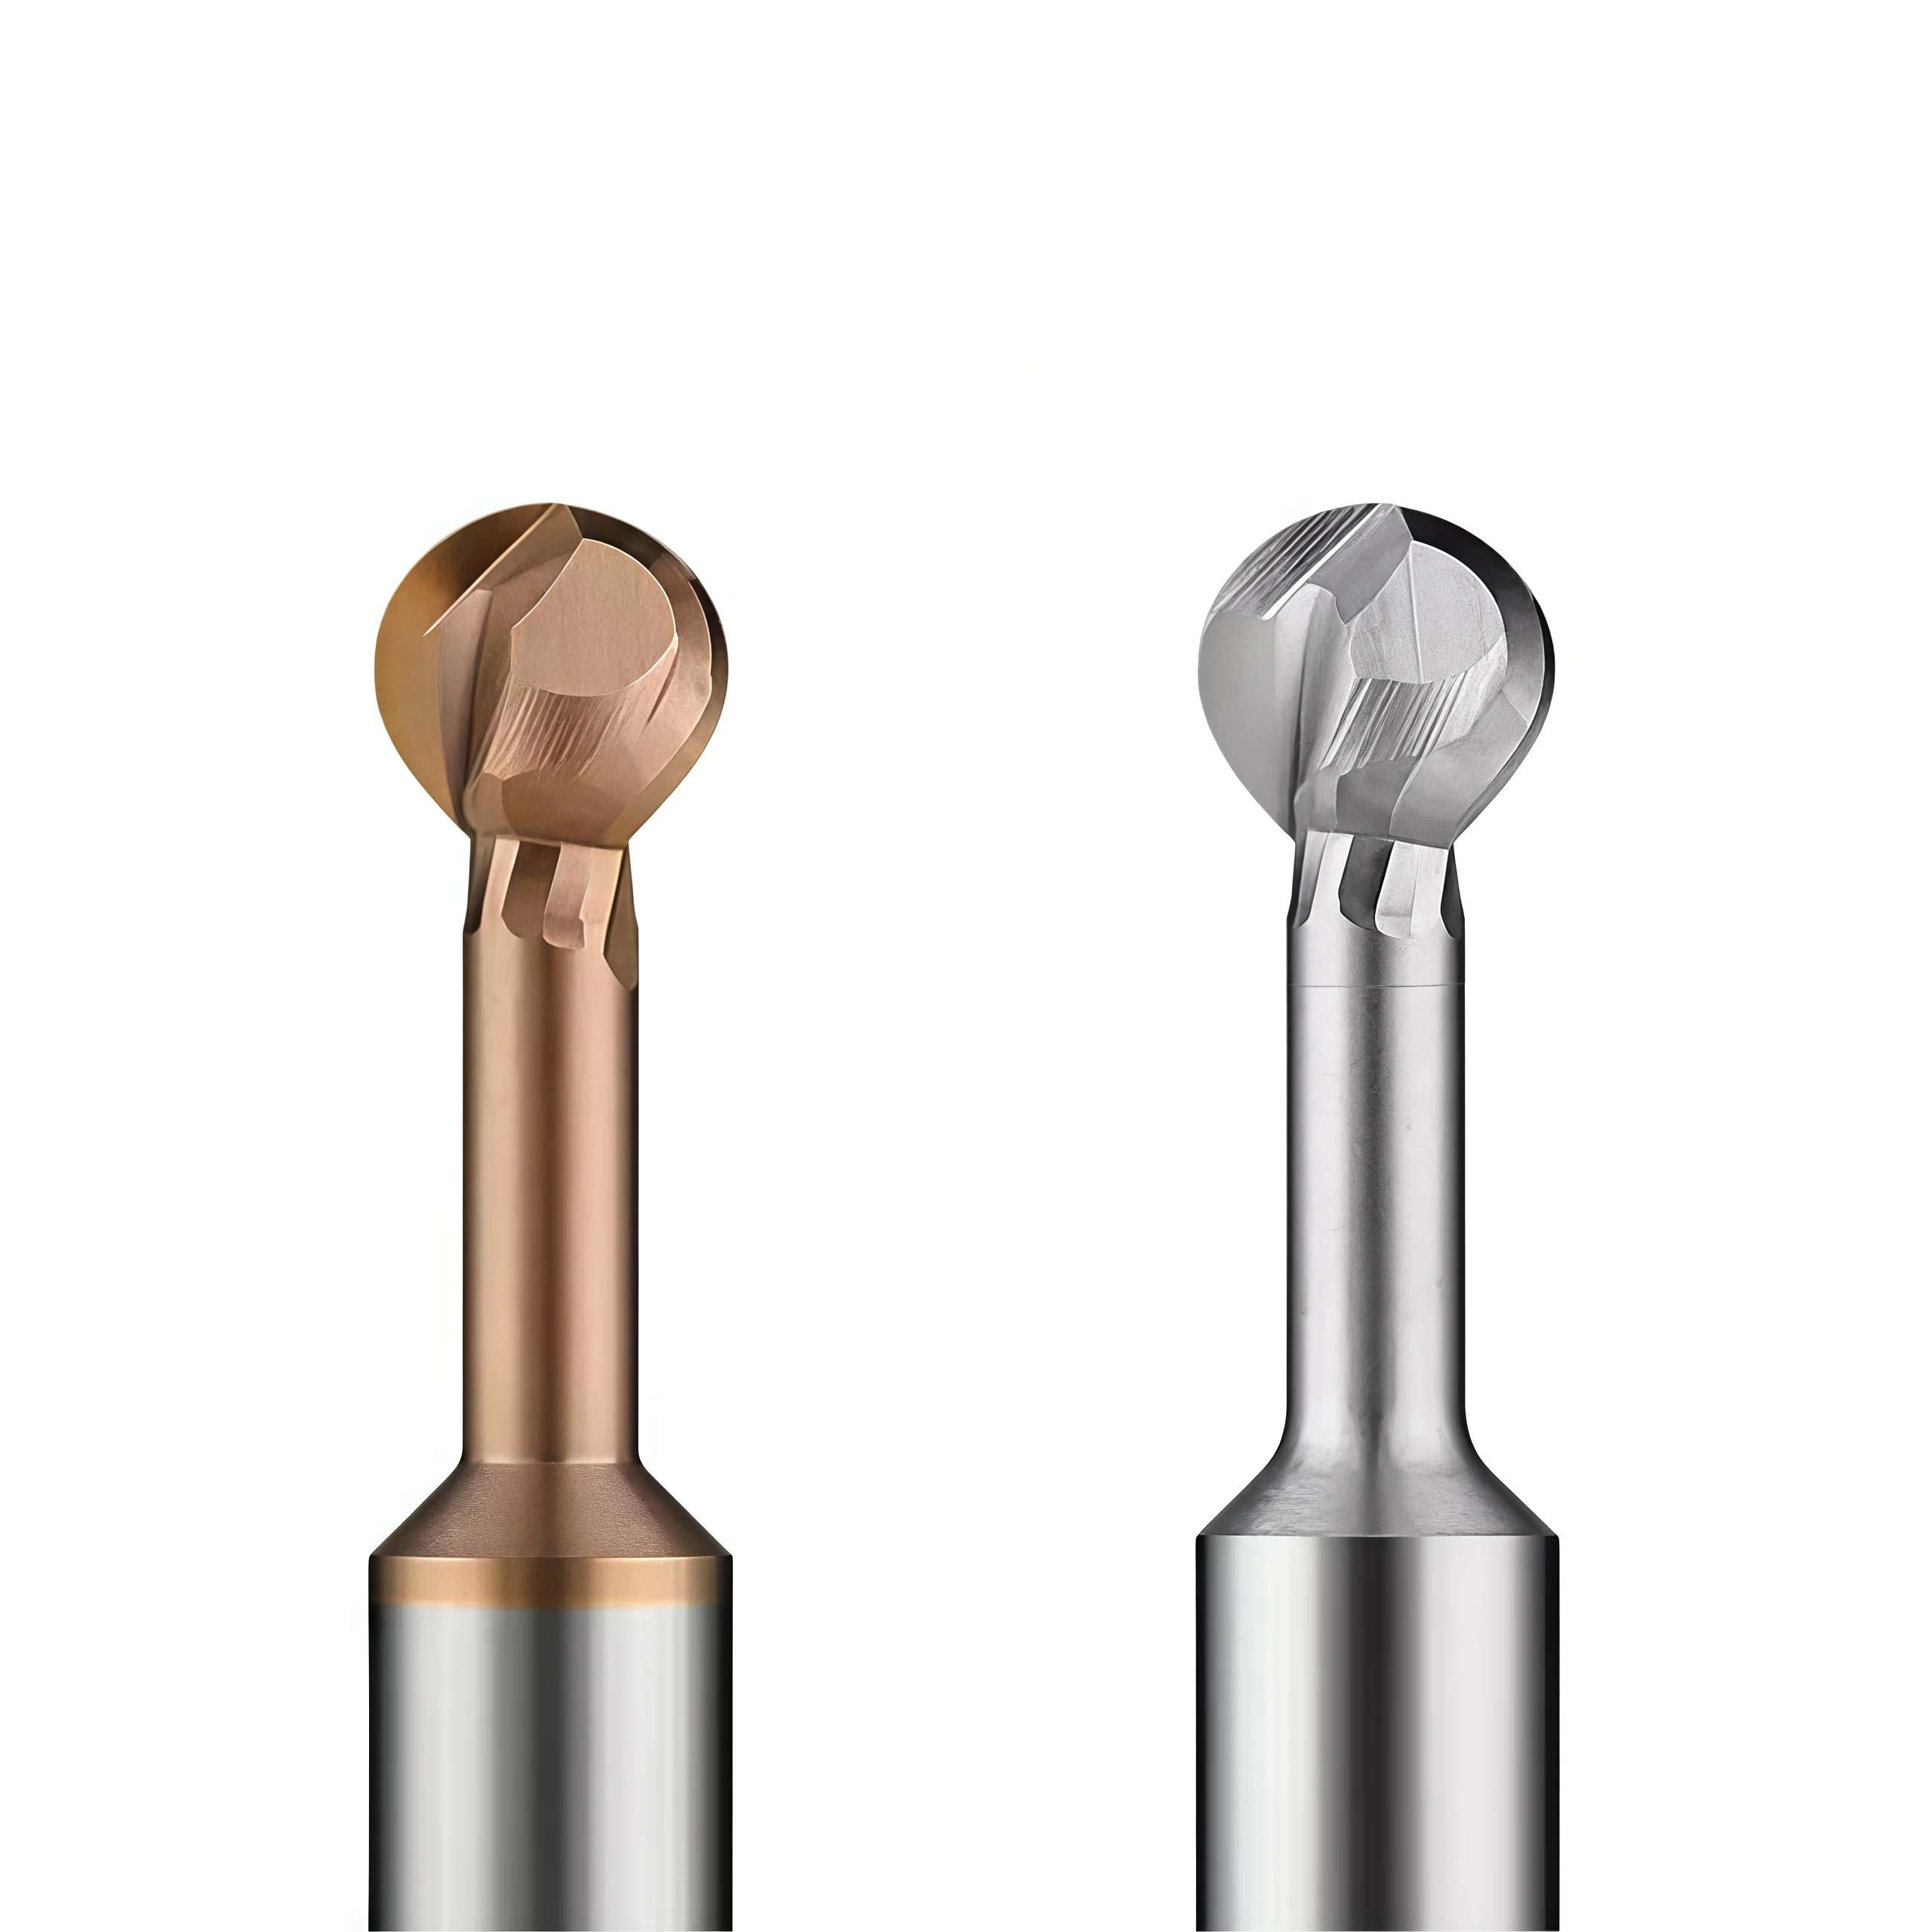
Spherical Cutting Head
The rounded cutting head can contact surfaces above, below and around its centerline, allowing radiused grooves and complex recessed profiles to be machined.
Relieved Neck
The reduced neck provides clearance behind the entry opening so the cutting head can reach undercuts, backside edges and recessed side surfaces.
R1–R10 Radius Series
A broad radius range supports small recessed features through larger radiused T-slot and side-profile applications.
Application-Specific Advantages
Undercut Access
Reach behind cavity walls, shoulders and openings after a suitable access path has been prepared.
Radiused Profiles
The spherical head produces blended and rounded forms rather than the flat form of a conventional T-slot cutter.
Multi-Angle Contact
Suitable for curved side surfaces and recessed 3D forms requiring contact from different tool orientations.
Solid Carbide Body
Solid carbide construction provides the rigid tool body required for controlled CNC profile milling.
Recommended Machining Operations
RECOMMENDED
RECOMMENDED
RECOMMENDED
SUITABLE
Typical Application Areas
| APPLICATION | MACHINING FEATURE |
|---|---|
| Radiused T-Slots | Rounded internal recesses and side grooves |
| Undercut Features | Recessed surfaces behind shoulders, cavity walls and openings |
| Backside Edges | Edge blending and deburring when machine access permits |
| Complex 3D Components | Curved and multi-angle recessed side surfaces |
Profile Note:
A lollipop ball nose cutter produces a rounded cutting form. If the component requires a flat, parallel-sided T-slot or a defined angled dovetail profile, select the corresponding T-slot or dovetail form cutter instead.
Recommended Undercut Milling Workflow
Prepare the Access Slot
Machine an entry slot or opening large enough for the spherical cutting head to pass through safely.
Enter Without Side Contact
Move the ball head through the prepared opening without forcing the full spherical profile into solid material.
Use Controlled Side Passes
Apply smooth lead-in moves and controlled radial engagement to reduce load on the relieved neck.
Product Details


Lollipop Ball Nose End Mill Dimensions
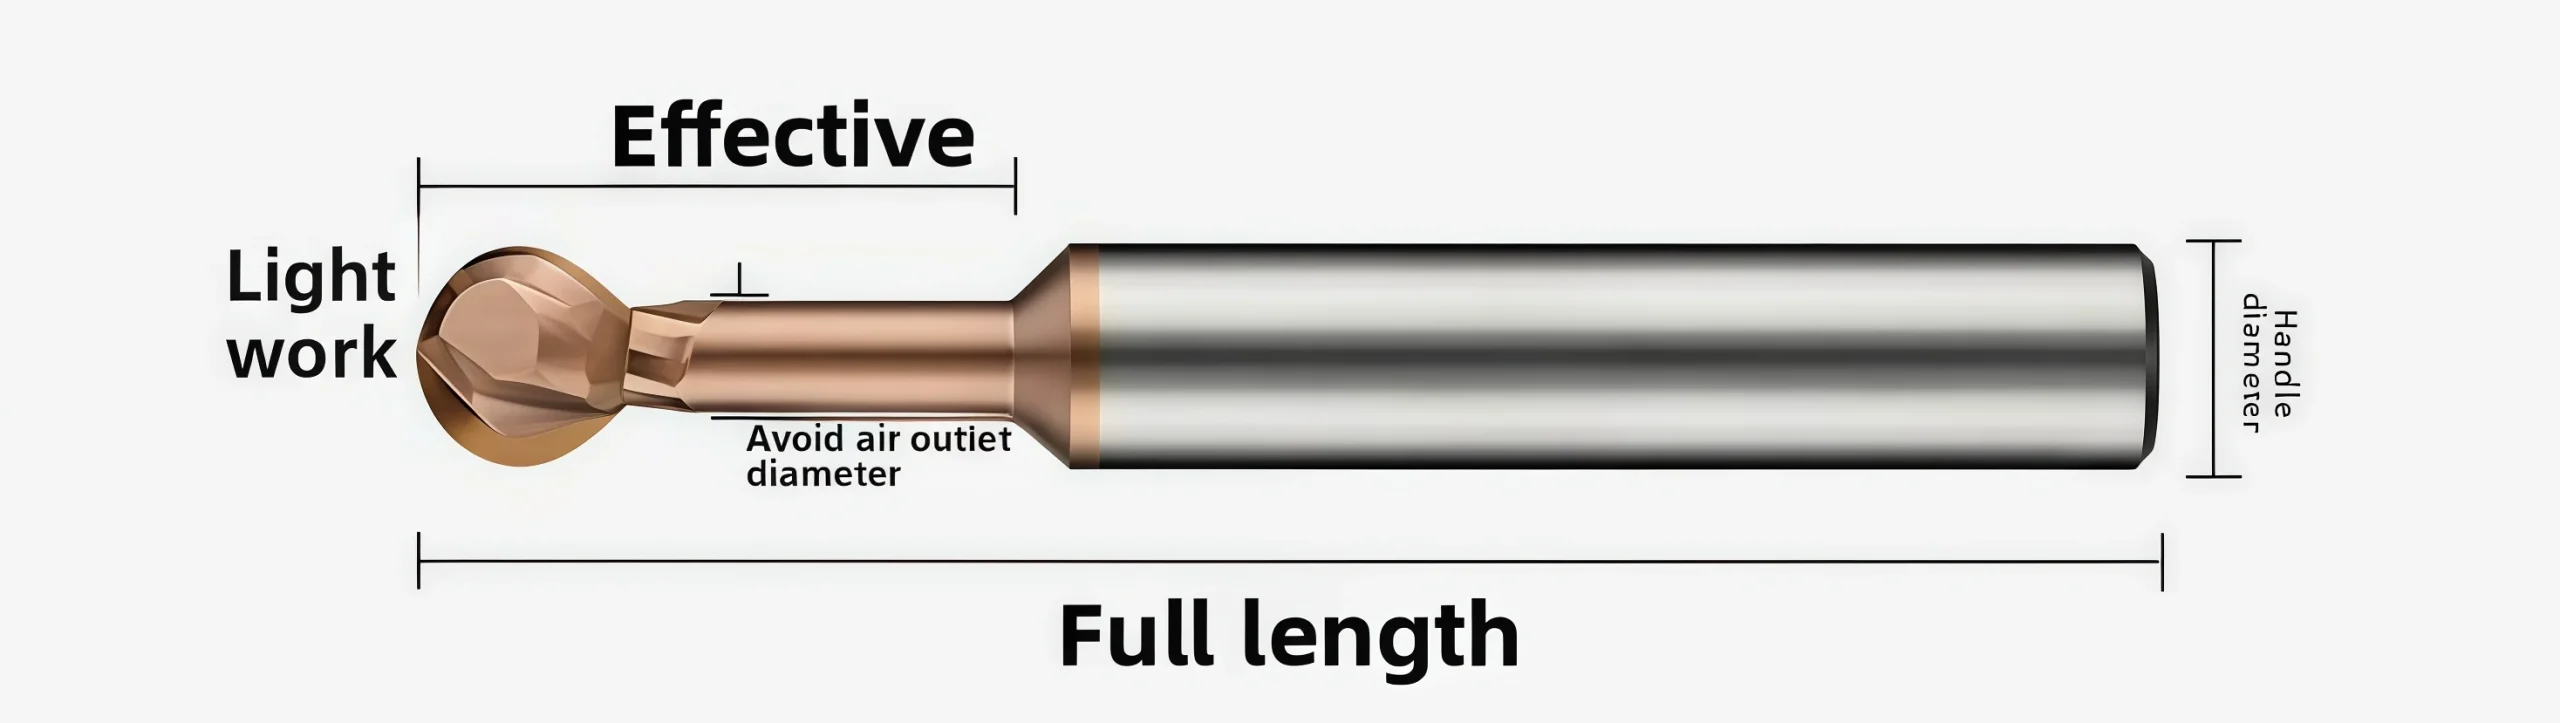
Tool selection should be based on ball radius, spherical-head envelope, relief diameter, relief length, shank diameter and overall length. The relieved neck must provide sufficient clearance throughout the complete undercut or backside-machining toolpath.
Technical Configuration
| PARAMETER | REFERENCE CONFIGURATION |
|---|---|
| Tipo de herramienta | Lollipop Ball Nose End Mill / Undercut Cutter |
| Material de la herramienta | Carburo sólido |
| Ball Radius Range | R1–R10 |
| Cutting Teeth | 2T for R1–R6 / 3T for R7–R10 |
| Relief Diameter | D1–D10 according to the documented radius series |
| Relief Length | 4–25 mm according to tool size |
| Diámetro del vástago | D4–D20 according to tool size |
| Longitud total | 50 / 60 / 75 mm in the current standard series |
| Primary Materials | Steel / Alloy Steel / Pre-Hardened Steel |
| Primary Applications | Radiused T-Slots / Undercutting / Backside Profiling / Recessed 3D Surfaces |
| Custom Requirements | Radius, relief diameter, relief length, shank size, overall length, tooth count, coating and profile requirements can be reviewed from drawings |
R1–R10 Standard Size Matrix
Current documented standard-reference sizes. All dimensions are in millimeters.
| BALL RADIUS R | RELIEF DIAMETER | RELIEF LENGTH | SHANK DIAMETER | OVERALL LENGTH | CUTTING TEETH |
|---|---|---|---|---|---|
| R1 | D1 | 4 | D4 | 50 | 2T |
| R1.5 | D1.5 | 5 | D4 | 50 | 2T |
| R2 | D2 | 6 | D4 | 50 | 2T |
| R2.5 | D2.5 | 10 | D6 | 50 | 2T |
| R3 | D3 | 10 | D6 | 50 | 2T |
| R4 | D4 | 12 | D8 | 60 | 2T |
| R5 | D5 | 15 | D10 | 60 | 2T |
| R6 | D6 | 15 | D12 | 60 | 2T |
| R7 | D7 | 25 | D14 | 75 | 3T |
| R8 | D8 | 25 | D16 | 75 | 3T |
| R9 | D9 | 25 | D18 | 75 | 3T |
| R10 | D10 | 25 | D20 | 75 | 3T |
Stable Machining Guidance
- Use the Largest Practical Neck: Select enough relief for the required undercut without choosing an unnecessarily slender neck.
- Limit Radial Engagement: Use progressive side passes rather than unnecessary full-profile engagement because the relieved neck is less rigid than the main shank.
- Check Entry Clearance: The prepared slot or opening must safely clear the spherical cutting head before side engagement begins.
- Control Chip Evacuation: Direct air or appropriate coolant toward the recessed cutting zone to reduce chip recutting and packing.
- Simulate the Complete Tool: Check the ball head, relieved neck, shank, holder and withdrawal path in CAM before machining enclosed or difficult-access features.
Carbide Lollipop Ball Nose End Mill Customization
Ball radius, relief diameter, relief length, shank diameter, overall length, cutting-tooth configuration, cutting-edge preparation and surface treatment can be configured for radiused T-slot, undercut and backside-profile machining. Standard configurations cover R1–R10, with 2-tooth designs used for R1–R6 and 3-tooth designs for R7–R10. Non-standard dimensions can be reviewed according to the entry opening, required undercut reach, finished profile, workpiece material and available holder clearance.
| PARAMETER | MANUFACTURING CAPABILITIES |
|---|---|
| Ball Radius (R) | The documented standard series covers R1, R1.5, R2, R2.5, R3, R4, R5, R6, R7, R8, R9 and R10. Non-standard radii can be reviewed according to the required finished profile and component drawing. |
| Spherical Head Geometry | Near-spherical cutting-head geometry can be matched to radiused grooves, recessed side surfaces, backside features and complex undercut profiles. |
| Relief Diameter | The standard series uses relief diameters from D1 to D10 depending on ball radius. Non-standard neck diameters can be reviewed according to entry clearance, undercut depth and required tool rigidity. |
| Relief Length | Standard relief lengths range from 4 mm to 25 mm according to tool size. Longer or application-specific reach can be reviewed according to cavity depth and surrounding clearance. |
| Cutting Teeth | Standard R1–R6 configurations use 2 cutting teeth, while R7–R10 use 3 cutting teeth. Alternative configurations can be reviewed when required by the tool size and machining application. |
| Shank Configuration | Straight cylindrical shank with standard sizes from D4 to D20 in the documented series. Drawing-defined shank diameters can be reviewed according to holder and machine requirements. |
| Longitud total | The current standard series uses 50 mm, 60 mm and 75 mm overall lengths. Custom lengths can be reviewed according to undercut depth, holder clearance and tool-rigidity requirements. |
| Head & Entry Clearance | The entry slot or opening must provide sufficient clearance for the spherical head to pass through before side engagement. Head envelope and access geometry should be checked against the component drawing. |
| Undercut Reach | Relief diameter and relief length can be matched to the required backside reach, cavity depth and side-wall clearance while maintaining as much neck rigidity as practical. |
| Cutting-Edge Preparation | Cutting-edge preparation can be reviewed according to workpiece material, hardness, cutting engagement, radius size and required surface condition. |
| Coating & Surface Treatment | Coating and surface treatment can be selected according to the workpiece grade, hardness, cutting conditions and required wear resistance. |
| Material de la pieza | Configurations can be reviewed for steel, alloy steel and pre-hardened steel according to the actual material grade, hardness and machining conditions. |
| Aplicación de mecanizado | Geometry can be reviewed for radiused T-slots, undercuts, backside-edge machining, recessed side profiles and complex 3D contouring. |
| Tool & Holder Clearance | The complete ball head, relieved neck, shank and holder envelope should be reviewed against the programmed toolpath and available cavity clearance. |
| Dimensional Tolerance | Drawing-defined requirements can be reviewed for ball radius, relief diameter, relief length, shank diameter, overall length and finished cutting profile. |
| Replacement Tool Matching | Existing lollipop or undercut cutters can be reviewed from a component drawing, existing tool drawing or physical sample when an equivalent or modified replacement configuration is required. |
Servicios de fabricación personalizada y marca propia
OEM manufacturing and private-label supply options are available for industrial distributors, tooling brands and repeat-production customers. Laser identification, label content, protective packaging and coating presentation can be configured according to the approved product specification and order requirements.

Laser Etching
Custom logos, tool codes, cutting dimensions, coating identification and batch numbers can be marked according to the available shank area.
Custom Labels & Packaging
Individual protective tubes, product labels, specification details, colored packaging tubes and private-label packaging can be reviewed.
Commercial Terms
MOQ, sample evaluation, custom-size trials, repeat orders and scheduled supply programs are confirmed according to the selected configuration.
Technical Workflow
A structured review process is used to confirm standard, customized and private-label square end mill requirements before production.
Inquiry
Submit the material, hardness, milling operation, dimensions, tolerance and quantity.
Engineering
Review flute geometry, helix angle, edge preparation, coating, ap and ae.
Commercial
Confirm quotation, MOQ, sample requirements, production schedule and delivery terms.
Production
CNC grinding, end-face formation, edge preparation, coating and laser marking.
Quality Control
Inspect diameter, flute length, shank, runout, square-end geometry and cutting edges.
Quality, Inspection & Delivery
Our solid carbide square end mills are controlled through material verification, precision grinding, in-process measurement and final inspection. Key dimensions, square-end geometry, cutting-edge condition, coating appearance and product identification are reviewed according to the approved specification or drawing before packing.

Three-Stage Quality Control
Inspection checkpoints are arranged around the manufacturing process to support dimensional consistency and repeat-order control.
Incoming Material Control
Carbide substrate grade, blank dimensions and supplied material information are checked against the production requirement.
In-Process Grinding Control
Cutting diameter, flute geometry, flute length, square-end profile and shank dimensions are monitored during CNC grinding.
Final Tool Inspection
Finished tools are reviewed for specified dimensions, runout, cutting-edge condition, coating appearance, marking and packing identification.
Key Inspection Characteristics
Inspection requirements are confirmed according to the standard product specification or the approved custom drawing.
| INSPECTION ITEM | CONTROL FOCUS | CONFIRMATION BASIS |
|---|---|---|
| Cutting Diameter (DC) | Diameter and dimensional consistency | Standard specification or approved drawing |
| Flute Length (APMX) | Effective cutting length | Confirmed product size or drawing requirement |
| Shank Diameter (DCON) | Clamping-section dimension and surface condition | Applicable shank specification |
| Overall Length (OAL) | Total tool length | Standard size matrix or approved drawing |
| Radial Runout | Concentricity between cutting section and shank | Agreed inspection requirement |
| Square-End Geometry | End-face profile, corner condition and center-cutting form | Selected tool configuration |
| Flute & Helix Profile | Flute count, helix form and grinding consistency | Approved manufacturing configuration |
| Cutting Edge & Coating | Edge condition, visible defects and coating appearance | Application-specific production requirement |
| Marking & Identification | Tool code, dimensions and batch information where applicable | Confirmed order and packaging specification |
Measurement & Batch Traceability
Optical measuring systems, tool inspection equipment and appropriate dimensional gauges are selected according to the feature being checked.
Optical Measurement
Profile and dimensional review of specified cutting features.
Runout Verification
Concentricity review based on the agreed product requirement.
Inspección de bordes
Magnified review of the end face, corners and cutting-edge condition.
Batch Identification
Order, product and batch information are linked where required for repeat supply.
Protective Packaging Process
Finished end mills are protected to reduce contact between cutting edges and to support clear product identification during storage and transportation.

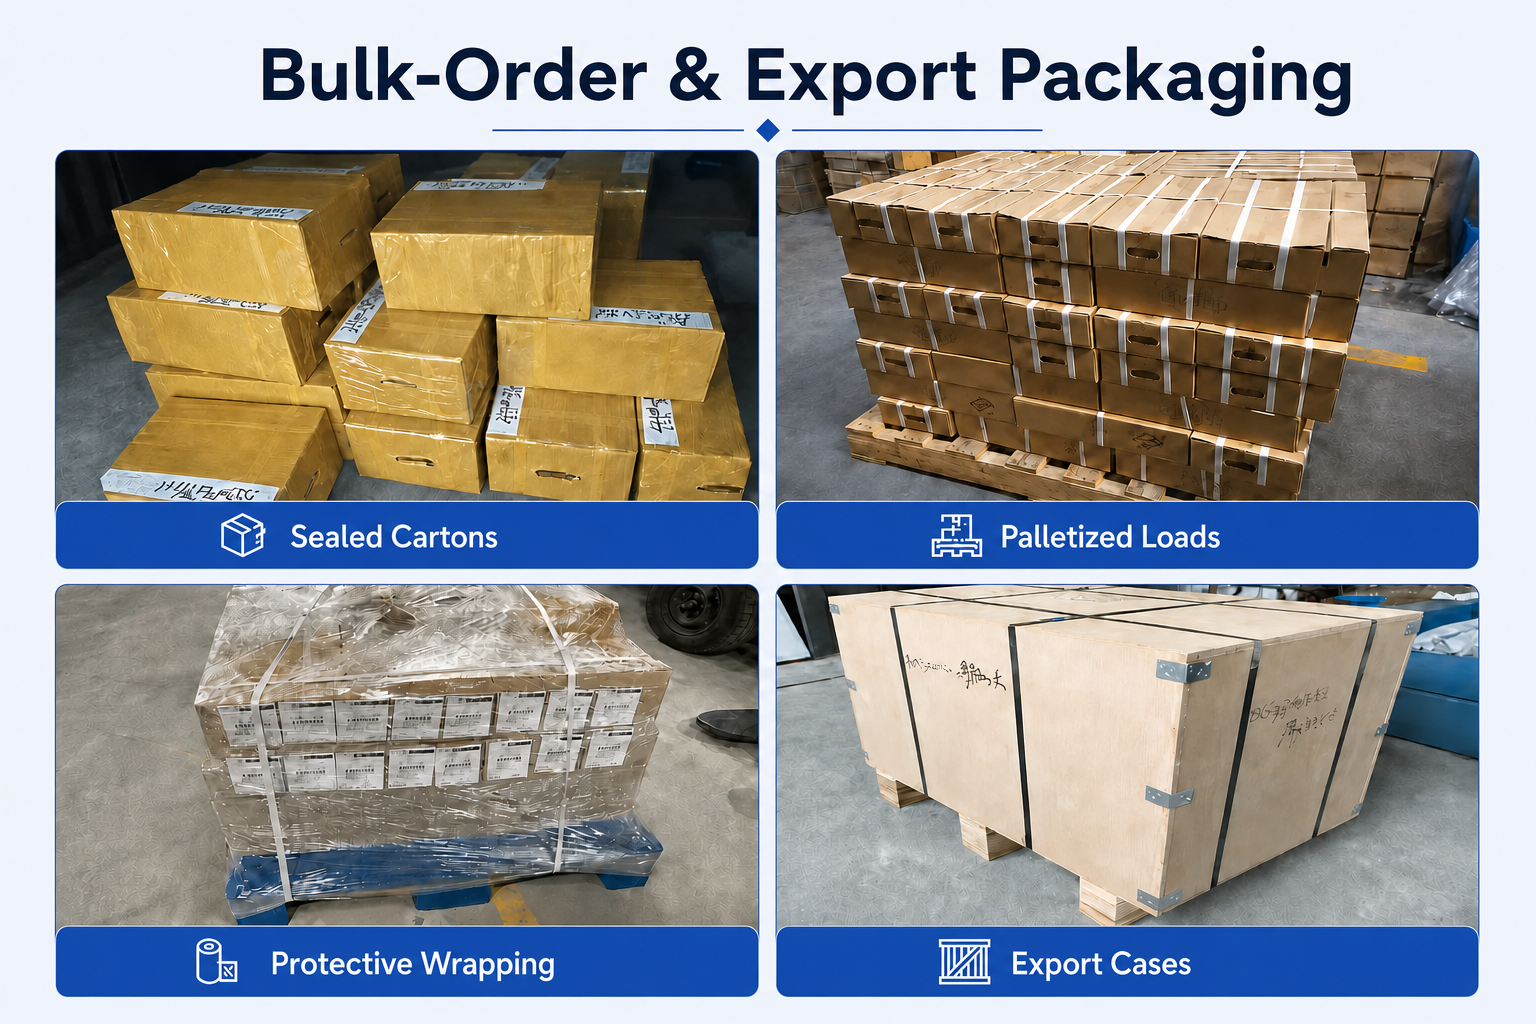
Bulk-Order & Export Packaging
Bulk shipments can be arranged with reinforced cartons, protective wrapping, palletized loading or export cases according to order quantity, shipment weight and agreed transportation requirements.
Delivery Coordination
Production completion, packing method and dispatch arrangements are confirmed according to the approved order. Courier, air, sea or customer-designated shipping options can be reviewed according to shipment size and destination. Final lead time is confirmed after product specifications, quantity and packaging requirements are approved.
Product & Application FAQs
Common questions about the R1–R10 solid carbide lollipop ball nose end mill for radiused T-slot milling, undercutting and recessed-profile machining.
What is a lollipop ball nose end mill used for?
Is this the same as a conventional T-slot cutter?
Why does the tool have a relieved neck?
What radius sizes are available?
How many cutting teeth does the tool have?
Does the tool require a pre-machined access slot?
Which materials is this series intended for?
How should the tool be used for deep undercuts?
Ordering & Customization FAQs
Ordering information for distributors, tooling suppliers and OEM customers requiring standard R1–R10 or application-specific lollipop cutters.
Can the ball radius and neck dimensions be customized?
Can you manufacture a replacement tool from a drawing or sample?
What dimensions should be confirmed before ordering?
What information should I provide for quotation?
Are OEM marking and private-label packaging available?
¿Cuál es el plazo de entrega habitual?
Technical Downloads
Reference documents for solid carbide milling cutter selection and machining-data review.
Solid Carbide End Mill Catalog
Review ball nose, specialty undercut and related solid carbide milling tools.
End Mill Speeds & Feeds Guide
Use as a general reference before confirming final lollipop and undercut-milling parameters.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.