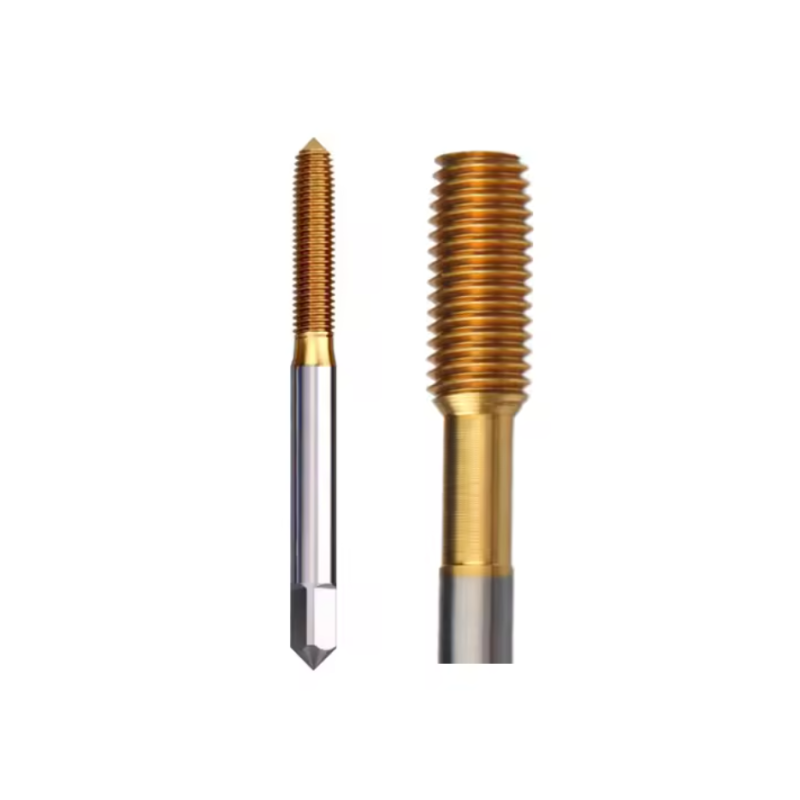
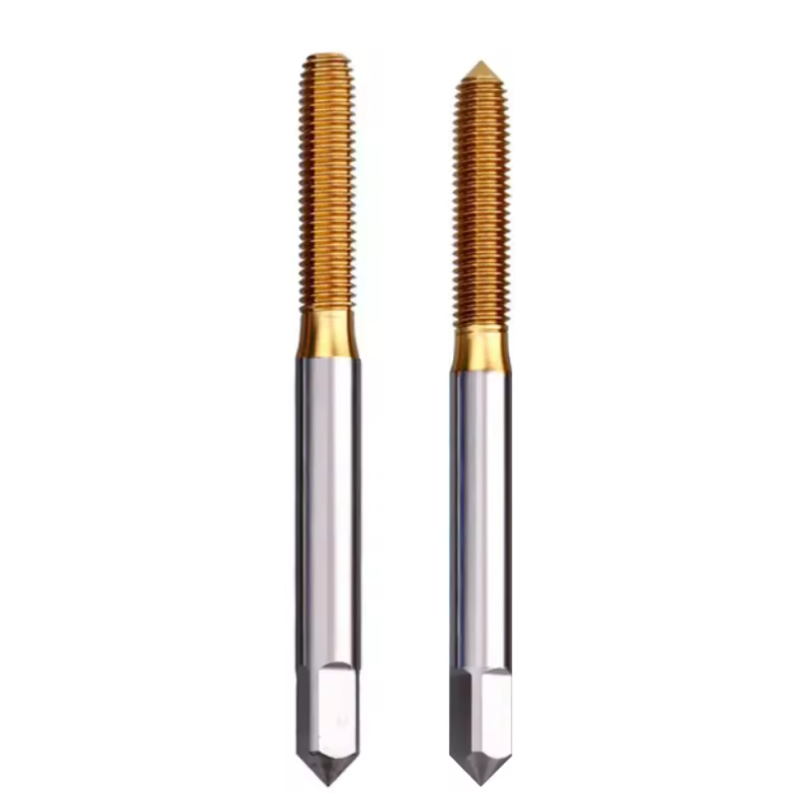
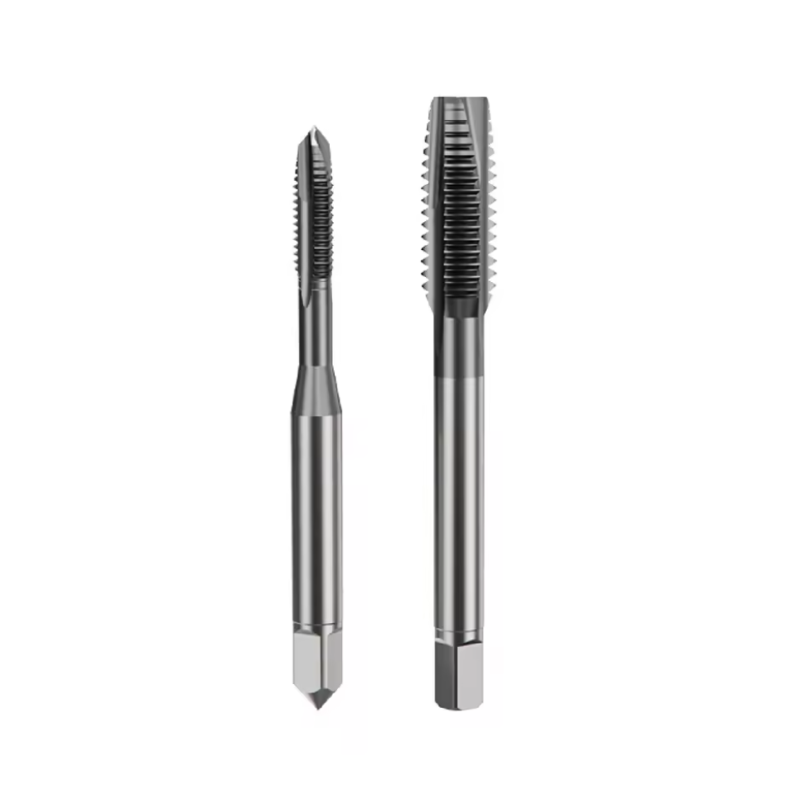
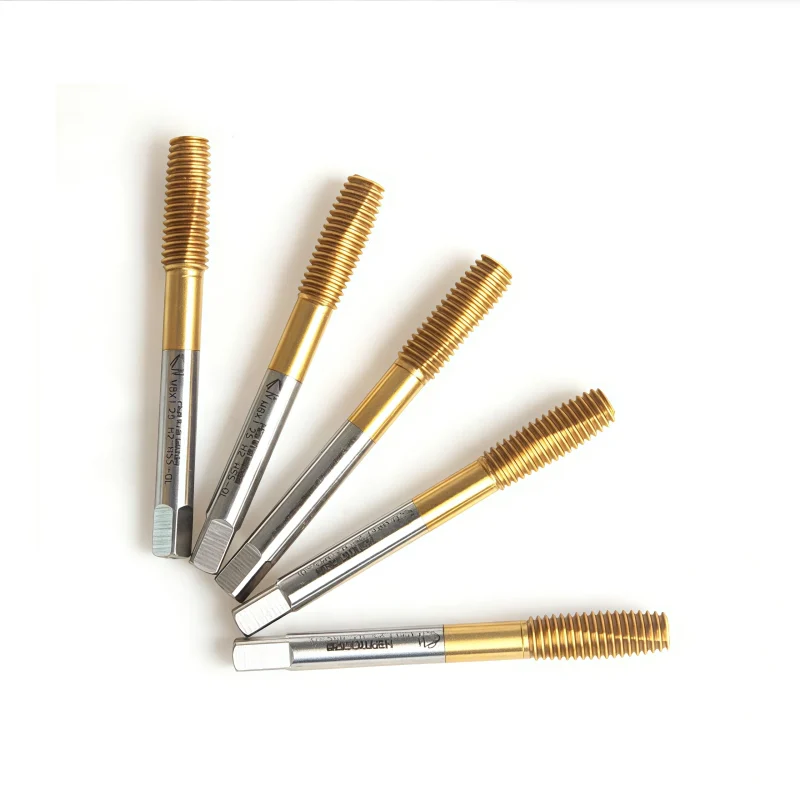
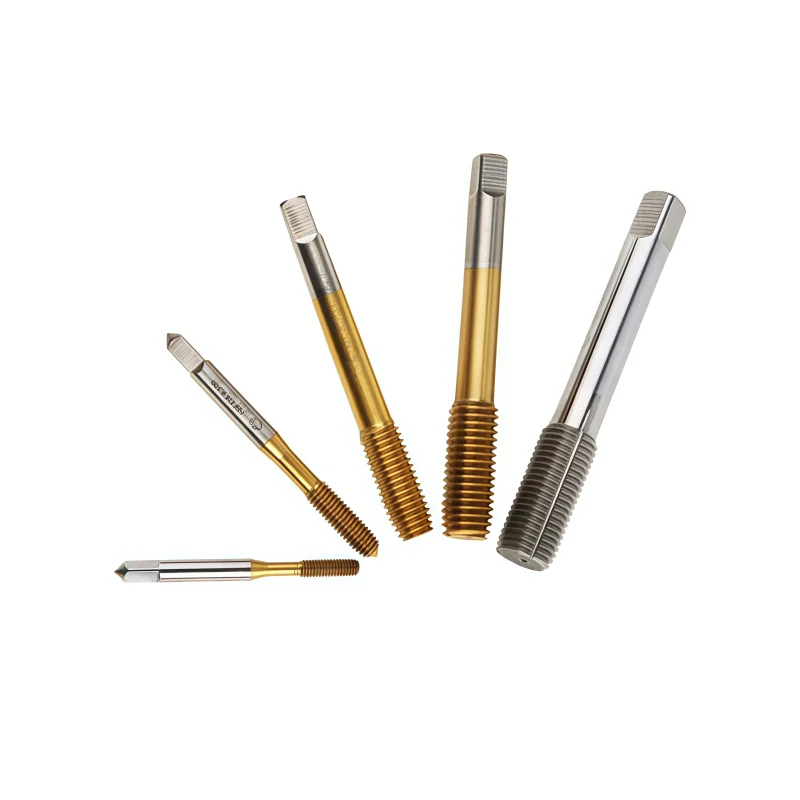
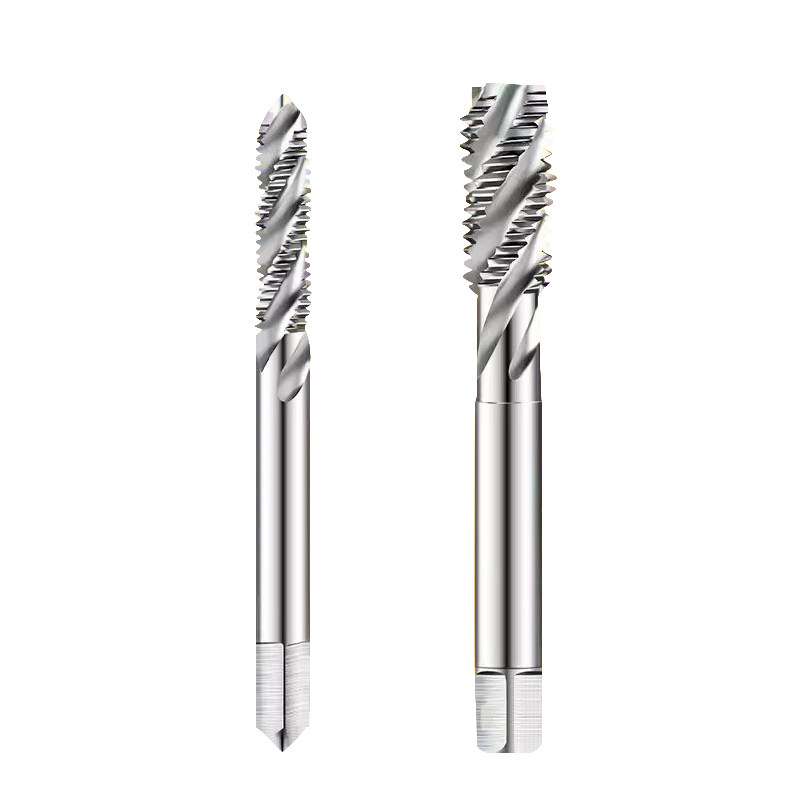
Long Shank HSS-PM Machine Taps – Spiral Point & Spiral Flute, M2–M16
Product Specifications
Consistent Quality
Consistent geometry across repeat orders.
Flexible Orders
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
Standard & Custom
Standard sizes and custom configurations.
Long Shank HSS-PM Machine Taps – M2–M16
These long shank HSS-PM machine taps are available in spiral point and spiral flute designs for metric internal threading from M2 × 0.4 to M16 × 2.0. The spiral point version directs chips forward for through holes, while the spiral flute version draws chips back toward the entry of blind holes. Both size charts list a 100 mm overall length across eleven specifications. Thread lengths differ between the two styles, so select the complete diameter and pitch, then check hole type, holder fit, required reach and available clearance. Confirm the specific PM steel grade, coating, thread tolerance and cutting conditions before production use.
Key Configuration

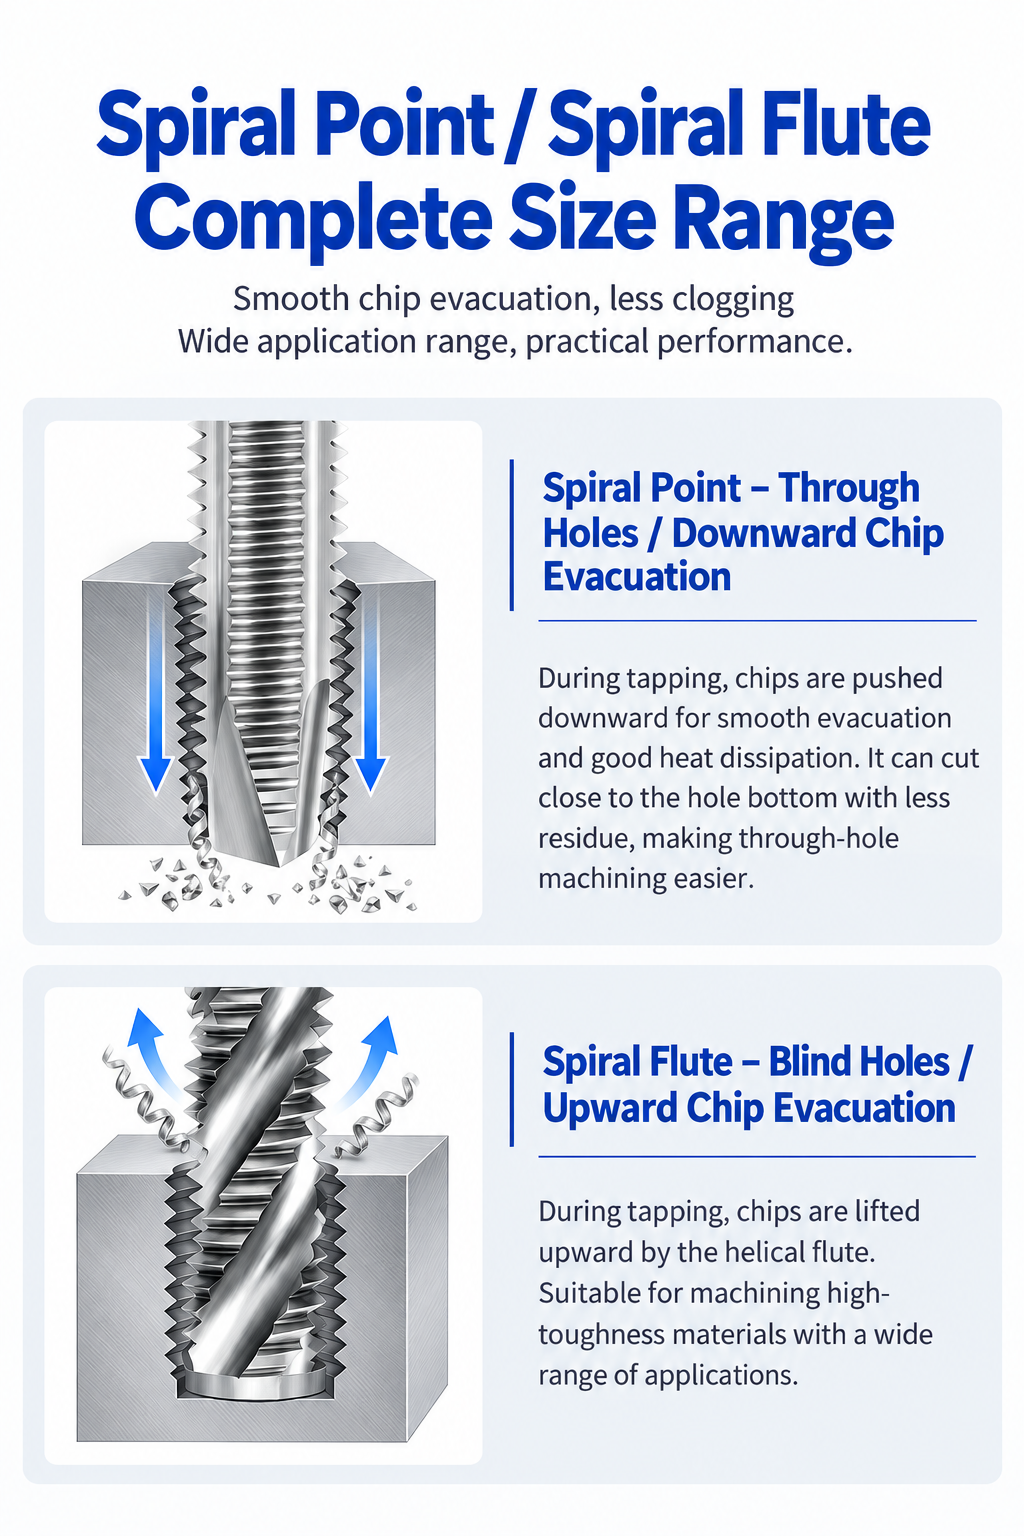
Spiral point for through holes; spiral flute for blind holes. Select according to chip-flow direction and available clearance.
The listed range covers M2 × 0.4 to M16 × 2.0. M10 × 1.25 and M12 × 1.5 must be ordered with their stated pitches.
Both charts list 100 mm overall length; shank diameters range from 3 to 12.5 mm. Check holder fit and setup rigidity.
Key Product Advantages




M2–M16 Metric Range
Eleven listed diameter and pitch combinations support small to medium metric threads.
HSS-PM Construction
Powder metallurgy high-speed steel substrate; confirm the exact grade for the order.
Hole-Specific Geometry
Choose spiral point or spiral flute according to through-hole or blind-hole chip evacuation.
Extended Tool Reach
The 100 mm listed overall length provides access where a shorter tap may not reach.
Tapping Applications
These long shank taps are intended for machine threading where the workpiece geometry requires additional tool reach. Select the spiral point style when chips can pass through the hole; select the spiral flute style when chips must return toward the entry of a blind hole.
Workpiece Material Selection

Material selection depends on the exact HSS-PM grade, tap geometry, coating and lubrication. The supplied drawings do not give an approved workpiece-material list; the groups below are applications to evaluate with the actual specification.
| MATERIAL GROUP | EXAMPLES | SELECTION NOTE |
|---|---|---|
| P Steel | Carbon and alloy steels | Confirm grade, coating and chip control |
| M Stainless Steel | Selected stainless steel grades | Application review required |
| K Cast Iron | Short-chipping cast iron grades | Confirm appropriate tap geometry |
| N Non-Ferrous | Selected aluminum and copper alloys | Confirm chip behavior and lubrication |

Product Details & Available Configurations
The drawings below show the two available cutting configurations. Each has pointed-end and flat-end illustrations; confirm the exact chamfer and end geometry for the selected order.


Browse the HSS Tap Range for other lengths and tapping geometries.
Size Chart & Specifications
Both configurations list eleven metric sizes from M2 × 0.4 to M16 × 2.0, a 100 mm overall length and shank diameters from 3 to 12.5 mm. Spiral point thread lengths range from 7.2 to 32 mm; spiral flute thread lengths range from 6 to 21 mm. Check the chart for the selected style and complete size-and-pitch designation.
Spiral Point – Through-Hole Version

Spiral Flute – Blind-Hole Version

Specification confirmation: The drawings identify HSS-PM and show three-flute pointed-end and flat-end illustrations. They do not specify the exact PM grade, coating, thread tolerance, chamfer length or coolant arrangement. Confirm those details for the ordered variant.
HSS Tap Speeds & Feed Settings
The chart below is a general HSS reference for M2–M12, not product-specific cutting data for this M2–M16 HSS-PM series. Confirm PM grade, coating, workpiece material, hole type, thread depth and lubrication before selecting a starting speed. M14 and M16 are outside the chart’s size range.
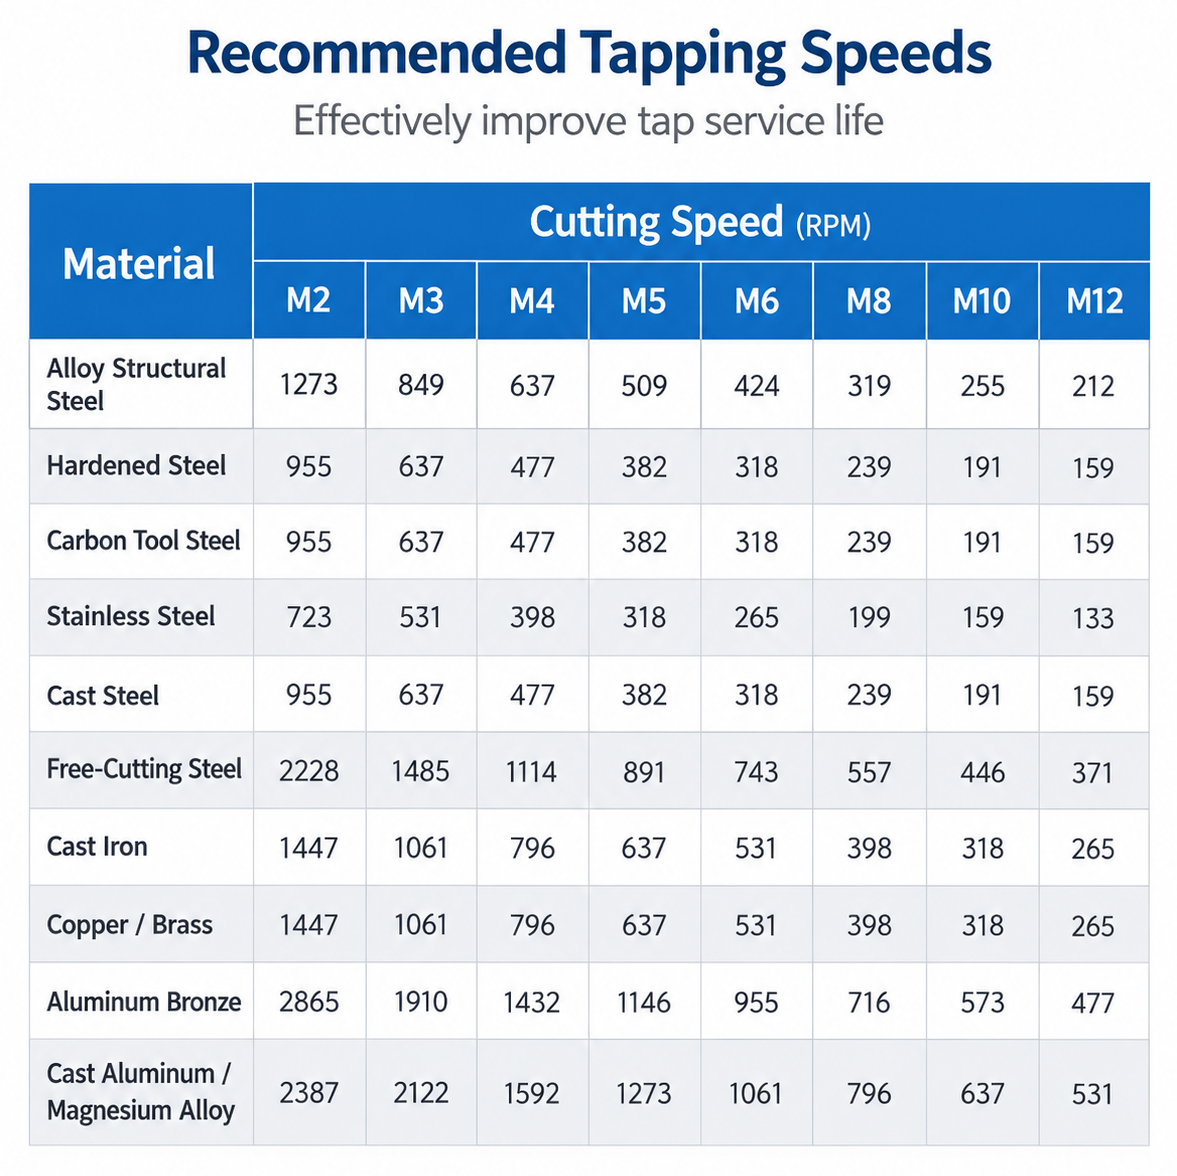
Setting Speed & Feed
Spindle speed: n = (1000 × Vc) / (π × D), where n is RPM, Vc is cutting speed in m/min and D is nominal tap diameter in mm.
Tapping feed: For the listed single-start metric threads, feed per revolution equals thread pitch. When programming in mm/min, F = n × P, where P is pitch in mm.
Calculation example: An M6 × 1.0 tap at 400 RPM requires 400 mm/min synchronized feed, or 1.0 mm/rev. This illustrates the feed calculation only; it is not a recommended speed for a particular material.
For additional reference, see our HSS cutting tools speeds & feeds guide.
Related Series & Downloads
For a standard-length through-hole option, see our HSS tap range.
View HY Taps Catalog — use this product page’s two charts for the listed 100 mm long shank configurations; other catalog series may differ.
HSS Tap Customization
For requirements beyond the standard range, send your tap drawing or application details. Custom HSS cutting and forming taps can be reviewed for the following specifications.
| PARAMETER | CUSTOMIZATION OPTIONS |
|---|---|
| Thread Specification | Metric, UNC/UNF and pipe threads; special diameters, pitches and left-hand threads. |
| Thread Accuracy | Tap limits and oversize allowances to suit the required internal-thread tolerance and gauging requirements. |
| Tap Geometry | Straight flute, spiral flute, spiral point or forming design; chamfer and working geometry matched to the application. |
| Length & Reach | Overall length, threaded-section length and neck clearance to suit thread depth and component access. |
| Shank & Drive Square | Shank diameter, square dimensions and holding length to match the tapping holder. |
| Material & Surface Finish | HSS or cobalt HSS grades; uncoated, TiN or TiCN options, depending on the tap design and workpiece material. |
Options depend on tap type and size. Final specifications, minimum order quantity and lead time are confirmed with the quotation.
OEM & Private Label
Customer branding and packaging can be specified for distributor and tooling-brand orders.
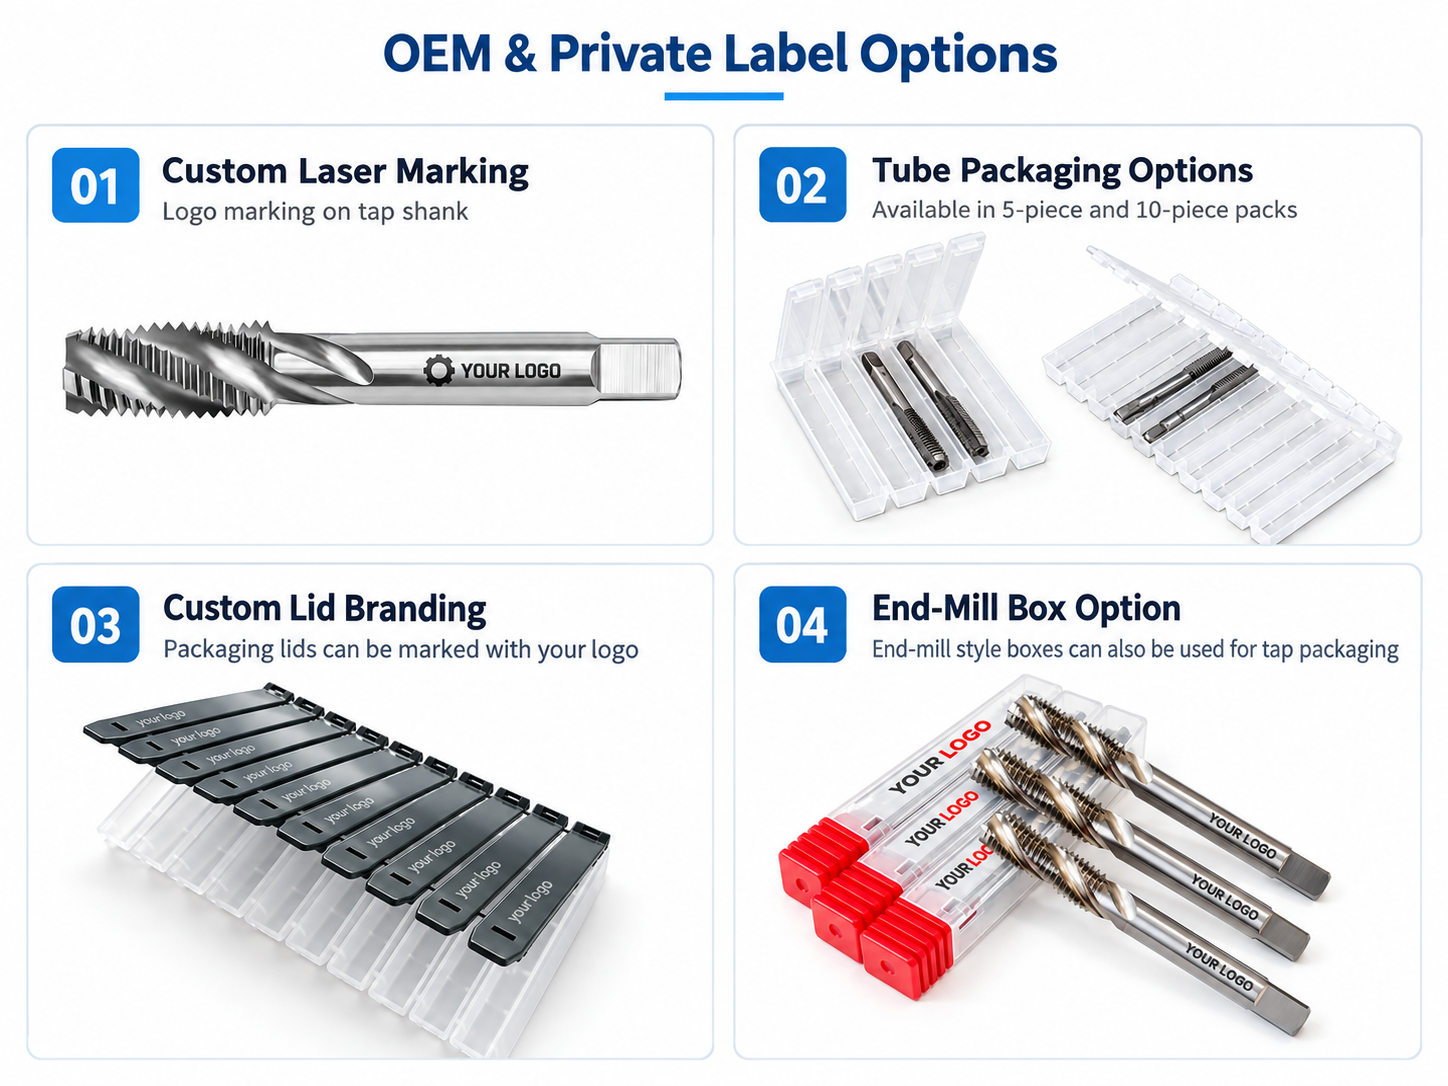
Laser marking: Logo, thread size, product code and batch identification, subject to available shank space. Labels & packaging: Protective tubes, product labels and branded packaging to the approved artwork.
For a quotation: Send a drawing or thread specification, required tolerance, workpiece material and hardness, blind or through-hole details, thread depth and quantity. Include machine, holder and lubrication details for application-specific requests.
HSS Tap Quality & Inspection
HSS cutting and forming taps are checked against the confirmed product specification or approved drawing. Material verification, in-process dimensional checks and final inspection focus on thread accuracy, tool geometry and consistent identification before packing.

Key Inspection Points
Inspection items and acceptance criteria depend on the tap type, size and agreed requirements.
| INSPECTION ITEM | CHECK POINTS |
|---|---|
| Material & Hardness | HSS or cobalt HSS grade and material records; hardness requirements and verification agreed for the selected grade. |
| Thread Form & Accuracy | Thread size, pitch, profile and specified tap limits against the confirmed specification or drawing. |
| Working Geometry | Flutes, spiral point and cutting edges for cutting taps; forming lobes and lubrication grooves, where present, for forming taps. Chamfer geometry checked for each design. |
| Tool Dimensions | Threaded-section length, overall length, shank diameter and drive-square dimensions. |
| Runout & Surface Condition | Specified runout, burrs, chipped edges and visible defects on cutting or forming surfaces. |
| Coating & Identification | Specified surface finish or coating, visible condition, tool marking and label accuracy. |
Inspection documentation: Specify any required material records, dimensional reports or sample-thread validation before ordering. Availability and inspection scope are confirmed with the quotation.
Packaging & Batch Identification
Individual protective packaging helps prevent damage to tap threads and working surfaces. Labels identify the tool specification and order or batch reference. Models, quantities and packing details are checked before dispatch.

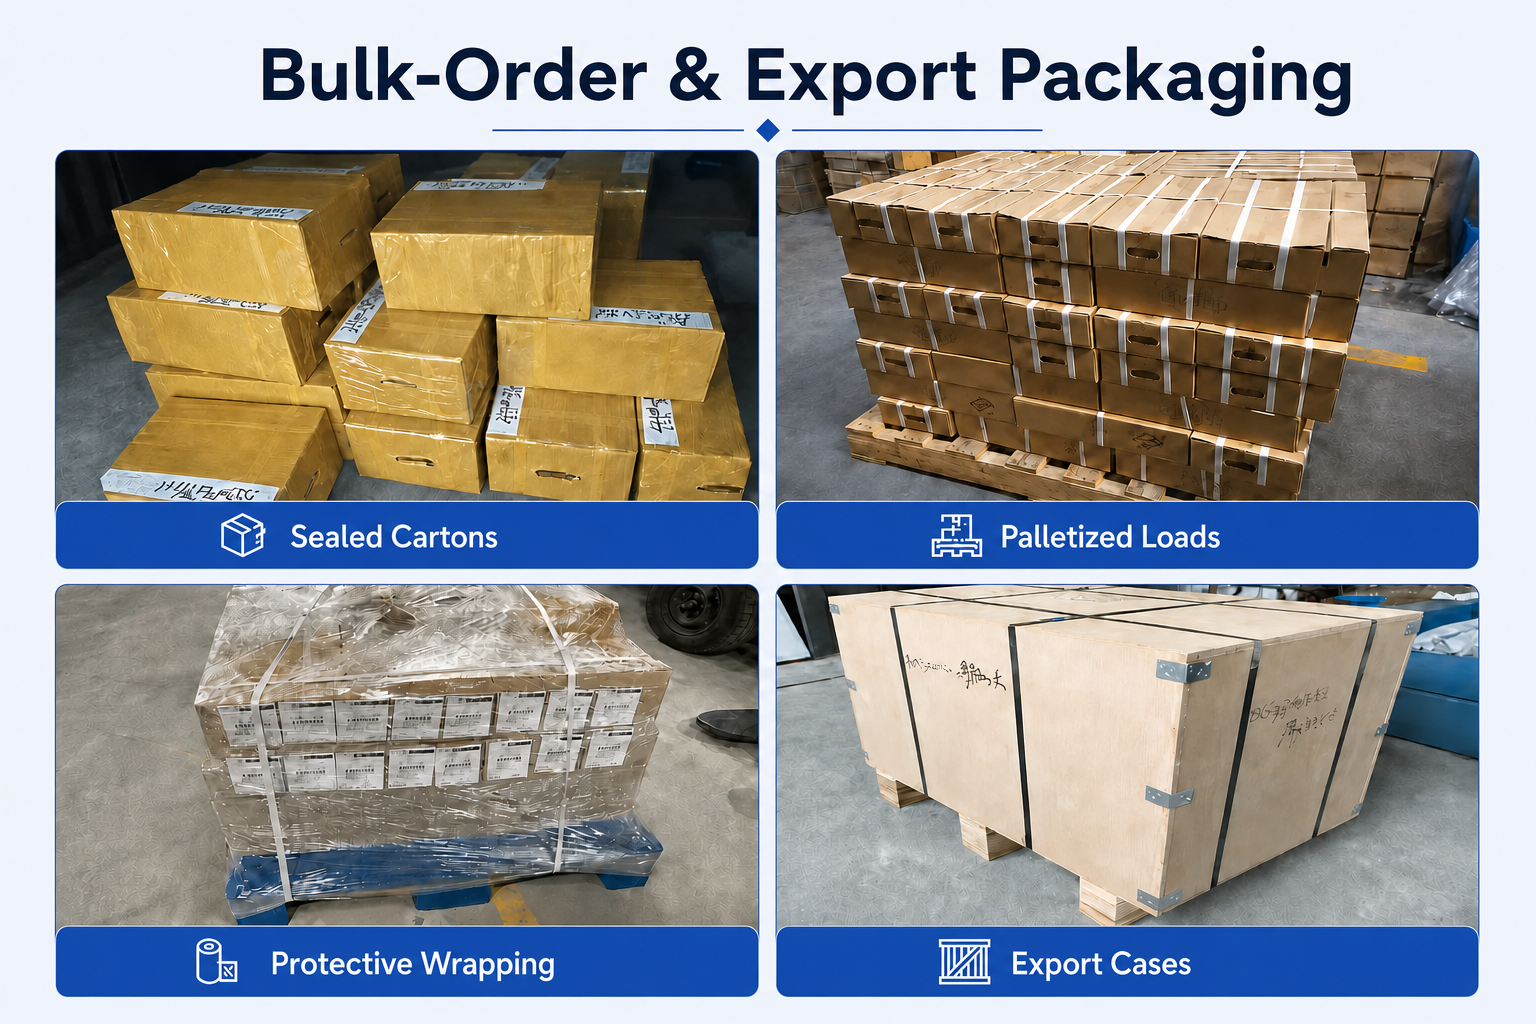
Export Packing & Delivery
Outer cartons, cushioning and export packing are selected for the order quantity and shipping method. Dispatch dates, freight and payment terms are confirmed with the order.

FAQ & Technical Support
Selection, hole preparation and ordering guidance for M2–M16 long shank HSS-PM spiral point and spiral flute machine taps.
Product & Application FAQs
Which sizes and lengths are listed for this series?
Both style charts list eleven metric sizes: M2 × 0.4, M2.5 × 0.45, M3 × 0.5, M4 × 0.7, M5 × 0.8, M6 × 1.0, M8 × 1.25, M10 × 1.25, M12 × 1.5, M14 × 2.0 and M16 × 2.0. The listed overall length is 100 mm for every size, with shank diameters from 3 to 12.5 mm. Thread lengths differ between the spiral point and spiral flute versions; check the chart for the selected style and size.
Should I choose the spiral point or spiral flute version?
Choose the spiral point version for through holes where chips can move forward and exit the hole. Choose the spiral flute version for blind holes where chips need to travel back toward the hole entry. Also consider the workpiece material, chip behavior, hole depth and available clearance before final selection.
Does the 100 mm overall length mean these taps can cut 100 mm deep threads?
No. The 100 mm value is the overall tool length, not the cutting length or achievable full-thread depth. The spiral point chart lists thread lengths from 7.2 to 32 mm, while the spiral flute chart lists 6 to 21 mm. Usable depth also depends on chamfer length, holder engagement, hole clearance and chip evacuation. State the required full-thread depth when requesting a recommendation.
Can the flat-end version cut full threads to the bottom of a blind hole?
The drawings show pointed-end and flat-end illustrations, but do not state the chamfer length or guaranteed full-thread depth. A flat end alone does not establish bottoming capability. Confirm the cutting lead, required complete-thread depth and remaining bottom clearance for the selected spiral flute tap.
What pilot-hole diameter should I use?
Do not use the “Tap Hole Dia.” column in the supplied images as a drill-size guide: its values repeat the nominal thread diameters. Determine the pilot-hole diameter from the complete thread size and pitch, workpiece material, required thread engagement and applicable tolerance. Confirm the drill size and inspect a trial thread before batch production.
Which workpiece materials can these taps machine?
The dimension drawings do not provide a confirmed material-compatibility list. Carbon and alloy steels, selected stainless steels, cast iron and non-ferrous alloys require application-specific review of PM grade, cutting geometry, coating, chip behavior and lubrication. Send the workpiece grade and hardness for a suitable recommendation.
What machine setup and tapping conditions should I check?
Check holder compatibility, tool alignment, overhang, workholding rigidity, pilot-hole size and chip clearance. For the listed single-start metric threads, synchronize feed per revolution with the specified pitch. Select spindle speed and lubrication for the actual workpiece, tap configuration and PM grade, then validate the setup with a trial cut.
Ordering & Customization FAQs
What information is needed for a quotation?
Specify spiral point or spiral flute, the complete metric thread size and pitch, quantity per size, workpiece grade and hardness, hole type and depth, required full-thread depth, and finished-thread tolerance. Include machine and holder details, any coating or chamfer requirement, and a drawing if the listed 100 mm overall length or other dimensions do not fit.
Can the length, tap geometry and OEM branding be customized?
Non-standard overall length, thread specifications, shank dimensions, cutting geometry, surface treatment, laser marking and packaging can be reviewed against your requirements. The available PM grade, manufacturing feasibility and inspection criteria are confirmed for each requested configuration before production.
Can spiral point and spiral flute sizes be combined in one order?
Mixed-style and mixed-size requests can be reviewed. Send a list showing the tap style, complete thread size and pitch, and quantity for each item. Sample availability, MOQ and lead time depend on the selected specifications and any customization.
Selection Guides
How to Choose HSS Cutting Tools
Thread Milling vs Tapping: Tool Selection
How to Choose a Thread Mill: Thread, Pitch & Tool Guide
The thread milling guides help compare alternative threading methods; their cutting data should not be applied to these machine taps.
Catalog & Technical Downloads
General tap series reference. Use this product page’s separate spiral point and spiral flute charts for the listed M2–M16 dimensions; other catalog series may differ.
HSS Cutting Tools Speeds & Feeds Guide (PDF)
General HSS reference. Confirm cutting speed for the actual HSS-PM grade, workpiece and tap style. For the listed single-start metric threads, synchronized tapping feed per revolution equals thread pitch.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.