
How to Choose a 4 Flute Carbide End Mill for Steel and Stainless Steel
4 flute carbide end mill selection involves more than diameter and an HRC label. Two Ø8 × 60 mm tools may differ in cutting length, shank, coating and application. Compare those details when quoting a replacement.
Use the seven checks below before ordering. Start with a model code, catalog page or photo; add the material and operation when available.
Quick Answer
Before ordering a four-flute carbide end mill, work through these seven checks:
- Material grade and condition: Identify the grade and condition, with hardness if known; distinguish steel from stainless steel.
- Square end, corner radius or ball nose: Match the cutting-end shape to the part drawing and feature.
- Standard and non-standard sizes: Choose a standard size or specify non-standard dimensions, units and tolerances on a drawing.
- What the tool will be used for: Identify slotting, side milling, profiling or finishing; consider chip removal and engagement.
- Cutting length and reach: Match the feature depth and access, including neck and holder clearance where needed.
- Tool geometry and coating: Use the selected model’s specification; flute count or coating colour alone is not enough.
- Order quantity, price and lead time: List quantities per size and agree price, availability, MOQ, delivery terms and any custom marking or packaging.
When Four Flutes Are a Useful Starting Point
Four flutes give four cutting edges per revolution. In many conventional designs, adding flutes leaves less chip space and allows a larger core. The balance still depends on the cutter’s geometry, diameter and cutting length.
For steel side milling and finishing, that design is often worth considering. It does not guarantee a better finish or a higher feed: the selected model and setup still need to suit the job.
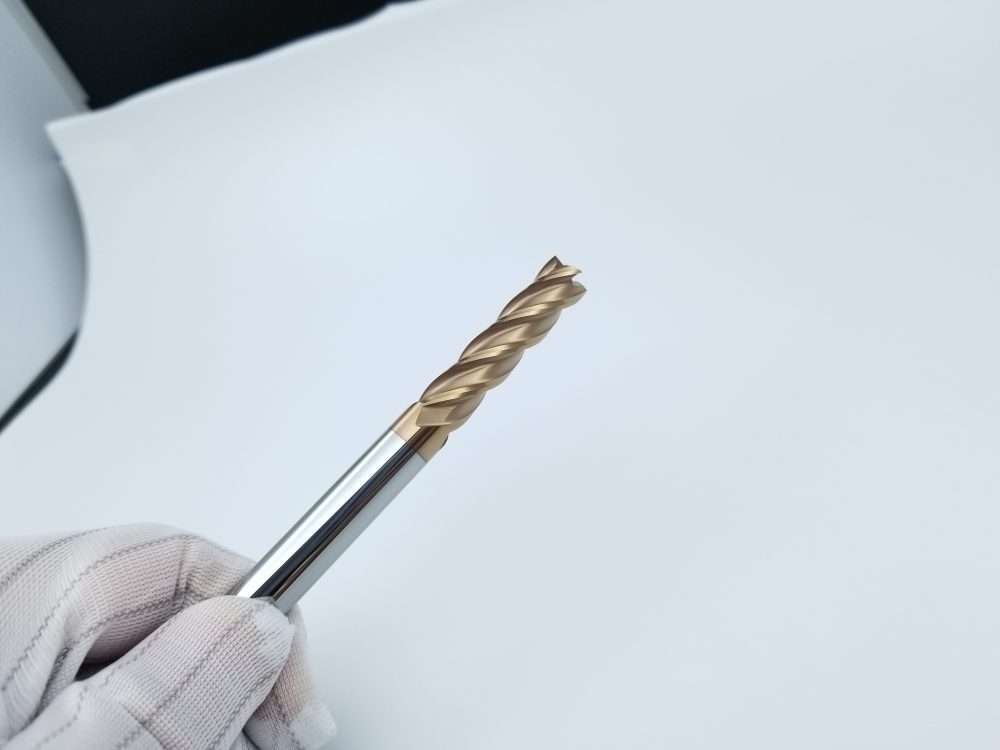
Two, Three or Four Flutes: Compare the Design
Use these common applications as a starting point when comparing tools of similar size. The preferred flute count can change with geometry and toolpath.
| Flute count | Typical use | Before choosing |
|---|---|---|
| 플루트 2개 | Often considered when larger flute space is useful, including many aluminum and slotting applications. | Material-specific geometry, chip removal and required stiffness. |
| 플루트 3개 | Common in aluminum tooling; dedicated designs also cover other materials and operations. | The exact material recommendation and geometry, rather than assuming every three-flute tool is for aluminum. |
| 플루트 4개 | Common in steel tooling for side milling, profiling and finishing. | Model suitability, chip space, engagement and setup for the actual job. |
Swipe horizontally to compare all columns on mobile.
For the underlying trade-off between flute count, core size and chip space, see Harvey Performance’s flute-count guide.
1. Material Grade and Condition
Ask for the material grade, not just “steel.” Annealed, hardened and cold-worked stock can require different selections.
| Customer material | Starting range to review | Information to confirm |
|---|---|---|
| Carbon or alloy steel | A suitable steel-milling series. | Grade, supplied condition, hardness if known, and operation. |
| 304, 316 or other stainless steel | A model recommended for that stainless application. | Exact grade, annealed or cold-worked condition, and operation. |
| Hardened steel | A series intended for the actual hardness. | Grade, measured hardness and required cutting operation. |
Swipe horizontally to compare all columns on mobile.
HRC series labels need context. An HRC55 or HRC65 label describes a supplier’s intended application range under specified conditions. It does not prove suitability for every material below that hardness, including stainless steel.
Compare our HRC55 four-flute square end mill for steel with the separate four-flute end mill range for stainless steel. Confirm the selected model rather than transferring one range’s specification to the other.
2. Choose Square End, Corner Radius or Ball Nose
Specify the end profile separately from flute count. Match it to the feature or the existing tool.
| End profile | Common feature | Confirm before ordering |
|---|---|---|
| Square end | Flat-bottom features and shoulders. | Required corner geometry and dimensional limits. |
| 모서리 반경 | Features that permit a corner radius. | Exact radius; a square-end replacement must satisfy the drawing. |
| 볼 코 | Curved surfaces and three-dimensional contours. | Ball diameter and the intended surface or toolpath. |
Swipe horizontally to compare all columns on mobile.
If the toolpath includes plunging or ramp entry, confirm center-cutting capability and the selected cutter’s entry limits.
For a closer comparison, read our corner radius end mill versus square end mill guide.
3. Standard and Non-Standard Sizes
Standard sizes are configurations in the supplier’s regular product range. Match the complete tool: cutting diameter, cutting length, overall length, shank and end profile. A common diameter alone does not identify a standard model.
Standard Size or Non-Standard Request?
| Request type | How to identify it | How to order |
|---|---|---|
| Standard size | The complete size and end profile match a regular model. | Use the model code; review its tolerances and availability. |
| Standard series variant | An available stub, long-flute, long-reach, inch-size or other regular option. | Review the product range first; a less common size may still be standard. |
| Non-standard size | The required size combination or tolerance is outside the supplier’s regular range. | Send a dimensioned drawing for feasibility, price, MOQ and lead-time review. |
Swipe horizontally to compare all columns on mobile.
A decimal diameter is not automatically non-standard, and a standard item is not necessarily in stock. Compare the actual specification across suppliers.
Specify Tool Sizes and Tolerances
Ø8 × 60 mm may mean cutting diameter and overall length in one catalog. It leaves other dimensions unspecified. Use descriptive names; dimension symbols and code order can differ between suppliers.
| Dimension | Specify | Why it matters |
|---|---|---|
| Cutting diameter | Nominal size, metric or inch units, and required tolerance. | Identify the finished cutter size; do not round an inch size to a nearby metric size. |
| 섕크 직경 | Size, holder-compatible shank tolerance and any required flat. | The shank may differ from the cutting diameter. |
| Length of cut / flute length | Required cutting length, using the supplier’s drawing definition. | Do not substitute overall length or reach for cutting length. |
| 전체 길이 | Total end-to-end tool length. | It is not a guaranteed cutting-depth rating. |
| Neck and reach, if applicable | Neck diameter, relieved length and the reach measurement endpoints. | Different reach definitions can hide a clearance mismatch. |
| Corner radius or ball profile | Required profile, radius and any critical profile tolerance. | A nominal radius alone may not satisfy the customer’s drawing. |
Swipe horizontally to compare all columns on mobile.
Keep cutter-diameter, shank and radius tolerances separate. State critical limits explicitly and agree whether they apply to the finished coated tool. Do not copy a finished-part tolerance directly onto the tool drawing.
For non-standard requests, send a dimensioned tool drawing or an annotated reference, the material and operation, quantity and required date. Retain the approved drawing revision for repeat orders. Installed projection and clamping length are setup dimensions; review them separately from overall tool length.
For dimension definitions, see Harvey Performance’s end mill anatomy guide.
4. What Will the Tool Be Used For?
The same material and diameter can require different tooling or cutting data when the operation changes.
| Operation | Main selection check | Tell the supplier |
|---|---|---|
| Side milling / profiling | Material suitability, reach and radial engagement. | Wall height, contour and available setup details. |
| Full-width slotting | Flute space and reliable chip removal. | Slot width, depth and how chips leave the cut. |
| Deep pocket machining | Reach, clearance and chip removal. | Pocket depth, access and holder clearance. |
| 마무리 | End profile, edge condition and dimensional requirements. | Surface requirements, tolerance and remaining stock. |
Swipe horizontally to compare all columns on mobile.
Do not transfer light side-milling settings directly to slotting. Trapped chips can be recut and damage the edge.
Review feed when engagement changes. Small radial engagement can reduce actual chip thickness relative to programmed feed per tooth. If you reduce stepover, check the toolmaker’s chip-thinning guidance as well; an excessive correction can overload the edge.
For starting-data checks, use our carbide end mill speeds and feeds guide alongside Sandvik Coromant’s chip-thickness guidance.
Need a Quote for a Replacement Tool?
Send the current model code, photo or drawing, plus sizes and quantities. Add the application if known so we can review a replacement option.
5. Cutting Length and Reach
Choose enough cutting length and clearance for the feature. Additional length can increase deflection and vibration risk.
| Requirement | Check | Avoid assuming |
|---|---|---|
| Cut a taller wall | Enough cutting length for the intended pass. | A longer cutting section is always better. |
| Reach a recessed feature | Neck relief, usable reach and interference. | Deep access always requires long flutes. |
| Clear the holder | Required projection and remaining clamping length. | The holder clears the feature because the tool fits. |
| Choose a longer tool | The complete tool and part geometry. | 100 mm overall length permits a 100 mm-deep cut. |
Swipe horizontally to compare all columns on mobile.
If chatter is already the problem, record where it begins and check the setup. Our guide to reducing chatter in end milling covers the broader troubleshooting process.
6. Tool Geometry and Coating
Confirm geometry and coating by model. Four flutes do not identify the helix, flute spacing or edge preparation.
| 기능 | What to confirm |
|---|---|
| Helix and flute spacing | Specified design; variable pitch or variable helix if required. |
| Edge preparation | Suitability for the material and operation; sharper or more heavily prepared is not universally better. |
| 코팅 | Actual coating name on the quoted model, including any optional configuration. |
Swipe horizontally to compare all columns on mobile.
| Range | Coating reference | Buying check |
|---|---|---|
| HRC45 steel series | AlTiN. | Confirm the quoted model and intended material. |
| HRC55 steel series | TiSiN. | Confirm the quoted model and intended material. |
| HRC65 steel series | AlTiSiN / specified Nano Blue. | Confirm the exact coating designation and configuration. |
| Stainless steel range | Confirm separately by model. | Identify the stainless grade and operation first. |
| Aluminum range | Uncoated / polished / DLC options. | Confirm the selected finish, geometry and coating, if applicable. |
Swipe horizontally to compare all columns on mobile.
These are series references, not proof of suitability for every material. Coating colour alone does not identify composition.
See our solid carbide end mill series guide to compare the ranges, then retain the final configuration in the quotation.
7. Order Quantity, Price and Lead Time
List quantities for each complete specification. Check the following points before accepting a quotation.
| Order item | Confirm in the quotation |
|---|---|
| Model and specification | Diameter, shank, cutting length, overall length, end profile and coating. |
| Quantity, price and MOQ | Quantity per size, unit price and minimum order quantity (MOQ). |
| Stock, lead time and shipping | Stock or production status, lead time, destination and shipping terms. |
| Custom marking and packaging | Required artwork or format; any effect on price, quantity or schedule. |
| Small trial orders | Dimensions, fit, surface requirements and intended-operation checks; record the approved model and test conditions. |
Swipe horizontally to compare all columns on mobile.
A photo helps identify the tool, but cannot confirm every tolerance or internal design detail.
What to Send for a Quote
START WITH THE DETAILS YOU HAVE
Your Tool List, Sizes and Quantities
Tool or reference
Model code, catalog page, photo or drawing.
Sizes and quantities
Required dimensions and quantity for each size.
Application, if known
Material grade, hardness and milling operation.
Helpful if available: cutting length, shank size, required reach, coating, destination country, target delivery date and marking or packaging needs.
Have only a photo or model list? Send it first. We can clarify the remaining details needed for a quotation.
Choose Your HY Tools End Mill Series
Use the product pages for dimensions and ordering details. Keep the steel and stainless steel ranges separate during comparison; their shared flute count does not make them interchangeable.
Steel and Alloy Steel
Review the HRC55 four-flute square-end range, then confirm the material, dimensions and coating.
스테인리스 스틸
Review the dedicated four-flute range and confirm the stainless grade, usable length and model-specific configuration.
For other end profiles and series, browse our solid carbide end mill collection.
Purchasing FAQ: Quotes, Small Trial Orders and Reorders
Select a question to view the answer.
Technical References
Send Your Four-Flute End Mill List
Send your model list or drawing, sizes and quantities for a quote. Include any marking, packaging or non-standard requirements.