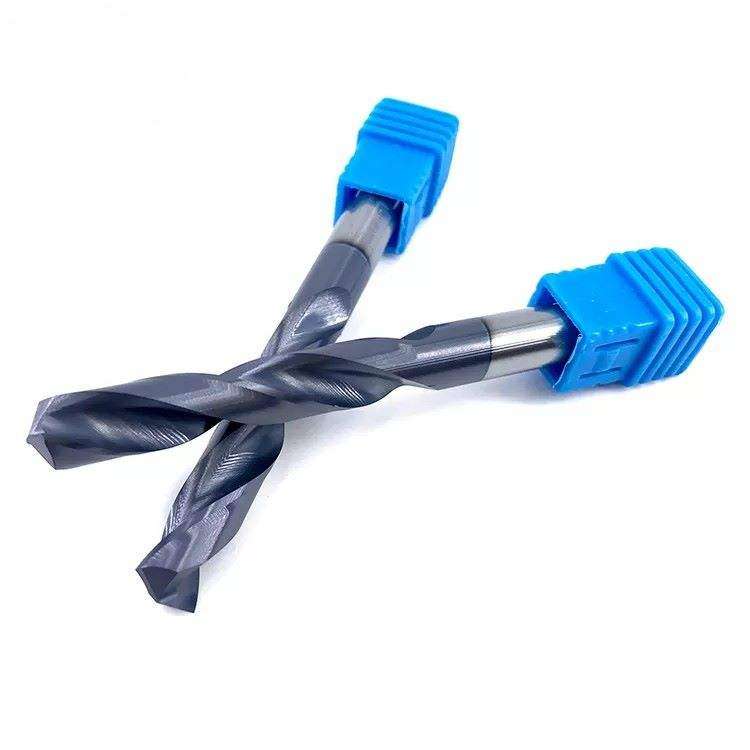
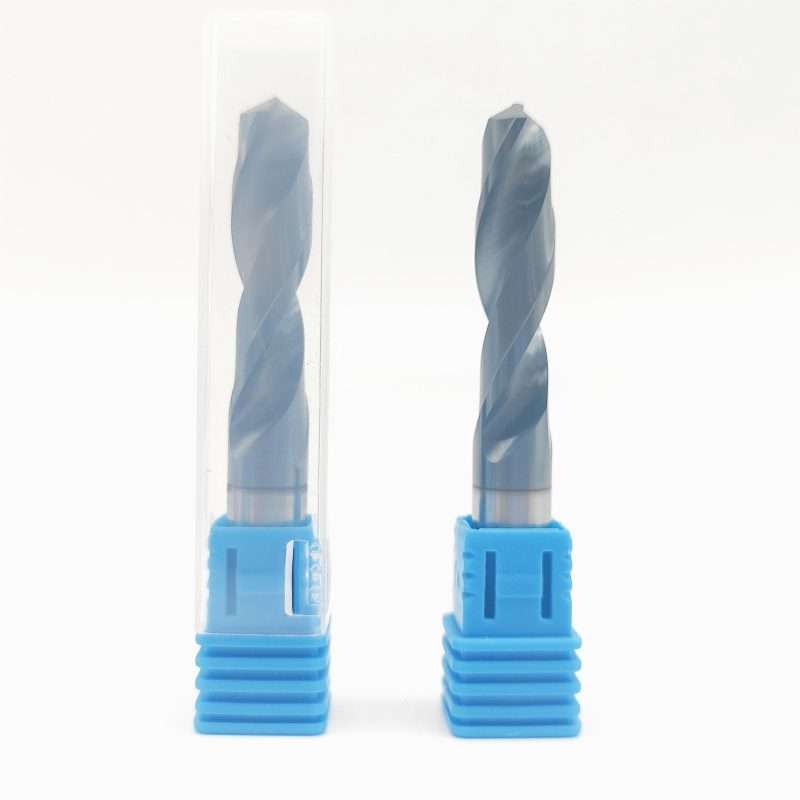
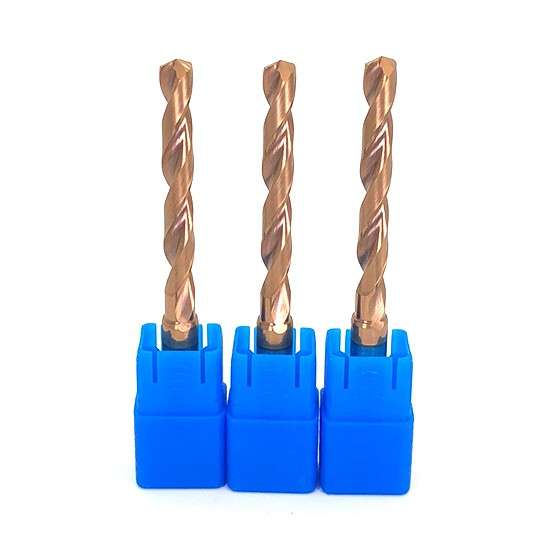
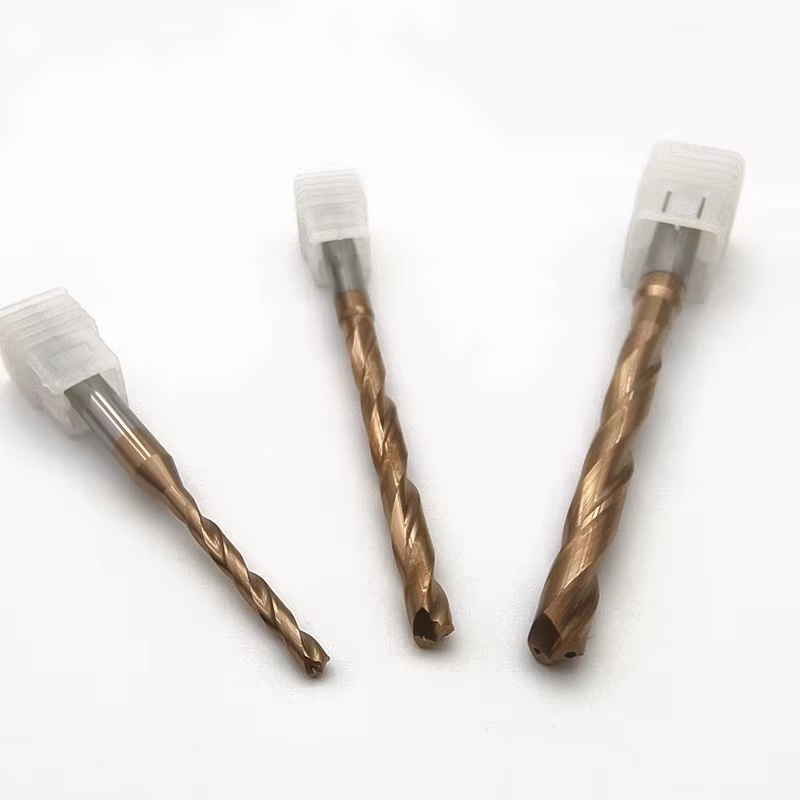
Stub-Length 2-Flute Solid Carbide Twist Drill for Precision Holes
Une qualité constante
Une géométrie constante d'une commande à l'autre.
Commandes flexibles
Petits lots et formats variés disponibles.
Assistance OEM
Marquage, étiquettes et emballages personnalisés.
Modèles standard et sur mesure
Dimensions standard et configurations sur mesure.
Stub-Length Carbide Twist Drill
This Stub-Length 2-Flute Solid Carbide Twist Drill is designed for precision shallow-hole machining where high rigidity, stable positioning and consistent hole dimensions are required. Its compact flute section and short overall length help reduce tool deflection and sensitivity to runout during CNC drilling. Manufactured from fine-grain solid carbide, the drill provides cutting-edge strength and dimensional stability for repeat production. A same-diameter straight-shank design supports simple, rigid clamping, while coated and uncoated configurations can be selected according to the workpiece material and machining conditions.
Key Configuration
Compact Stub-Length Design
Short flute length and compact overall length improve rigidity and help reduce bending during precision shallow-hole drilling.
2-Flute Spiral Geometry
Two precision-ground spiral flutes provide cutting-edge support and chip space for blind-hole and through-hole operations.
Same-Diameter Straight Shank
Each listed size group uses a cylindrical straight shank with D = d for a simple and stable clamping configuration.
Key Product Advantages
High-Rigidity Holemaking
The short cutting section reduces unnecessary unsupported length, supporting stable entry and lower tool deflection in shallow-hole machining.
Precision Hole Consistency
Fine-grain carbide and a compact tool structure support repeatable hole position, diameter and straightness under a rigid, low-runout setup.
Controlled Chip Evacuation
Two spiral flutes provide chip space for short blind and through holes when coolant or air delivery and drilling conditions are properly matched.
Material-Specific Surface Options
Coated, uncoated or polished configurations can be selected together with point and edge preparation for the confirmed workpiece material.
Compatibilité avec les matériaux des pièces à usiner
| ISO CODE | GROUPE DE MATÉRIAUX | REPRESENTATIVE MATERIALS | CONFIGURATION FOCUS |
|---|---|---|---|
| P | Steel | Carbon, alloy and pre-hardened steel | Edge Support / Coating |
| M | Acier inoxydable | Selected stainless grades | Material-Specific Geometry |
| K | Fonte | Gray and ductile cast iron | Wear-Resistant Geometry |
| N | Non-Ferrous Metals | Aluminum, copper and brass | Uncoated / Polished Option |
Applications & Target Scope
- Precision shallow-hole drilling
- Blind-hole and short through-hole machining
- Small-diameter precision holes
- Mold and mechanical component production
- Repeat-batch CNC hole machining
- Applications where reduced deflection and high tool rigidity are priorities
Product & Machining Details
Technical Specifications & Dimensions
The supplied Stub-Length 2-Flute Solid Carbide Twist Drill series covers Ø1.0–20.0 mm cutting diameters with a same-diameter cylindrical shank. Flute length, shank length and overall length increase by diameter group while retaining the compact structure required for precision short-hole machining.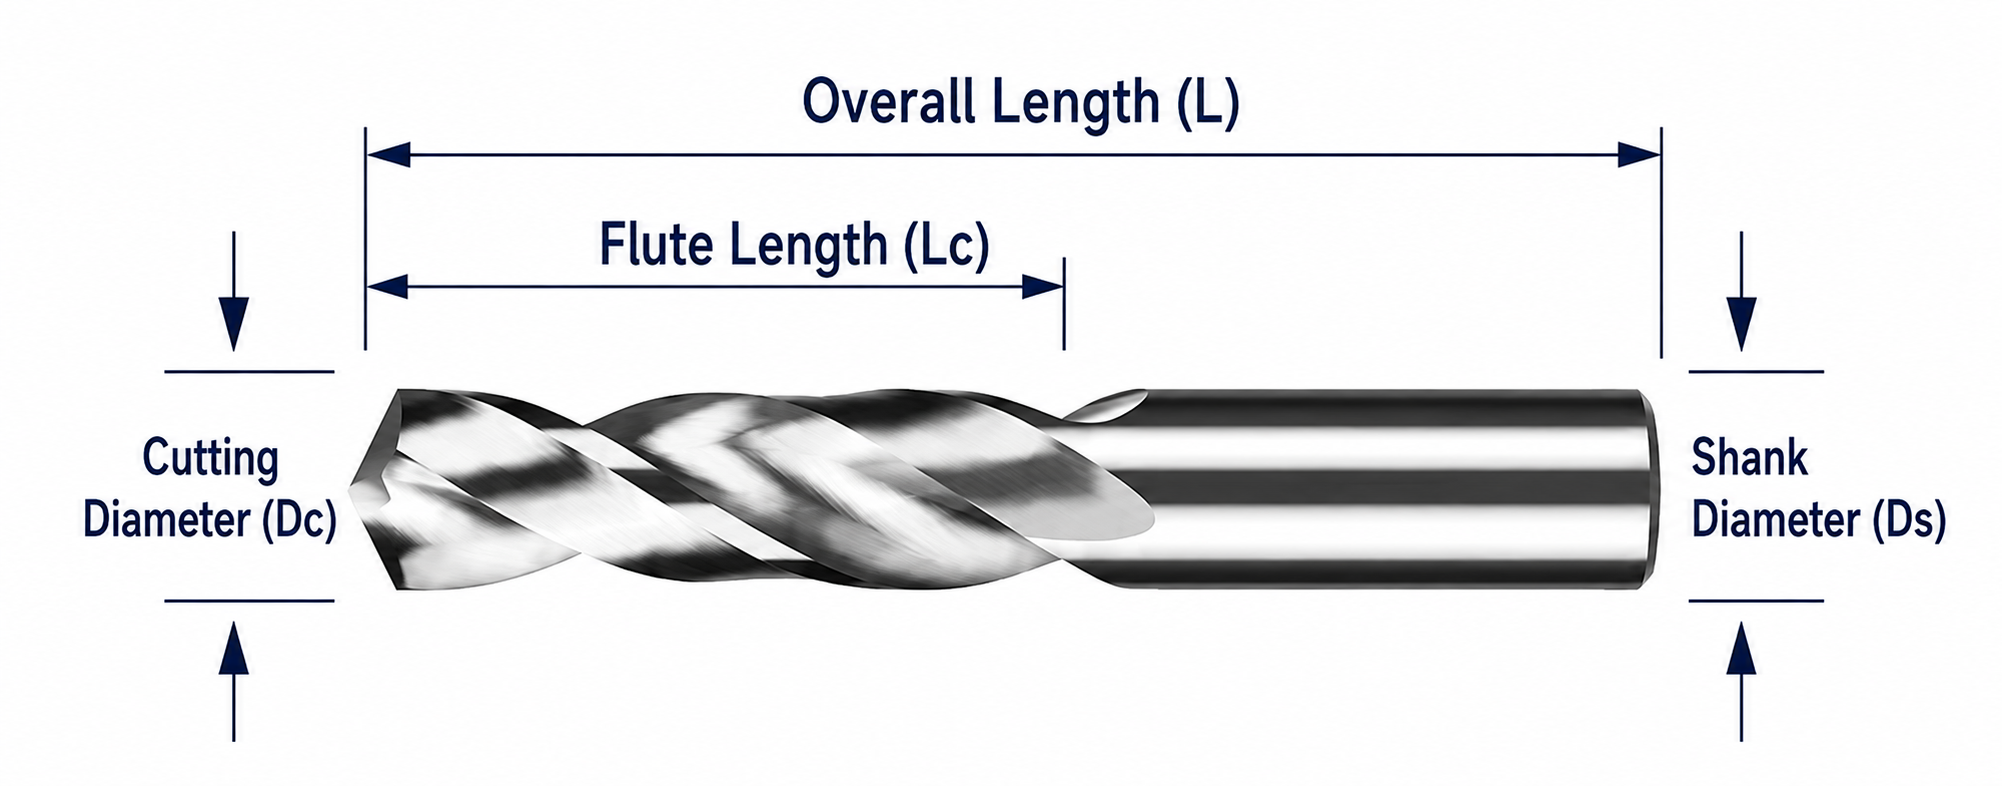
Standard Size Matrix
Each size group uses a same-diameter straight shank with D = d. Select the required cutting diameter within the corresponding range and confirm the final dimensional tolerance before ordering.
| d (mm) | L1 (mm) | D (mm) | L3 (mm) | L (mm) |
|---|---|---|---|---|
| 1.0–1.2 | 15 | 1.0–1.2 | 23 | 38 |
| 1.3–2.0 | 20 | 1.3–2.0 | 20 | 40 |
| 2.1–3.1 | 20 | 2.1–3.1 | 20 | 40 |
| 3.2–4.1 | 25 | 3.2–4.1 | 20 | 45 |
| 4.2–5.6 | 28 | 4.2–5.6 | 22 | 50 |
| 5.7–6.6 | 30 | 5.7–6.6 | 25 | 55 |
| 6.7–8.6 | 35 | 6.7–8.6 | 25 | 60 |
| 8.7–10.5 | 35 | 8.7–10.5 | 30 | 65 |
| 10.6–12.8 | 40 | 10.6–12.8 | 30 | 70 |
| 12.9–20.0 | 60 | 12.9–20.0 | 40 | 100 |
Stub-Length Precision-Hole Guidance
- Minimize Tool Overhang: Use the shortest practical unsupported length to preserve the rigidity advantage of the stub-length design.
- Control Holder Runout: Use a precision collet, hydraulic holder or shrink-fit holder with low spindle and tool runout.
- Use a Stable Entry Surface: Flat entry is preferred; curved, inclined or interrupted surfaces may require spot drilling or dedicated point geometry.
- Maintain Chip Evacuation: Use suitable coolant or air delivery and leave sufficient chip space in blind holes.
Recommended Starting Cutting Parameters
Starting speed and feed should be selected for the exact diameter, workpiece material, coating, hole depth, machine rigidity, holder runout and coolant condition. Begin conservatively and adjust after checking entry stability, chip evacuation, hole quality and tool wear.
Solid Carbide Drill Cutting Data Guide
Use the guide as a starting reference and adjust according to the selected material-specific drill configuration.
Stub-Length Selection Guide
Choose Stub Length
When high rigidity, shallow-hole capability, reduced deflection and repeatable hole dimensions are the main priorities.
Choose Jobber Length
When additional flute length and general-purpose reach are required for standard CNC drilling.
Choose Long Series
When the required hole position or depth cannot be reached by a stub-length or jobber-length tool.
For additional sizes and related drill series, View the Solid Carbide Drill Catalog.
Stub-Length Precision Drill Customization
Cutting diameter, short flute, compact overall length, point geometry, edge preparation and tolerance can be configured for rigid precision-hole machining. The short construction is maintained to minimize overhang and support positional stability.
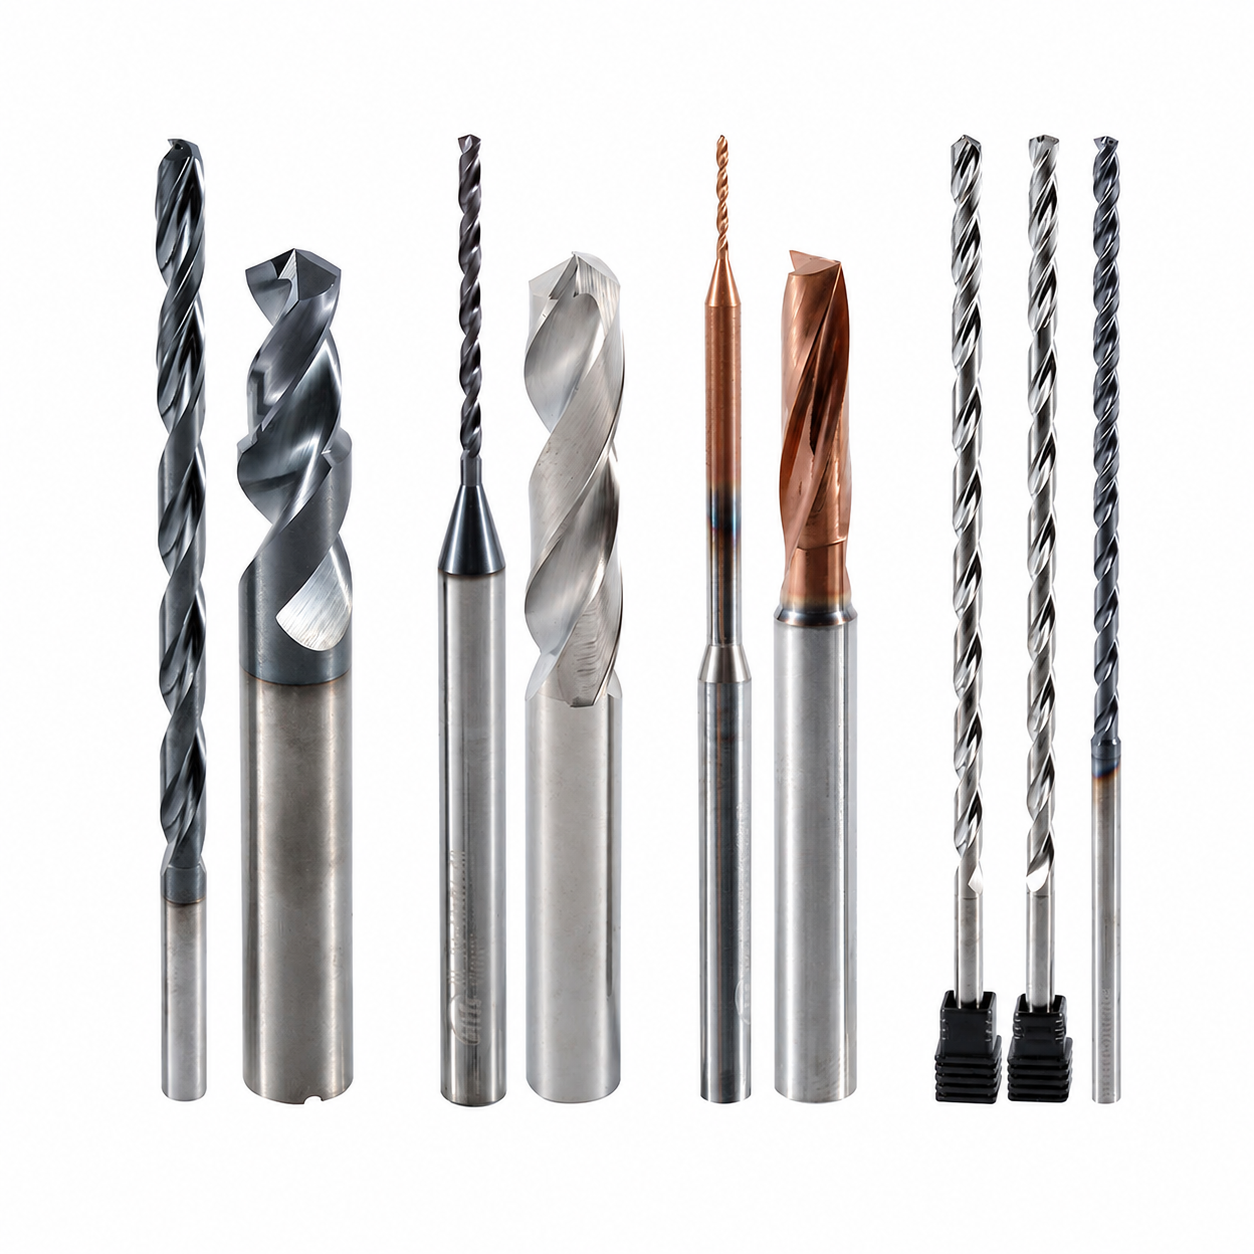
Rigid Stub-Length Geometry & Edge Preparation
Point form, web thinning, short flute, margins and cutting-edge preparation can be configured for controlled entry, low deflection and stable precision drilling.

Diameter & Compact-Length Options
Metric, fractional-inch and drawing-defined diameters can be combined with short flute, compact overall length and matched shank dimensions.
Services OEM et de marque de distributeur
OEM manufacturing and private-label supply options for precision machining facilities, industrial distributors and high-accuracy tooling customers.
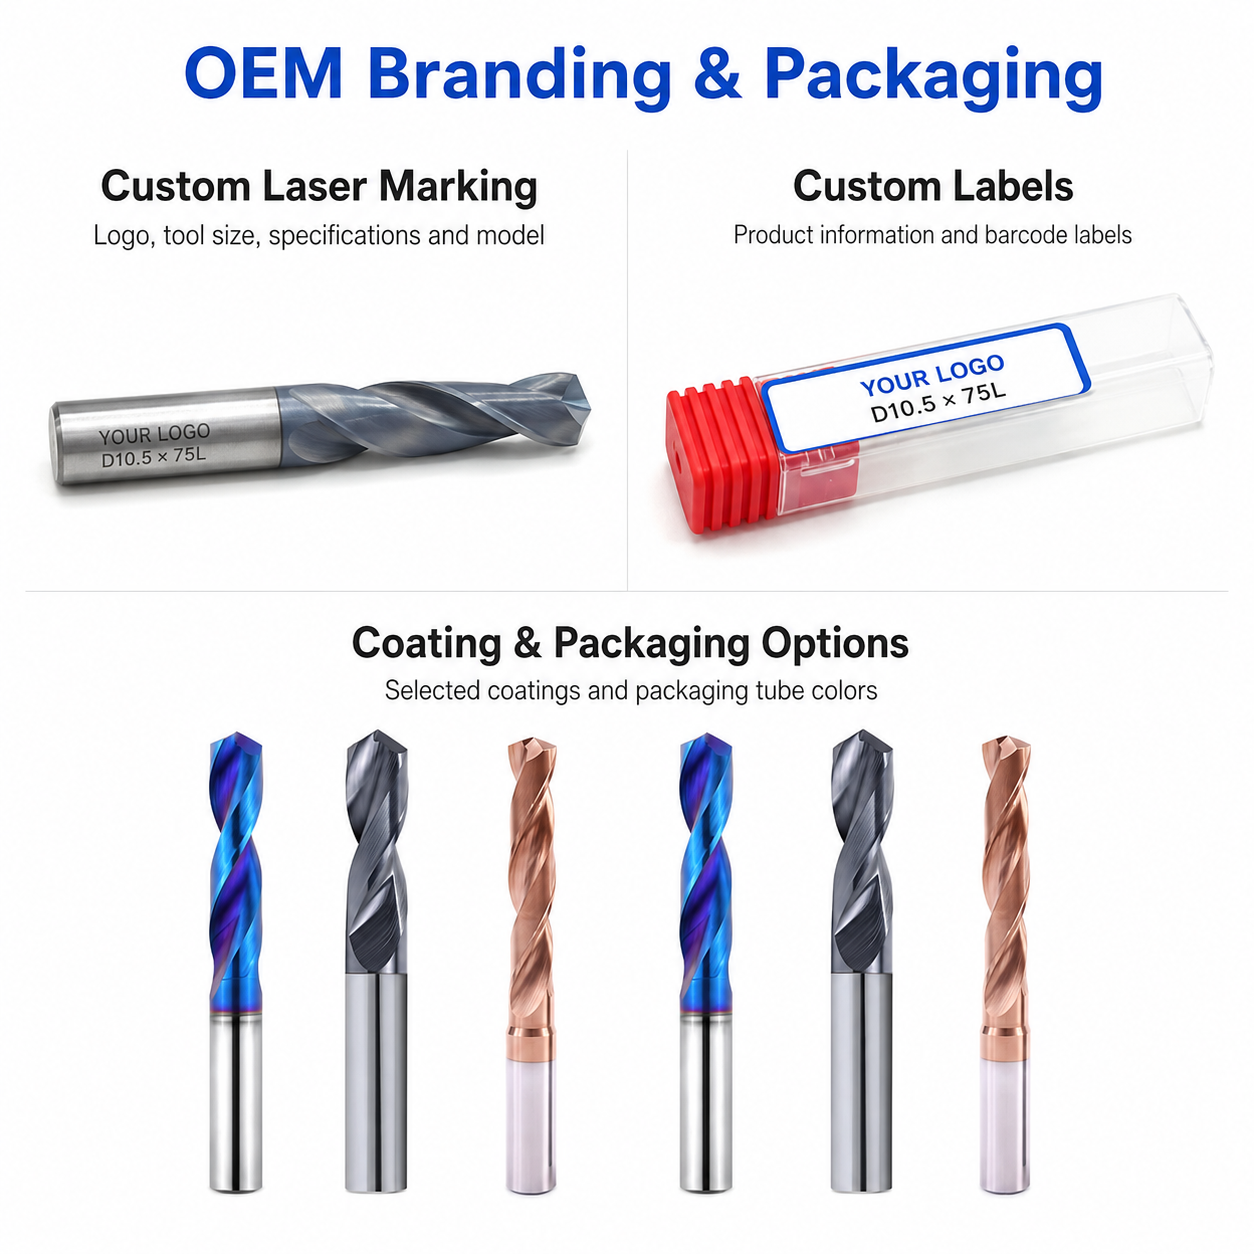
Gravure au laser
Custom laser marking for logos, tool codes, diameter specifications, coating identification and batch numbers.
Custom Packaging
Individual protective tubes, diameter labels, multi-pack boxes, custom inserts and private-label packaging options.
Conditions commerciales
Flexible MOQ options for standard configurations, custom sizes, trial orders and scheduled repeat supply.
Processus technique
Demande de renseignements
Submit the material, shallow-hole dimensions, positional tolerance and quantity.
Ingénierie
Compact length, point geometry, edge preparation and coating are reviewed.
Commercial
Quotation, MOQ, production schedule and delivery terms are confirmed.
Production
Short-tool CNC grinding, edge preparation, coating and identification.
Contrôle qualité
Diameter, compact length, point geometry, runout and cutting edges are inspected.
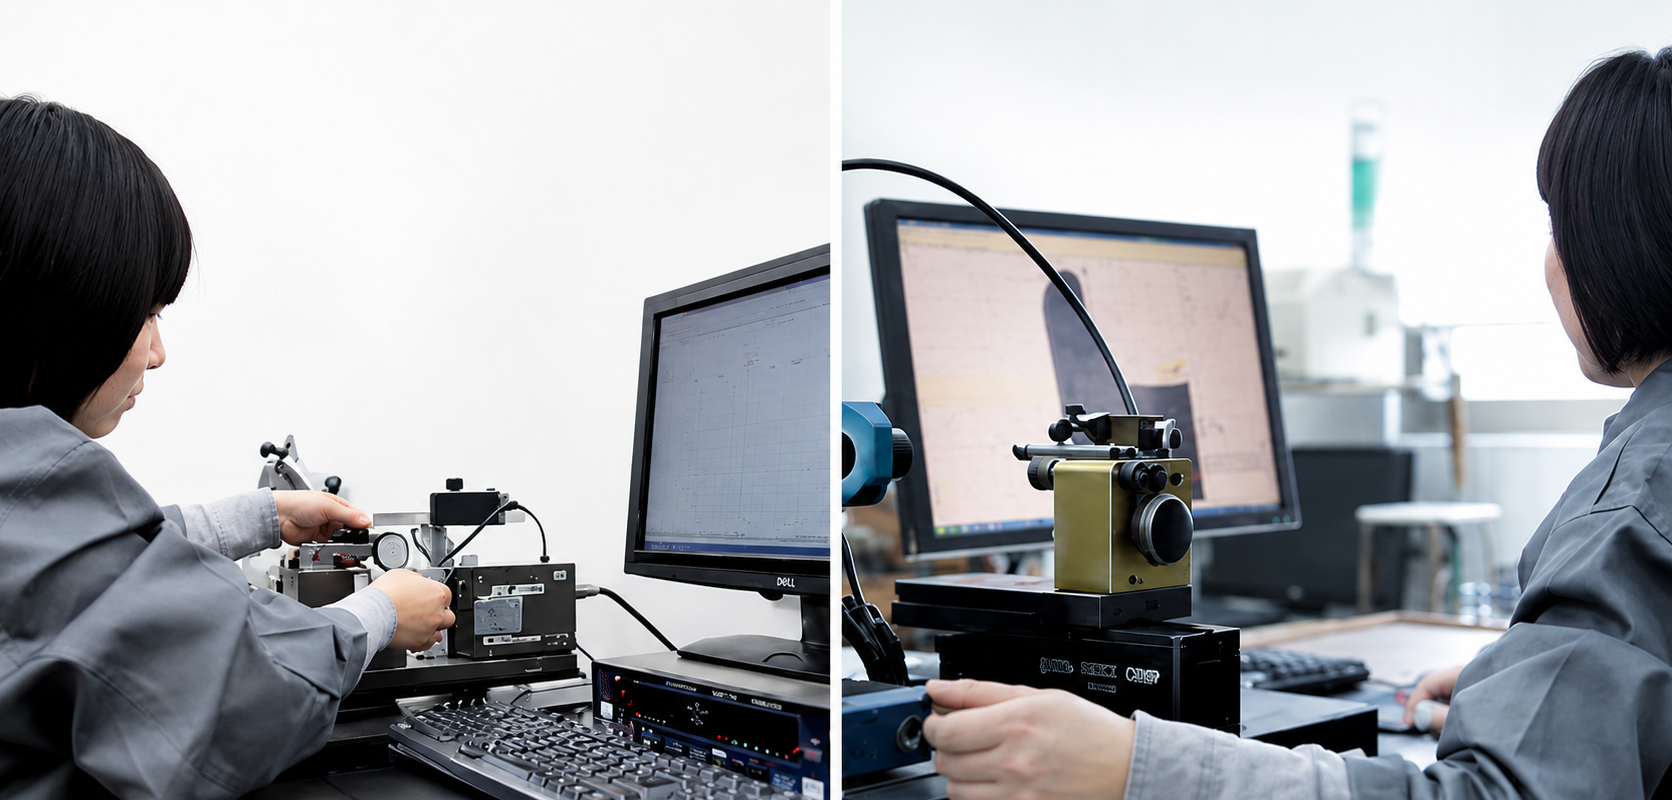
Inspection & Quality Control
Drill dimensions, cutting-edge geometry and visible surface condition are checked according to the confirmed product specification and application requirements.
Protective Packing for Shipment
Finished drills are protected individually before batch labeling and export-carton reinforcement.

Individual Tool Protection
Each drill is individually protected in a plastic tube to reduce contact damage during storage, handling and transportation.
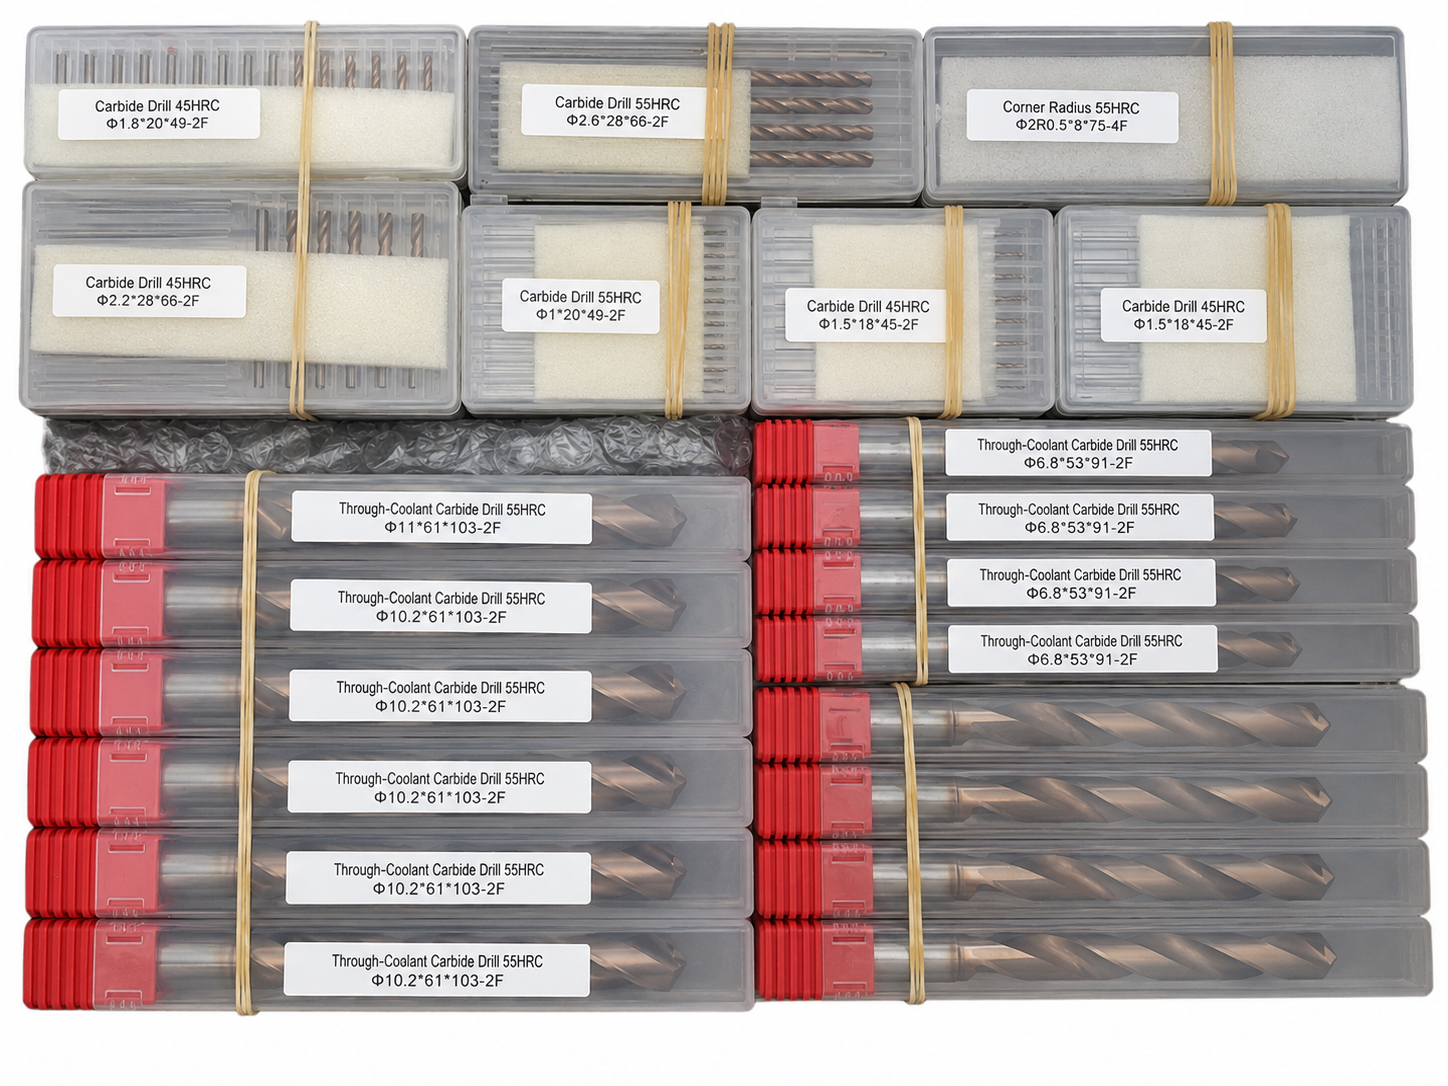
Batch & Label Verification
Tools are grouped and labeled by specification to support order verification before carton packing.

Export Carton Protection
Batch packaging, cushioning materials and reinforced export cartons are selected according to the order quantity and shipping method.
Reference Lead Time
The following timeframes are general references. Availability and production scheduling are reviewed for each order.
Shipping Options
Shipping arrangements can be selected according to order size, delivery schedule and destination.

Product FAQs
Product-specific information about stub-length drilling, precision-hole applications, tool rigidity, chip evacuation, material selection and available custom configurations.
What is a stub-length solid carbide drill used for?
A stub-length drill uses a shorter flute and reduced unsupported cutting length to increase rigidity. It is suitable for precision shallow holes, positioning holes and short drilling operations where hole location, diameter stability and controlled entry are more important than extended drilling depth.
Why choose a stub-length drill instead of a standard-length drill?
The shorter cutting section reduces tool deflection and sensitivity to vibration. When the required hole depth is limited, a stub-length configuration can provide higher rigidity and more stable entry than using a longer drill with unnecessary flute length.
How does the 2-flute geometry support precision hole drilling?
The 2-flute geometry provides a practical balance between cutting-edge support and chip space. With controlled point geometry, low runout and rigid toolholding, it supports stable penetration and consistent chip evacuation in short precision-hole operations.
What machining conditions are important for precision holes?
Low spindle and holder runout, a rigid setup, clean clamping surfaces and the shortest practical tool overhang are important. Stable entry, appropriate coolant delivery and continuous chip evacuation should also be maintained to support hole size and position consistency.
Can the diameter, flute length, point geometry and coating be customized?
Yes. Cutting diameter, flute length, shank diameter, overall length, point geometry, edge preparation and coating can be reviewed according to the required hole depth, workpiece material, tolerance and machine setup. Non-standard dimensions can also be evaluated from a customer drawing.
What information is required for a quotation?
Please provide the cutting diameter, finished-hole tolerance, hole depth, flute length, workpiece material and hardness, coolant condition, machine type and required quantity. For non-standard dimensions or special hole requirements, a drawing is recommended before quotation.
Ordering & OEM FAQs
General information for trial orders, mixed sizes, private labeling and repeat distributor supply.
Do you accept small trial orders?
Yes. Small trial quantities can be reviewed for hole-quality testing, dimensional verification and tool-life evaluation before larger repeat orders.
Can mixed drill sizes be ordered together?
Yes. Different cutting diameters and stub-length configurations can normally be combined in one order when the carbide, coating and production requirements are compatible. Mixed-size orders are suitable for distributors and multi-size application testing.
Is OEM laser marking available?
Yes. Custom laser marking for logos, item numbers, tool sizes and batch identification can be reviewed together with private labels and OEM packaging requirements.
What is the typical production lead time?
Lead time depends on diameter, flute length, coating, quantity and whether the drill uses a standard or custom configuration. Final production scheduling is confirmed after the dimensions and technical requirements are approved.
Downloads & Technical Resources
Access drill series information and starting cutting-data references for precision-hole application review.
Vous avez besoin d'informations sur les tailles, les prix ou les options personnalisées ?
Veuillez nous indiquer le type d'outil requis, ses dimensions, les quantités, le matériau de la pièce à usiner ainsi que toute exigence spécifique à un équipementier ou toute demande sur mesure. Nous vous confirmerons les caractéristiques techniques adaptées, la disponibilité, le délai de livraison et les détails du devis.
Les croquis, les listes de dimensions et les photos de référence sont les bienvenus.