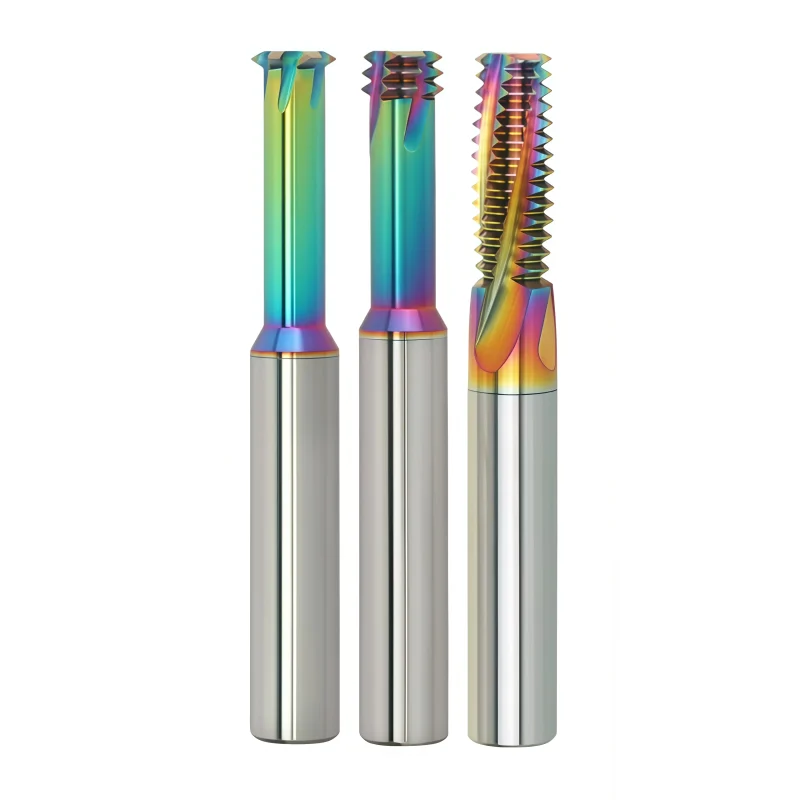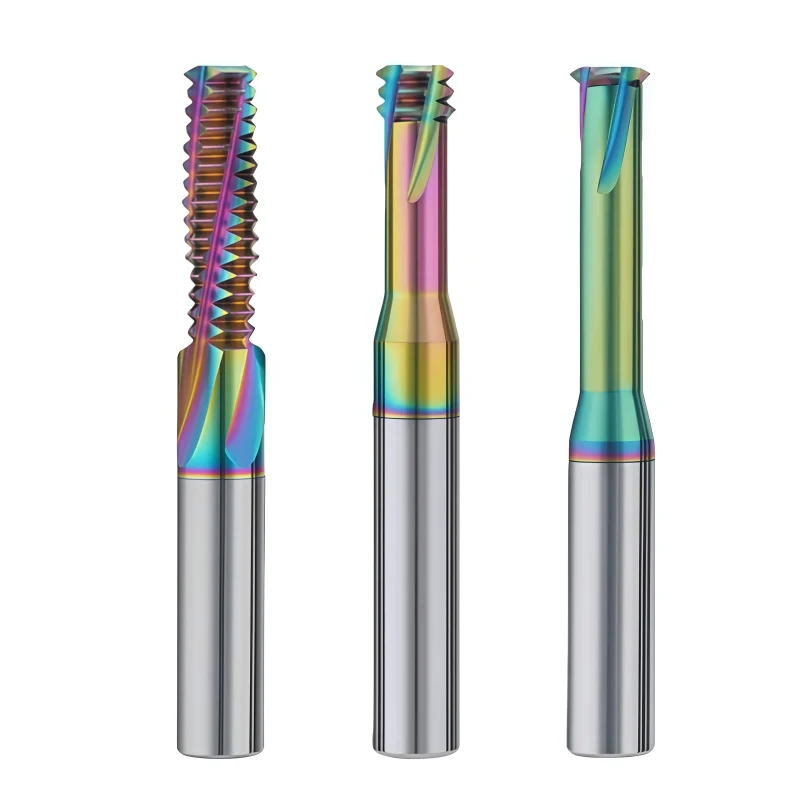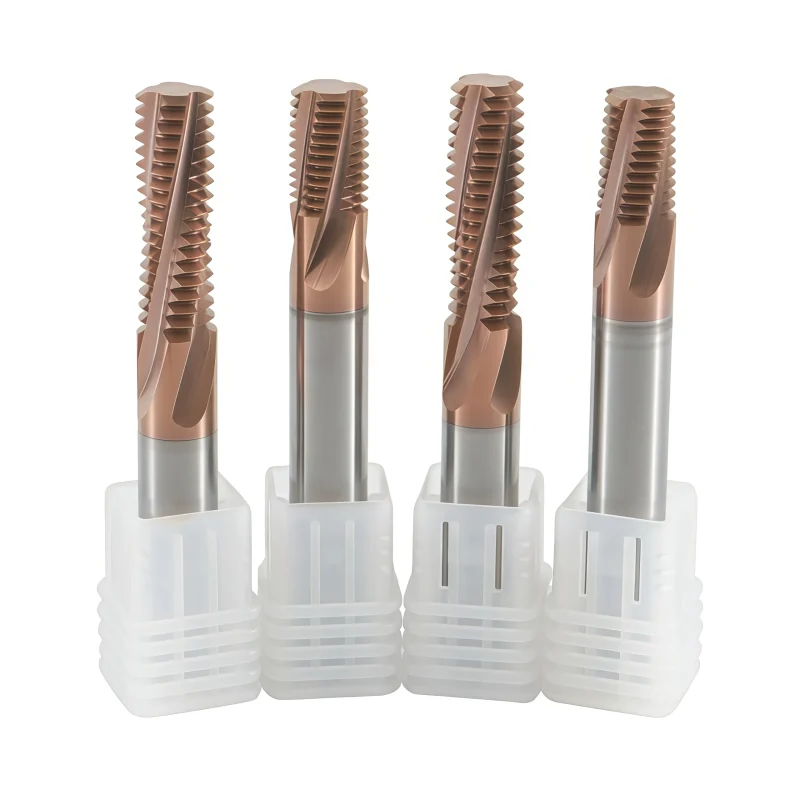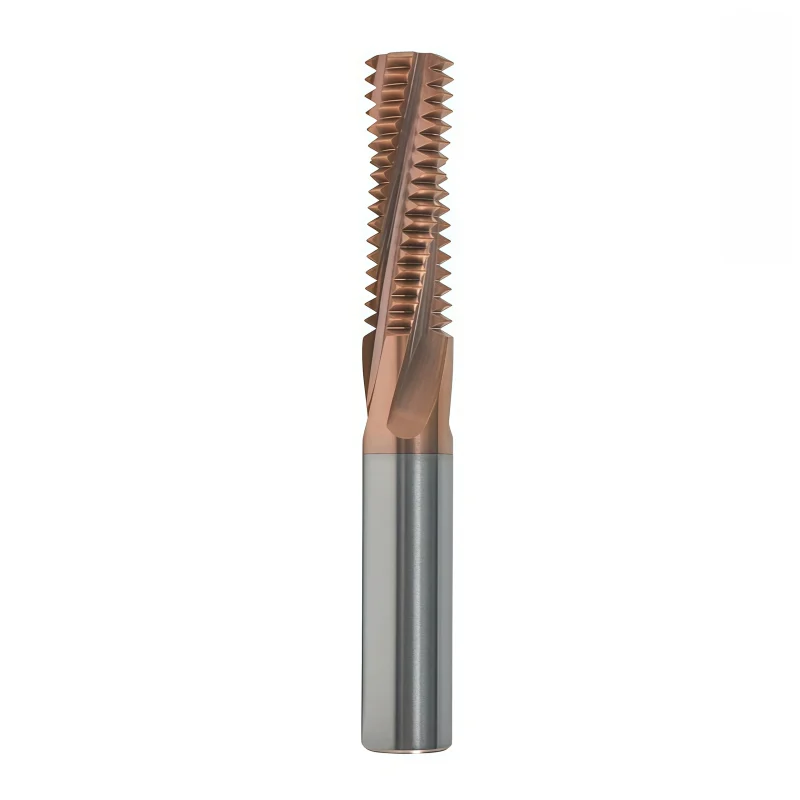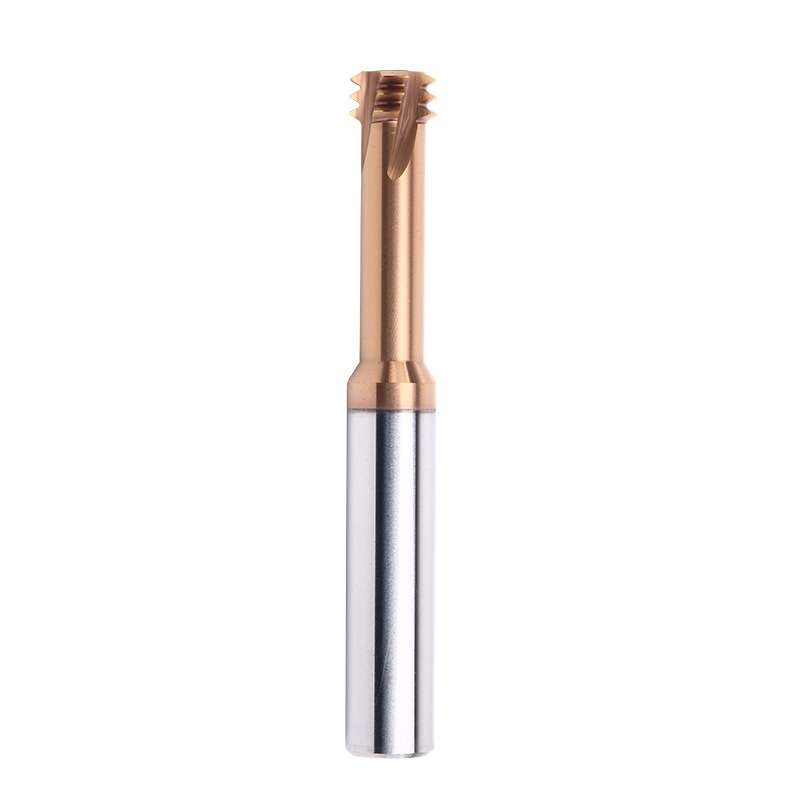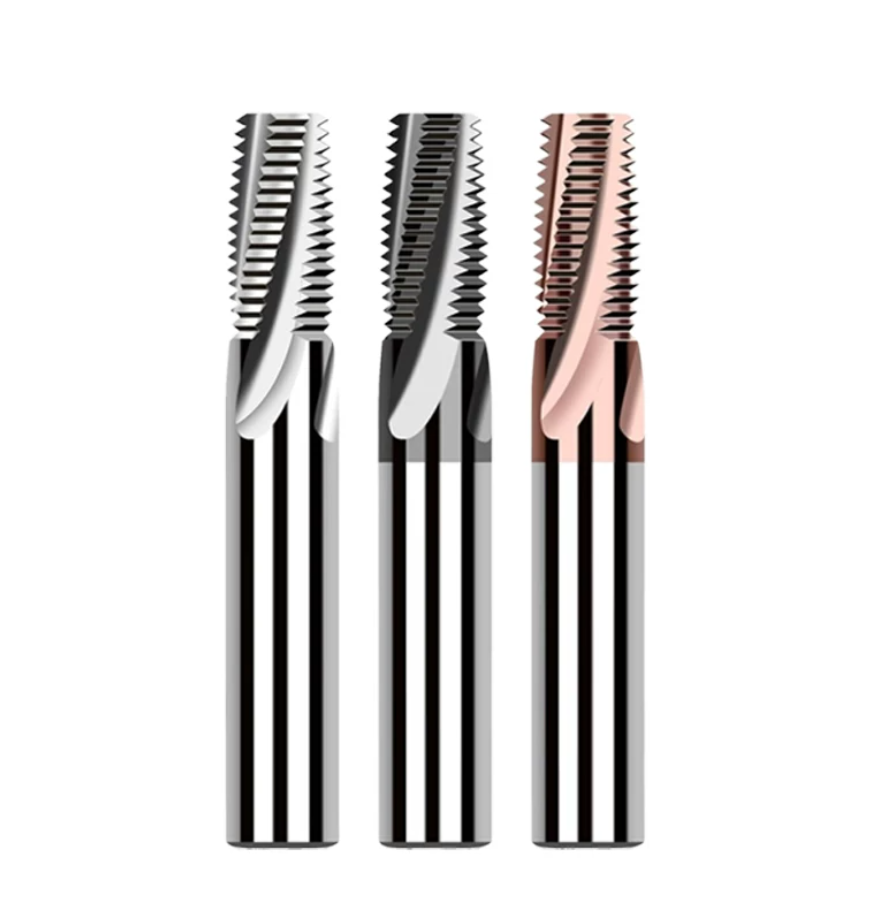
Solid Carbide NPT and NPTF Full-Profile Thread Mills for Taper Pipe Threads
SOLID CARBIDE NPT / NPTF FULL-PROFILE THREAD MILL
Precision CNC thread milling for 60° internal NPT and NPTF taper pipe threads, with a 1:16 taper, nominal sizes from 1/16″ to 1″ and 11.5–27 TPI.
Product Configuration
Taper Pipe Thread Milling ApplicationInternal NPT and NPTF taper pipe threads produced by CNC helical interpolation. Separate tool codes are provided for each standard; select the correct tool and matching gauge according to the drawing.
Consistent Quality
Consistent geometry across repeat orders.
سفارشهای انعطافپذیر
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
استاندارد و سفارشی
Standard sizes and custom configurations.
NPT & NPTF Full-Profile Thread Mill Overview
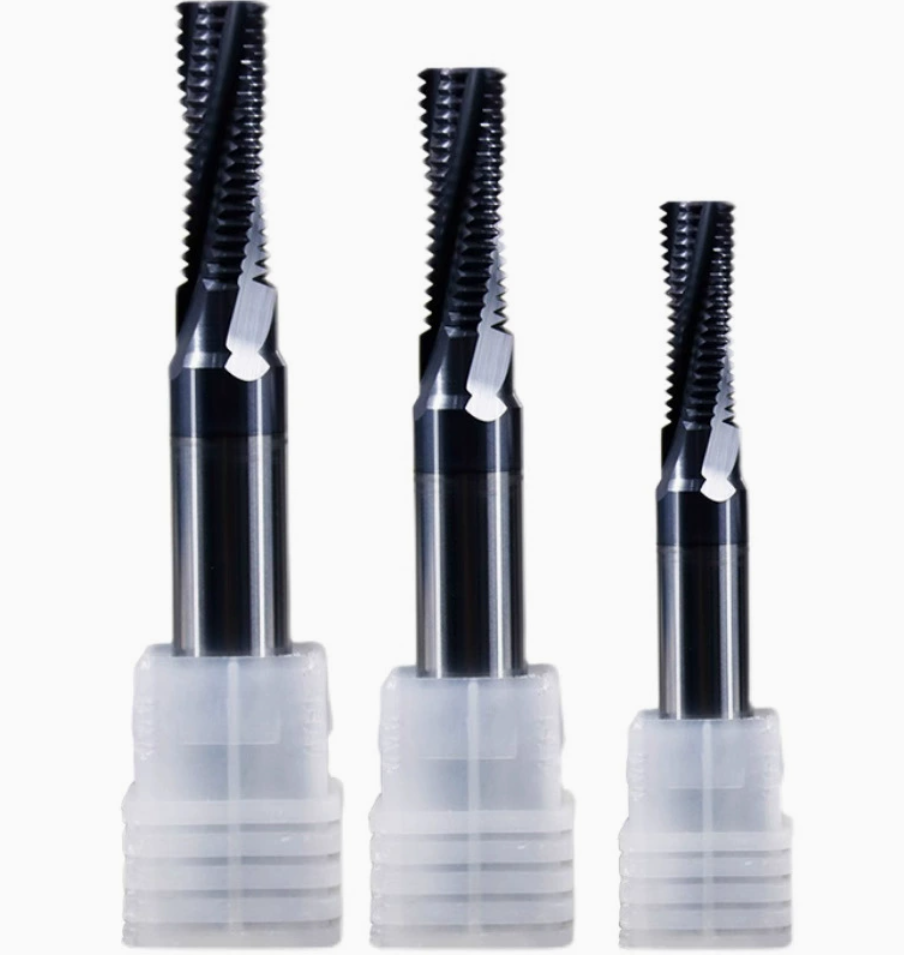
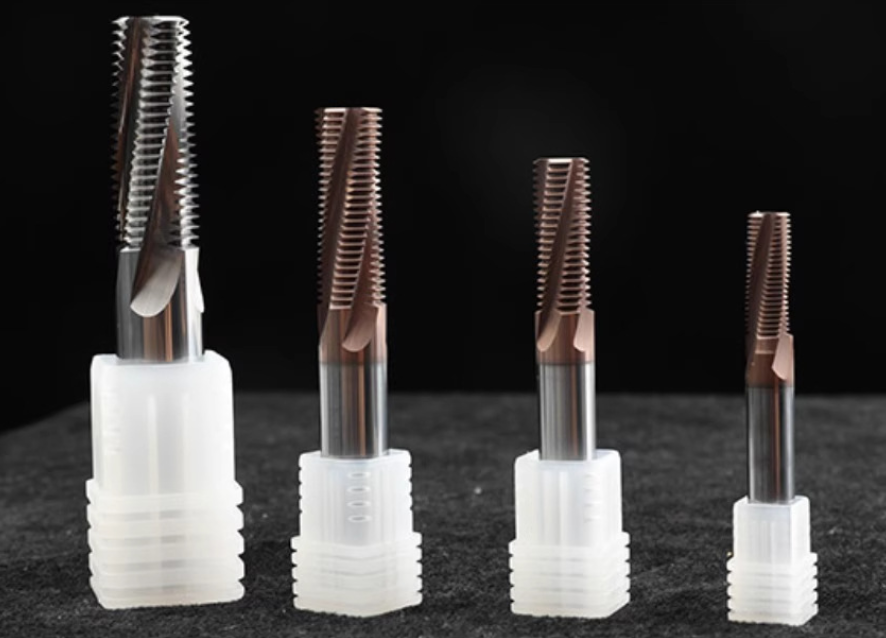
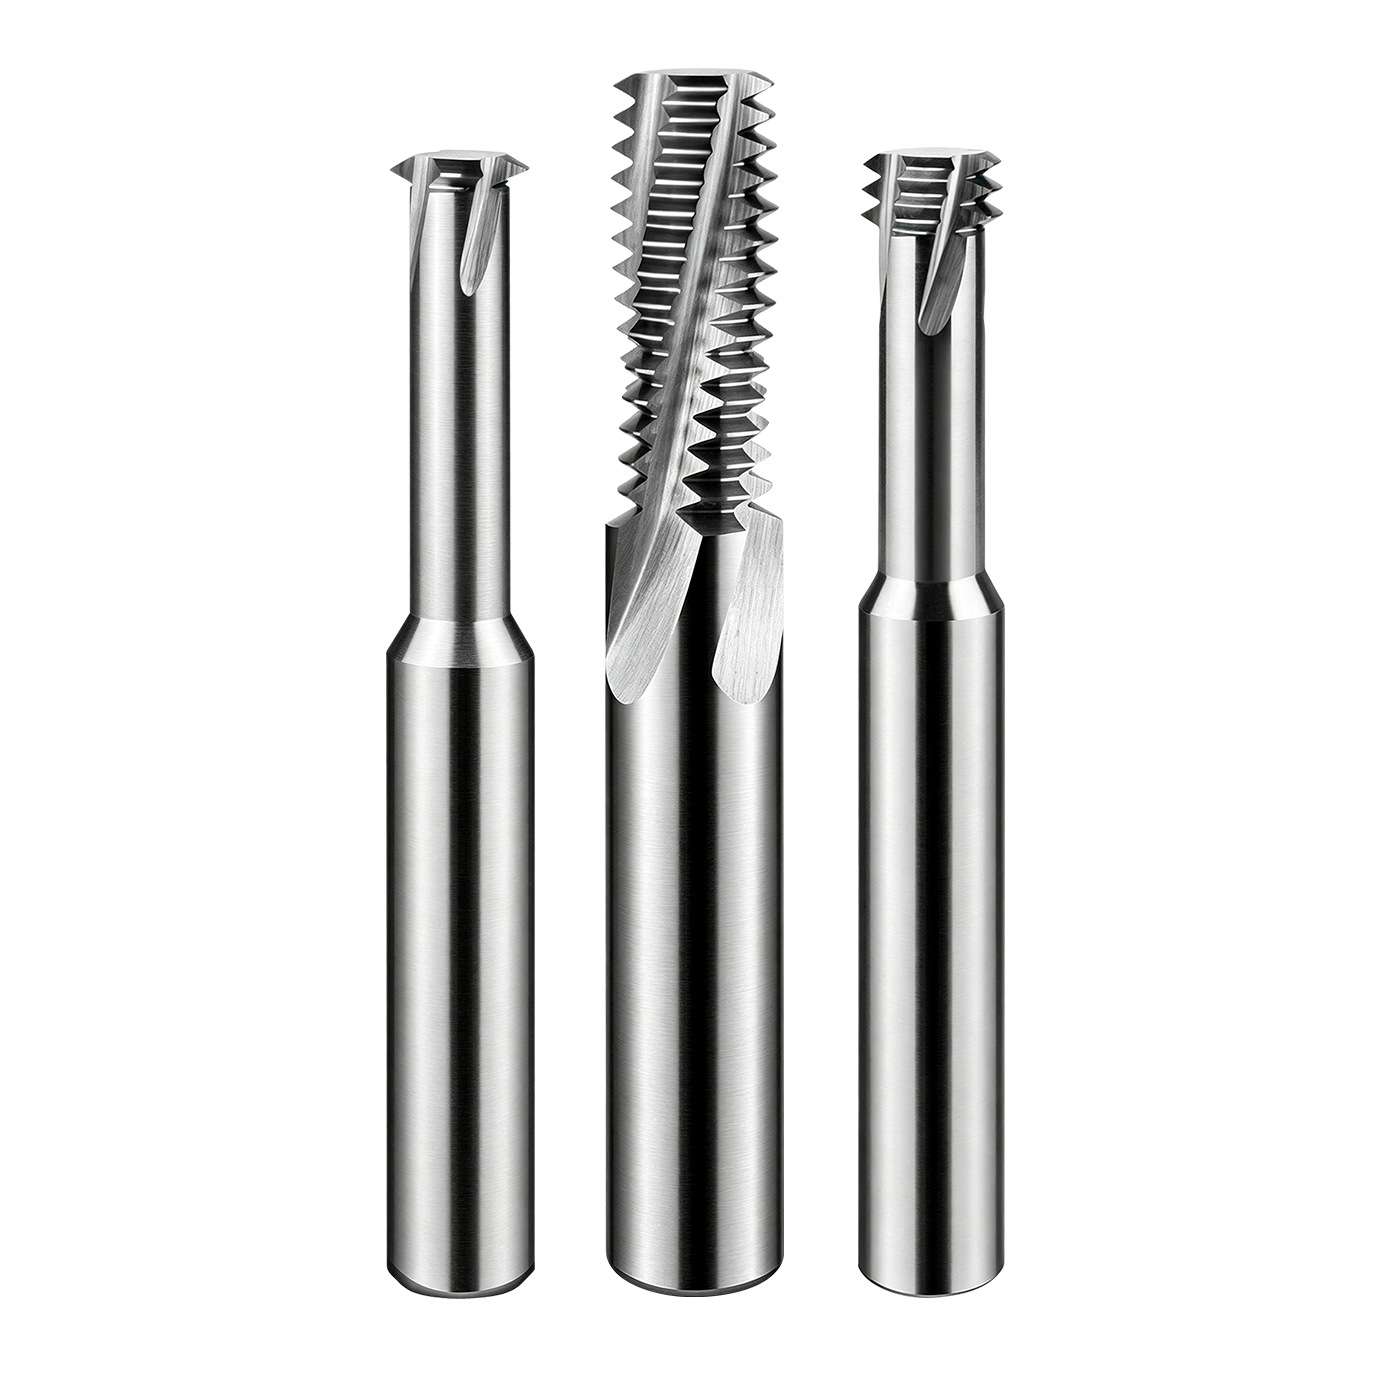
These solid carbide full-profile thread mills are designed for precision CNC machining of 60° NPT and NPTF internal taper pipe threads. The 1:16 taper geometry and size-specific full-profile cutting teeth generate the thread flanks, crest and root form in a controlled helical milling cycle. Standard configurations cover nominal pipe sizes from 1/16″ to 1″, 11.5 to 27 TPI, cutter diameters from Ø5.4 to Ø17.38 mm and 4- or 5-flute designs according to tool size.
Key Configuration
60° Full-Profile Geometry
Size-specific cutting teeth reproduce the complete 60° pipe-thread form, supporting controlled flank, crest and root generation in one helical milling cycle.
1:16 Tapered Thread Path
The cutter geometry and programmed CNC path are matched to the 1:16 pipe-thread taper for consistent internal NPT or NPTF thread production.
Separate NPT & NPTF Series
Dedicated NPT and NPTF product codes help prevent standard mix-ups and allow the specified pipe thread to be selected, programmed and inspected independently.
Key Product Advantages
Complete Thread Form
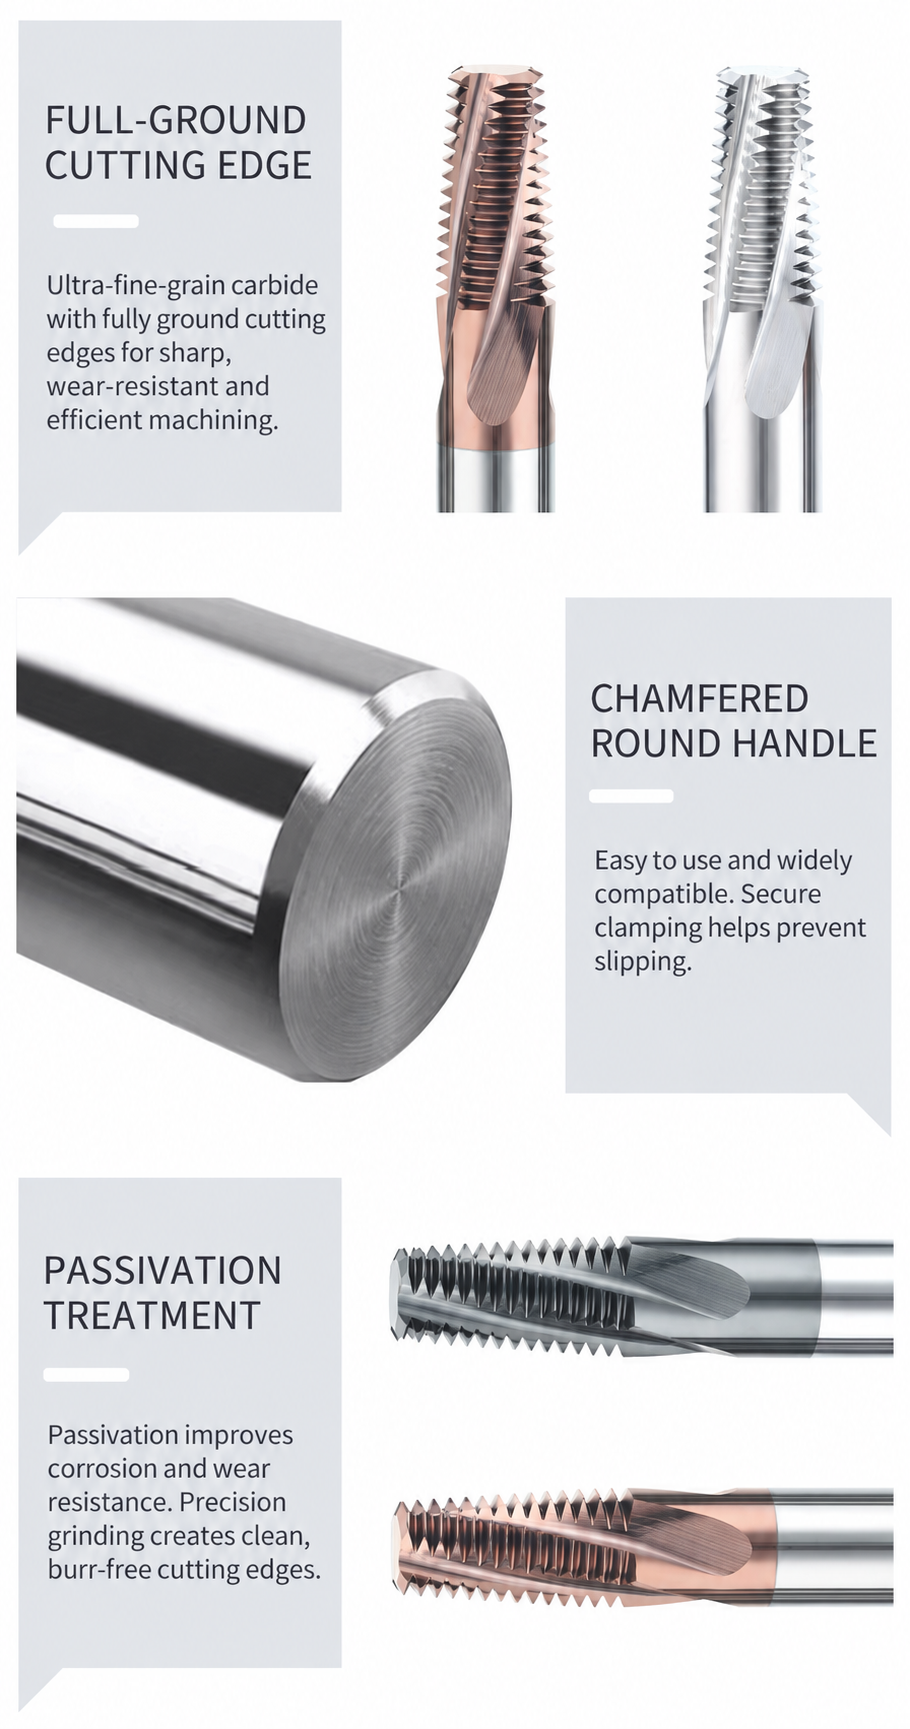
Full-profile teeth machine the specified 60° taper pipe thread form with repeatable axial pitch and profile geometry.
Controlled Taper
A taper-specific CNC path supports consistent thread engagement and gauge control across the machined length.
Stable Multi-Flute Cutting
Standard 4-flute and 5-flute configurations balance cutting load, tool-body rigidity and productivity according to size.
Carbide Rigidity
Fine-grain solid carbide construction supports dimensional stability, wear resistance and controlled cutting in demanding pipe-thread applications.
Pipe Thread Milling Operations
The standard series is intended for CNC milling of internal tapered pipe threads. Final tool selection must match the specified thread standard, nominal pipe size, TPI, required thread length, pilot-bore diameter and gauge requirement.
Workpiece Material Compatibility
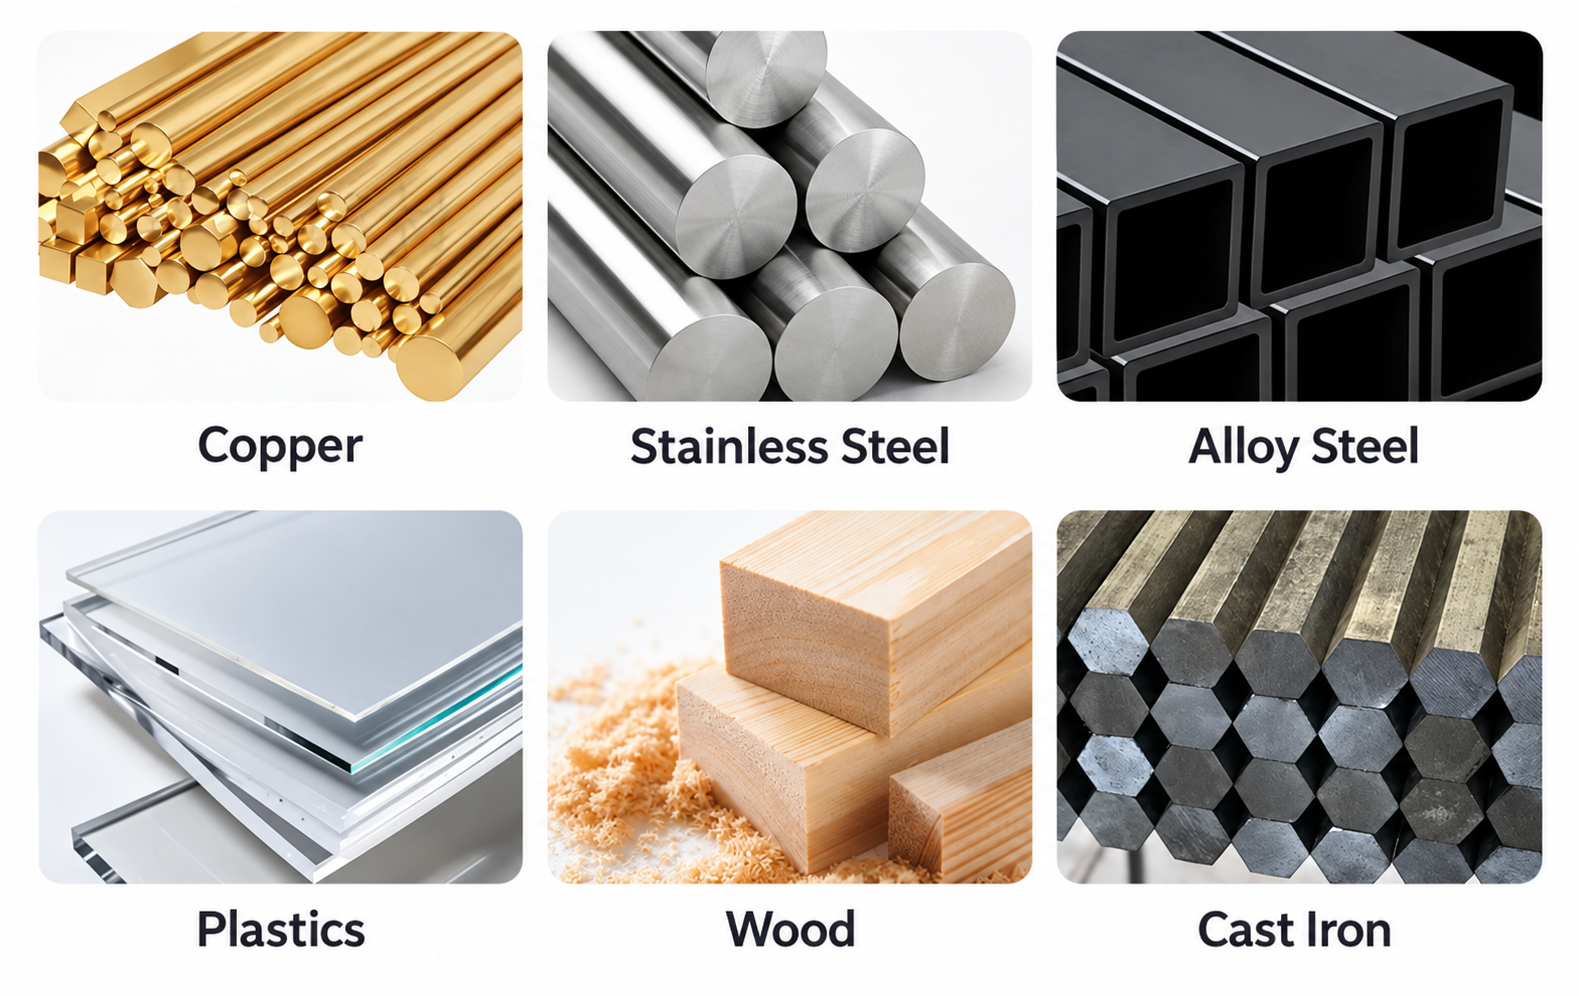
| MATERIAL GROUP | EXAMPLES | APPLICATION LEVEL |
|---|---|---|
| P Steel | Carbon, alloy and prehardened steels up to approximately 48 HRC | Primary application |
| M Stainless Steel | Austenitic and martensitic stainless steels | Primary application |
| K Cast Iron | Gray and selected ductile cast irons | Primary application |
| N Non-Ferrous | Aluminum and copper alloys | Suitable with matched grade / coating |
| S Superalloys & Titanium | Selected heat-resistant alloys and titanium alloys | Application review recommended |
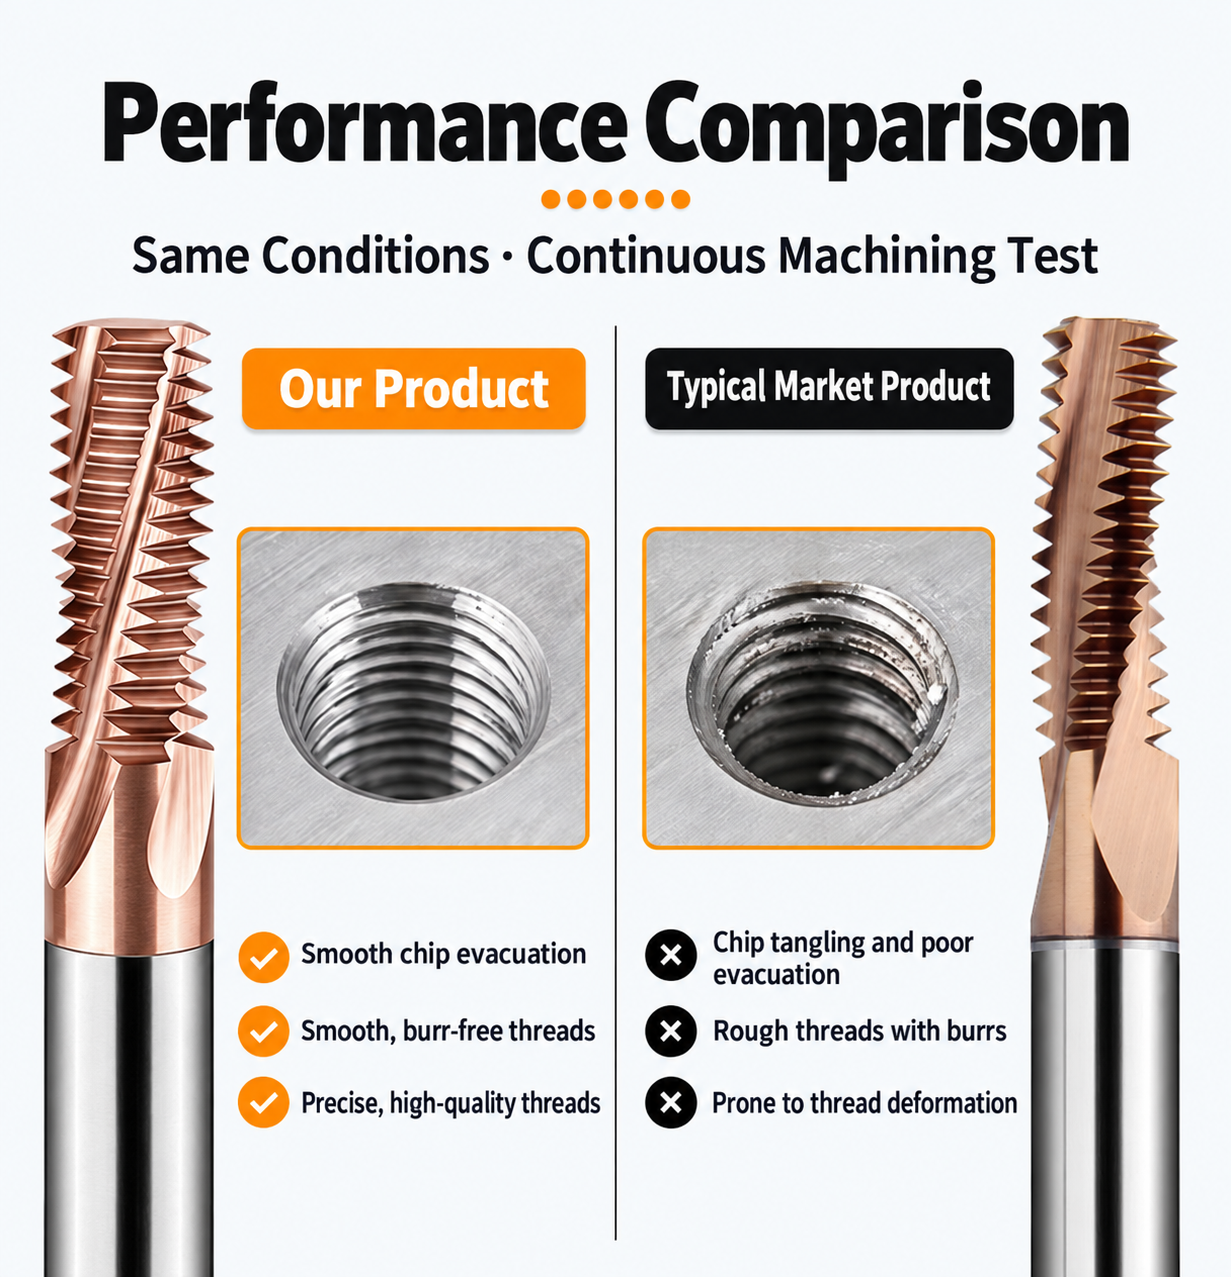
Thread Quality & Chip Evacuation Comparison
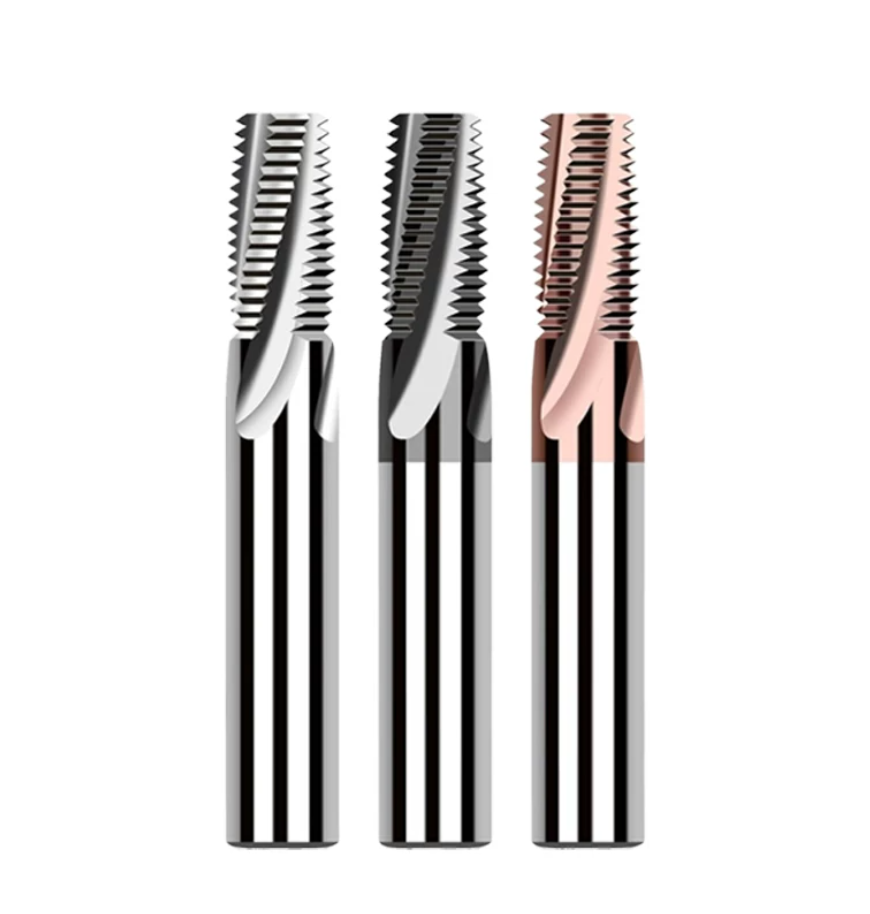
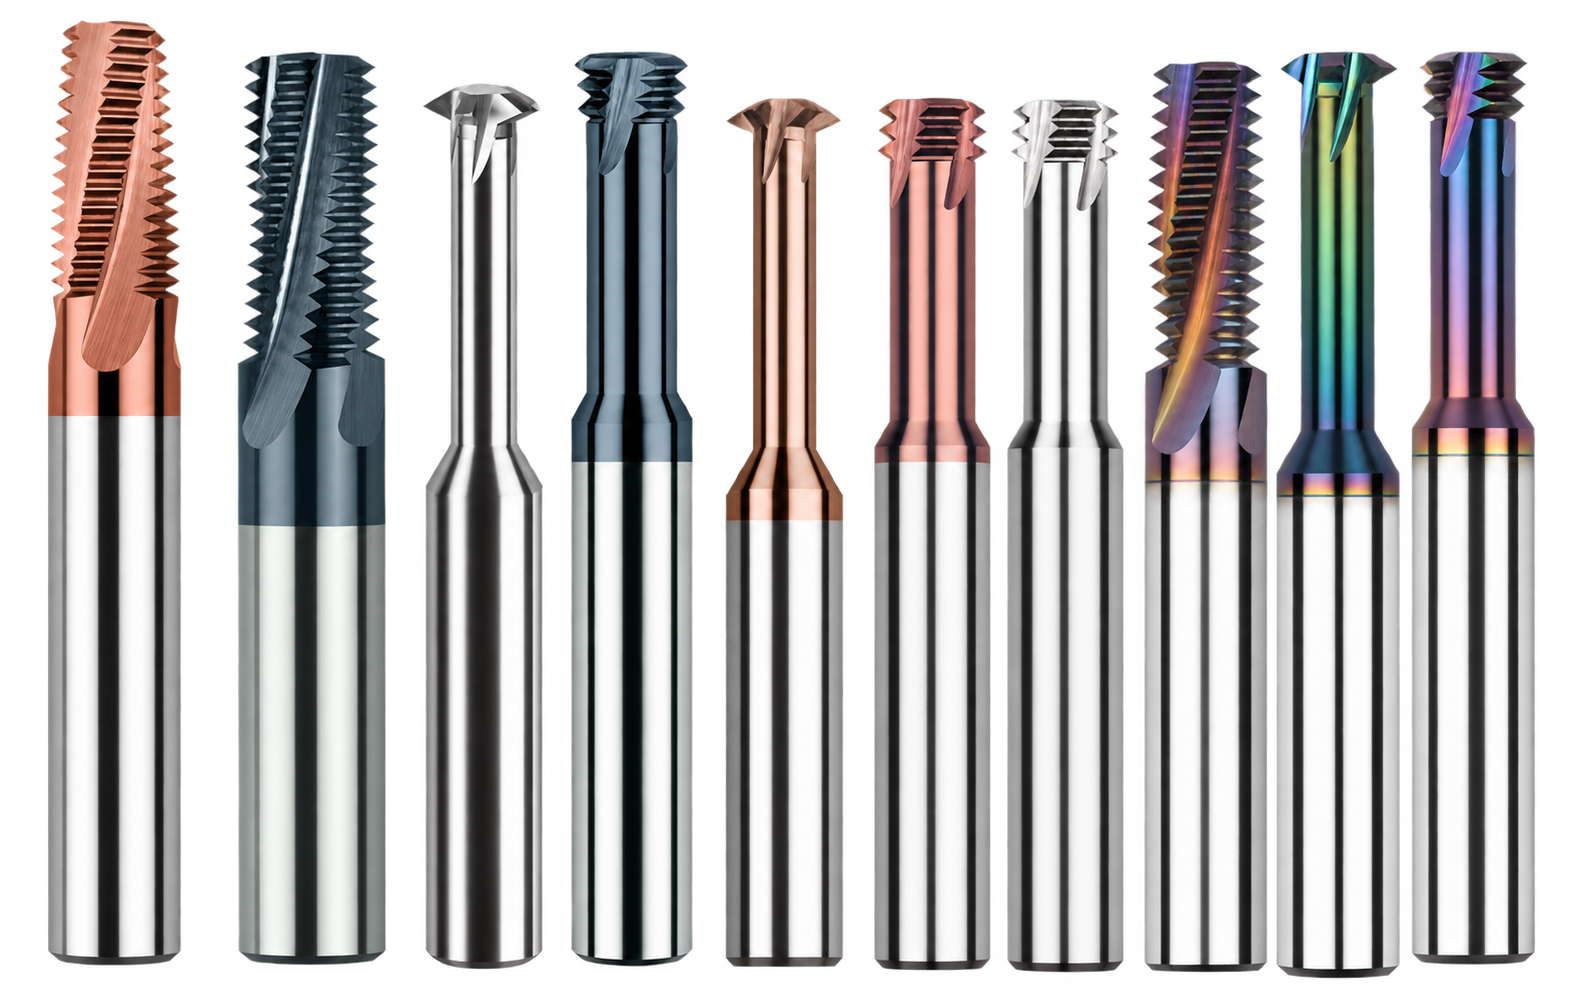
The comparison below illustrates the thread finish and chip-evacuation performance observed during continuous machining under comparable test conditions. Optimized flute geometry and precision-ground full-profile cutting edges support smoother chip evacuation, cleaner thread surfaces and more consistent NPT/NPTF thread formation.
Need help confirming the pipe-thread standard, nominal size or cutter configuration? Read our Thread Mill Selection Guide.
Tool Nomenclature & Dimensions
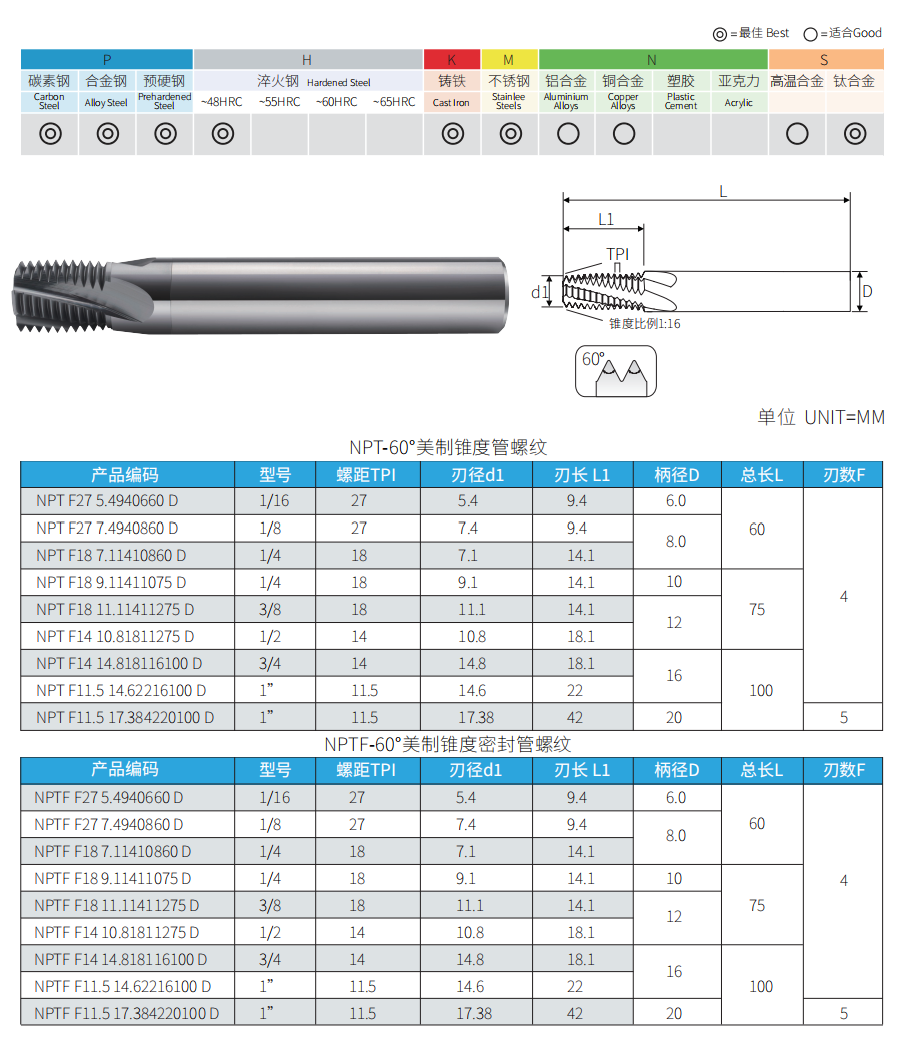
Reference dimensions and standard configurations for NPT and NPTF full-profile solid carbide taper pipe thread mills. All linear dimensions are in millimeters; nominal pipe sizes and TPI follow the specified inch pipe-thread designation.
Technical Configuration
| PARAMETER | SPECIFICATION |
|---|---|
| Tool Material | Fine-Grain Solid Carbide |
| Thread Standards | NPT / NPTF — Select the Dedicated Series |
| Thread Milling Type | Full-Profile Internal Taper Pipe Thread Mill |
| Included Thread Angle | 60° |
| Taper Ratio | 1:16 |
| Nominal Pipe Size | 1/16″–1″ |
| Thread Range | 11.5 / 14 / 18 / 27 TPI |
| Cutter Diameter d1 | Ø5.4–Ø17.38 mm |
| Cutting Length L1 | 9.4–42 mm |
| Shank Diameter D | Ø6 / Ø8 / Ø10 / Ø12 / Ø16 / Ø20 mm |
| Overall Length L | 60 / 75 / 100 mm |
| Flute Count F | 4 Flutes / 5 Flutes According to Size |
| Coating Options | Coated / Uncoated / Application-Specific Coating |
| Primary Materials | Steel / Stainless Steel / Cast Iron / Selected Non-Ferrous and S-Group Materials |
| Custom Options | Thread Standard / Size / d1 / L1 / D / L / Coating / OEM Marking |
Standard NPT & NPTF Size Matrix
NPT and NPTF standard models share the dimensional range shown below but use separate product codes. Confirm the required pipe-thread specification before ordering; the two series should not be selected interchangeably.
| NPT PRODUCT CODE | NPTF PRODUCT CODE | SIZE | TPI | d1 Cutter Dia. | L1 Cutting Length | D Shank Dia. | L Overall Length | F Flutes |
|---|---|---|---|---|---|---|---|---|
| NPT F27 5.4940660 D | NPTF F27 5.4940660 D | 1/16 | 27 | 5.4 | 9.4 | 6 | 60 | 4 |
| NPT F27 7.4940860 D | NPTF F27 7.4940860 D | 1/8 | 27 | 7.4 | 9.4 | 8 | 60 | 4 |
| NPT F18 7.11410860 D | NPTF F18 7.11410860 D | 1/4 | 18 | 7.1 | 14.1 | 8 | 60 | 4 |
| NPT F18 9.11411075 D | NPTF F18 9.11411075 D | 1/4 | 18 | 9.1 | 14.1 | 10 | 75 | 4 |
| NPT F18 11.11411275 D | NPTF F18 11.11411275 D | 3/8 | 18 | 11.1 | 14.1 | 12 | 75 | 4 |
| NPT F14 10.81811275 D | NPTF F14 10.81811275 D | 1/2 | 14 | 10.8 | 18.1 | 12 | 75 | 4 |
| NPT F14 14.818116100 D | NPTF F14 14.818116100 D | 3/4 | 14 | 14.8 | 18.1 | 16 | 100 | 4 |
| NPT F11.5 14.62216100 D | NPTF F11.5 14.62216100 D | 1″ | 11.5 | 14.6 | 22 | 16 | 100 | 4 |
| NPT F11.5 17.384220100 D | NPTF F11.5 17.384220100 D | 1″ | 11.5 | 17.38 | 42 | 20 | 100 | 5 |
Recommended Starting Cutting Parameters
Numeric cutting-speed and feed values are not specified in the source chart. Starting parameters should therefore be confirmed according to cutter diameter d1, workpiece material, coating, thread size, engagement length, machine rigidity and toolholder runout.
| PARAMETER | SELECTION BASIS | STARTING GUIDANCE |
|---|---|---|
| Cutting Speed / Spindle Speed | d1 / material / carbide grade / coating | Confirm by the selected tool size and workpiece material |
| Feed Rate | d1 / TPI / flute count / engagement | Begin conservatively and optimize after gauge-verified test cutting |
| Helical Toolpath | Nominal size / TPI / 1:16 taper | Program a taper-compensated path for the selected NPT or NPTF standard |
| Radial Compensation | Gauge result / wear / required fit | Apply small controlled corrections after inspection |
| Coolant & Chip Control | Material / blind or through hole / chip evacuation | Prevent chip recutting and maintain a clear cutting zone |
NPT & NPTF Thread Mill Application Guidance
- Thread Standard: Confirm whether the drawing specifies NPT or NPTF; use the dedicated tool series and inspection method.
- Nominal Size & TPI: Match both values to the standard size matrix before selecting the cutter.
- Pilot Bore & Cutter Diameter: Verify that d1 clears the prepared bore and that the programmed entry and retract paths are safe.
- Tapered Toolpath: Program the helical interpolation path for the required 1:16 taper rather than using a straight-thread cycle.
- Gauge Verification: Inspect the finished thread with the correct NPT or NPTF gauge and adjust radial compensation in controlled increments.
- Toolholding: Use a clean, low-runout precision holder and the shortest practical setup to maintain profile accuracy.
- Custom Applications: Provide the complete thread callout, component drawing, material and gauge requirement for non-standard reach, coating or geometry.
Thread Mill Selection Resources
Not sure which pipe-thread standard, nominal size or cutter configuration matches the application? Use our selection guide or send the complete thread callout and component drawing for review.
NPT & NPTF Full-Profile Thread Mill Customization
NPT or NPTF thread standard, nominal pipe size, TPI, cutter diameter, cutting length, shank diameter, overall length, flute count, edge preparation and coating can be configured for precision CNC taper-pipe thread milling. Standard models cover 1/16 to 1 inch pipe sizes, 11.5 to 27 TPI, a 60° full-profile form and a 1:16 taper. Non-standard dimensions and application-specific geometry can be reviewed according to the required thread standard, engagement length, workpiece material, machining access and gauging requirement.
| PARAMETER | MANUFACTURING CAPABILITIES |
|---|---|
| Thread Standard | Separate NPT general-purpose and NPTF Dryseal configurations. The required standard must be confirmed from the customer drawing and matching gauge specification before production |
| Pipe Size & TPI | Standard nominal sizes from 1/16 to 1 inch with 27, 18, 14 or 11.5 TPI; special configurations are reviewed against the required NPT or NPTF thread specification |
| Cutter Diameter D1 | Standard cutter diameters from Ø5.4 to Ø17.38 mm, with the diameter selected according to nominal pipe size, pilot-bore clearance, thread engagement and holder access |
| Cutting Length L1 | Standard cutting lengths from 9.4 to 42 mm; custom reach is reviewed according to required thread engagement, workpiece access and the need to limit unnecessary overhang |
| Shank Diameter D | Standard Ø6, Ø8, Ø10, Ø12, Ø16 and Ø20 mm cylindrical shanks, with custom clamping dimensions reviewed according to holder and machine requirements |
| Overall Length L | Standard overall lengths of 60, 75 and 100 mm, with drawing-defined long-reach configurations reviewed for restricted-access taper-pipe threads |
| Flute Count F | Standard 4-flute geometry for most sizes and a 5-flute option for the Ø17.38 mm cutter, selected according to tool diameter, rigidity and chip-space requirements |
| Full-Profile Geometry | Precision-ground 60° full-profile cutting teeth and 1:16 taper geometry are configured for the specified NPT or NPTF thread and CNC helical interpolation strategy |
| Cutting-Edge Preparation | Cutting-edge preparation, rake geometry, relief geometry and core design can be reviewed according to workpiece material, hardness, tool diameter and expected cutting load |
| Coating Selection | Uncoated and application-specific coated configurations are available according to steel, stainless steel, cast iron, aluminum, copper and other confirmed workpiece materials |
| Thread Milling Application | Configurations are intended for internal NPT or NPTF taper-pipe threads in through or blind-hole CNC applications, subject to sufficient bottom clearance and chip evacuation |
| Dimensional Tolerance | Drawing-defined requirements for 60° profile geometry, 1:16 taper, TPI, D1, L1, D, L, shank accuracy, runout and other critical features can be reviewed before production |
خدمات OEM و برند خصوصی
OEM manufacturing and private-label supply options are available for cutting-tool distributors, tooling brands and repeat-production customers. Laser identification, NPT/NPTF tool codes, nominal size, TPI, custom labels, protective packaging and coating presentation can be configured according to the approved taper-pipe thread mill specification.

Laser Etching
Custom logos, NPT or NPTF identification, nominal pipe size, TPI, tool code, coating reference and batch number can be laser marked according to the available shank area.
Custom Labels & Packaging
Individual protective tubes, standard-specific labels, nominal-size and TPI identification, colored tubes and private-label packaging can be reviewed for distributor and OEM programs.
Commercial Terms
MOQ, standard-size samples, custom tool trials, repeat orders and scheduled supply programs are confirmed according to the NPT/NPTF standard, nominal size, TPI, dimensions, coating and packaging requirements.
Technical Workflow
A structured review process is used to prevent NPT/NPTF mix-ups and confirm standard, customized and private-label full-profile taper-pipe thread mill requirements before production.
Inquiry
Submit NPT or NPTF, nominal pipe size, TPI, engagement length, pilot bore, material, gauge requirement and quantity.
Engineering
Review the 60° profile, 1:16 taper, TPI, D1, L1, D and L dimensions, flute count, carbide grade, coating and CNC path requirements.
Commercial
Confirm quotation, MOQ, sample requirements, custom-tool conditions, production schedule and delivery terms.
Production
Carbide blank preparation, CNC flute grinding, full-profile tooth and taper grinding, edge preparation, coating and standard-specific laser marking.
Quality Control
Inspect NPT/NPTF identification, TPI, 60° profile, 1:16 taper, D1, L1, D, L, flute count, runout, cutting edges and coating condition.
Quality, Inspection & Delivery
Our solid carbide NPT and NPTF full-profile thread mills are controlled through carbide material verification, precision CNC grinding, in-process measurement and final inspection. NPT/NPTF identification, TPI, 60° thread profile, 1:16 taper geometry, cutter diameter, cutting length, shank dimensions, flute count, runout, cutting-edge condition and coating appearance are reviewed against the approved specification or custom drawing before packing.
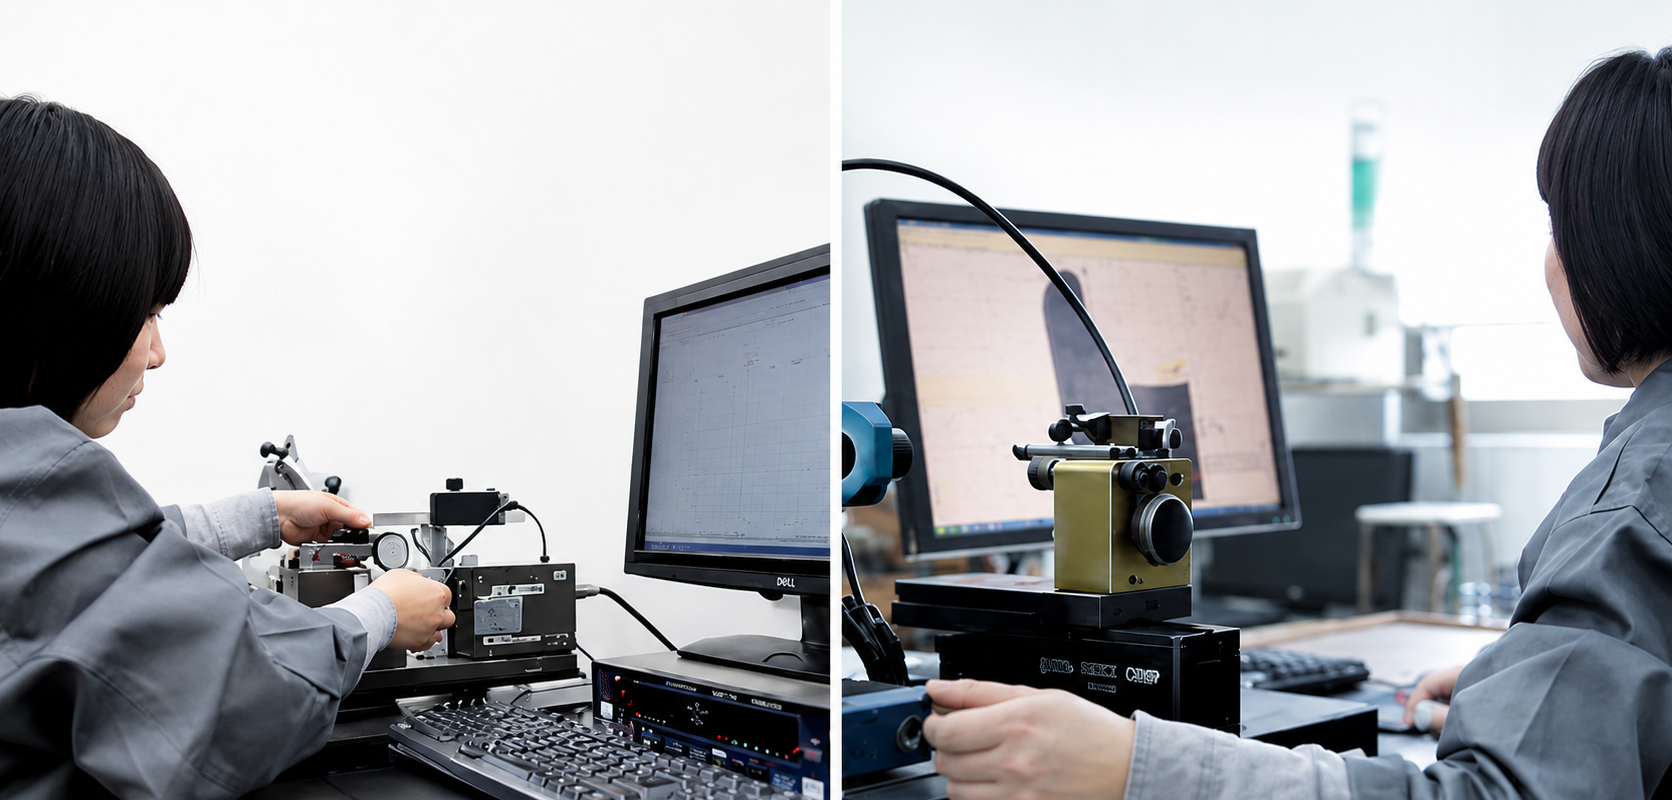
Three-Stage Quality Control
Inspection checkpoints are arranged throughout production to support dimensional consistency, correct NPT/NPTF separation, taper-profile accuracy and repeat-order control.
Incoming Material Control
Carbide substrate grade, blank diameter, blank length and supplied material information are checked against the confirmed NPT or NPTF full-profile thread mill production requirement.
In-Process Grinding Control
TPI-related tooth geometry, 60° profile, 1:16 taper, cutter diameter d1, cutting length L1, flute configuration and shank diameter D are monitored during precision CNC grinding.
Final Tool Inspection
Finished tools are reviewed for NPT/NPTF identification, nominal size, TPI, full-profile and taper geometry, specified dimensions, radial runout, cutting edges, coating, laser marking and packing labels.
Key Inspection Characteristics
Inspection requirements are confirmed according to the selected NPT or NPTF tool specification, standard size matrix, matching gauge requirement or approved custom drawing.
| INSPECTION ITEM | CONTROL FOCUS | CONFIRMATION BASIS |
|---|---|---|
| Thread Standard & TPI | Correct NPT or NPTF identification and 11.5 / 14 / 18 / 27 TPI tooth spacing | Approved product code, nominal pipe size and order specification |
| Cutter Diameter (d1) | Cutting-section diameter and dimensional consistency | Standard size matrix or approved drawing |
| Cutting Length (L1) | Full-profile cutting length and usable thread engagement | Standard size matrix, required engagement or approved drawing |
| Shank Diameter (D) | Clamping-section diameter and surface condition | Applicable standard or custom shank specification |
| Overall Length (L) | Total tool length and configuration consistency | Standard size matrix or approved drawing |
| Flute Count (F) | 4-flute or 5-flute configuration and tooth-to-tooth grinding consistency | Selected standard or custom tool configuration |
| 60° Profile & 1:16 Taper | Included thread angle, full-profile tooth form, taper direction and taper consistency | Selected NPT/NPTF configuration and approved manufacturing specification |
| Radial Runout | Concentricity between cutting section and shank | Agreed inspection requirement or approved drawing |
| Cutting Edge & Coating | Edge condition, visible defects, coating coverage and surface appearance | Application-specific carbide, edge-preparation and coating requirement |
| Marking & Identification | NPT/NPTF designation, nominal pipe size, TPI, tool code and batch information | Confirmed order and OEM packaging specification |
Measurement & Batch Traceability
Optical measuring systems, tool inspection equipment and appropriate dimensional gauges are selected according to the NPT/NPTF cutting profile and dimensional feature being checked.
Optical Measurement
Profile and dimensional review of the 60° full-profile teeth, 1:16 taper geometry and specified tool dimensions.
Runout Verification
Concentricity between the full-profile cutting section and precision shank is reviewed according to the agreed requirement.
Cutting-Edge Inspection
Magnified inspection checks cutting edges, profile surfaces, relief areas and visible grinding defects.
Batch Identification
NPT/NPTF designation, nominal size, TPI, product code, order and batch information are linked where required for repeat supply.
Protective Packaging Process
Finished NPT and NPTF thread mills are individually protected to reduce contact with precision-ground full-profile teeth while keeping the two standards, nominal sizes, TPI values and batch identities clearly separated during storage and transportation.

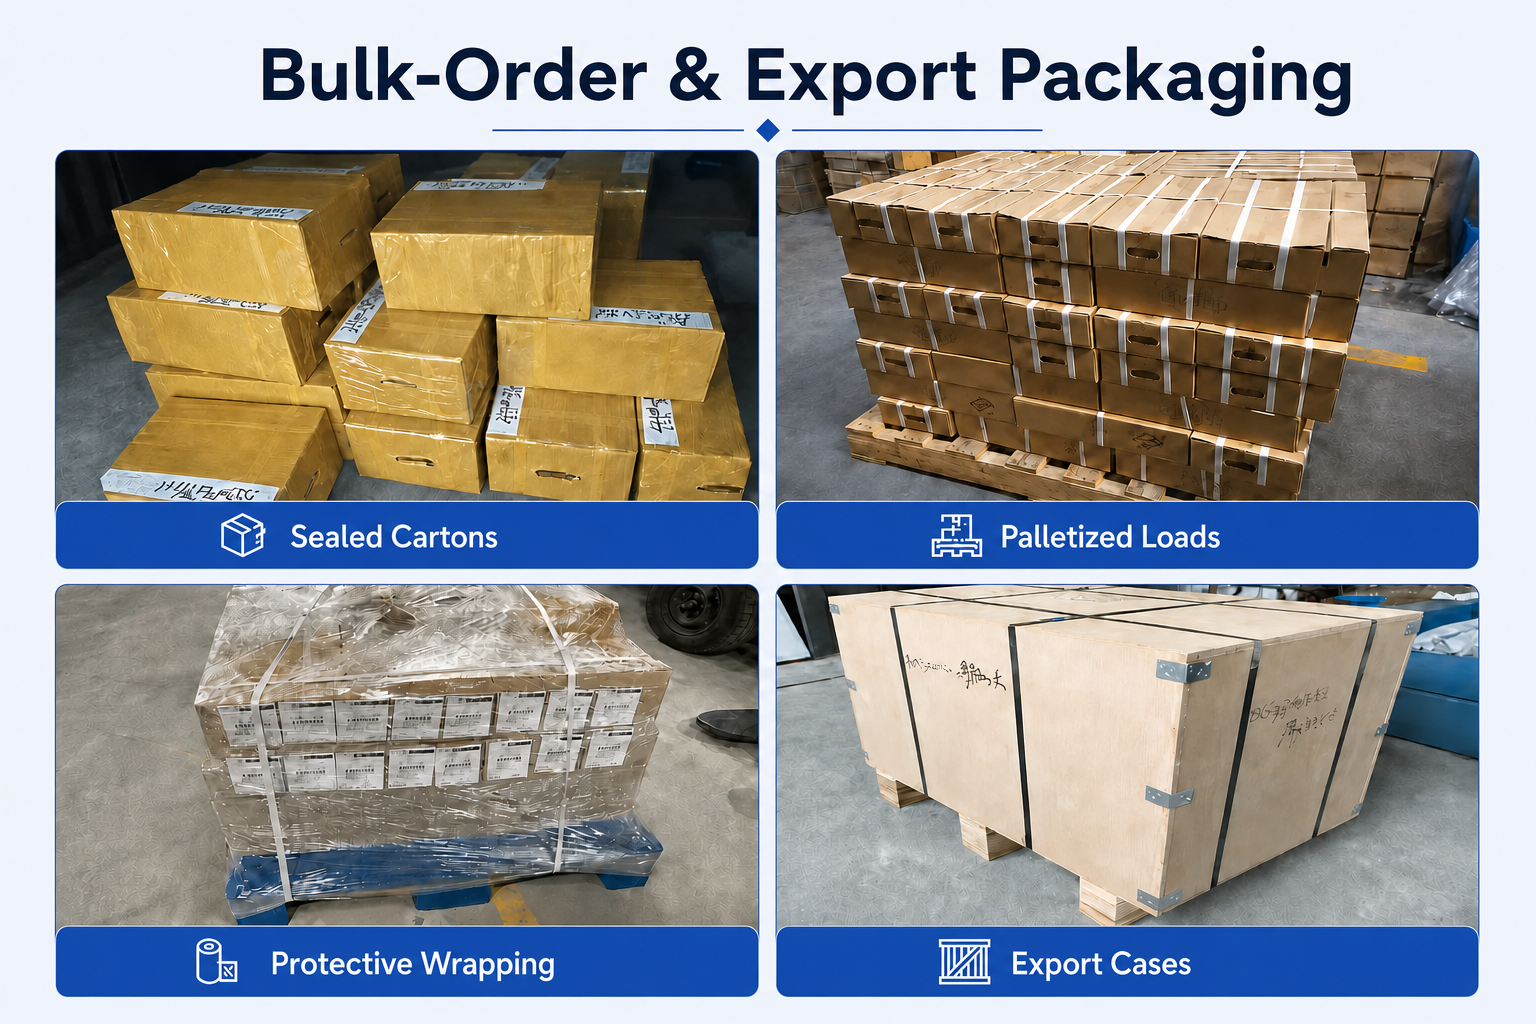
Bulk-Order & Export Packaging
Bulk orders of standard and custom NPT/NPTF full-profile thread mills can be arranged with separated model labeling, reinforced cartons, protective wrapping, palletized loading or export cases according to order quantity and transportation requirements.

Delivery Coordination
Production completion, NPT/NPTF identification, inspection status, packing method and dispatch arrangements are confirmed against the approved order. In-stock standard sizes can normally be prepared for shipment within 1–3 days. Custom-tool lead time is confirmed after the thread standard, nominal size, TPI, dimensions, coating, quantity, gauge requirement and packaging are approved. Courier, air, sea or customer-designated shipping options can be reviewed according to shipment size and destination.
FAQ & Downloads
Review common selection, application and ordering questions for solid carbide NPT and NPTF full-profile thread mills used for CNC internal taper-pipe threading, including the difference between the two standards, nominal pipe size and TPI selection, pilot-hole preparation, tool dimensions, gauging and customization options.
Product & Application FAQs
Selection and application guidance for precision CNC thread milling.
What is an NPT/NPTF full-profile thread mill?
It is a solid carbide CNC tool with multiple precision-ground teeth that generate a 60° internal taper-pipe thread by helical interpolation. The tool geometry follows a 1:16 taper and produces the complete thread profile over its cutting length. This series is intended for NPT general-purpose or NPTF Dryseal internal threads where thread size, taper and gauge position must be controlled through the tool path and machining setup.
What is the difference between NPT and NPTF, and can the same tool be used?
NPT is a general-purpose 60° tapered pipe thread that normally relies on a sealing compound, while NPTF is a Dryseal thread designed with different crest-and-root relationships to promote metal-to-metal sealing. They are related standards but should not be treated as interchangeable. Select the tool code specifically marked NPT or NPTF and confirm the customer drawing and matching gauge requirement before machining.
How do I select the correct nominal size, TPI, d1 and L1?
Start with the specified NPT or NPTF nominal pipe size and its required TPI: 27, 18, 14 or 11.5 TPI in this range. Then select a standard model whose cutter diameter d1 clears the prepared pilot hole and whose cutting length L1 covers the required thread engagement. Use the shortest suitable reach to maintain rigidity, and confirm shank diameter D, overall length L, holder access and bottom clearance before programming.
Can these full-profile pipe thread mills be used in blind holes?
Yes, provided the pilot hole is deep enough for the full cutting length, entry movement and required bottom clearance. The programmed helical path must reproduce the 1:16 taper without allowing the tool or shank to contact the hole bottom or wall. For blind holes, confirm usable hole depth, thread engagement, chip evacuation and coolant access before selecting L1 and setting the tool path.
What materials can this solid carbide thread mill machine?
The standard series is primarily suited to carbon steel, alloy steel, prehardened steel, cast iron, stainless steel and titanium, with suitable configurations also available for aluminum, copper and selected high-temperature alloys. Carbide grade, coating and starting cutting data should be matched to the material, hardness, nominal pipe size, TPI, thread engagement, tool overhang and machine rigidity.
How should the finished NPT or NPTF thread be checked?
Use the correct gauge for the specified standard—an NPT gauge for NPT threads and the required NPTF Dryseal gauge for NPTF threads. Check the first machined part for gauge position, taper engagement and thread condition, then make small CNC tool-path adjustments if necessary. A visually acceptable thread is not sufficient evidence of conformance, and an NPT gauge should not be substituted for an NPTF inspection requirement.
Ordering & Customization FAQs
Information for distributors, tooling brands and customers sourcing standard or custom solid carbide thread mills.
What standard NPT and NPTF full-profile thread mill sizes are available?
Separate NPT and NPTF model ranges cover 1/16, 1/8, 1/4, 3/8, 1/2, 3/4 and 1 inch nominal pipe sizes with 27, 18, 14 and 11.5 TPI. Standard cutter diameters d1 are Ø5.4–Ø17.38 mm, cutting lengths L1 are 9.4–42 mm, shanks D are Ø6–Ø20 mm, and overall lengths L are 60, 75 or 100 mm. Most models have four flutes; the Ø17.38 mm model has five.
Can you manufacture custom NPT or NPTF thread mills?
Yes. Custom nominal sizes, TPI, cutter diameter d1, cutting length L1, shank diameter D, overall length L, flute configuration, carbide grade, edge preparation and coating can be reviewed. Please provide NPT or NPTF, the pipe-thread drawing, gauge requirement, engagement length, pilot-bore information, workpiece material, machine conditions and order quantity.
Are OEM marking, custom coatings and private-label packaging available for thread mills?
Yes. Laser marking can include the customer logo, NPT or NPTF designation, nominal pipe size, TPI, tool code and batch number. Custom labels, protective tubes, coating identification and private-label packaging can also be reviewed for distributor and OEM programs.
What is the lead time for standard and custom solid carbide thread mills?
In-stock standard NPT/NPTF models can normally be prepared for shipment within 1–3 working days. Custom tools require confirmation of the thread standard, nominal size, TPI, drawing, gauge requirement, dimensions, carbide grade, coating, quantity and packaging before the production lead time is confirmed.
Technical Downloads
Access general carbide tooling references for product selection and CNC machining parameter review.
Solid Carbide Thread Mills Catalog
Thread-mill families, thread standards, configurations, dimensional ranges and application references.
Carbide Tool Speeds & Feeds Guide
General starting cutting-data references and adjustment guidance for carbide tooling applications.
NPT/NPTF thread-milling data should be confirmed according to cutter diameter, nominal pipe size, TPI, engagement length, workpiece material and hardness, coating, tool overhang, holder runout and machine rigidity. Verify the first completed thread with the correct matching gauge before batch production.
Related Guides & Thread Mill Resources
Explore practical thread-milling selection guides and related solid carbide thread mill series for different thread standards, materials and machining requirements.
Selection guidance for thread standards, pitch, tool style, diameter, depth and workpiece material.
Compare flexibility, thread size range, breakage risk and typical machining applications.
Browse metric, inch, UNC/UNF, NPT/NPTF, single-form, full-profile and material-specific thread mill series.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.