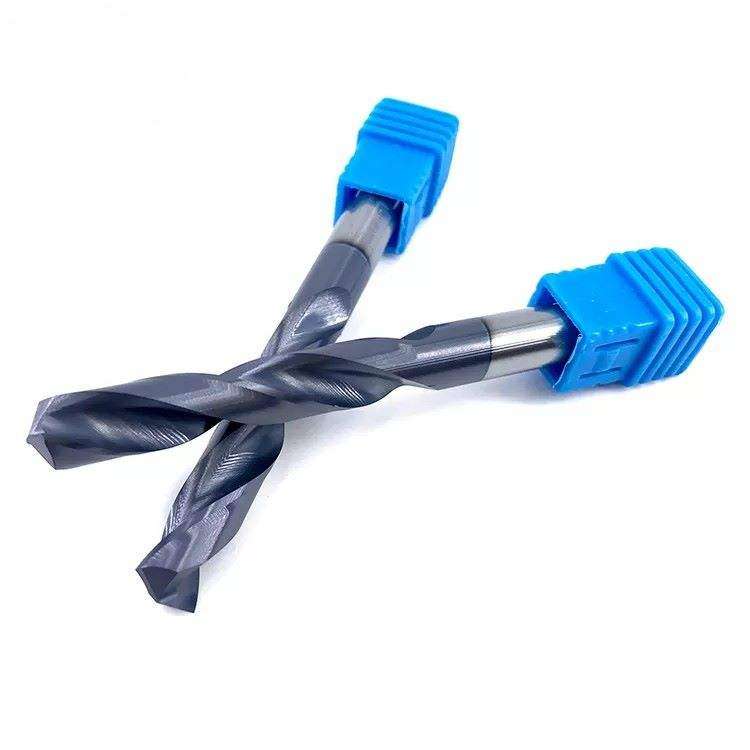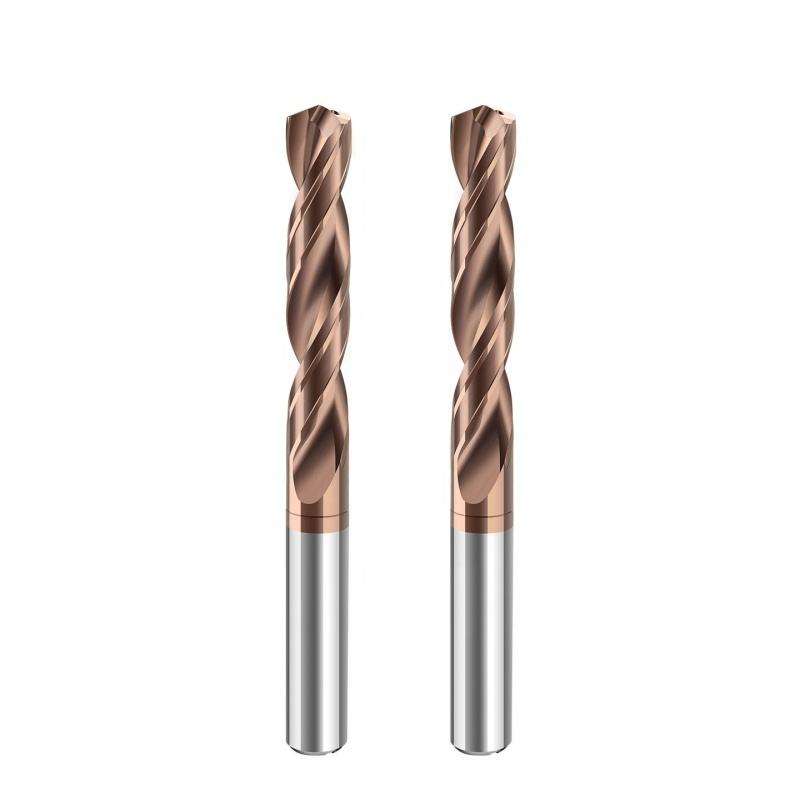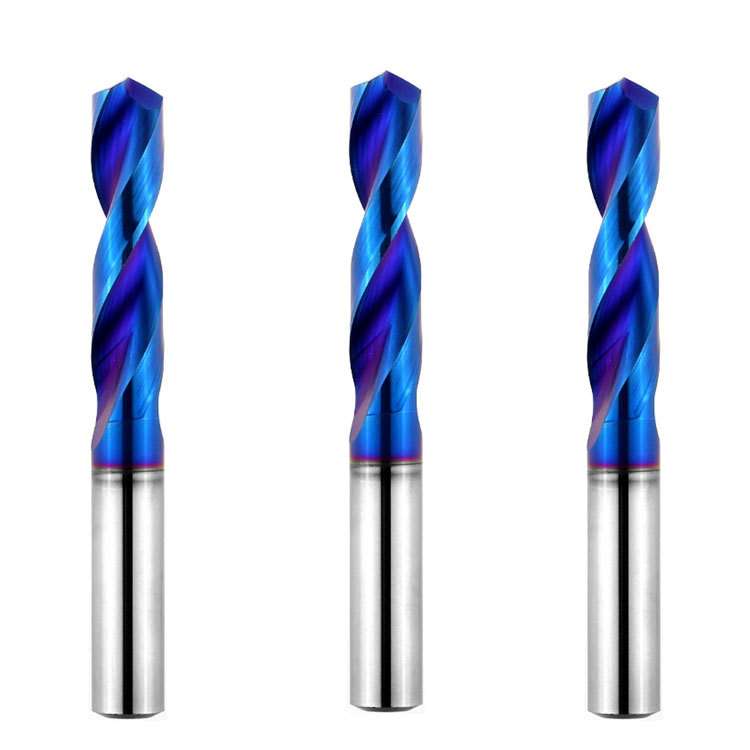
HRC65 2-Flute Solid Carbide Twist Drill for Stainless Steel
Tutarlı Kalite
Tekrarlanan siparişlerde tutarlı geometri.
Esnek Siparişler
Küçük partiler ve farklı boyutlarda seçenekler mevcuttur.
OEM Desteği
Özel işaretleme, etiketler ve ambalajlama.
Standart ve Özel
Standart boyutlar ve özel konfigürasyonlar.
HRC65 Carbide Twist Drill Overview
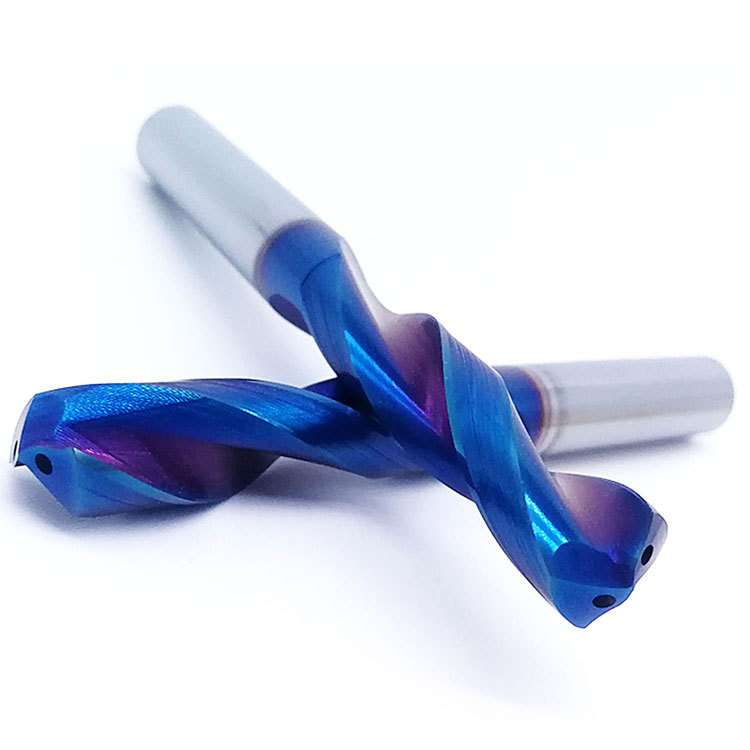
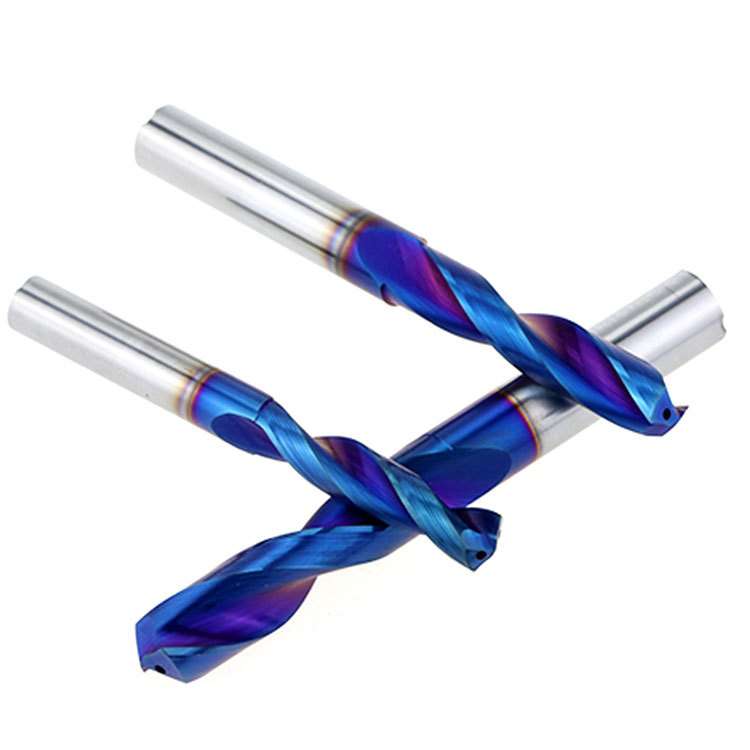
This 2-flute solid carbide twist drill is configured for precision CNC drilling in stainless steel, including selected hardened conditions after application confirmation. Reinforced cutting edges, controlled chip-forming geometry and a nano blue wear-resistant coating support heat control, edge stability and consistent hole production under rigid machining conditions. Standard 3×D, 5×D and 8×D sizes are available, while diameter, length, edge preparation, coating, coolant channels, marking and packaging can be reviewed for custom or OEM requirements.
Key Configuration
Stainless-Steel Point Geometry
Application-specific point and edge preparation maintain cutting action and help limit rubbing in demanding stainless-steel conditions.
Reinforced Two-Flute Edge
Two reinforced cutting edges balance usable sharpness with resistance to chipping and high cutting loads.
External or Through Coolant
Coolant configuration can be selected according to diameter, drilling depth, chip evacuation and machine capability.
Key Product Advantages
Controlled Chip Formation
The two-flute profile provides chip space and supports consistent evacuation of long stainless-steel chips.
Heat-Resistant Coating
Nano blue coating supports heat and wear resistance during demanding stainless-steel drilling cycles.
Fine-Grain Carbide Substrate
The carbide substrate provides rigidity and edge support for repeatable CNC hole production.
Flexible Depth Configurations
Standard 3×D, 5×D and 8×D series cover short, medium-depth and deeper drilling requirements.
Stainless Steel & Hardness Compatibility
HRC65 is an upper application target for selected confirmed conditions, not a universal setting for every stainless steel grade.
Applications & Target Scope
- Stainless-steel valve, pump and fitting components
- Food-processing and chemical-equipment components
- Medical and marine stainless-steel parts
- Housings and precision mechanical components
- Selected hardened stainless-steel applications after technical confirmation
Product & Cutting-Edge Details
Tool Nomenclature & Dimensions
Standard dimensional parameters and technical nomenclature for HRC65 2-flute solid carbide twist drills for stainless steel.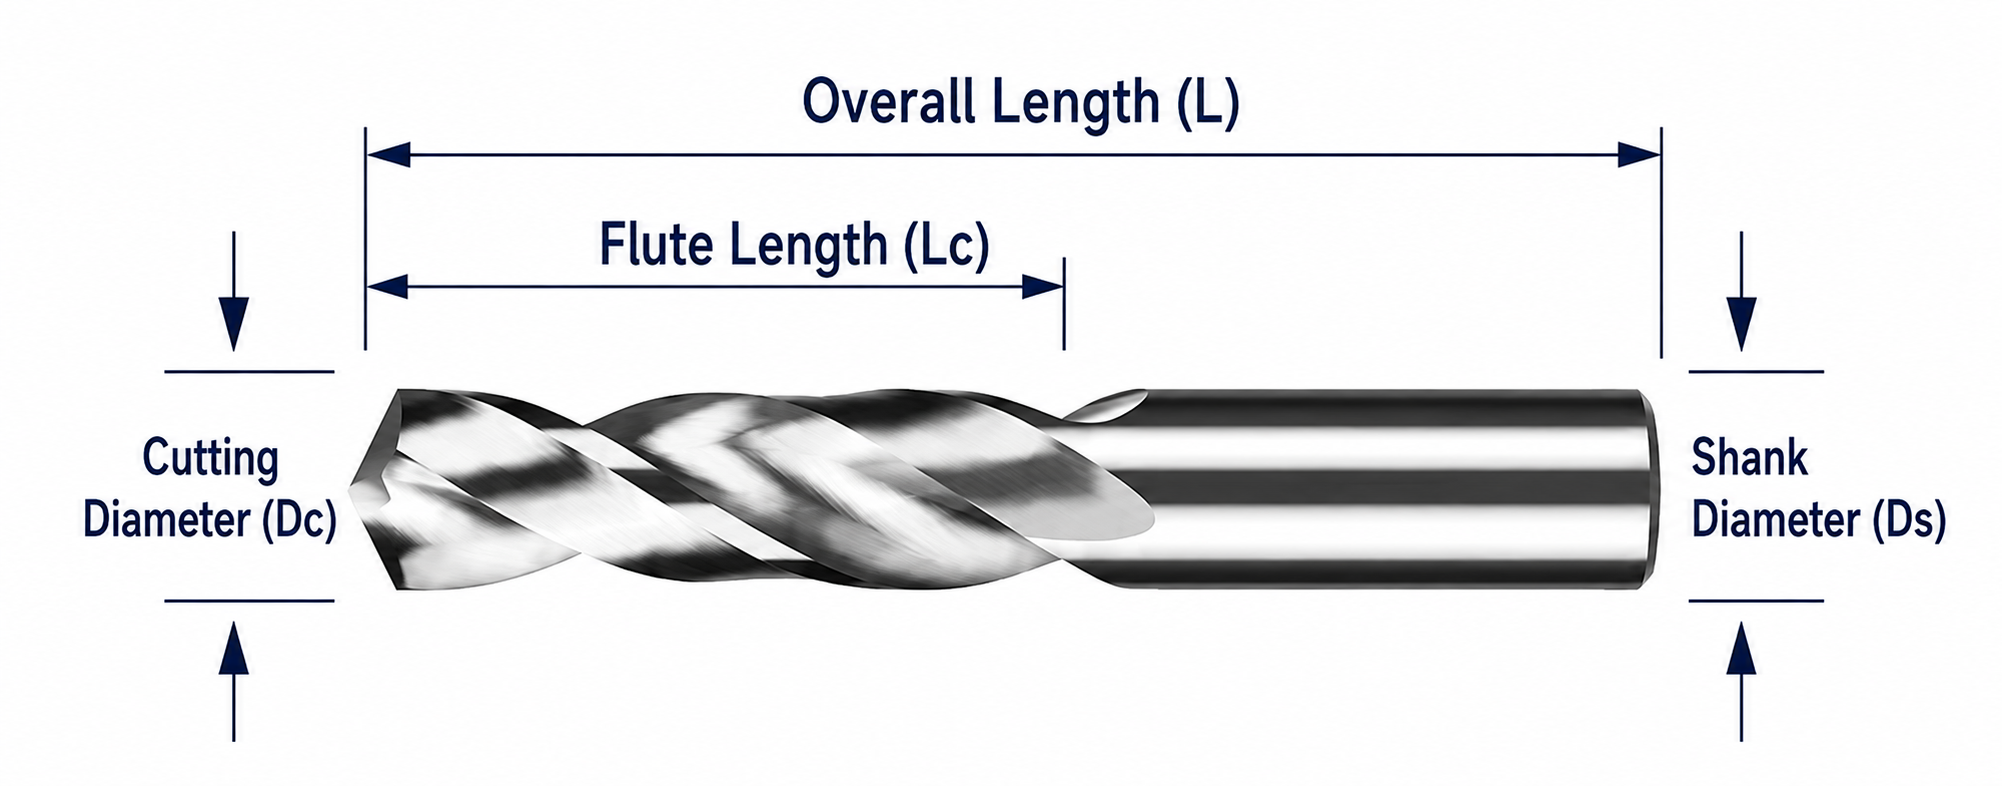
Technical Configuration
Standard construction and available configuration details for this stainless-steel drill series.
Standard Size Matrix
Reference 3×D, 5×D and 8×D configurations. D is cutting diameter, L1 is flute length and L is overall length. Dimensions are in millimetres.
| d1 | 3D L1 | 3D L | 5D L1 | 5D L | 8D L1 | 8D L |
|---|---|---|---|---|---|---|
| 3 | 20 | 62 | 28 | 66 | 30 | 70 |
| 4 | 24 | 66 | 36 | 74 | 42 | 83 |
| 5 | 28 | 66 | 44 | 82 | 50 | 90 |
| 6 | 28 | 66 | 44 | 82 | 57 | 97 |
| 7 | 34 | 79 | 53 | 91 | 76 | 116 |
| 8 | 41 | 79 | 53 | 91 | 76 | 116 |
| 9 | 47 | 89 | 61 | 103 | 87 | 131 |
| 10 | 47 | 89 | 61 | 103 | 95 | 139 |
| 11 | 55 | 102 | 71 | 118 | 106 | 155 |
| 12 | 55 | 102 | 71 | 118 | 114 | 163 |
| 13 | 60 | 107 | 77 | 124 | 133 | 182 |
| 14 | 60 | 107 | 77 | 124 | 133 | 182 |
| 15 | 65 | 115 | 83 | 133 | 152 | 204 |
| 16 | 65 | 115 | 83 | 133 | 152 | 204 |
| 17 | 73 | 123 | 93 | 143 | 171 | 223 |
| 18 | 73 | 123 | 93 | 143 | 171 | 223 |
| 19 | 79 | 133 | 101 | 153 | 190 | 244 |
| 20 | 79 | 133 | 101 | 153 | 190 | 244 |
L1 is the flute length, not the maximum blind-hole depth. Through coolant is preferred for deeper 5D and 8D holes.
Stainless-Steel Drilling Guidance
Reduce cutting speed as hardness rises and maintain a stable, non-rubbing feed. Final data depend on grade, heat treatment, diameter, depth, coolant and rigidity.
| Malzeme | Main Challenge | Parameter Strategy | Soğutma sıvısı |
|---|---|---|---|
| 304 / 304L | Work hardening, adhesion, long chips | Use continuous feed; avoid rubbing and dwell | External coolant for shallow holes; through coolant for deeper holes |
| 316 / 316L | Adhesion, heat, work hardening | Use conservative speed and stable feed | Reliable coolant and chip evacuation |
| 410 / 420 / 430 | Hardness and edge load vary by condition | Reduce speed as hardness increases; maintain stable feed | Through coolant preferred for deeper holes |
| 17-4PH / 15-5PH | Load varies by H condition | Confirm heat-treatment state | Stable coolant and rigid holding |
| Duplex 2205 / Super Duplex | High force, heat and difficult chips | Use rigid setup and conservative conditions | Through coolant strongly recommended |
Recommended Starting Cutting Parameters
General starting values and detailed application parameters are available in our technical guide.
Solid Carbide Drill Cutting Data Guide
Access starting speeds and feeds for stainless-steel product selection and application trials.
Drilling Product Family Overview
Select the matching series according to drilling depth and stainless-steel application conditions.
HY-SS-3D Series
Short Drilling
HY-SS-5D Series
Medium-Depth Drilling
HY-HRC65 Series
Current Series
HY-SS-8D Series
Deep-Hole Drilling
For additional sizes and related drill series, View the Solid Carbide Drill Catalog. Custom dimensions can be reviewed according to your drawing or application requirements.
HRC65 Stainless Steel Drill Customization
Cutting diameter, flute length, reinforced point geometry, chip-space design, edge preparation and coating can be configured for selected stainless-steel applications. Work hardening, heat, chip evacuation and actual material hardness are reviewed before production.
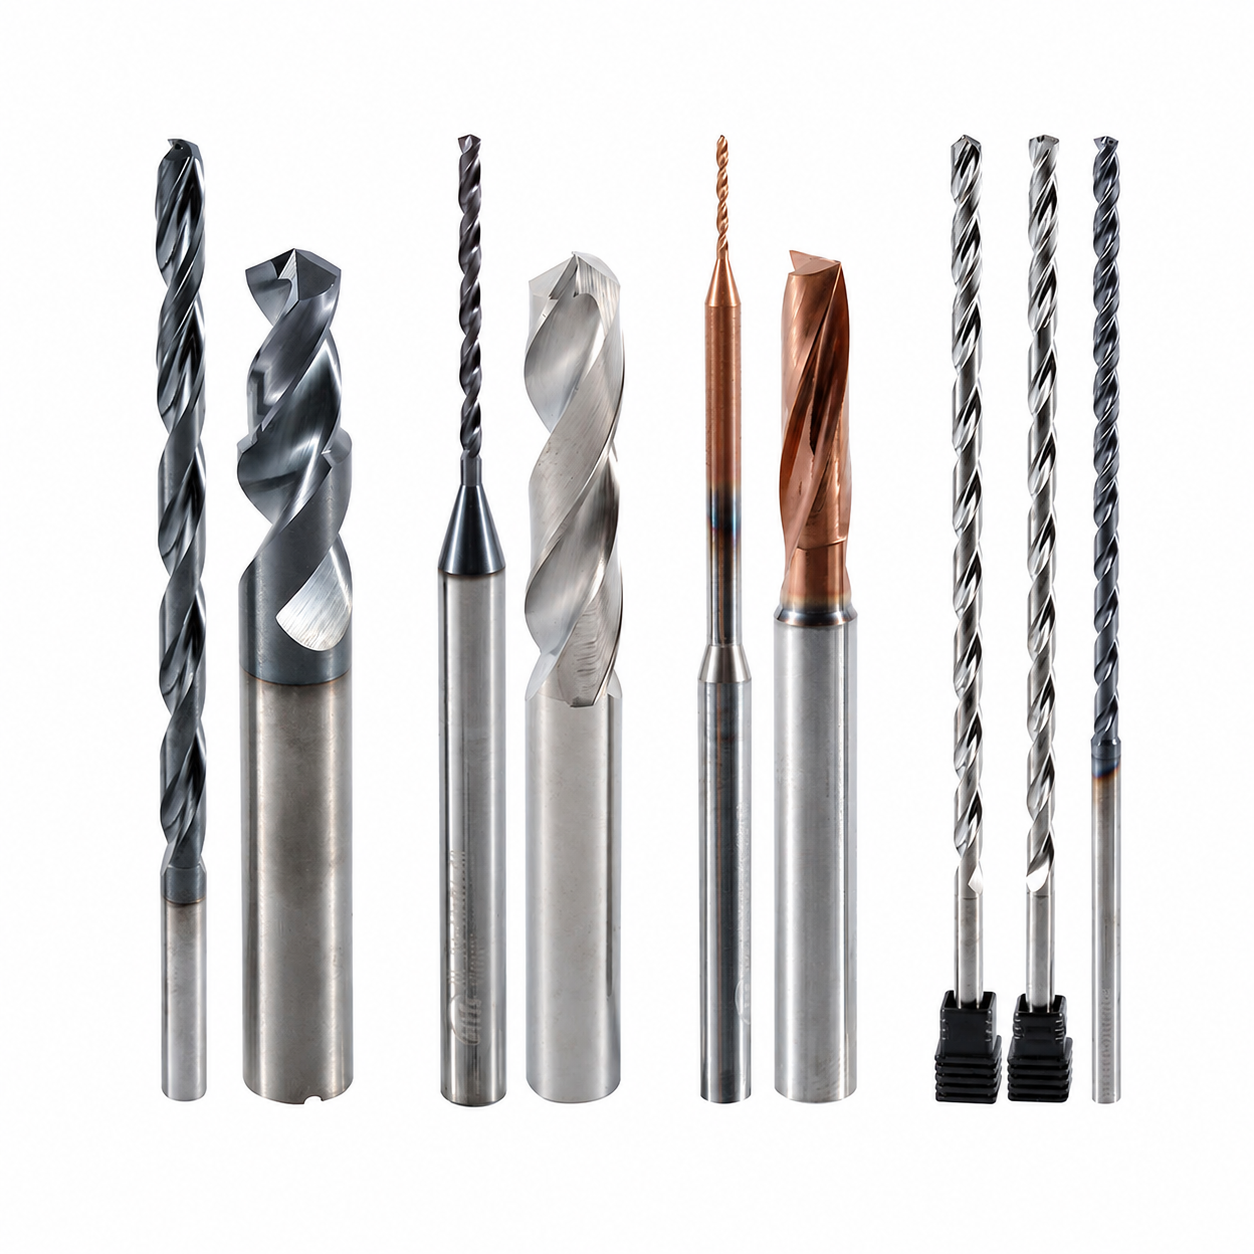
Stainless Steel Geometry & Edge Preparation
Point geometry, web thinning, flute space and edge preparation can be configured to manage work hardening, cutting load and chip evacuation while preserving micro-edge strength.

Diameter & Length Options
Metric and drawing-defined diameters can be configured with application-matched flute, reach, shank and overall dimensions.
OEM ve Özel Etiket Hizmetleri
OEM manufacturing and private-label supply options for stainless-steel manufacturers, specialty-tool distributors and confirmed hard-material customers.
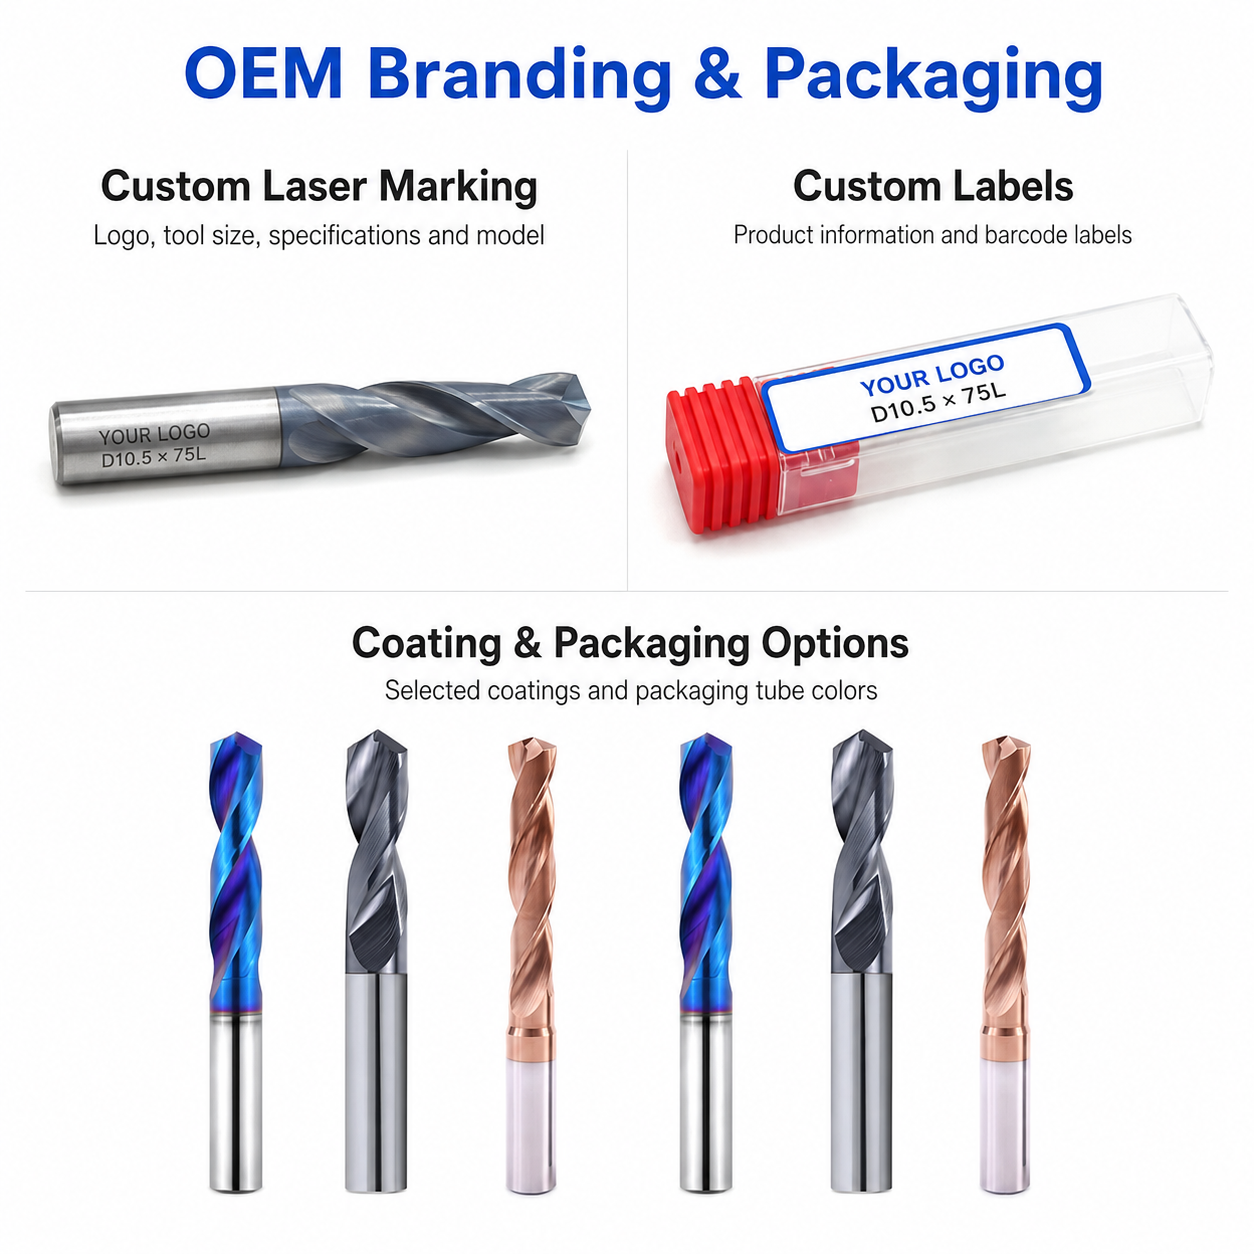
Lazer Kazıma
Custom laser marking for logos, tool codes, diameter specifications, coating identification and batch numbers.
Custom Packaging
Individual protective tubes, diameter labels, multi-pack boxes, custom inserts and private-label packaging options.
Ticari Şartlar
Flexible MOQ options for standard configurations, custom sizes, trial orders and scheduled repeat supply.
Teknik İş Akışı
Sorgulama
Submit the stainless grade, hardness, hole dimensions, coolant and quantity.
Mühendislik
Work-hardening risk, geometry, edge preparation, coating and coolant are reviewed.
Ticari
Quotation, MOQ, production schedule and delivery terms are confirmed.
Üretim
Precision grinding, edge preparation, PVD coating and tool identification.
Kalite Kontrolü
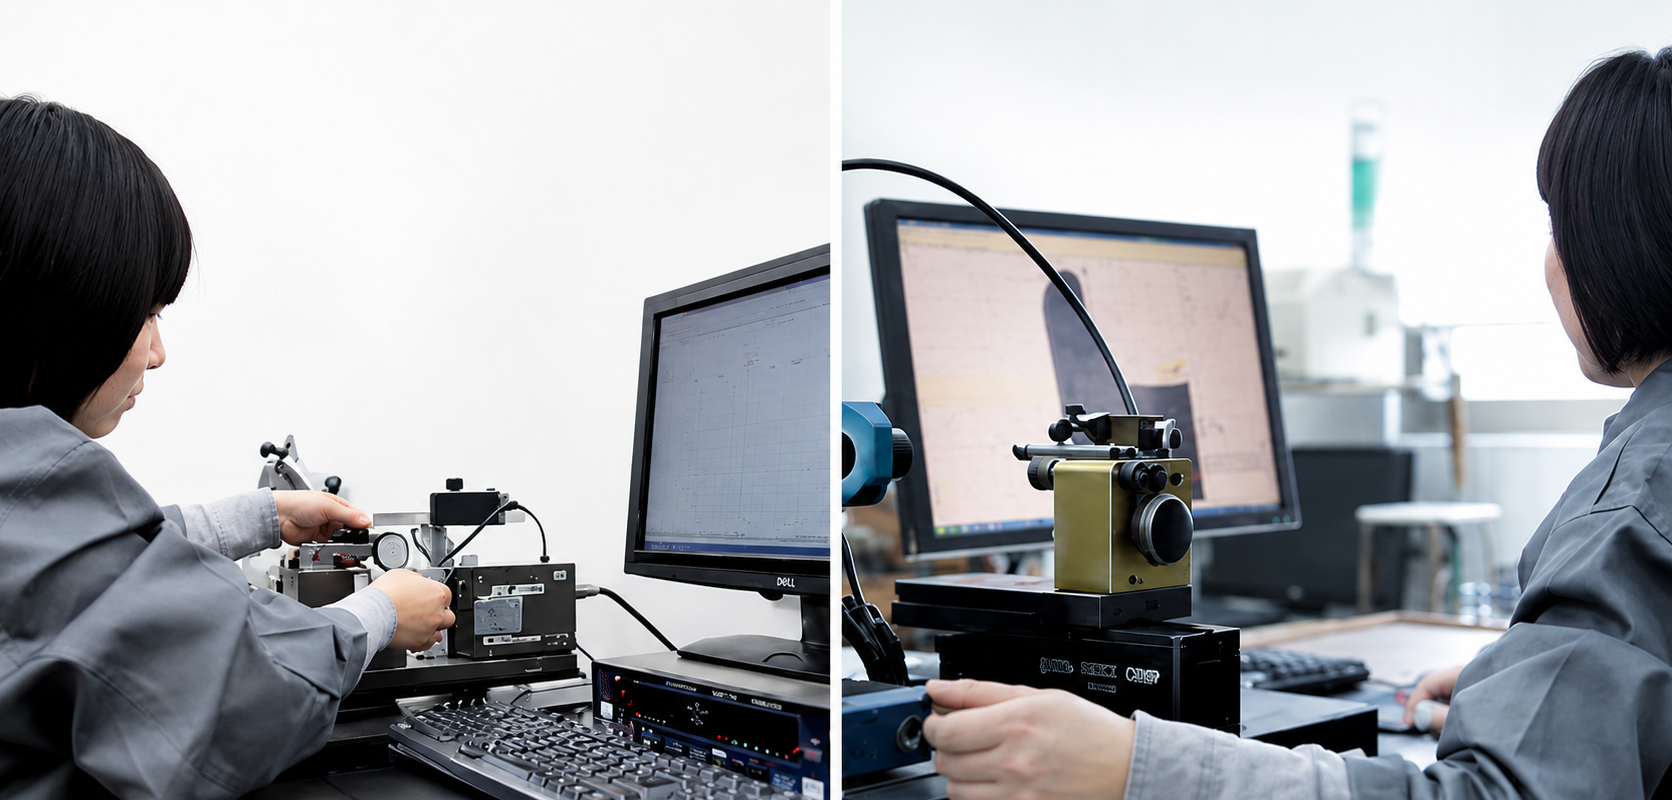
Diameter, point geometry, coating, runout and cutting edges are inspected.
Inspection & Quality Control
Drill dimensions, cutting-edge geometry and visible surface condition are checked according to the confirmed product specification and application requirements.
Protective Packing for Shipment
Finished drills are protected individually before batch labeling and export-carton reinforcement.

Individual Tool Protection
Each drill is individually protected in a plastic tube to reduce contact damage during storage, handling and transportation.
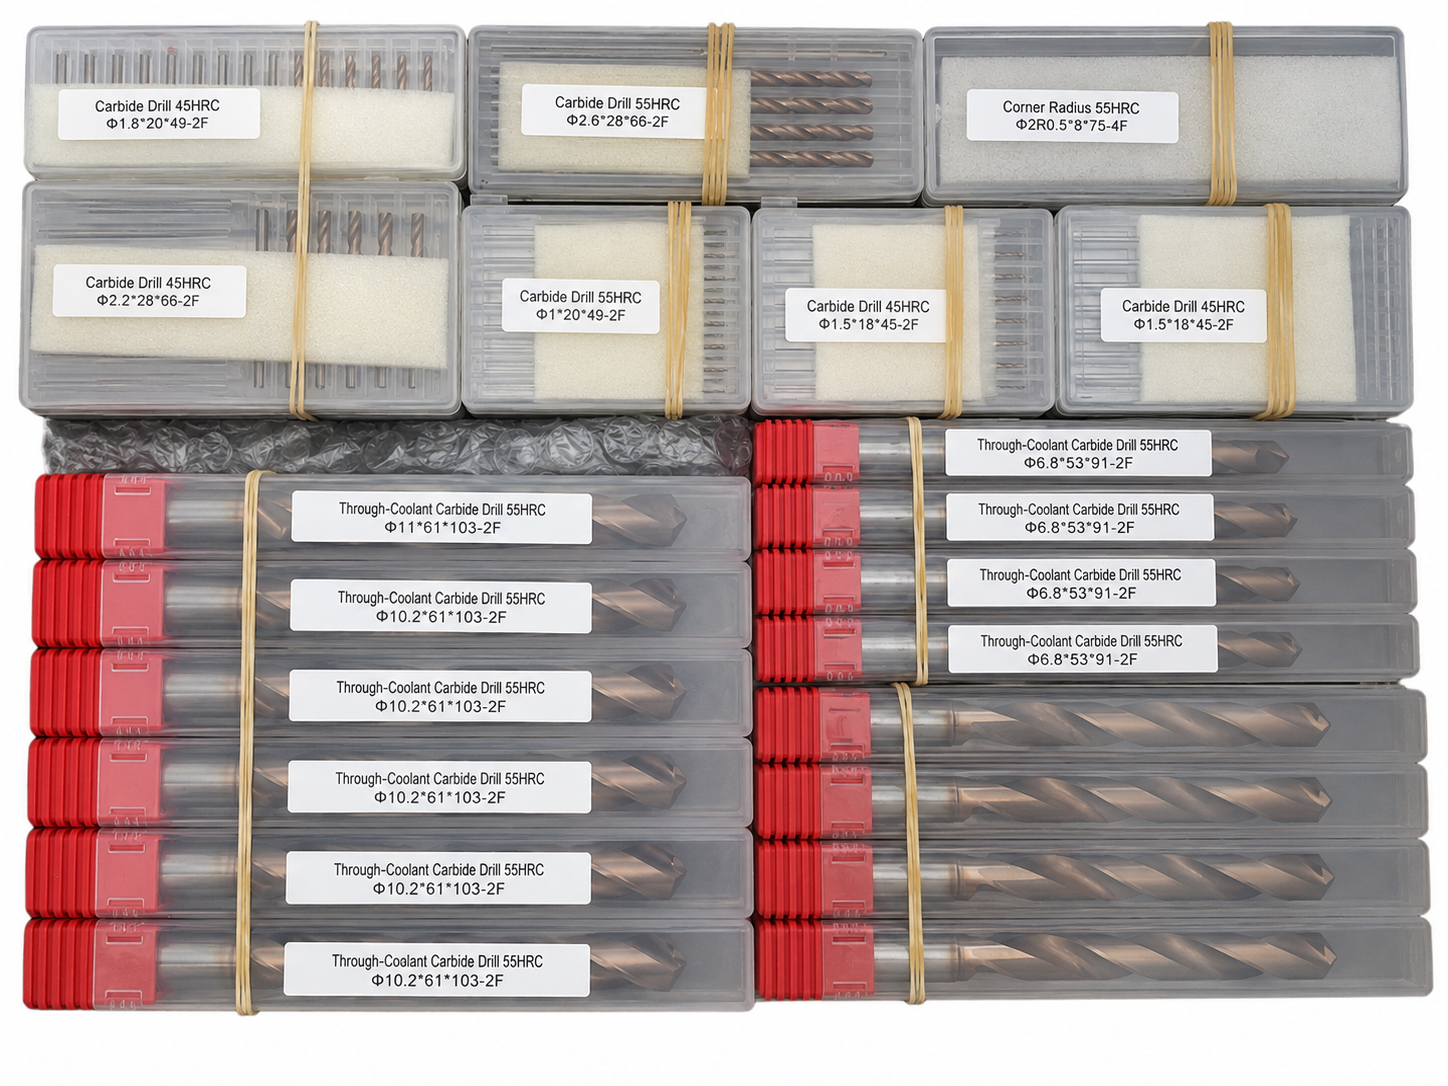
Batch & Label Verification
Tools are grouped and labeled by specification to support order verification before carton packing.

Export Carton Protection
Batch packaging, cushioning materials and reinforced export cartons are selected according to the order quantity and shipping method.
Reference Lead Time
The following timeframes are general references. Availability and production scheduling are reviewed for each order.
Shipping Options
Shipping arrangements can be selected according to order size, delivery schedule and destination.

Product FAQs
Product-specific information about stainless steel applications, 2-flute geometry, coating selection, coolant requirements and available configurations for this solid carbide twist drill.
Which stainless steel grades is this drill designed for?
This drill is designed primarily for austenitic and selected martensitic or duplex stainless steels, including commonly machined grades such as 304, 316 and 2205. Final suitability should be confirmed according to the exact material grade, hardness, hole depth and machining conditions.
What does HRC65 mean in this product series?
HRC65 identifies the performance positioning of the carbide drill series and its wear-resistant tool configuration. It does not mean that every stainless steel workpiece up to 65 HRC can be drilled. The actual machinable hardness depends on the material grade, coating, drill geometry, machine rigidity and coolant conditions.
Why is the cutting geometry optimized for stainless steel?
Stainless steel has a strong tendency to work-harden and generate heat during drilling. The drill geometry is designed to maintain a positive cutting action, control thrust and support stable chip formation while reducing rubbing at the cutting edges.
Why does this drill use a 2-flute design?
The 2-flute design provides a balance between cutting-edge strength, drilling stability and chip space. Its flute geometry helps remove stainless steel chips while maintaining sufficient rigidity for consistent CNC hole production.
Which coating is recommended for stainless steel drilling?
AlCrN, AlTiN and other application-specific PVD coatings can be reviewed according to the stainless steel grade, cutting speed, hole depth and coolant condition. The selected coating should provide suitable heat resistance, wear resistance and low-friction chip flow.
What coolant method is recommended?
Consistent coolant delivery is recommended to control cutting temperature and support chip evacuation. External or through-coolant configurations can be selected according to the drilling depth, tool diameter and machine setup. Coolant interruption should be avoided during continuous drilling.
What information is required for a quotation?
Please provide the required diameter, hole depth, stainless steel grade, material hardness, coolant method, coating preference and estimated quantity. A drawing is recommended for stepped, long-reach or other non-standard drill requirements.
Ordering & OEM FAQs
General information for trial orders, mixed-size purchasing, private labeling and production scheduling.
Do you accept small trial orders?
Yes. Small sample or trial orders are welcomed for evaluating hole quality, chip evacuation, cutting stability and tool life before committing to volume purchasing.
Can mixed sizes be ordered together?
Yes. Standard and custom sizes can be combined in one order when the geometry, carbide grade and coating requirements are compatible. Mixed-size purchasing is suitable for distributors, wholesalers and batch inventory planning.
Can the drill dimensions and geometry be customized?
Yes. The cutting diameter, flute length, overall length, shank diameter, point geometry, flute profile, edge preparation, coolant configuration and dimensional tolerance can be reviewed according to the application or customer drawing.
Is OEM laser marking available?
Yes. Custom shank laser marking such as logo, model number, specifications or batch identification can be reviewed together with OEM labels, individual tool protection and branded packaging requirements.
What is the typical production lead time?
Standard stock items normally have a shorter lead time, while custom dimensions, special coatings and OEM orders require additional production time. The exact schedule is confirmed according to specification, quantity, coating and current production capacity.
Downloads & Technical Resources
Access product dimensions, series information and starting cutting data for product selection and stainless steel drilling application review.
Ölçüler, fiyatlar veya özel seçenekler mi arıyorsunuz?
Gerekli takım türünü, boyutlarını, miktarlarını, iş parçası malzemesini ve varsa OEM veya özel gereksinimleri bize iletin. Uygun teknik özellikleri, stok durumunu, teslim süresini ve fiyat teklifi ayrıntılarını size teyit edeceğiz.
Çizimler, boyut listeleri ve referans fotoğraflar memnuniyetle kabul edilir.