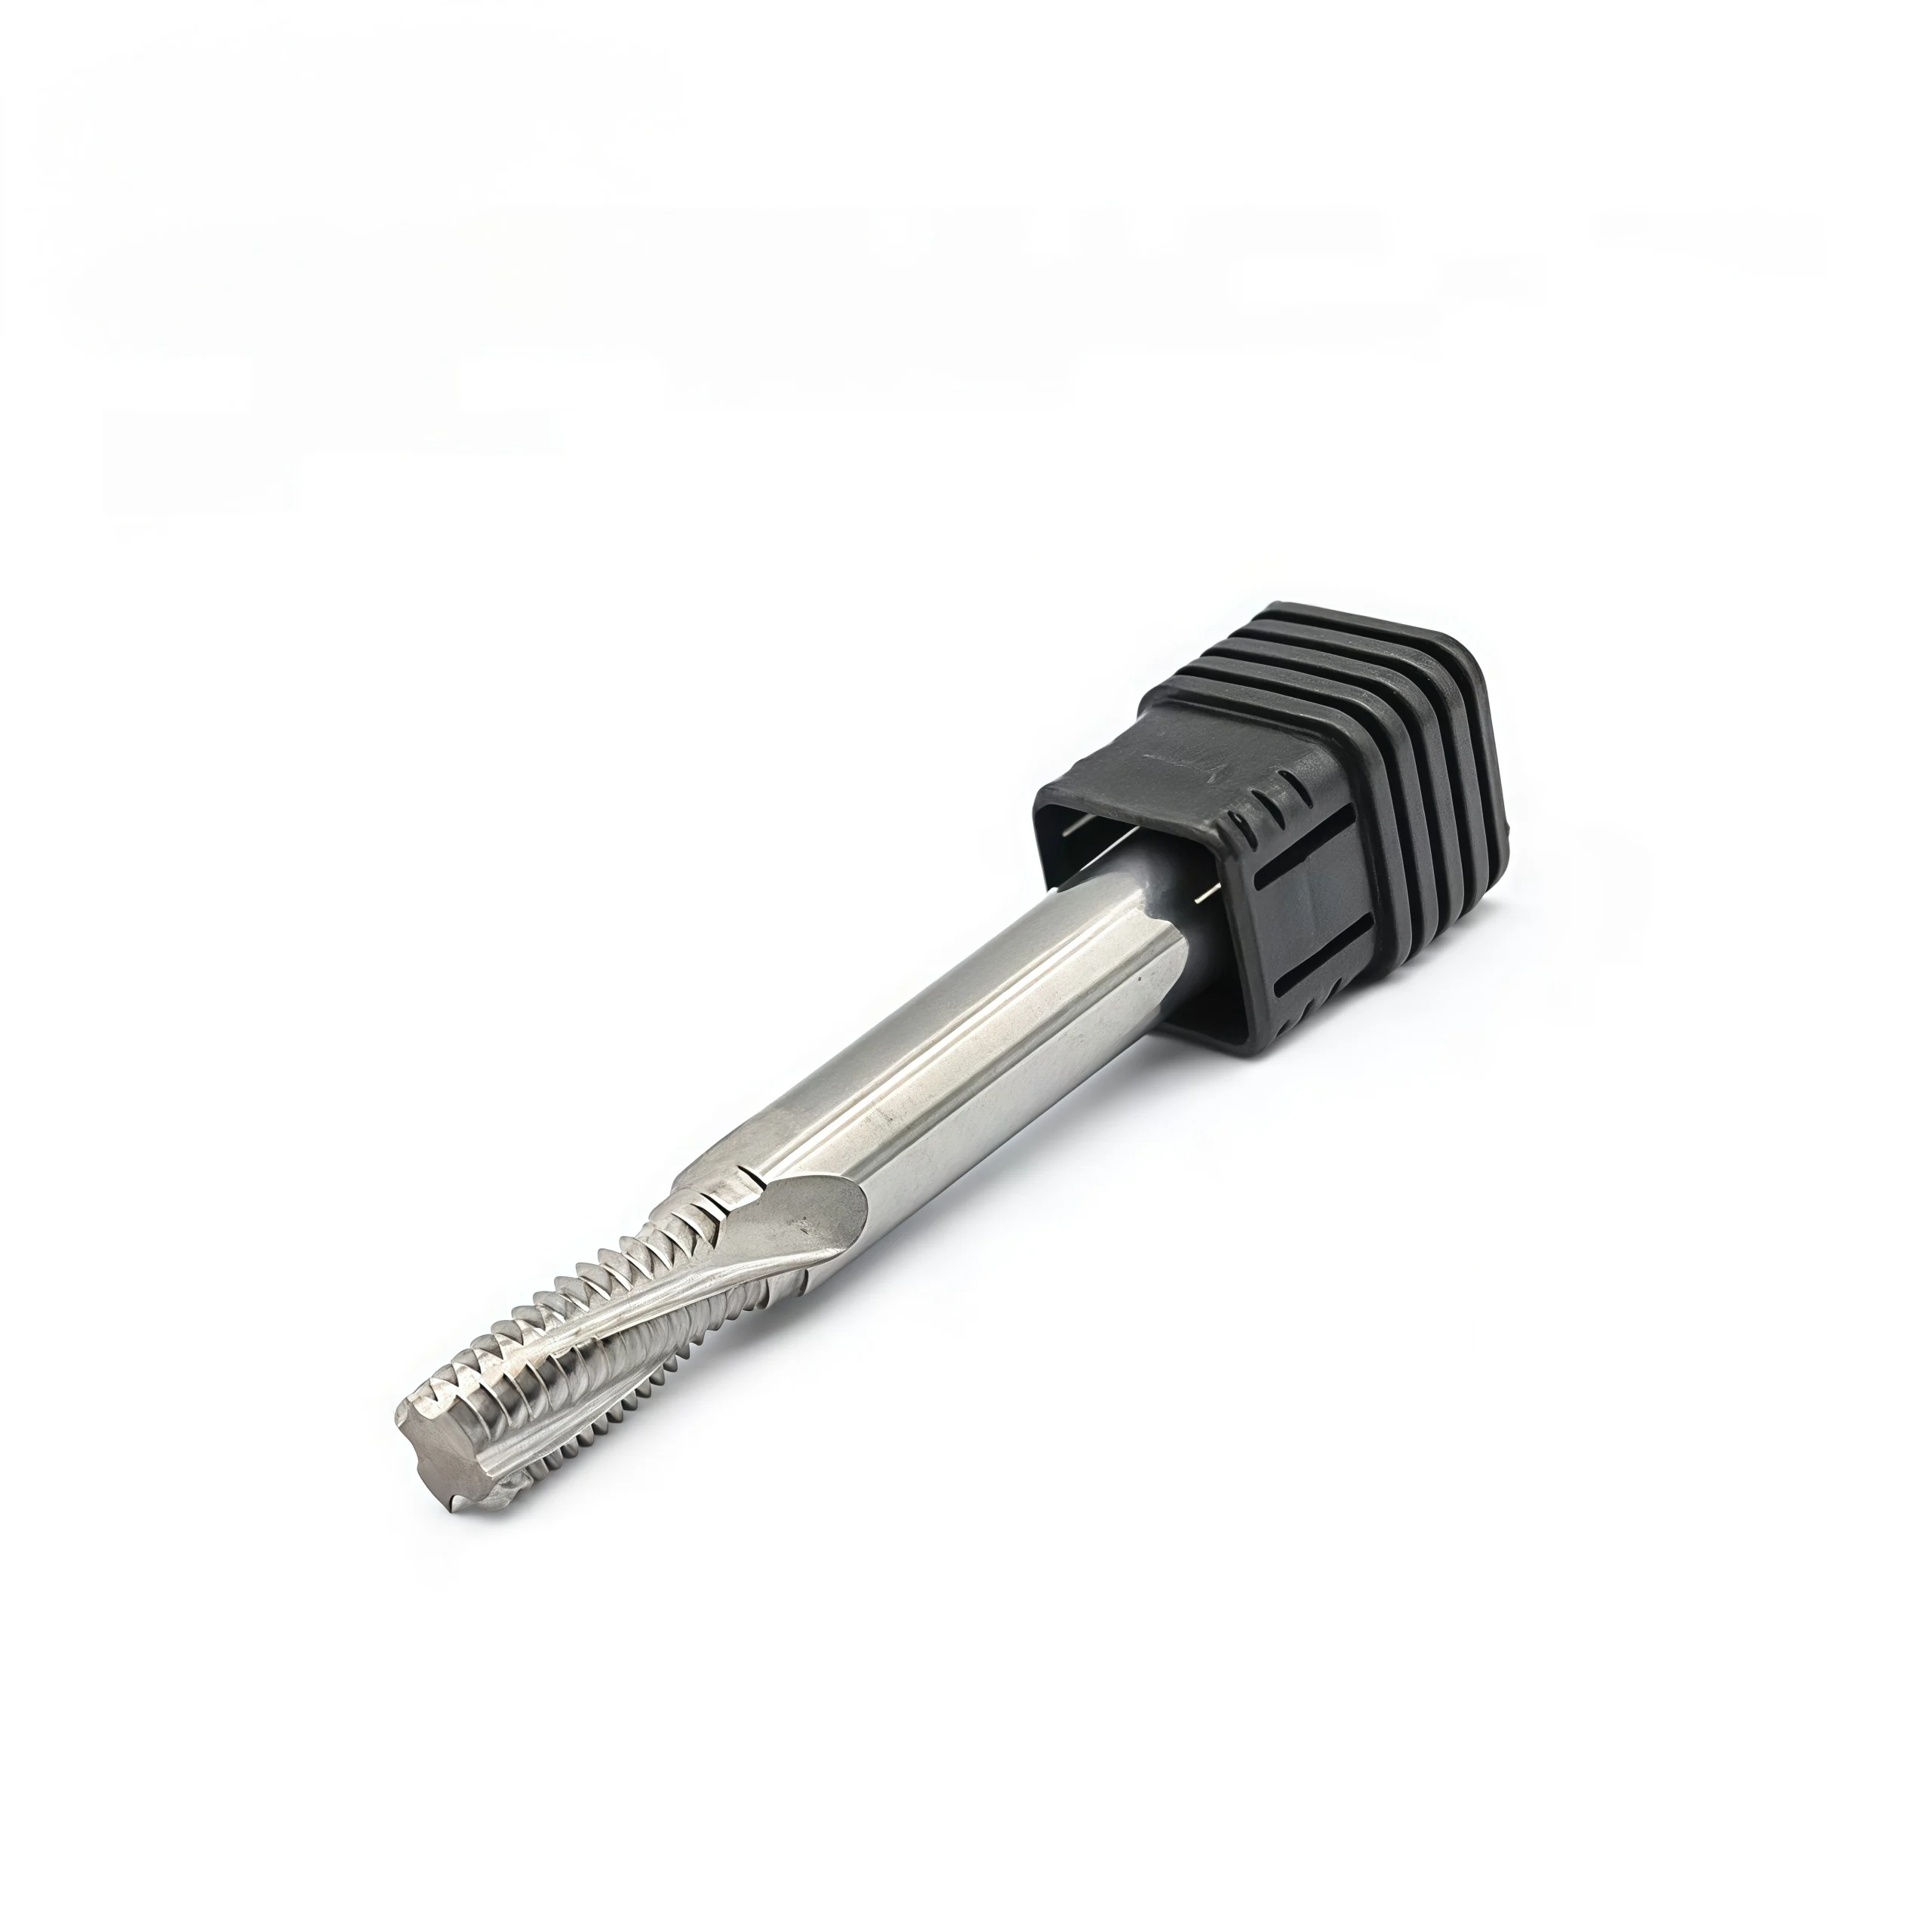
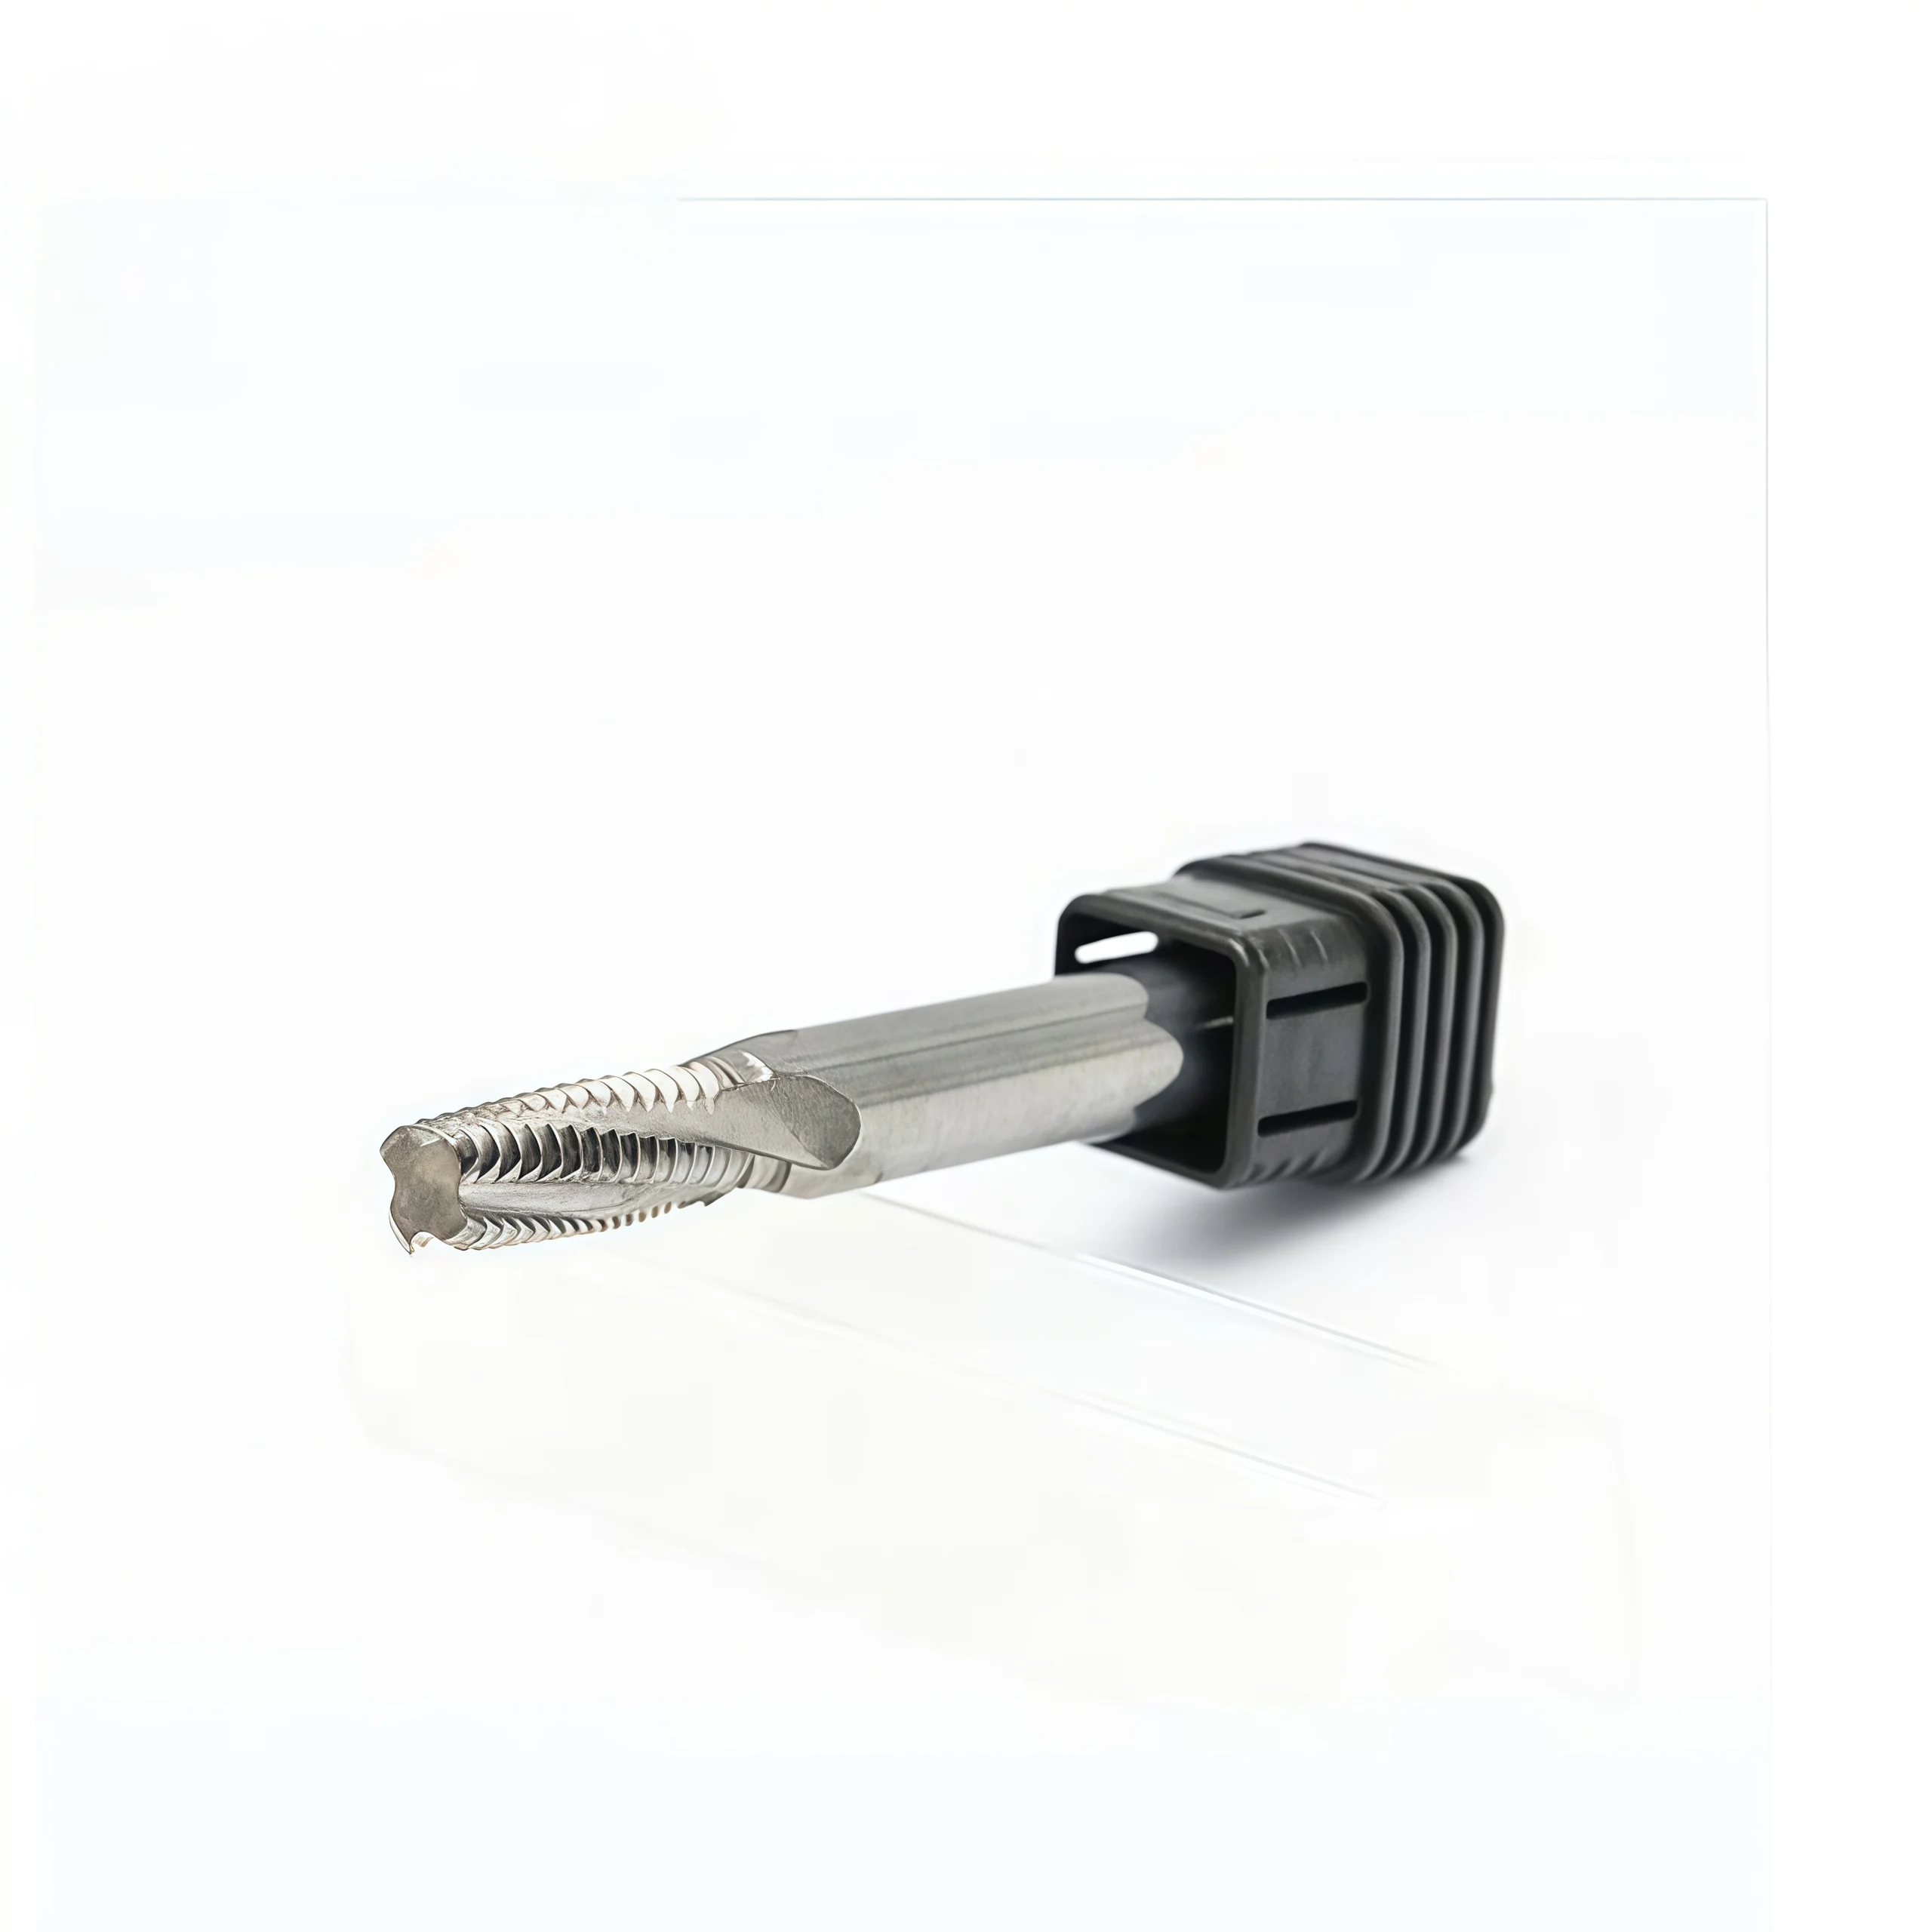
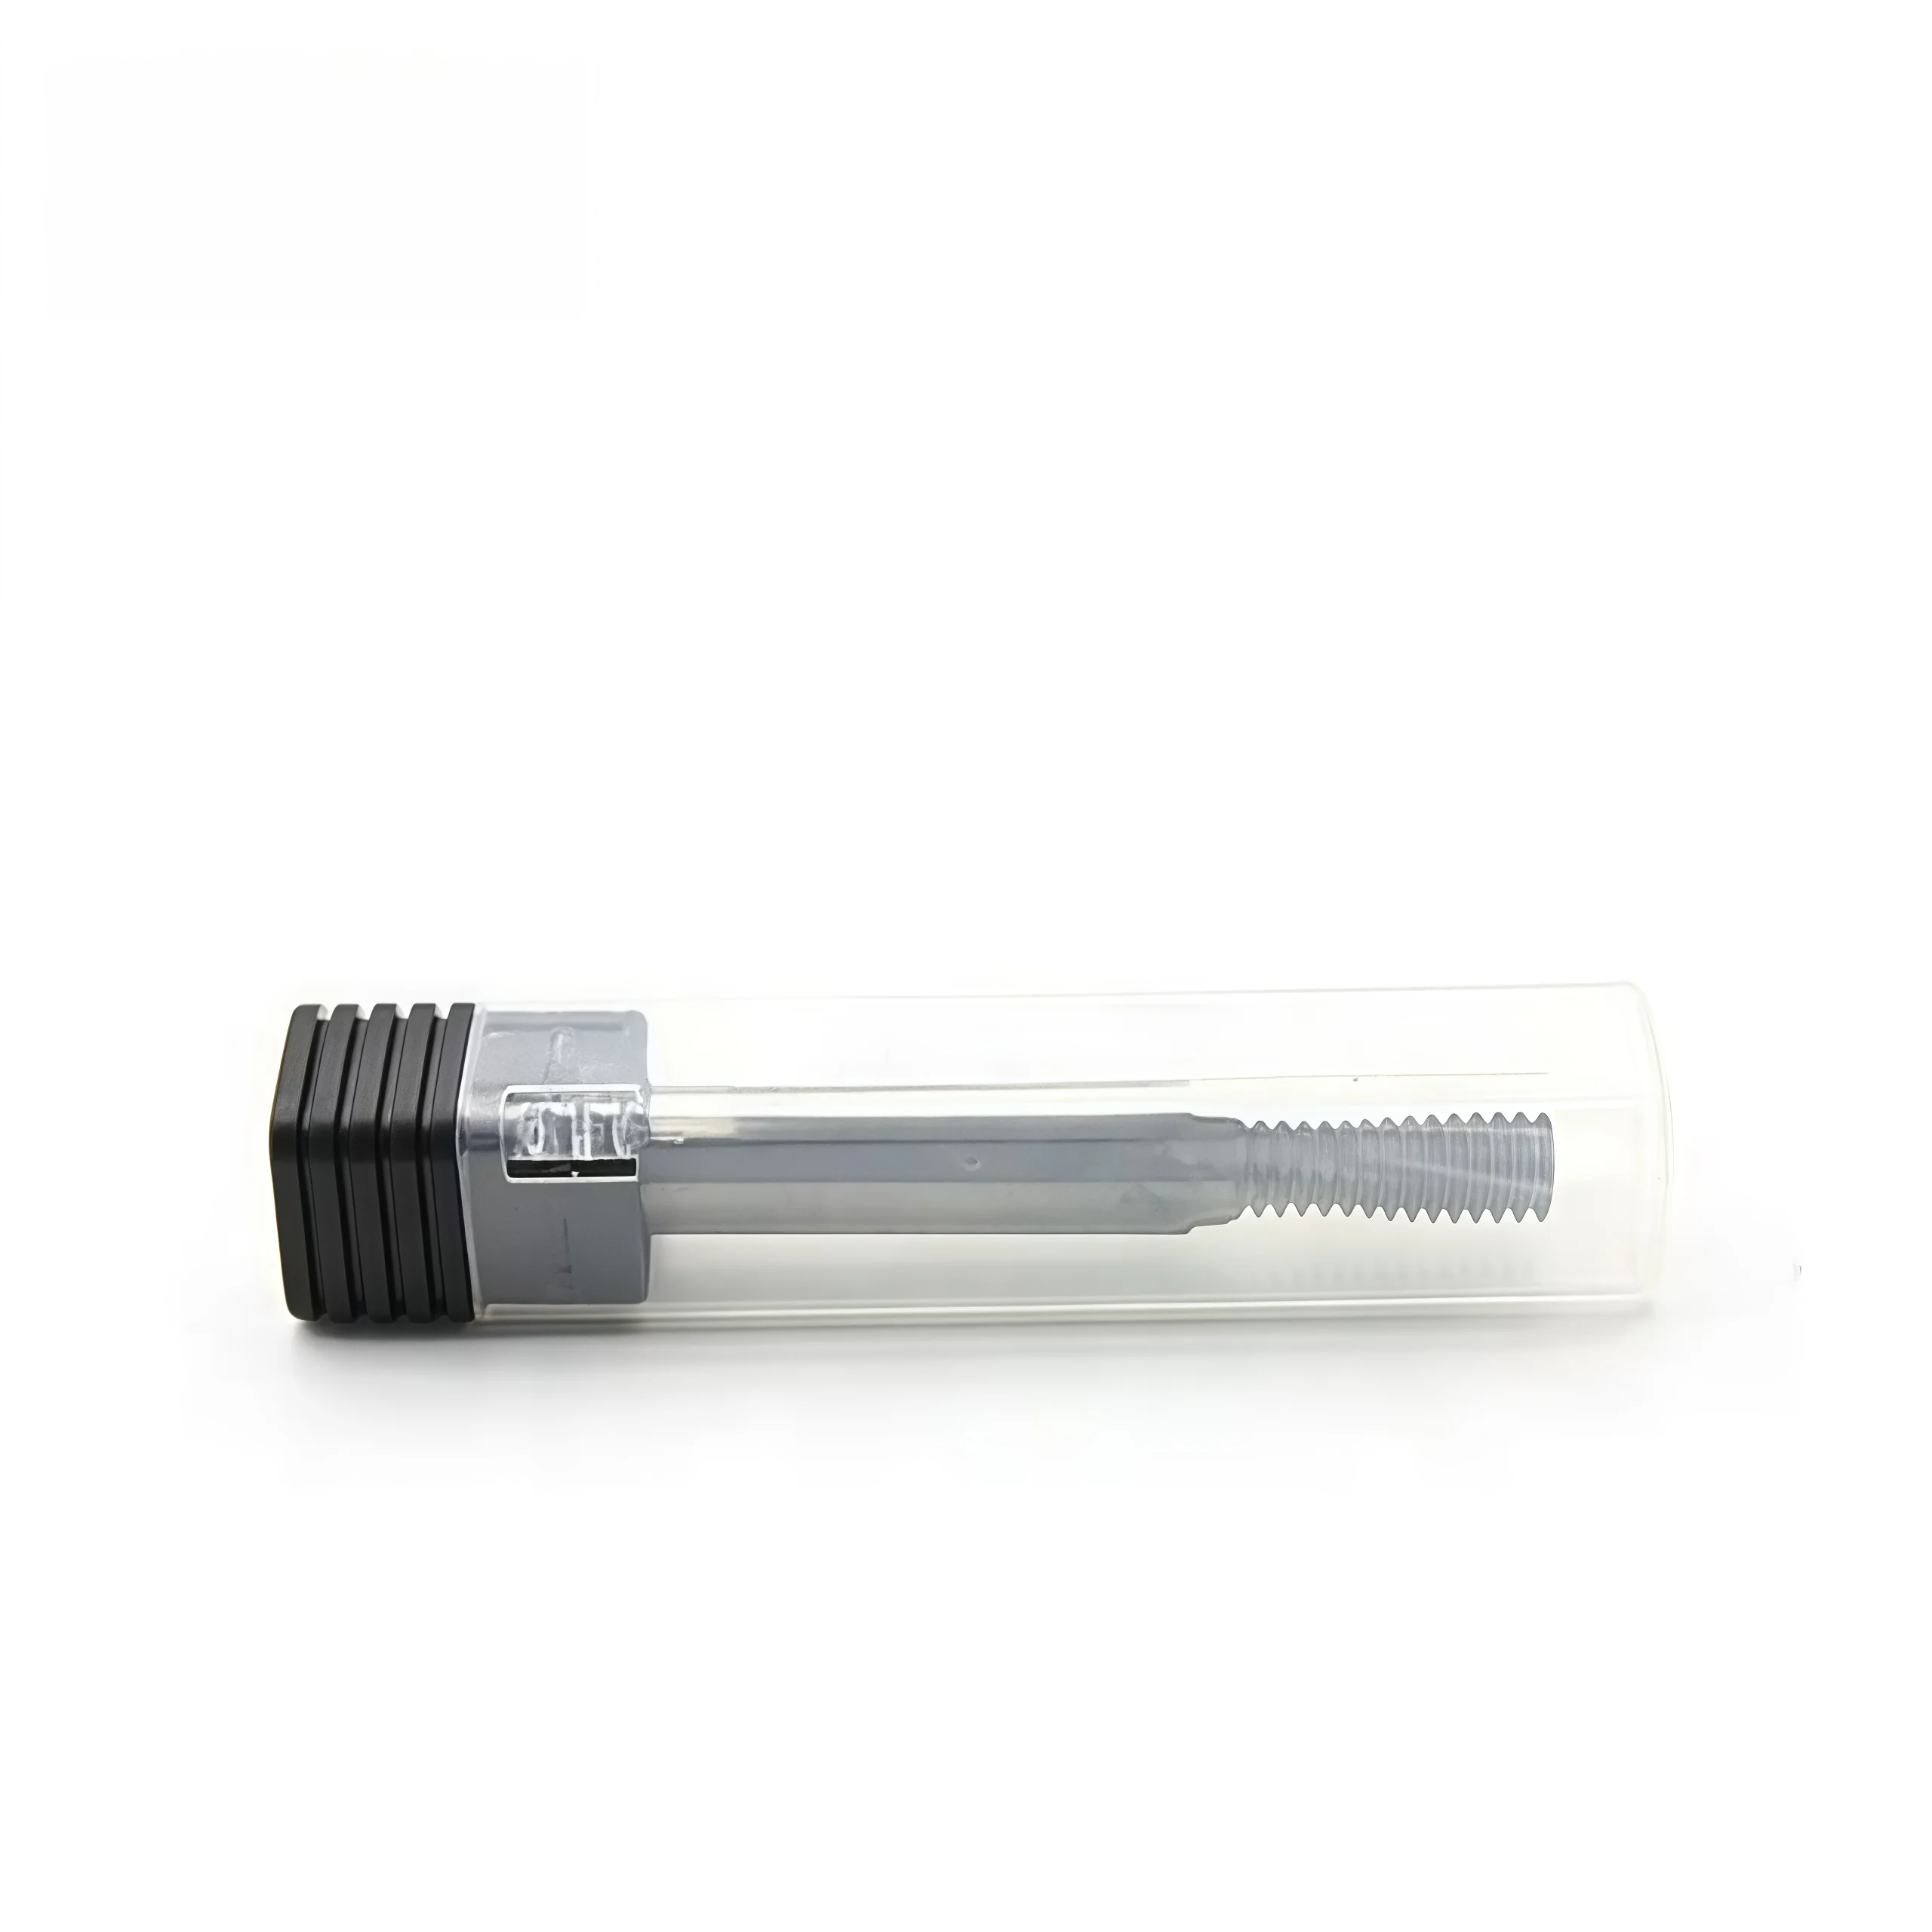



Solid Carbide Thread Mill Series for Aluminum
Solid Carbide Thread Mill Series for Aluminum
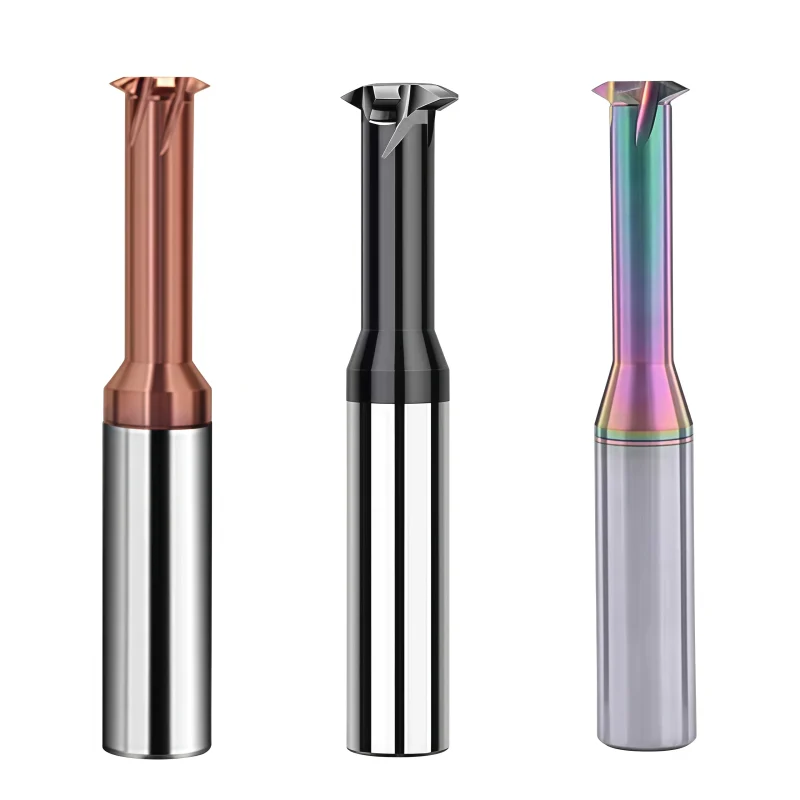
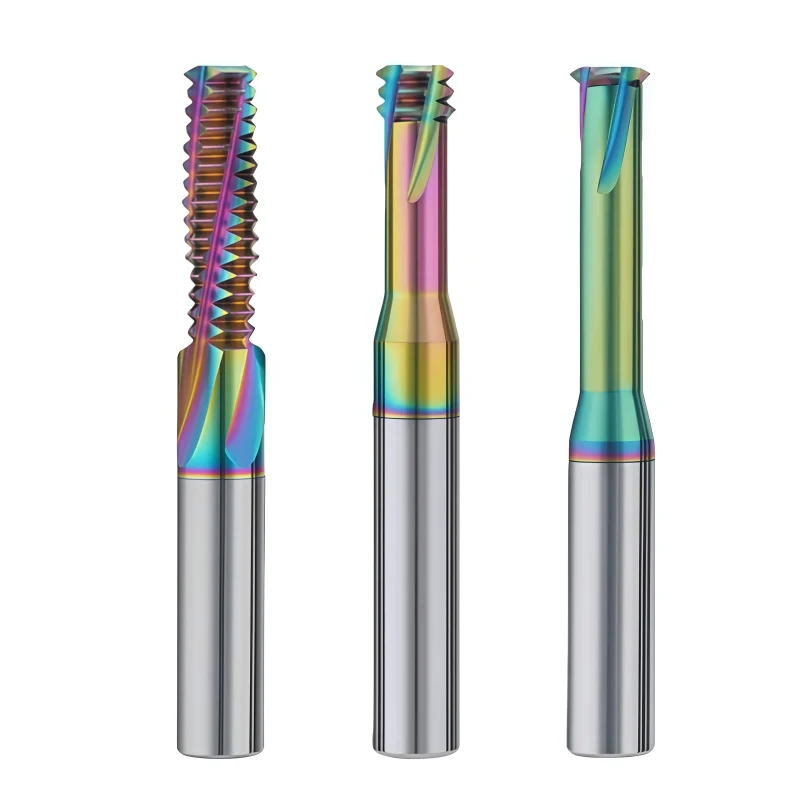
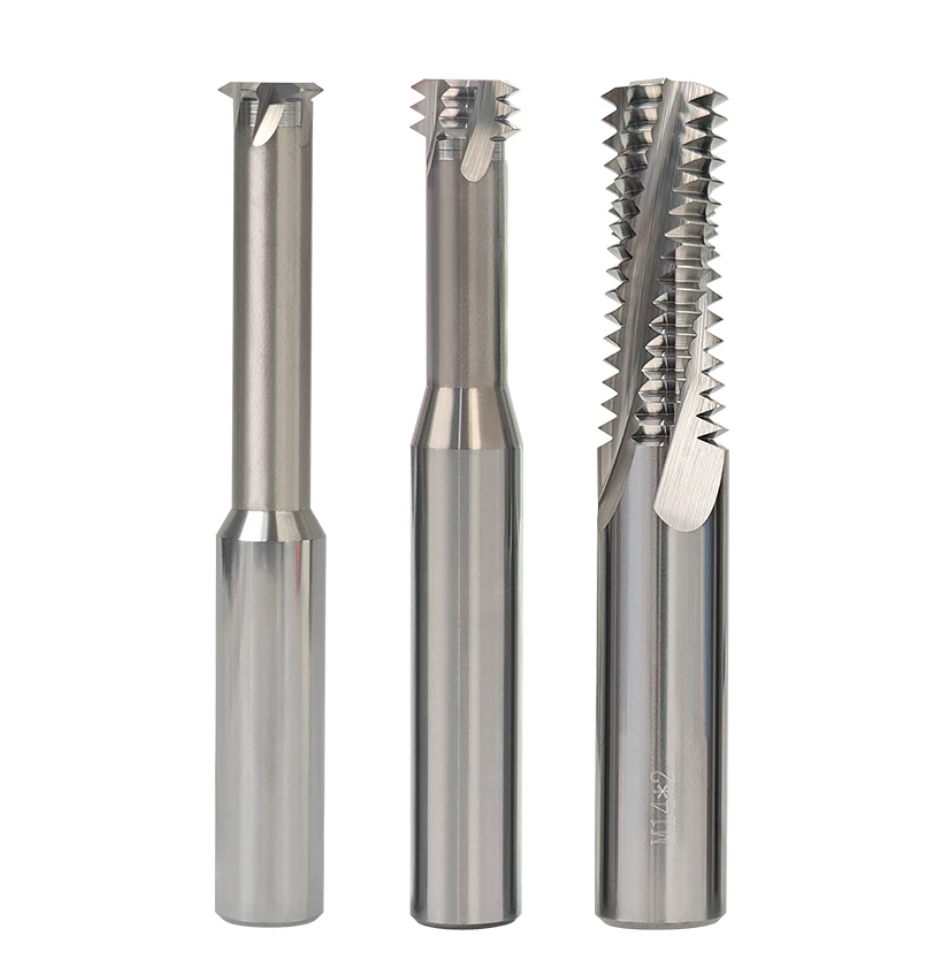
Solid carbide thread mills for precision CNC internal threading in aluminum and selected non-ferrous materials, available in single-form, 3-tooth and full-profile configurations.
Ürün Yapılandırması
Birincil UygulamaPrecision internal thread milling in aluminum components using CNC circular or helical interpolation.
Tutarlı Kalite
Tekrarlanan siparişlerde tutarlı geometri.
Esnek Siparişler
Küçük partiler ve farklı boyutlarda seçenekler mevcuttur.
OEM Desteği
Özel işaretleme, etiketler ve ambalajlama.
Standart ve Özel
Standart boyutlar ve özel konfigürasyonlar.
Solid Carbide Thread Mill Series for Aluminum
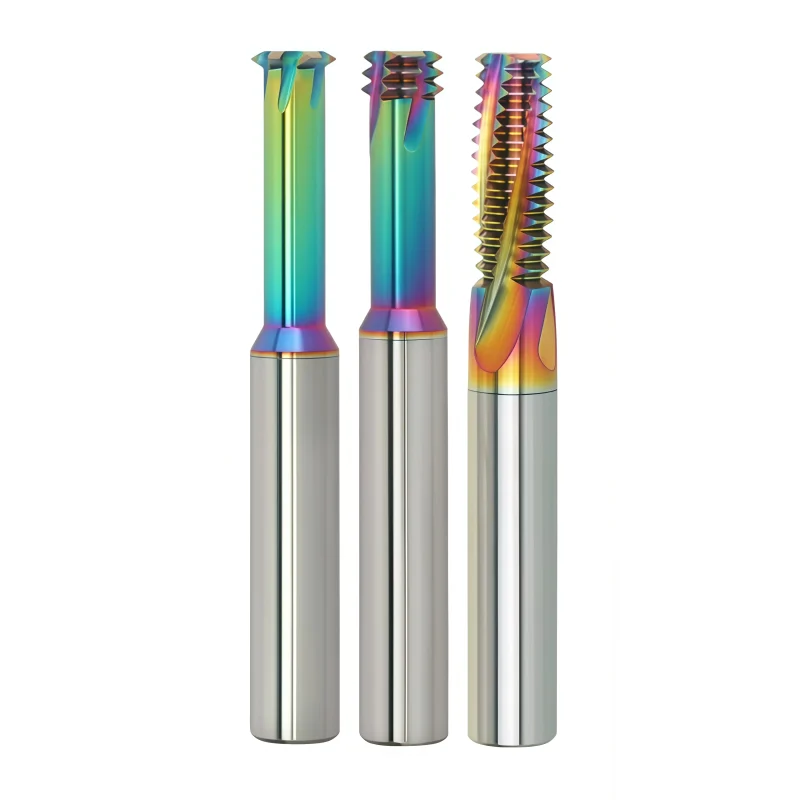
A solid carbide thread mill series developed for precision CNC internal threading in aluminum and selected non-ferrous materials. Single-form, 3-tooth and full-profile configurations provide different options for thread depth, pitch requirements and machining efficiency, while aluminum-focused cutting geometry supports smooth chip evacuation and stable thread quality.
Key Configuration
Solid Carbide
Precision-ground carbide construction.
Three Configurations
Single-Form / 3-Tooth / Full-Profile.
Aluminum Focus
Designed for aluminum and selected non-ferrous materials.
CNC Thread Milling
For circular or helical interpolation.
Product Advantage
Aluminum-focused geometry combines sharp cutting, open chip space and solid carbide rigidity for controlled CNC thread milling.
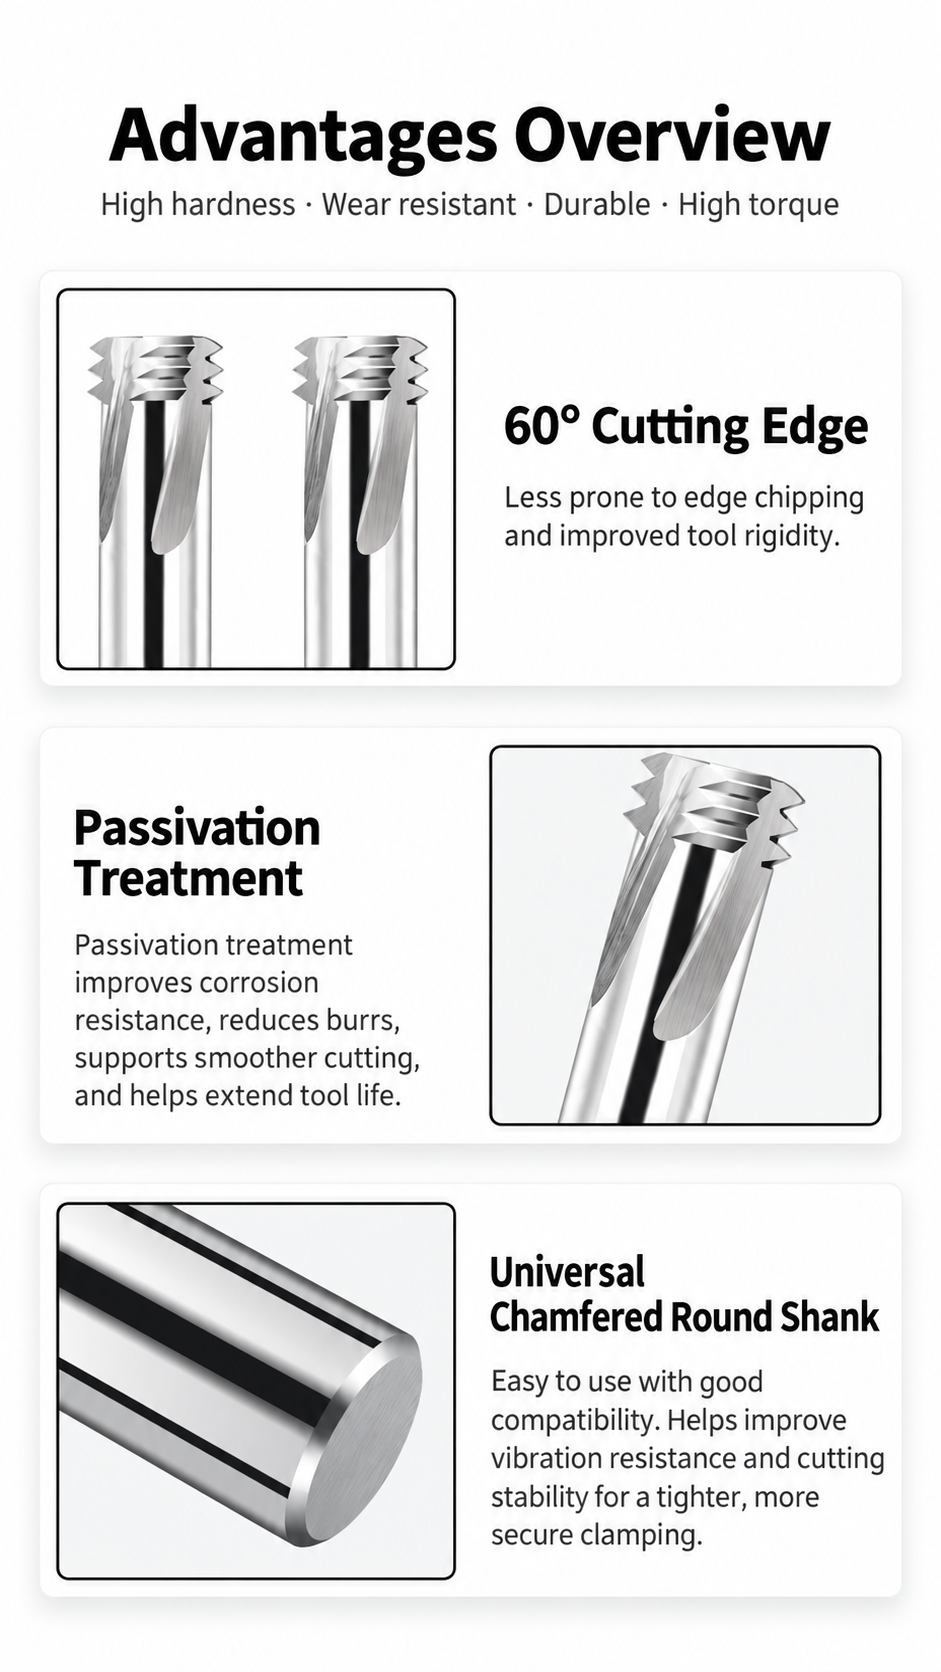
Machining Features
Key design details for aluminum and non-ferrous thread-milling applications.
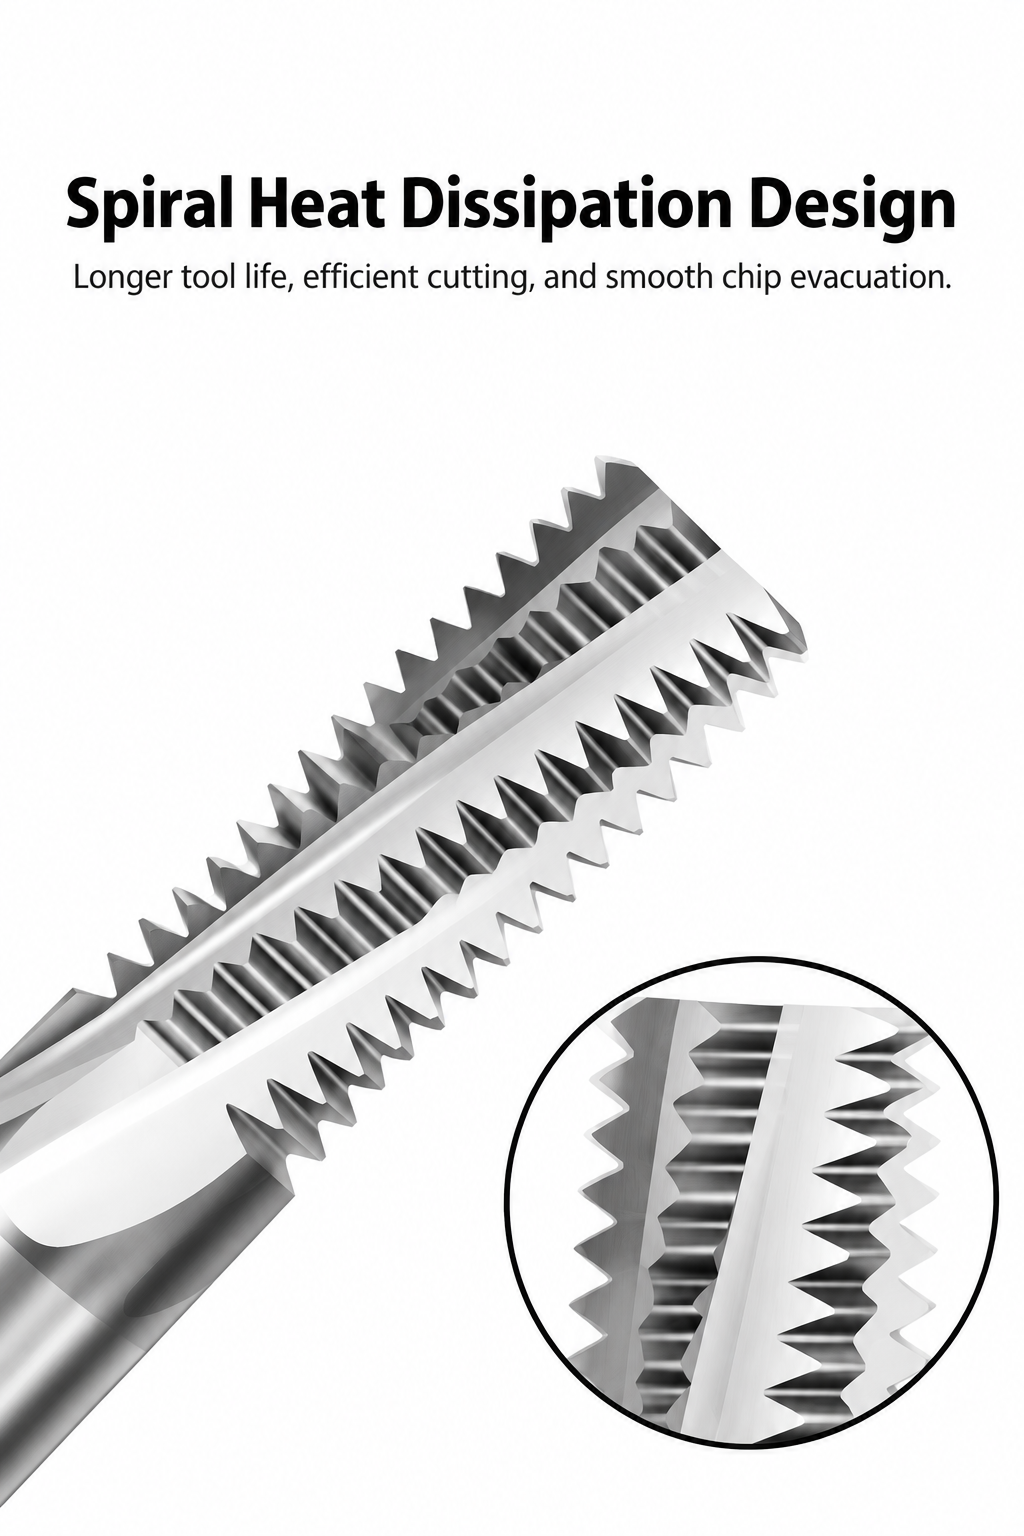
Heat & Chip Control
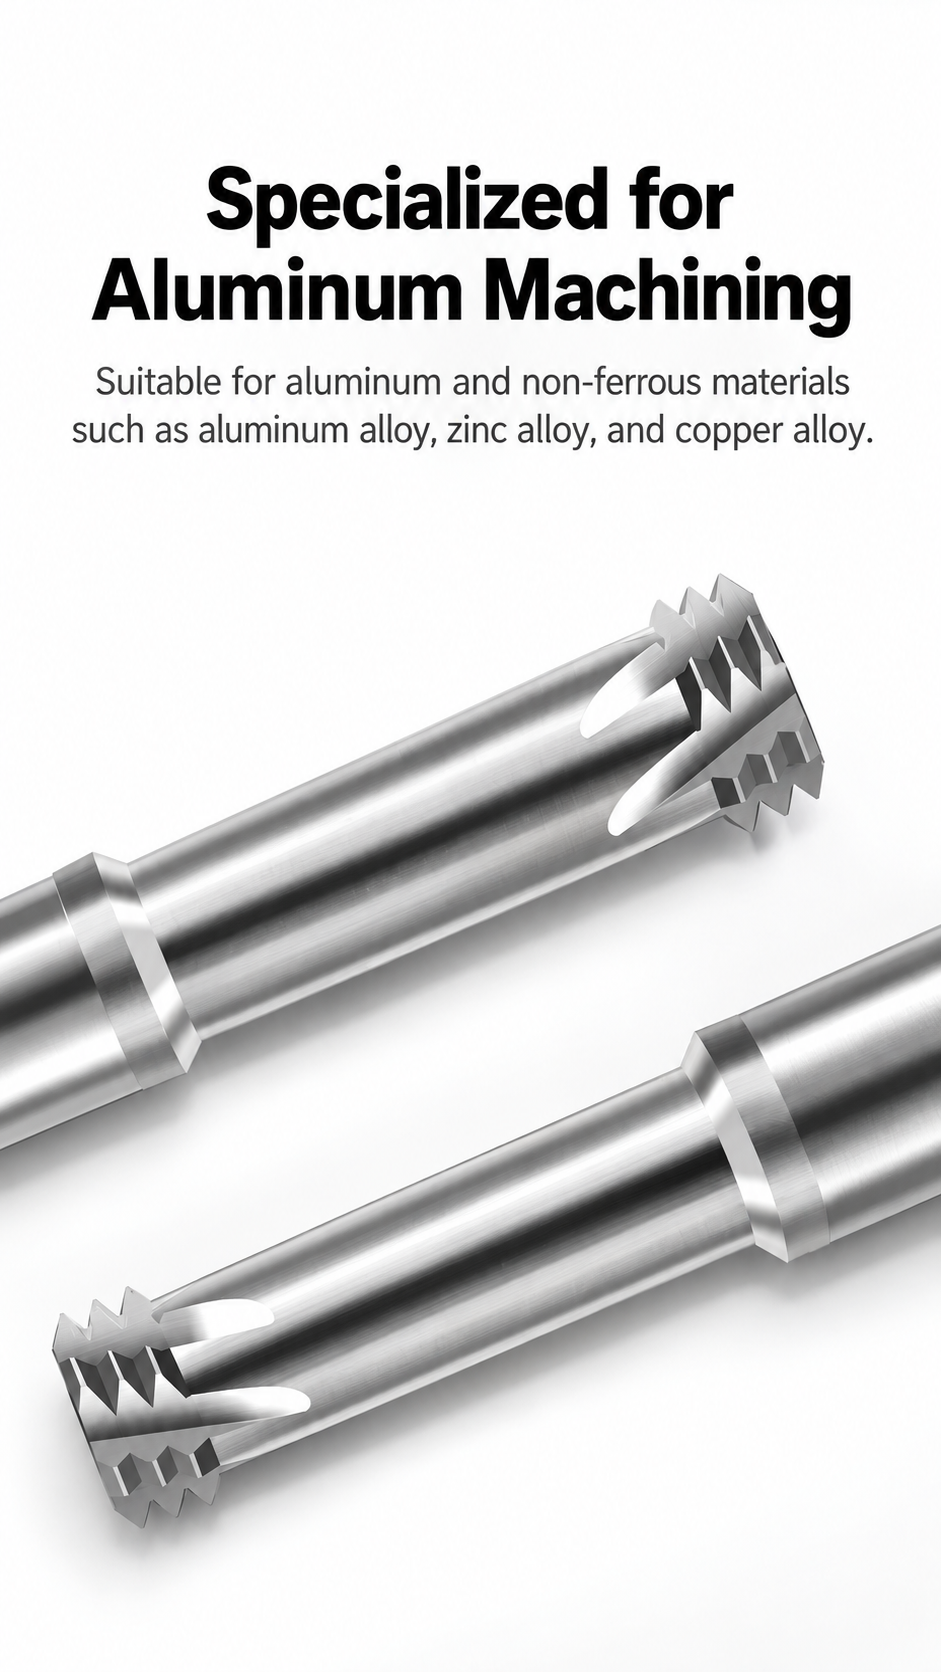
Spiral Flute Geometry
Spiral cutting geometry supports chip movement away from the cutting zone during thread milling.
Aluminum Application
Geometry for Non-Ferrous Machining
Cutting geometry is configured around the low cutting resistance and chip-flow requirements of aluminum machining.
Chip Evacuation
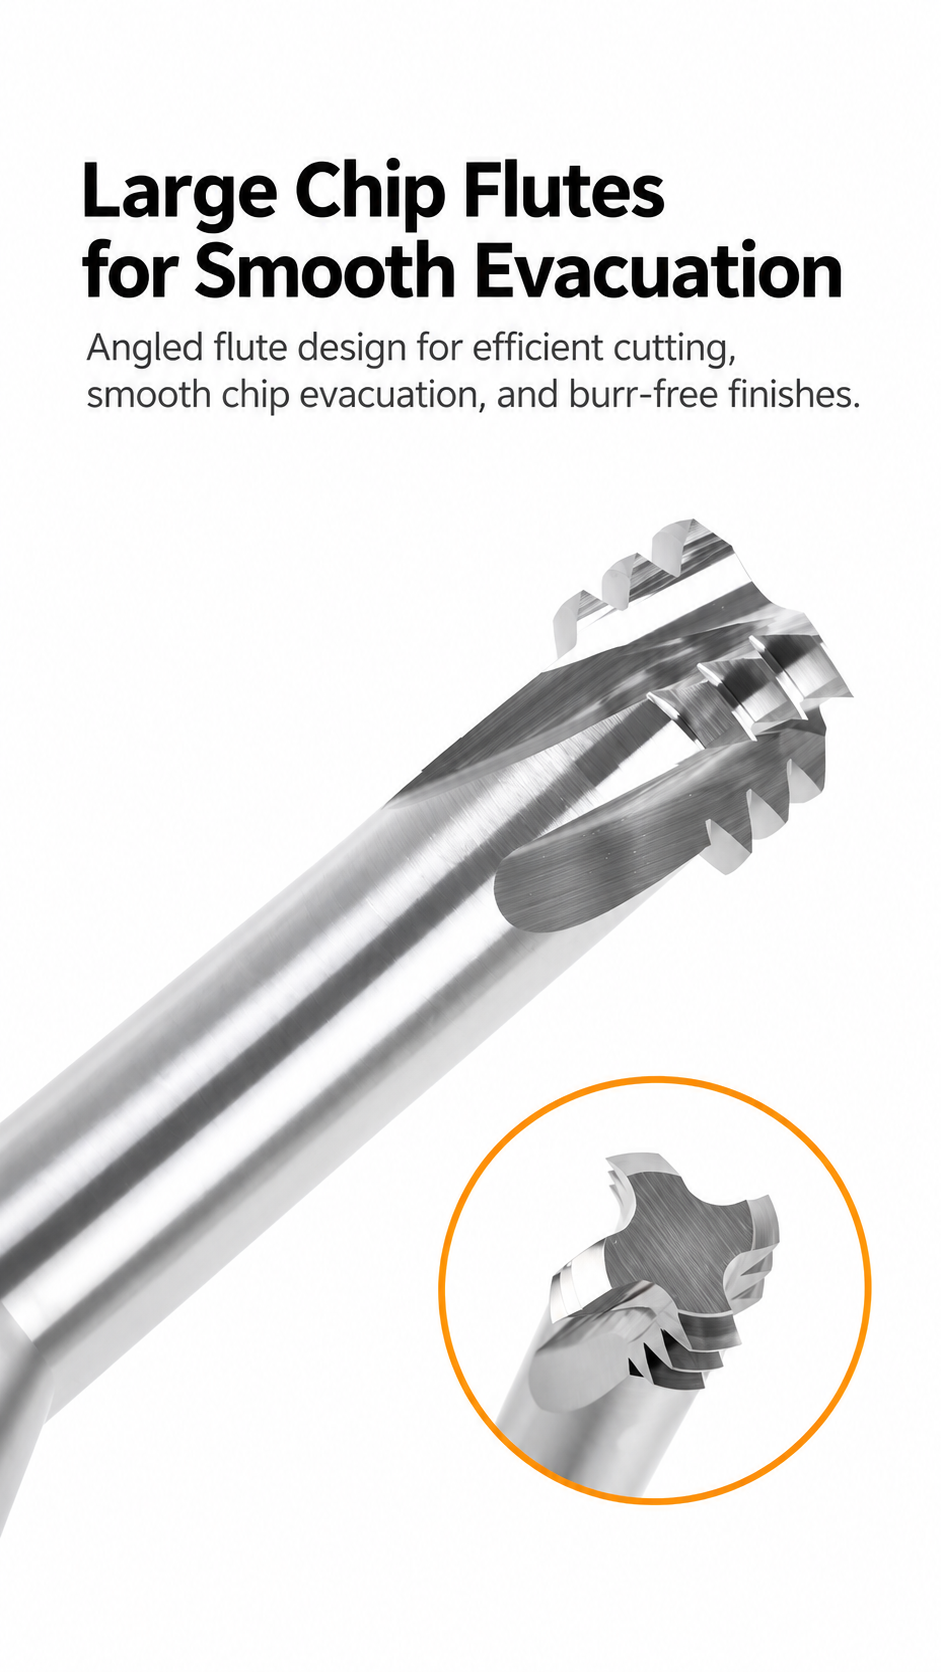
Large Chip Flutes
Open flute space provides clearance for chip evacuation during aluminum internal thread milling.
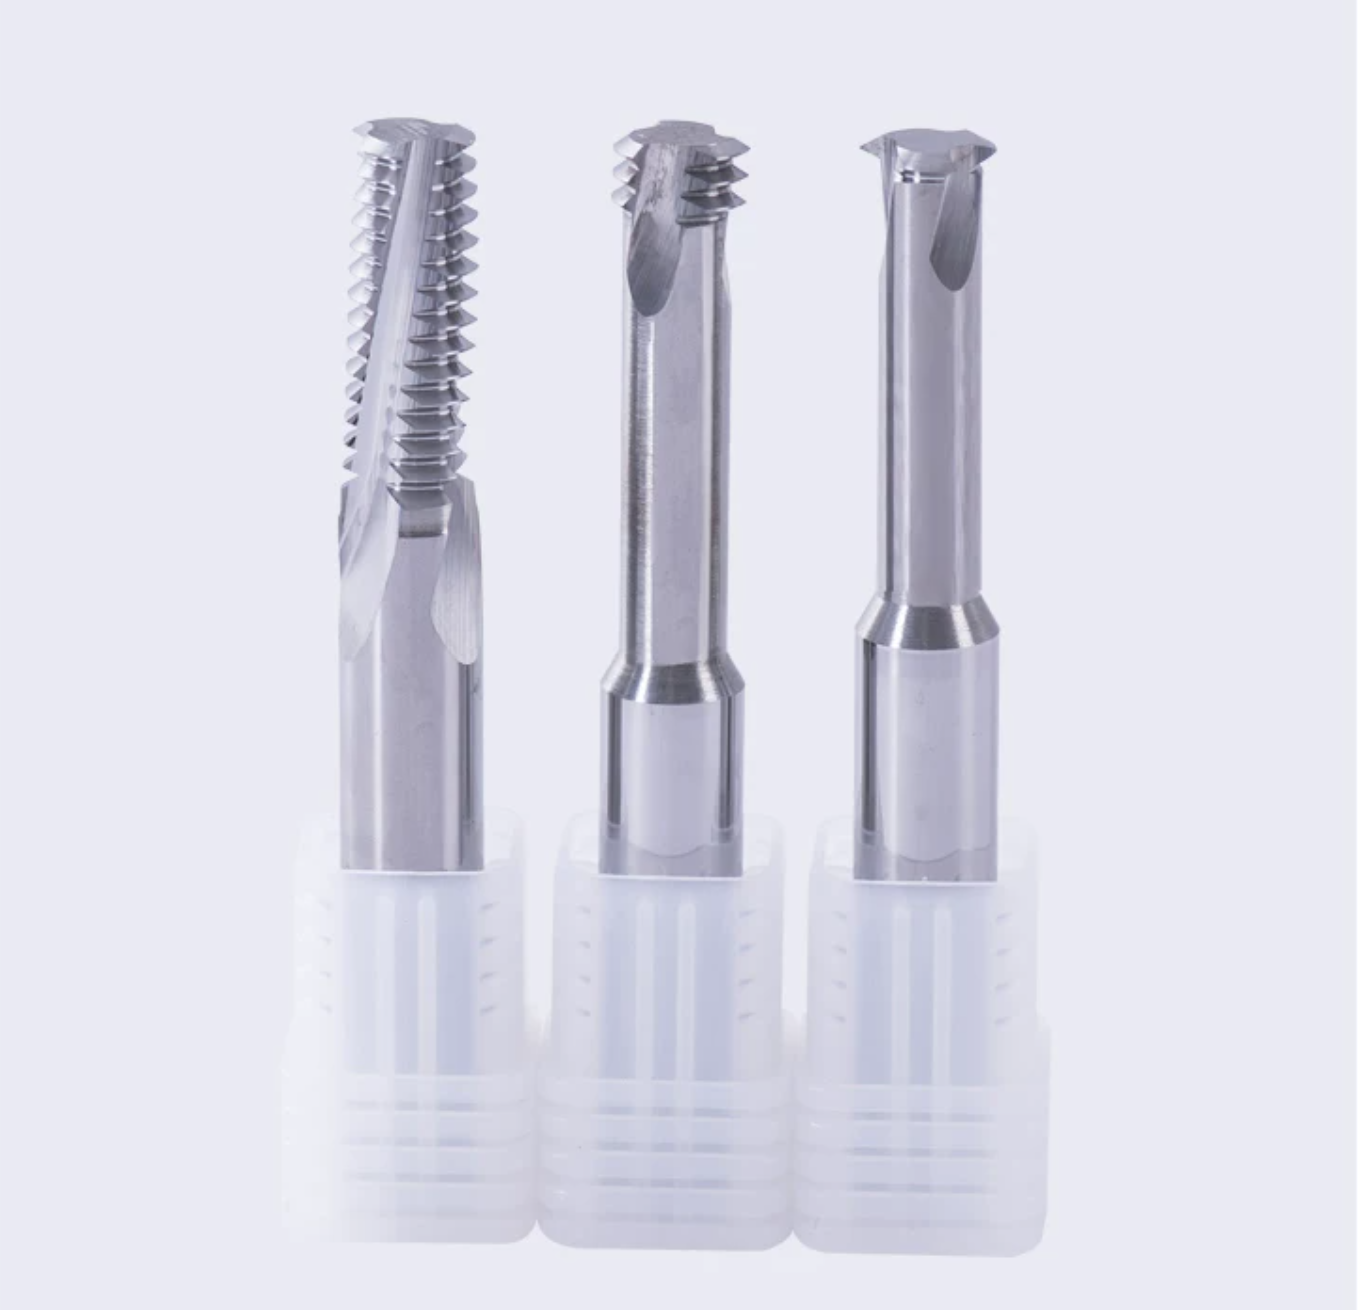
Thread Mill Configurations
Choose the cutting configuration according to thread depth, pitch and production requirement.
Single-Form
Flexible configuration for different thread depths and compatible thread sizes.
3-Tooth
Three thread-form teeth provide a practical balance between flexibility and machining efficiency.
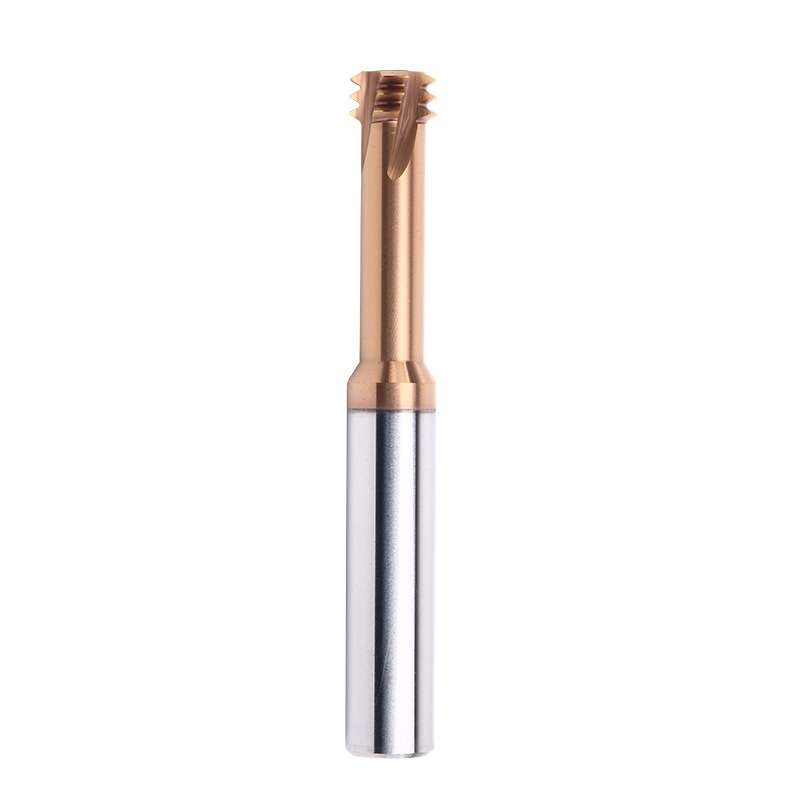
Full-Profile
Pitch-specific multi-tooth geometry for efficient repeat-production thread milling.
Thread Milling Applications
Suitable for precision internal threads, blind-hole threads and CNC circular-interpolation applications in aluminum components. 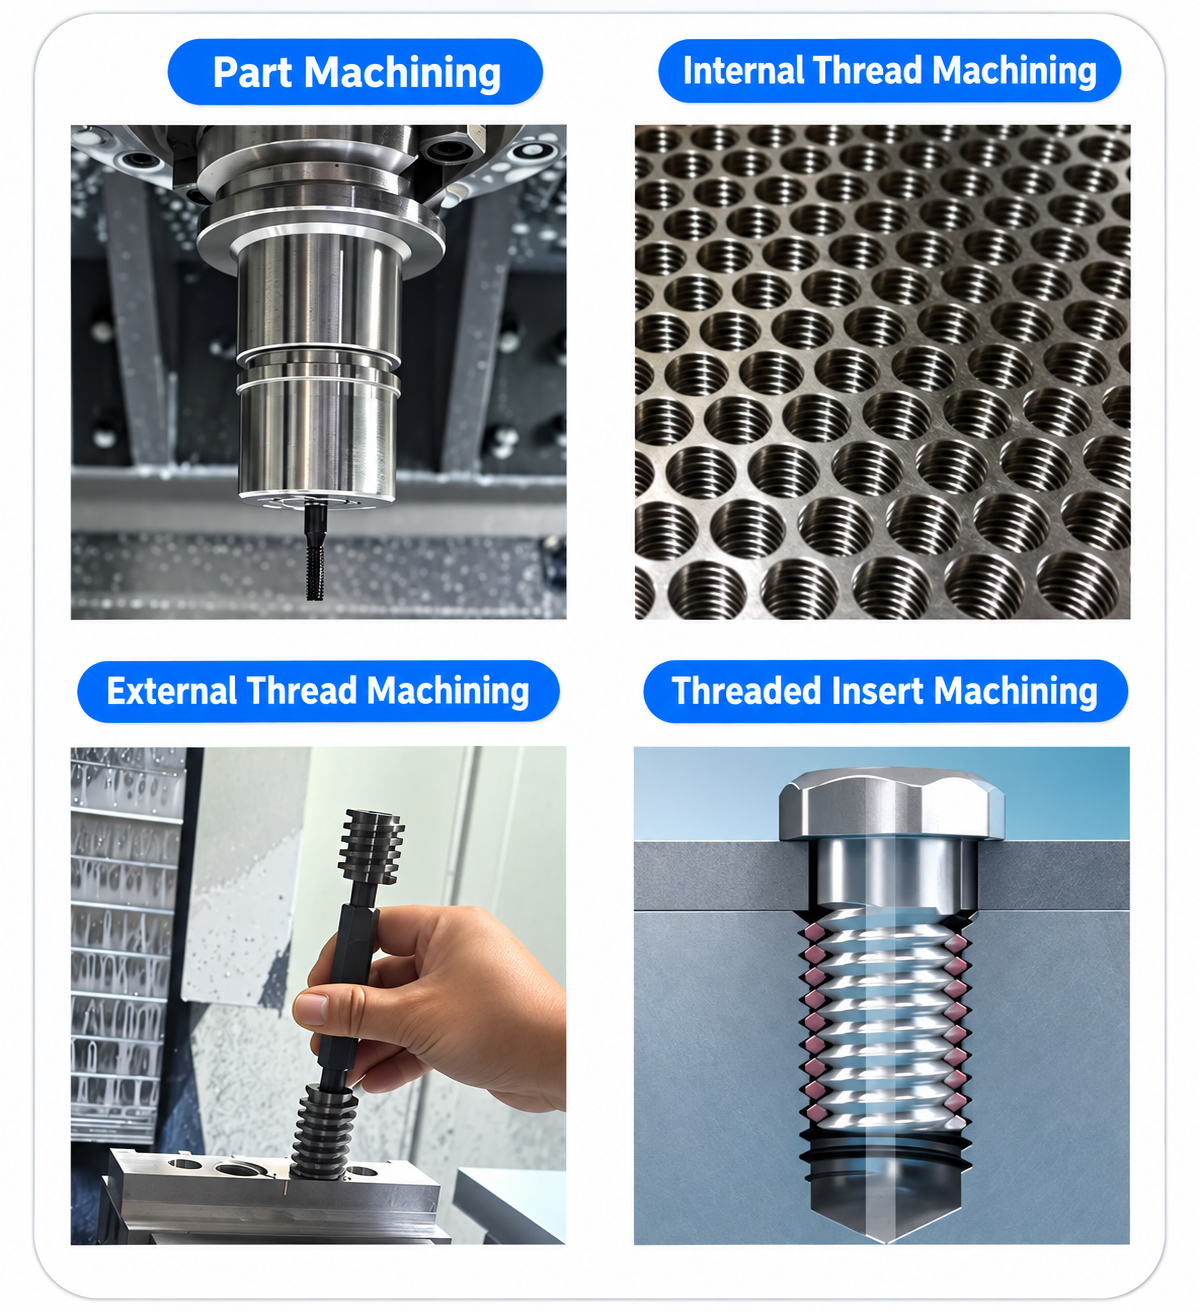
Başvuru Belgeleri
Primarily developed for aluminum, with additional configurations available for selected non-ferrous materials.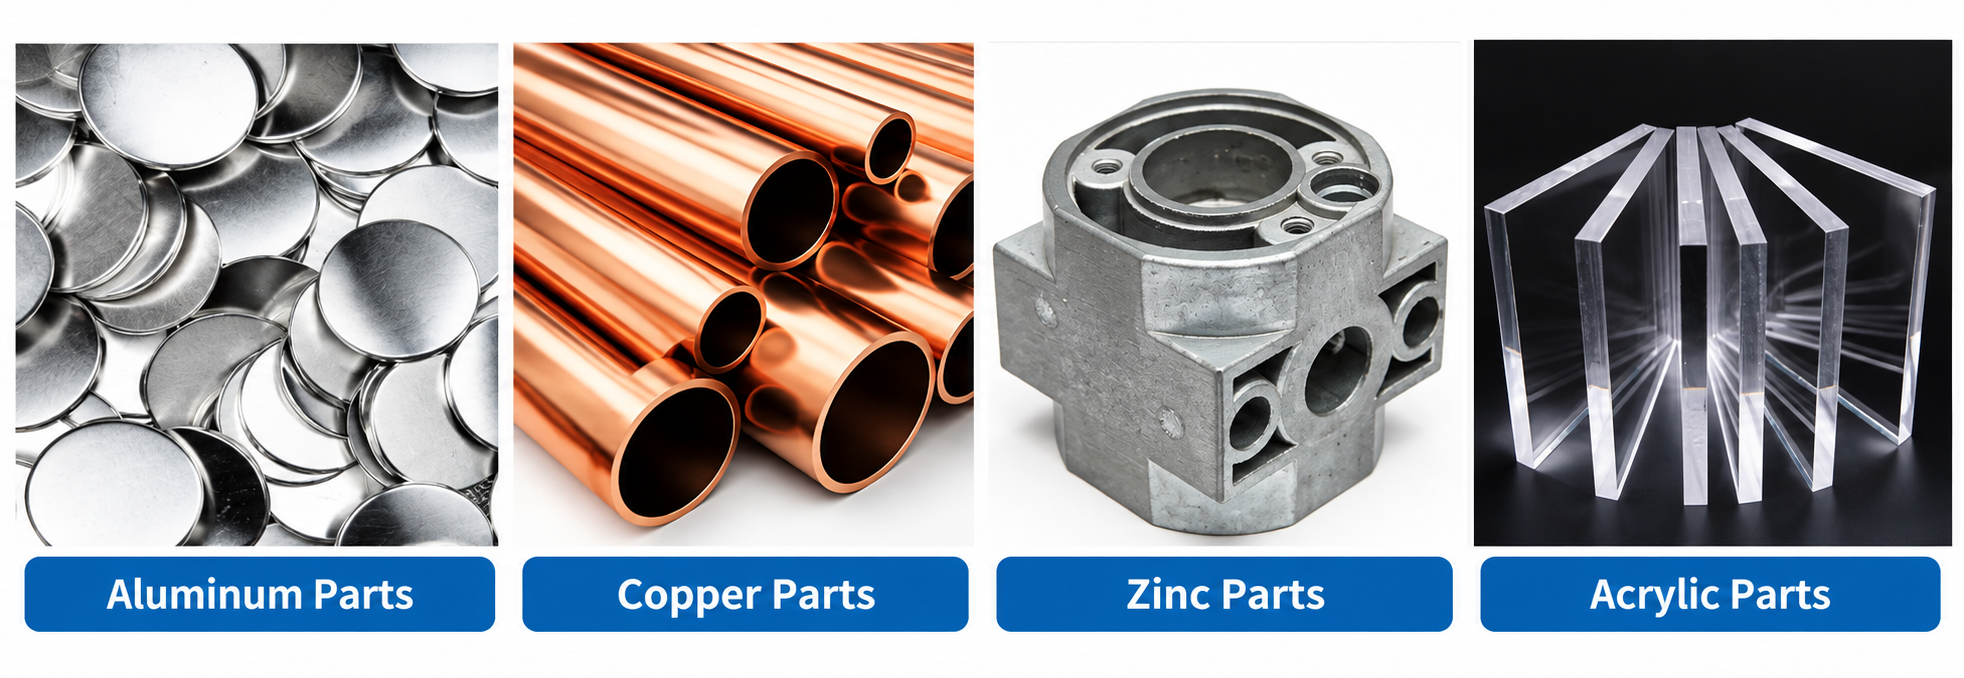
AlüminyumCopperZinc AlloysSelected Non-Ferrous Materials
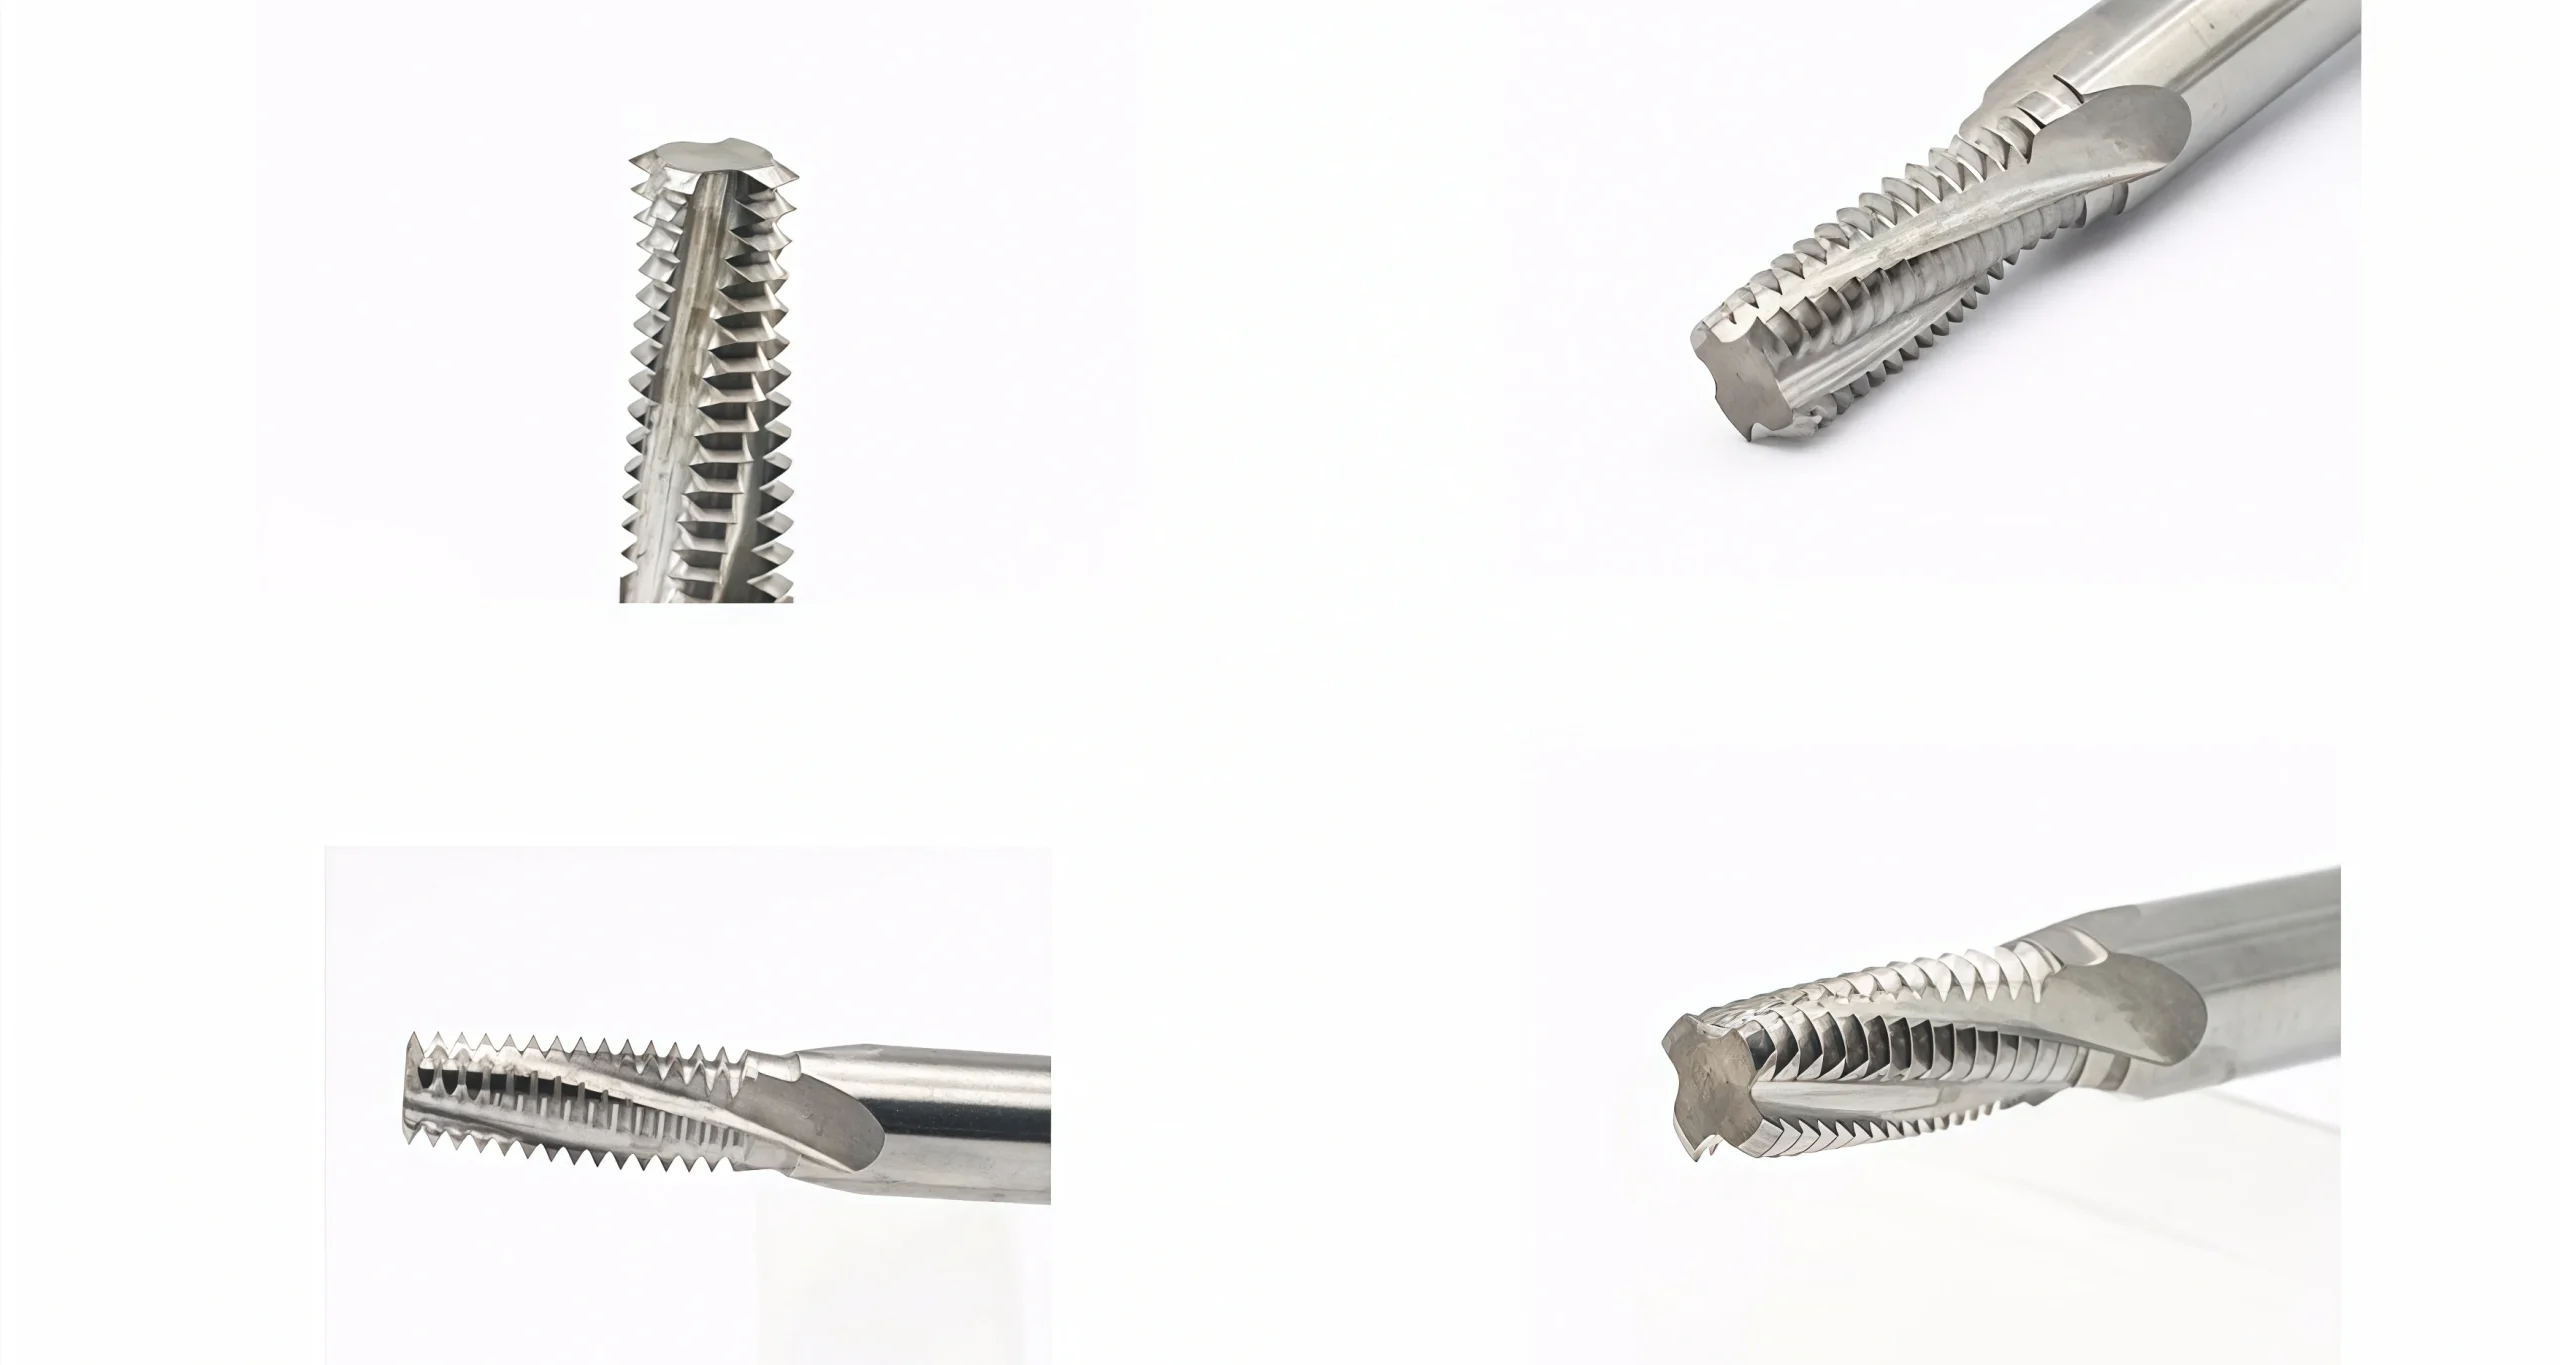
Tool Details
Close-up views of the carbide substrate, cutting edge and finished tool.
Solid Carbide Substrate
Solid carbide construction provides rigidity for precision CNC thread milling.

Keskin Kesici Kenar
Precision-ground cutting edges support smooth cutting and clean thread formation.
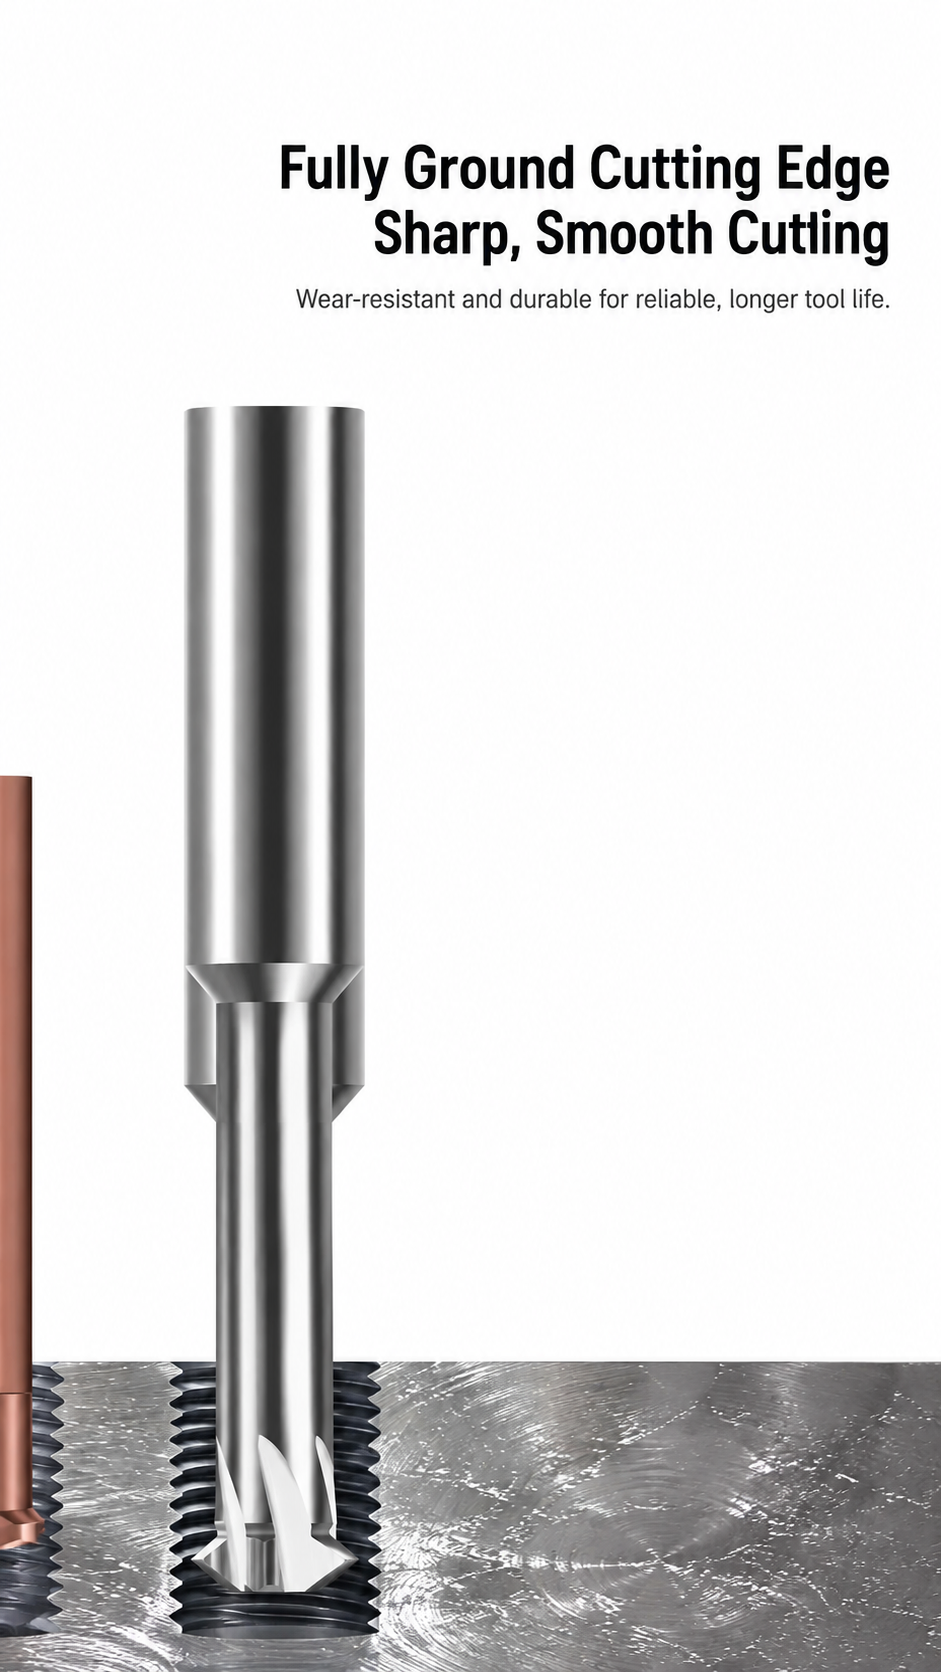
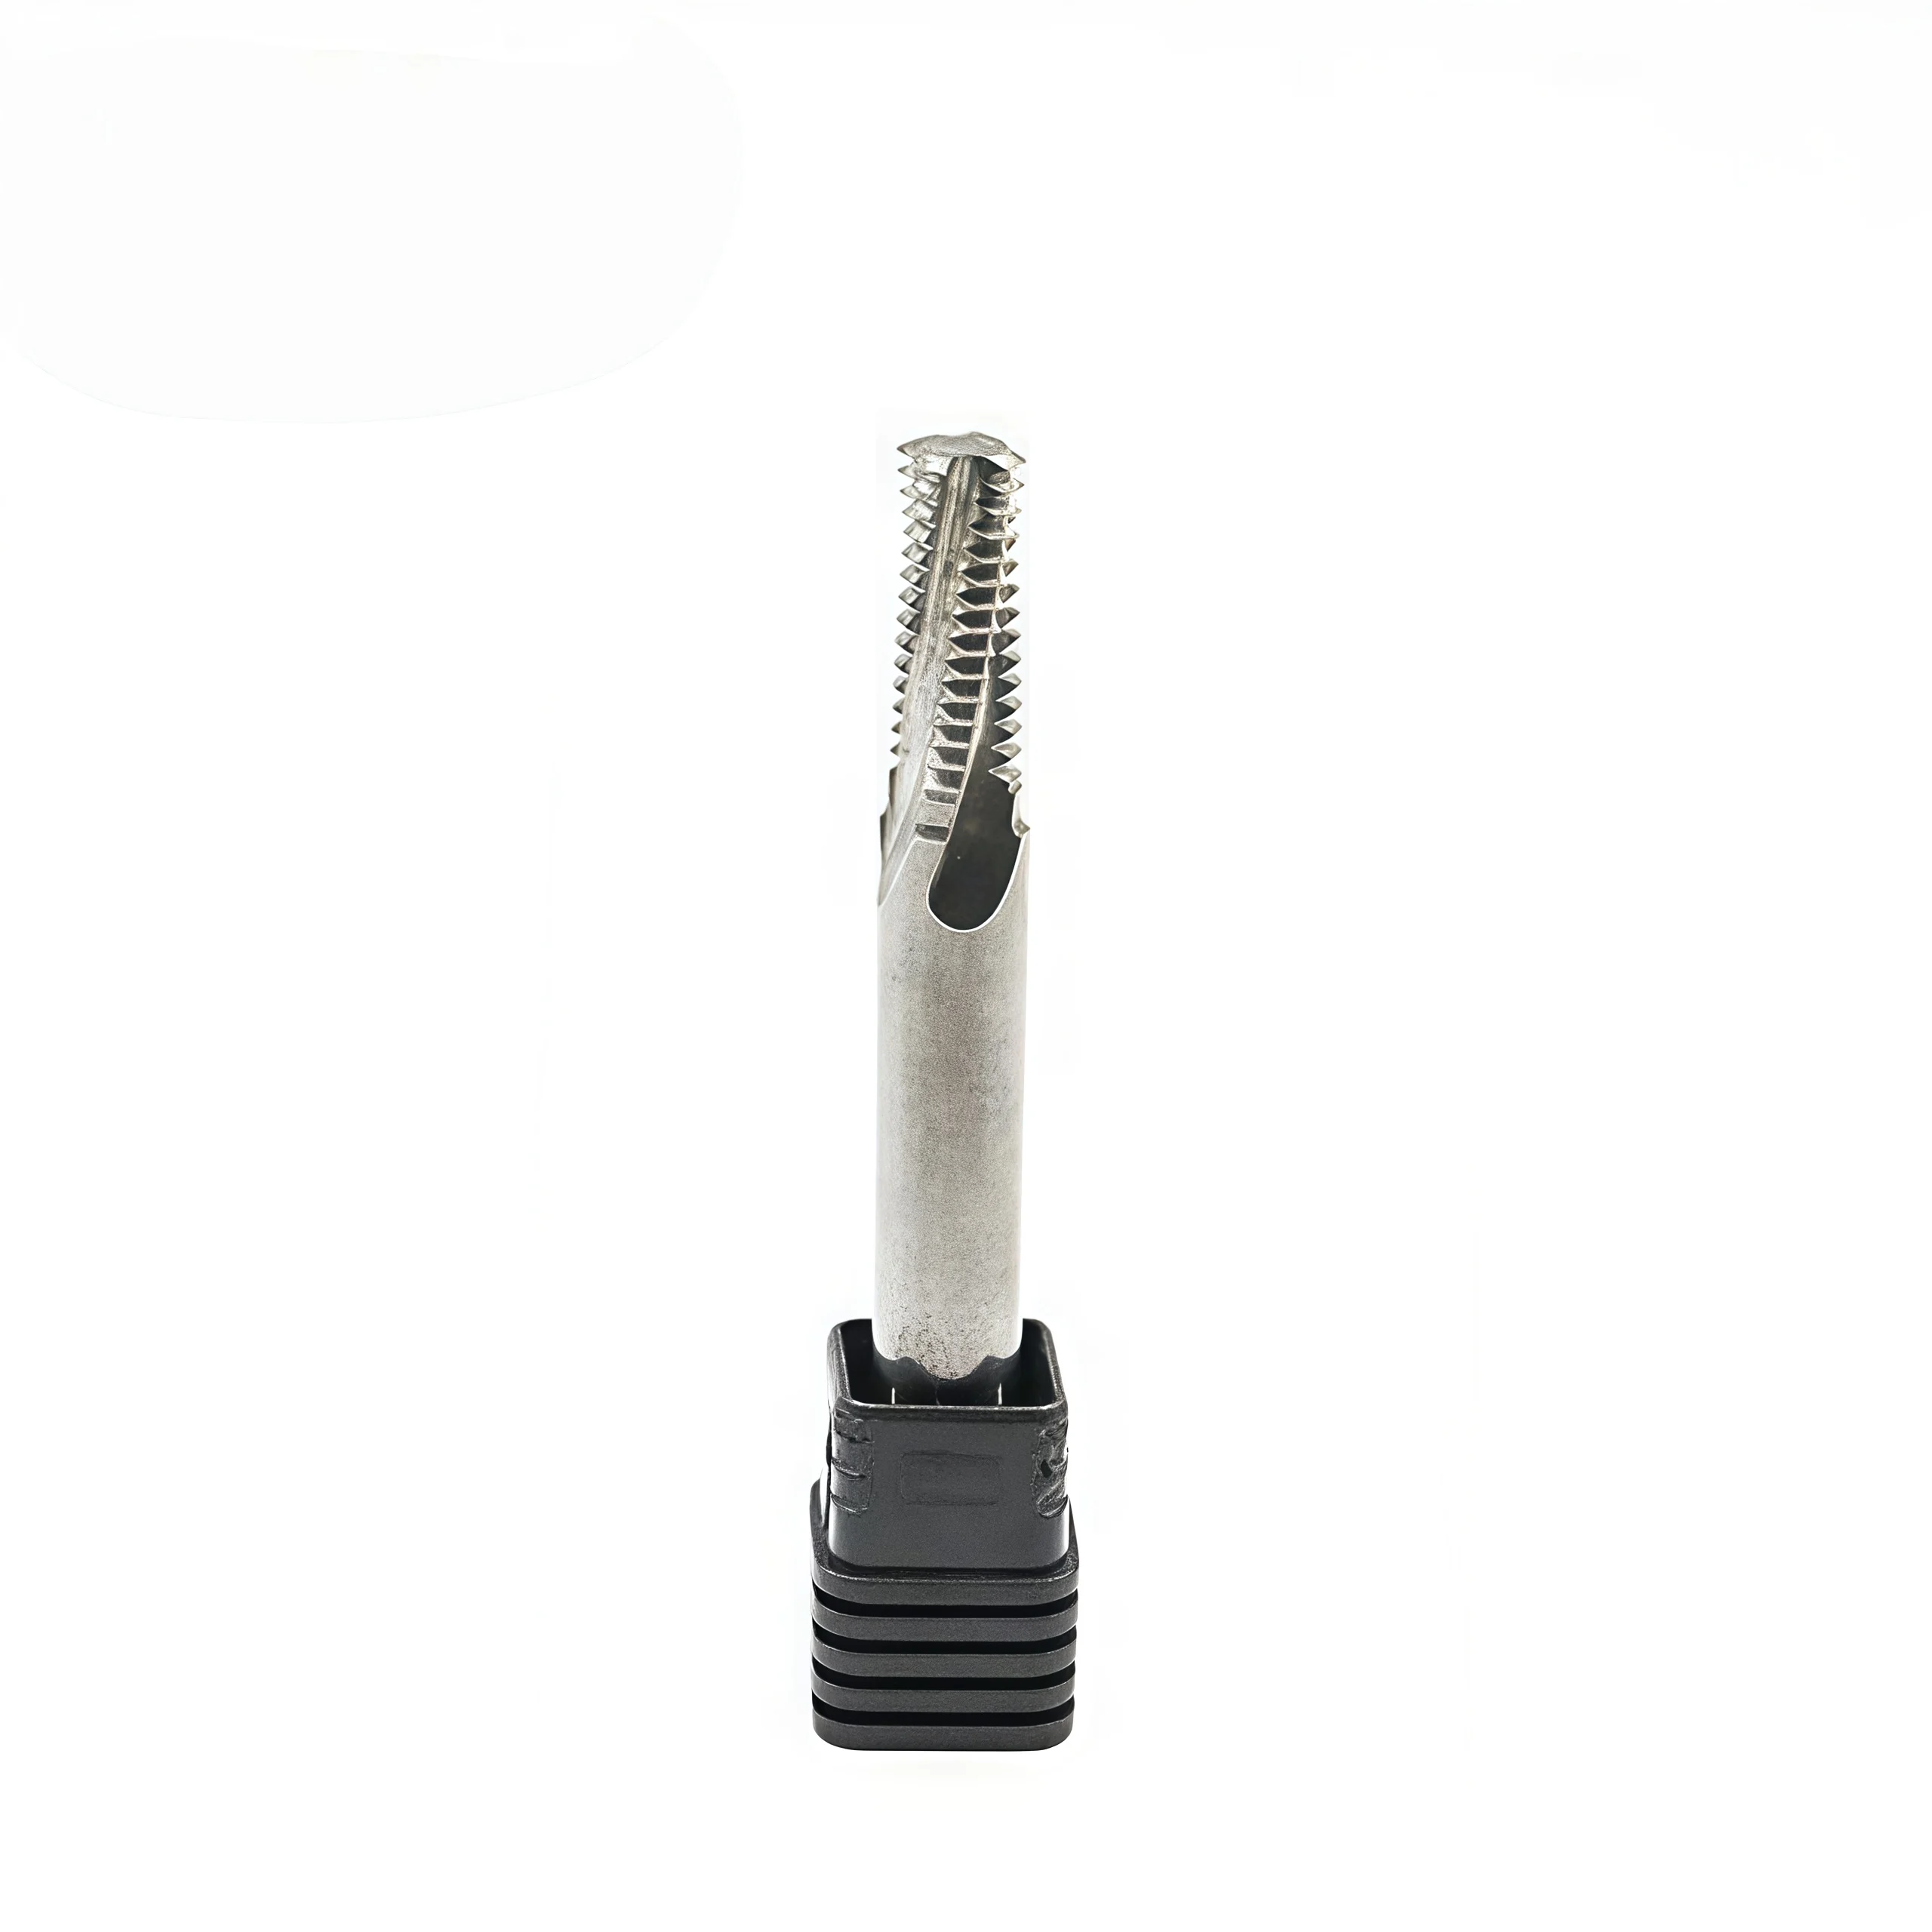
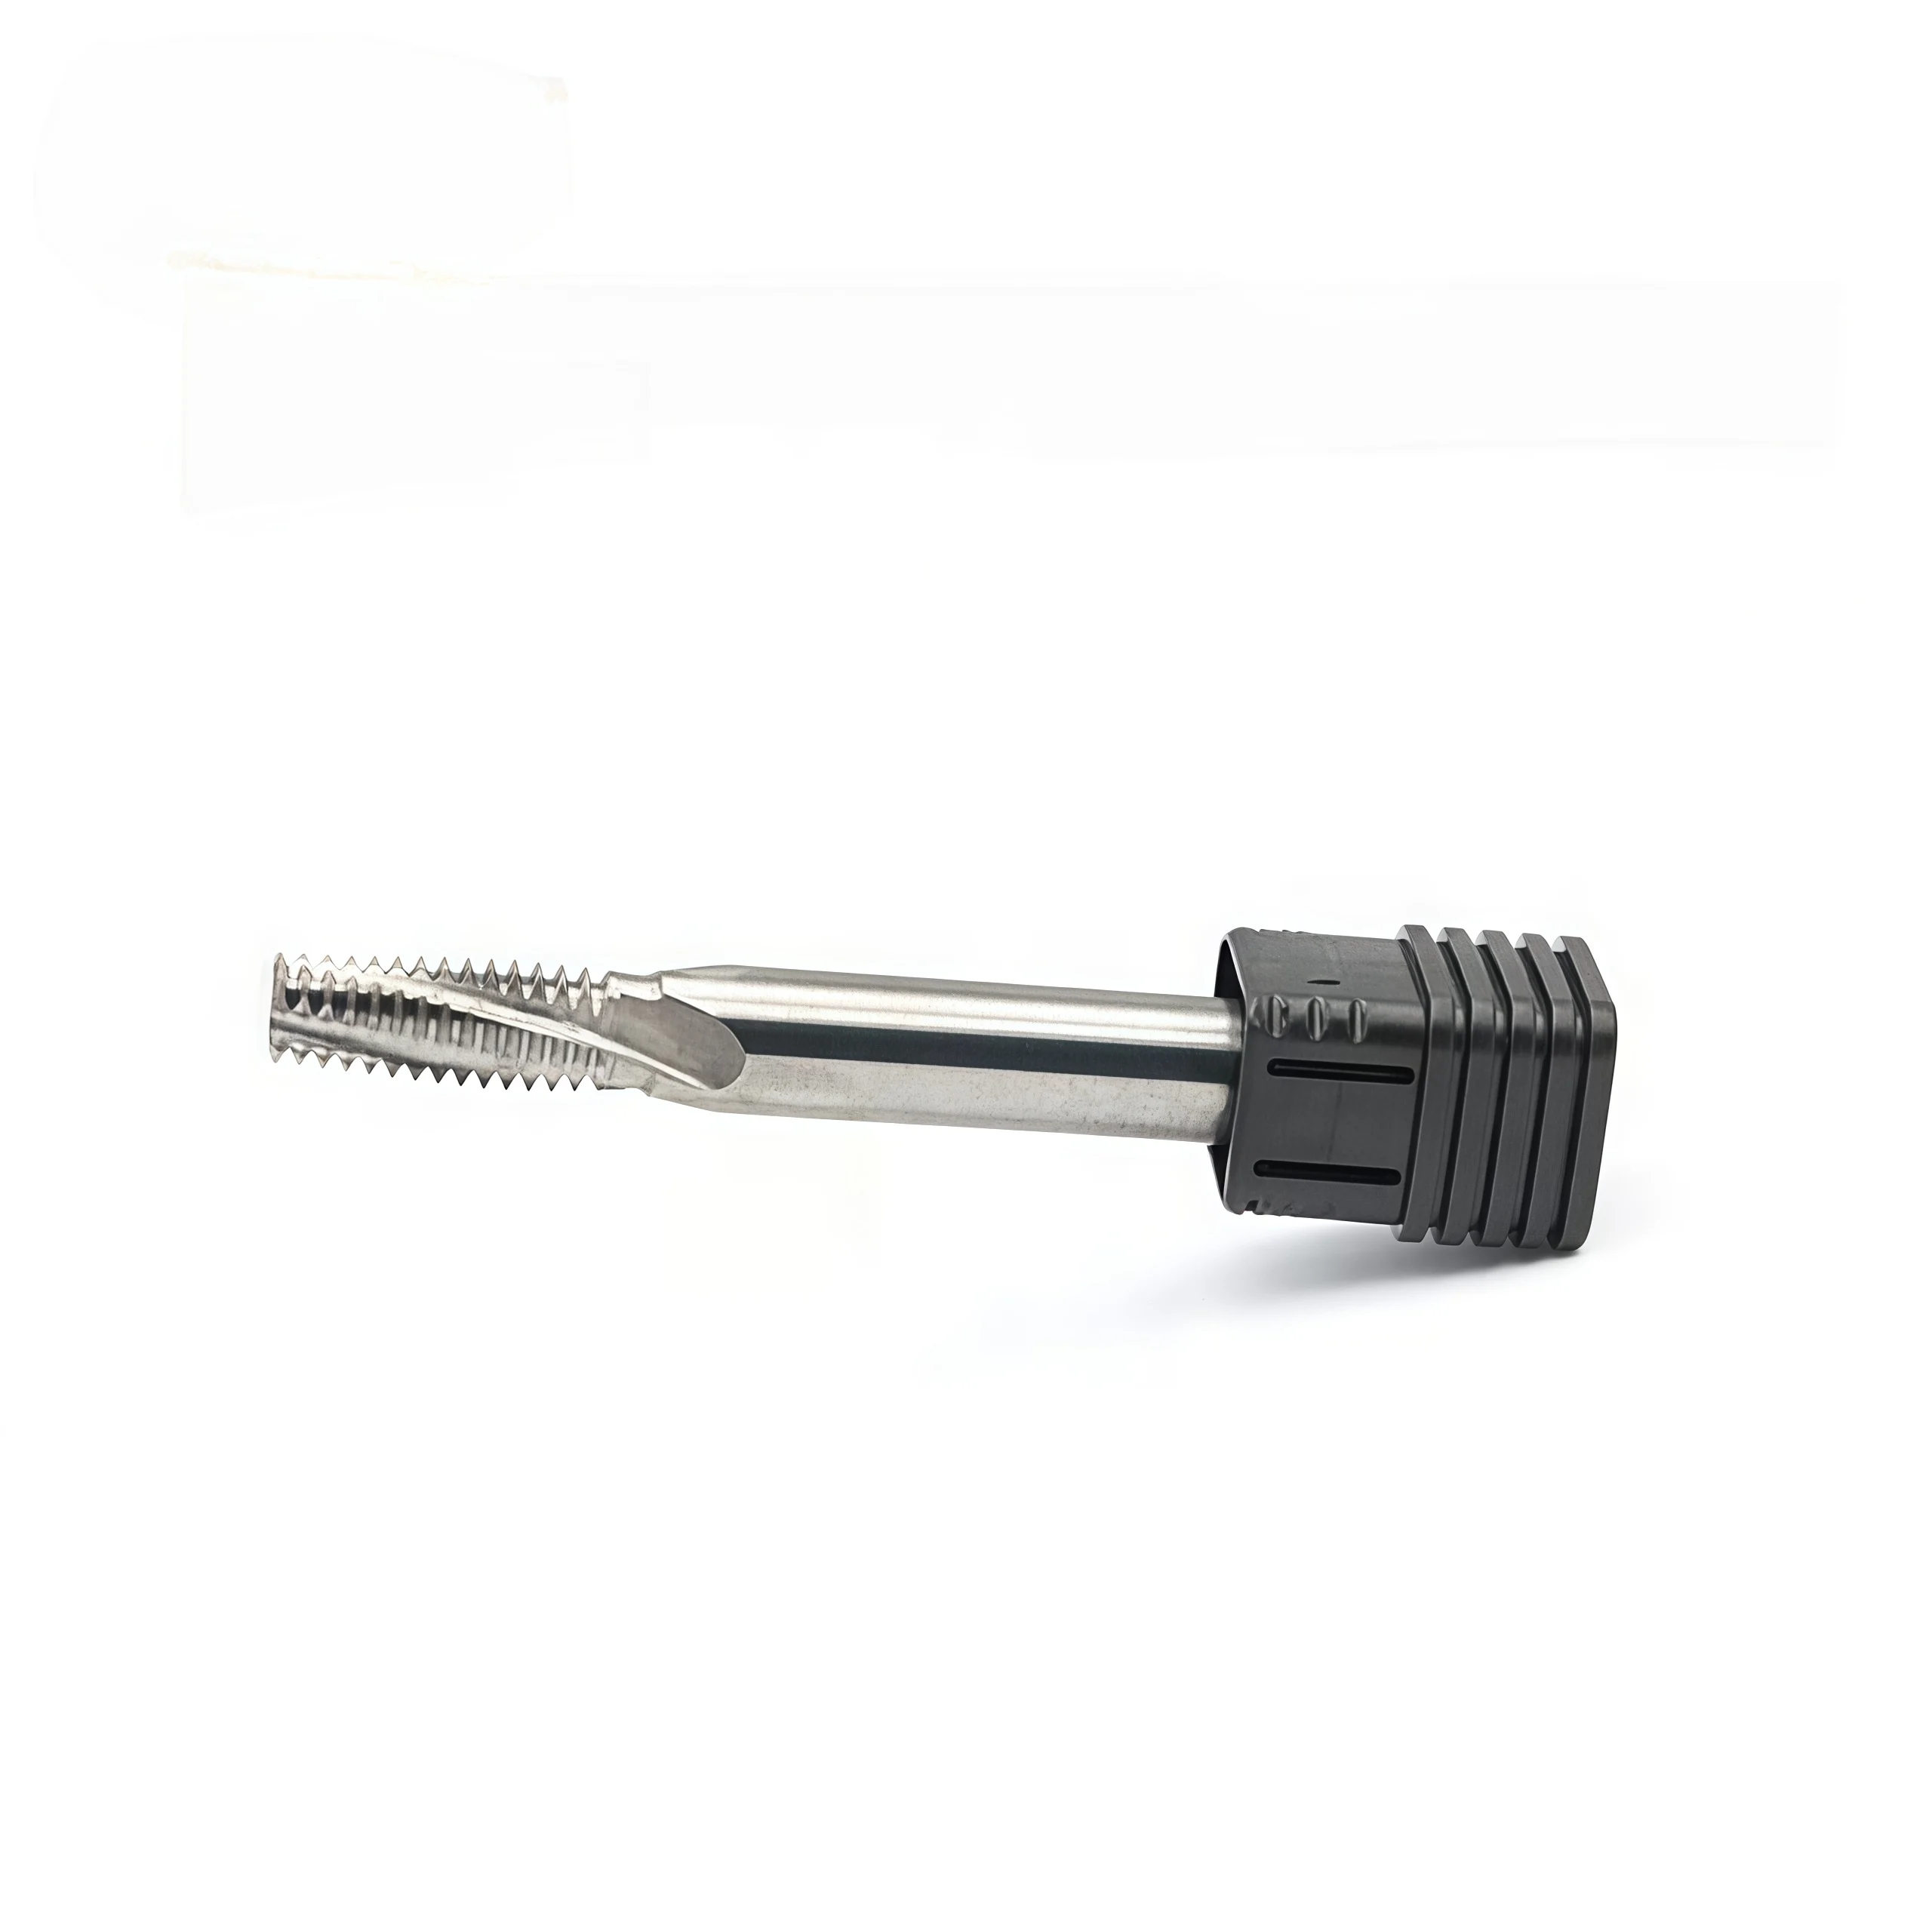
Finished Tool
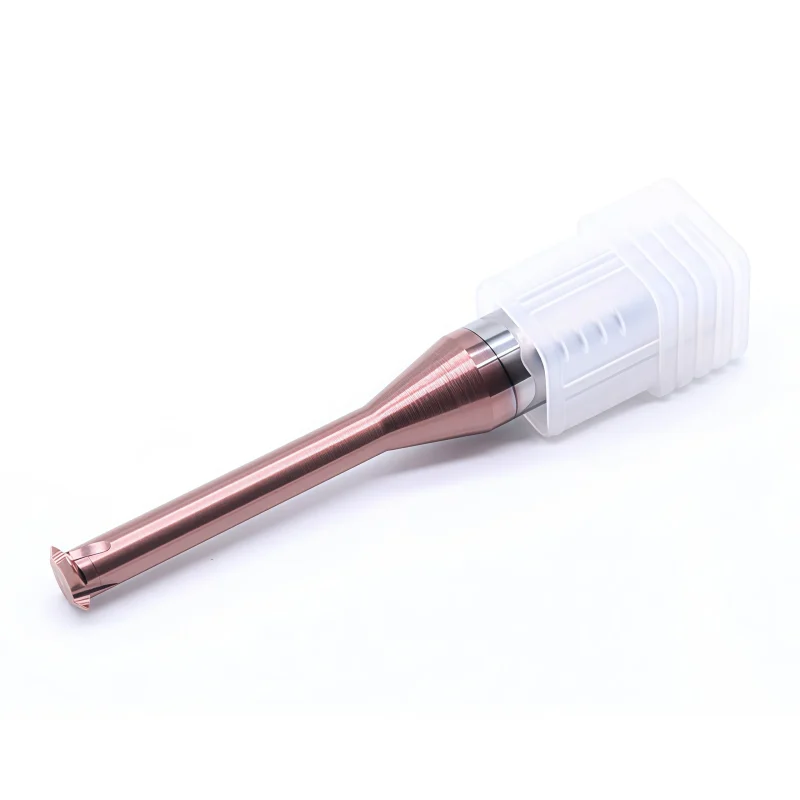
Product detail view for aluminum thread-milling applications.
Product Video
Product and machining reference for the aluminum solid carbide thread mill series.
Need help selecting the right thread style, pitch or cutter type? Read our Thread Mill Selection Guide.
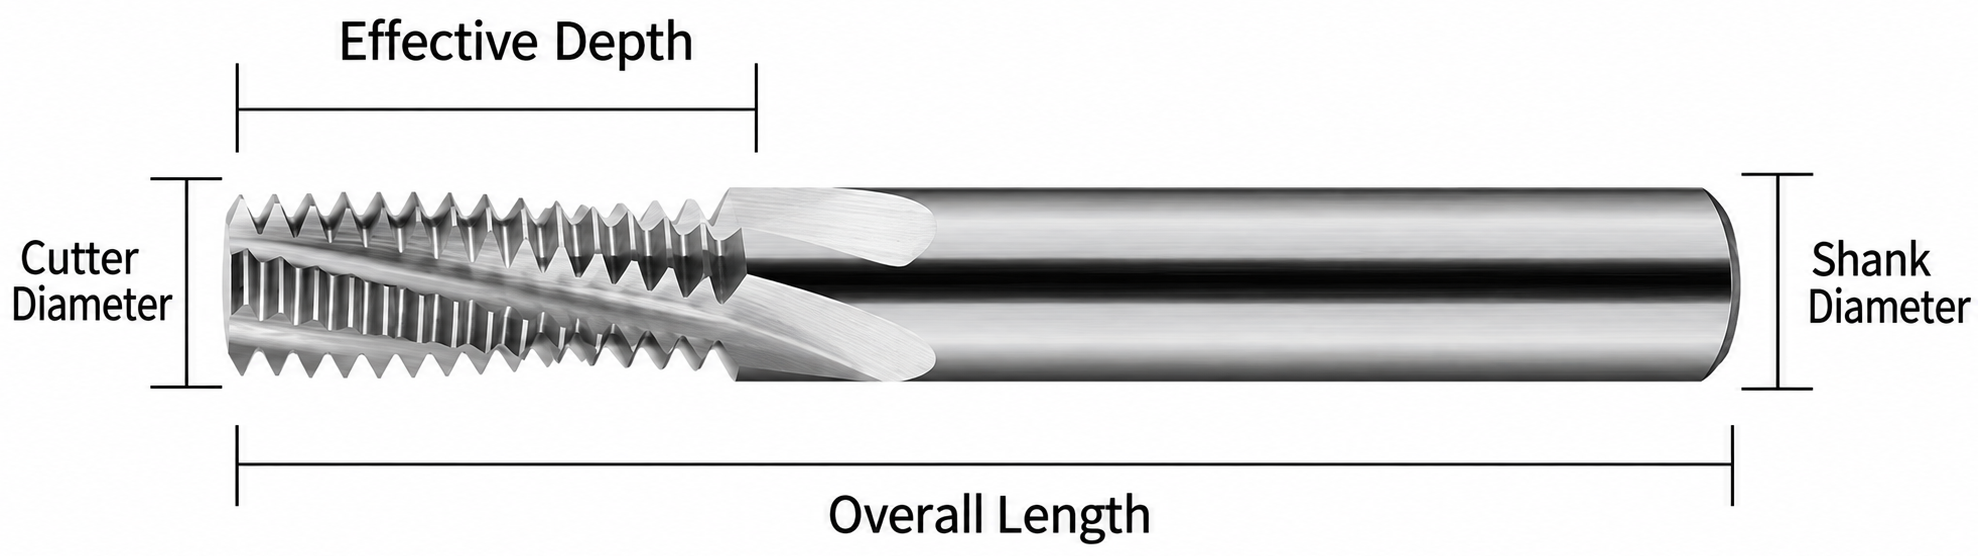
Tool Nomenclature & Dimensions
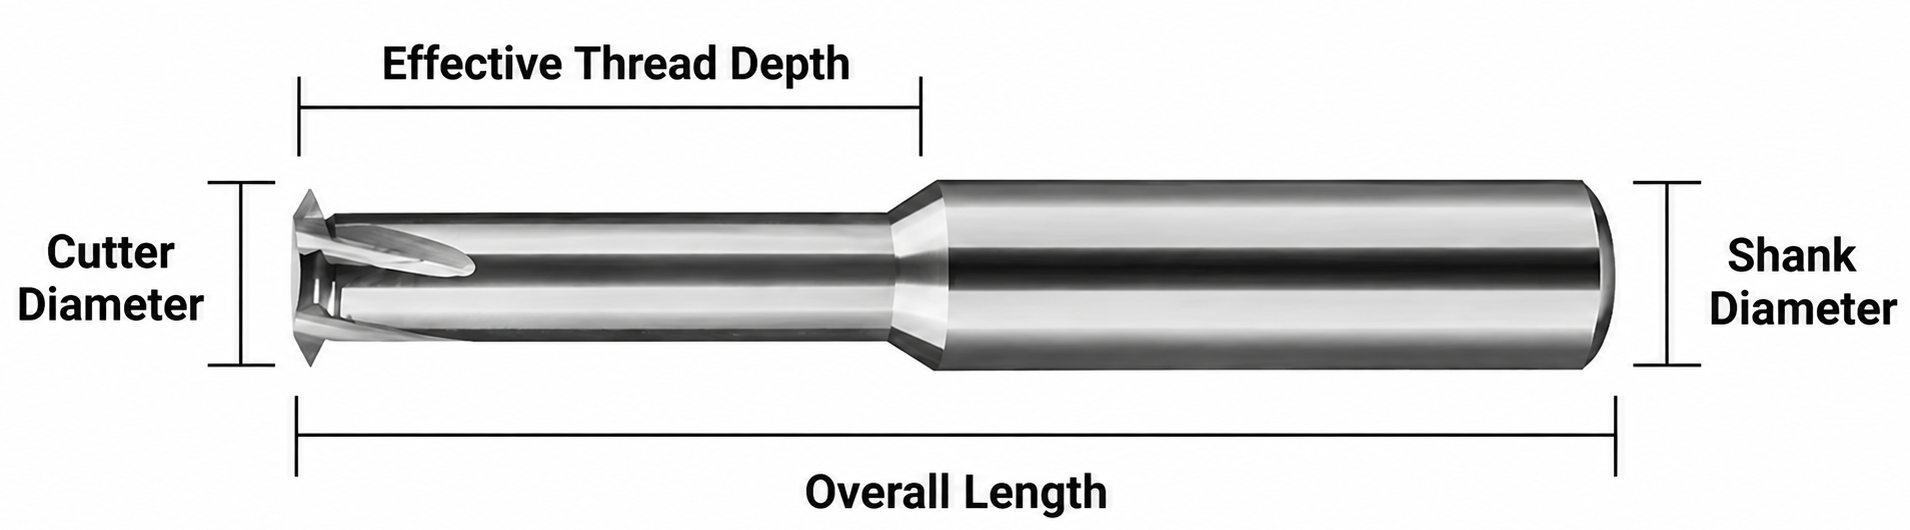
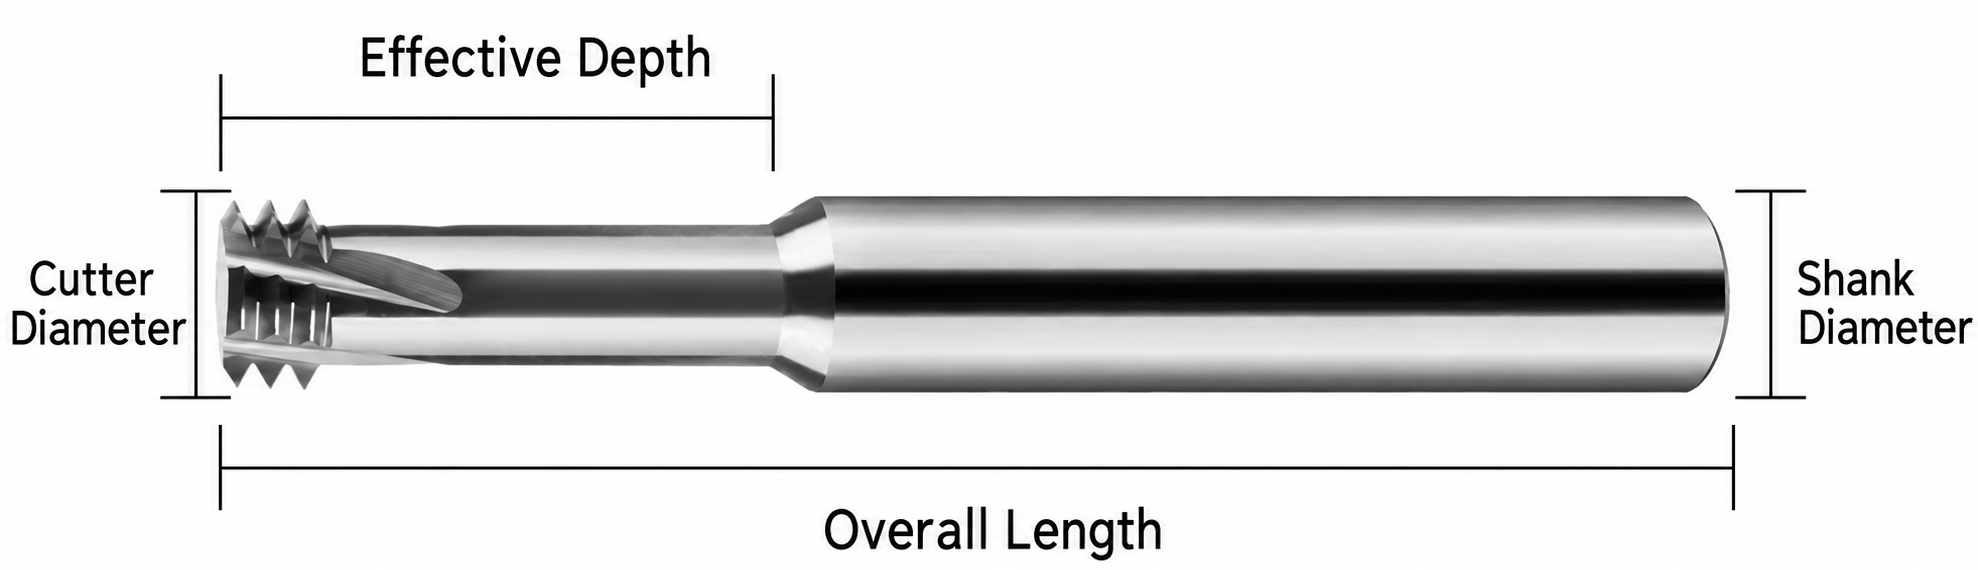
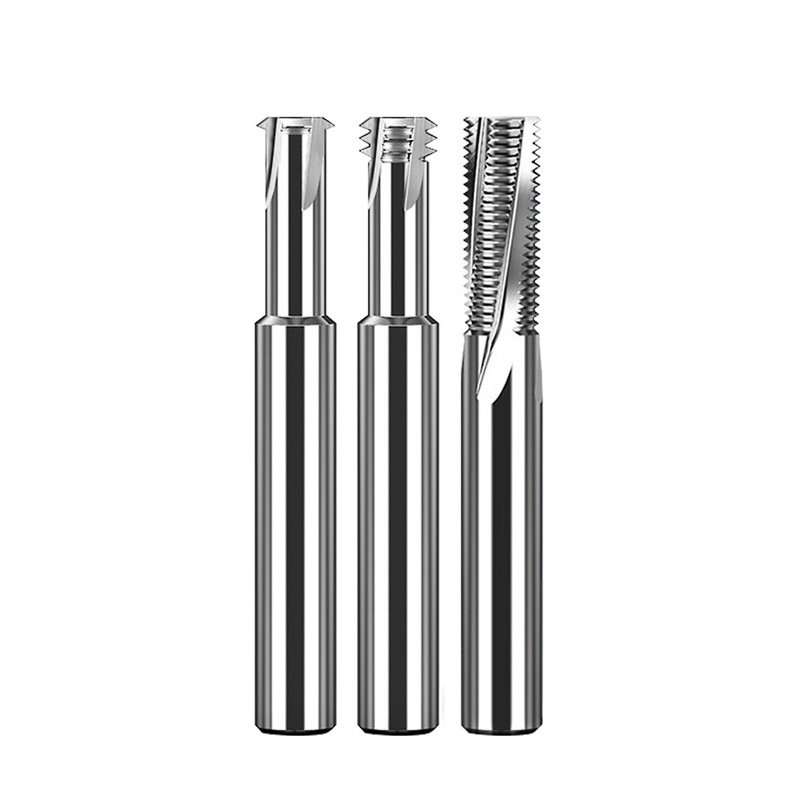
Reference dimensions for the aluminum solid carbide thread mill series. Single-form, 3-tooth and full-profile configurations use different cutting-section geometries while the main dimensional references remain based on cutting diameter, effective thread depth, shank diameter and overall length.
Single-Form
3-Tooth
Full-Profile
Technical Configuration
| PARAMETRE | SERIES CONFIGURATION |
|---|---|
| Alet Malzemesi | Solid Carbide |
| Thread Mill Configurations | Single-Form / 3-Tooth / Full-Profile |
| Uzunluk Seçenekleri | Standard / Extended |
| Thread Standard | Metric Series Shown in Size Matrix |
| Pitch Range | P0.15–P4.0 in Supplied Series |
| Cutting Diameter d | Ø0.43–Ø20 mm in Supplied Series |
| Effective Thread Depth L1 | 1.2–50 mm Depending on Configuration |
| Shank Diameter D | Ø4–Ø20 mm |
| Toplam Uzunluk L | 50 / 60 / 65 / 75 / 83 / 100 mm Depending on Series |
| Flute Count F | 3–6 Depending on Tool Size and Configuration |
| Birincil Uygulama | CNC Internal Thread Milling in Aluminum |
Standard Size Matrix
Open the required series below to review standard dimensions. Multiple configurations may be available for the same nominal thread size depending on pitch, effective depth, shank diameter and overall length.
Single-Form — Standard Length
Standard single-form metric thread mills with multiple pitch and diameter combinations.
| Thread Size | P | d | L1 | D | L | F | Clearance | Pre-Hole Dia. |
|---|---|---|---|---|---|---|---|---|
| M0.6×0.15 | 0.15 | 0.43 | 1.2 | 4 | 50 | 3 | 0.25 | 0.45 |
| M0.8×0.2 | 0.20 | 0.55 | 2 | 4 | 50 | 3 | 0.34 | 0.60 |
| M0.9×0.225 | 0.225 | 0.60 | 2 | 4 | 50 | 3 | 0.37 | 0.675 |
| M1×0.25 | 0.25 | 0.73 | 2.3 | 4 | 50 | 3 | 0.43 | 0.75 |
| M1.2×0.25 | 0.25 | 0.92 | 2.8 | 4 | 50 | 3 | 0.61 | 0.95 |
| M1.4×0.3 | 0.30 | 1.05 | 3.2 | 4 | 50 | 3 | 0.64 | 1.10 |
| M1.6×0.35 | 0.35 | 1.21 | 3.5 | 4 | 50 | 3 | 0.69 | 1.25 |
| M2×0.4 | 0.40 | 1.54 | 6 | 4 | 50 | 3 | 0.90 | 1.60 |
| M2.5×0.45 | 0.45 | 1.96 | 7.5 | 4 | 50 | 3 | 1.25 | 2.05 |
| M3×0.5 | 0.50 | 2.40 | 9 | 4 | 50 | 3 | 1.55 | 2.50 |
| M4×0.7 | 0.70 | 3.15 | 12 | 4 | 50 | 3 | 1.93 | 3.30 |
| M5×0.8 | 0.80 | 4.00 | 12 | 4 | 50 | 4 | 2.70 | 4.20 |
| M5×0.8 | 0.80 | 4.00 | 13 | 6 | 50 | 4 | 2.43 | 4.20 |
| M6×0.5 | 0.50 | 5.00 | 16 | 6 | 50 | 4 | 2.75 | 5.50 |
| M6×0.75 | 0.75 | 5.00 | 16 | 6 | 50 | 4 | 2.75 | 5.25 |
| M6×1.0 | 1.00 | 4.75 | 15 | 6 | 50 | 4 | 2.95 | 5.00 |
| M8×0.5 | 0.50 | 6.00 | 16 | 6 | 50 | 4 | 3.28 | 7.50 |
| M8×0.75 | 0.75 | 6.00 | 16 | 6 | 50 | 4 | 3.28 | 7.25 |
| M8×1.0 | 1.00 | 6.00 | 16 | 6 | 50 | 4 | 3.28 | 7.00 |
| M8×1.25 | 1.25 | 5.95 | 20 | 6 | 60 | 4 | 3.74 | 6.75 |
| M8×1.25 | 1.25 | 5.95 | 17.5 | 6 | 50 | 4 | 3.77 | 6.75 |
| M10×0.5 | 0.50 | 8.00 | 25 | 8 | 60 | 4 | 4.98 | 9.50 |
| M10×0.75 | 0.75 | 8.00 | 25 | 8 | 60 | 4 | 4.98 | 9.25 |
| M10×1.0 | 1.00 | 8.00 | 25 | 8 | 60 | 4 | 4.98 | 9.00 |
| M10×1.25 | 1.25 | 8.00 | 25 | 8 | 60 | 4 | 4.98 | 8.75 |
| M10×1.5 | 1.50 | 7.90 | 25 | 8 | 60 | 4 | 4.99 | 8.50 |
| M12×0.5 | 0.50 | 10.00 | 30 | 10 | 75 | 5 | 5.95 | 11.50 |
| M12×0.75 | 0.75 | 10.00 | 30 | 10 | 75 | 5 | 5.95 | 11.25 |
| M12×1.0 | 1.00 | 10.00 | 30 | 10 | 75 | 5 | 5.95 | 11.00 |
| M12×1.25 | 1.25 | 10.00 | 30 | 10 | 75 | 5 | 5.95 | 10.75 |
| M12×1.5 | 1.50 | 10.00 | 30 | 10 | 75 | 5 | 5.95 | 10.50 |
| M12×1.75 | 1.75 | 9.90 | 30 | 10 | 75 | 6 | 6.96 | 10.25 |
| M14×1.0 | 1.00 | 12.00 | 35 | 12 | 75 | 5 | 7.44 | 13.00 |
| M14×1.5 | 1.50 | 12.00 | 35 | 12 | 75 | 5 | 7.44 | 12.50 |
| M14×2.0 | 2.00 | 9.90 | 30 | 10 | 75 | 6 | 6.95 | 12.00 |
| M16×1.0 | 1.00 | 12.00 | 35 | 12 | 75 | 5 | 7.44 | 15.00 |
| M16×1.5 | 1.50 | 12.00 | 35 | 12 | 75 | 5 | 7.44 | 14.50 |
| M16×2.0 | 2.00 | 11.90 | 35 | 12 | 75 | 6 | 8.40 | 14.00 |
| M18×2.5 | 2.50 | 14.00 | 40 | 14 | 100 | 5/6 | 8.90 | 15.50 |
| M20×2.5 | 2.50 | 16.00 | 45 | 16 | 100 | 5/6 | 9.74 | 17.50 |
| M30×3.5 | 3.50 | 16.00 | 45 | 16 | 100 | 5 | 10.06 | 26.50 |
| M24×3.0 | 3.00 | 16.00 | 45 | 16 | 100 | 5/6 | 9.74 | 21.00 |
| M36×4.0 | 4.00 | 20.00 | 50 | 20 | 100 | 6 | 12.10 | 32.00 |
Single-Form — Extended Length
Extended 75 mm and 100 mm configurations for deeper or restricted-access internal threads.
| Thread Size | P | d | L1 | D | L | F | Pre-Hole Dia. | Clearance |
|---|---|---|---|---|---|---|---|---|
| M1.6×0.35 | 0.35 | 1.21 | 3.5 | 4 | 75 | 3 | 1.25 | 0.72 |
| M2×0.4 | 0.40 | 1.54 | 6 | 4 | 75 | 3 | 1.60 | 0.92 |
| M2×0.4 | 0.40 | 1.54 | 6 | 4 | 100 | 3 | 1.60 | 0.89 |
| M2.5×0.45 | 0.45 | 1.96 | 7.5 | 4 | 75 | 3 | 2.05 | 1.19 |
| M2.5×0.45 | 0.45 | 1.96 | 7.5 | 4 | 100 | 3 | 2.05 | 1.25 |
| M3×0.5 | 0.50 | 2.40 | 9 | 4 | 75 | 3 | 2.50 | 1.58 |
| M3×0.5 | 0.50 | 2.40 | 9 | 4 | 100 | 3 | 2.50 | 1.61 |
| M4×0.7 | 0.70 | 3.15 | 12 | 4 | 75 | 4 | 3.30 | 2.11 |
| M4×0.7 | 0.70 | 3.15 | 12 | 4 | 100 | 4 | 3.30 | 2.13 |
| M5×0.8 | 0.80 | 4.00 | 15 | 6 | 75 | 4 | 4.20 | 2.92 |
| M5×0.8 | 0.80 | 4.00 | 15 | 6 | 100 | 4 | 4.20 | 2.92 |
| M6×1.0 | 1.00 | 4.75 | 18 | 6 | 75 | 4 | 5.00 | 3.32 |
| M6×1.0 | 1.00 | 4.75 | 18 | 6 | 100 | 4 | 5.00 | 3.02 |
| M8×1.25 | 1.25 | 5.95 | 20 | 6 | 75 | 4 | 6.75 | 4.08 |
| M8×1.25 | 1.25 | 5.95 | 25 | 6 | 100 | 4 | 6.75 | 4.11 |
| M10×1.5 | 1.50 | 7.90 | 30 | 8 | 75 | 6 | 8.50 | 5.47 |
| M10×1.5 | 1.50 | 7.90 | 30 | 8 | 100 | 6 | 8.50 | 5.55 |
| M12×1.75 | 1.75 | 9.90 | 35 | 10 | 100 | 6 | 10.25 | 7.18 |
| M16×2.0 | 2.00 | 11.90 | 35 | 12 | 100 | 6 | 14.00 | 8.56 |
3-Tooth — Standard Length
Three thread-form cutting teeth for a balance between thread-depth flexibility and machining efficiency.
| Thread Size | P | d | L1 | F | D | L | Clearance | Pre-Hole Dia. |
|---|---|---|---|---|---|---|---|---|
| M1×0.25 | 0.25 | 0.73 | 2.3 | 3 | 4 | 50 | 0.40 | 0.75 |
| M1.2×0.25 | 0.25 | 0.92 | 3.3 | 3 | 4 | 50 | 0.55 | 0.95 |
| M1.4×0.3 | 0.30 | 1.05 | 3.2 | 3 | 4 | 50 | 0.60 | 1.10 |
| M1.6×0.35 | 0.35 | 1.21 | 3.5 | 3 | 4 | 50 | 0.63 | 1.25 |
| M1.8×0.35 | 0.35 | 1.40 | 4 | 3 | 4 | 50 | 0.93 | 1.45 |
| M2×0.4 | 0.40 | 1.54 | 4.5 | 3 | 4 | 50 | 0.88 | 1.60 |
| M2.2×0.45 | 0.45 | 1.65 | 5 | 3 | 4 | 50 | 0.94 | 1.75 |
| M2.5×0.45 | 0.45 | 1.96 | 5.5 | 3 | 4 | 50 | 1.15 | 2.05 |
| M3×0.5 | 0.50 | 2.42 | 7 | 3 | 4 | 50 | 1.54 | 2.50 |
| M3.5×0.6 | 0.60 | 2.75 | 9 | 3 | 4 | 50 | 1.90 | 2.90 |
| M4×0.5 | 0.50 | 3.40 | 8 | 3 | 4 | 50 | 2.47 | 3.50 |
| M4×0.7 | 0.70 | 3.15 | 10 | 3 | 4 | 50 | 1.97 | 3.30 |
| M4.5×0.75 | 0.75 | 3.50 | 11 | 3 | 4 | 50 | 2.50 | 3.75 |
| M5×0.5 | 0.50 | 3.90 | 8 | 3 | 4 | 50 | 2.98 | 4.50 |
| M5×0.75 | 0.75 | 3.90 | 8 | 3 | 4 | 50 | 2.47 | 4.25 |
| M5×0.8 | 0.80 | 4.00 | 12 | 3 | 6 | 50 | 2.54 | 4.20 |
| M5×0.8 | 0.80 | 3.95 | 12 | 3 | 4 | 50 | 2.64 | 4.20 |
| M6×0.5 | 0.50 | 4.80 | 13 | 3 | 6 | 50 | 4.20 | 5.50 |
| M6×0.75 | 0.75 | 5.00 | 13 | 3 | 6 | 50 | 3.77 | 5.25 |
| M6×1.0 | 1.00 | 4.75 | 13 | 3 | 6 | 50 | 3.03 | 5.00 |
| M8×0.75 | 0.75 | 5.95 | 20 | 3 | 6 | 60 | 3.79 | 7.25 |
| M8×1.0 | 1.00 | 5.90 | 20 | 3 | 6 | 60 | 4.50 | 6.00 |
| M8×0.5 | 0.50 | 5.95 | 16 | 4 | 6 | 50 | 5.06 | 7.50 |
| M8×1.25 | 1.25 | 5.95 | 20 | 3 | 6 | 60 | 3.81 | 6.75 |
| M10×1.0 | 1.00 | 7.90 | 21 | 4 | 8 | 60 | 6.50 | 9.00 |
| M10×0.5 | 0.50 | 7.95 | 25 | 4 | 8 | 60 | 7.00 | 9.50 |
| M10×0.75 | 0.75 | 7.95 | 25 | 4 | 8 | 60 | 6.80 | 9.25 |
| M10×1.25 | 1.25 | 7.95 | 21 | 4 | 8 | 60 | 6.15 | 8.75 |
| M10×1.5 | 1.50 | 7.90 | 22 | 4 | 8 | 60 | 5.82 | 8.50 |
| M12×1.0 | 1.00 | 9.90 | 30 | 4 | 10 | 75 | 8.36 | 11.00 |
| M12×1.5 | 1.50 | 9.90 | 30 | 4 | 10 | 75 | 7.80 | 10.50 |
| M12×1.25 | 1.25 | 9.90 | 30 | 4 | 10 | 75 | 8.40 | 10.75 |
| M12×1.75 | 1.75 | 9.90 | 28 | 4 | 10 | 75 | 7.59 | 10.25 |
| M14×2.0 | 2.00 | 9.90 | 28 | 4 | 10 | 75 | 6.99 | 12.00 |
| M16×1.5 | 1.50 | 11.90 | 35 | 4 | 12 | 75 | 9.72 | 14.50 |
| M16×2.0 | 2.00 | 11.90 | 35 | 4 | 12 | 75 | 8.99 | 14.00 |
| M18×2.5 | 2.50 | 13.90 | 40 | 5 | 14 | 83 | 10.34 | 15.50 |
| M20×2.5 | 2.50 | 15.90 | 50 | 6 | 16 | 100 | 12.36 | 17.50 |
| M24×3.0 | 3.00 | 15.90 | 50 | 6 | 16 | 100 | 11.77 | 21.00 |
| M30×3.5 | 3.50 | 15.90 | 50 | 6 | 16 | 100 | 11.15 | 20.50 |
3-Tooth — Extended Length
Extended 75 mm and 100 mm configurations for deeper thread locations and restricted machining access.
| Thread Size | P | d | L1 | F | D | L | Clearance | Pre-Hole Dia. |
|---|---|---|---|---|---|---|---|---|
| M1×0.25 | 0.25 | 0.73 | 2.3 | 3 | 4 | 75 | 0.34 | 0.75 |
| M1.4×0.3 | 0.30 | 1.05 | 3.2 | 3 | 4 | 75 | 0.64 | 1.10 |
| M1.6×0.35 | 0.35 | 1.21 | 5 | 3 | 4 | 100 | 0.68 | 1.25 |
| M2×0.4 | 0.40 | 1.54 | 6 | 3 | 4 | 75 | 1.03 | 1.60 |
| M2×0.4 | 0.40 | 1.54 | 6 | 3 | 4 | 100 | 0.92 | 1.60 |
| M2.5×0.45 | 0.45 | 1.96 | 7.5 | 3 | 4 | 75 | 1.28 | 2.05 |
| M2.5×0.45 | 0.45 | 1.96 | 7.5 | 3 | 4 | 100 | 1.24 | 2.05 |
| M3×0.5 | 0.50 | 2.40 | 9 | 3 | 4 | 75 | 1.50 | 2.50 |
| M3×0.5 | 0.50 | 2.40 | 9 | 3 | 4 | 100 | 1.58 | 2.50 |
| M4×0.7 | 0.70 | 3.15 | 12 | 3 | 4 | 75 | 2.08 | 3.30 |
| M4×0.7 | 0.70 | 3.15 | 12 | 3 | 4 | 100 | 2.10 | 3.30 |
| M5×0.8 | 0.80 | 4.00 | 15 | 3 | 6 | 75 | 2.89 | 4.20 |
| M5×0.8 | 0.80 | 4.00 | 15 | 3 | 6 | 100 | 2.77 | 4.20 |
| M6×1.0 | 1.00 | 4.75 | 18 | 3 | 6 | 75 | 3.46 | 5.00 |
| M6×1.0 | 1.00 | 4.75 | 18 | 3 | 6 | 100 | 3.30 | 5.00 |
| M8×1.25 | 1.25 | 5.90 | 25 | 3 | 6 | 75 | 4.18 | 6.75 |
| M8×1.25 | 1.25 | 5.90 | 25 | 3 | 6 | 100 | 4.11 | 6.75 |
| M10×1.5 | 1.50 | 7.90 | 30 | 4 | 8 | 75 | 5.83 | 8.50 |
| M10×1.5 | 1.50 | 7.90 | 30 | 4 | 8 | 100 | 5.83 | 8.50 |
| M12×1.75 | 1.75 | 9.90 | 35 | 4 | 10 | 100 | 8.50 | 10.25 |
| M16×2.0 | 2.00 | 11.90 | 35 | 4 | 12 | 100 | 9.07 | 14.00 |
Full-Profile — Standard Series
Pitch-specific multi-tooth configurations for efficient repeat-production internal thread milling.
| Thread Size | P | d | D | L1 | L | F | Pre-Hole Dia. |
|---|---|---|---|---|---|---|---|
| M1.6×0.35 | 0.35 | 1.20 | 4 | 3.5 | 50 | 3 | 1.25 |
| M2×0.4 | 0.40 | 1.54 | 4 | 6 | 50 | 3 | 1.60 |
| M2.5×0.45 | 0.45 | 1.96 | 4 | 6 | 50 | 3 | 2.05 |
| M3×0.5 | 0.50 | 2.40 | 4 | 7.5 | 50 | 3 | 2.50 |
| M3.5×0.6 | 0.60 | 2.75 | 4 | 8.5 | 50 | 3 | 2.90 |
| M4×0.5 | 0.50 | 3.00 | 4 | 8 | 50 | 3 | 3.50 |
| M4×0.7 | 0.70 | 3.15 | 4 | 12 | 50 | 3 | 3.30 |
| M4.5×0.75 | 0.75 | 3.40 | 4 | 9 | 50 | 3 | 3.75 |
| M5×0.5 | 0.50 | 3.90 | 4 | 12 | 50 | 3 | 4.50 |
| M5×0.8 | 0.80 | 3.95 | 4 | 12 | 50 | 3 | 4.20 |
| M5×0.8 | 0.80 | 3.90 | 6 | 13 | 50 | 3 | 4.20 |
| M6×0.5 | 0.50 | 4.80 | 6 | 13 | 50 | 3 | 5.50 |
| M6×0.75 | 0.75 | 3.90 | 4 | 12 | 50 | 3 | 5.25 |
| M6×0.75 | 0.75 | 5.00 | 6 | 17 | 60 | 3 | 5.25 |
| M6×1.0 | 1.00 | 3.95 | 4 | 12 | 50 | 3 | 5.00 |
| M6×1.0 | 1.00 | 4.75 | 6 | 15 | 50 | 3 | 5.00 |
| M8×0.5 | 0.50 | 5.90 | 6 | 16 | 60 | 3 | 7.50 |
| M8×0.75 | 0.75 | 5.95 | 6 | 18 | 60 | 3 | 7.25 |
| M8×1.0 | 1.00 | 5.95 | 6 | 15 | 60 | 3 | 7.00 |
| M8×1.25 | 1.25 | 5.90 | 6 | 20 | 60 | 3 | 6.75 |
| M10×0.5 | 0.50 | 7.90 | 8 | 20 | 65 | 4 | 9.50 |
| M10×0.75 | 0.75 | 7.90 | 8 | 22 | 65 | 4 | 9.25 |
| M10×1.0 | 1.00 | 7.95 | 8 | 22 | 65 | 4 | 9.00 |
| M10×1.25 | 1.25 | 7.90 | 8 | 20 | 65 | 3 | 8.75 |
| M10×1.5 | 1.50 | 7.70 | 8 | 22 | 65 | 4 | 8.50 |
| M12×0.5 | 0.50 | 9.95 | 10 | 25 | 75 | 4 | 11.50 |
| M12×0.75 | 0.75 | 9.95 | 10 | 20 | 75 | 4 | 11.25 |
| M12×1.0 | 1.00 | 9.90 | 10 | 28 | 75 | 4 | 11.00 |
| M12×1.25 | 1.25 | 9.90 | 10 | 25 | 75 | 4 | 10.75 |
| M12×1.5 | 1.50 | 9.40 | 10 | 24 | 75 | 4 | 10.50 |
| M12×1.75 | 1.75 | 9.50 | 10 | 25 | 75 | 4 | 10.25 |
| M14×0.5 | 0.50 | 11.90 | 12 | 30 | 75 | 4 | 13.50 |
| M14×1.0 | 1.00 | 11.90 | 12 | 30 | 75 | 4 | 13.00 |
| M14×1.5 | 1.50 | 9.90 | 10 | 25 | 75 | 4 | 12.50 |
| M14×1.5 | 1.50 | 11.20 | 12 | 30 | 75 | 4 | 12.50 |
| M14×2.0 | 2.00 | 9.90 | 10 | 30 | 75 | 4 | 12.00 |
| M14×2.0 | 2.00 | 11.20 | 12 | 30 | 75 | 4 | 12.00 |
| M16×1.5 | 1.50 | 12.00 | 12 | 30 | 75 | 4 | 14.50 |
| M16×1.5 | 1.50 | 13.90 | 14 | 33 | 83 | 4 | 14.50 |
| M16×2.0 | 2.00 | 11.90 | 12 | 30 | 75 | 4 | 14.00 |
| M16×1.0 | 1.00 | 13.90 | 14 | 33 | 100 | 4 | 15.00 |
| M18×2.0 | 2.00 | 13.90 | 14 | 33 | 100 | 4 | 16.00 |
| M18×2.5 | 2.50 | 13.90 | 14 | 33 | 100 | 5 | 15.50 |
| M20×1.5 | 1.50 | 15.95 | 16 | 40 | 100 | 5 | 18.50 |
| M20×2.0 | 2.00 | 15.95 | 16 | 40 | 100 | 5 | 18.00 |
| M22×1.0 | 1.00 | 16.00 | 16 | 40 | 100 | 5 | 21.00 |
| M20×2.5 | 2.50 | 15.90 | 16 | 40 | 100 | 5 | 17.50 |
| M24×3.0 | 3.00 | 15.90 | 16 | 40 | 100 | 5 | 21.00 |
| D20×P2.0 | 2.00 | 20.00 | 20 | 40 | 100 | 5 | 18.00 |
| D20×P4.0 | 4.00 | 20.00 | 20 | 40 | 100 | 5 | 16.00 |
| M30×3.5 | 3.50 | 16.00 | 16 | 40 | 100 | 5 | 26.50 |
| D16×1.25 | 1.25 | 16.00 | 16 | 40 | 100 | 5 | 14.75 |
How to Select a Configuration
Single-Form
Best when thread-depth flexibility and a broader range of compatible thread sizes are required.
3-Tooth
A balanced option where both machining efficiency and thread-depth flexibility are important.
Full-Profile
Suitable for repeat-production threading where the pitch and thread specification are already defined.
 Machining Notes
For stable thread milling and consistent tool performance, check the following setup conditions before machining.
Check Tool Runout
Check tool runout before machining. If radial runout exceeds 0.01 mm, correct the setup before cutting.
Minimize Tool Overhang
Use the shortest practical tool overhang. For longer reach, reduce spindle speed, feed rate or cutting load as required.
Respond to Vibration
If abnormal vibration or cutting noise occurs, reduce the feed rate or cutting load until machining becomes stable.
Maintain Chip Evacuation
For aluminum machining, use suitable air blast, mist or cutting fluid to improve chip evacuation and reduce material adhesion at the cutting edge.
Thread Mill Selection Resources
Not sure which thread mill matches your thread standard, pitch, diameter or machining application? Use our practical selection guide to compare thread specifications, tool styles and machining requirements before selecting a cutter.
Aluminum Thread Mill Customization
Single-form, 3-tooth and full-profile thread mills can be configured for aluminum and selected non-ferrous machining. Thread pitch, cutting diameter, effective thread depth, shank diameter, overall length, cutting configuration, flute geometry and coating can be reviewed according to the required internal thread, component geometry and machining conditions.
| PARAMETRE | CUSTOMIZATION OPTIONS |
|---|---|
| Tool Configuration | Single-Form / 3-Tooth / Full-Profile |
| Thread Pitch P | Standard and non-standard metric pitches can be reviewed according to the required thread specification |
| Cutting Diameter d | Cutting diameter can be selected according to thread size, prepared-hole diameter and required clearance |
| Effective Thread Depth L1 | Standard and extended-reach configurations available according to required thread depth and machining access |
| Shank Diameter D | Shank diameter can be matched to toolholder and machine requirements |
| Toplam Uzunluk L | Standard and extended overall lengths can be reviewed for deeper or restricted-access applications |
| Flute Count F | Flute count is selected according to tool diameter, cutting configuration and chip-evacuation requirement |
| Chip-Groove Geometry | Open flute and chip-groove geometry can be optimized for aluminum and other non-ferrous materials |
| Cutting-Edge Preparation | Sharp or application-matched cutting-edge preparation can be reviewed according to material and thread size |
| Kaplama | Uncoated, DLC or application-specific coating options can be reviewed according to the workpiece material |
| Length Series | Standard Length / Extended Length |
| Uygulama | Internal thread milling, blind-hole threading and CNC circular or helical interpolation |
OEM & Private Label
OEM marking, product identification and private-label packaging can be configured for distributors, tooling brands and repeat-order programs.

Lazer Kazıma
Logo, thread size, pitch, tool code and batch information can be marked on the tool where space allows.
Özel Etiketler ve Ambalajlar
Custom labels, protective tubes and private-label packaging can be reviewed for distributor and OEM orders.
Sample & Bulk Orders
Standard-size samples, custom-tool trials and repeat bulk supply can be reviewed according to specification and quantity.
Teknik İş Akışı
Tool configuration and commercial requirements are confirmed before production.
Sorgulama
Confirm thread size, pitch, depth, material and quantity.
Mühendislik
Select tool configuration, dimensions, flute geometry and coating.
Ticari
Confirm quotation, MOQ, samples and lead time.
Üretim
Carbide preparation, CNC grinding, coating and marking.
Inspection
Check dimensions, cutting geometry, runout and identification.
Kalite, Denetim ve Teslimat
Aluminum thread mills are controlled through carbide blank inspection, precision CNC grinding, dimensional measurement and final tool inspection. Critical dimensions, cutting geometry, flute condition, radial runout, coating appearance and product identification are reviewed before packing.

Üç Aşamalı Kalite Kontrolü
Incoming Material
Carbide blank dimensions and supplied material information are checked against the confirmed production requirement.
In-Process Grinding
Pitch, cutting diameter, effective depth, flute geometry and shank dimensions are monitored during CNC grinding.
Final Inspection
Finished tools are checked for dimensions, edge condition, runout, coating appearance, marking and packing identification.
Temel Denetim Özellikleri
| DENETİM KONUSU | KONTROL ODAĞI | REFERENCE |
|---|---|---|
| Thread Pitch P | Pitch consistency and cutting-profile spacing | Confirmed thread specification |
| Cutting Diameter d | Cutting-section diameter | Size matrix or drawing |
| Effective Depth L1 | Working reach and cutting-section length | Standard or extended series |
| Shank Diameter D | Clamping dimension and surface condition | Tool specification |
| Toplam Uzunluk L | Toplam alet uzunluğu | Size matrix or drawing |
| Kesim Geometrisi | Single-form / 3-tooth / full-profile configuration | Approved production configuration |
| Flute & Chip Groove | Flute condition and chip-clearance geometry | Tool size and application |
| Radyal Salgı | Kesme bölümü ile şaft arasındaki eşmerkezlilik | Inspection requirement |
| Son Teknoloji ve Kaplama | Edge condition and coating appearance | Application requirement |
Measurement & Batch Control
Geometry Measurement
Optical inspection of pitch and cutting geometry.
Çıkma Kontrolü
Concentricity is checked between cutting section and shank.
Kenar Denetimi
Magnified inspection checks edge and flute condition.
Parti Tanımlama
Size, pitch, product code and order information can be linked for repeat supply.
Koruyucu Ambalajlama Süreci
Finished thread mills are individually protected to reduce contact with precision-ground cutting edges during storage and transportation.

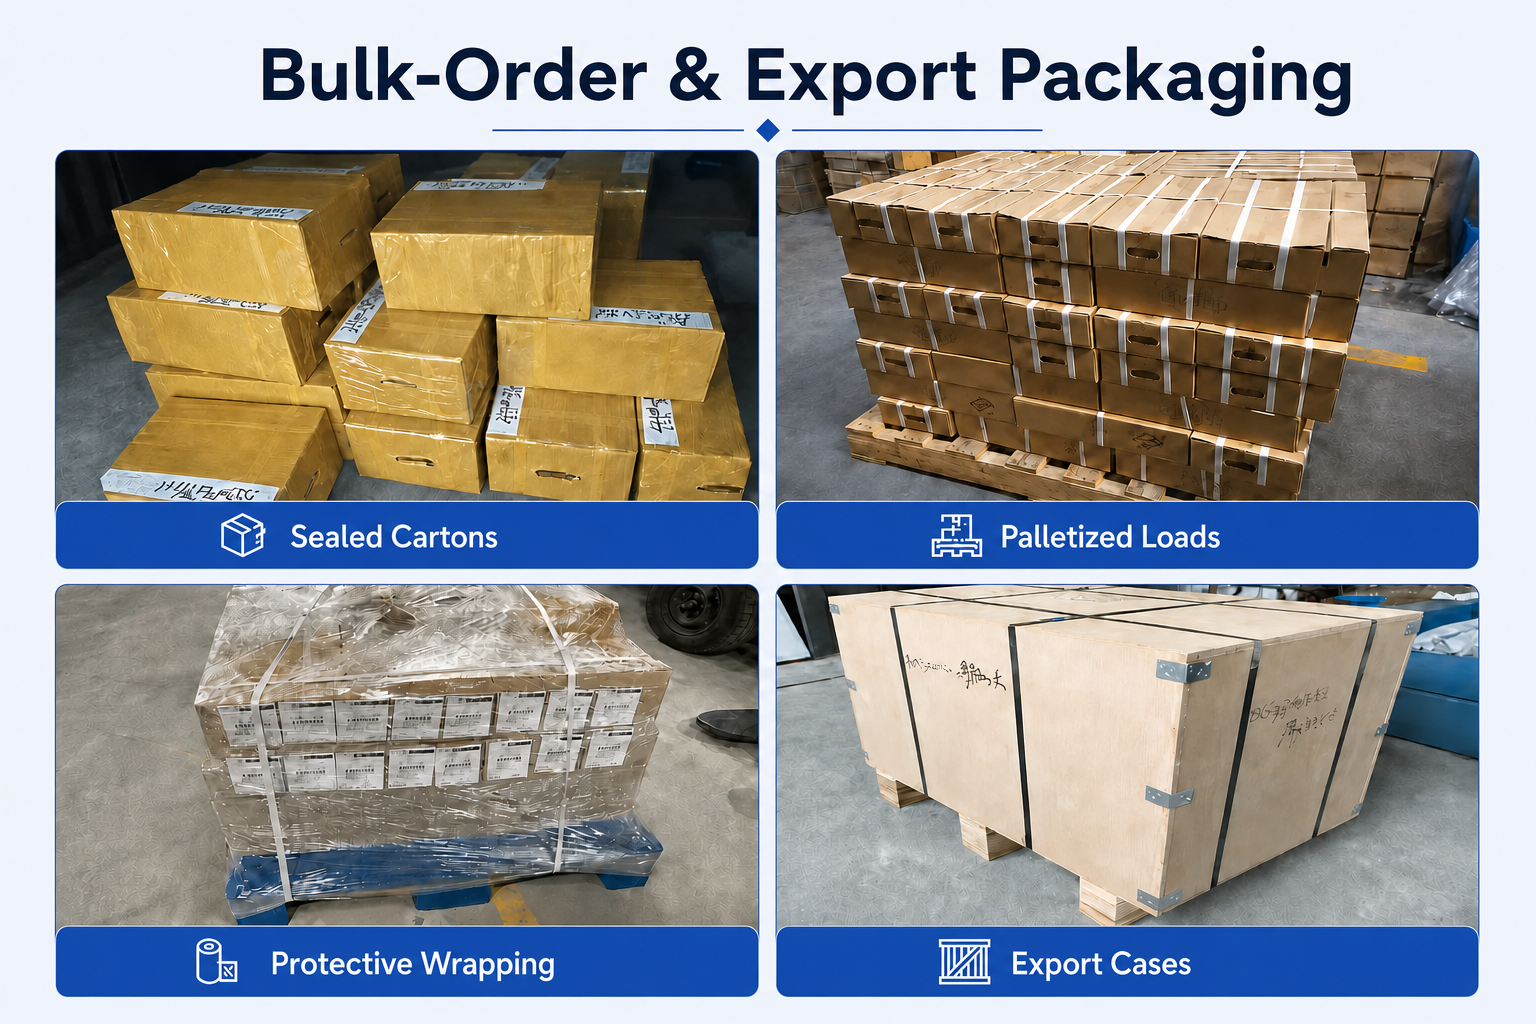
Toplu Sipariş ve İhracat Ambalajı
Bulk orders can be arranged with reinforced cartons, protective wrapping, palletized loading or export cases according to shipment requirements.
Teslimat Koordinasyonu
In-stock standard sizes can normally be prepared for shipment within 1–3 days. Lead time for custom configurations is confirmed after thread specification, dimensions, coating, quantity and packaging requirements are approved.
Sık Sorulan Sorular ve İndirmeler
Common selection, application and ordering questions for the solid carbide thread mill series for aluminum.
Ürün ve Uygulama SSS'leri
What configurations are available for this aluminum thread mill series?
The series includes single-form, 3-tooth and full-profile configurations. Standard and extended-length options are available for selected sizes.
How should I choose between single-form, 3-tooth and full-profile?
Single-form provides greater thread-depth flexibility, 3-tooth offers a balance between flexibility and machining efficiency, and full-profile is suited to repeat-production applications with a confirmed pitch and thread specification.
What materials can these thread mills machine?
The series is primarily developed for aluminum and aluminum alloys. Selected configurations can also be reviewed for copper, zinc alloys and other compatible non-ferrous materials.
Are these thread mills suitable for blind holes?
Yes, provided the prepared-hole depth, required thread depth, tool reach and bottom clearance are suitable. Chip evacuation should also be considered for deeper blind holes.
Why are extended-length thread mills available?
Extended-length tools provide additional reach for deeper thread locations or restricted-access components. Use the shortest practical tool length that provides sufficient access.
Can the thread diameter be adjusted through the CNC program?
Yes. In compatible applications, the finished thread diameter can be fine-adjusted through the programmed interpolation radius or tool compensation.
What coolant or chip-control method is recommended for aluminum?
Air blast, mist or suitable cutting fluid can be used according to the thread depth and machining setup. Good chip evacuation helps reduce chip recutting and material adhesion.
Sipariş ve Özelleştirme ile İlgili Sık Sorulan Sorular
What information should I provide for tool selection?
Please provide thread size and pitch, workpiece material, prepared-hole diameter, required thread depth, blind-hole or through-hole condition and order quantity.
Can you manufacture custom aluminum thread mills?
Yes. Thread pitch, cutting diameter, effective depth, shank diameter, overall length, flute configuration and coating can be reviewed according to the machining application or drawing.
OEM etiketleme ve özel markalı ambalajlama seçenekleri mevcut mu?
Yes. Laser marking, custom labels, protective tubes and private-label packaging can be reviewed according to the confirmed specification and order quantity.
What is the lead time?
In-stock standard sizes can normally be prepared for shipment within 1–3 days. Custom tool lead time is confirmed after dimensions, configuration, coating, quantity and packaging requirements are approved.
Teknik Dosyalar
General carbide tooling references for product selection and cutting-parameter review.
Solid Carbide Tool Catalog
Product families and reference size information.
Threading & Reaming Tools Cutting Data
General starting references for carbide threading tools.
Final thread-milling parameters should be confirmed according to cutter diameter, pitch, thread depth, aluminum grade, tool configuration, coating, tool overhang and machine rigidity.
Related Guides & Thread Mill Resources
Explore practical thread-milling selection guides and related solid carbide thread mill series for different thread standards, materials and machining requirements.
Selection guidance for thread standards, pitch, tool style, diameter, depth and workpiece material.
Compare flexibility, thread size range, breakage risk and typical machining applications.
Browse metric, inch, UNC/UNF, single-form, full-profile and application-specific thread mill series.
Ölçüler, fiyatlar veya özel seçenekler mi arıyorsunuz?
Gerekli takım türünü, boyutlarını, miktarlarını, iş parçası malzemesini ve varsa OEM veya özel gereksinimleri bize iletin. Uygun teknik özellikleri, stok durumunu, teslim süresini ve fiyat teklifi ayrıntılarını size teyit edeceğiz.
Çizimler, boyut listeleri ve referans fotoğraflar memnuniyetle kabul edilir.