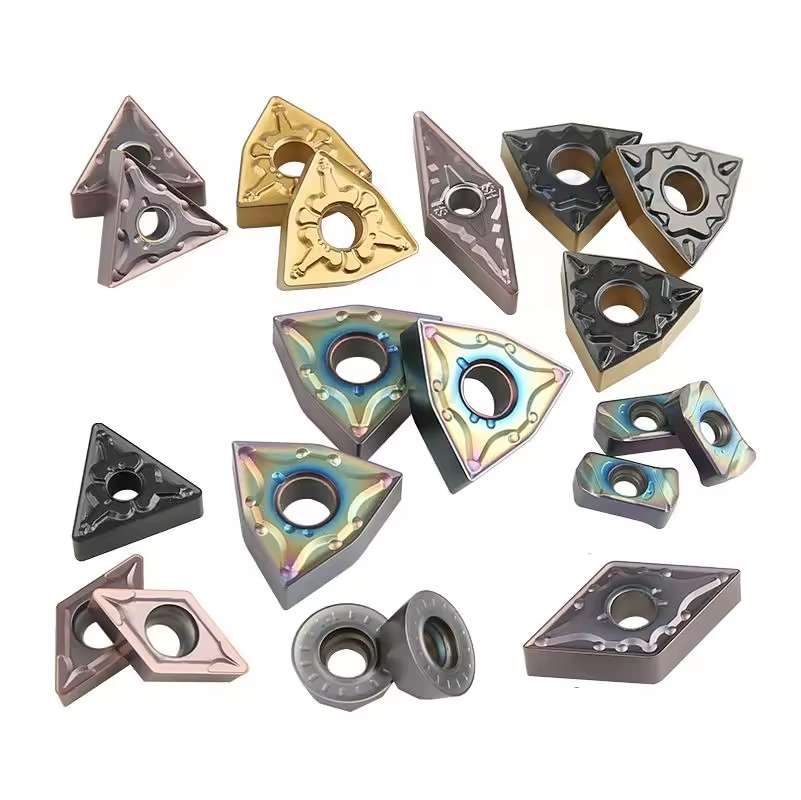
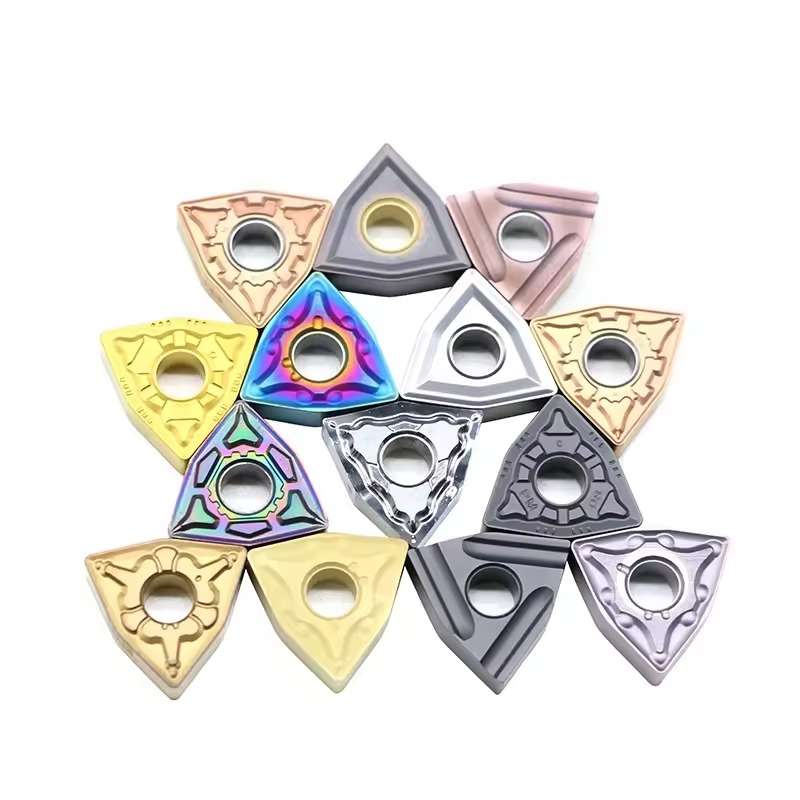
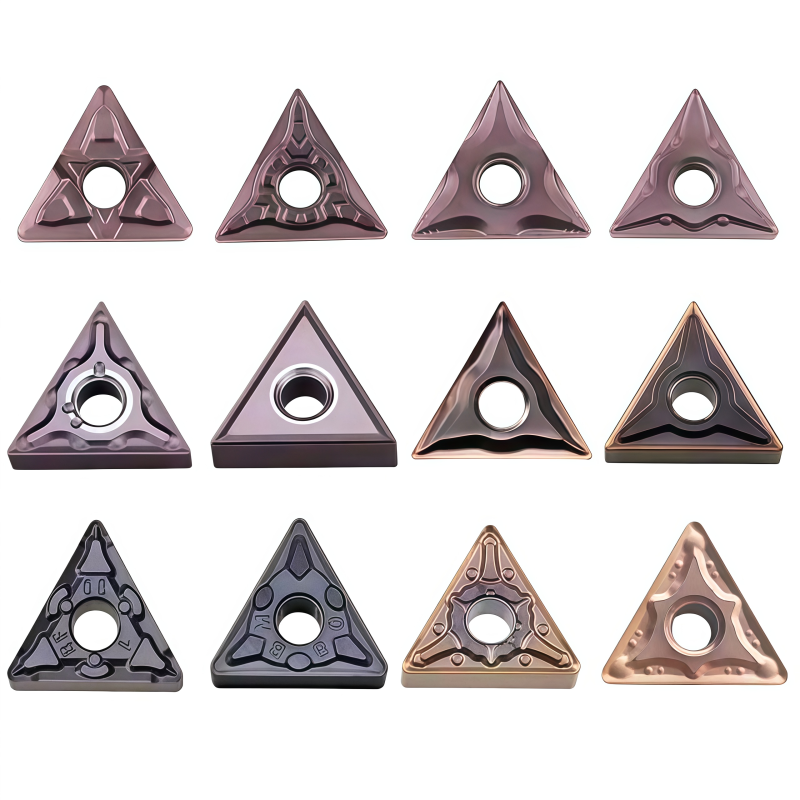
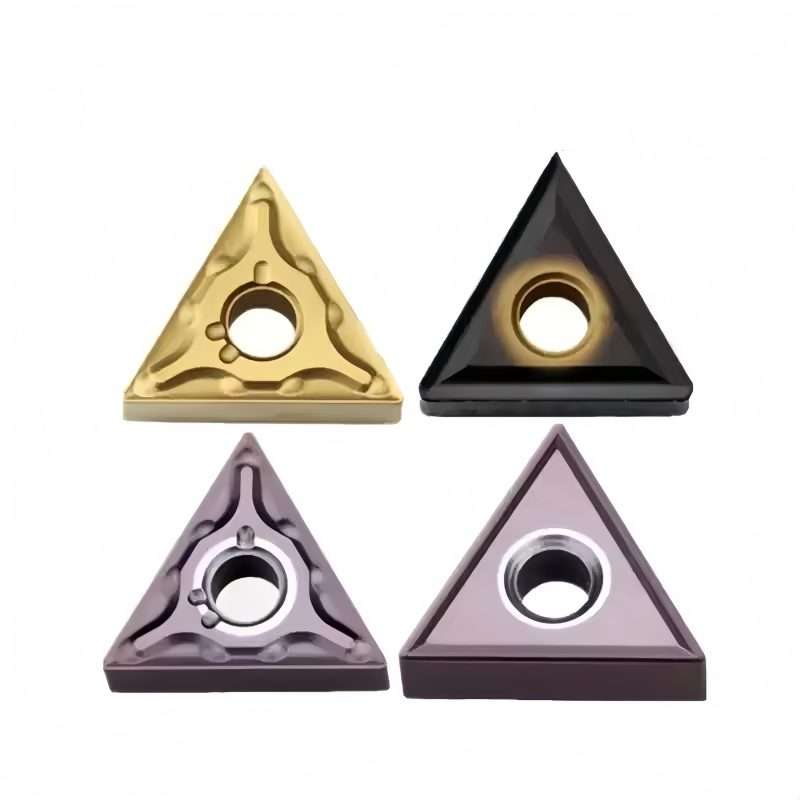
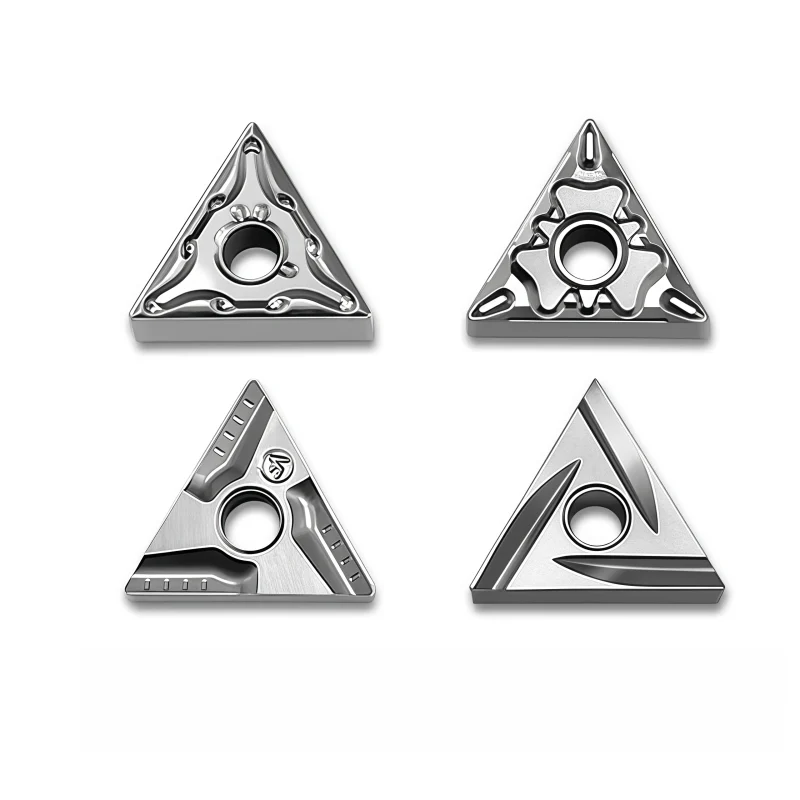
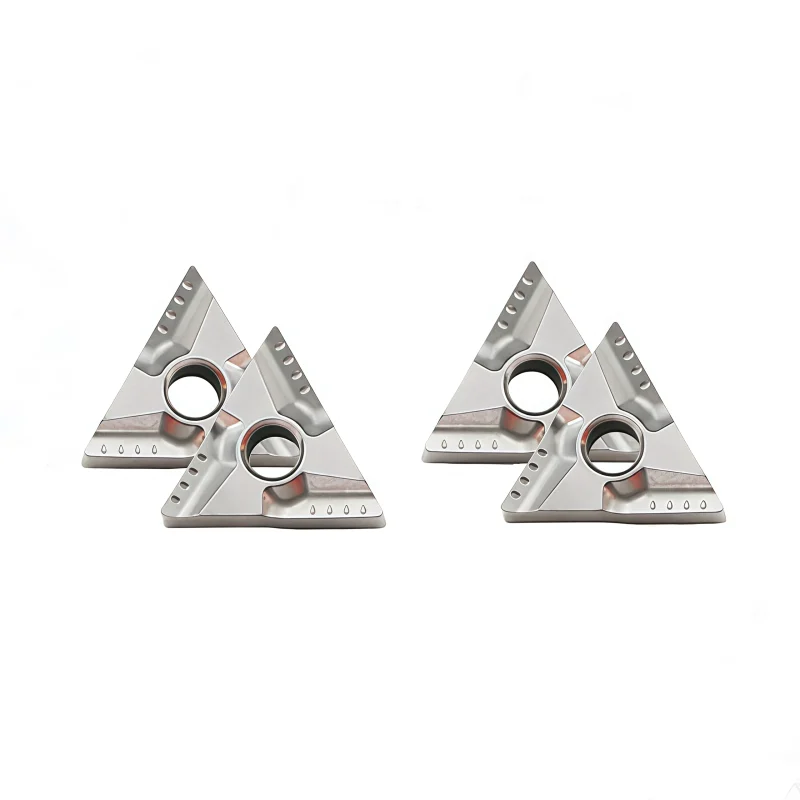
เม็ดมีดกลึงคาร์ไบด์ TNMG 1604 สำหรับสแตนเลส
TNMG 1604 carbide turning inserts for stainless steel turning, facing and profiling. Six usable edges and application-matched grades and chipbreakers support chip control and wear resistance, with mixed-model orders and private-label packaging available.
เหล็กไม่ржаว
Six Cutting Edges
Chipbreaker Options
บรรจุภัณฑ์ OEM
◆ภาพรวมผลิตภัณฑ์
The TNMG 1604 series carbide turning inserts are designed for external turning, facing and profiling of stainless-steel components on CNC lathes. Their triangular negative geometry provides strong cutting-edge support and multiple usable cutting edges, making the series suitable for continuous production and repeat machining.
Stainless steel can generate high cutting temperatures, work hardening and built-up edge. TNMG 1604 inserts can therefore be supplied with different carbide substrates, PVD/CVD coatings and chipbreakers to balance edge sharpness, toughness, chip control and wear resistance.
Customers selecting inserts for different workpiece groups can also compare the complete TNMG 1604 insert range according to material, chipbreaker and grade requirements.
| Insert Series | TNMG 1604 | Standard Models | 160404 / 160408 / 160412 |
|---|---|---|---|
| Insert Shape | Triangular, 60° included angle | การเคลียร์สินค้า | Negative, 0° clearance |
| Corner Radius | 0.4 / 0.8 / 1.2 mm | Operations | Turning / Facing / Profiling |
| Primary Material | เหล็กไม่ржаวง | Processing Range | Finishing / Medium / Selected roughing |
| ตัวเลือกระดับ | Multiple carbide grades by confirmation | ตัวเลือกการเคลือบ | PVD / CVD options |
| Standard Pack | 10 pieces per box | Supply Options | Standard / Mixed models / Private label |
Grade, chipbreaker, coating, material suitability and stock status should be confirmed using the complete insert code.
◆TNMG 1604 Model Selection
| แบบ | Corner Radius | Edge Characteristic | General Selection |
|---|---|---|---|
| TNMG 160404 | 0.4 มม. | Lower radial cutting force | Finishing and lighter turning conditions |
| TNMG 160408 | 0.8 มม. | Balanced strength and finish | General medium turning |
| TNMG 160412 | 1.2 mm | Stronger corner support | Higher feed and stable heavier cuts |
Corner-radius selection also affects radial cutting force, surface finish and chip thickness. Confirm suitability through the complete cutting conditions.
The following reference images show TNMG 1604 dimensions, chipbreaker options, available grades and material recommendations. Send the complete current code for accurate replacement matching.
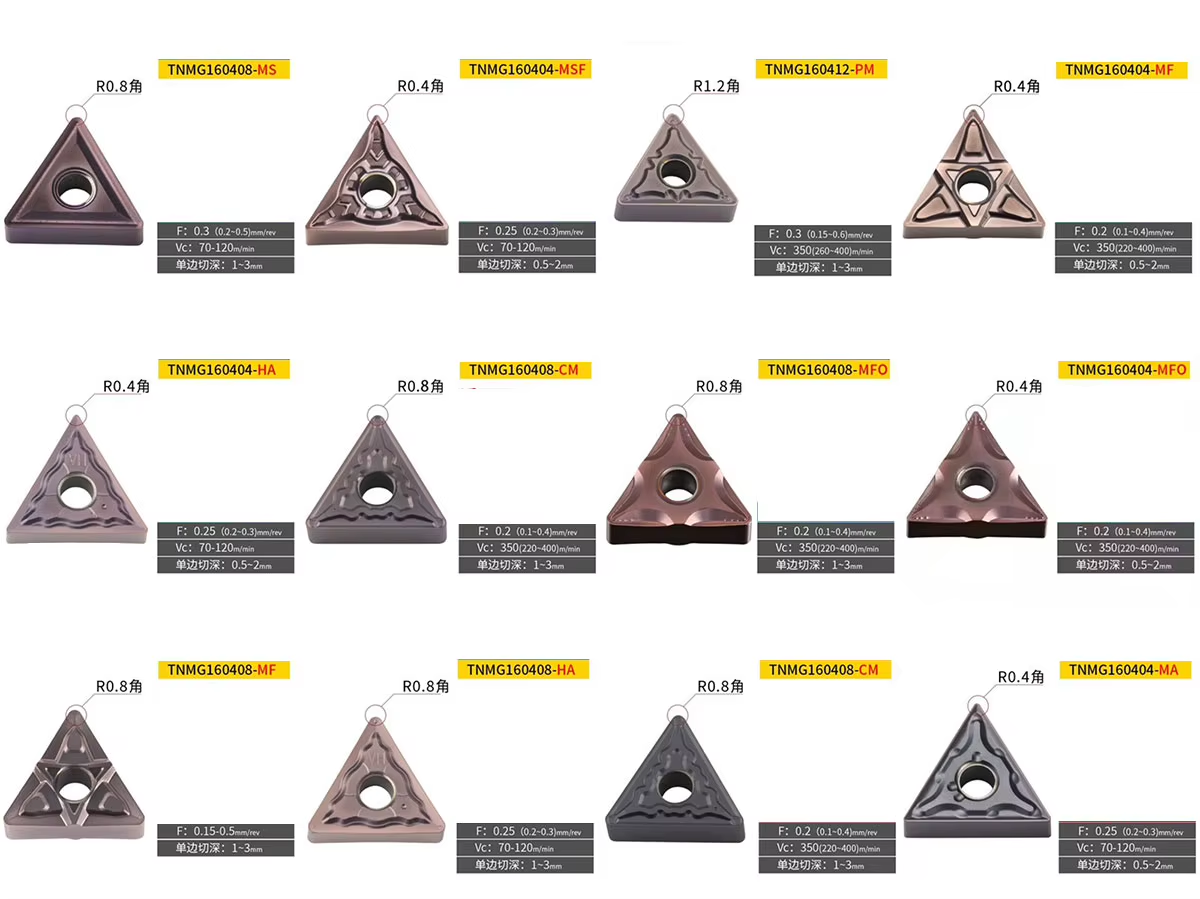
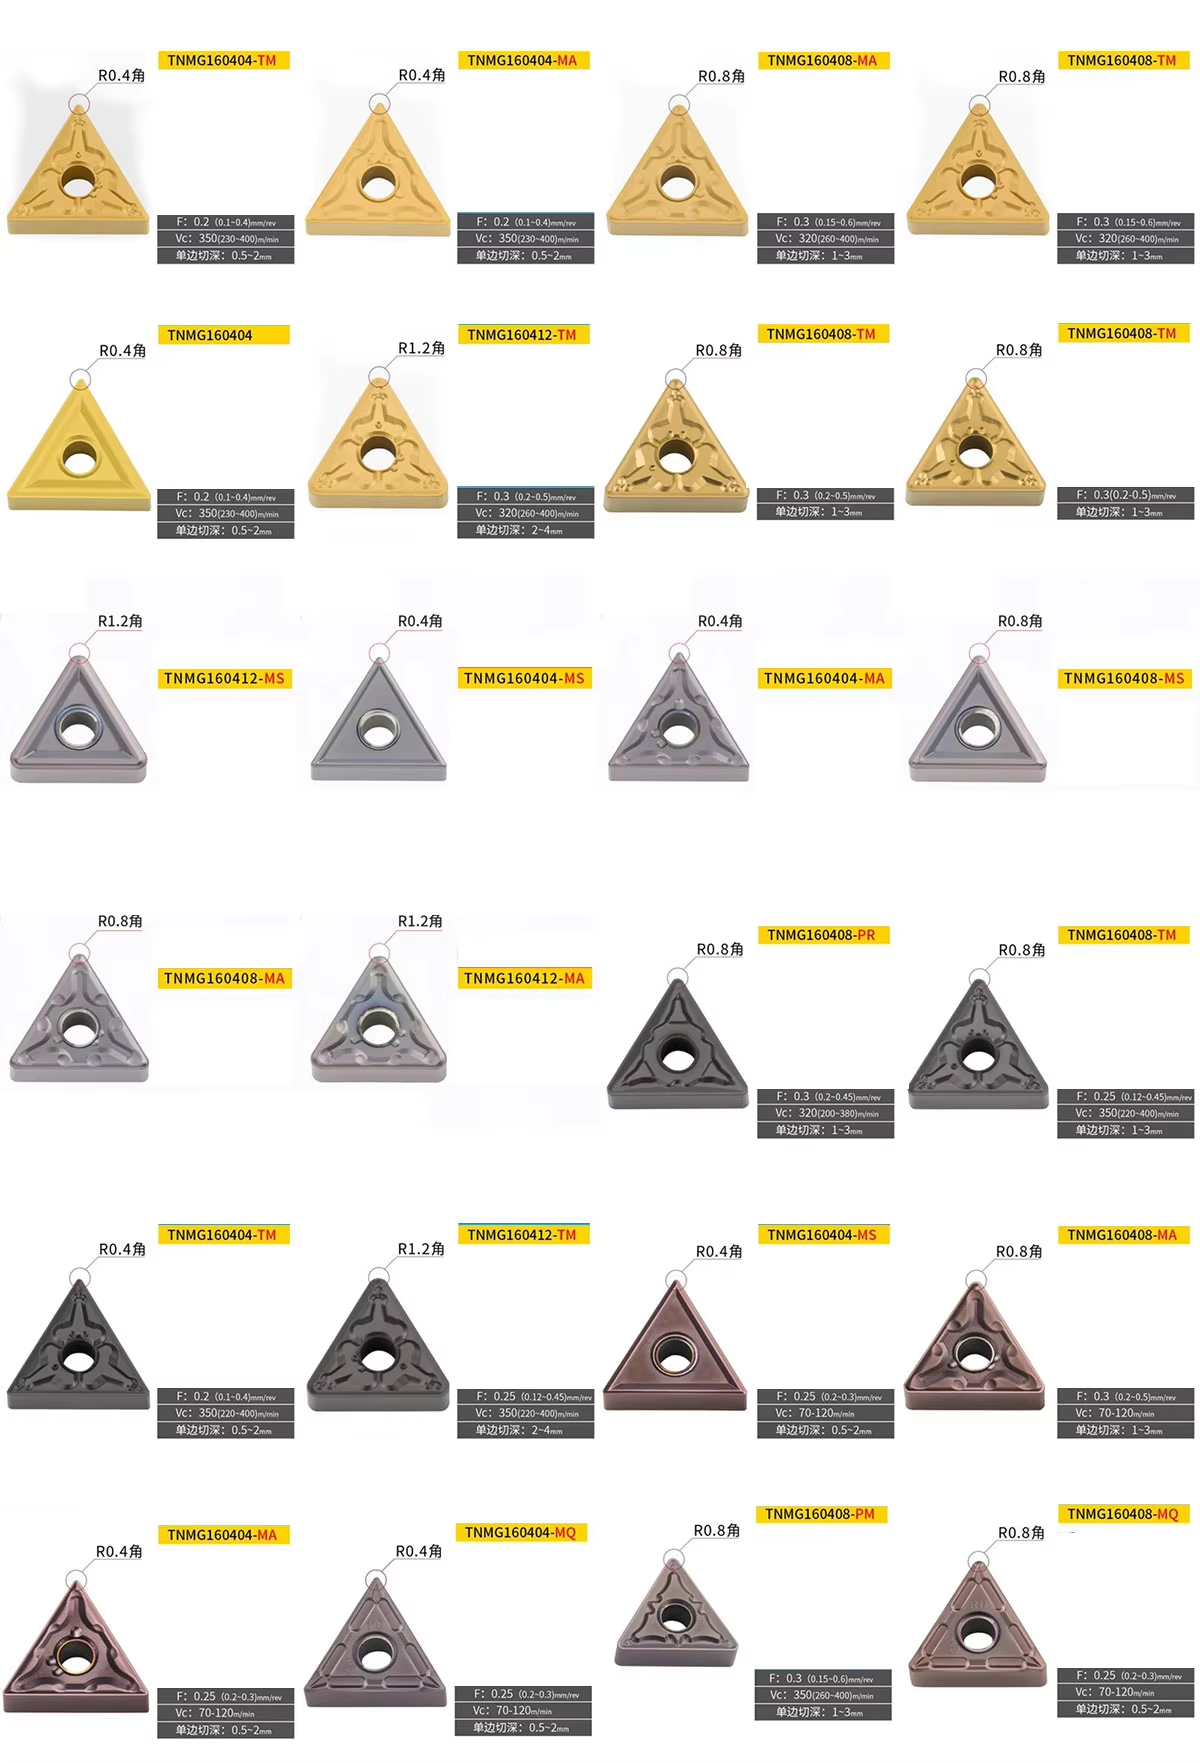
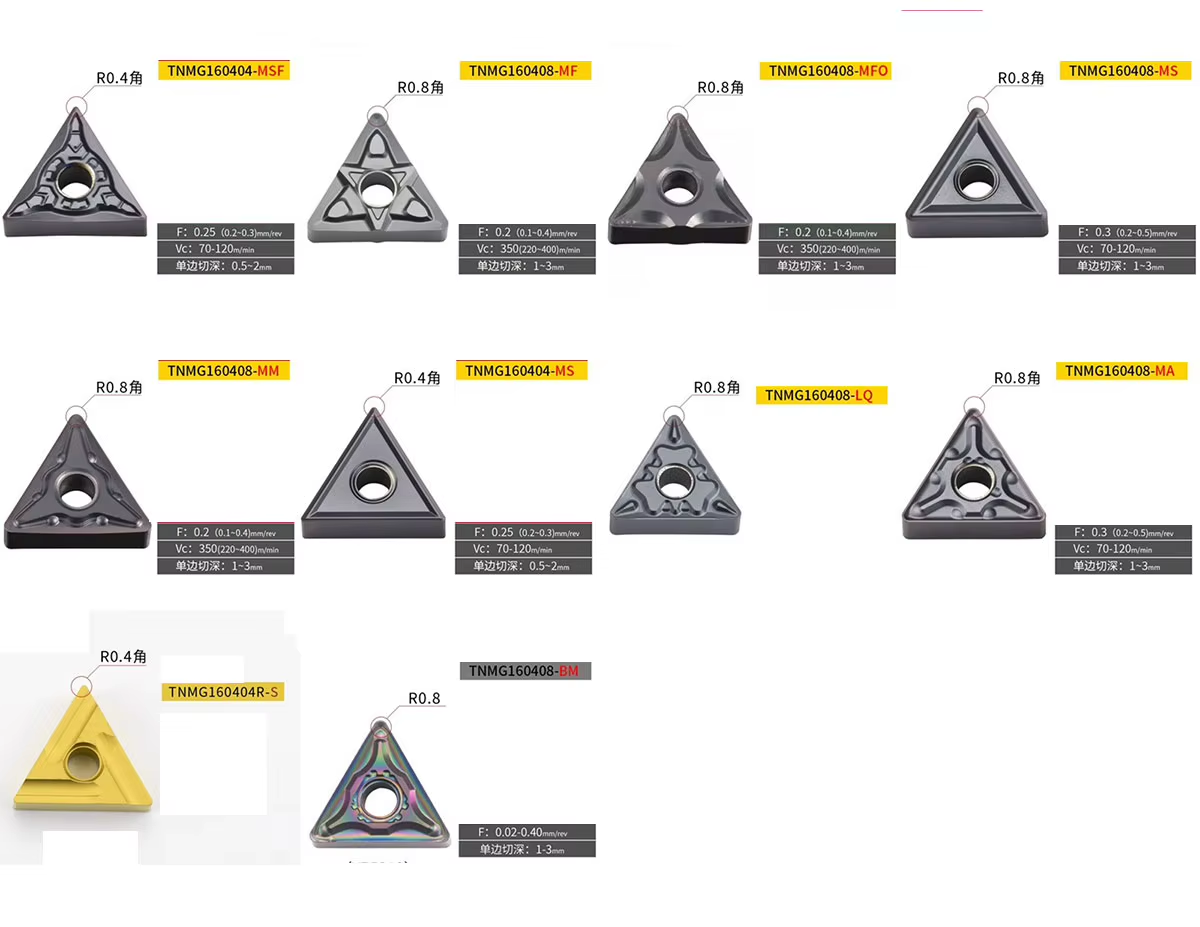
Stainless steels can work-harden quickly and retain heat near the cutting edge. An unsuitable insert may produce long chips, built-up edge, poor surface quality or premature edge failure.
TNMG 1604 selection should therefore consider edge sharpness, coating, carbide toughness, chipbreaker range and tool-holder rigidity together rather than selecting by size alone.
◆Chipbreaker and Product Details


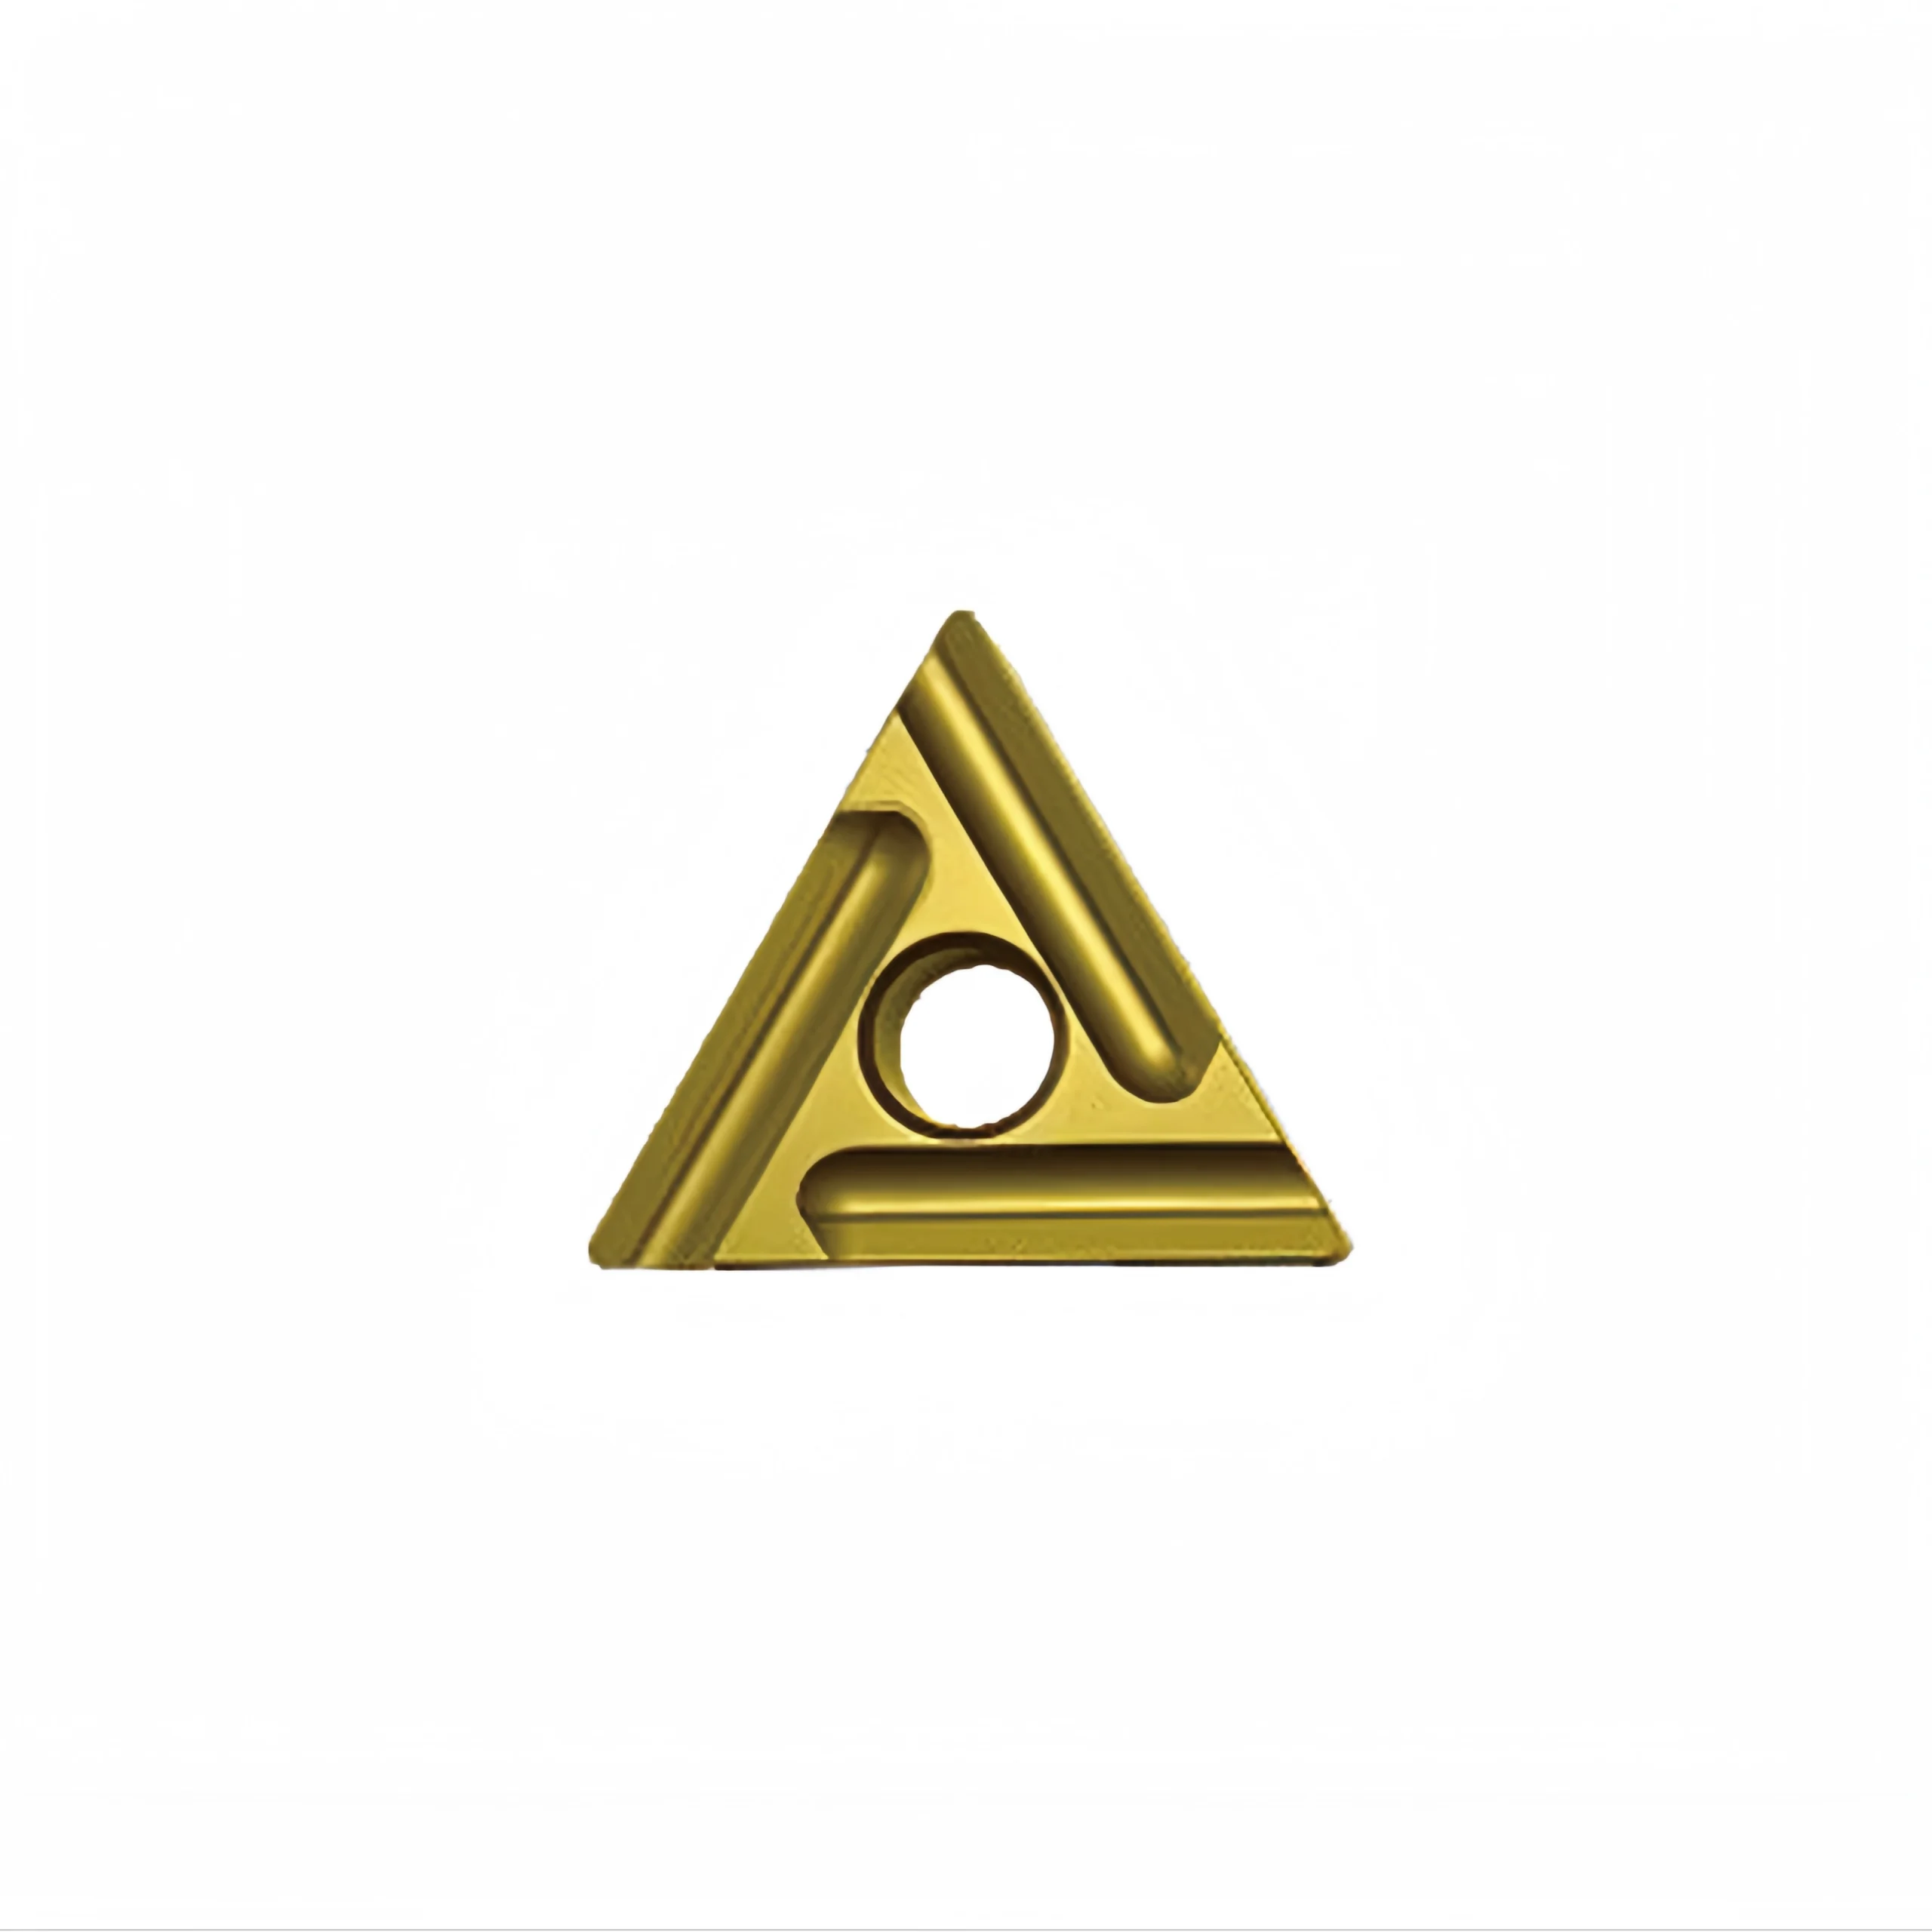
Different stainless-steel grades and turning conditions require different combinations of edge sharpness and toughness. Finishing geometries generally use smaller feeds and depths of cut, while medium and roughing geometries require stronger edge support.
Coating color alone cannot identify the insert grade. Confirm the printed code or package label before placing a repeat or replacement order.
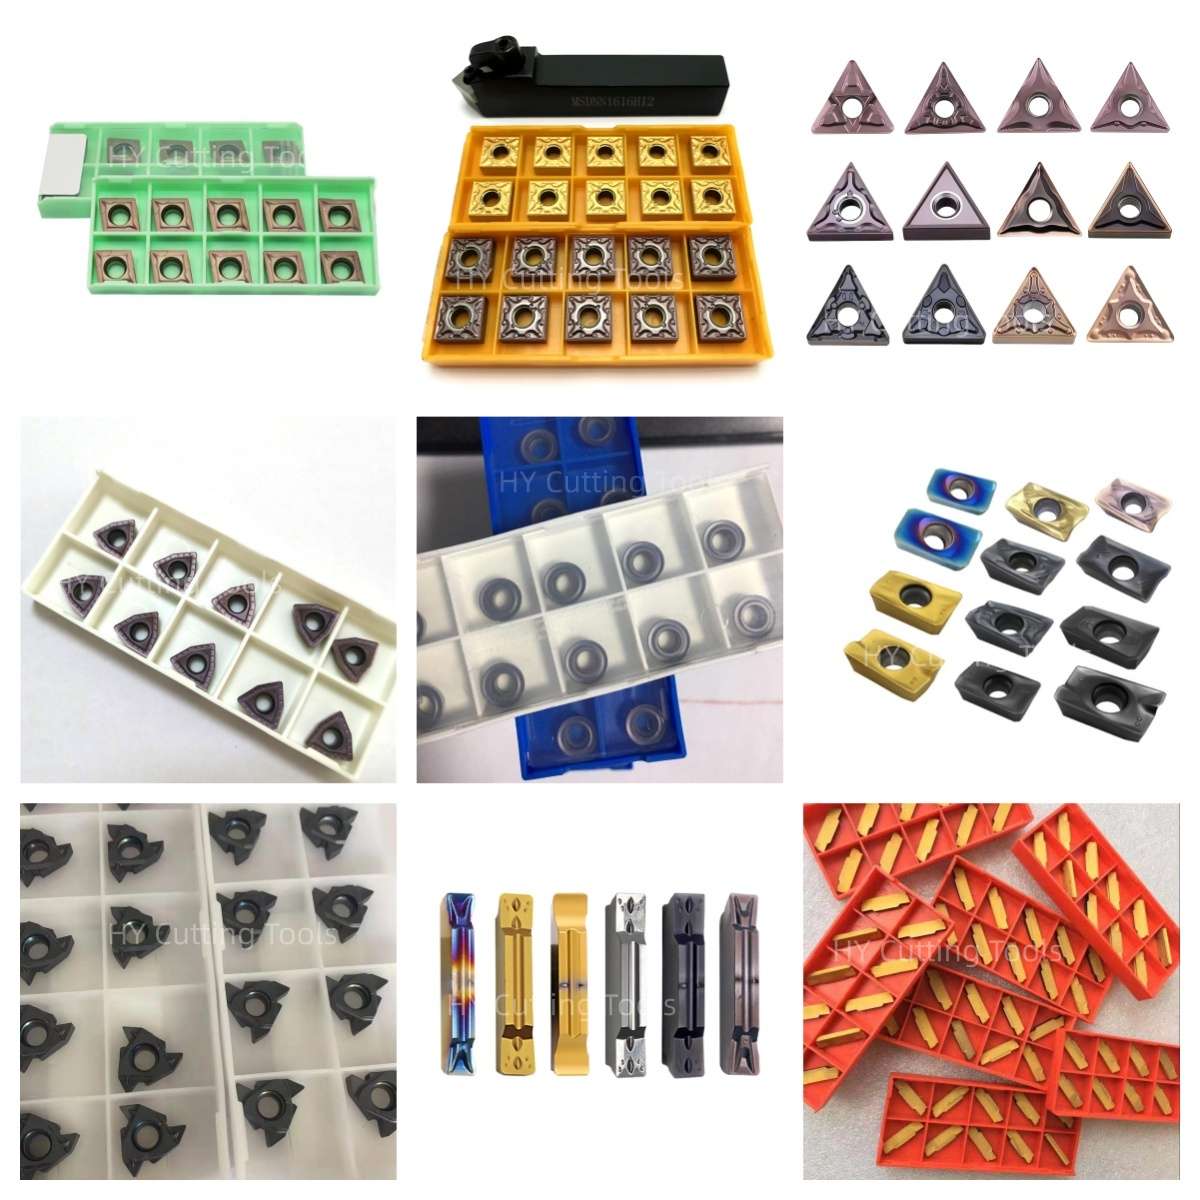
TNMG inserts are normally packed in compartment boxes to protect the cutting edges and preserve clear model, grade and batch identification. Final packaging and supply details are confirmed according to the selected models and order quantity.
- Complete TNMG insert code, grade and chipbreaker
- Compatible tool-holder model
- Stainless-steel grade and workpiece hardness
- Finishing, medium or roughing operation
- Required quantity and packaging preference
If the complete insert code is unavailable, send clear photographs of the top marking, chipbreaker surface, side profile, original box label and compatible tool holder.
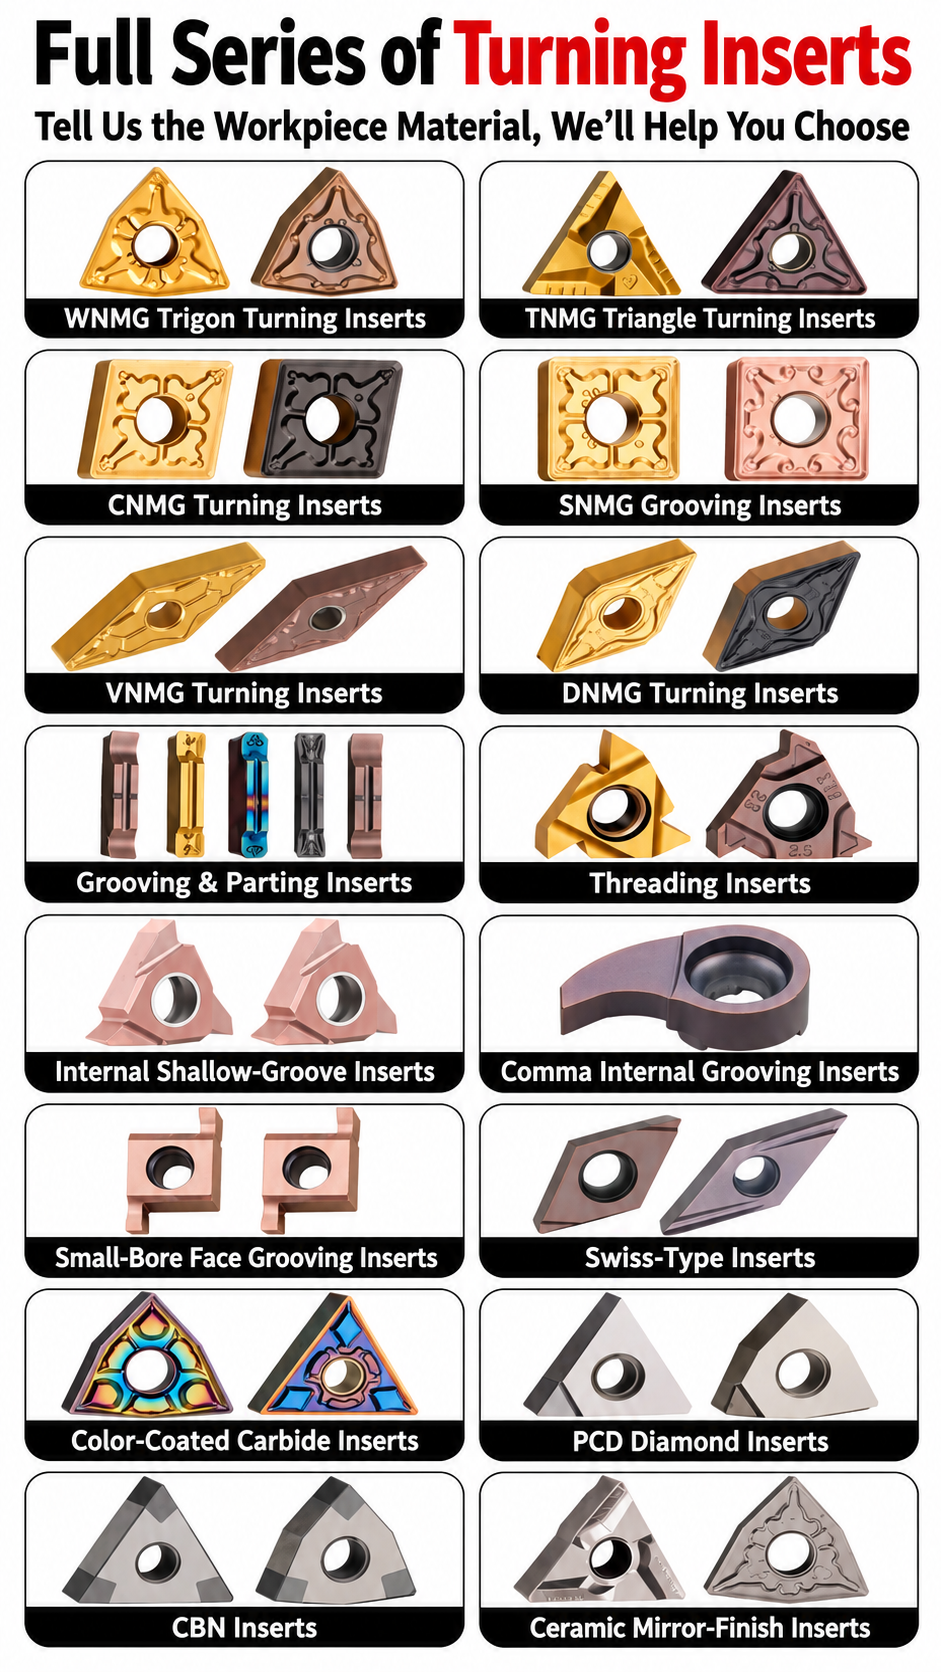
◆ข้อมูลทางเทคนิคและตารางขนาด
This TNMG 1604 range covers 160404, 160408 and 160412 for stainless-steel turning, with nominal corner radii of 0.4, 0.8 and 1.2 mm. TNMG is a 60° triangular, negative-clearance insert with a fixing hole. The common 16-size family references below assist holder selection; the approved drawing and complete chipbreaker/grade code determine the supplied configuration.
| Base ISO Size | IC (mm) | S (mm) | Hole D1 (mm) | Corner Radius RE (mm) | Application Consideration |
|---|---|---|---|---|---|
| TNMG 160404 | 9.52* | 4.76* | 3.81* | 0.4 | Smaller radius; consider for lighter stainless-steel finishing cuts. |
| TNMG 160408 | 9.52* | 4.76* | 3.81* | 0.8 | Balanced radius for stable medium turning, subject to chipbreaker and grade. |
| TNMG 160412 | 9.52* | 4.76* | 3.81* | 1.2 | Larger radius; check machine rigidity and radial-force sensitivity. |
◆รายการตรวจสอบสเปกตามรุ่น
| พารามิเตอร์ | รายละเอียดที่ต้องยืนยัน |
|---|---|
| Insert geometry | 60° triangular, double-sided TNMG form with 0° clearance and a fixing hole; check the actual chipbreaker and holder seat. |
| Nominal size and radius | 1604 size family; select 0.4, 0.8 or 1.2 mm radius according to feed, profile, finish and setup rigidity in stainless steel. |
| Carbide grade | The Overview lists multiple carbide grades without mapping them to each radius. Confirm an ISO M application grade for the actual stainless-steel type, hardness and cut continuity. |
| Chipbreaker and coating | Confirm the selected stainless-steel chipbreaker, substrate, PVD/CVD coating and recommended feed/depth range. Coating color alone does not identify a grade. |
| Holder compatibility | Check TNMG 16 pocket, thickness, hole, clamp, seat, approach angle and tool hand against the holder manufacturer's specification. |
| Supply and packing | Overview reference: 10 pieces per plastic box. Confirm pack count, mixed-model supply, stock and labeling by complete order code. |
Stainless Steel Grade & Chipbreaker Selection
Select the chipbreaker by the actual feed and depth of cut, then match a carbide grade and coating to the stainless-steel family and cut continuity. The Overview lists finishing, medium and selected roughing conditions, but does not identify a complete order code for each combination.
| การดำเนินการ | Selection Priority | Confirm for the Complete Code |
|---|---|---|
| Finishing | Chip formation and surface finish at the planned lower feed and depth | Edge preparation, radius, grade and minimum effective feed |
| Medium turning | Balance chip control, edge strength and wear resistance | Operating window, coolant and stainless-steel grade |
| Selected roughing | Edge toughness and stability under higher or interrupted load | Approved geometry, grade, holder rigidity and permissible load |
◆How to Select a TNMG Insert for Stainless Steel
See the คู่มือการเลือกอินเสิร์ต CNC for additional shape, grade and radius checks.
◆เริ่มข้อมูลการตัด
The Overview does not give a validated cutting-speed, feed or depth-of-cut range for a complete TNMG grade and chipbreaker. Obtain starting data for the exact stainless-steel grade, insert code, coolant and cut continuity. Maintain sufficient feed for the selected geometry, avoid rubbing or dwell, and adjust after observing chip formation and edge wear.
◆ซีรีส์ที่เกี่ยวข้องและเอกสารอ้างอิงทางเทคนิค
Compare other turning geometries in the ชุดใบตัดคาร์ไบด์สำหรับการกลึงและกัด. For a current TNMG stainless-steel series drawing, holder match, grade-specific cutting data or quotation, send the complete model and application details.
◆การปรับแต่งชิ้นส่วนคาร์ไบด์และบริการ OEM
โปรดระบุใบตัดสำหรับกระบวนการกลึง ชิ้นงาน และอุปกรณ์จับยึด เราสามารถตรวจสอบตัวเลือกใบตัดมาตรฐาน รูปทรงเฉพาะตามการใช้งาน และข้อกำหนดสำหรับแบรนด์ส่วนตัว โดยใช้รหัสใบตัด แบบวาด หรือตัวอย่างของท่าน เกรด ชั้นเคลือบ ขนาด และปริมาณการสั่งซื้อที่มีอยู่จะได้รับการยืนยันสำหรับแต่ละซีรีส์ที่ท่านขอ.
เรขาคณิตและการควบคุมชิป
ตรวจสอบตัวตัดเศษ (chipbreaker), มุมเอียง (rake), การเตรียมคมตัด (cutting-edge preparation), รัศมีปลายคม (nose radius) และออกแบบมุม (corner design) ให้เหมาะสมกับกระบวนการทำงานและชิ้นงาน ตรวจสอบความเข้ากันได้ของตัวจับ (holder) ก่อนอนุมัติรูปทรงที่ปรับเปลี่ยนแล้ว.
วัสดุฐานและชั้นเคลือบ
เลือกชนิดคาร์ไบด์และชั้นเคลือบที่เหมาะสมกับวัสดุชิ้นงาน สภาพการตัด และความสมดุลที่ต้องการระหว่างความทนต่อการสึกหรอและความแข็งของขอบตัด.
ขนาดและ OEM
ตรวจสอบขนาดของแผ่นแทรก ความหนา คุณสมบัติการกำหนดตำแหน่งและการยึดตรึง ค่าความคลาดเคลื่อน การทำเครื่องหมายด้วยเลเซอร์ และการบรรจุภัณฑ์ภายใต้แบรนด์ส่วนตัว ให้สอดคล้องกับข้อกำหนดที่ได้รับการอนุมัติ.
◆ตัวเลือกการปรับแต่ง
โปรดใช้ช่องข้อมูลด้านล่างเมื่อส่งคำสอบถาม ตัวเลือกที่แน่นอนจะขึ้นอยู่กับตระกูลชิ้นส่วน และจะได้รับการยืนยันในใบเสนอราคาหรือแบบวาดที่ได้รับการอนุมัติ.
| ข้อมูลทางเทคนิค | รายละเอียดที่ต้องยืนยัน |
|---|---|
| ประเภทการแทรก | ใบตัดสำหรับการกลึง การกัด การทำเกลียว การทำร่อง หรือการเจาะ; โปรดส่งรหัสสินค้าหรือแบบวาดมา. |
| ขนาดและรูปทรง | รูปทรง ขนาด ความหนา เส้นผ่านศูนย์กลางของวงที่เขียนได้หรือความยาวของขอบ รูปแบบของรูหรือส่วนจับยึด และรุ่นของตัวจับยึด. |
| รูปทรงการตัด | ตัวหักเศษ, รัศมีปลายหรือมุม, การเตรียมคมตัด, ทิศทางการตัด และรูปทรงที่เหมาะสมกับการใช้งานเฉพาะ. |
| เกรดและชั้นเคลือบ | กลุ่มและระดับของชิ้นงาน, วัสดุฐานคาร์ไบด์, ระบบการเคลือบ และสภาพการตัดแบบเปียกหรือแห้ง. |
| ความทนทานและการตรวจสอบ | ขนาดสำคัญ ข้อกำหนดเกี่ยวกับรูปทรง วิธีการตรวจสอบ และรายงานที่จำเป็น. |
| การนำเสนอของ OEM | การพิมพ์หรือทำเครื่องหมายบนกล่อง, เนื้อหาบนฉลาก, รูปแบบบรรจุภัณฑ์ และจำนวนต่อแพ็ก. |
◆วิธีขอทำแผ่นแทรกตามสั่ง

ส่งความต้องการเกี่ยวกับใบแทรกของคุณผ่านทาง แบบฟอร์มติดต่อ หรือดูข้อมูลเพิ่มเติมของเรา บริการ OEM และบริการแบรนด์ส่วนตัว.
◆การควบคุมคุณภาพของแผ่นคาร์ไบด์

คุณภาพของชิ้นส่วนแทรกขึ้นอยู่กับระดับคุณภาพที่ได้รับการอนุมัติ รูปทรง การเคลือบผิว และข้อกำหนดด้านขนาด เราจะตรวจสอบข้อกำหนดเมื่อยืนยันคำสั่งซื้อ และปรับขอบเขตการตรวจสอบให้สอดคล้องกับซีรีส์ของชิ้นส่วนแทรกและแบบวาดของลูกค้า หากมี โปรดแจ้งขนาดสำคัญหรือความต้องการด้านเอกสารก่อนเริ่มการผลิต เพื่อให้สามารถรวมไว้ในแผนการตรวจสอบที่ตกลงกันไว้.
01 · วัสดุที่รับเข้า
ตรวจสอบให้แน่ใจว่าเกรดคาร์ไบด์หรือเอกสารเกี่ยวกับวัสดุที่ระบุไว้ตรงกับข้อกำหนดในคำสั่งซื้อ.
02 · การตรวจสอบระหว่างกระบวนการผลิต
ตรวจสอบขนาดและคุณสมบัติขั้นสูงระหว่างกระบวนการผลิต เพื่อให้สอดคล้องกับข้อกำหนดที่ได้รับการอนุมัติ.
03 · การตรวจสอบขั้นสุดท้าย
ตรวจสอบขนาดที่ตกลงกันไว้ ลักษณะภายนอก สภาพขอบ การระบุชนิดการเคลือบ และการทำเครื่องหมายตามความเหมาะสม.
04 · บทรีวิวการแพ็กของ
ตรวจสอบรหัสสินค้า ปริมาณ ป้าย และบรรจุภัณฑ์ป้องกัน ให้ตรงกับคำสั่งซื้อที่ได้รับการอนุมัติ.
◆การตรวจสอบและจัดทำเอกสาร
ควรตกลงกันเกี่ยวกับจุดตรวจสอบและเกณฑ์การรับสินค้าสำหรับชุดสินค้าที่สั่งซื้อ สำหรับชิ้นส่วนแทรกที่ผลิตตามสั่ง แบบวาดที่ได้รับการอนุมัติจะมีน้ำหนักมากกว่าคำอธิบายทั่วไปในแคตตาล็อก.
| ตรวจสอบพื้นที่ | สิ่งที่ต้องตรวจสอบ |
|---|---|
| ขนาดและรูปทรง | ระบุขนาด ความหนา รัศมีมุม คุณสมบัติการยึด และค่าความคลาดเคลื่อนในแบบวาด (หากมี). |
| รูปทรงการตัด | ตัวตัดเศษ, การเตรียมขอบ, มุมที่สามารถใช้งานได้ และรูปทรงตามความเหมาะสม. |
| เกรดและชั้นเคลือบ | ระดับที่ได้รับการอนุมัติและชื่อประเภทการเคลือบ; วิธีตรวจสอบตามคำขอใดๆ. |
| รูปลักษณ์และบรรจุภัณฑ์ | ความเสียหายที่เห็นได้ชัดบริเวณขอบ, รอยเครื่องหมาย, รหัสสินค้า, จำนวน และรูปแบบการบรรจุ. |
| เอกสารที่ขอ | รายงานการตรวจสอบ เอกสารเกี่ยวกับวัสดุหรือชั้นเคลือบ การอนุมัติตัวอย่าง หรือการระบุล็อต ตามที่ตกลงกัน. |
◆การสั่งซื้อและการส่งสินค้า

โปรดส่งรายชื่อรหัสสินค้าและปริมาณการสั่งซื้อแบบบรรทัดต่อบรรทัด สำหรับใบเสนอราคาที่มีขนาดสินค้าหลากหลาย โดยสถานะสินค้าในสต็อก ปริมาณสั่งซื้อขั้นต่ำ ข้อกำหนดเกี่ยวกับตัวอย่าง และระยะเวลาการผลิต ได้ถูกยืนยันแล้วสำหรับแต่ละเกรด ชั้นเคลือบ และรูปแบบสินค้า.
ส่งรายชื่อสินค้าและข้อกำหนดด้านคุณภาพผ่านทาง แบบฟอร์มติดต่อ เพื่อตรวจสอบรายละเอียดทางเทคนิค ความพร้อมในการจัดส่ง และการยืนยันการจัดส่ง.
◆คำถามที่พบบ่อยเกี่ยวกับผลิตภัณฑ์
Why use a TNMG insert for stainless-steel turning?
TNMG is a 60° triangular, negative-clearance insert with a fixing hole and multiple usable edges. A suitable chipbreaker and ISO M carbide grade can be selected for external turning or facing of stainless steel. Holder angle, workpiece grade and cut conditions determine whether this geometry fits the operation.
What changes between TNMG 160404, 160408 and 160412?
Their nominal corner radii are 0.4, 0.8 and 1.2 mm. A smaller radius may suit lighter finishing cuts; a larger radius offers more corner support but can increase radial force. Choose with the stainless-steel grade, chipbreaker, feed, finish and setup rigidity in mind.
Can all three radii use the same holder?
They share the TNMG 1604 base designation, but verify the holder pocket, insert thickness, fixing hole, clamp, approach angle and part clearance. The nose radius and chosen chipbreaker can change usable profile access even when the insert seats in the same holder.
How do I select a grade for 304, 316 or another stainless steel?
Specify the exact stainless grade and hardness, operation, cut continuity, coolant and current wear pattern. The Overview does not assign a named carbide grade to every radius or chipbreaker. Confirm an ISO M application grade, coating and starting cutting data for the complete code; duplex or precipitation-hardening grades may need a different selection from 304/316.
Why does chipbreaker selection matter in stainless steel?
Stainless steel can produce long chips and built-up edge. A chipbreaker needs sufficient feed and depth of cut to work as intended while maintaining edge strength. Confirm the supplier’s geometry-specific operating range; neither the TNMG size nor coating color identifies the correct chipbreaker.
How do I reduce work hardening and built-up edge?
Use the grade-specific cutting data and a stable feed that lets the selected edge cut rather than rub. Avoid unnecessary dwell, keep the setup rigid, and apply coolant consistently where required. Check chip flow, adhesion, wear and finish in a controlled trial.
◆คำถามที่พบบ่อยเกี่ยวกับการสั่งซื้อและ OEM
What should I send for a TNMG replacement inquiry?
Provide the original manufacturer, full insert code, grade and chipbreaker, photos of the marking and both faces, holder model, stainless-steel grade, cutting conditions, current wear issue and required quantity. Compare a proposed replacement in a controlled machining trial.
Can I order different radii or grades together?
Send a line-by-line list with each complete TNMG code, grade, chipbreaker and quantity. Mixed-model availability, minimum order quantity and dispatch time are confirmed by item. The Overview lists 10 pieces per box as its standard reference.
ผมสามารถขอตัวอย่างก่อนที่จะสั่งซื้อในปริมาณใหญ่ได้ไหมครับ?
Provide the complete code, holder, workpiece and planned test conditions. Confirm sample availability and evaluation criteria by grade; compare wear, chip control, surface finish and cost per accepted part under the same setup.
Are private-label packaging and customer SKU labels available?
The Overview lists neutral and private-label packaging, customer SKU and barcode labels. Send the artwork, marking requirements, pack quantity and expected order volume so feasibility, minimum quantity and lead time can be confirmed.
◆คู่มือและข้อมูลอ้างอิงทางเทคนิค
ใช้ คู่มือการเลือกอินเสิร์ต CNC for holder, grade, corner-radius and chipbreaker checks. The คู่มือประเภทใบตัดคาร์ไบด์ อธิบายเกี่ยวกับกลุ่มอินเสิร์ตที่กว้างขึ้น.
For the current TNMG stainless-steel drawing, grade-specific cutting data or quotation, send your complete insert and holder codes with the stainless-steel grade and quantity.
ต้องการทราบขนาด ราคา หรือตัวเลือกการปรับแต่งตามความต้องการหรือไม่?
ส่งรายละเอียดและจำนวนที่ต้องการเพื่อรับใบเสนอราคา.
- ขนาดมาตรฐาน
- คำสั่งซื้อทดลองในปริมาณน้อย
- ขนาดผสม
- OEM และตามสั่ง
ดูรหัส QR – ติดต่อฝ่ายขายผ่าน WeChat
สแกนเพื่อติดต่อเราผ่าน WeChat.
สแกนเพื่อติดต่อเราผ่าน WeChat.