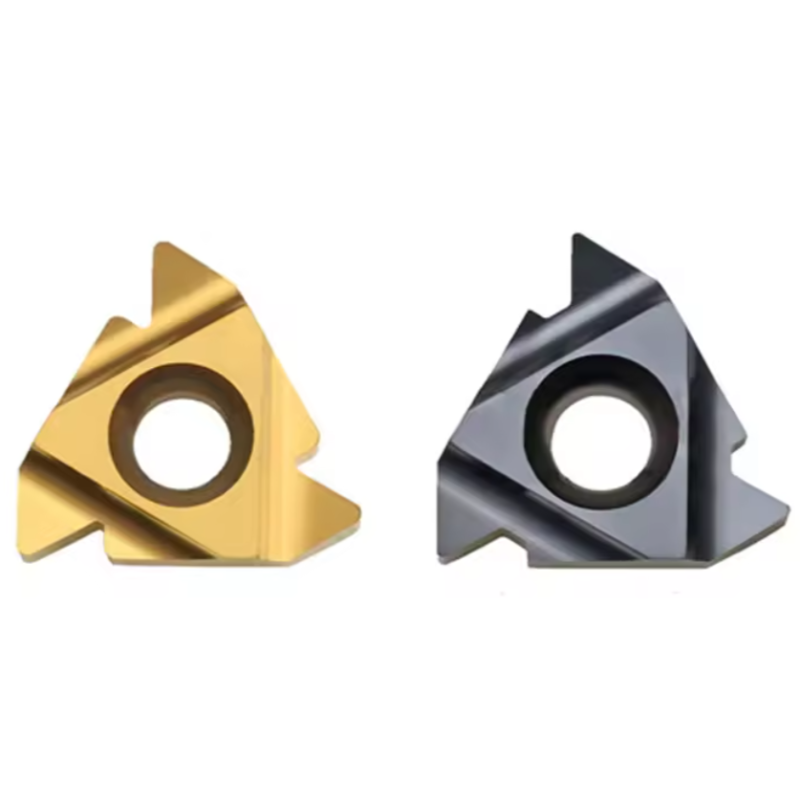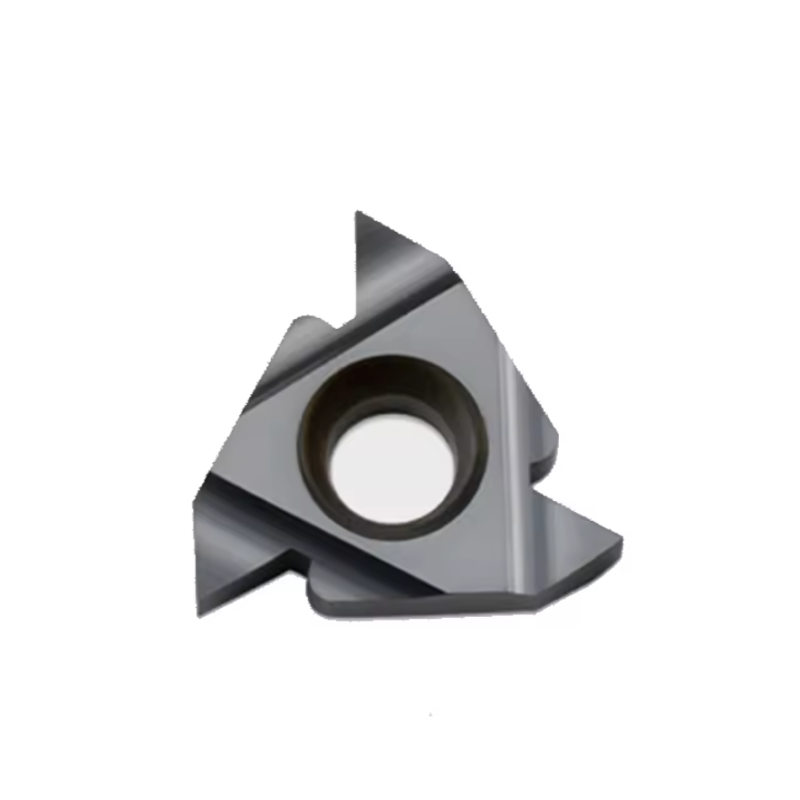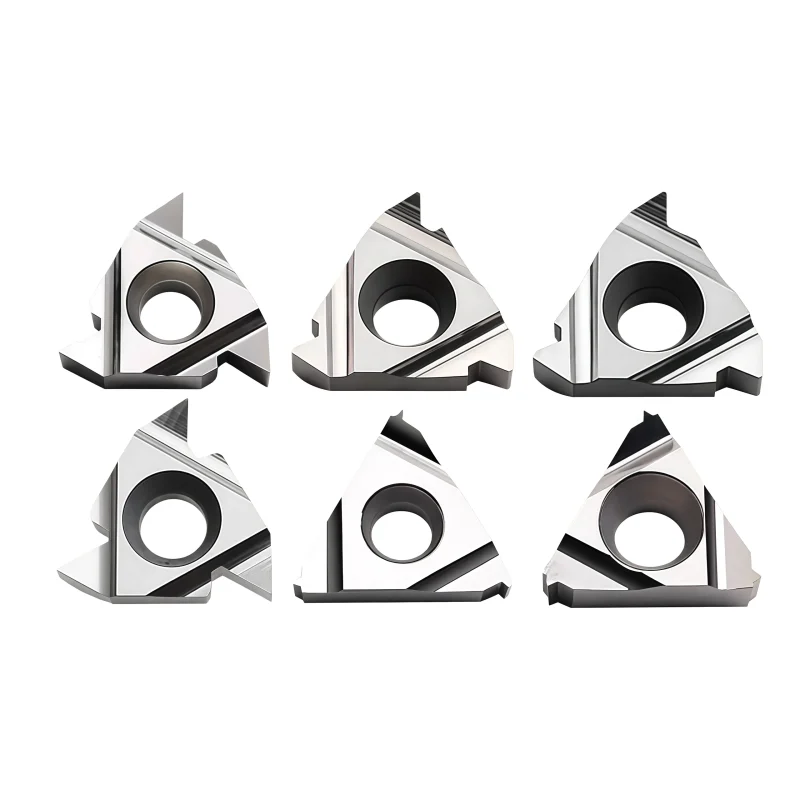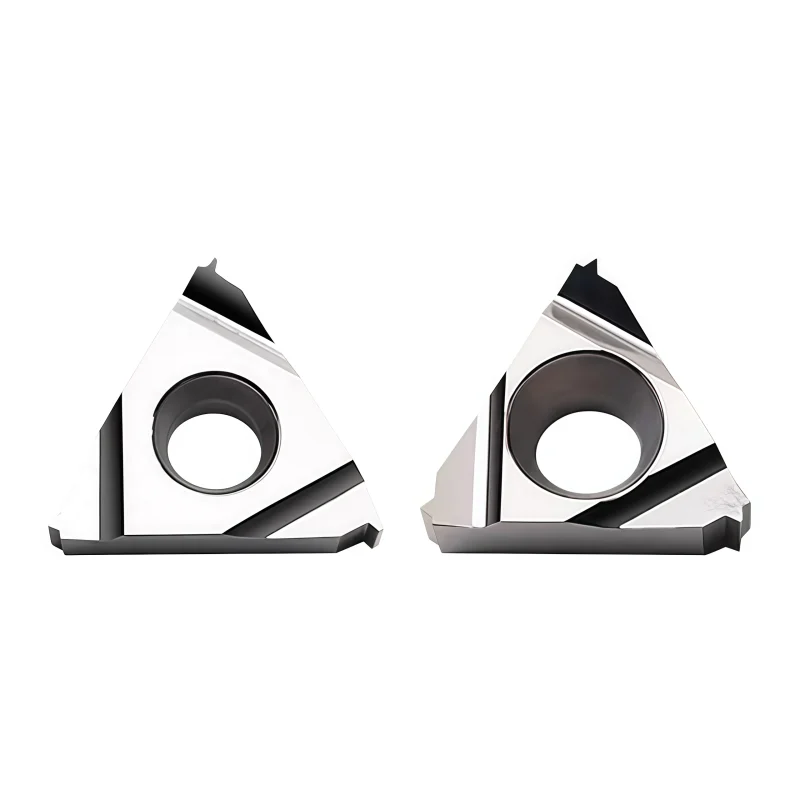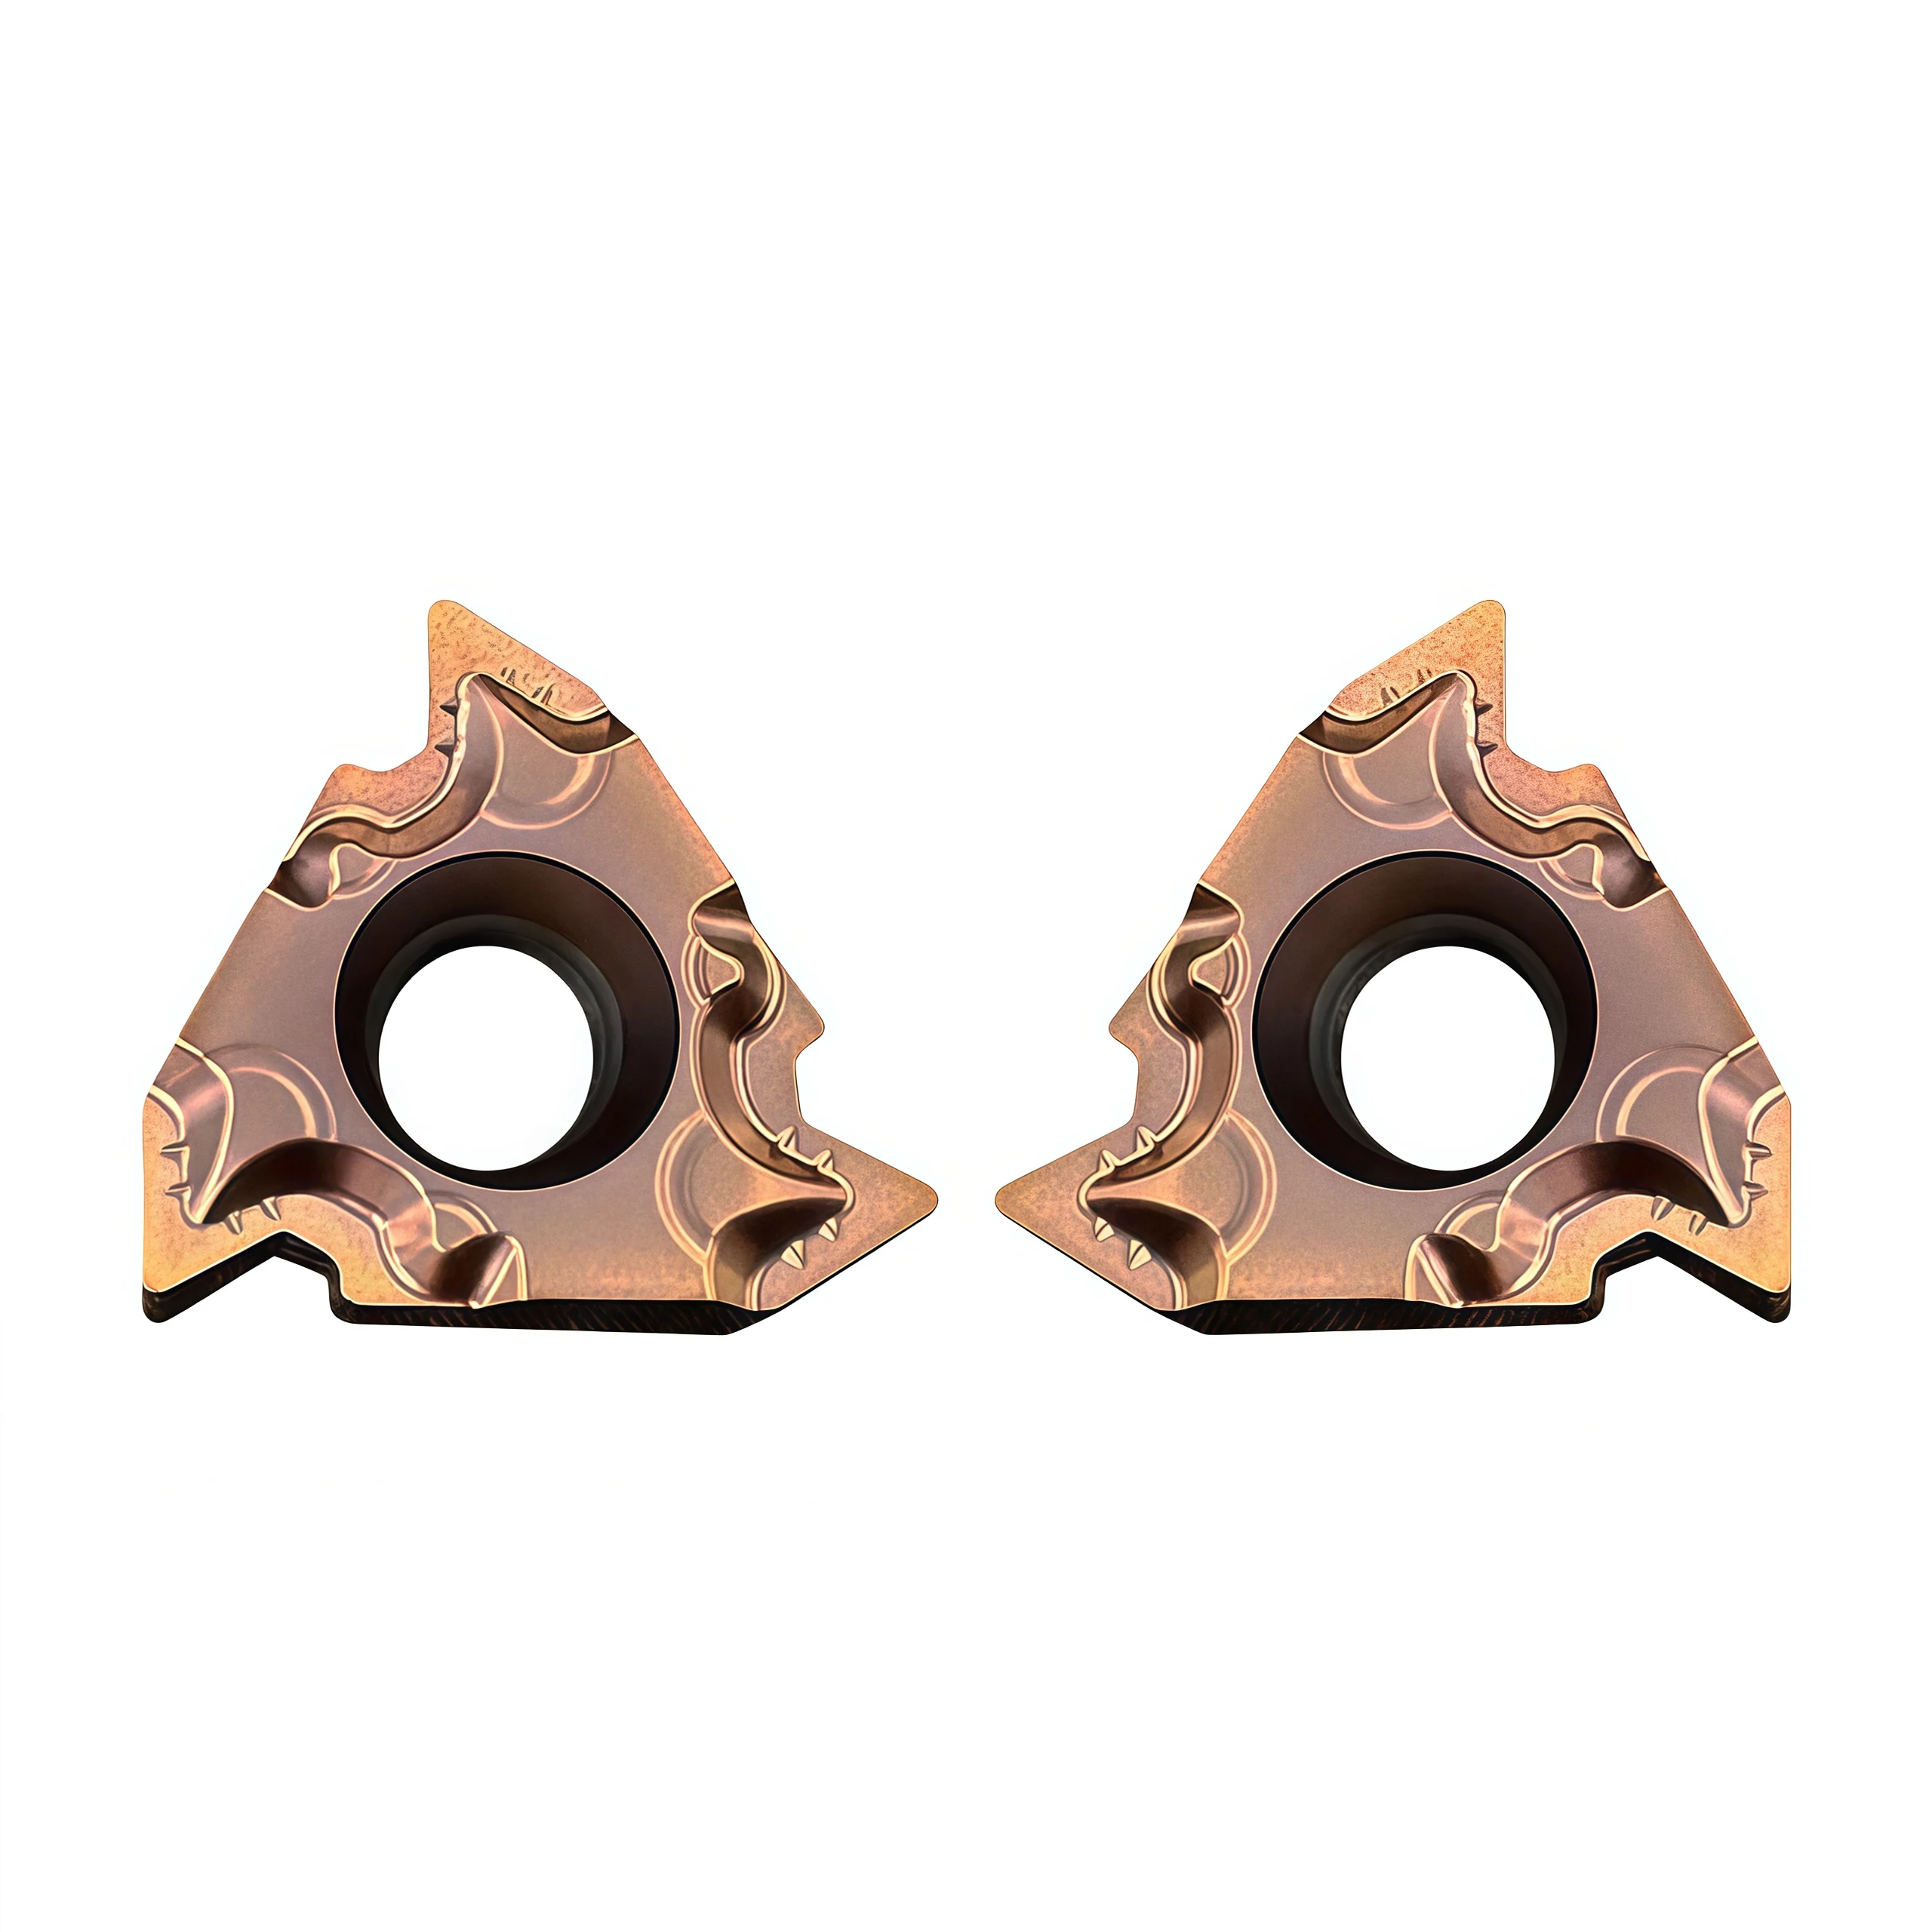
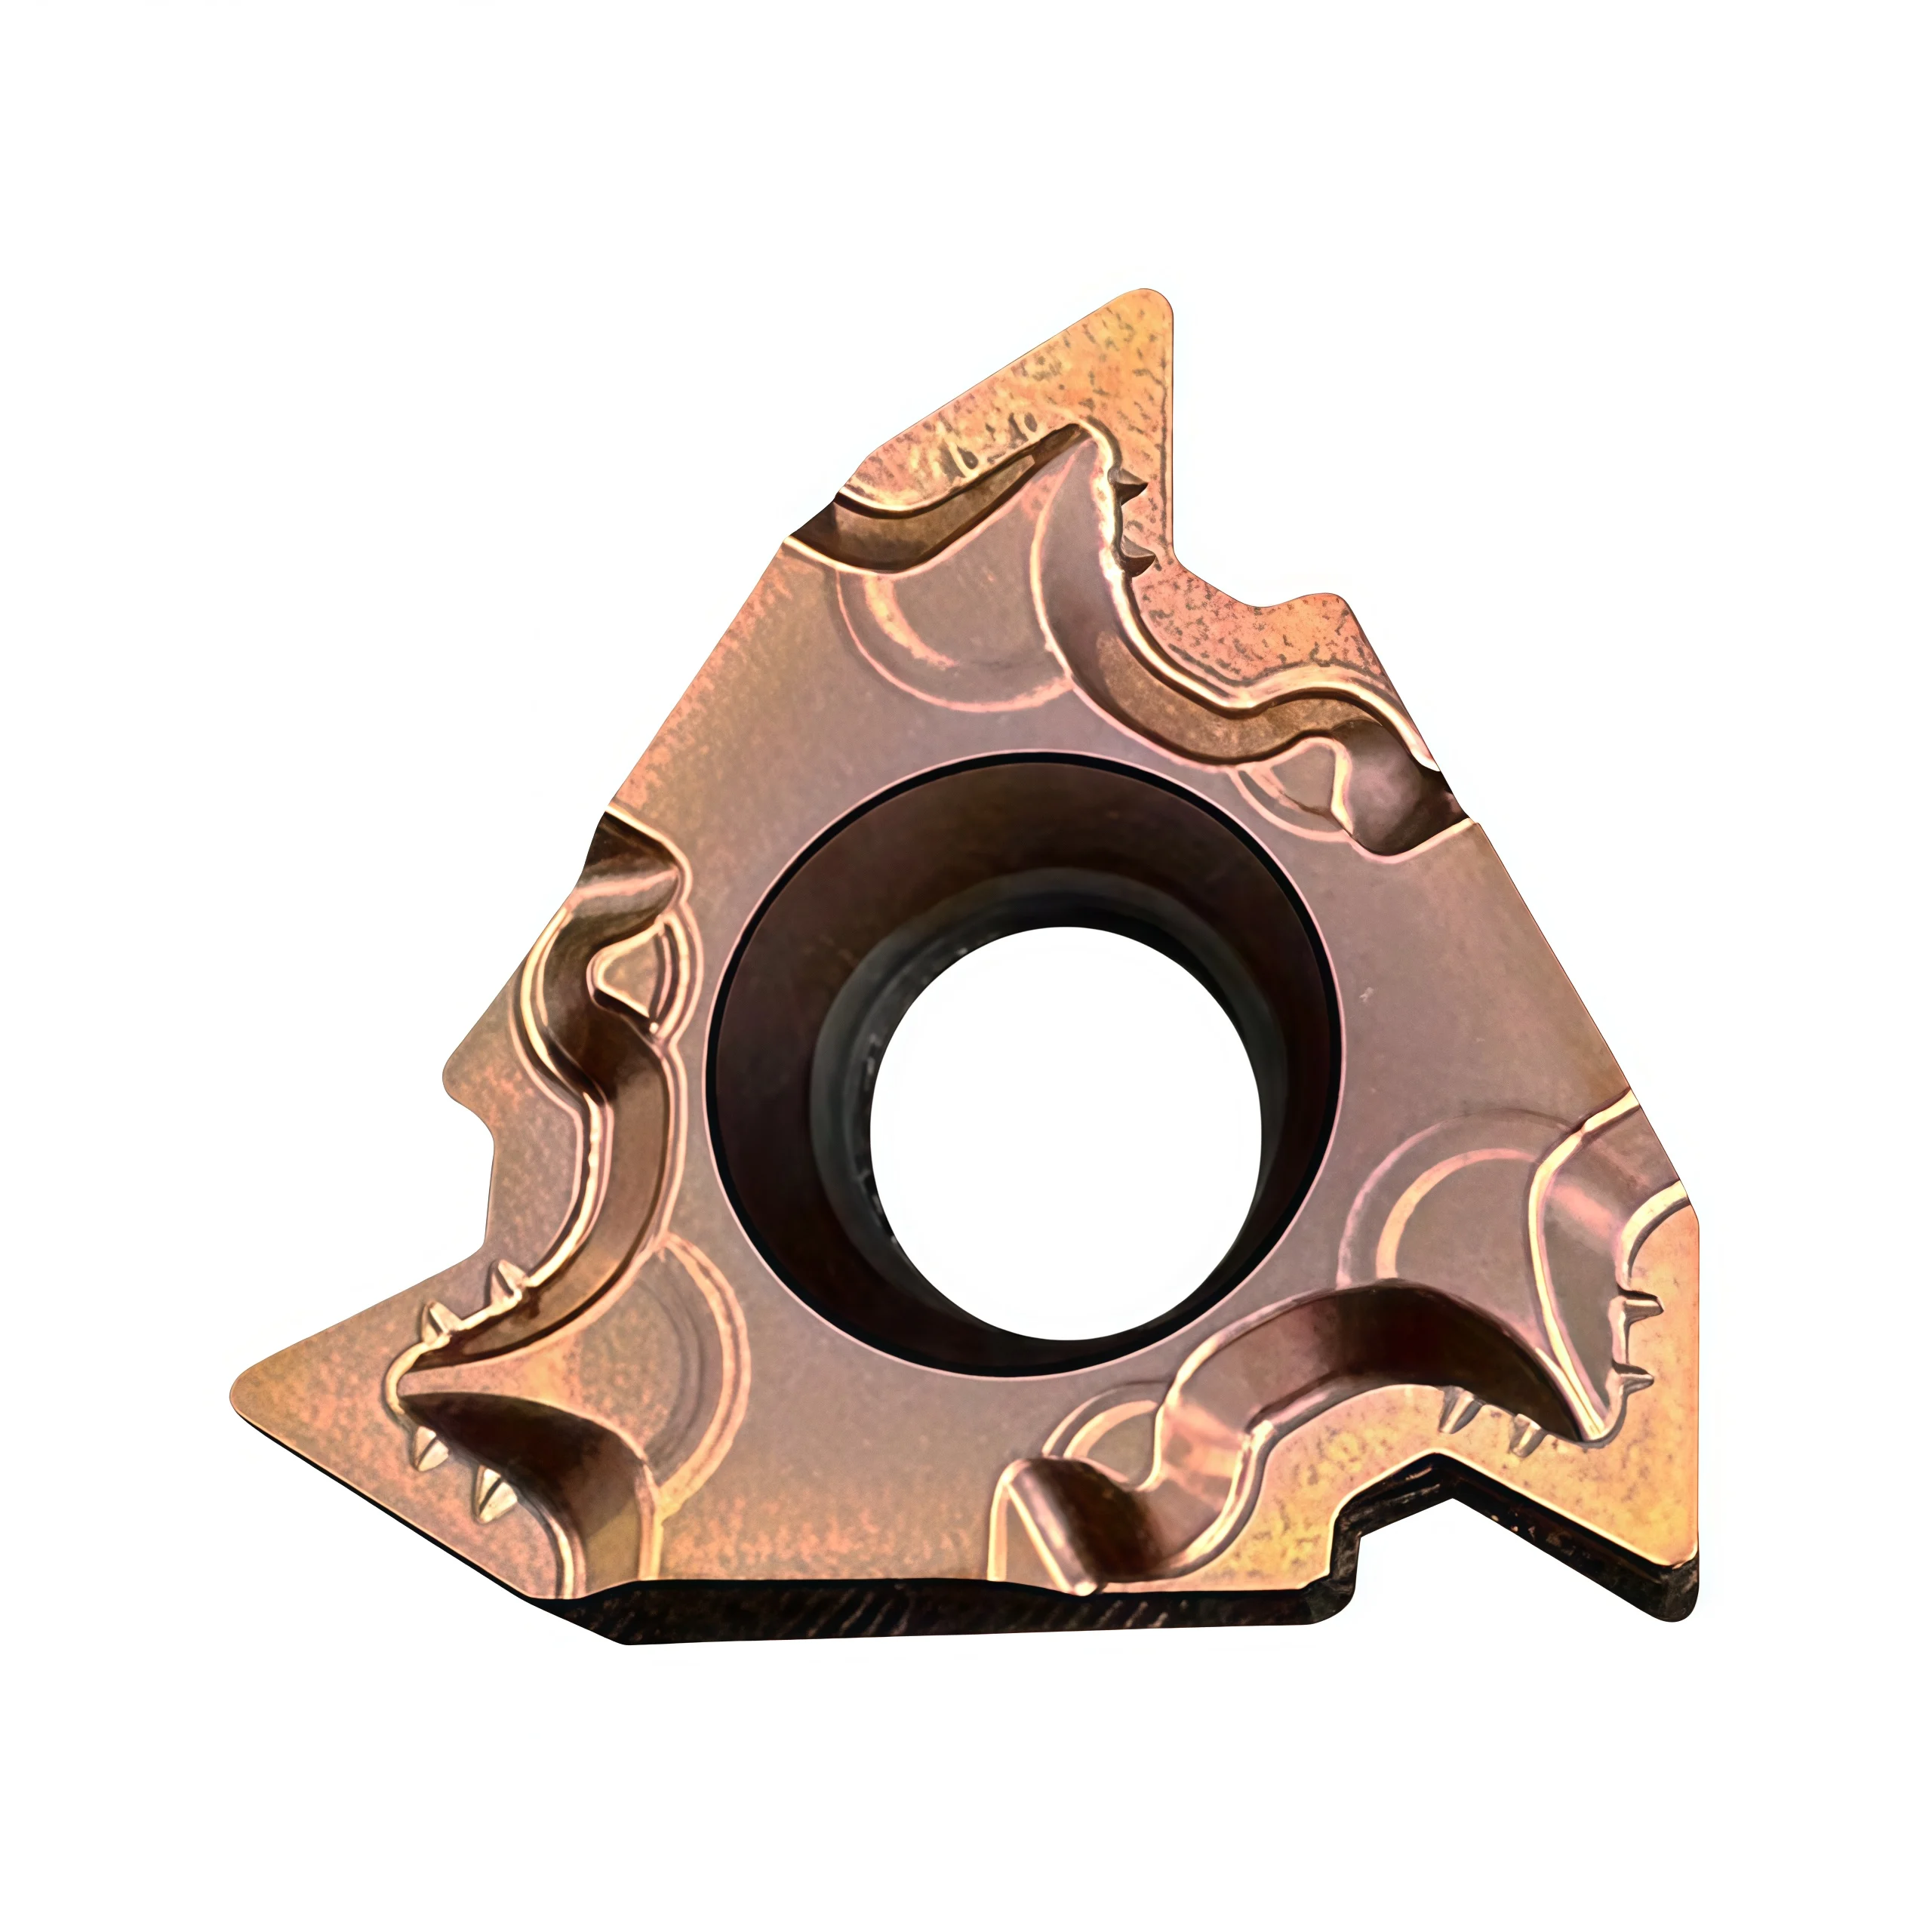
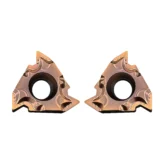
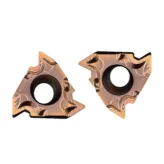
เม็ดมีดกลึงเกลียวคาร์ไบด์ 22ER/22IRM 3.5 ISO สำหรับสแตนเลส
22ER and 22IRM carbide inserts support external and internal ISO threading in stainless steel at a 3.5 mm pitch. Precision-ground profiles and application-matched coated grades help maintain thread form and edge durability, with code matching and private-label packaging available.
3.5 mm ISO Pitch
External / Internal
เหล็กไม่ржаว
บรรจุภัณฑ์ OEM
◆22ER/22IRM Insert Overview
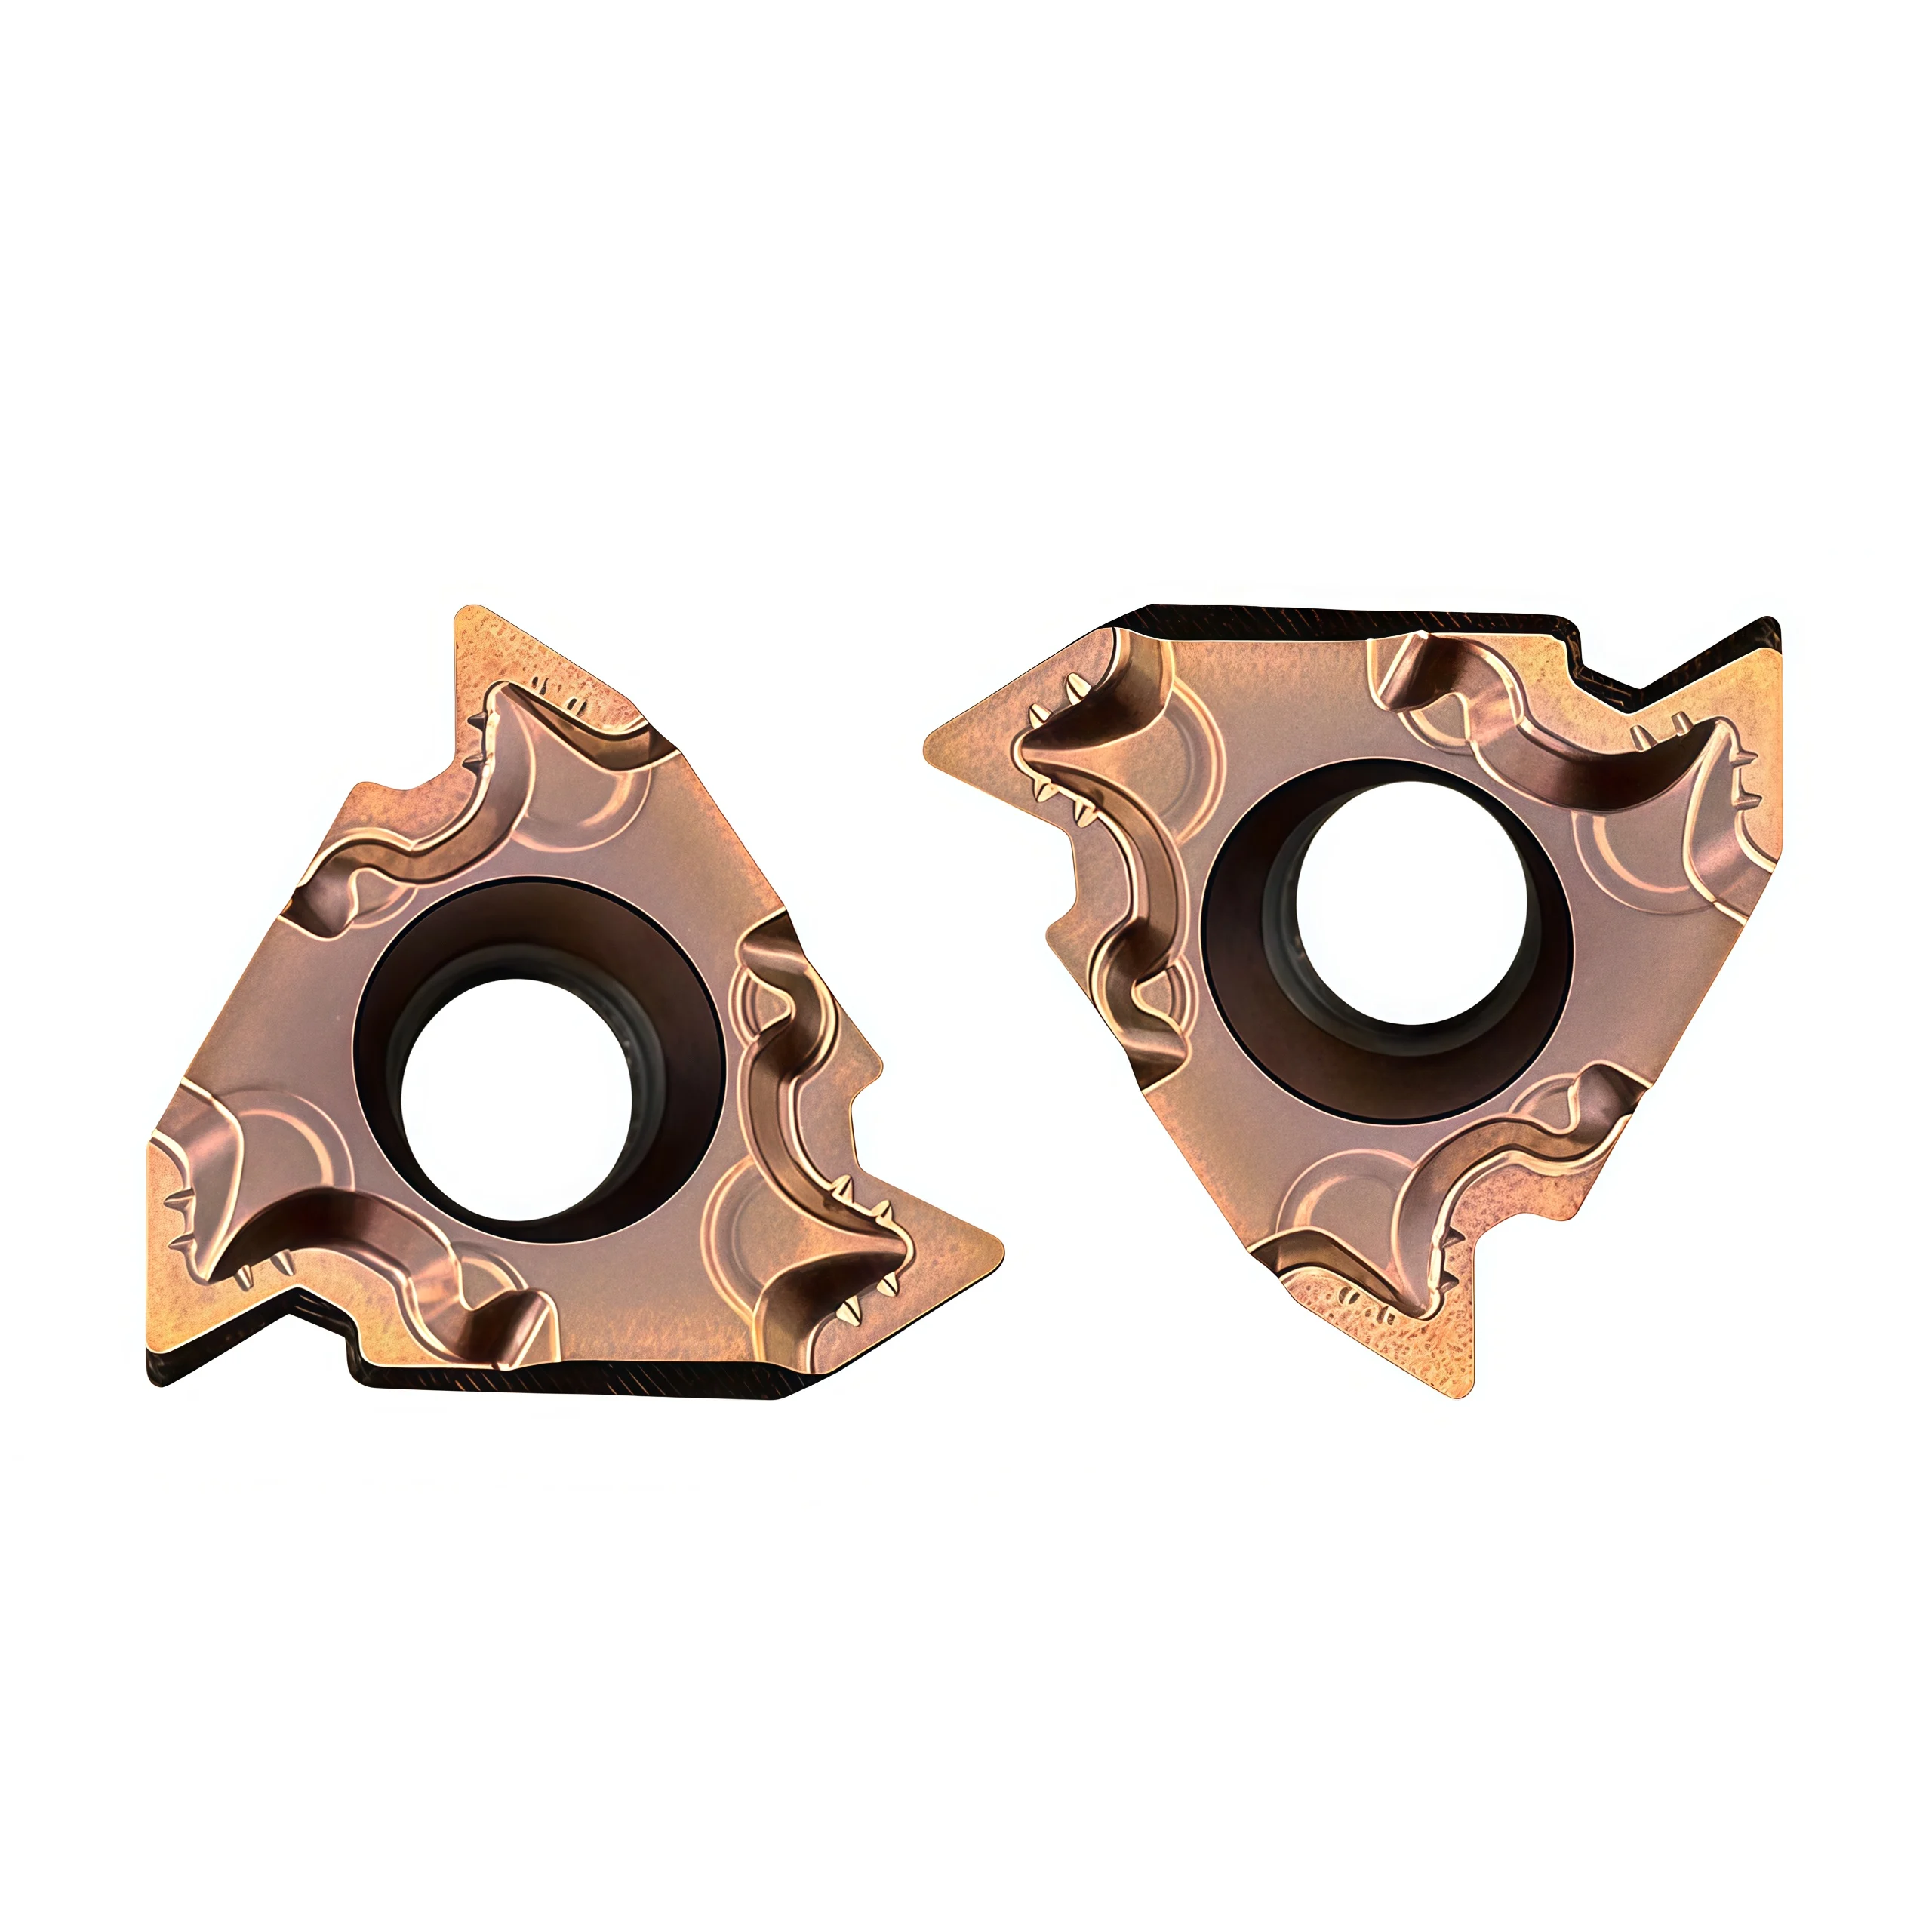
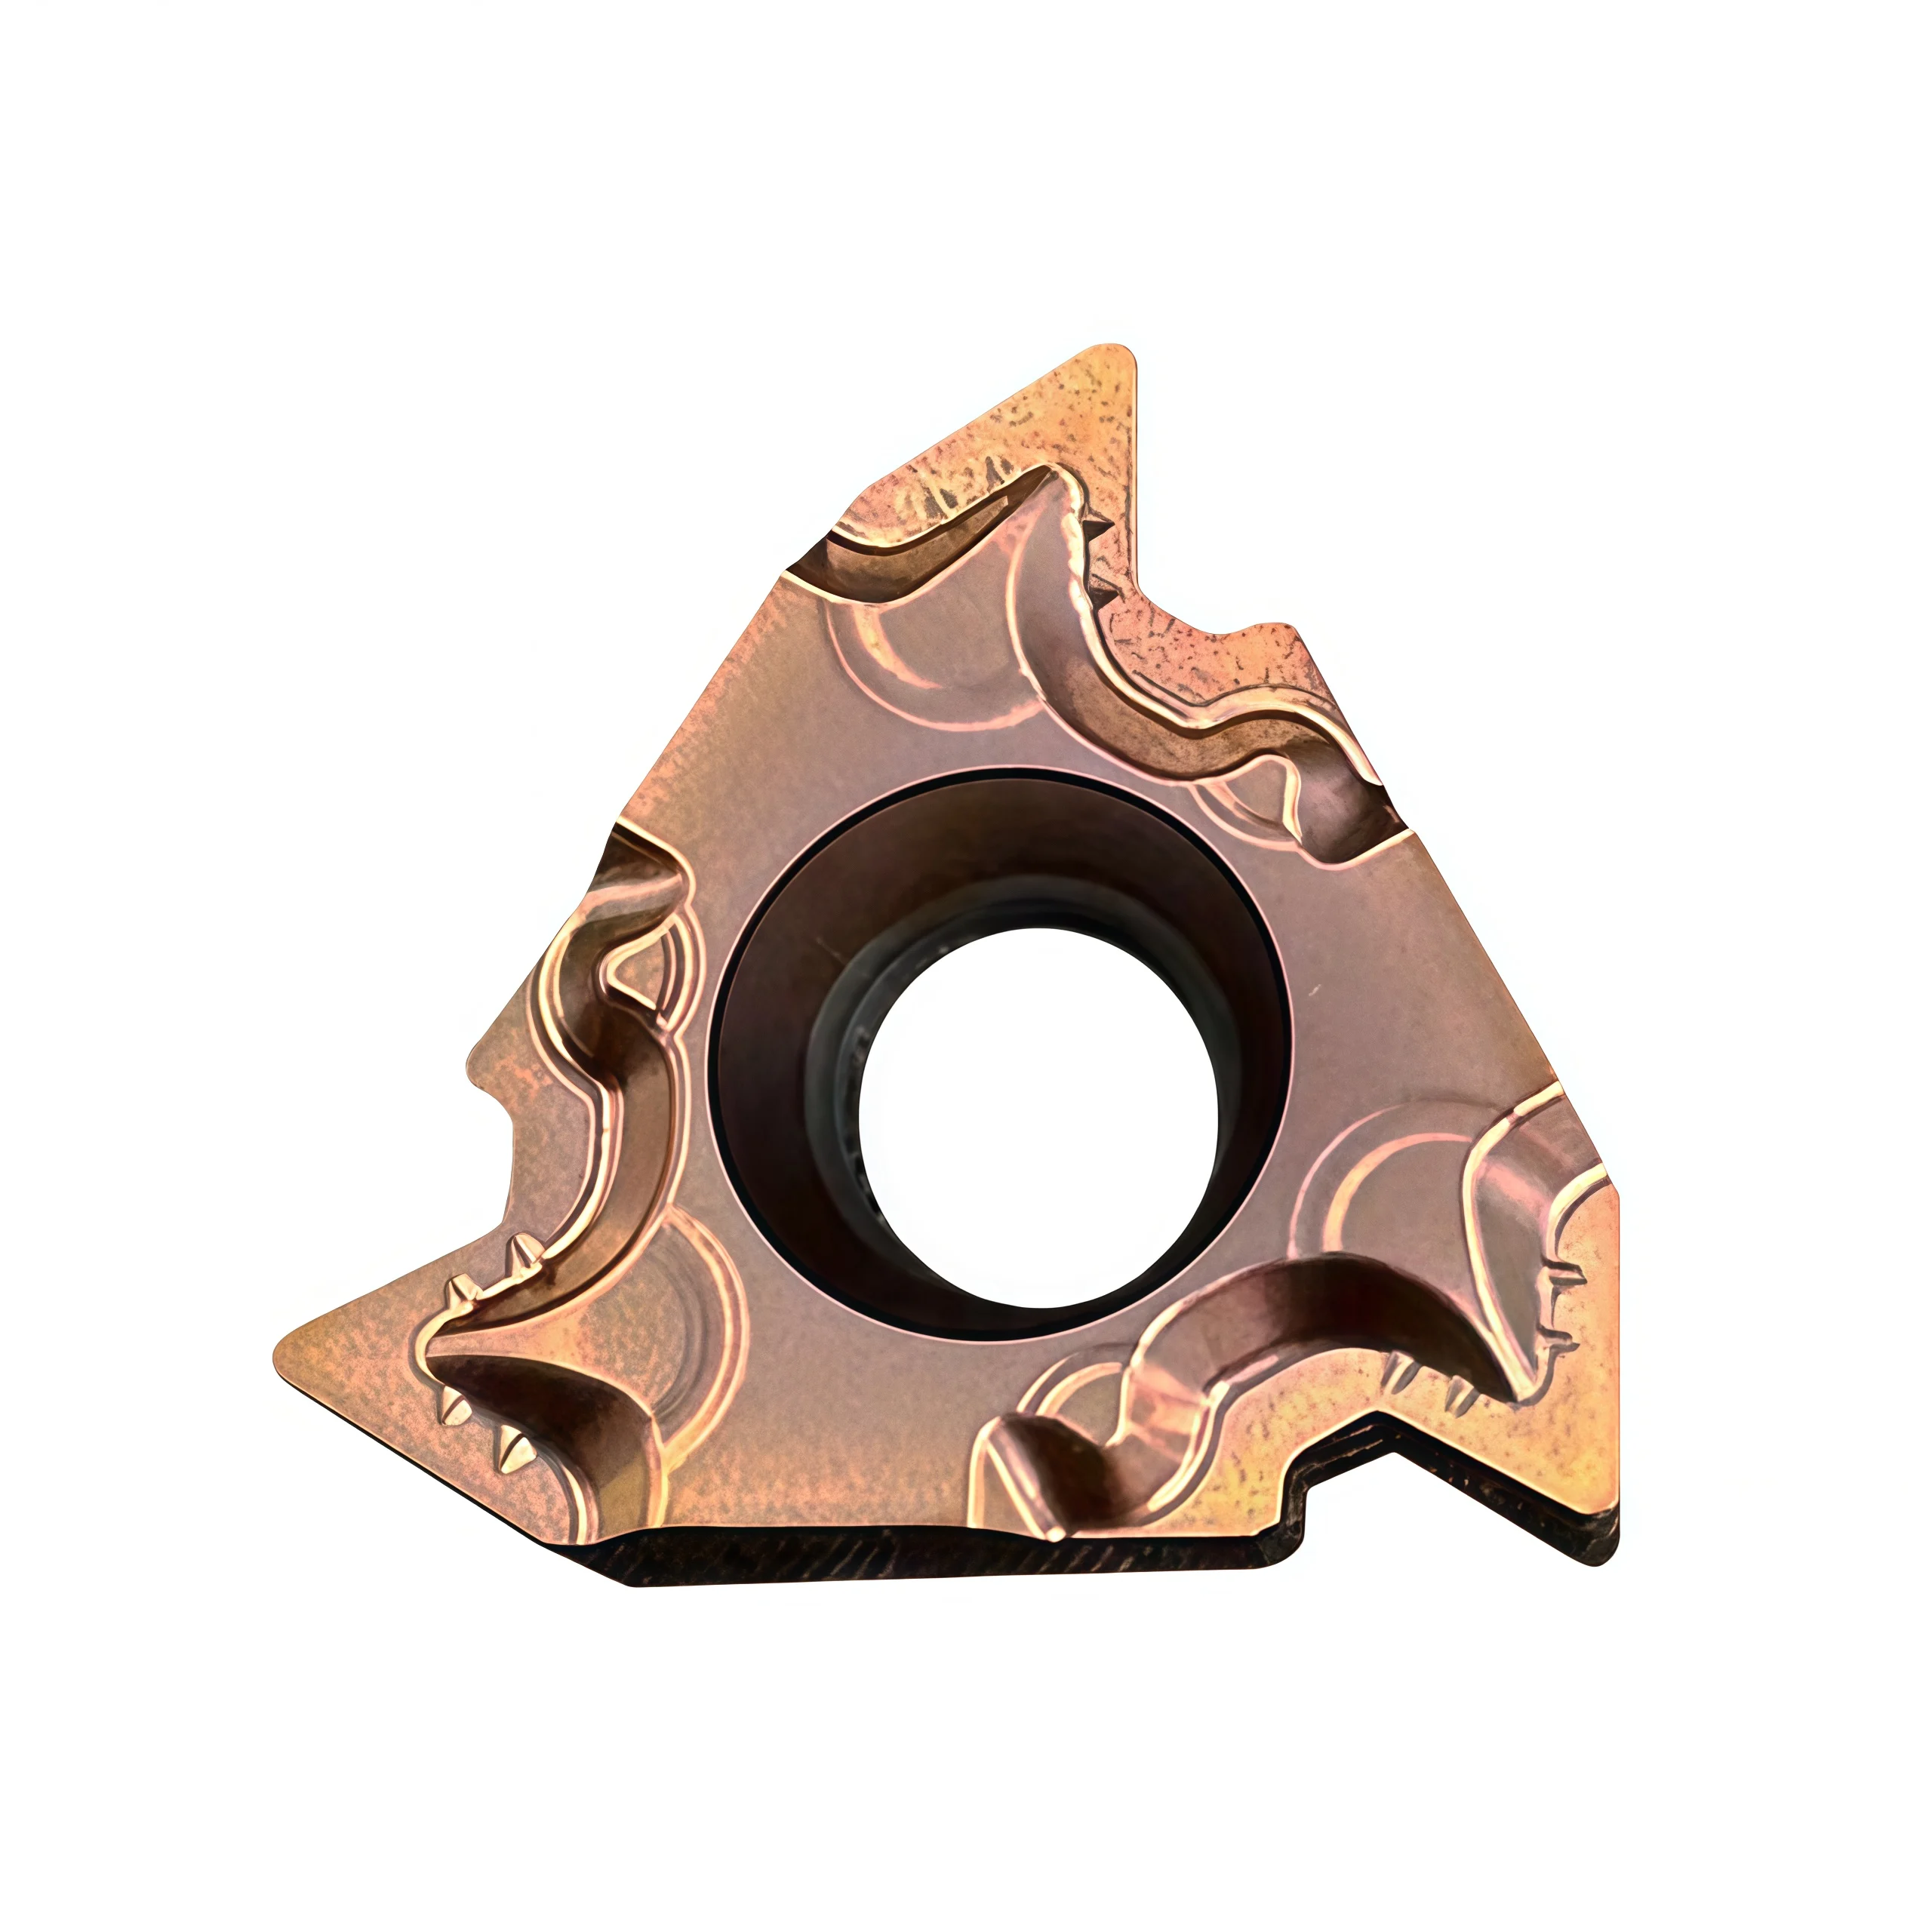
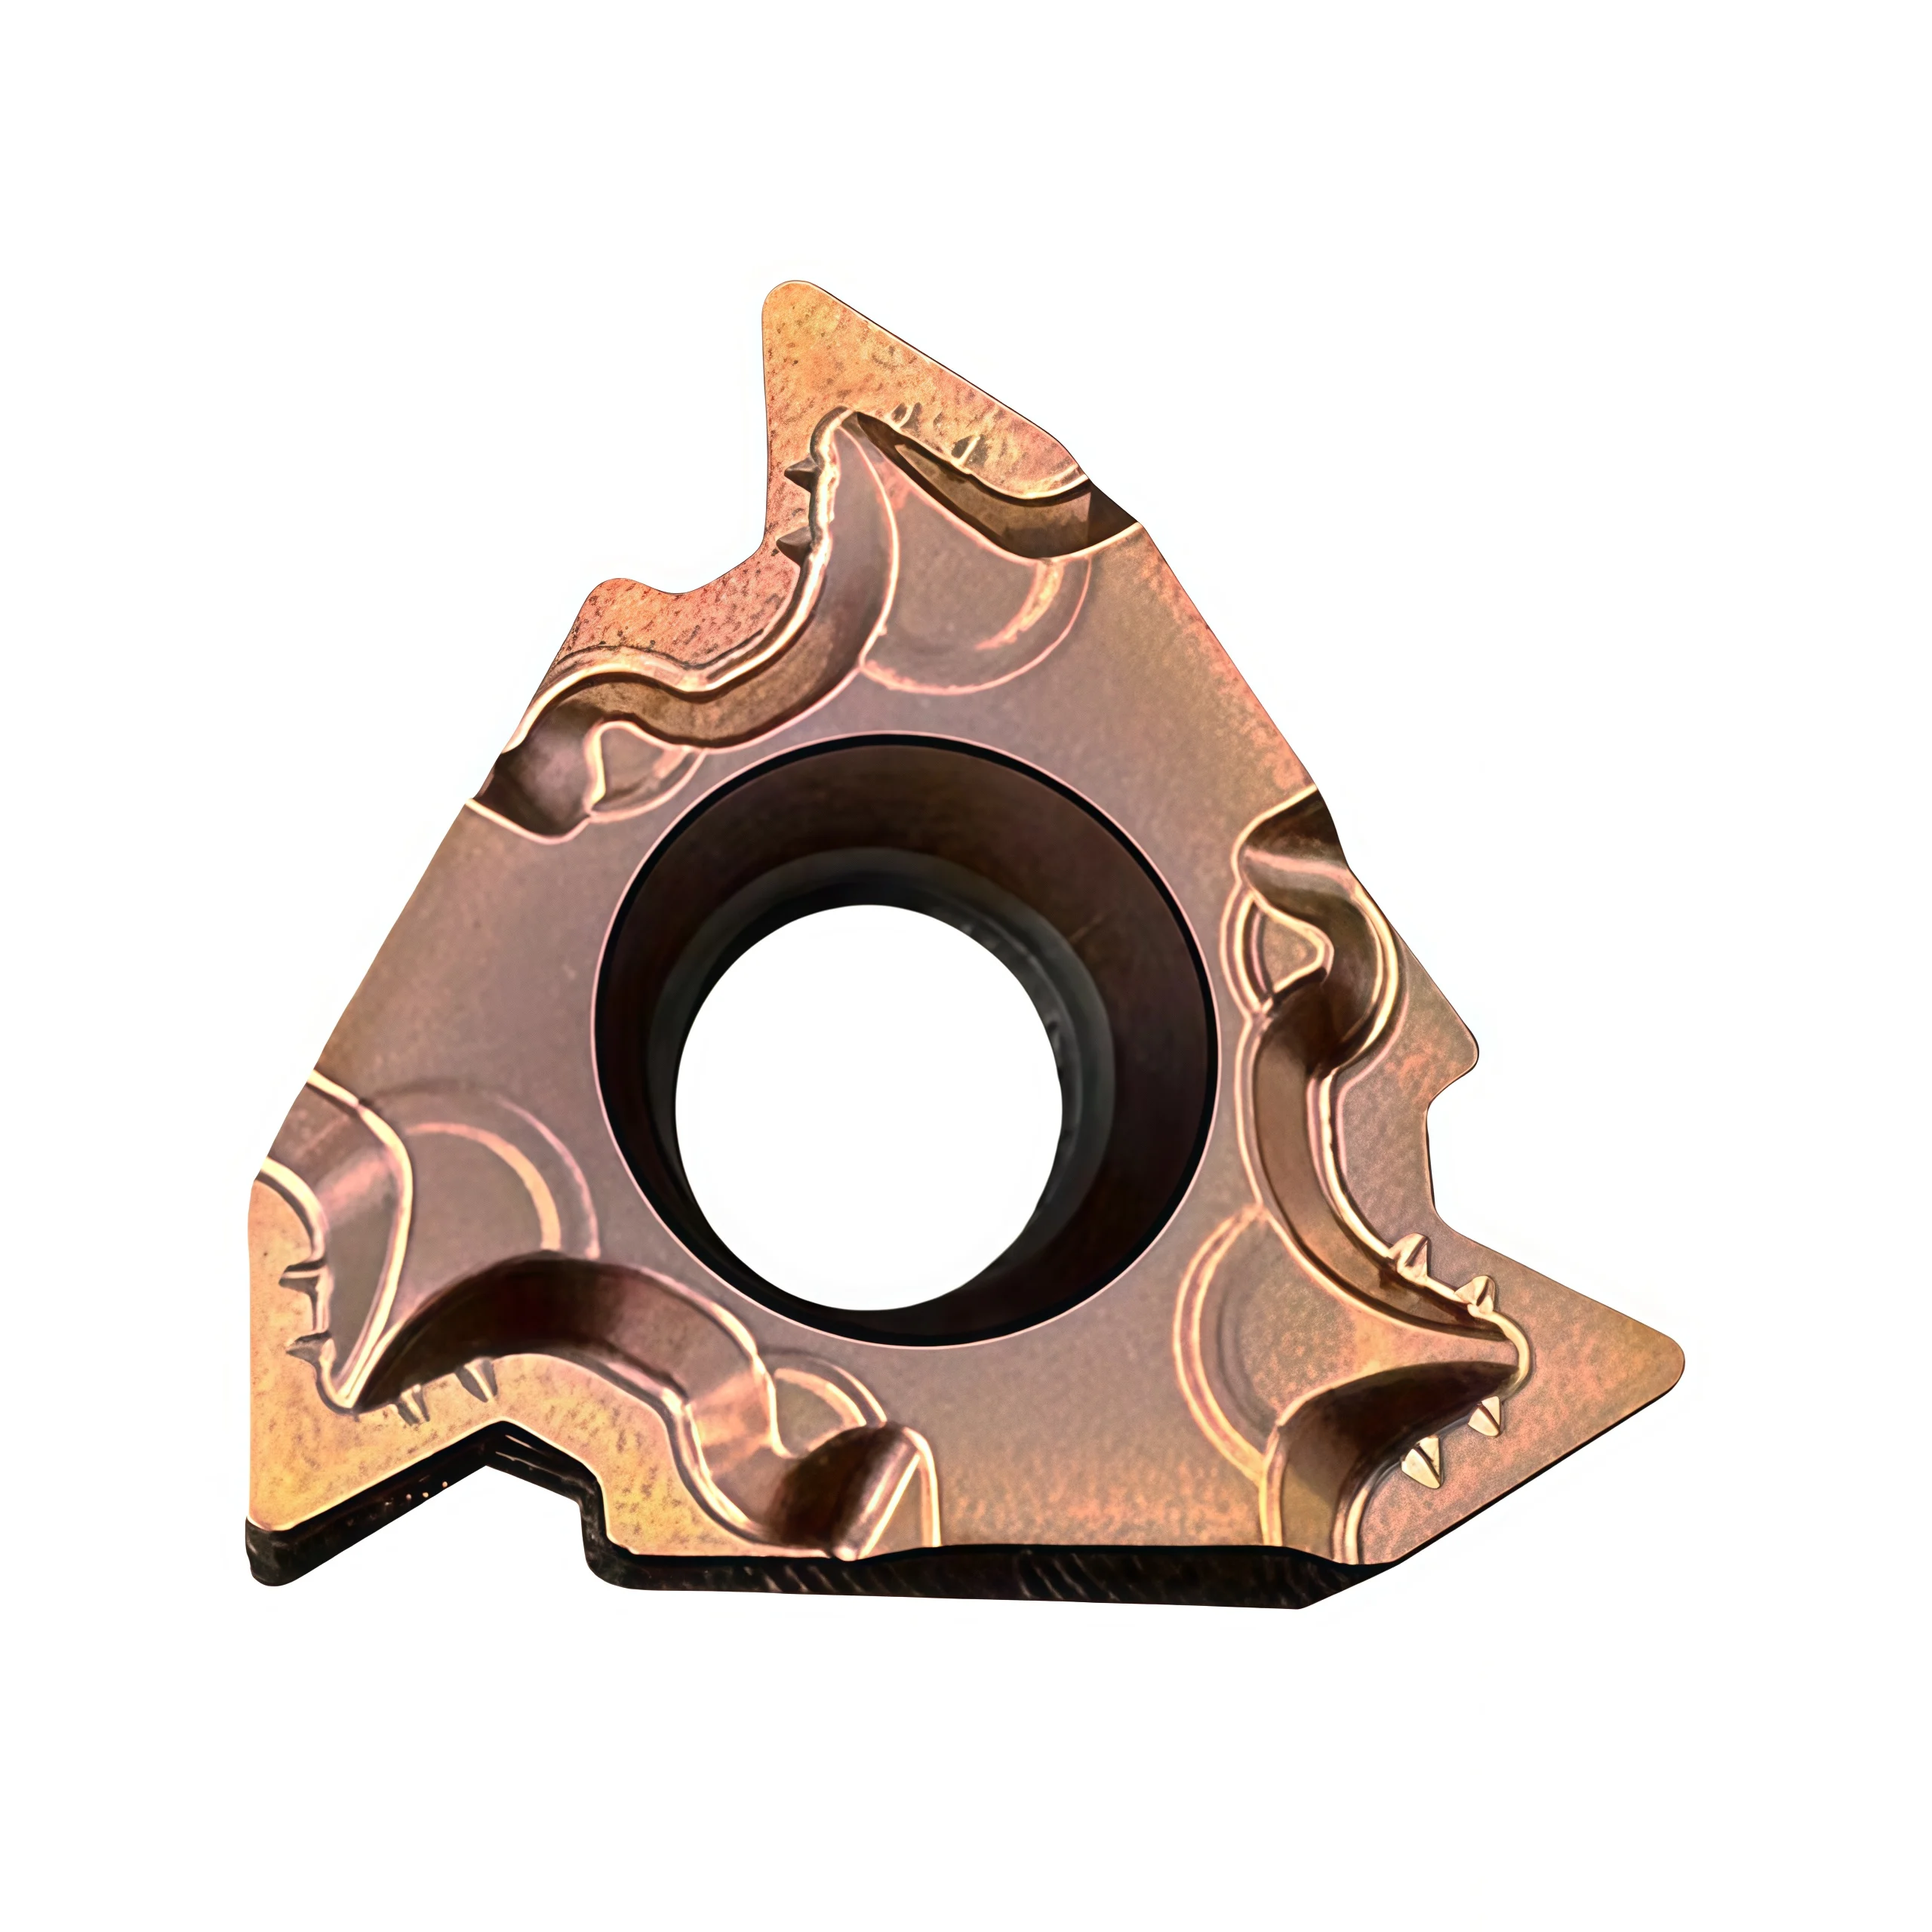
สิ่งเหล่านี้ 22-size carbide thread-turning inserts are presented for external (22ER) and internal (22IRM) 60° metric threading of stainless-steel components. Select a pitch-specific 3.5 ISO full-profile insert when the drawing calls for a 3.5 mm metric thread and a formed crest. An N60 partial-profile insert is a separate geometry that may cover a stated range of metric pitches; confirm the actual insert designation and range before ordering.
For 304, 316 or other stainless grades, review the insert’s verified carbide grade, coating, cutting-edge geometry and holder with the workpiece and thread drawing. Reliable threading also depends on suitable infeed passes, chip evacuation, correct helix clearance and finished-thread gauging. The exact dimensions and cutting data must be confirmed for the selected HY item.
◆Key Configurations
| Configuration | Selection Point |
|---|---|
| 22ER / 22IRM | External / internal threading insert families; match the insert to the correct holder and hand. |
| 3.5 ISO | Pitch-specific 60° ISO metric full-profile geometry for P = 3.5 mm, if confirmed on the SKU. |
| N60 | A 60° partial-profile geometry designation, not a carbide grade or the same edge as 3.5 ISO full profile. |
| Grade / coating | Confirm the actual carbide grade and coating for each complete item code; neither is established by “N60.” |
◆Stainless-Steel Threading Considerations
Profile and crest: a confirmed full-profile insert cuts the specified crest; a partial-profile insert requires the starting diameter to be prepared correctly.
Chip control: select a stainless-suitable edge and coating by grade, then check chip flow and coolant delivery during the trial cut.
Internal-thread clearance: check minimum bore, overhang, chip space, holder orientation and shim or anvil tilt for a 22IRM setup.
Thread verification: use the drawing’s thread class and an appropriate gauge; the profile name alone does not specify finished-thread tolerance.
◆Original Product Images
◆Application & Ordering
Send the metric thread designation and tolerance, 3.5 ISO or N60 profile choice, external/internal location, right/left hand, holder model, stainless-steel grade, diameter, thread length and quantity. Request a drawing and material-specific cutting recommendation for the selected configuration.
See our คู่มือการเลือกอินเสิร์ต CNC หรือ request a specification check.
◆Specifications & Configurations
Choose the complete insert code by thread location, pitch-specific or partial-profile geometry, material grade and holder. The source description gives no HY dimension drawing or verified grade code, so dimensions and cutting speeds should be confirmed against the ordered item.
| พารามิเตอร์ | Specification / Confirmation |
|---|---|
| Insert family | 22ER for external threading; 22IRM for internal threading. “22” is an insert-size family, not the workpiece diameter. |
| Thread form | 60° metric ISO profile; confirm the complete thread designation and tolerance from the drawing. |
| 3.5 ISO option | Nominal P = 3.5 mm, pitch-specific full profile with crest-forming edge when verified by the full model code. |
| N60 option | 60° partial V-profile designation; confirm the actual pitch range and crest preparation for the HY SKU. |
| วัสดุของเครื่องมือ | Carbide substrate; specific grade and coating to be confirmed. N60 is not a substrate or PVD grade. |
| Workpiece focus | Stainless steel; check exact grade, hardness and cutting conditions for the quoted insert grade. |
| Dimensions / fit | Verify insert dimensions, pocket, clamping method, hand, shim/anvil and minimum bore against the HY drawing and holder. |
| Ordering | Specify profile, ER or IRM, right/left hand, grade/coating and quantity on each order line. |
◆3.5 ISO vs. N60 Profile
| Feature | 3.5 ISO full profile | N60 partial profile |
|---|---|---|
| Pitch selection | P = 3.5 mm. | Multiple stated pitches; request the HY product's approved range. |
| Thread crest | Forms the crest when the starting diameter leaves suitable finishing stock. | Does not top the crest; prepare the outside or bore diameter first. |
| Order check | Confirm metric full-profile SKU and 3.5 mm pitch. | Confirm V-profile code, pitch range and minimum nose radius. |
◆Cutting Data & Setup
Axial feed: For a single-start P3.5 metric thread, the tool advances 3.5 mm per spindle revolution along the thread axis. Use a suitable series of controlled radial or flank infeed passes; this feed value does not call for the full thread depth in one pass.
Speed and coolant: Select starting cutting speed, pass distribution and coolant from the confirmed grade and coating, stainless-steel grade, diameter, depth, holder rigidity and chip behavior. No universal speed, minimum coolant pressure or tool-life increase is specified here.
For the final dimension sheet, holder fit and cutting recommendation, ส่งรหัสชิ้นส่วนแทรกและตัวถือทั้งหมด with the thread drawing and workpiece grade.
◆การปรับแต่งชิ้นส่วนคาร์ไบด์และบริการ OEM
โปรดระบุใบตัดสำหรับกระบวนการกลึง ชิ้นงาน และอุปกรณ์จับยึด เราสามารถตรวจสอบตัวเลือกใบตัดมาตรฐาน รูปทรงเฉพาะตามการใช้งาน และข้อกำหนดสำหรับแบรนด์ส่วนตัว โดยใช้รหัสใบตัด แบบวาด หรือตัวอย่างของท่าน เกรด ชั้นเคลือบ ขนาด และปริมาณการสั่งซื้อที่มีอยู่จะได้รับการยืนยันสำหรับแต่ละซีรีส์ที่ท่านขอ.
เรขาคณิตและการควบคุมชิป
ตรวจสอบตัวตัดเศษ (chipbreaker), มุมเอียง (rake), การเตรียมคมตัด (cutting-edge preparation), รัศมีปลายคม (nose radius) และออกแบบมุม (corner design) ให้เหมาะสมกับกระบวนการทำงานและชิ้นงาน ตรวจสอบความเข้ากันได้ของตัวจับ (holder) ก่อนอนุมัติรูปทรงที่ปรับเปลี่ยนแล้ว.
วัสดุฐานและชั้นเคลือบ
เลือกชนิดคาร์ไบด์และชั้นเคลือบที่เหมาะสมกับวัสดุชิ้นงาน สภาพการตัด และความสมดุลที่ต้องการระหว่างความทนต่อการสึกหรอและความแข็งของขอบตัด.
ขนาดและ OEM
ตรวจสอบขนาดของแผ่นแทรก ความหนา คุณสมบัติการกำหนดตำแหน่งและการยึดตรึง ค่าความคลาดเคลื่อน การทำเครื่องหมายด้วยเลเซอร์ และการบรรจุภัณฑ์ภายใต้แบรนด์ส่วนตัว ให้สอดคล้องกับข้อกำหนดที่ได้รับการอนุมัติ.
◆ตัวเลือกการปรับแต่ง
โปรดใช้ช่องข้อมูลด้านล่างเมื่อส่งคำสอบถาม ตัวเลือกที่แน่นอนจะขึ้นอยู่กับตระกูลชิ้นส่วน และจะได้รับการยืนยันในใบเสนอราคาหรือแบบวาดที่ได้รับการอนุมัติ.
| ข้อมูลทางเทคนิค | รายละเอียดที่ต้องยืนยัน |
|---|---|
| ประเภทการแทรก | ใบตัดสำหรับการกลึง การกัด การทำเกลียว การทำร่อง หรือการเจาะ; โปรดส่งรหัสสินค้าหรือแบบวาดมา. |
| ขนาดและรูปทรง | รูปทรง ขนาด ความหนา เส้นผ่านศูนย์กลางของวงที่เขียนได้หรือความยาวของขอบ รูปแบบของรูหรือส่วนจับยึด และรุ่นของตัวจับยึด. |
| รูปทรงการตัด | ตัวหักเศษ, รัศมีปลายหรือมุม, การเตรียมคมตัด, ทิศทางการตัด และรูปทรงที่เหมาะสมกับการใช้งานเฉพาะ. |
| เกรดและชั้นเคลือบ | กลุ่มและระดับของชิ้นงาน, วัสดุฐานคาร์ไบด์, ระบบการเคลือบ และสภาพการตัดแบบเปียกหรือแห้ง. |
| ความทนทานและการตรวจสอบ | ขนาดสำคัญ ข้อกำหนดเกี่ยวกับรูปทรง วิธีการตรวจสอบ และรายงานที่จำเป็น. |
| การนำเสนอของ OEM | การพิมพ์หรือทำเครื่องหมายบนกล่อง, เนื้อหาบนฉลาก, รูปแบบบรรจุภัณฑ์ และจำนวนต่อแพ็ก. |
◆วิธีขอทำแผ่นแทรกตามสั่ง

ส่งความต้องการเกี่ยวกับใบแทรกของคุณผ่านทาง แบบฟอร์มติดต่อ หรือดูข้อมูลเพิ่มเติมของเรา บริการ OEM และบริการแบรนด์ส่วนตัว.
◆การควบคุมคุณภาพของแผ่นคาร์ไบด์

คุณภาพของชิ้นส่วนแทรกขึ้นอยู่กับระดับคุณภาพที่ได้รับการอนุมัติ รูปทรง การเคลือบผิว และข้อกำหนดด้านขนาด เราจะตรวจสอบข้อกำหนดเมื่อยืนยันคำสั่งซื้อ และปรับขอบเขตการตรวจสอบให้สอดคล้องกับซีรีส์ของชิ้นส่วนแทรกและแบบวาดของลูกค้า หากมี โปรดแจ้งขนาดสำคัญหรือความต้องการด้านเอกสารก่อนเริ่มการผลิต เพื่อให้สามารถรวมไว้ในแผนการตรวจสอบที่ตกลงกันไว้.
01 · วัสดุที่รับเข้า
ตรวจสอบให้แน่ใจว่าเกรดคาร์ไบด์หรือเอกสารเกี่ยวกับวัสดุที่ระบุไว้ตรงกับข้อกำหนดในคำสั่งซื้อ.
02 · การตรวจสอบระหว่างกระบวนการผลิต
ตรวจสอบขนาดและคุณสมบัติขั้นสูงระหว่างกระบวนการผลิต เพื่อให้สอดคล้องกับข้อกำหนดที่ได้รับการอนุมัติ.
03 · การตรวจสอบขั้นสุดท้าย
ตรวจสอบขนาดที่ตกลงกันไว้ ลักษณะภายนอก สภาพขอบ การระบุชนิดการเคลือบ และการทำเครื่องหมายตามความเหมาะสม.
04 · บทรีวิวการแพ็กของ
ตรวจสอบรหัสสินค้า ปริมาณ ป้าย และบรรจุภัณฑ์ป้องกัน ให้ตรงกับคำสั่งซื้อที่ได้รับการอนุมัติ.
◆การตรวจสอบและจัดทำเอกสาร
ควรตกลงกันเกี่ยวกับจุดตรวจสอบและเกณฑ์การรับสินค้าสำหรับชุดสินค้าที่สั่งซื้อ สำหรับชิ้นส่วนแทรกที่ผลิตตามสั่ง แบบวาดที่ได้รับการอนุมัติจะมีน้ำหนักมากกว่าคำอธิบายทั่วไปในแคตตาล็อก.
| ตรวจสอบพื้นที่ | สิ่งที่ต้องตรวจสอบ |
|---|---|
| ขนาดและรูปทรง | ระบุขนาด ความหนา รัศมีมุม คุณสมบัติการยึด และค่าความคลาดเคลื่อนในแบบวาด (หากมี). |
| รูปทรงการตัด | ตัวตัดเศษ, การเตรียมขอบ, มุมที่สามารถใช้งานได้ และรูปทรงตามความเหมาะสม. |
| เกรดและชั้นเคลือบ | ระดับที่ได้รับการอนุมัติและชื่อประเภทการเคลือบ; วิธีตรวจสอบตามคำขอใดๆ. |
| รูปลักษณ์และบรรจุภัณฑ์ | ความเสียหายที่เห็นได้ชัดบริเวณขอบ, รอยเครื่องหมาย, รหัสสินค้า, จำนวน และรูปแบบการบรรจุ. |
| เอกสารที่ขอ | รายงานการตรวจสอบ เอกสารเกี่ยวกับวัสดุหรือชั้นเคลือบ การอนุมัติตัวอย่าง หรือการระบุล็อต ตามที่ตกลงกัน. |
◆การสั่งซื้อและการส่งสินค้า
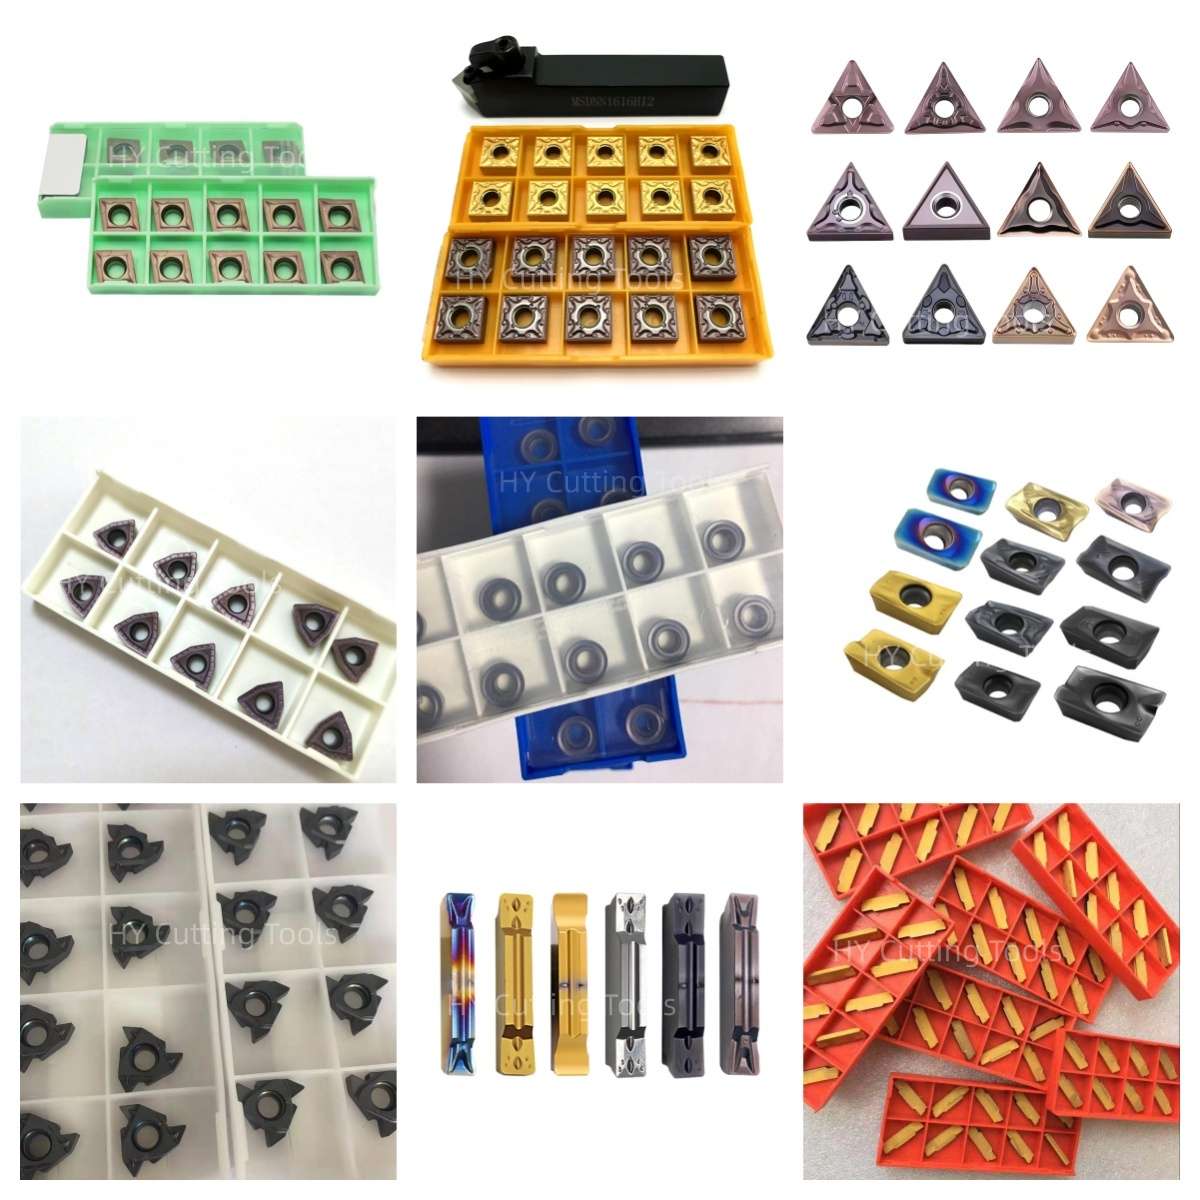

โปรดส่งรายชื่อรหัสสินค้าและปริมาณการสั่งซื้อแบบบรรทัดต่อบรรทัด สำหรับใบเสนอราคาที่มีขนาดสินค้าหลากหลาย โดยสถานะสินค้าในสต็อก ปริมาณสั่งซื้อขั้นต่ำ ข้อกำหนดเกี่ยวกับตัวอย่าง และระยะเวลาการผลิต ได้ถูกยืนยันแล้วสำหรับแต่ละเกรด ชั้นเคลือบ และรูปแบบสินค้า.
ส่งรายชื่อสินค้าและข้อกำหนดด้านคุณภาพผ่านทาง แบบฟอร์มติดต่อ เพื่อตรวจสอบรายละเอียดทางเทคนิค ความพร้อมในการจัดส่ง และการยืนยันการจัดส่ง.
◆คำถามที่พบบ่อยเกี่ยวกับผลิตภัณฑ์
What is the difference between 22ER and 22IRM?
22ER designates an external thread-turning insert, while 22IRM is an internal-threading variant. Match each insert to its approved holder, orientation, hand and clamping arrangement; check the minimum bore and boring-bar overhang for internal work.
Does “3.5 ISO” mean a 3.5 mm metric pitch?
Yes, in a verified 3.5 ISO full-profile threading insert designation it refers to a 60° metric thread with P = 3.5 mm. The finished thread size and tolerance still come from the workpiece drawing.
Is N60 the carbide grade or the same as 3.5 ISO?
No. N60 identifies a 60° partial-profile geometry in the referenced insert nomenclature; it is not a carbide grade. A 3.5 ISO full-profile edge forms the pitch-specific crest, while a partial-profile N60 edge does not. Confirm the complete HY item code and actual grade.
Can an N60 partial-profile insert cut a 3.5 mm thread?
Only when the selected SKU's approved pitch range includes 3.5 mm and its nose radius fits the required thread form. Prepare the outside or bore diameter for the crest before cutting, then gauge the final thread.
Are all 22ER/22IRM variants suitable for 304, 316 and duplex stainless steel?
Suitability depends on the confirmed carbide grade, coating, edge geometry, workpiece hardness and cutting conditions. Provide the exact stainless grade, thread dimensions and holder so the insert and trial settings can be selected by application.
Should P3.5 threading be completed in one pass?
No. For a single-start P3.5 thread, synchronized axial advance is 3.5 mm per revolution; the thread depth is normally reached over multiple controlled infeed passes. Set cutting speed and pass schedule for the actual insert grade, material and setup.
◆คำถามที่พบบ่อยเกี่ยวกับการสั่งซื้อและ OEM
What details should I send for an exact quotation?
Send the full insert code or box-label photo, 3.5 ISO or N60 profile, ER/IRM application, hand, holder code, complete metric thread designation and tolerance, stainless-steel grade, thread diameter and length, quantity and packaging requirements.
Can I use an insert with the same “22” designation in my current holder?
The 22 family name alone does not establish pocket fit. Compare the complete insert dimensions, locating surfaces, clamp, shim or anvil, right/left hand and holder manufacturer's approved models before substitution.
Is PVD coating standard, and what cutting speed should I use?
The original description does not identify a verified HY grade or coating for each code. Ask for the actual grade and its stainless-steel cutting data; cutting speed also depends on the workpiece grade, diameter, setup, thread depth and coolant.
Are samples or custom markings available?
Include the complete model, quantity, drawing and any marking or box-label requirements in the inquiry. Sample availability, OEM options, minimum quantity and dispatch time are confirmed against the chosen configuration.
◆คู่มือและข้อมูลอ้างอิงทางเทคนิค
ใช้ คู่มือการเลือกอินเสิร์ต CNC to review insert grade, geometry and holder checks. Refer to the selected model's drawing and cutting data before programming.
For the full product designation and availability, send your thread drawing and holder code.
ต้องการทราบขนาด ราคา หรือตัวเลือกการปรับแต่งตามความต้องการหรือไม่?
ส่งรายละเอียดและจำนวนที่ต้องการเพื่อรับใบเสนอราคา.
- ขนาดมาตรฐาน
- คำสั่งซื้อทดลองในปริมาณน้อย
- ขนาดผสม
- OEM และตามสั่ง
ดูรหัส QR – ติดต่อฝ่ายขายผ่าน WeChat
สแกนเพื่อติดต่อเราผ่าน WeChat.
สแกนเพื่อติดต่อเราผ่าน WeChat.