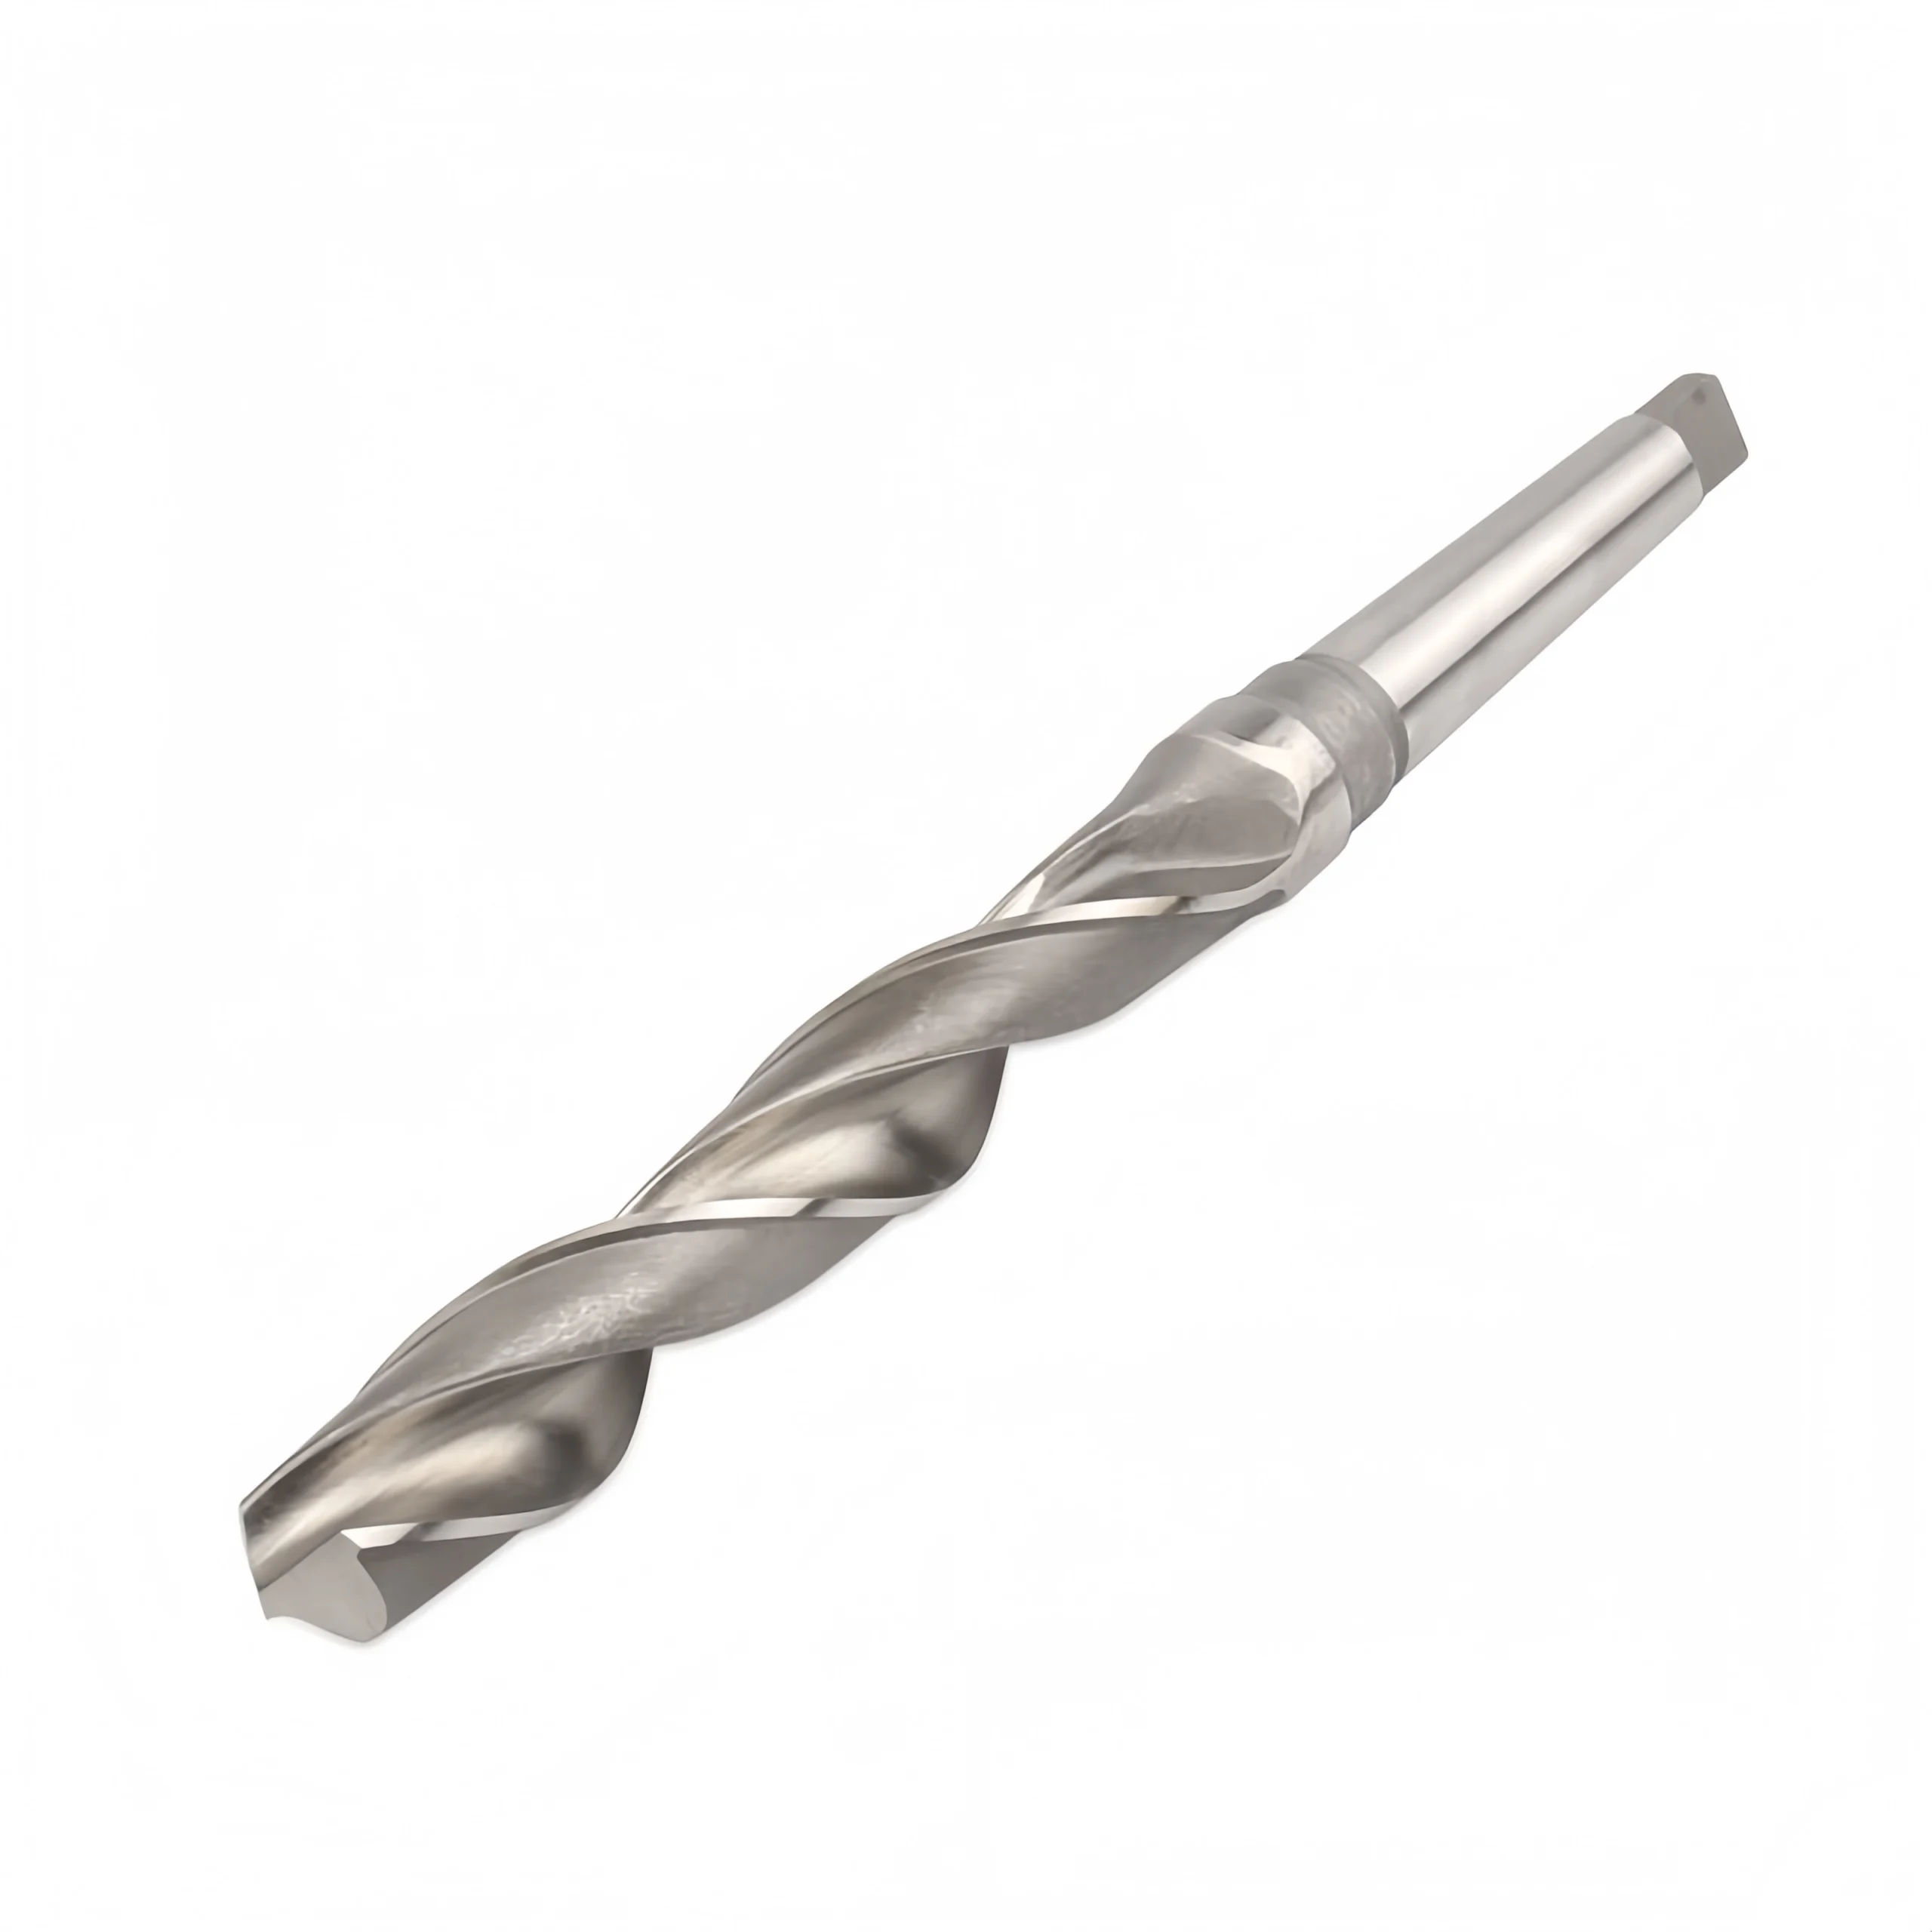

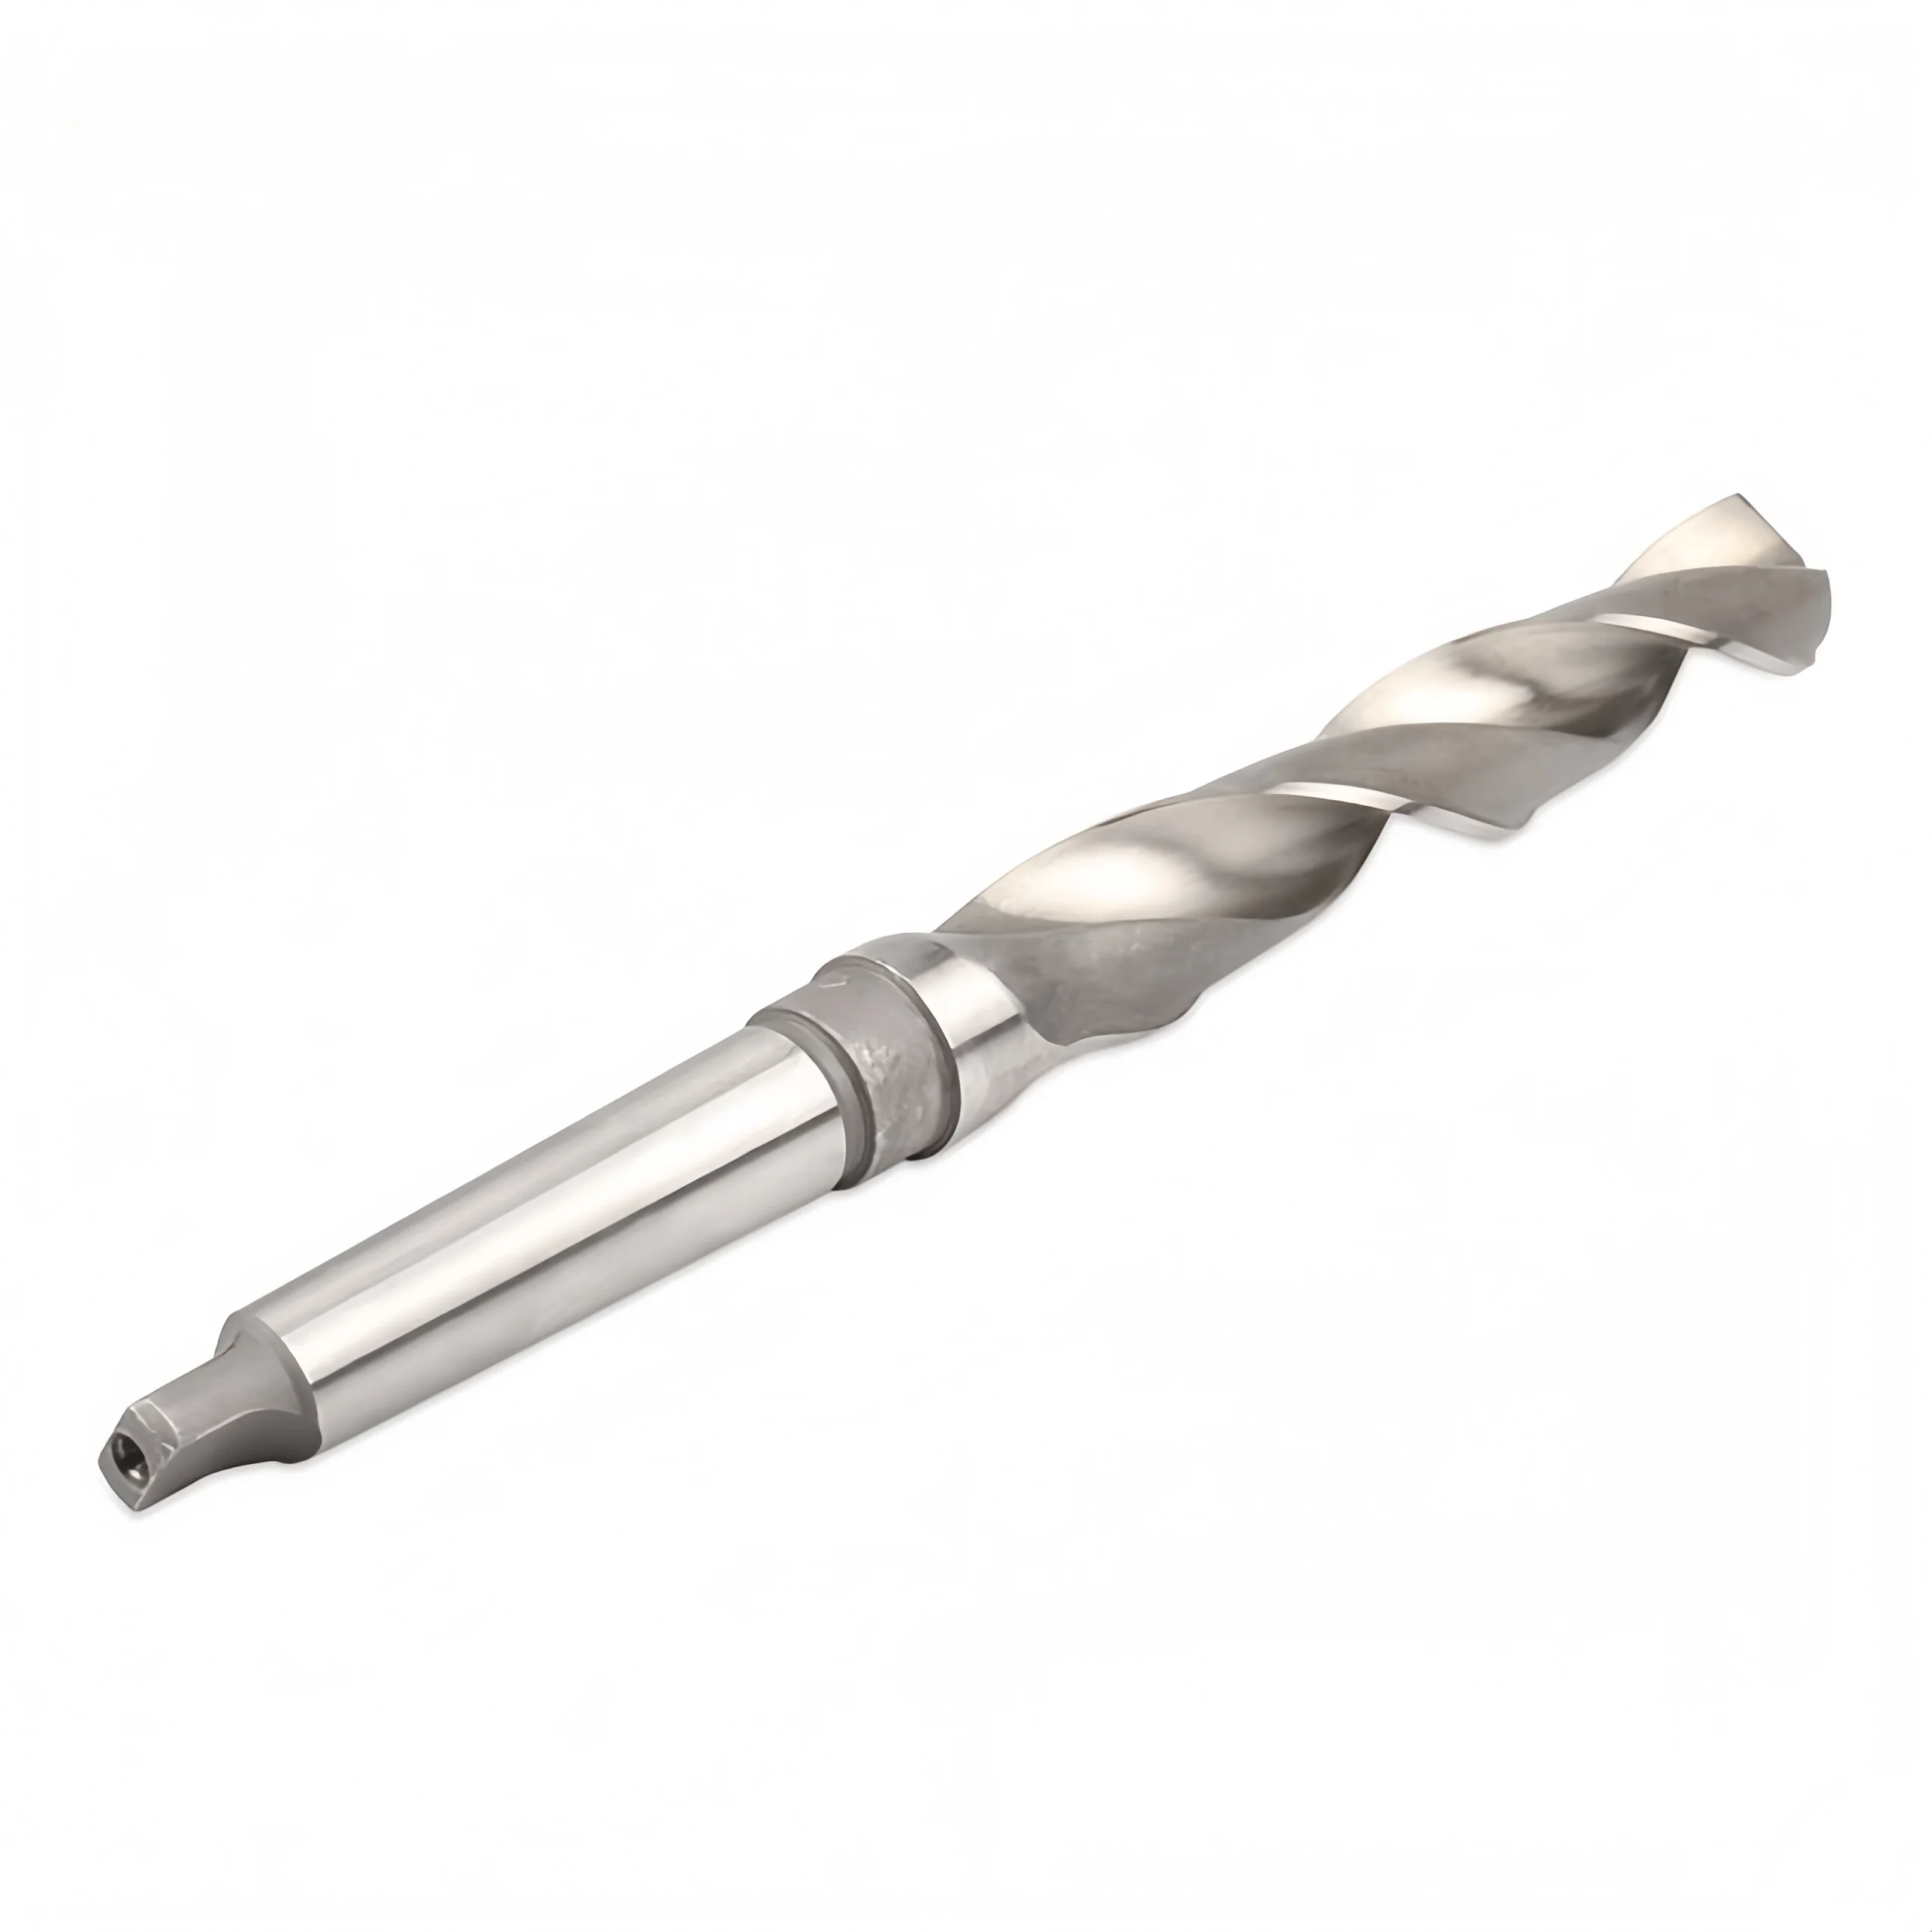
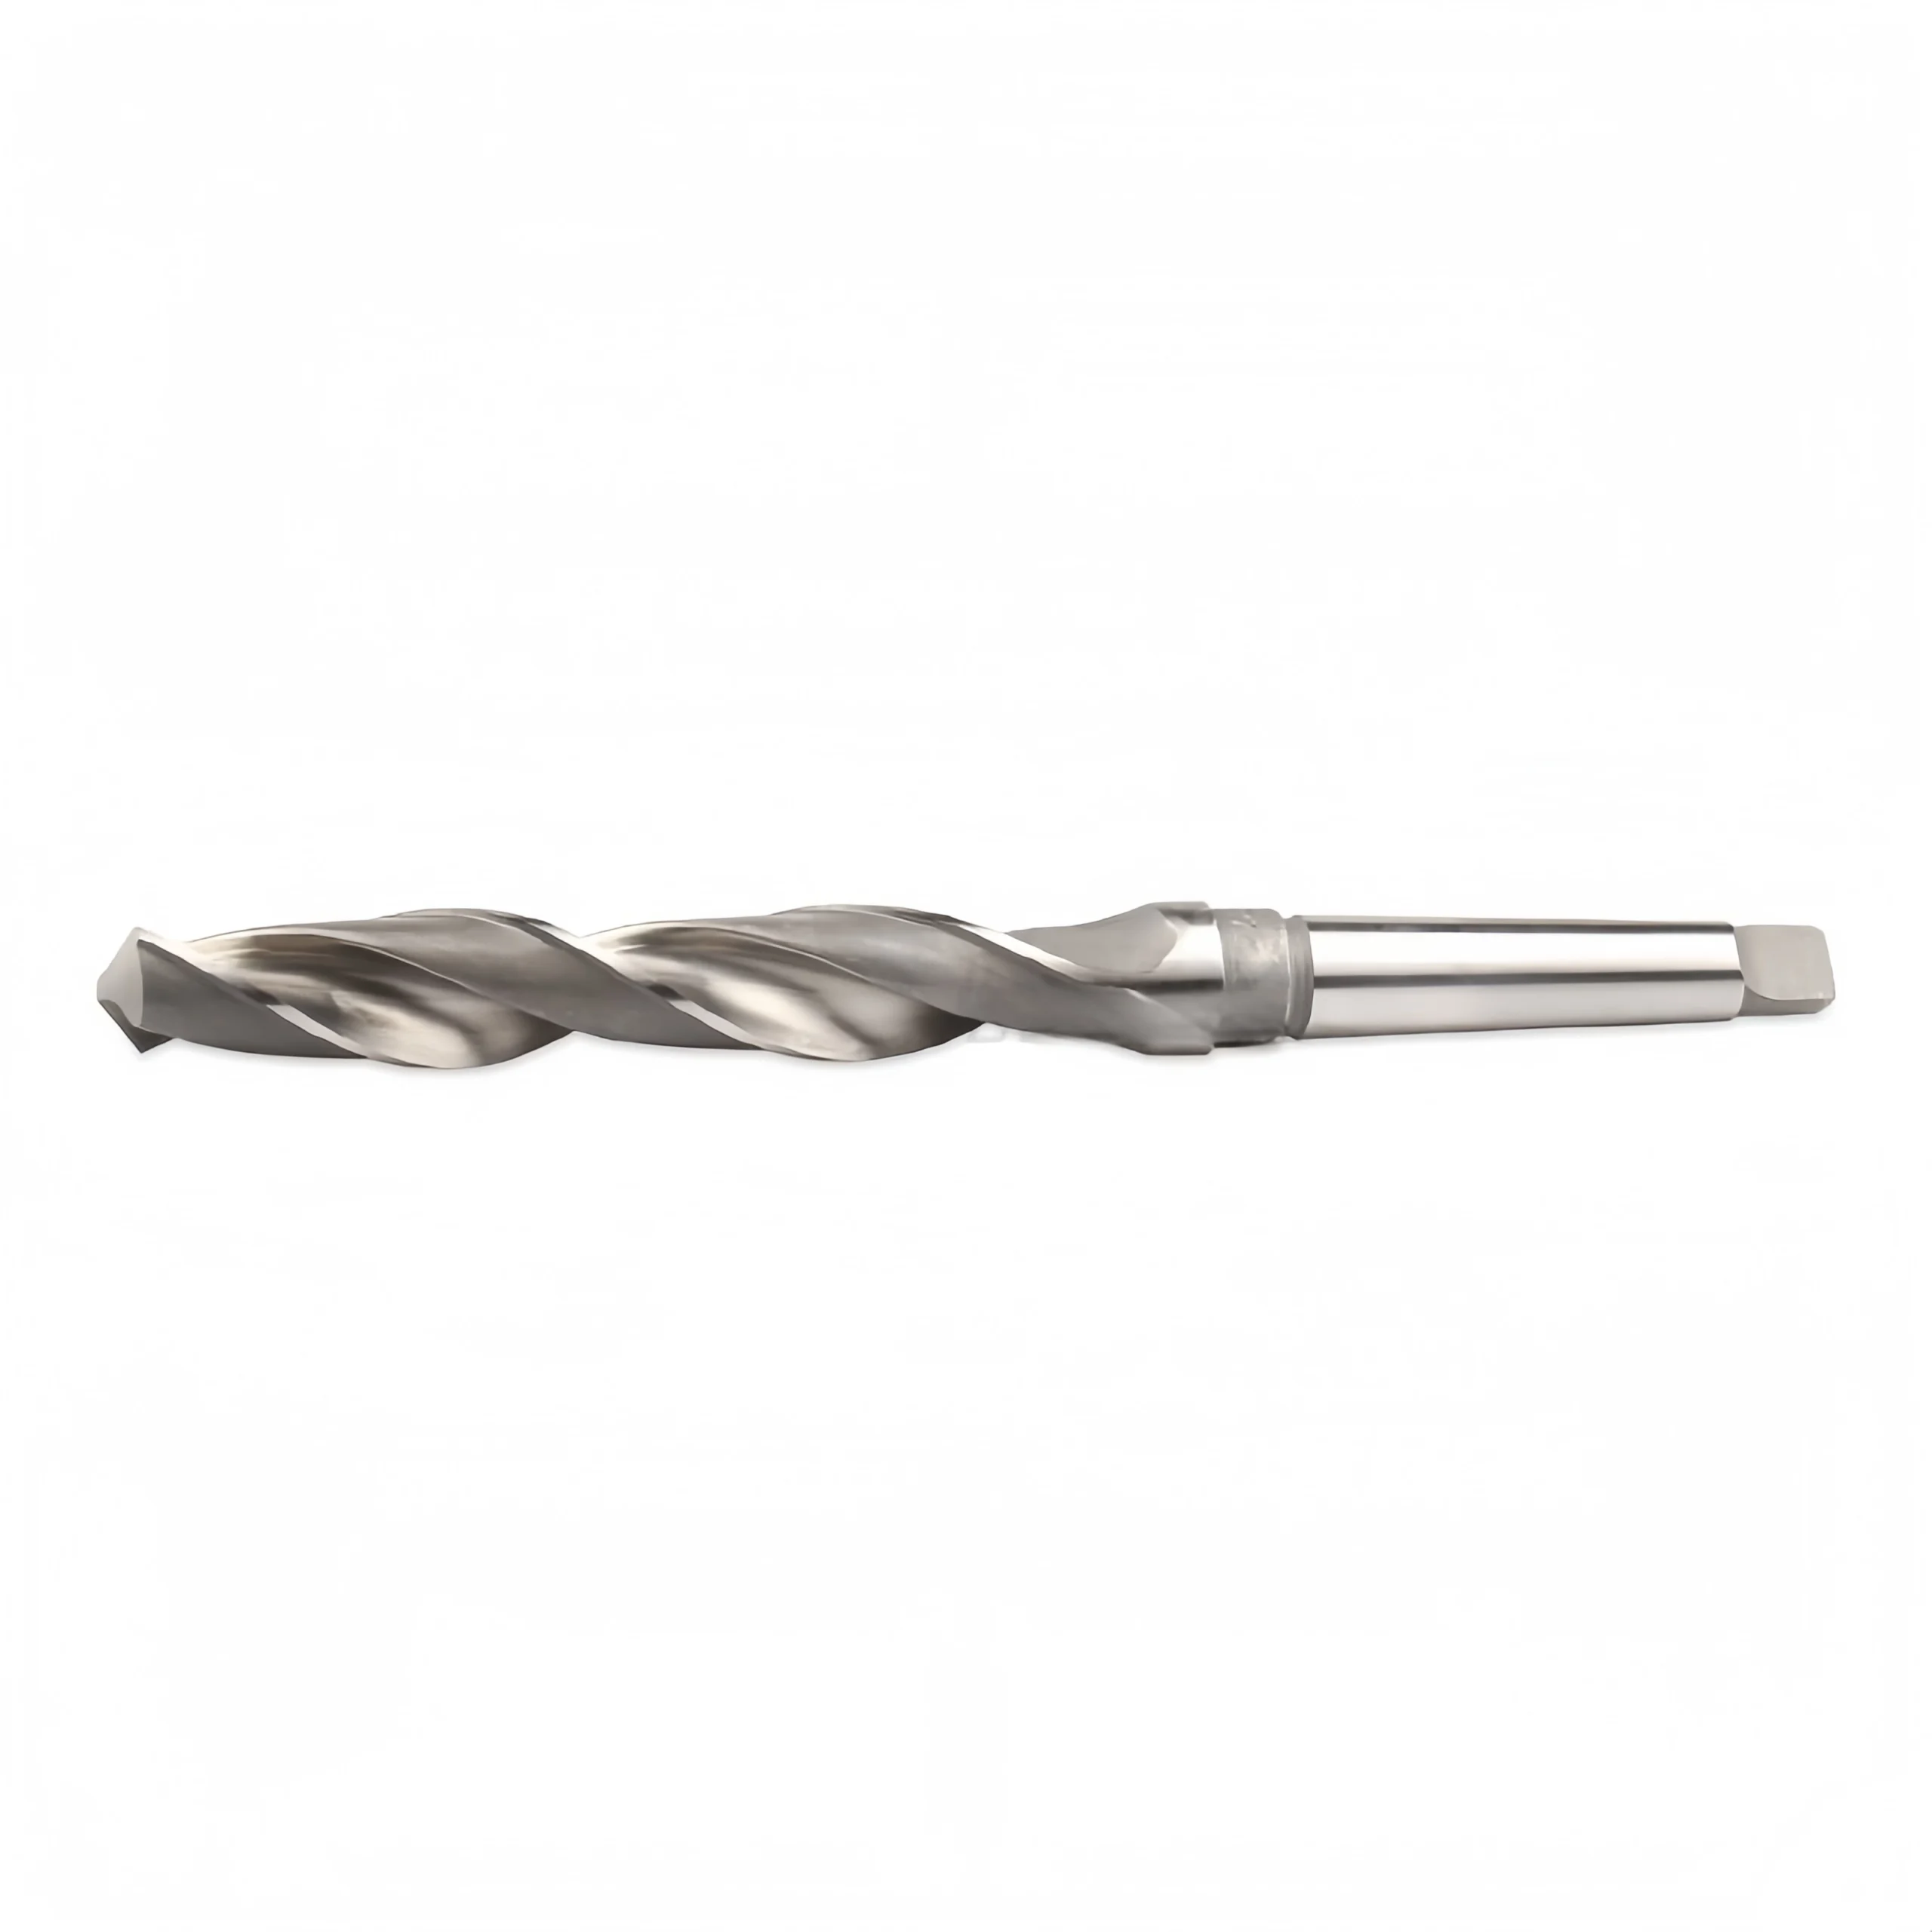
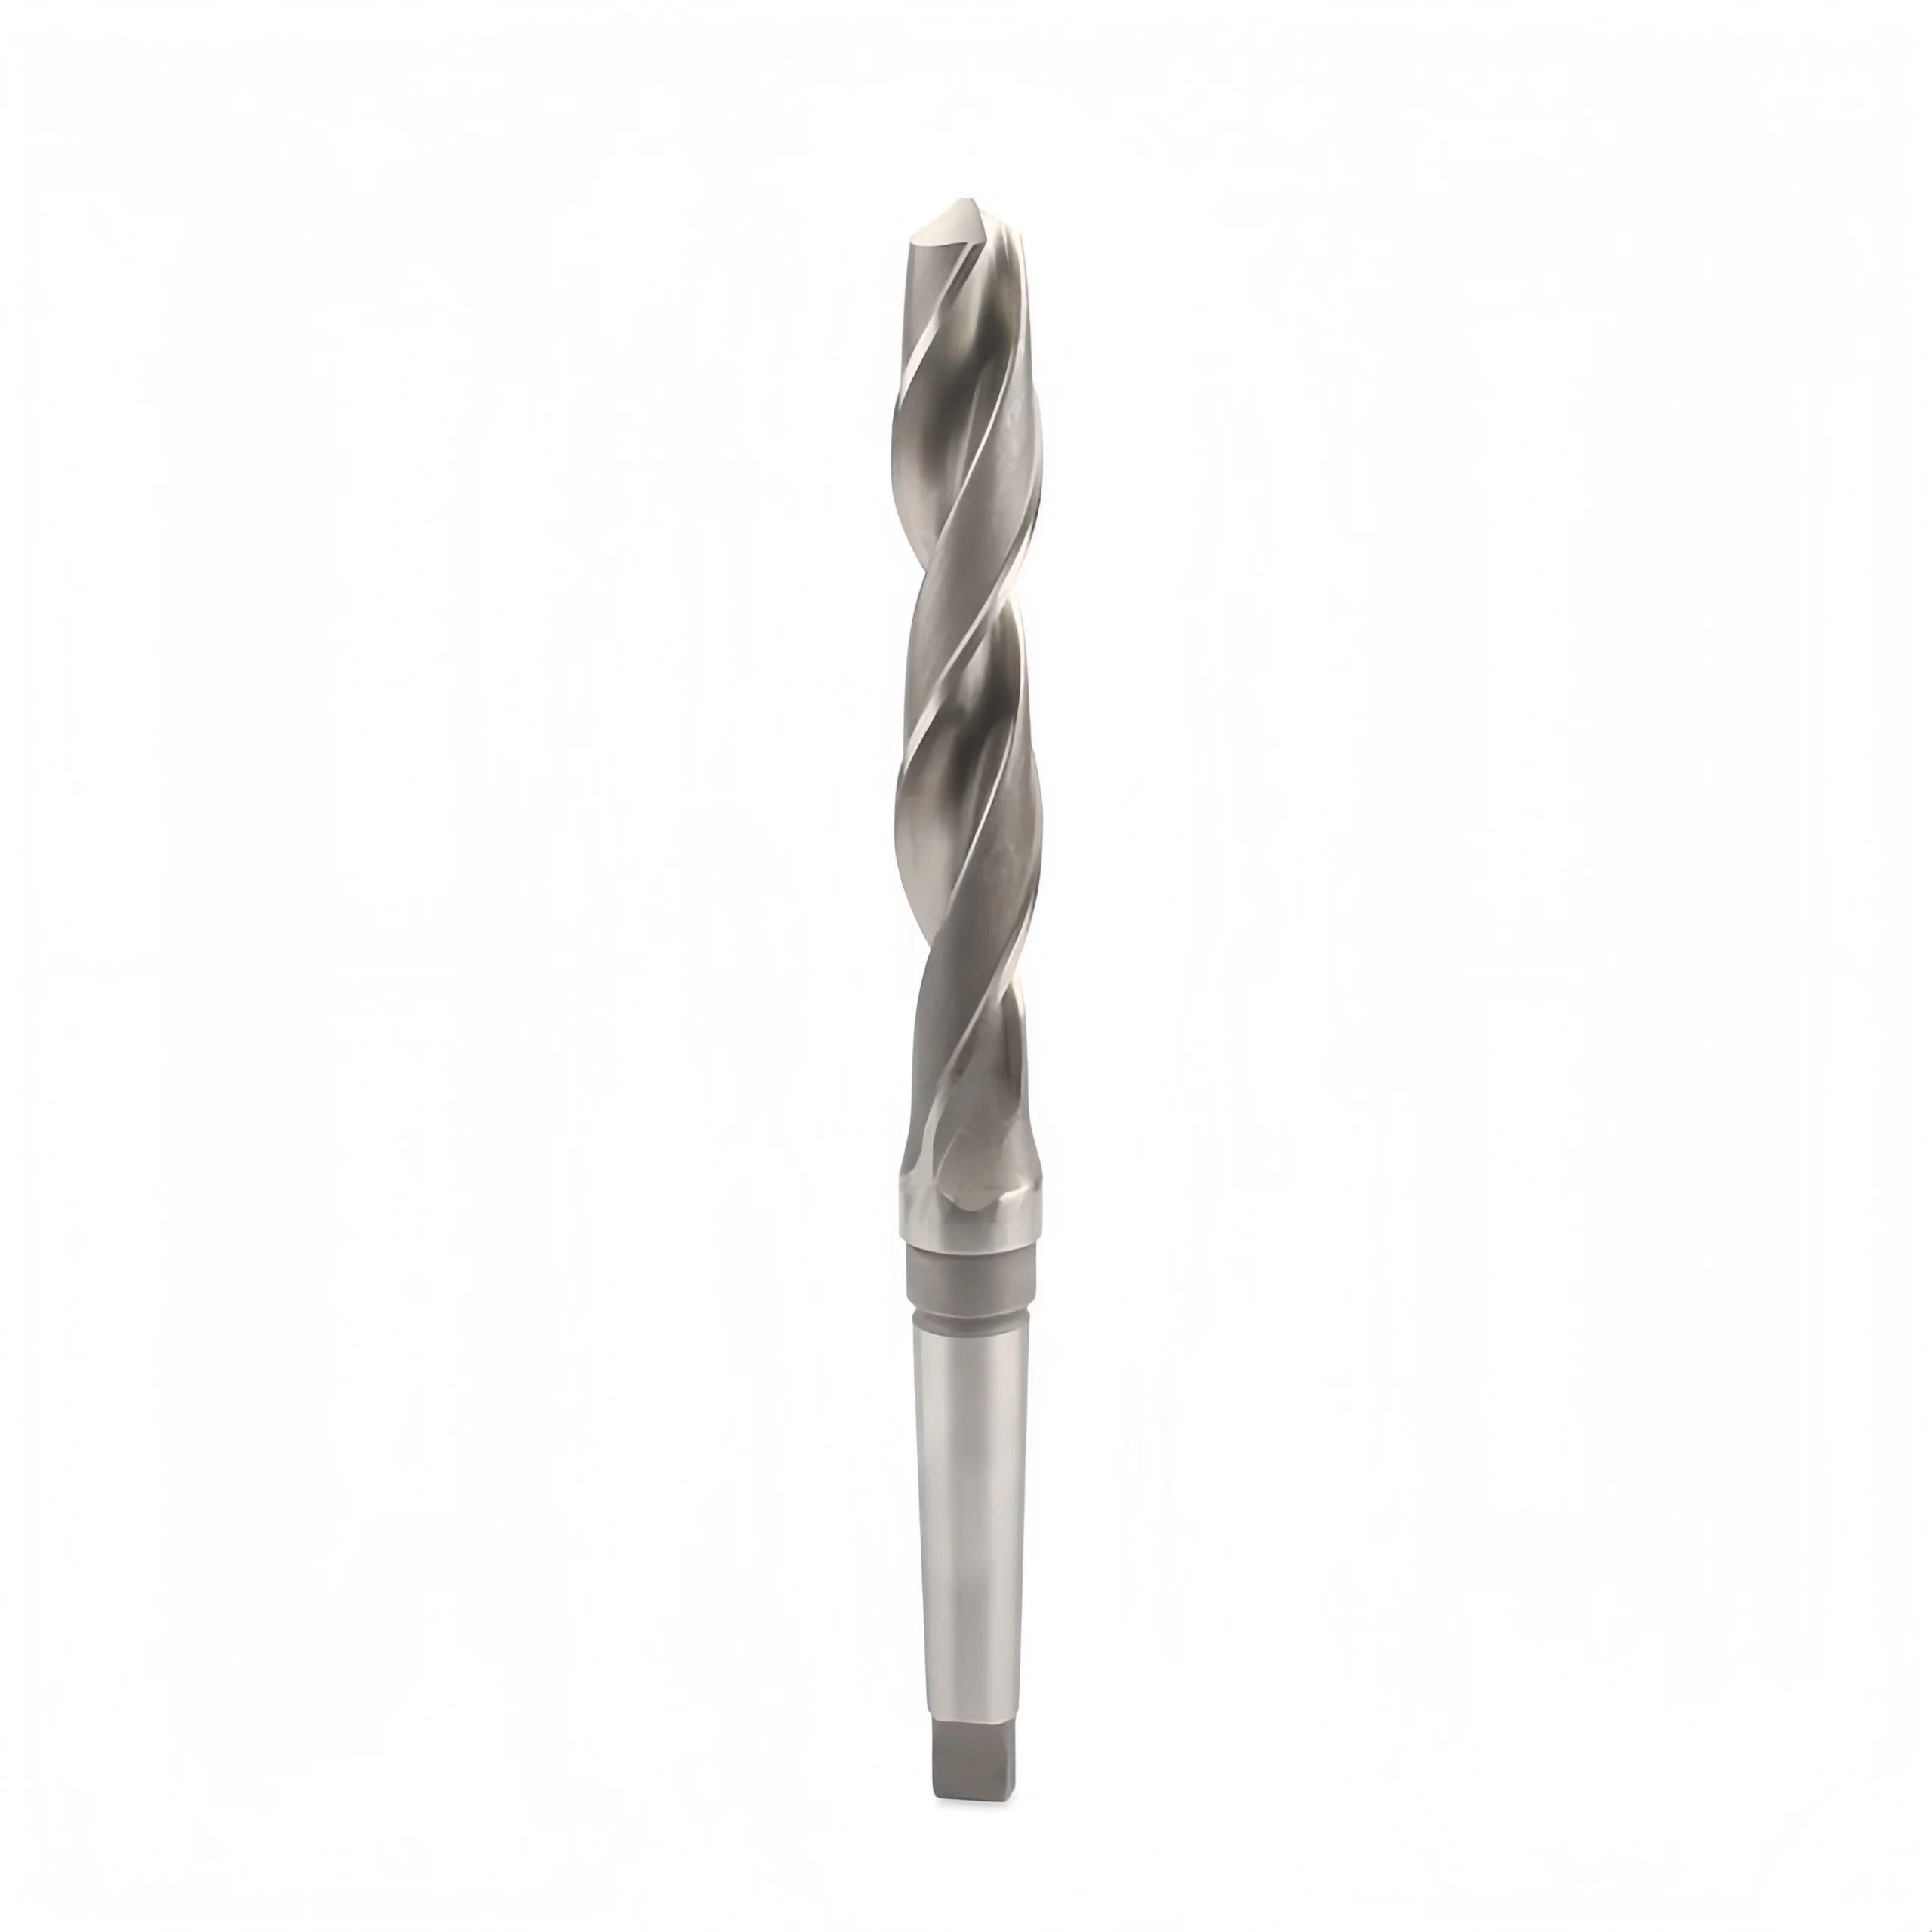
M2 HSS Morse Taper Shank Drill Bits
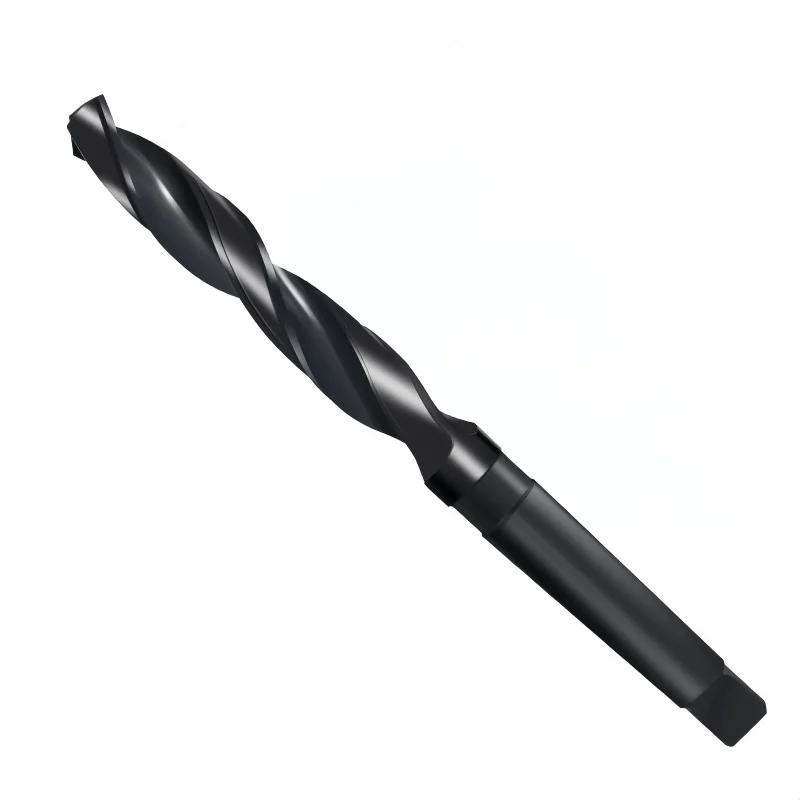
M2 HSS Morse taper shank drill bits for machine drilling in general steels, cast iron and selected non-ferrous metals. The size chart lists 134 diameters from Ø5 to Ø76 mm, with diameter-specific flute lengths, overall lengths and MT1–MT5 taper sizes.
Product Specifications
Consistent Quality
Consistent geometry across repeat orders.
Pedidos flexíveis
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
Padrão e personalizado
Standard sizes and custom configurations.
Visão geral do produto
O M2 HSS Morse Taper Shank Drill Bits are built for stable, high-torque holemaking on radial drilling machines, pillar drills, lathes, and other machine tools equipped with a compatible Morse-taper socket or sleeve. The self-holding taper fits directly into a matching spindle or adapter, avoiding the capacity and slippage limitations of a conventional drill chuck when larger drill diameters are required.
Fabricado a partir de M2 high-speed steel, the drills balance cutting-edge wear resistance with the toughness needed for general industrial drilling. They are suited primarily to carbon steel, structural steel, low-alloy steel, cast iron, and selected non-ferrous metals under appropriate cutting conditions. The cutting edges can be resharpened, making this series a practical choice for maintenance, fabrication, machinery production, and larger-diameter metal drilling.

Industrial drilling setup using a taper-shank twist drill. Machine rigidity, correct taper engagement, coolant supply, chip evacuation, and stable workholding are essential for large-diameter drilling.
Why Use a Morse Taper Shank?
Morse Taper vs. Straight Shank
| Selection Point | Morse Taper Shank | Straight Shank |
|---|---|---|
| Machine interface | Directly seats in a matching taper socket or sleeve | Held by a drill chuck, collet, or other holder |
| Typical use | Higher-torque and larger-diameter industrial drilling | Flexible tool changes and smaller general drilling |
| Required check | Correct MT number, clean taper, and full seating | Holder capacity, grip length, and runout |
| Removal | Use the machine’s approved drift or ejection mechanism | Release the chuck or holder according to its instructions |
Why M2 High-Speed Steel?
Point Geometry & Cutting Thrust
Type N Flute Geometry
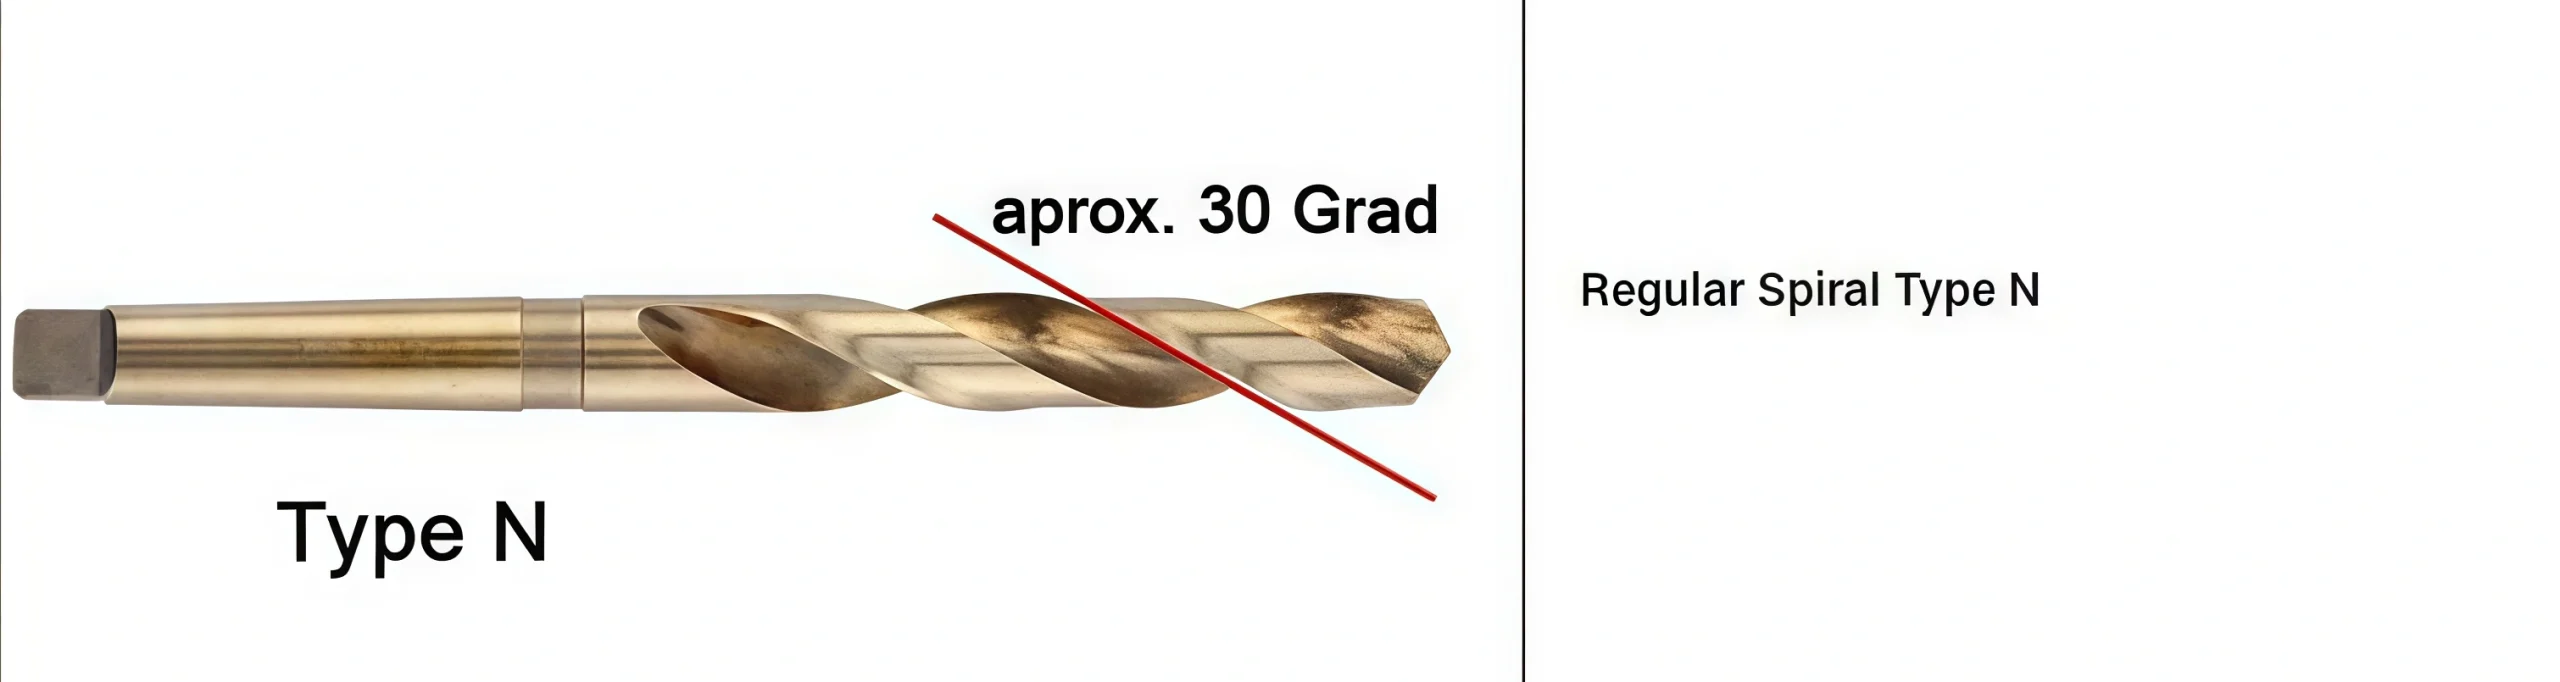
The illustrated Type N regular spiral uses an approximately 30° helix for general metal drilling. The two flutes balance edge support with chip space, but coolant flow and retract strategy must still be matched to the material, diameter, and hole depth.
Manufacturing & Finish Options
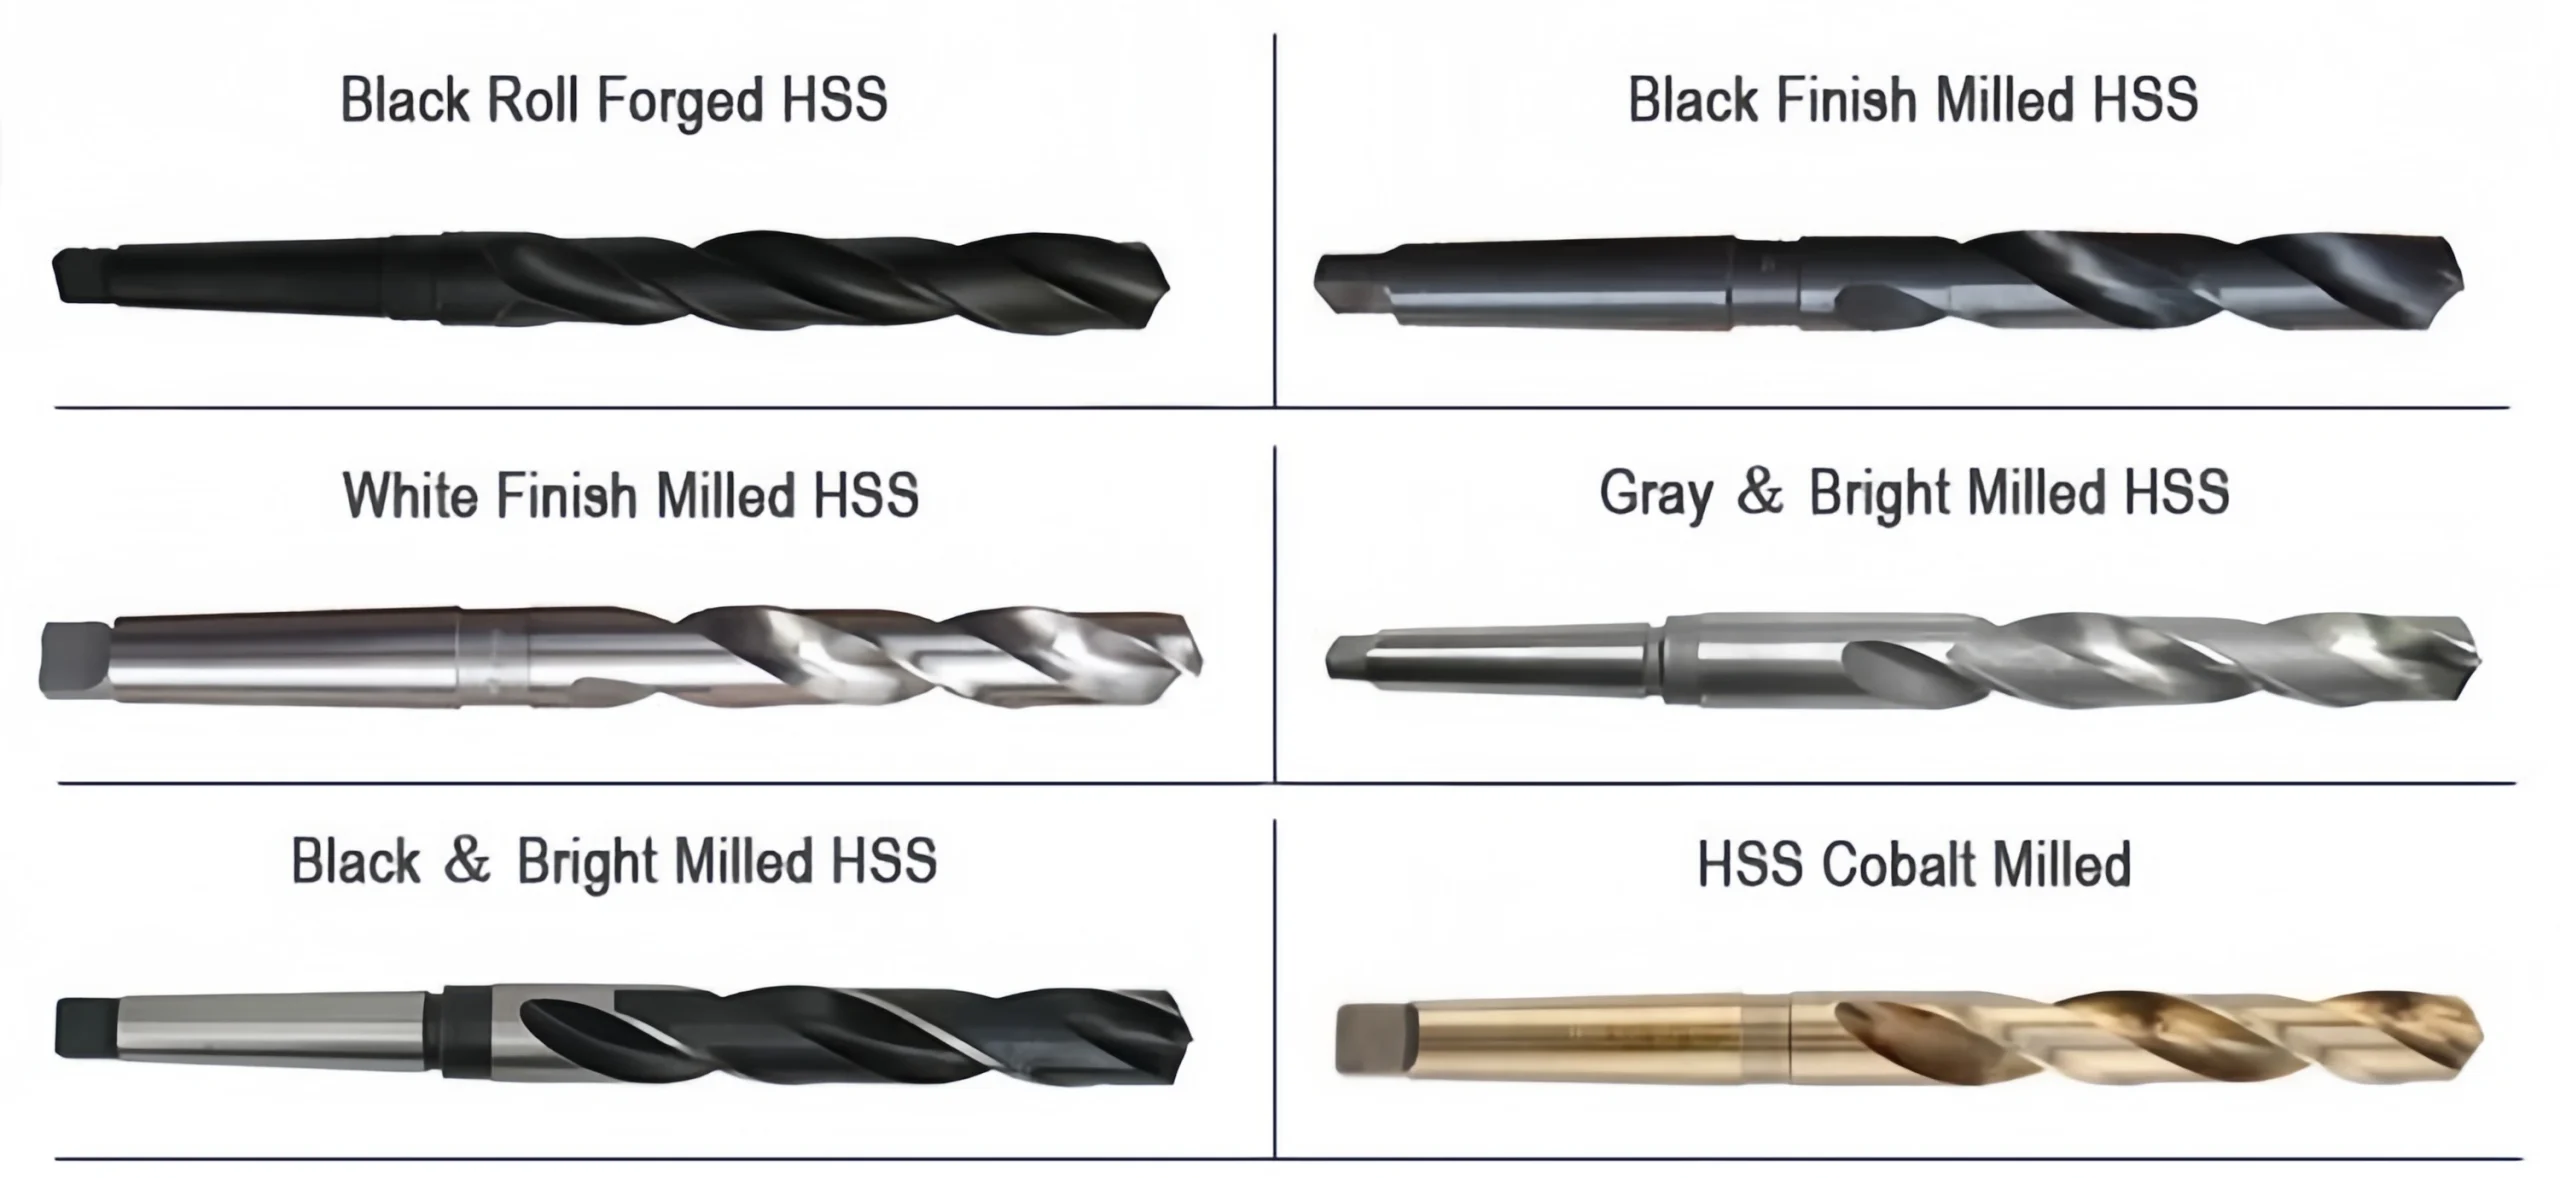
Long & Extra-Long Series

Recommended Application Range
General Steel & Structural MetalCarbon steel, structural steel, low-alloy steel, machinery components, plates, blocks, and fabricated metal parts.
Cast Iron & Copper AlloysConfirm the exact grade, point geometry, flute finish, lubrication method, and chip control before production.
Stainless & Heat-Resistant AlloysM35 or M42 cobalt HSS may be more appropriate where higher hot hardness and wear resistance are needed.
Position Within the HSS Drill Family
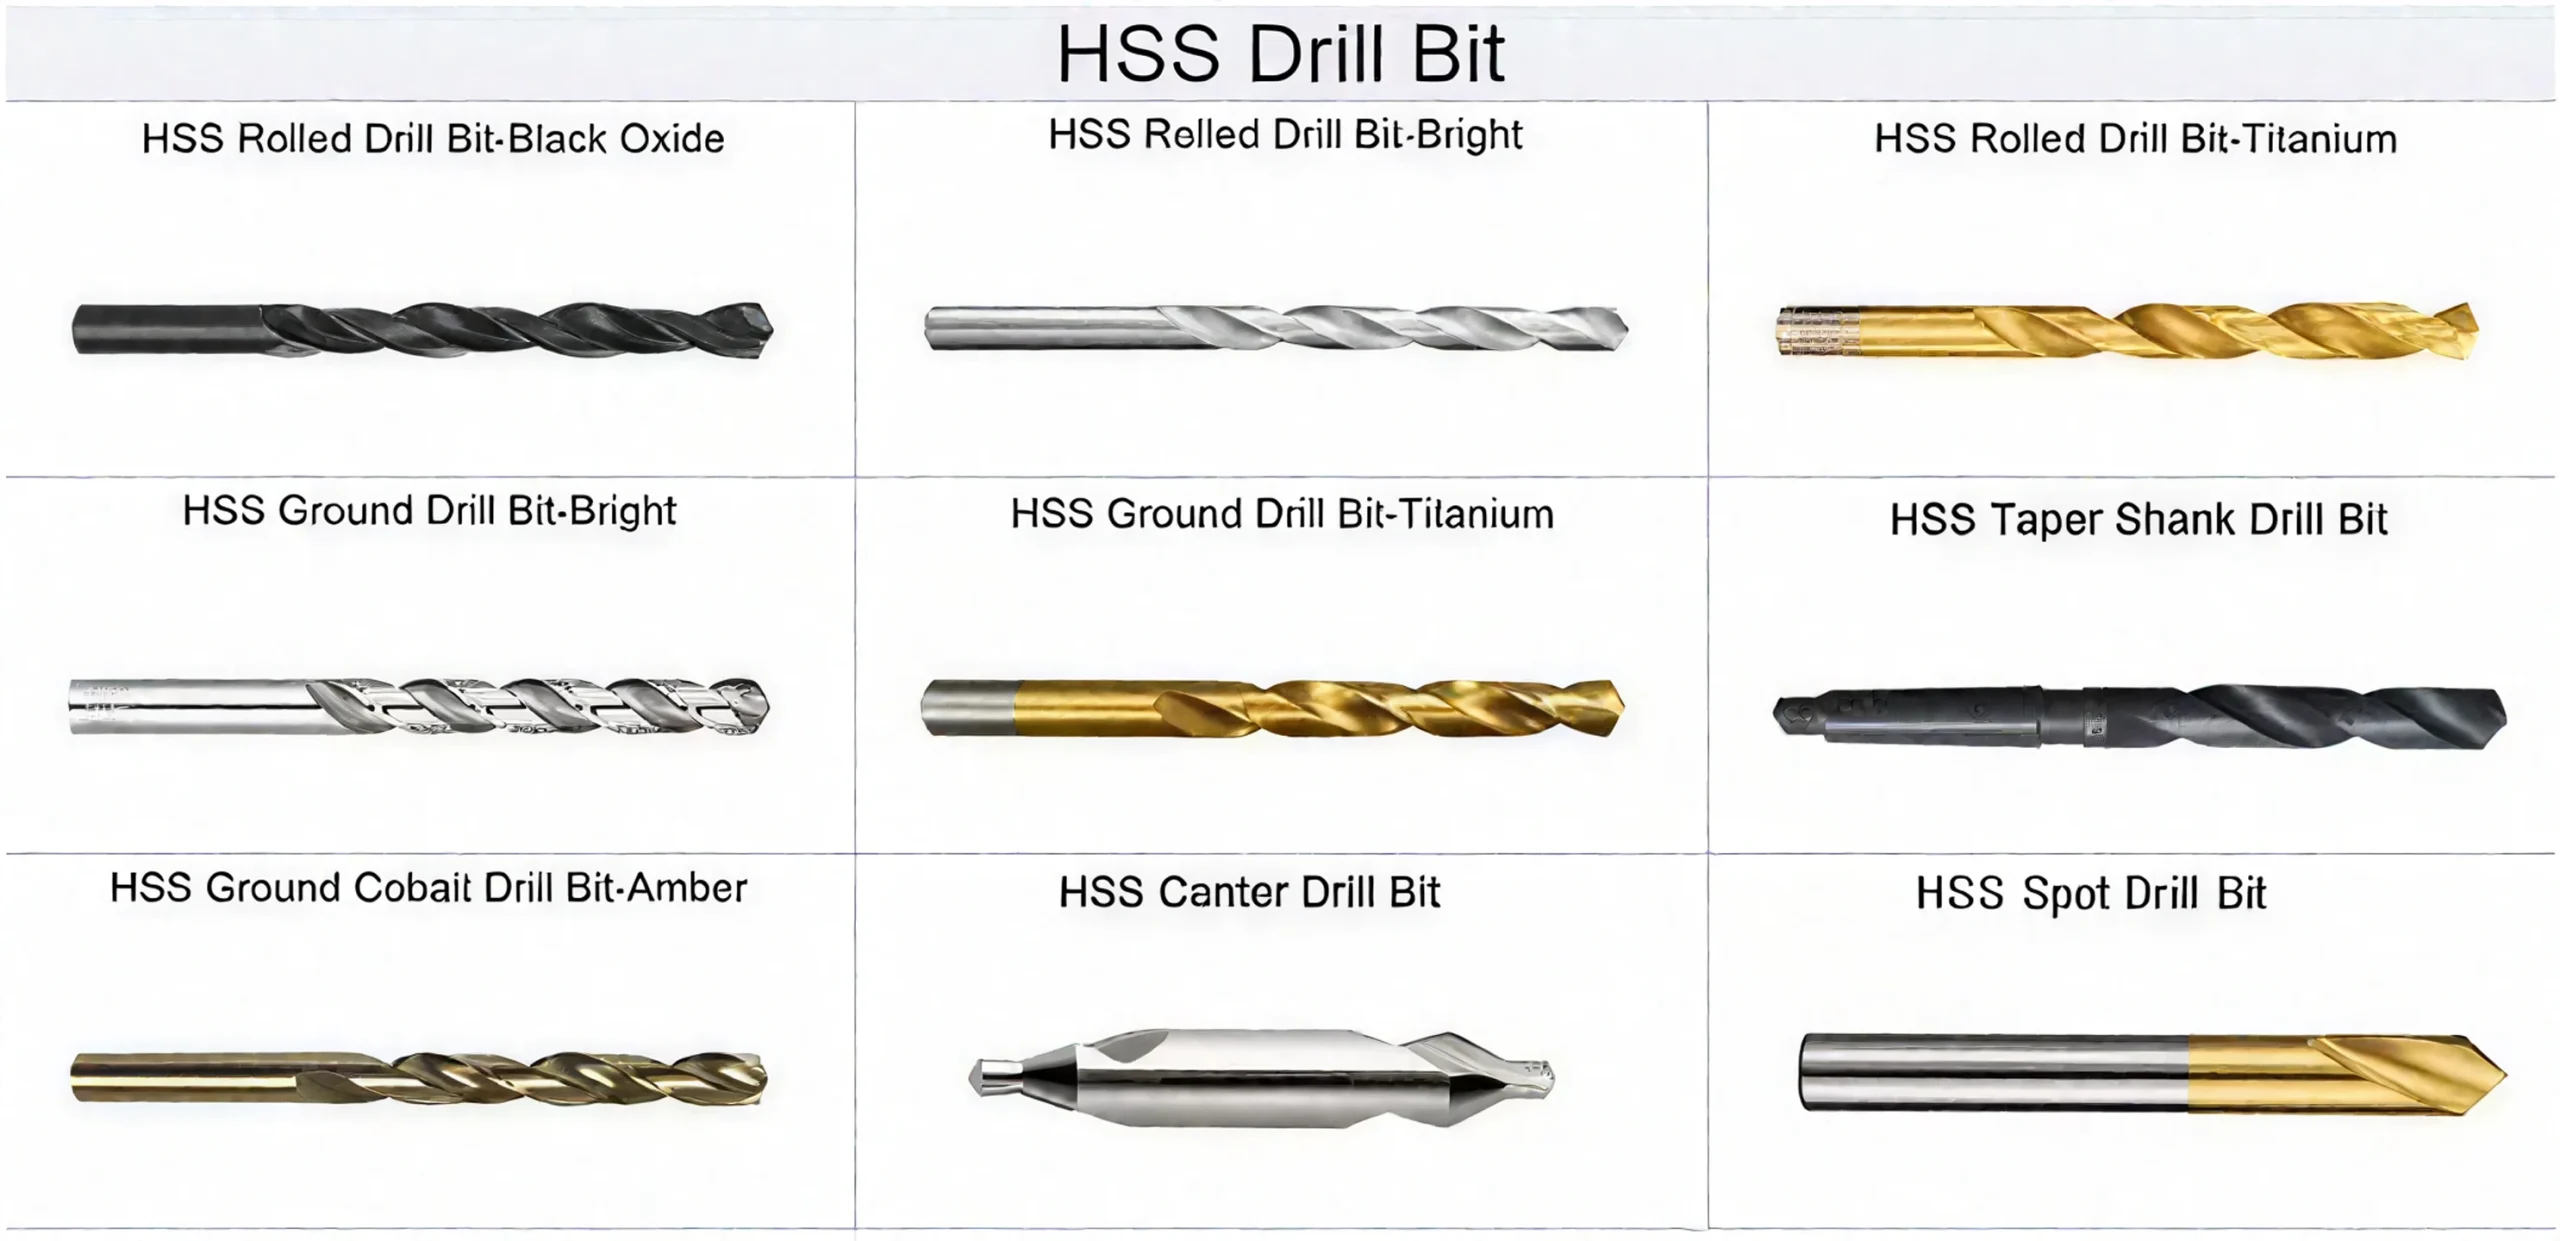
The taper-shank drill is one member of the wider HSS holemaking family. Select by machine connection and hole requirement first, then confirm HSS grade, manufacturing method, surface finish, point form, and length series.
Setup & Machining Recommendations
 Related HSS Hole-Making Tools
Browse the complete HSS drill range, or select a related tool according to required reach, diameter, workpiece material, and hole-starting operation.
FOR EXTENDED REACHExtra-Long HSS Morse Taper DrillConsider this series when the standard or long drill cannot reach the required feature.
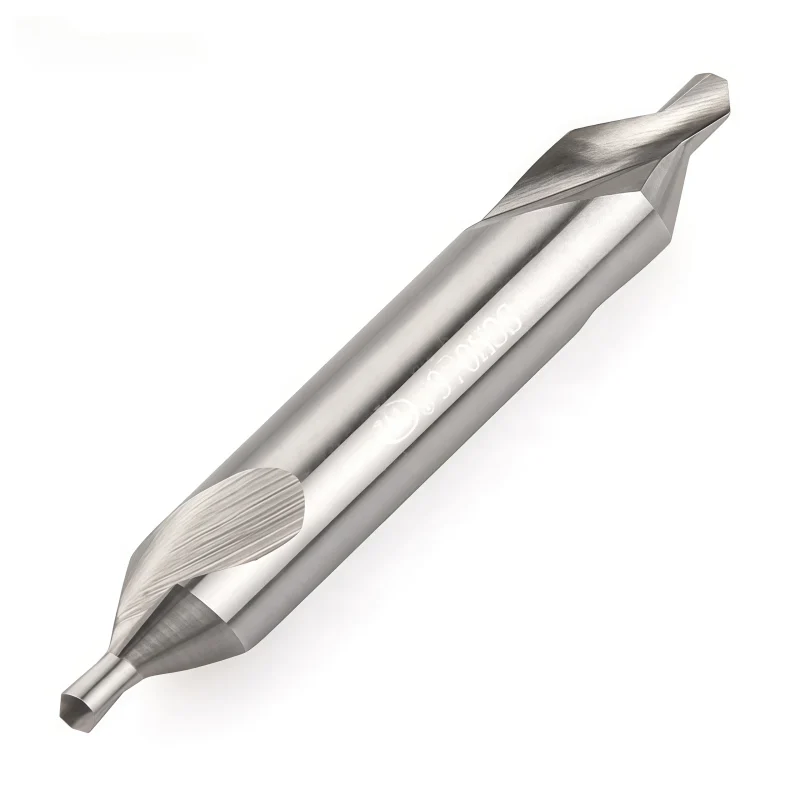
FOR LARGE DIAMETERSØ31–50 mm HSS 6542 Taper-Shank DrillA dedicated M2/6542 option for larger general-steel holes.FOR MATERIAL-GRADE SELECTIONM2 / M35 / M42 HSS Drill SeriesCompare general M2 HSS with cobalt grades for tougher or hotter-cutting materials.FOR HOLE STARTINGM2 HSS Center DrillUse a suitable centering operation when the surface or positional requirement demands it.
Size Chart & Specifications
M2 HSS Morse Taper Shank Drill Bits are listed in 134 diameters from Ø5 to Ø76 mm. Flute lengths (L1) range from 52 to 260 mm, overall lengths (L) from 133 to 447 mm, and the specified shank sizes from MT1 to MT5. All dimensions are in millimeters. Select the required diameter and check its corresponding flute length, overall length and Morse taper against the machine setup.
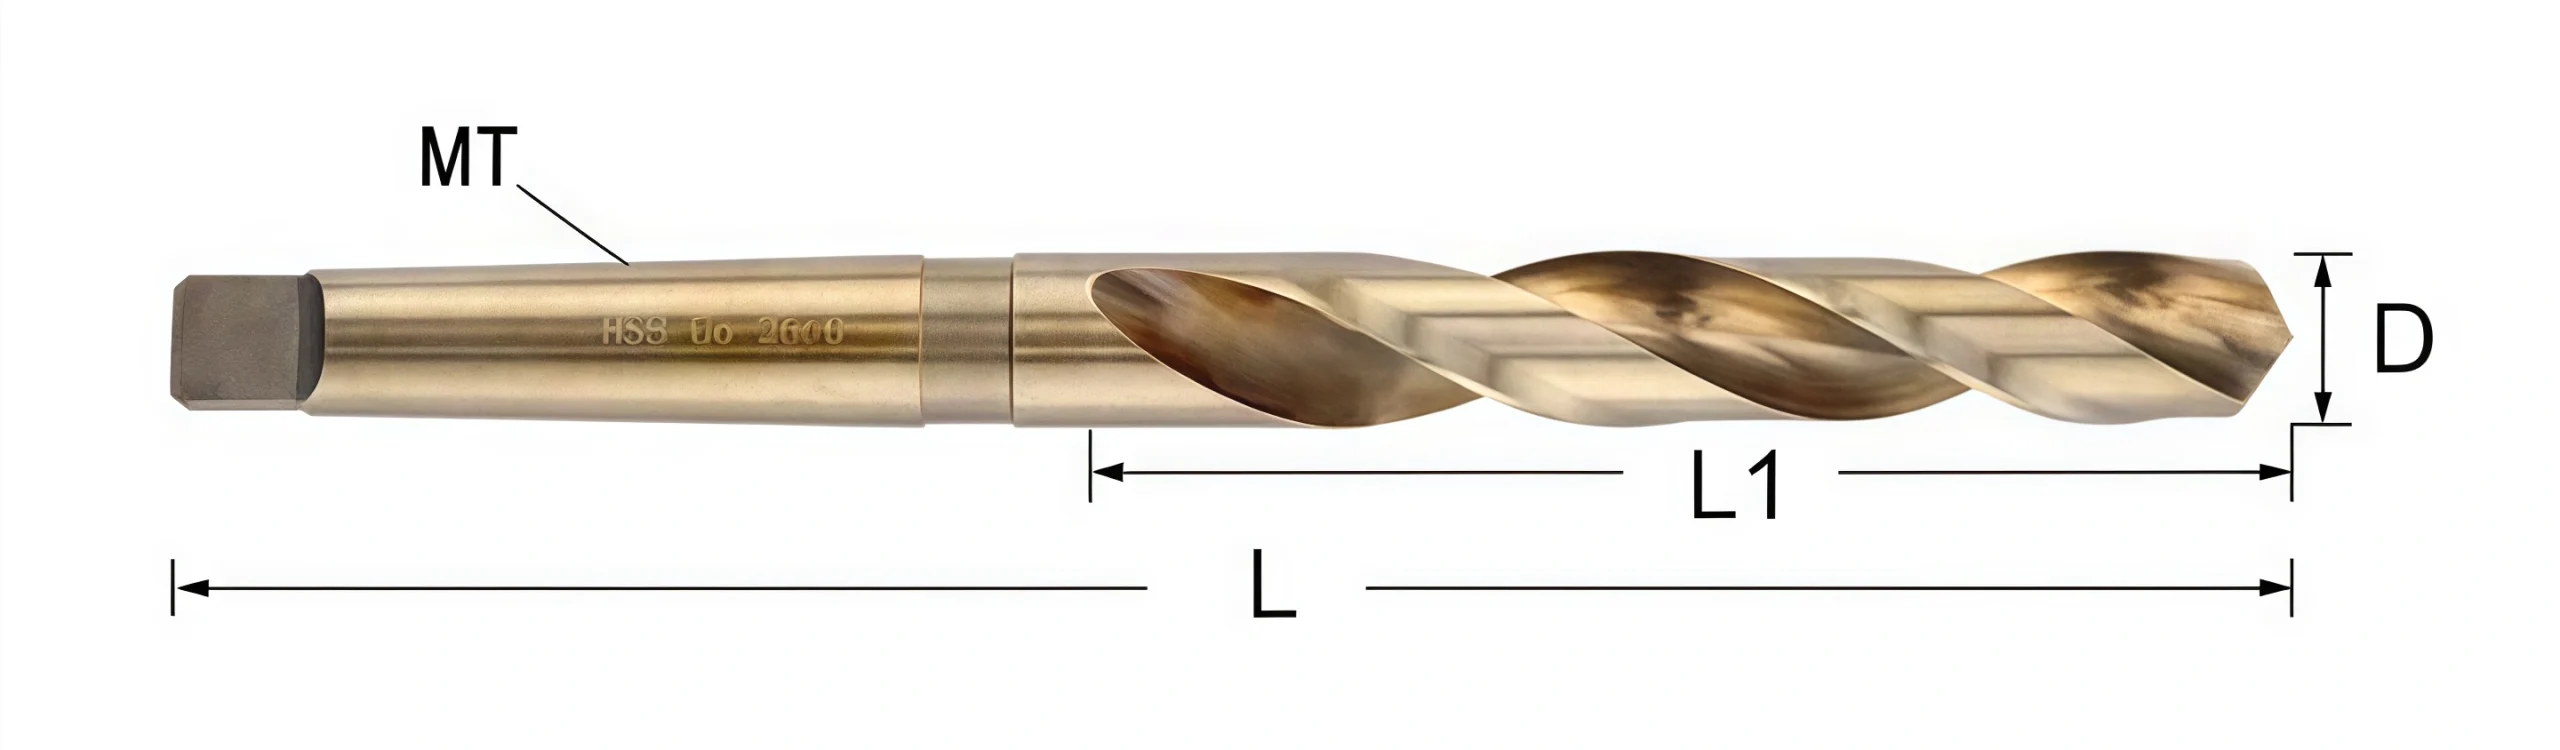
| Diameter D (mm) | Flute L1 (mm) | Overall L (mm) | Morse Taper | Diameter D (mm) | Flute L1 (mm) | Overall L (mm) | Morse Taper |
|---|---|---|---|---|---|---|---|
| 5 | 52 | 133 | MT1 | 29.5 | 175 | 296 | MT3 |
| 5.2 | 52 | 133 | MT1 | 30 | 175 | 296 | MT3 |
| 5.5 | 57 | 138 | MT1 | 30.5 | 180 | 301 | MT3 |
| 5.8 | 57 | 138 | MT1 | 31 | 180 | 301 | MT3 |
| 6 | 57 | 138 | MT1 | 31.5 | 180 | 301 | MT3 |
| 6.2 | 63 | 144 | MT1 | 32 | 185 | 334 | MT4 |
| 6.5 | 63 | 144 | MT1 | 32.5 | 185 | 334 | MT4 |
| 6.8 | 69 | 150 | MT1 | 33 | 185 | 334 | MT4 |
| 7 | 69 | 150 | MT1 | 33.5 | 185 | 334 | MT4 |
| 7.2 | 69 | 150 | MT1 | 34 | 190 | 339 | MT4 |
| 7.5 | 69 | 150 | MT1 | 34.5 | 190 | 339 | MT4 |
| 7.8 | 75 | 156 | MT1 | 35 | 190 | 339 | MT4 |
| 8 | 75 | 156 | MT1 | 35.5 | 190 | 339 | MT4 |
| 8.2 | 75 | 156 | MT1 | 36 | 195 | 344 | MT4 |
| 8.5 | 75 | 156 | MT1 | 36.5 | 195 | 344 | MT4 |
| 8.8 | 81 | 162 | MT1 | 37 | 195 | 344 | MT4 |
| 9 | 81 | 162 | MT1 | 38 | 200 | 349 | MT4 |
| 9.2 | 81 | 162 | MT1 | 38.5 | 200 | 349 | MT4 |
| 9.5 | 81 | 162 | MT1 | 39 | 200 | 349 | MT4 |
| 9.8 | 87 | 168 | MT1 | 39.5 | 200 | 349 | MT4 |
| 10 | 87 | 168 | MT1 | 40 | 200 | 349 | MT4 |
| 10.2 | 87 | 168 | MT1 | 40.5 | 205 | 354 | MT4 |
| 10.5 | 87 | 168 | MT1 | 41 | 205 | 354 | MT4 |
| 10.8 | 94 | 175 | MT1 | 41.5 | 205 | 354 | MT4 |
| 11 | 94 | 175 | MT1 | 42 | 205 | 354 | MT4 |
| 11.2 | 94 | 175 | MT1 | 42.5 | 205 | 354 | MT4 |
| 11.5 | 94 | 175 | MT1 | 43 | 210 | 359 | MT4 |
| 11.8 | 94 | 175 | MT1 | 43.5 | 210 | 359 | MT4 |
| 12 | 101 | 182 | MT1 | 44.5 | 210 | 359 | MT4 |
| 12.2 | 101 | 182 | MT1 | 45 | 210 | 359 | MT4 |
| 12.5 | 101 | 182 | MT1 | 45.5 | 215 | 364 | MT4 |
| 12.8 | 101 | 182 | MT1 | 46 | 215 | 364 | MT4 |
| 13 | 101 | 182 | MT1 | 46.5 | 215 | 364 | MT4 |
| 13.2 | 101 | 182 | MT1 | 47 | 215 | 364 | MT4 |
| 13.5 | 108 | 189 | MT1 | 47.5 | 215 | 364 | MT4 |
| 13.8 | 108 | 189 | MT1 | 48 | 220 | 369 | MT4 |
| 14 | 108 | 189 | MT2 | 48.5 | 220 | 369 | MT4 |
| 14.5 | 114 | 212 | MT2 | 49 | 220 | 369 | MT4 |
| 15 | 114 | 212 | MT2 | 49.5 | 220 | 369 | MT4 |
| 15.5 | 120 | 218 | MT2 | 50 | 220 | 369 | MT4 |
| 16 | 120 | 218 | MT2 | 50.5 | 220 | 374 | MT4 |
| 16.5 | 125 | 223 | MT2 | 51 | 225 | 412 | MT4 |
| 17 | 125 | 223 | MT2 | 52 | 225 | 412 | MT5 |
| 17.5 | 130 | 228 | MT2 | 53 | 225 | 412 | MT5 |
| 18 | 130 | 228 | MT2 | 54 | 230 | 417 | MT5 |
| 18.5 | 135 | 233 | MT2 | 55 | 230 | 417 | MT5 |
| 19 | 135 | 233 | MT2 | 56 | 230 | 417 | MT5 |
| 19.5 | 140 | 238 | MT2 | 57 | 235 | 422 | MT5 |
| 20 | 140 | 238 | MT2 | 58 | 235 | 422 | MT5 |
| 20.5 | 145 | 243 | MT2 | 59 | 235 | 422 | MT5 |
| 21 | 145 | 243 | MT2 | 60 | 235 | 422 | MT5 |
| 21.5 | 150 | 248 | MT2 | 61 | 240 | 427 | MT5 |
| 22 | 150 | 248 | MT2 | 62 | 240 | 427 | MT5 |
| 22.5 | 155 | 253 | MT2 | 63 | 240 | 427 | MT5 |
| 23 | 155 | 253 | MT2 | 64 | 245 | 432 | MT5 |
| 23.5 | 155 | 276 | MT3 | 65 | 245 | 432 | MT5 |
| 24 | 160 | 281 | MT3 | 66 | 245 | 432 | MT5 |
| 24.5 | 160 | 281 | MT3 | 67 | 245 | 432 | MT5 |
| 25 | 160 | 281 | MT3 | 68 | 250 | 437 | MT5 |
| 25.5 | 165 | 286 | MT3 | 69 | 250 | 437 | MT5 |
| 26 | 165 | 286 | MT3 | 70 | 250 | 437 | MT5 |
| 26.5 | 165 | 286 | MT3 | 71 | 250 | 437 | MT5 |
| 27 | 170 | 291 | MT3 | 72 | 255 | 442 | MT5 |
| 27.5 | 170 | 291 | MT3 | 73 | 255 | 442 | MT5 |
| 28 | 170 | 291 | MT3 | 74 | 255 | 442 | MT5 |
| 28.5 | 175 | 296 | MT3 | 75 | 255 | 442 | MT5 |
| 29 | 175 | 296 | MT3 | 76 | 260 | 447 | MT5 |
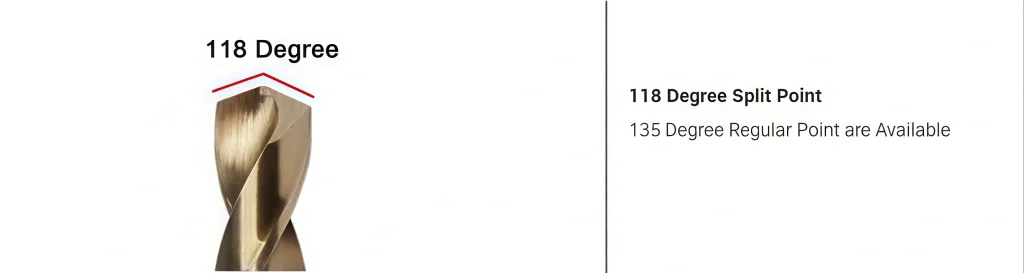
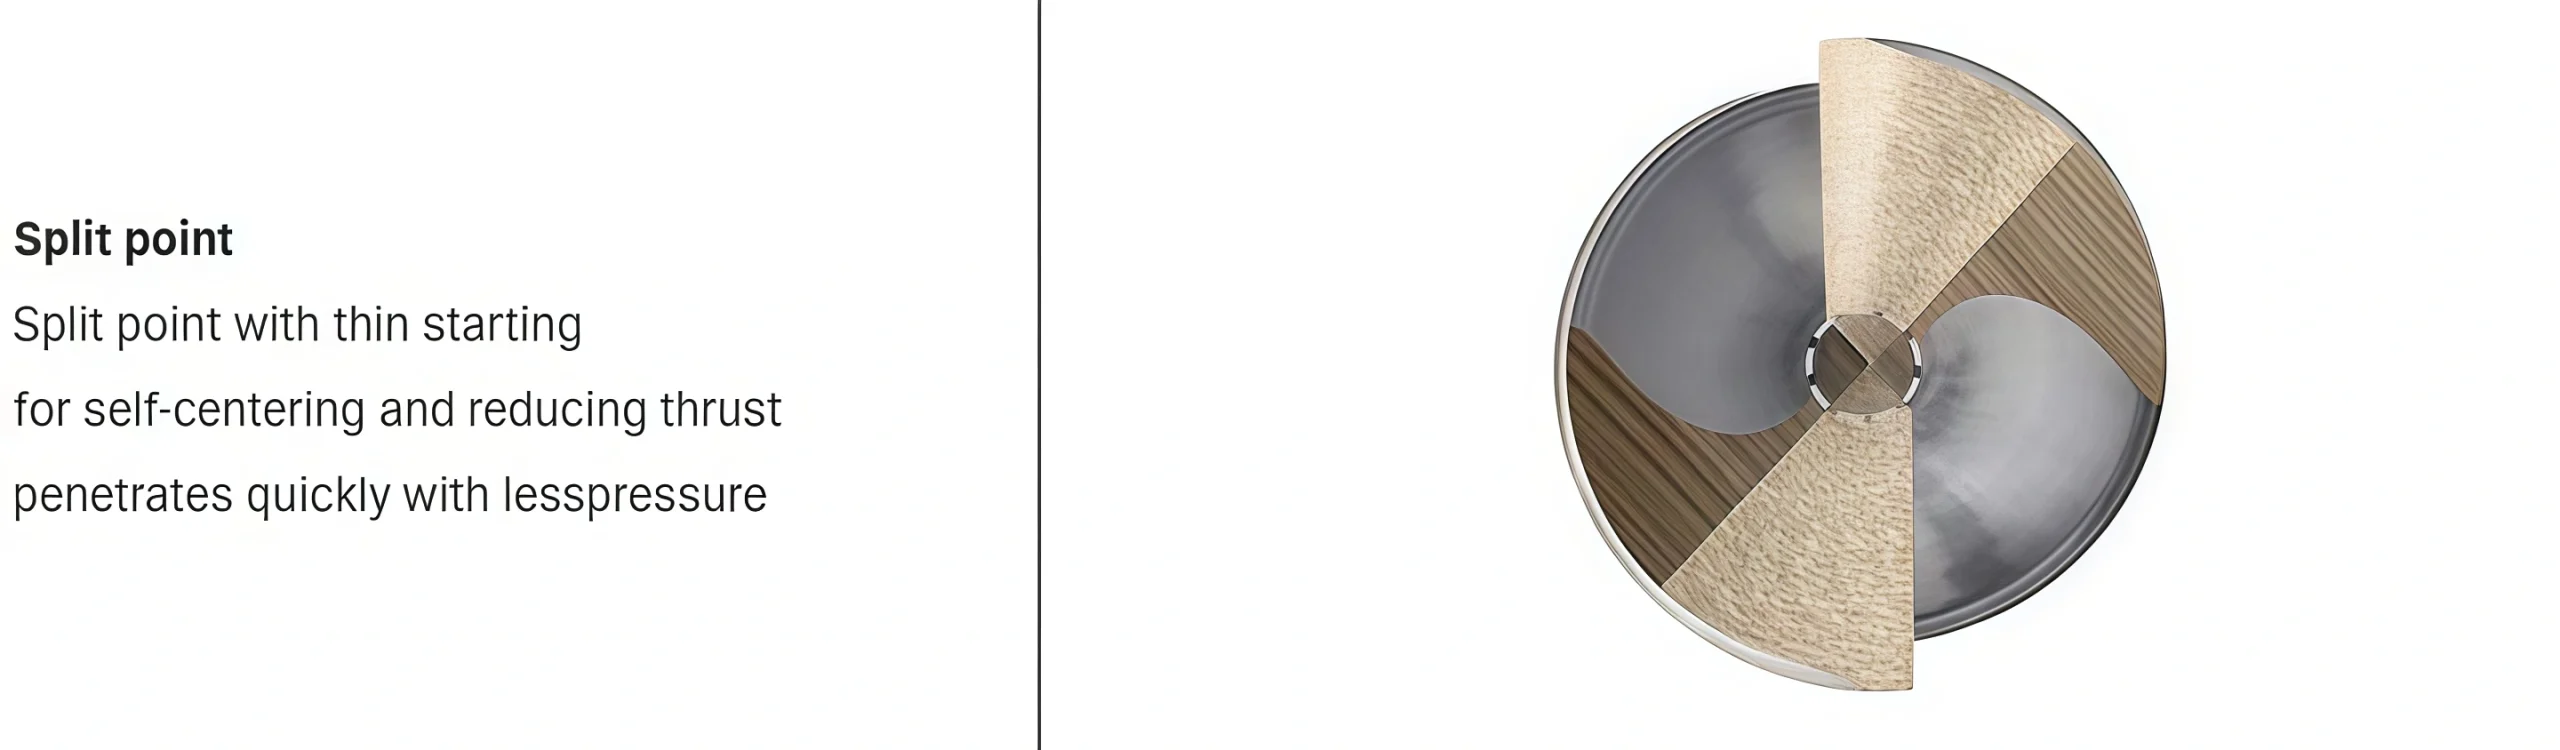
Specification confirmation: M2 HSS is the stated tool material. Confirm the manufacturing standard, diameter tolerance, point form, finish and exact MT socket compatibility for the ordered size. The illustrated 118°, 135° and split-point designs are options; the size table does not assign a specific point form to each diameter.
HSS Drill Speeds & Feed Settings
Select starting cutting data for the confirmed M2 HSS drill geometry, workpiece grade and hardness, drill diameter, hole depth and coolant supply. The dimension table does not specify cutting speeds or feed rates.
Setting Speed & Feed
Spindle speed: n = (1000 × Vc) / (π × D), where n is RPM, Vc is cutting speed in m/min and D is drill diameter in mm.
Feed rate: F = n × f, where F is feed in mm/min and f is feed per revolution in mm/rev.
Calculation example: At 300 RPM and 0.15 mm/rev, the programmed feed is 45 mm/min. This demonstrates the calculation only and is not a cutting recommendation for every diameter or material.
For additional reference, see our HSS cutting tools speeds & feeds guide. Confirm tool-specific values for the selected drill and workpiece.
HSS Drill Customization & OEM
HSS drills can be reviewed against your hole requirements, workpiece material and machine setup. We can discuss application-specific dimensions, cutting geometry, tool material, surface finish and private-label presentation. Available options depend on the drill type and the confirmed manufacturing specification.
Point & Cutting Geometry
Review point angle, point thinning, flute design and cutting-edge geometry according to the workpiece and drilling operation. Geometry options vary between twist drills, center drills and special drills.
Dimensions & Shank
Specify cutting diameter, flute length, overall length and the required shank configuration. Straight-shank, Morse-taper, extra-long and other constructions are reviewed by product series.
Finish & OEM Branding
Review a suitable coating or surface finish where applicable. Laser marking, labels and packaging can be discussed for distributor and private-label orders.
Opções de personalização
| Parâmetro | Information to Confirm |
|---|---|
| Drill Type | Twist drill, center drill, extra-long drill or application-specific design |
| Material da ferramenta | Required HSS grade, such as M2, M35 or M42, subject to the selected series |
| Diameter | Cutting diameter and required diameter tolerance |
| Length & Reach | Flute length, overall length, drilling depth and clearance requirements |
| Point & Flutes | Point geometry, flute design and chip-evacuation requirements |
| Haste | Shank type and dimensions required by the holder |
| Acabamento da superfície | Uncoated, coated or treated finish, where suitable for the tool and application |
| OEM Presentation | Tool marking, product labels and packaging requirements |
Options are reviewed for the specific product and order. A listed option does not imply that every HSS drill series has the same material, geometry, shank or coating choices.
What to Send for a Custom Drill Quote
Send the drill type, diameter, hole depth, workpiece grade, required geometry, shank or holder details, quantity and any coating or marking requirements. A drawing or reference sample helps confirm non-standard dimensions.
Submit a Custom Tool RequestHSS Drill Quality Control
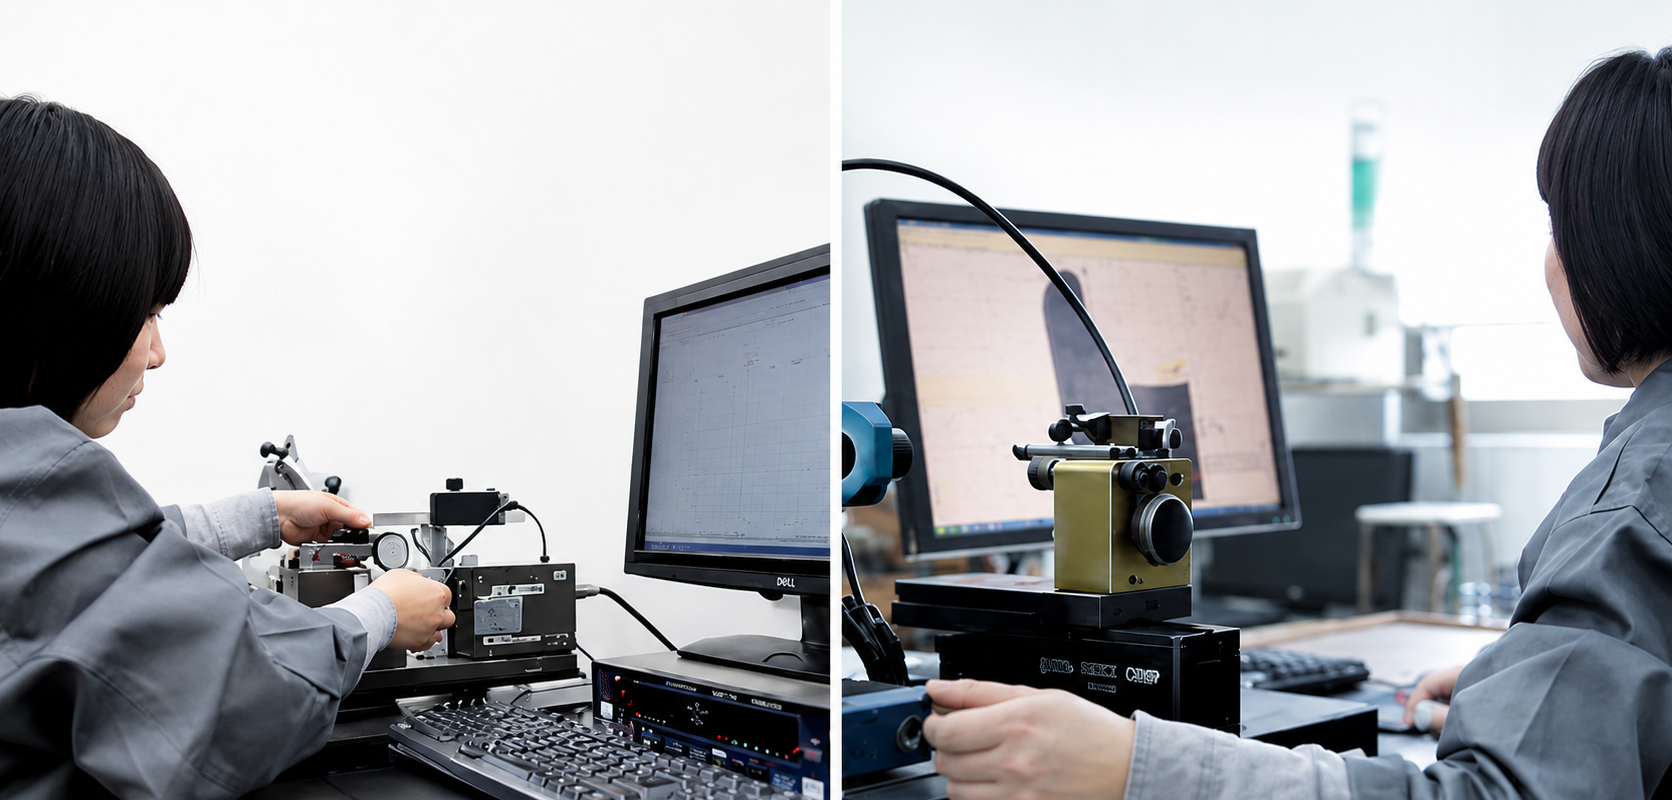
HSS drills are reviewed against the confirmed product specification or approved drawing. Checks are selected according to drill type, size, geometry and finish, from incoming material through grinding, final inspection and packing.
Material Verification
Check the specified HSS grade and incoming material information against the production order.
In-Process Checks
Review key dimensions and ground features during production so deviations can be addressed before final inspection.
Final Tool Inspection
Check the applicable diameter, lengths, point geometry, cutting edges and shank against the approved specification.
Marking & Packing
Verify the model identification, order quantity and agreed packaging before dispatch.
Inspection Checkpoints
| Recurso | Check Against the Confirmed Specification |
|---|---|
| Cutting Diameter | Nominal size and specified diameter tolerance |
| Flute & Overall Length | Required cutting length, tool reach and overall dimension |
| Point Geometry | Point angle, symmetry and specified point features |
| Cutting Edges & Flutes | Visible edge condition and the relevant ground flute features |
| Shank & Finish | Specified shank dimensions and applicable coating or surface finish |
| Order Identification | Model, size, quantity, marking and agreed packaging |
 Learn more about our manufacturing and quality process.
Product FAQs
What sizes are listed for these M2 HSS Morse taper drills?
The specification table lists 134 diameters from Ø5 to Ø76 mm. Flute lengths (L1) range from 52 to 260 mm, overall lengths (L) from 133 to 447 mm, and Morse taper sizes from MT1 to MT5. Check the exact combination for your selected diameter in the size chart.
How do I choose the correct Morse taper size?
Select the required drill diameter first, then check its assigned MT number in the specification table. The taper must fit the machine spindle, tailstock or a suitable reducing sleeve. Confirm that both taper surfaces are clean and that the drill seats correctly before machining.
Which materials can these M2 HSS drills machine?
M2 HSS is a general-purpose choice for carbon steel, structural steel, low-alloy steel, cast iron and selected non-ferrous metals when the drill geometry and cutting conditions are matched to the workpiece. For stainless steel or heat-resistant alloys, provide the material grade and hardness so the appropriate HSS grade and point geometry can be reviewed.
Are 118°, 135° and split-point drills all standard specifications?
The product images illustrate these point-geometry options, but the dimension table does not assign a point form to each diameter. Confirm the available point angle and whether a split point is required for the exact size before ordering.
Does flute length equal the maximum drilling depth?
No. L1 is the physical flute length. Usable drilling depth also depends on the drill point, chip clearance, coolant delivery, workholding and whether the hole is blind or through. Provide the required hole depth when selecting the drill.
How should I set speed and feed for larger diameters?
Select cutting speed and feed per revolution for the confirmed M2 HSS drill geometry, workpiece material, diameter and coolant setup. Larger diameters generally require a lower spindle speed at the same cutting speed. Check machine rigidity and chip evacuation; assess whether a pilot hole is appropriate, then validate the setup with a trial hole.
Ordering & OEM FAQs
What information should I send for a quotation?
Send the required diameter and quantity per size, machine socket or MT number, workpiece material, hole depth and hole type. Include any requirements for point angle, split point, surface finish, diameter tolerance, marking or packaging.
Can I request non-standard dimensions or OEM branding?
Custom diameter, flute length, overall length, point geometry, surface finish and OEM marking requests can be reviewed. Send a drawing or specification sheet; feasibility, tolerance, minimum quantity and lead time will be confirmed for the requested configuration.
Can I order several diameters together?
Yes. Send a diameter-by-diameter quantity list for a mixed-size quotation. Stock availability, MOQ and dispatch timing will be confirmed for each selected size. If you require Ø37.5 mm or Ø44 mm, request confirmation because those diameters are not listed in the supplied table.
Downloads & Technical Reference
For general HSS drilling calculations and starting references, see the HSS cutting tools speeds & feeds guide. Confirm tool-specific cutting data for the ordered diameter, point geometry and workpiece.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.