

8D Through-Coolant Solid Carbide Drill for Deep-Hole Drilling
8×D Depth
Deep-Hole Drilling
Through-Coolant
Chip Evacuation
Helical Flutes
Chip Flow
Solid Carbide
Drilling Stability
8D Through-Coolant Carbide Drill for Deep-Hole Drilling
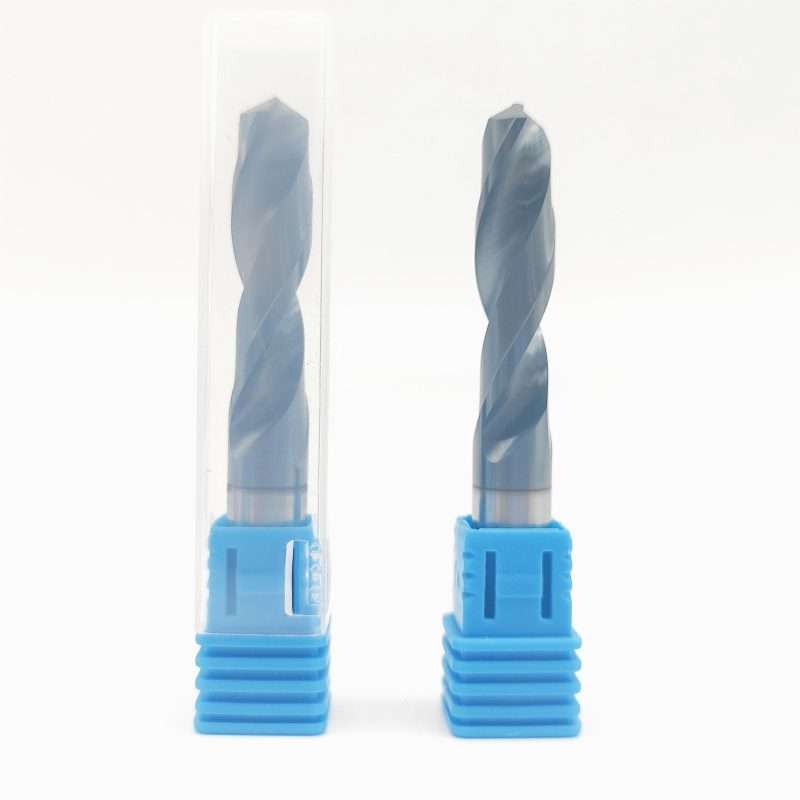
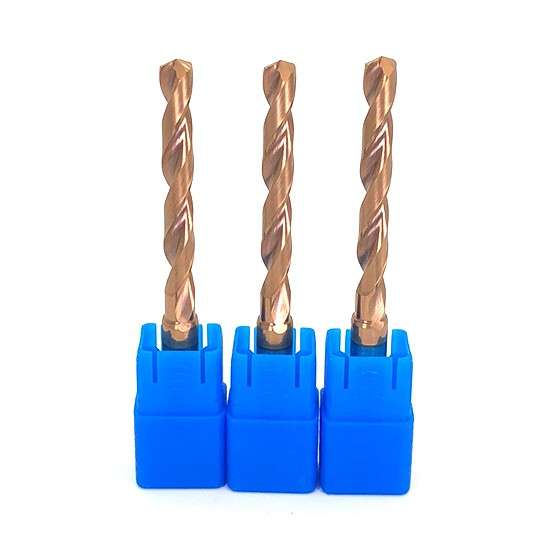
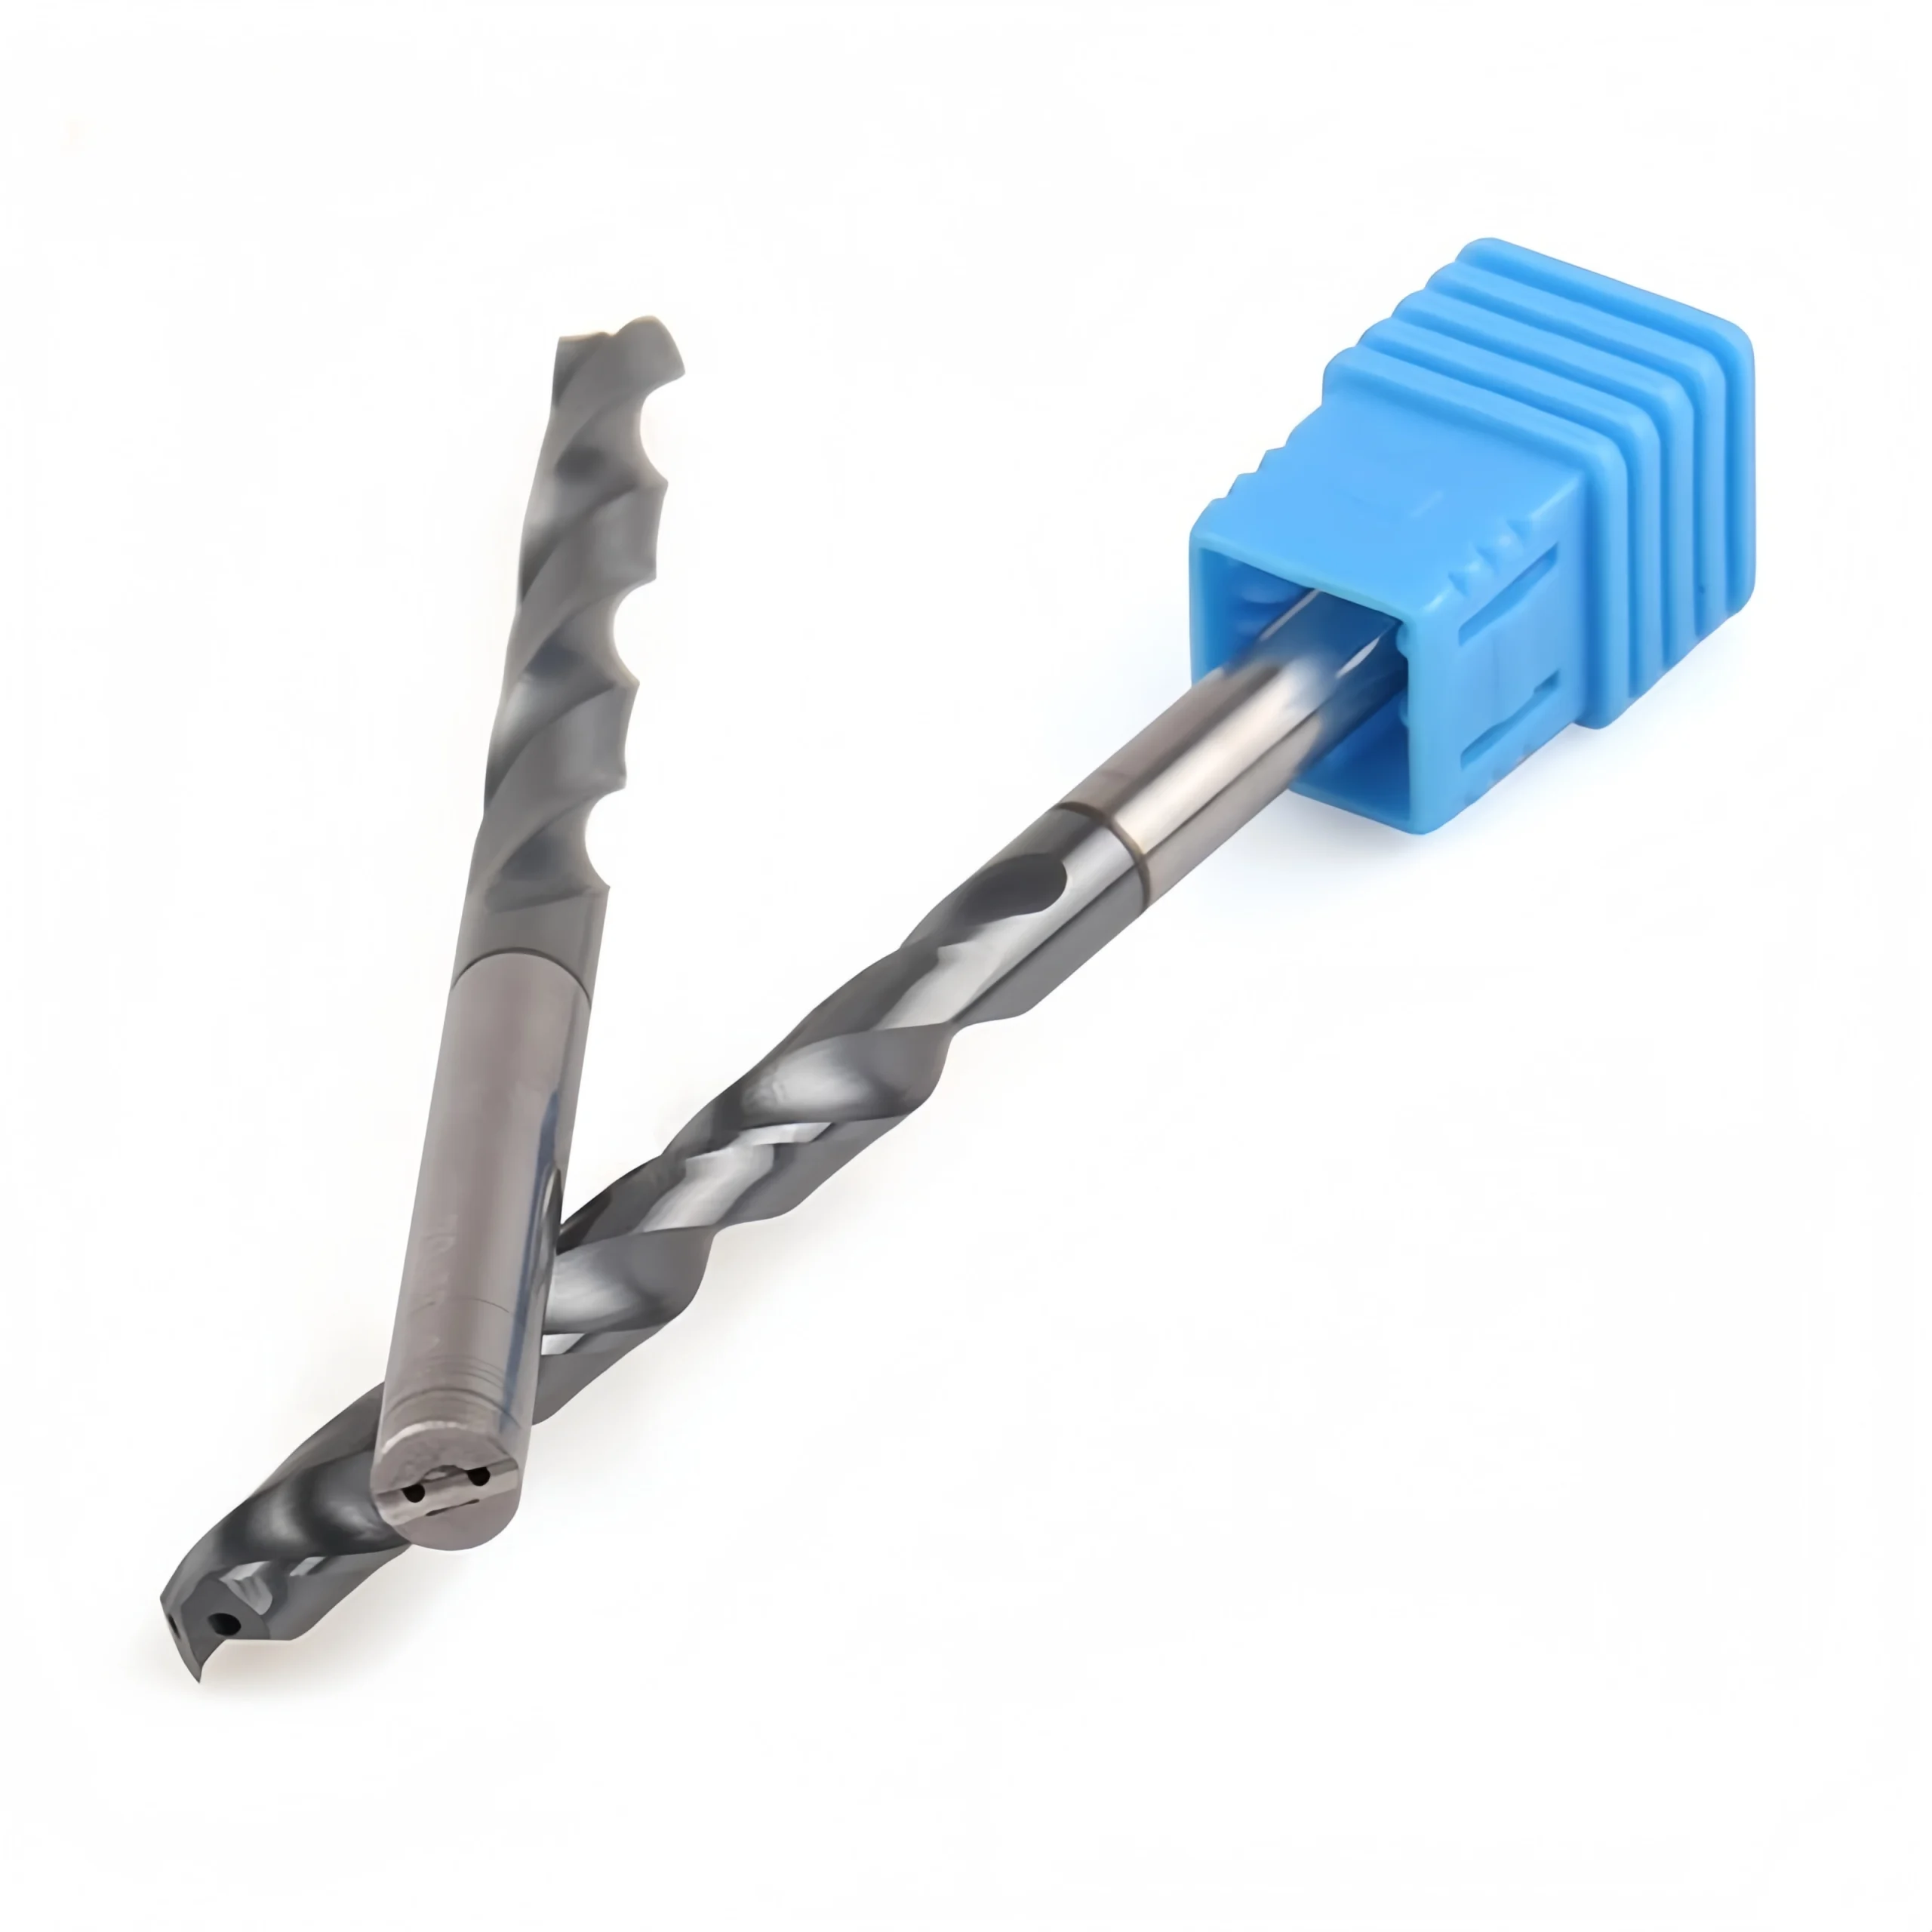
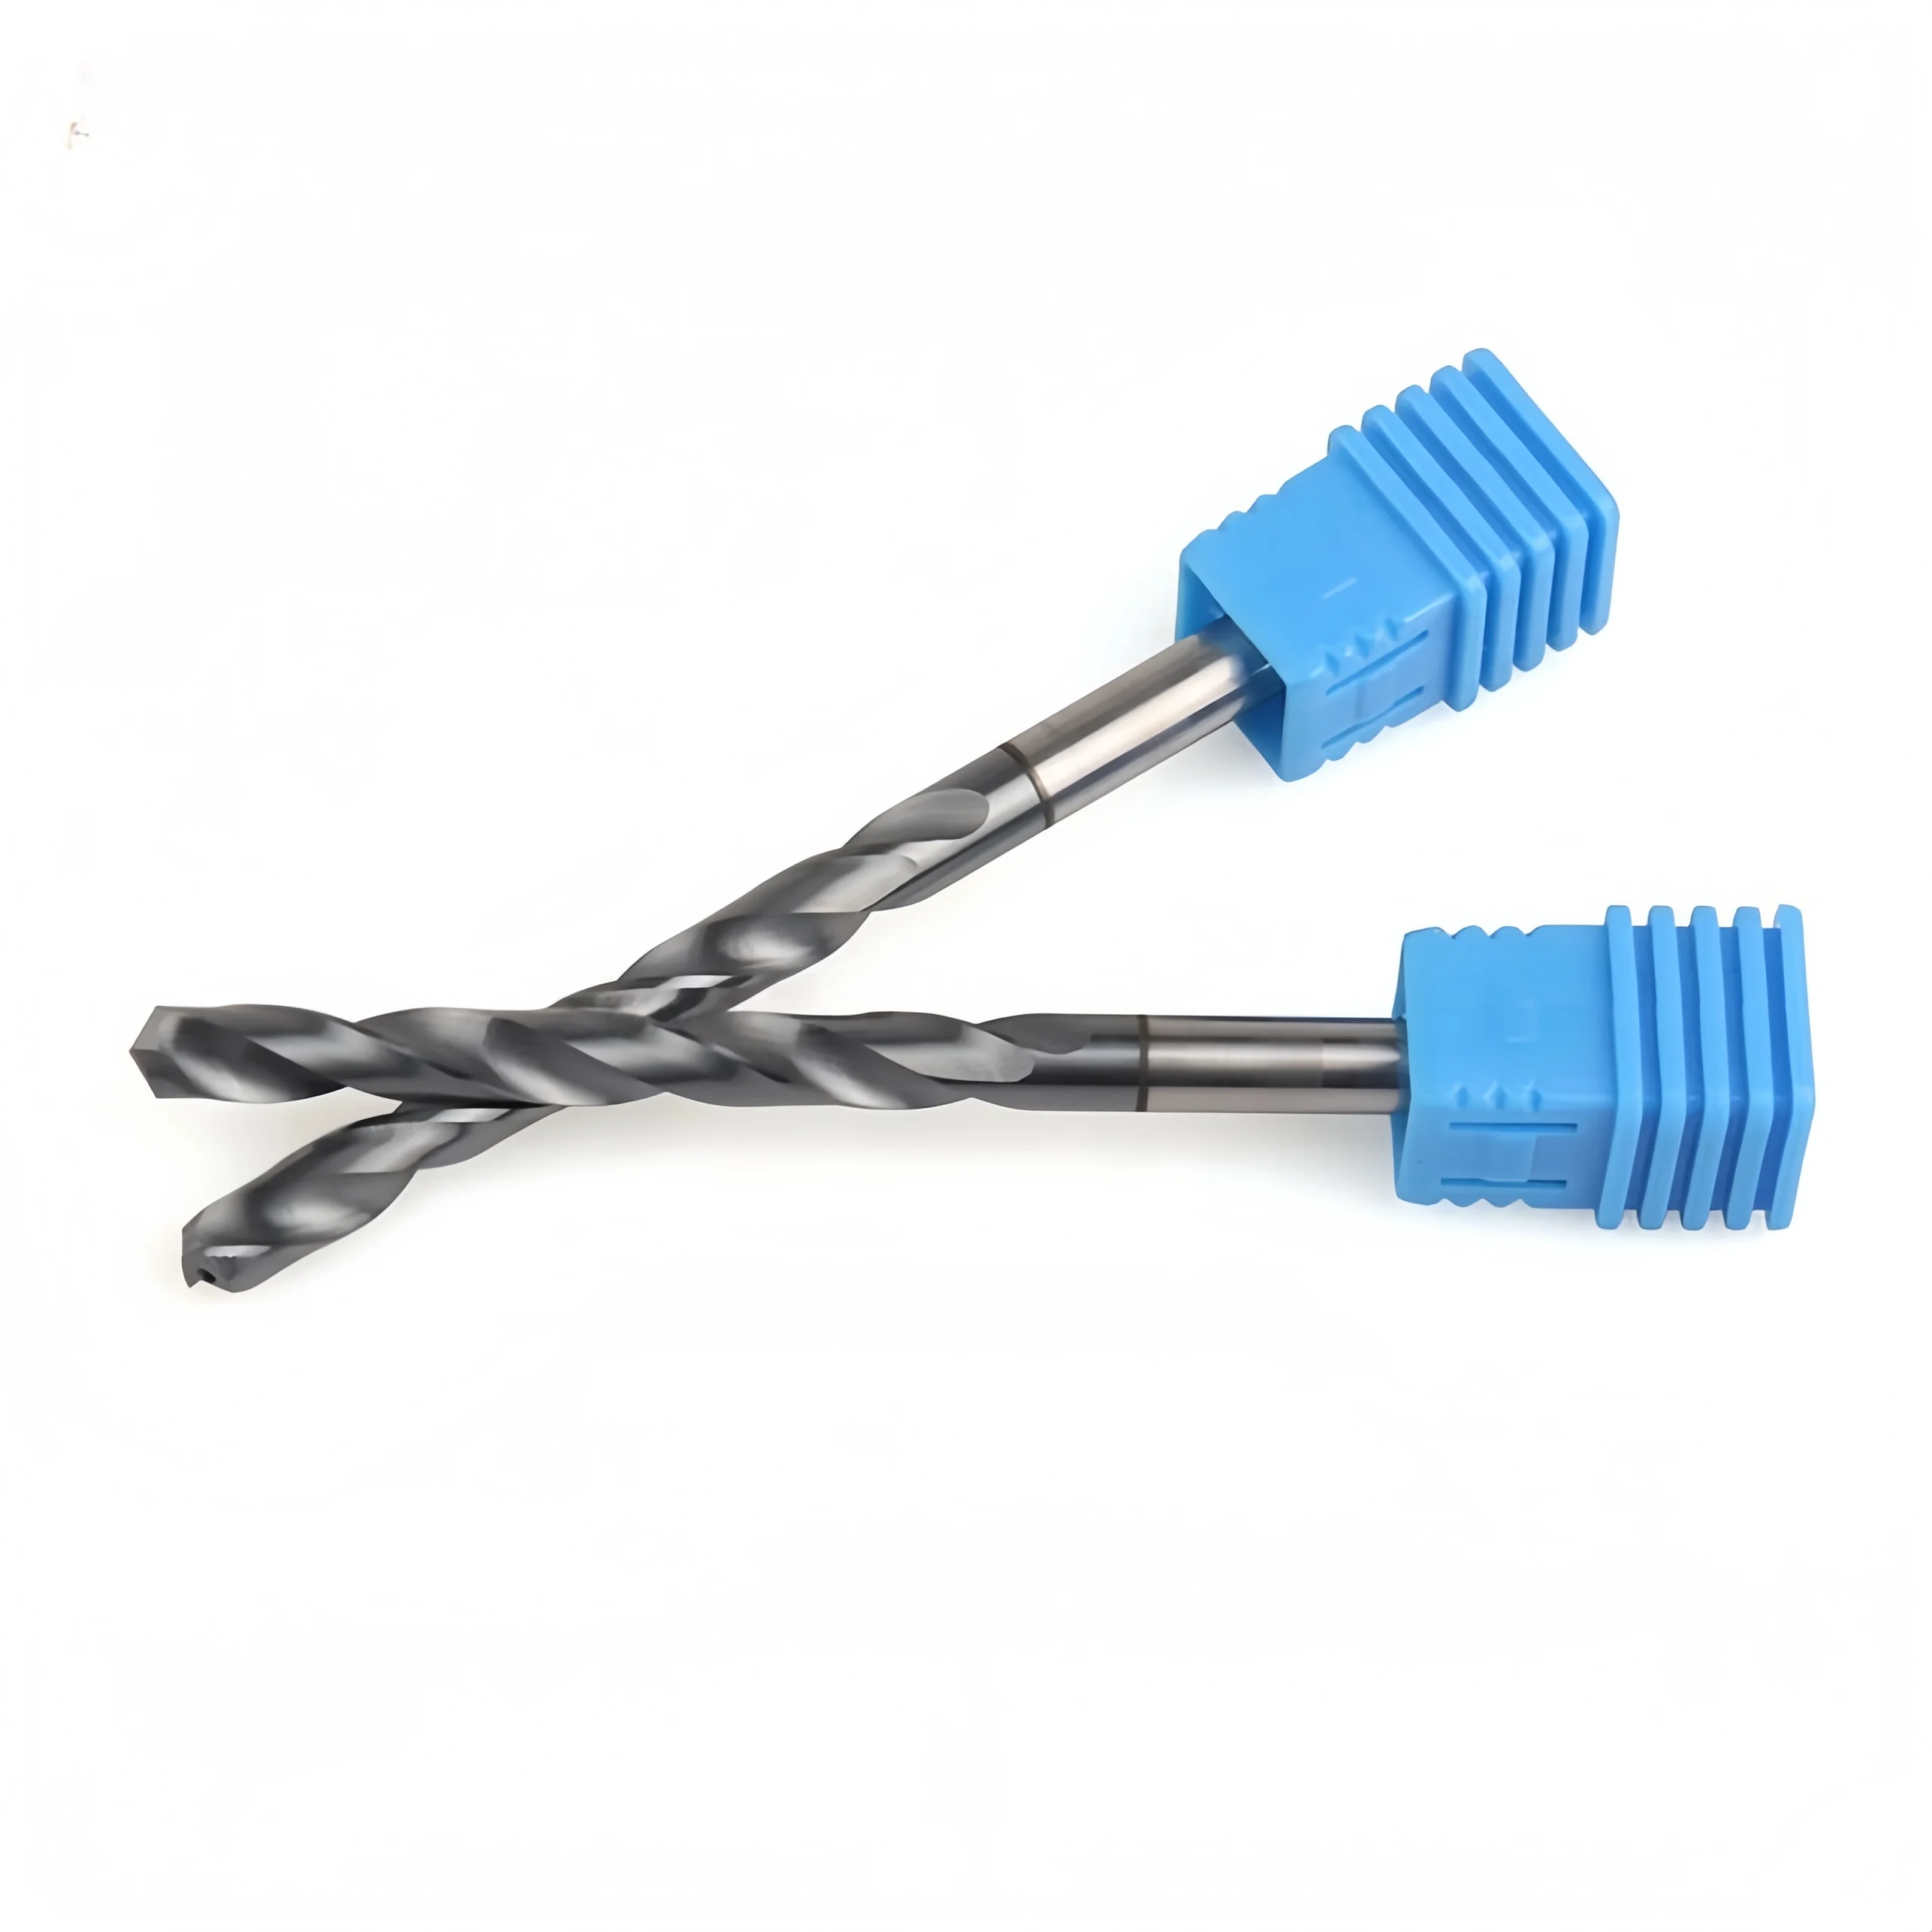
This 8D through-coolant solid carbide drill is designed for CNC deep-hole drilling up to 8×D. Internal coolant and extended helical flutes help evacuate chips and control cutting heat. Reference diameters range from Ø3 to Ø20 mm, with custom options available for review.
8D Deep-Hole Drill Configuration
1
8×D Drilling Depth
Extended geometry for holes up to a nominal depth of 8×D.
2
Internal Coolant Delivery
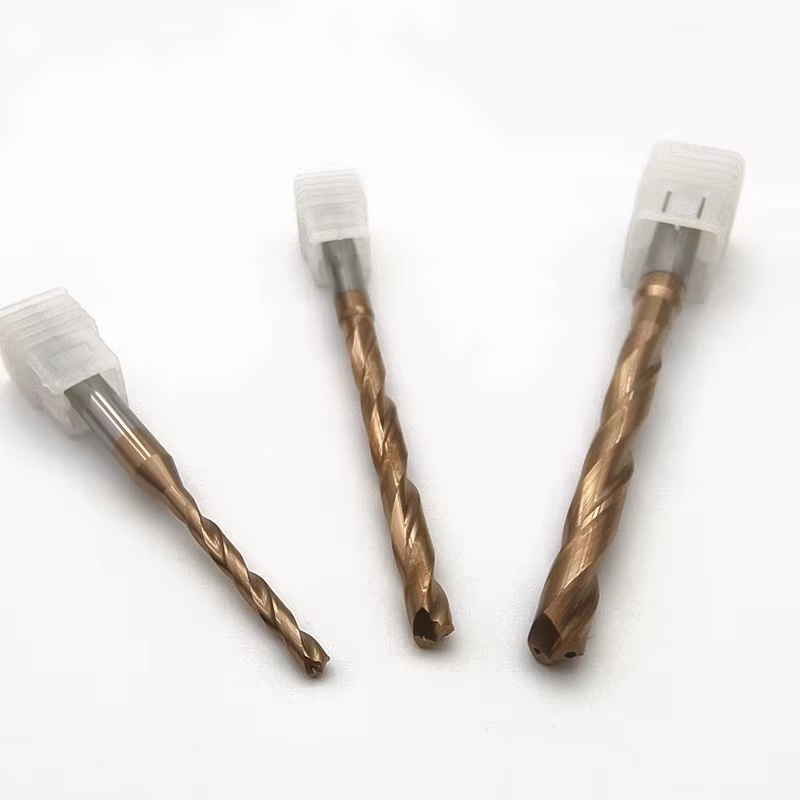
Coolant reaches the drill point to assist deep-hole chip evacuation and cooling.
3
Helical Flutes & Coating
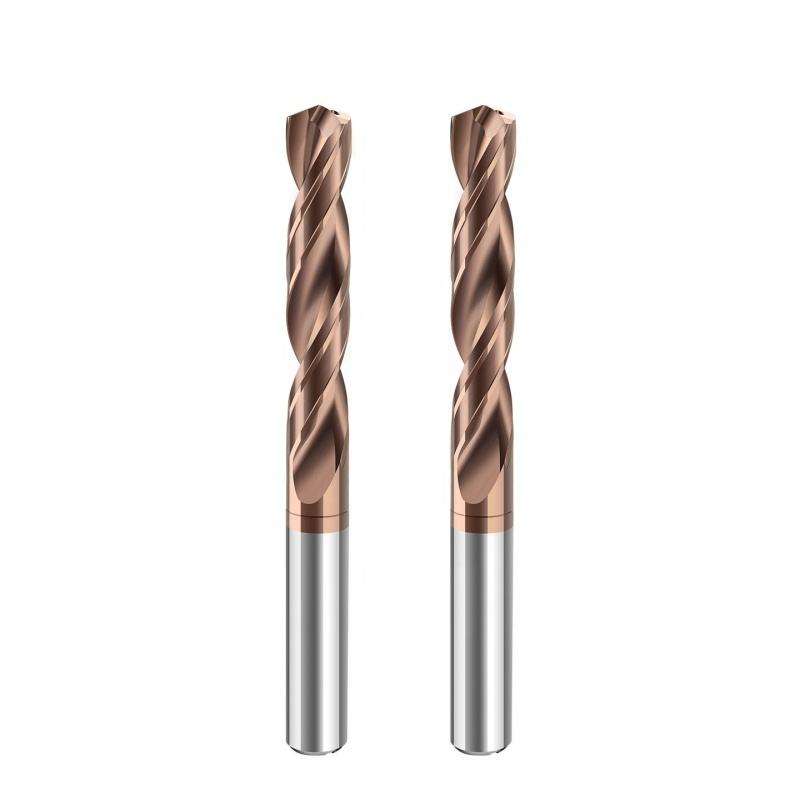
Helical flutes guide chips out of the hole; coating options support wear resistance.
8D Through-Coolant Drill Product View
8D Deep-Hole Drill Advantages
01
8×D Deep-Hole Reach
Extended flutes provide chip space for 8×D drilling.
02
Coolant at the Drill Point
Through-coolant reaches the cutting zone inside deep holes.
03
Solid Carbide Rigidity
Solid carbide construction supports stable CNC deep-hole drilling.
04
Deep-Hole Chip Evacuation
Helical flutes and coolant help move chips out of 8×D holes.
05
Wear-Resistant Coating
Application-matched coatings help manage cutting-edge wear.
06
Precision Shank Clamping
Straight shank suits compatible low-runout holders.
Internal Coolant & Cutting-Edge Detail
Chip Flow: Coolant assists chip flow through extended flutes.
8D Drill Geometry & Product Views
Why Through-Coolant Matters in 8D Drilling
At 8×D depth, chips travel farther and external coolant has limited access to the drill point. Internal coolant supports heat control and chip evacuation inside the hole.
8D Deep-Hole Drilling Applications
- Mold cooling channels and tooling plates
- Deep holes in hydraulic manifolds and valve blocks
- Automotive housings and structural components
- 8×D holes in precision CNC components
- Blind and through holes with internal coolant
- Standard and custom deep-hole drilling applications
8D Deep-Hole Drilling Requirements
• Low-Runout Toolholding
Use a precision holder and minimize overhang.
• Stable Internal Coolant
Check coolant pressure, flow, filtration and clear outlets.
• Material-Matched Cutting Data
Match speed and feed to material, hardness, diameter and coating.
• Monitor Chip Flow
Stop drilling if chips pack or coolant flow becomes restricted.
For holder, runout and coolant setup, see our tooling system and CNC productivity guide.
8D Through-Coolant Drill Dimensions
Reference dimensions for 8D through-coolant carbide drills designed for deep-hole drilling and chip evacuation. Available sizes: Ø3–20 mm.

8D Carbide Drill Standard Sizes
Reference cutting diameters, flute lengths and overall lengths. All dimensions in mm.
| Cutting Diameter d1 | Flute Length L1 | Overall Length L |
|---|---|---|
| 3 | 30 | 70 |
| 4 | 42 | 83 |
| 5 | 50 | 90 |
| 6 | 57 | 97 |
| 7 | 76 | 116 |
| 8 | 76 | 116 |
| 9 | 87 | 131 |
| 10 | 95 | 139 |
| 11 | 106 | 155 |
| 12 | 114 | 163 |
| 13 | 133 | 182 |
| 14 | 133 | 182 |
| 15 | 152 | 204 |
| 16 | 152 | 204 |
| 17 | 171 | 223 |
| 18 | 171 | 223 |
| 19 | 190 | 244 |
| 20 | 190 | 244 |
Dimension Note: L1 is flute length, not maximum blind-hole depth. Confirm usable 8×D depth and drill-point allowance.
Need Sizes, Pricing or Custom Options?
Send your diameter, hole depth, material, coolant conditions and quantity.
Request a Quote8D Deep-Hole Drill Customization
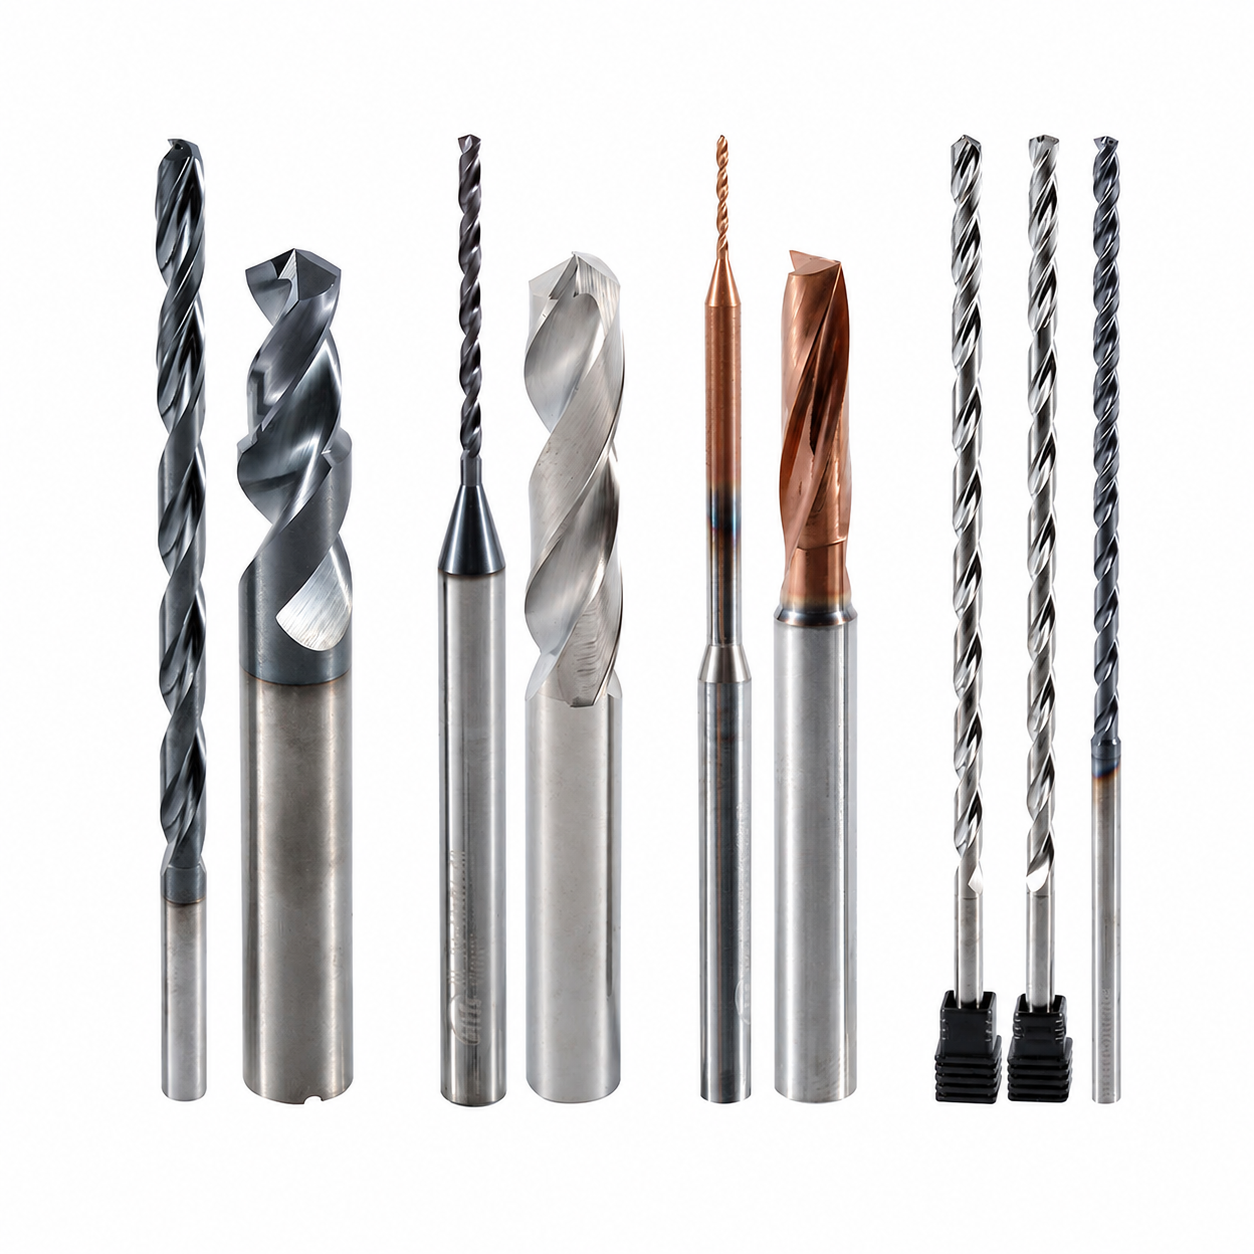
Custom 8D through-coolant carbide drills with application-matched geometry, dimensions and coatings for deep-hole drilling and chip evacuation.
Deep-Hole Geometry & Coating
Custom point, flute, margin and edge geometry, with coatings selected for the workpiece material.

8D Dimensions & Coolant Design
Custom diameters, lengths and shanks, with internal coolant options reviewed for 8×D depth.
Engineering Review: Confirm hole depth, material, tolerance, coolant pressure, pilot-hole requirements and quantity before production.
OEM & Private-Label 8D Drills
OEM deep-hole drill supply for cutting-tool distributors, tooling brands and repeat orders.
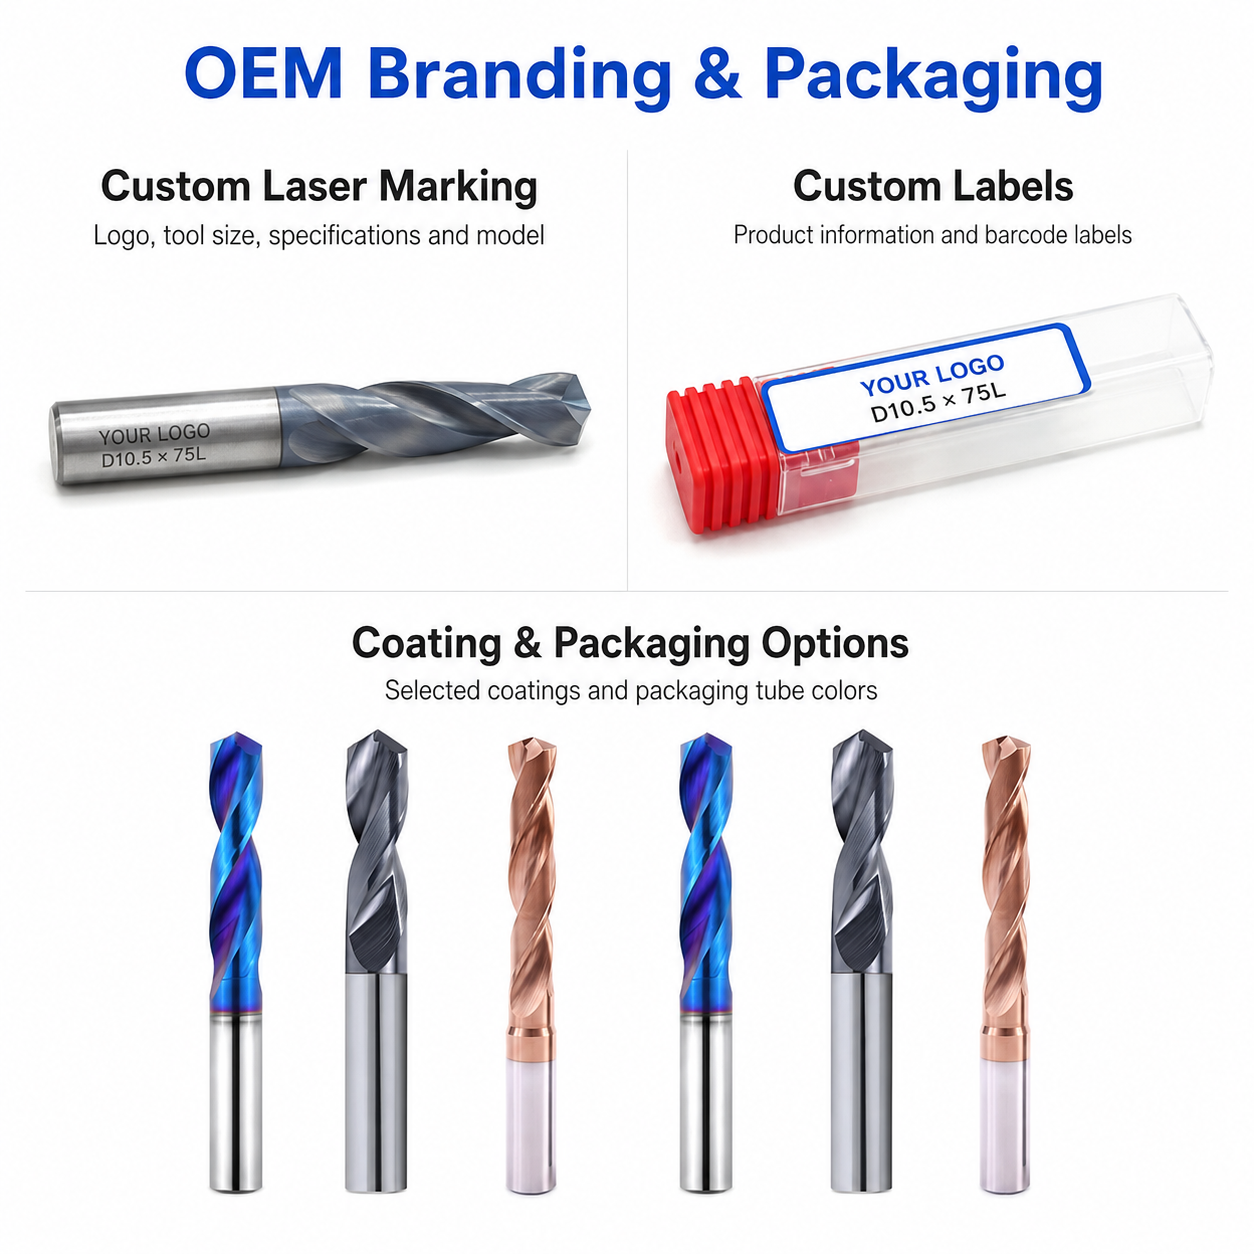
Laser Marking
Custom logos, tool codes and size marking.
Private-Label Packaging
Protective tubes, custom labels and branded boxes.
Trial & Repeat Orders
Small-batch trials and repeat supply by approved specifications.
8D Deep-Hole Drill Quality Control
Inspection of 8D through-coolant carbide drills focuses on dimensions, cutting geometry and visible coolant outlet condition.
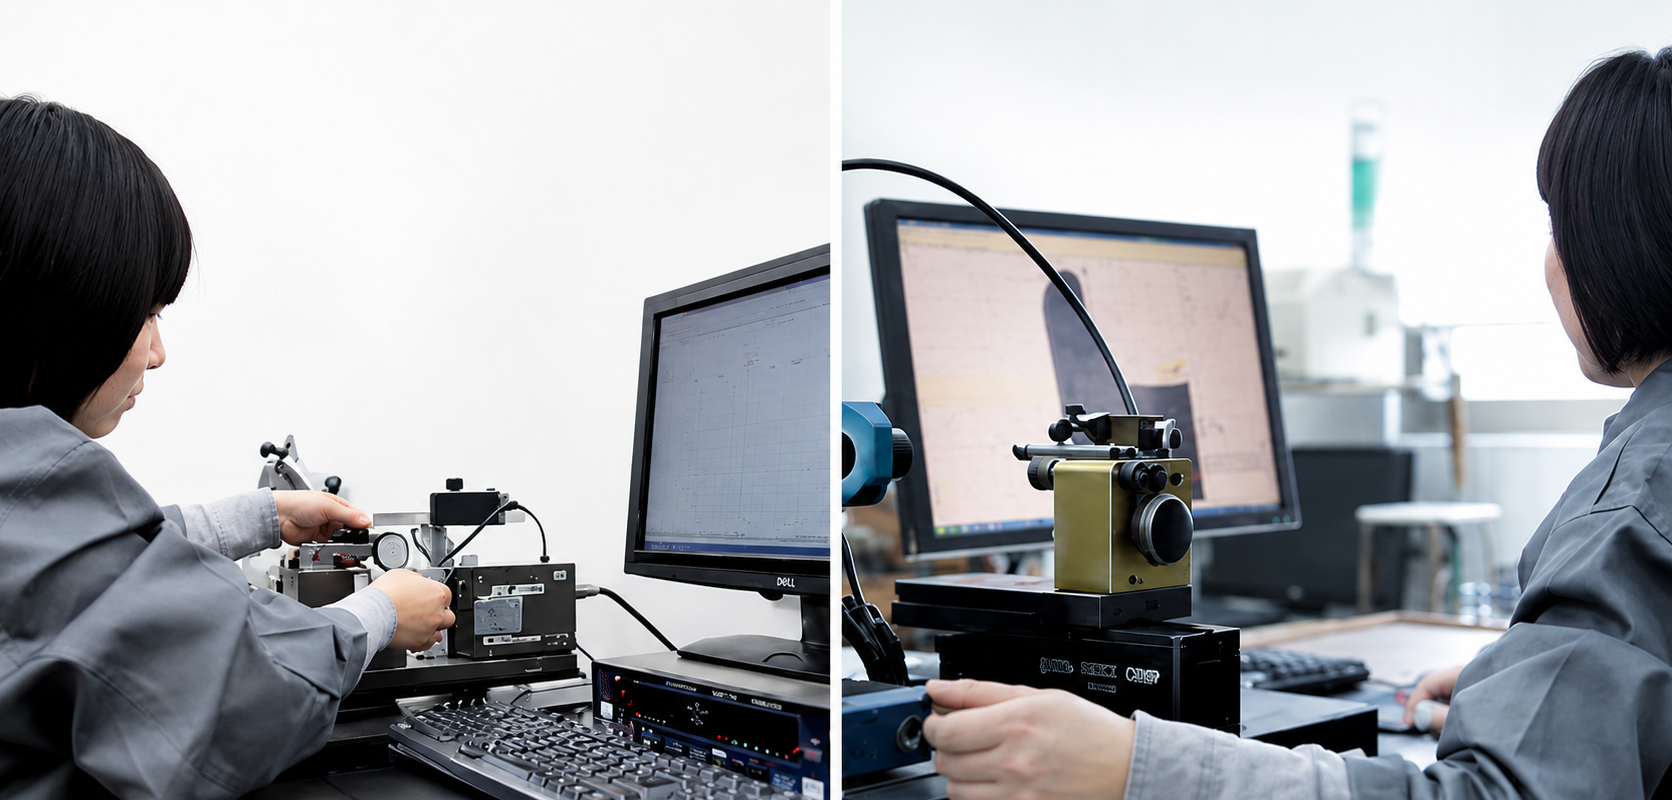
Dimensions & Runout
Diameter, 8D lengths, shank and runout.
Cutting Geometry
Drill point, helical flutes, edges and coating.
Coolant Outlets
Visible outlet position and condition.
Inspection tolerances and any coolant flow testing are confirmed by specification.
View Manufacturing & QualityProtective Packaging & Batch Identification
Individual protection and batch labels support safe shipment and repeat supply of carbide deep-hole drills.

Individual Protection
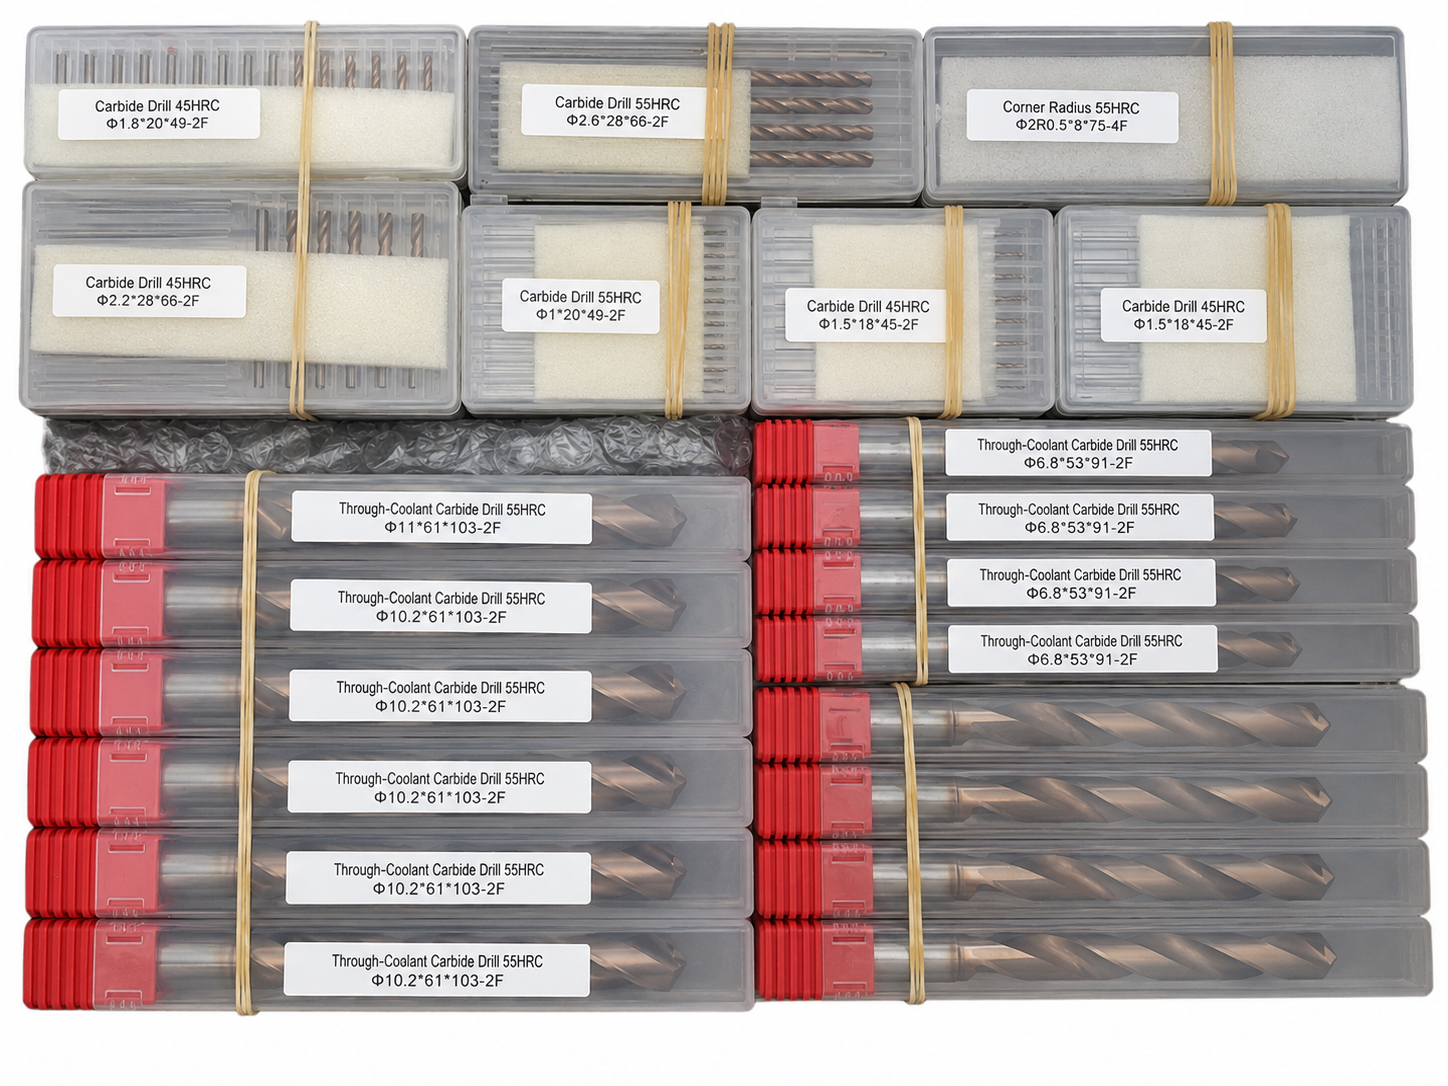
Batch Identification

Export Packaging
OEM labels and private-label packaging are available upon request.
Lead Time & Shipping
Lead Time: Confirmed by 8D drill specifications, coating, quantity and production schedule.
Shipping: International express, air freight, sea freight or customer-nominated forwarder.
View Buyer & Reseller Resources
8D Through-Coolant Carbide Drill FAQs
Common questions about 8×D deep-hole drilling, internal coolant, chip evacuation and machining requirements.
What does 8D mean in carbide drilling?
8D refers to a nominal drilling depth of eight times the cutting diameter. An Ø8 mm drill, for example, has an 8×D depth of 64 mm. Confirm usable depth for the selected tool.
Why use through-coolant for 8D deep-hole drilling?
Internal coolant reaches the drill point and supports chip evacuation and heat control through extended helical flutes.
What coolant pressure is required for an 8D drill?
Required pressure and flow depend on drill diameter, material and hole depth. Use stable through-spindle coolant with suitable filtration and clear channels.
Is a pilot hole required for 8D drilling?
Pilot-hole requirements depend on the drill design, entry surface and machine setup. Confirm the recommended entry procedure before deep-hole drilling.
Which materials are suitable for 8D carbide drills?
Selected steel (ISO P), stainless steel (ISO M) and cast iron (ISO K) applications can be reviewed. Confirm grade, hardness, coating and cutting conditions.
What sizes and hole types are supported?
Reference diameters cover Ø3–20 mm. Blind and through holes can be reviewed within the tool's usable 8×D depth. Allow for drill-point geometry.
How should speeds and feeds be selected for 8D drilling?
Match cutting data to material, hardness, diameter, coating and coolant supply. Verify chip evacuation and machining stability during trials.
8D Deep-Hole Drill Ordering & OEM FAQs
Trial orders, custom specifications and repeat OEM supply.
Can I order small quantities or mixed diameters?
Yes. Small trial orders and mixed Ø3–20 mm sizes are supported, subject to availability and configuration.
Are custom 8D drills and OEM branding available?
Yes. Custom dimensions, geometry, coatings, laser marking and private-label packaging are available for review.
What information is needed for a quotation?
Provide diameter, hole depth, material grade, tolerance, coolant capability and quantity. Lead time is confirmed by specification and order.
Need Sizes, Pricing or Custom Options?
Send your specifications and quantity for a quote.
- Standard Sizes
- Small Trial Orders
- Mixed Sizes
- OEM & Custom
View QR Code – Contact Sales on WeChat
Scan to contact us on WeChat.
Scan to contact us on WeChat.