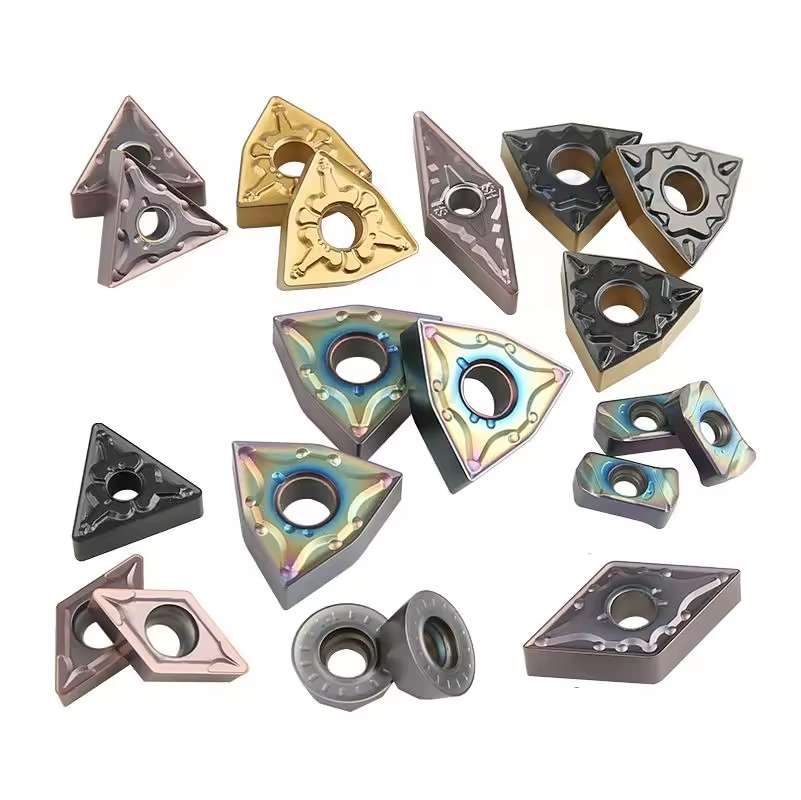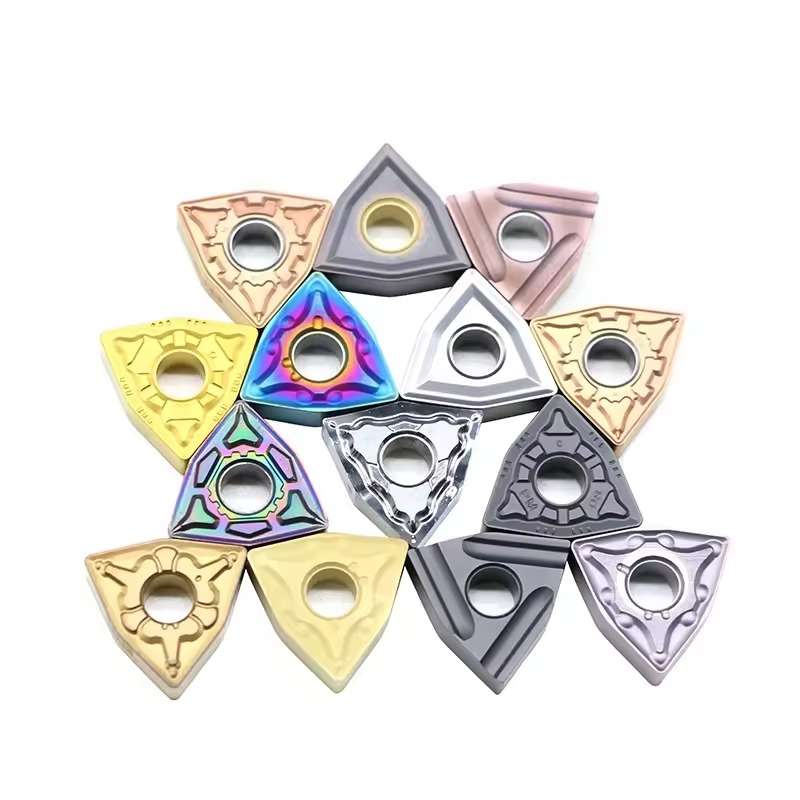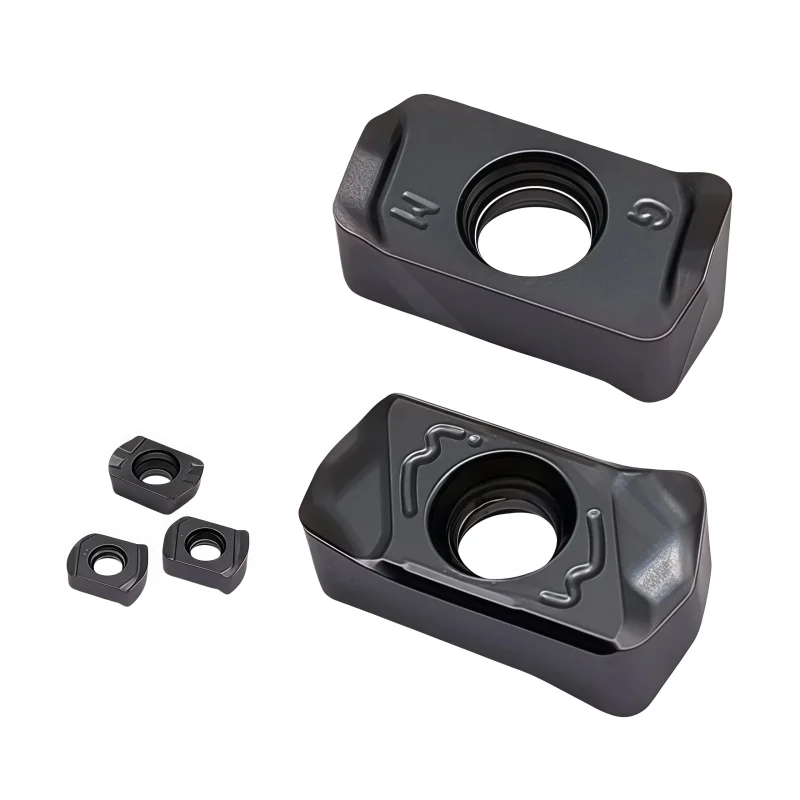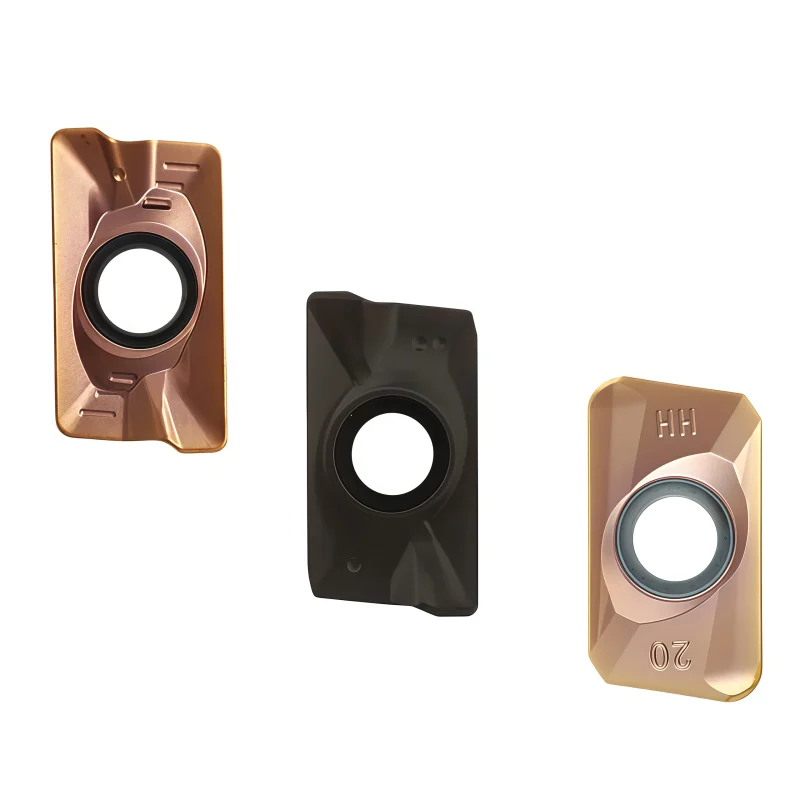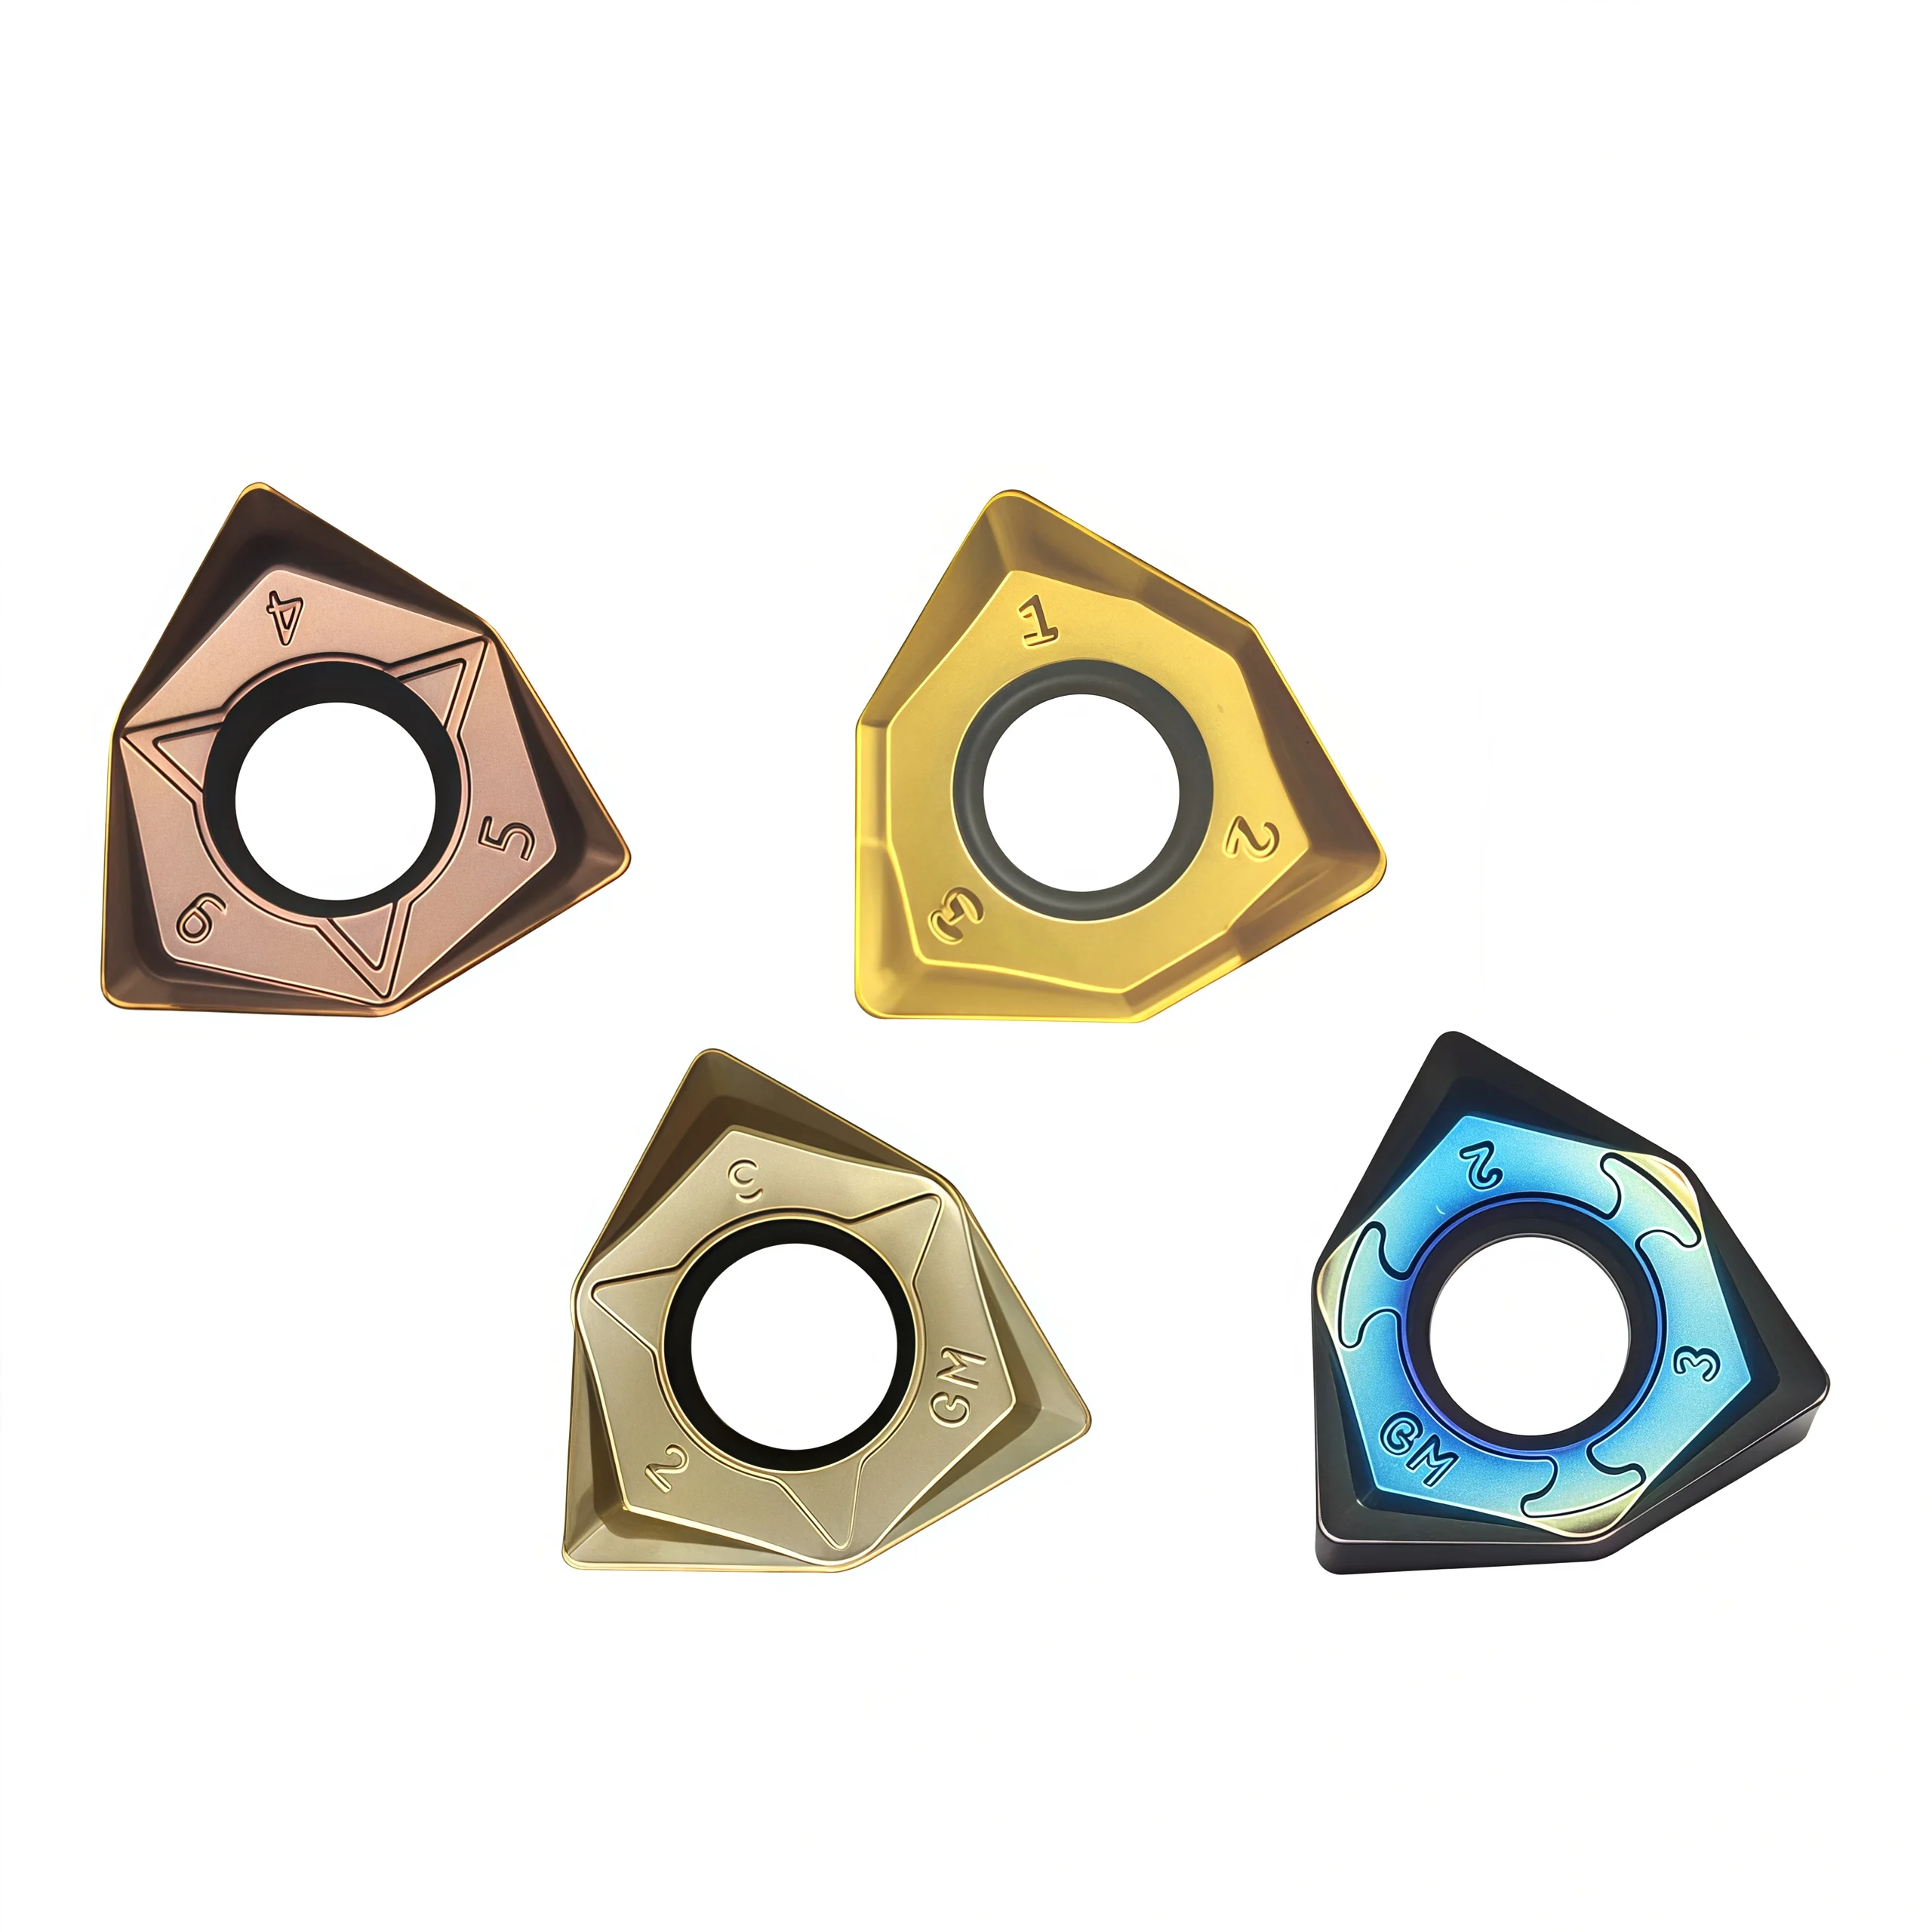
WNMU 040304/060408/080608EN 90° Carbide Shoulder Milling Inserts
WNMU 90° carbide shoulder milling inserts are designed for efficient square-shoulder milling, facing and step machining. The double-sided geometry provides multiple usable cutting edges, while the available sizes support different cutter diameters and machining loads. Suitable grades can be selected for steel, stainless steel and cast iron applications.
Qualità costante
Consistent geometry across repeat orders.
Ordini flessibili
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
Standard e personalizzati
Standard sizes and custom configurations.
◆Panoramica del prodotto
WNMU 040304, 060408 and 080608EN are carbide milling insert sizes offered for compatible 90° shoulder milling cutters. The series targets square-shoulder and side-milling operations where cutter rigidity, edge strength and chip evacuation matter. Choose the insert size and full suffix for the specified cutter pocket, then select the carbide grade and geometry for the workpiece and cutting load.
The supplied description presents a double-sided range for roughing. Actual usable-edge count, maximum axial depth of cut, coating and material range must be confirmed by complete item code and cutter-body drawing. A nominal 90° cutter designation alone does not guarantee a perfectly square wall or a flat pocket floor in every setup.
◆Key Configuration
Three WNMU Sizes
040304, 060408 and 080608EN identify separate size or geometry options. Match the exact designation to the manufacturer’s approved cutter pocket.
90° Shoulder Milling
Use a suitable square-shoulder cutter for wall and floor machining. Verify effective cutting diameter, maximum depth and corner geometry for the complete tool assembly.
Grade & Edges
Confirm carbide grade, coating, chipbreaker and usable edges by SKU. The original copy does not identify one verified PVD grade or common edge count for all three sizes.
◆Applications & Selection
The range may be considered for shoulder milling, side milling and roughing of carbon or alloy steel, stainless steel and cast iron when a suitable insert grade is available. Tool steel and heat-treated workpieces require grade-specific approval. Deep pocketing, slotting, ramping and heavy interrupted cuts depend on the cutter body’s stated limits and machine rigidity.
◆Product Images
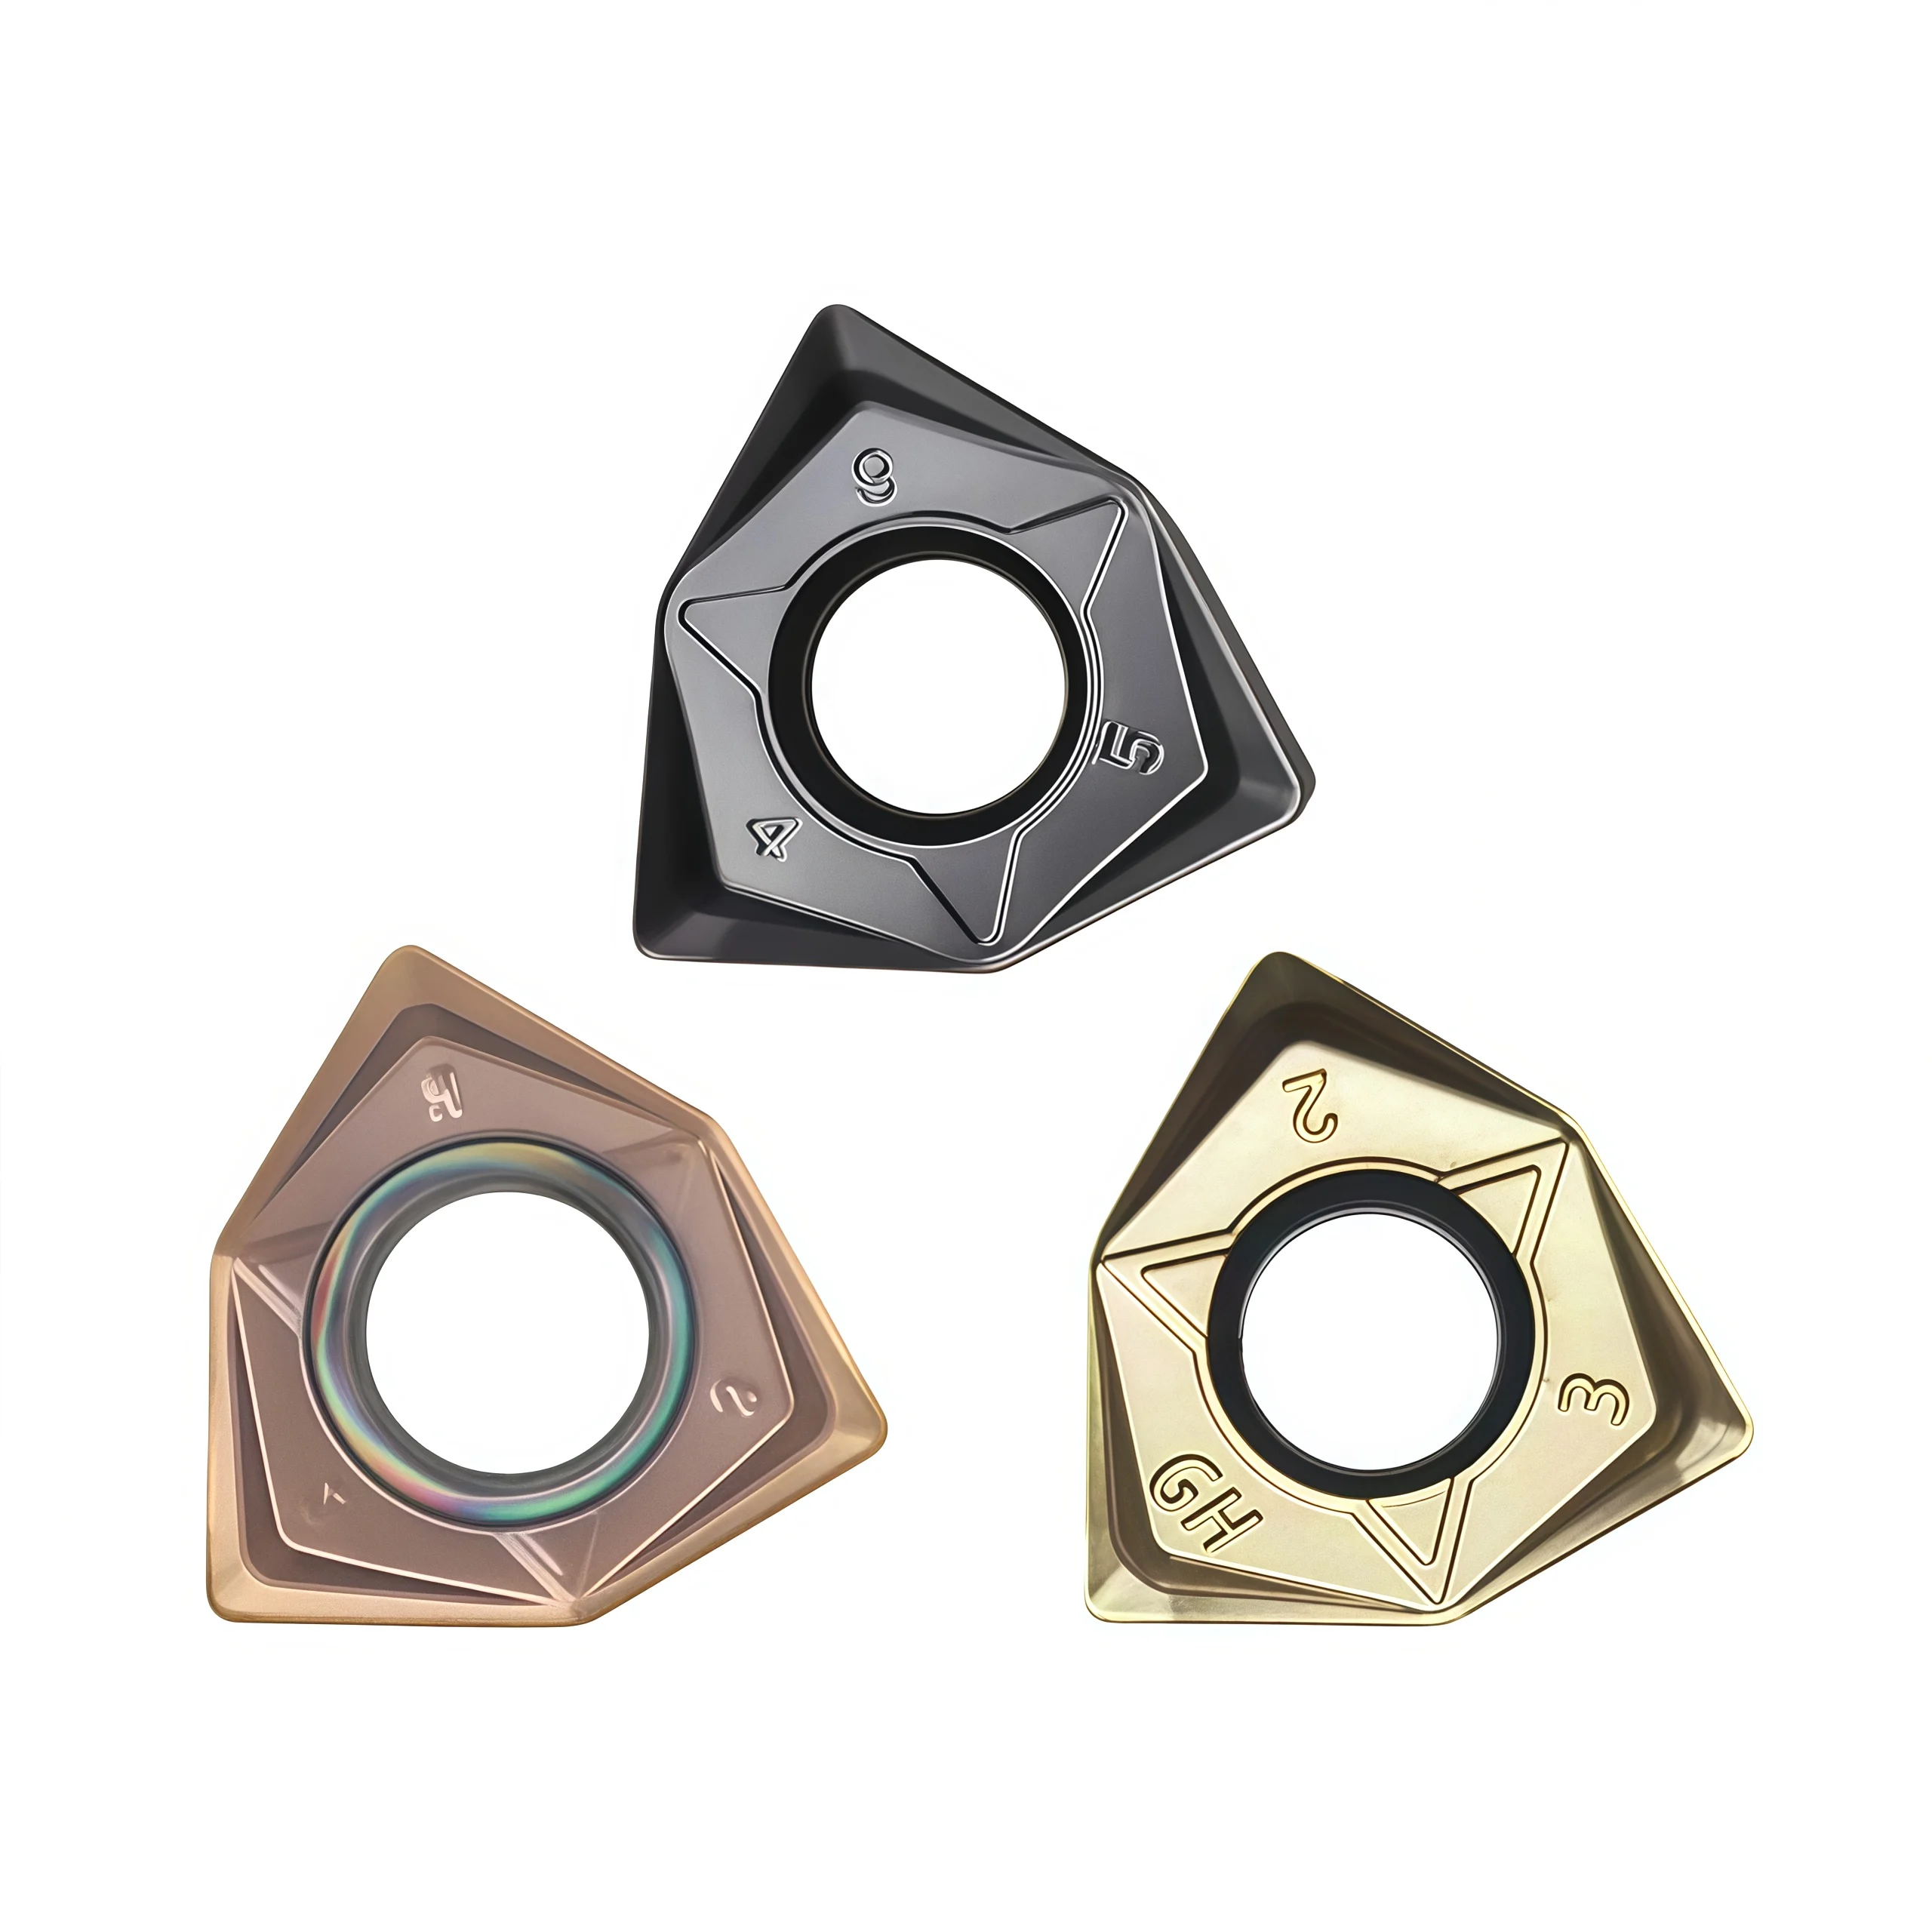
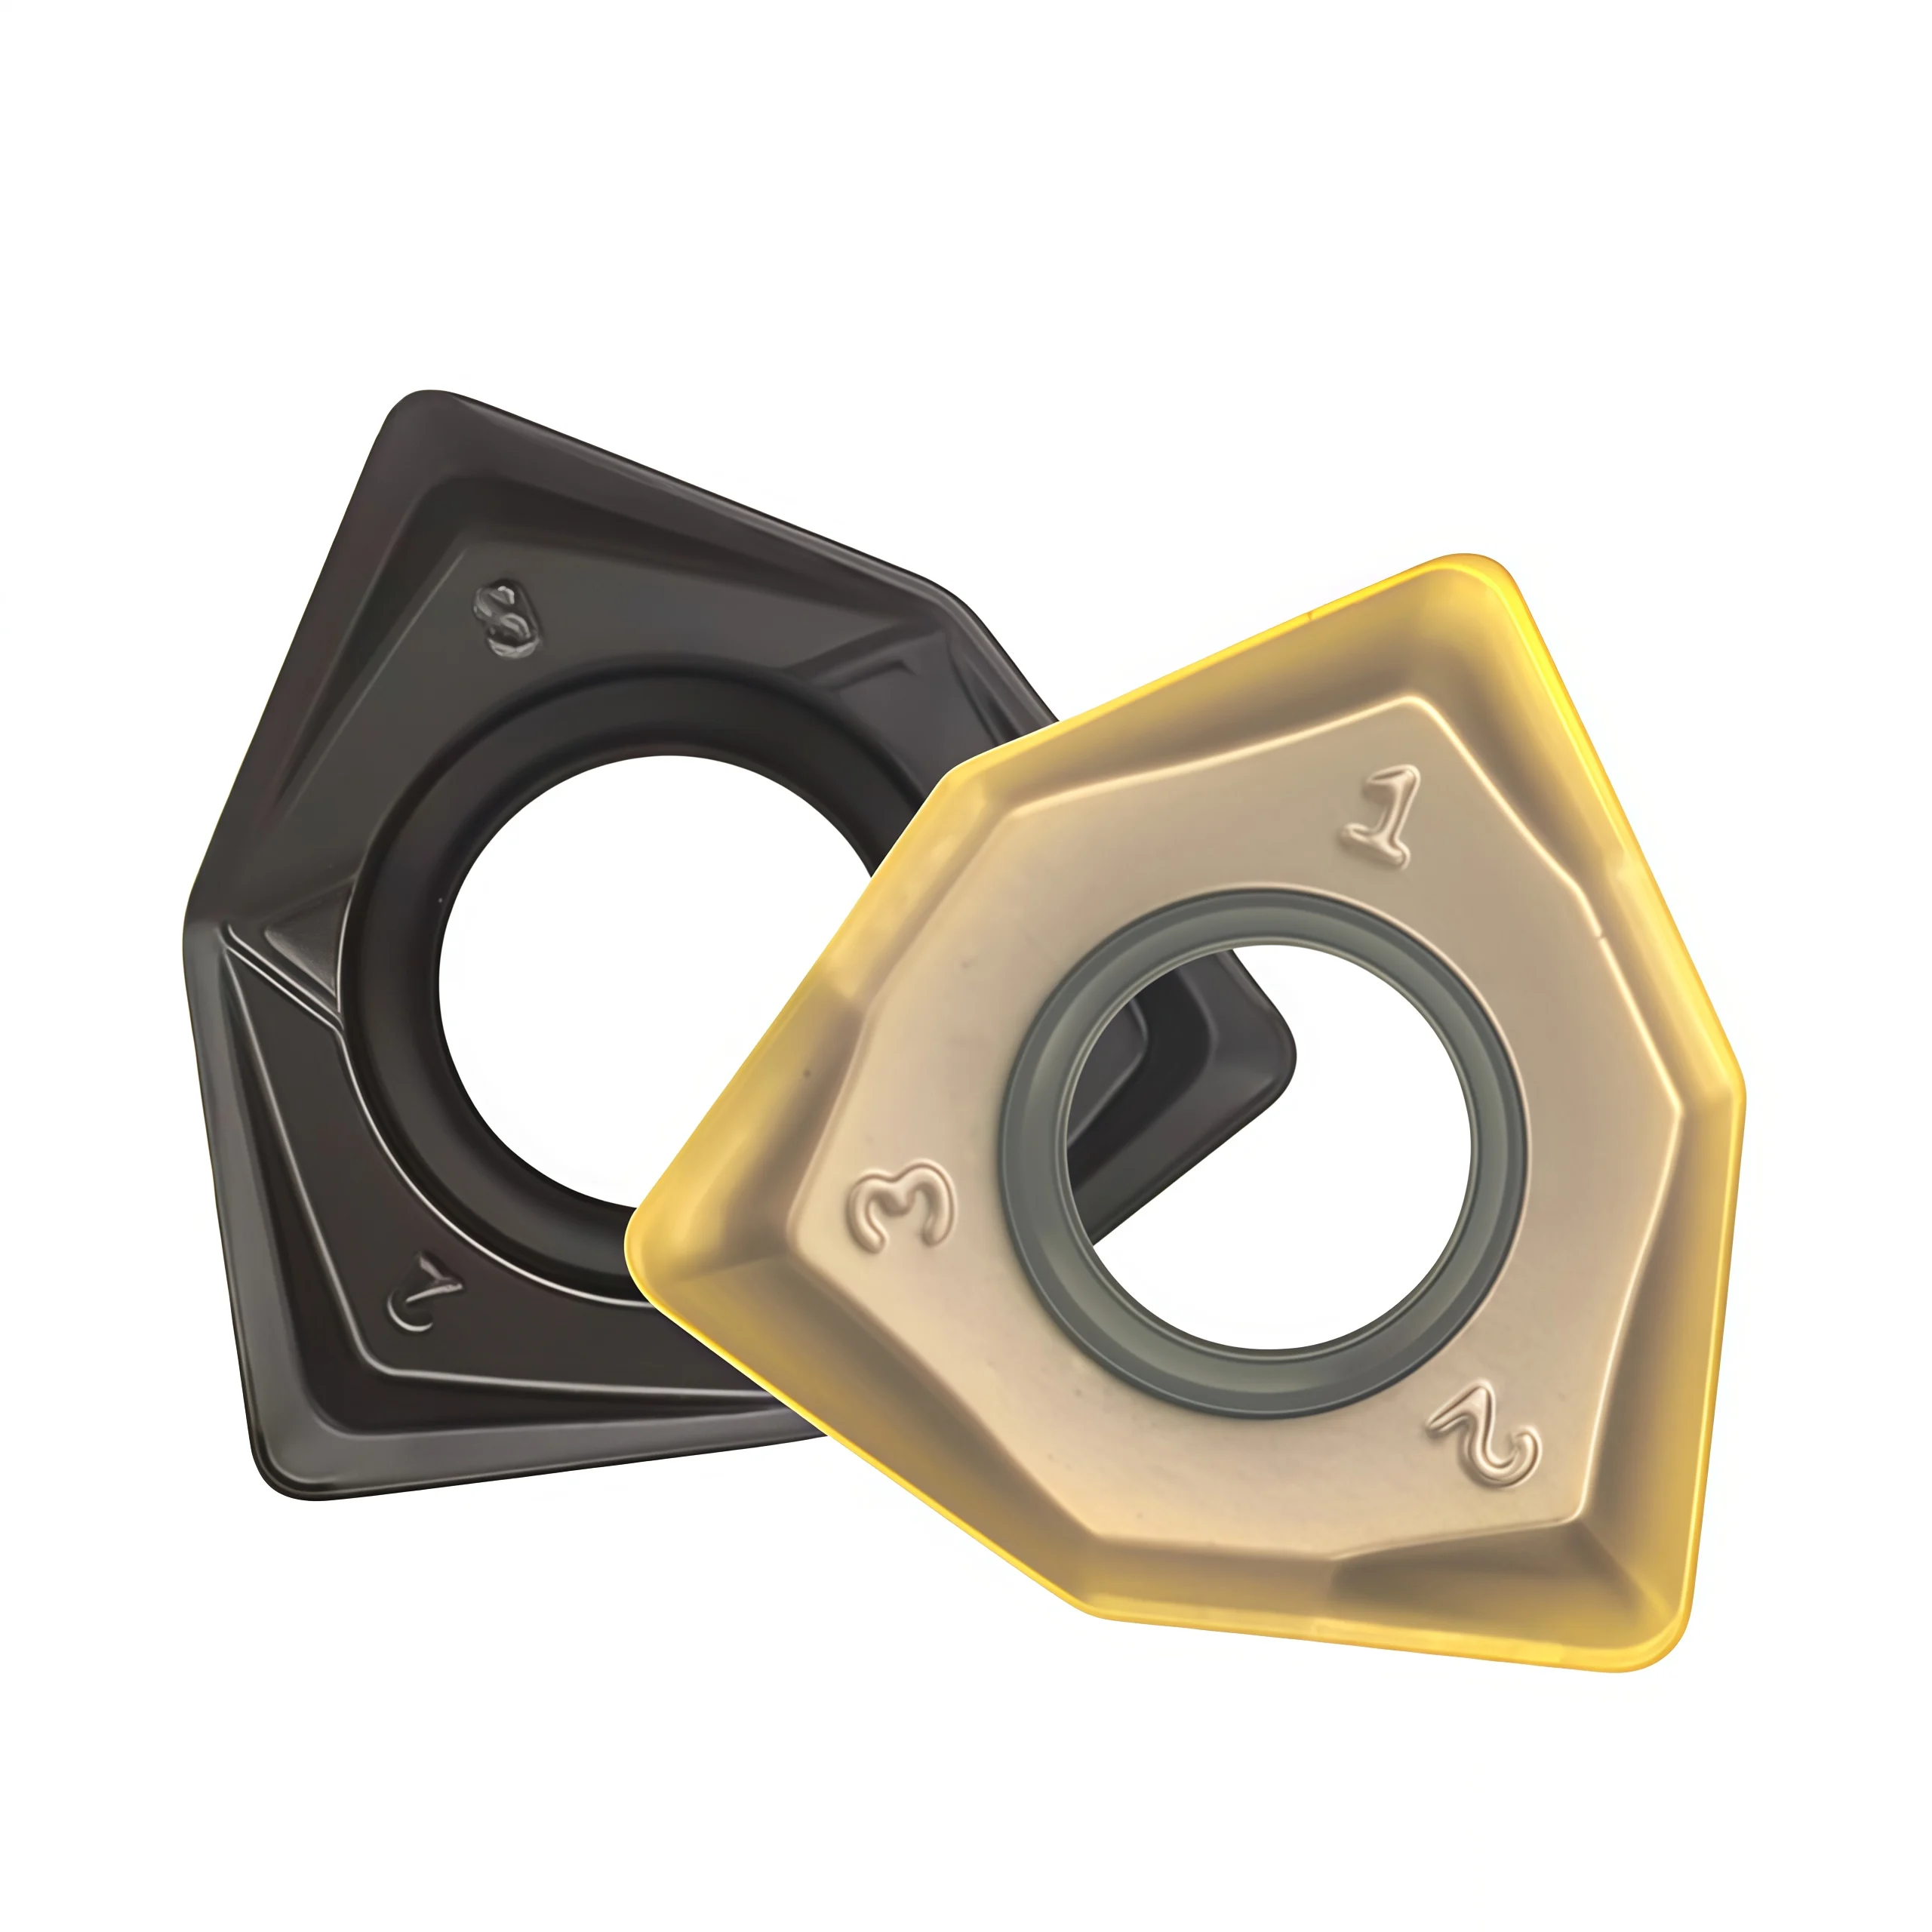
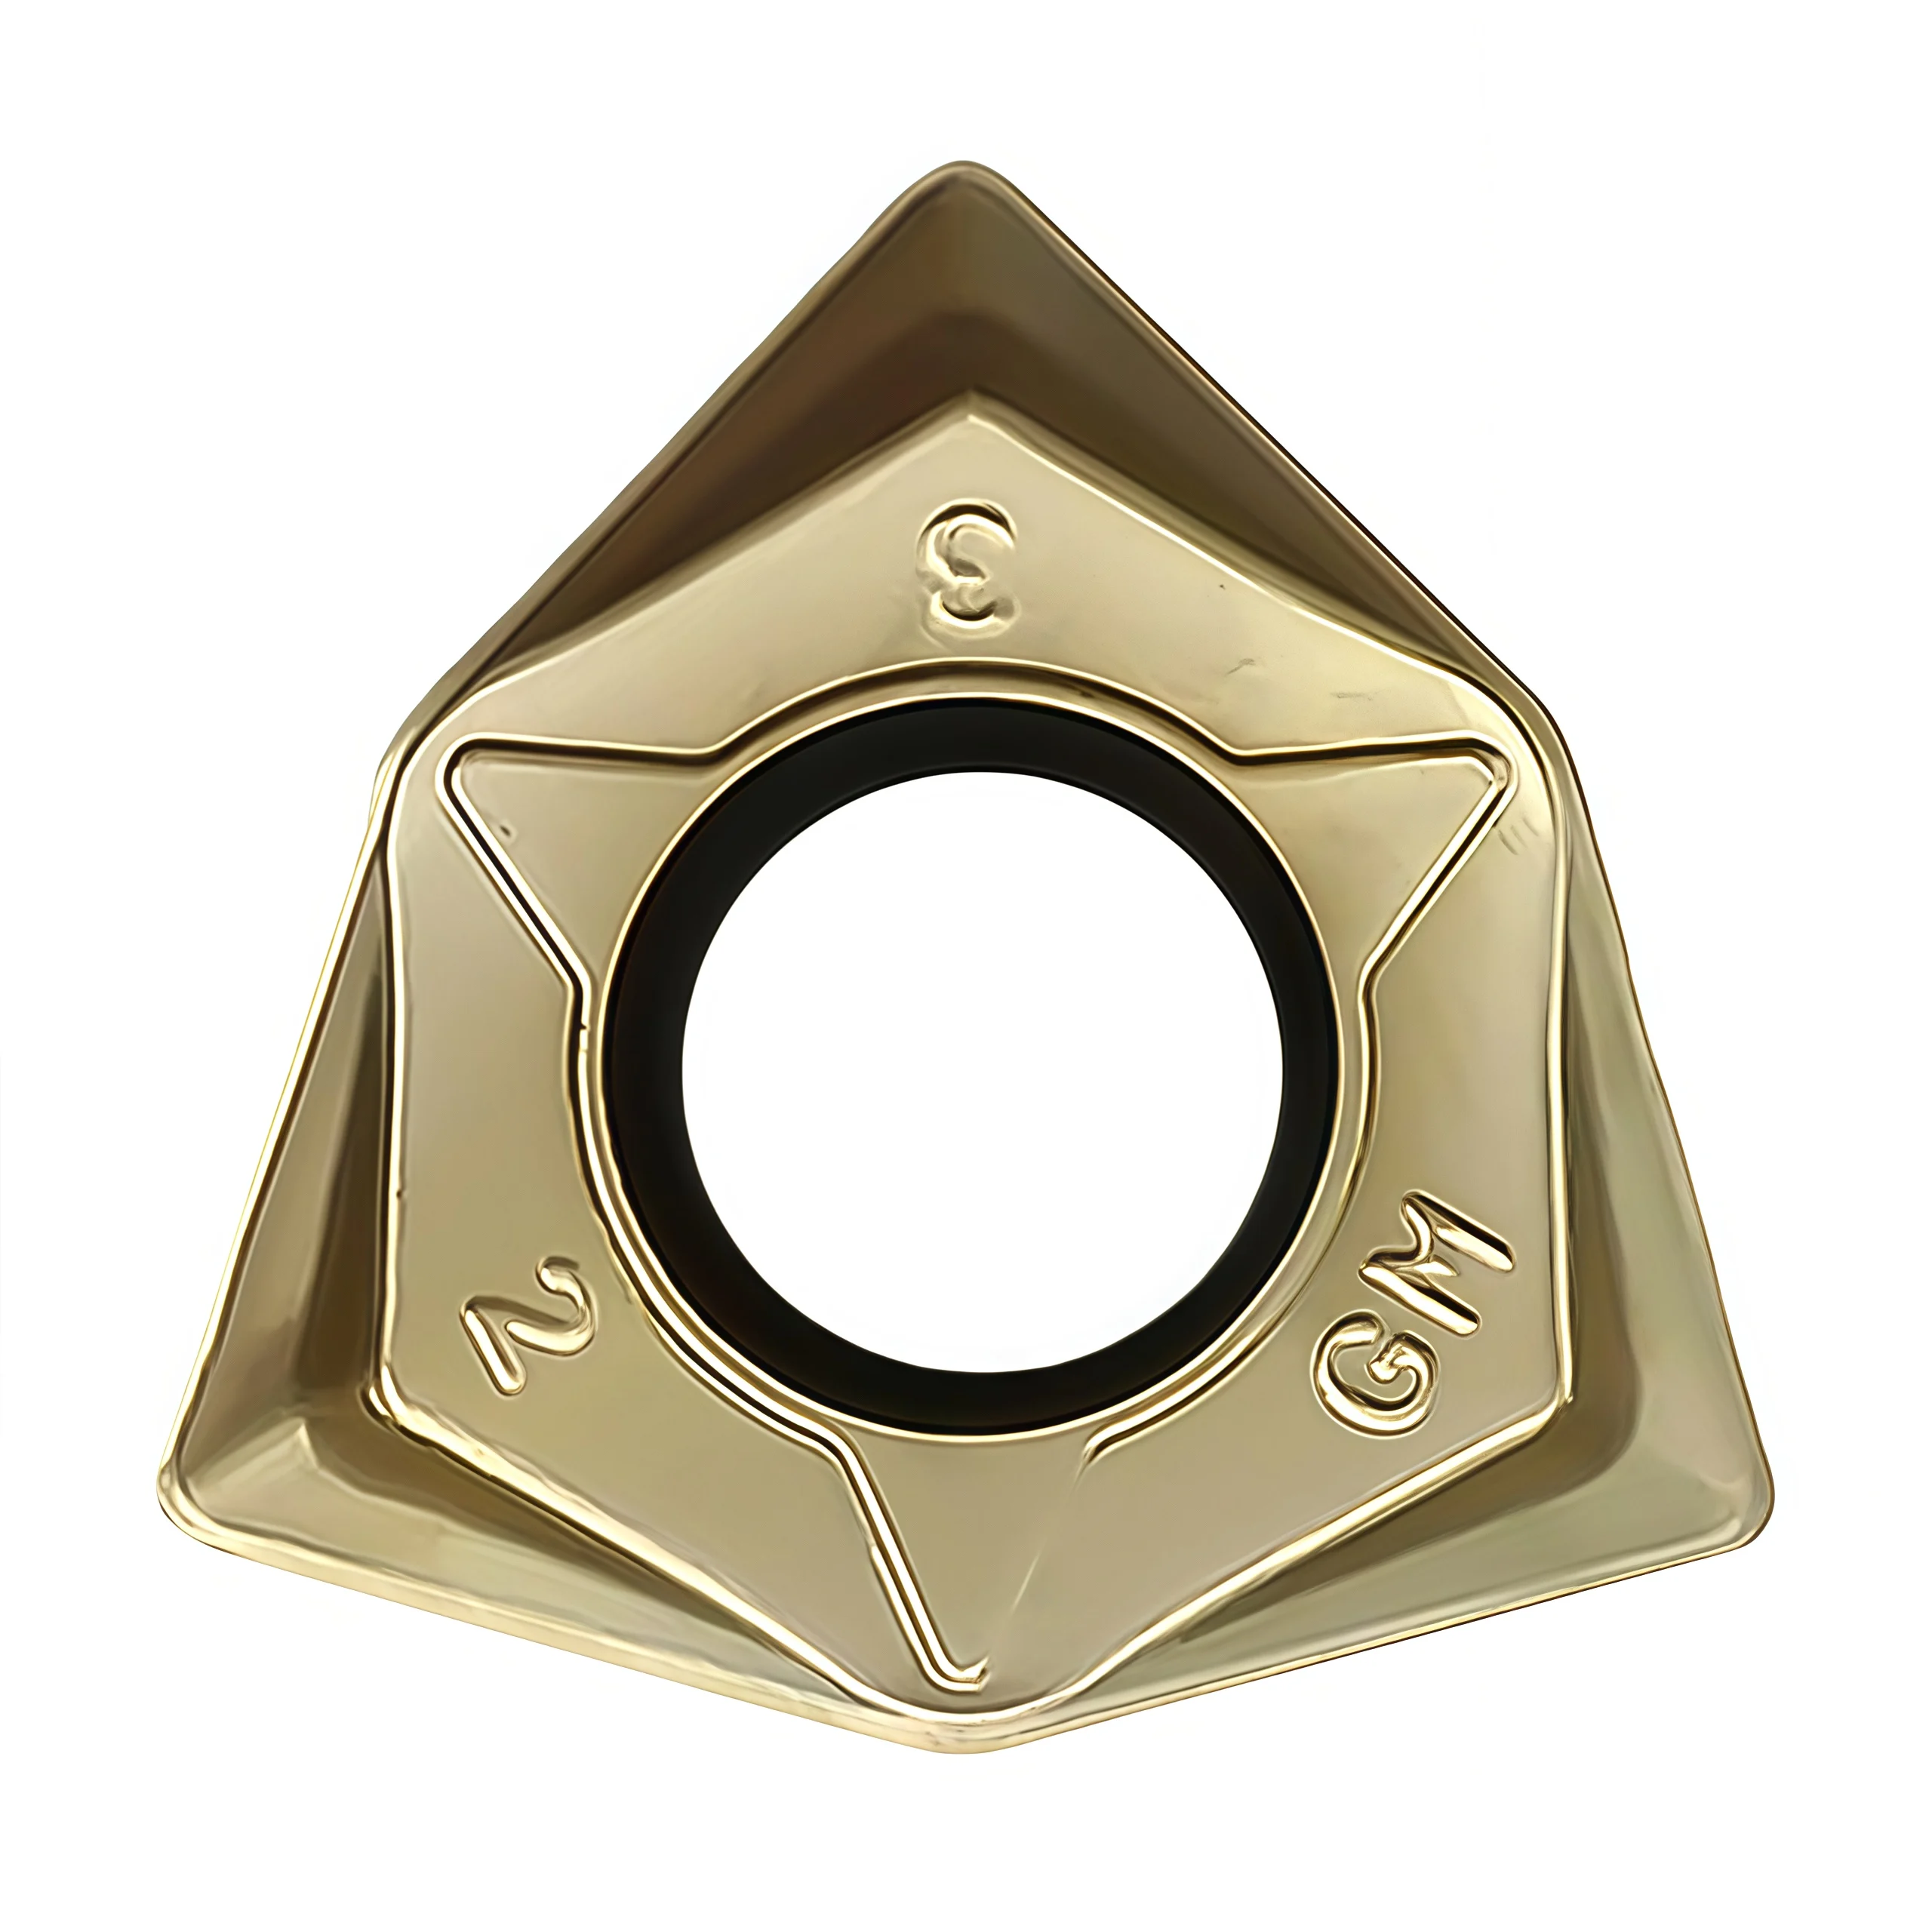
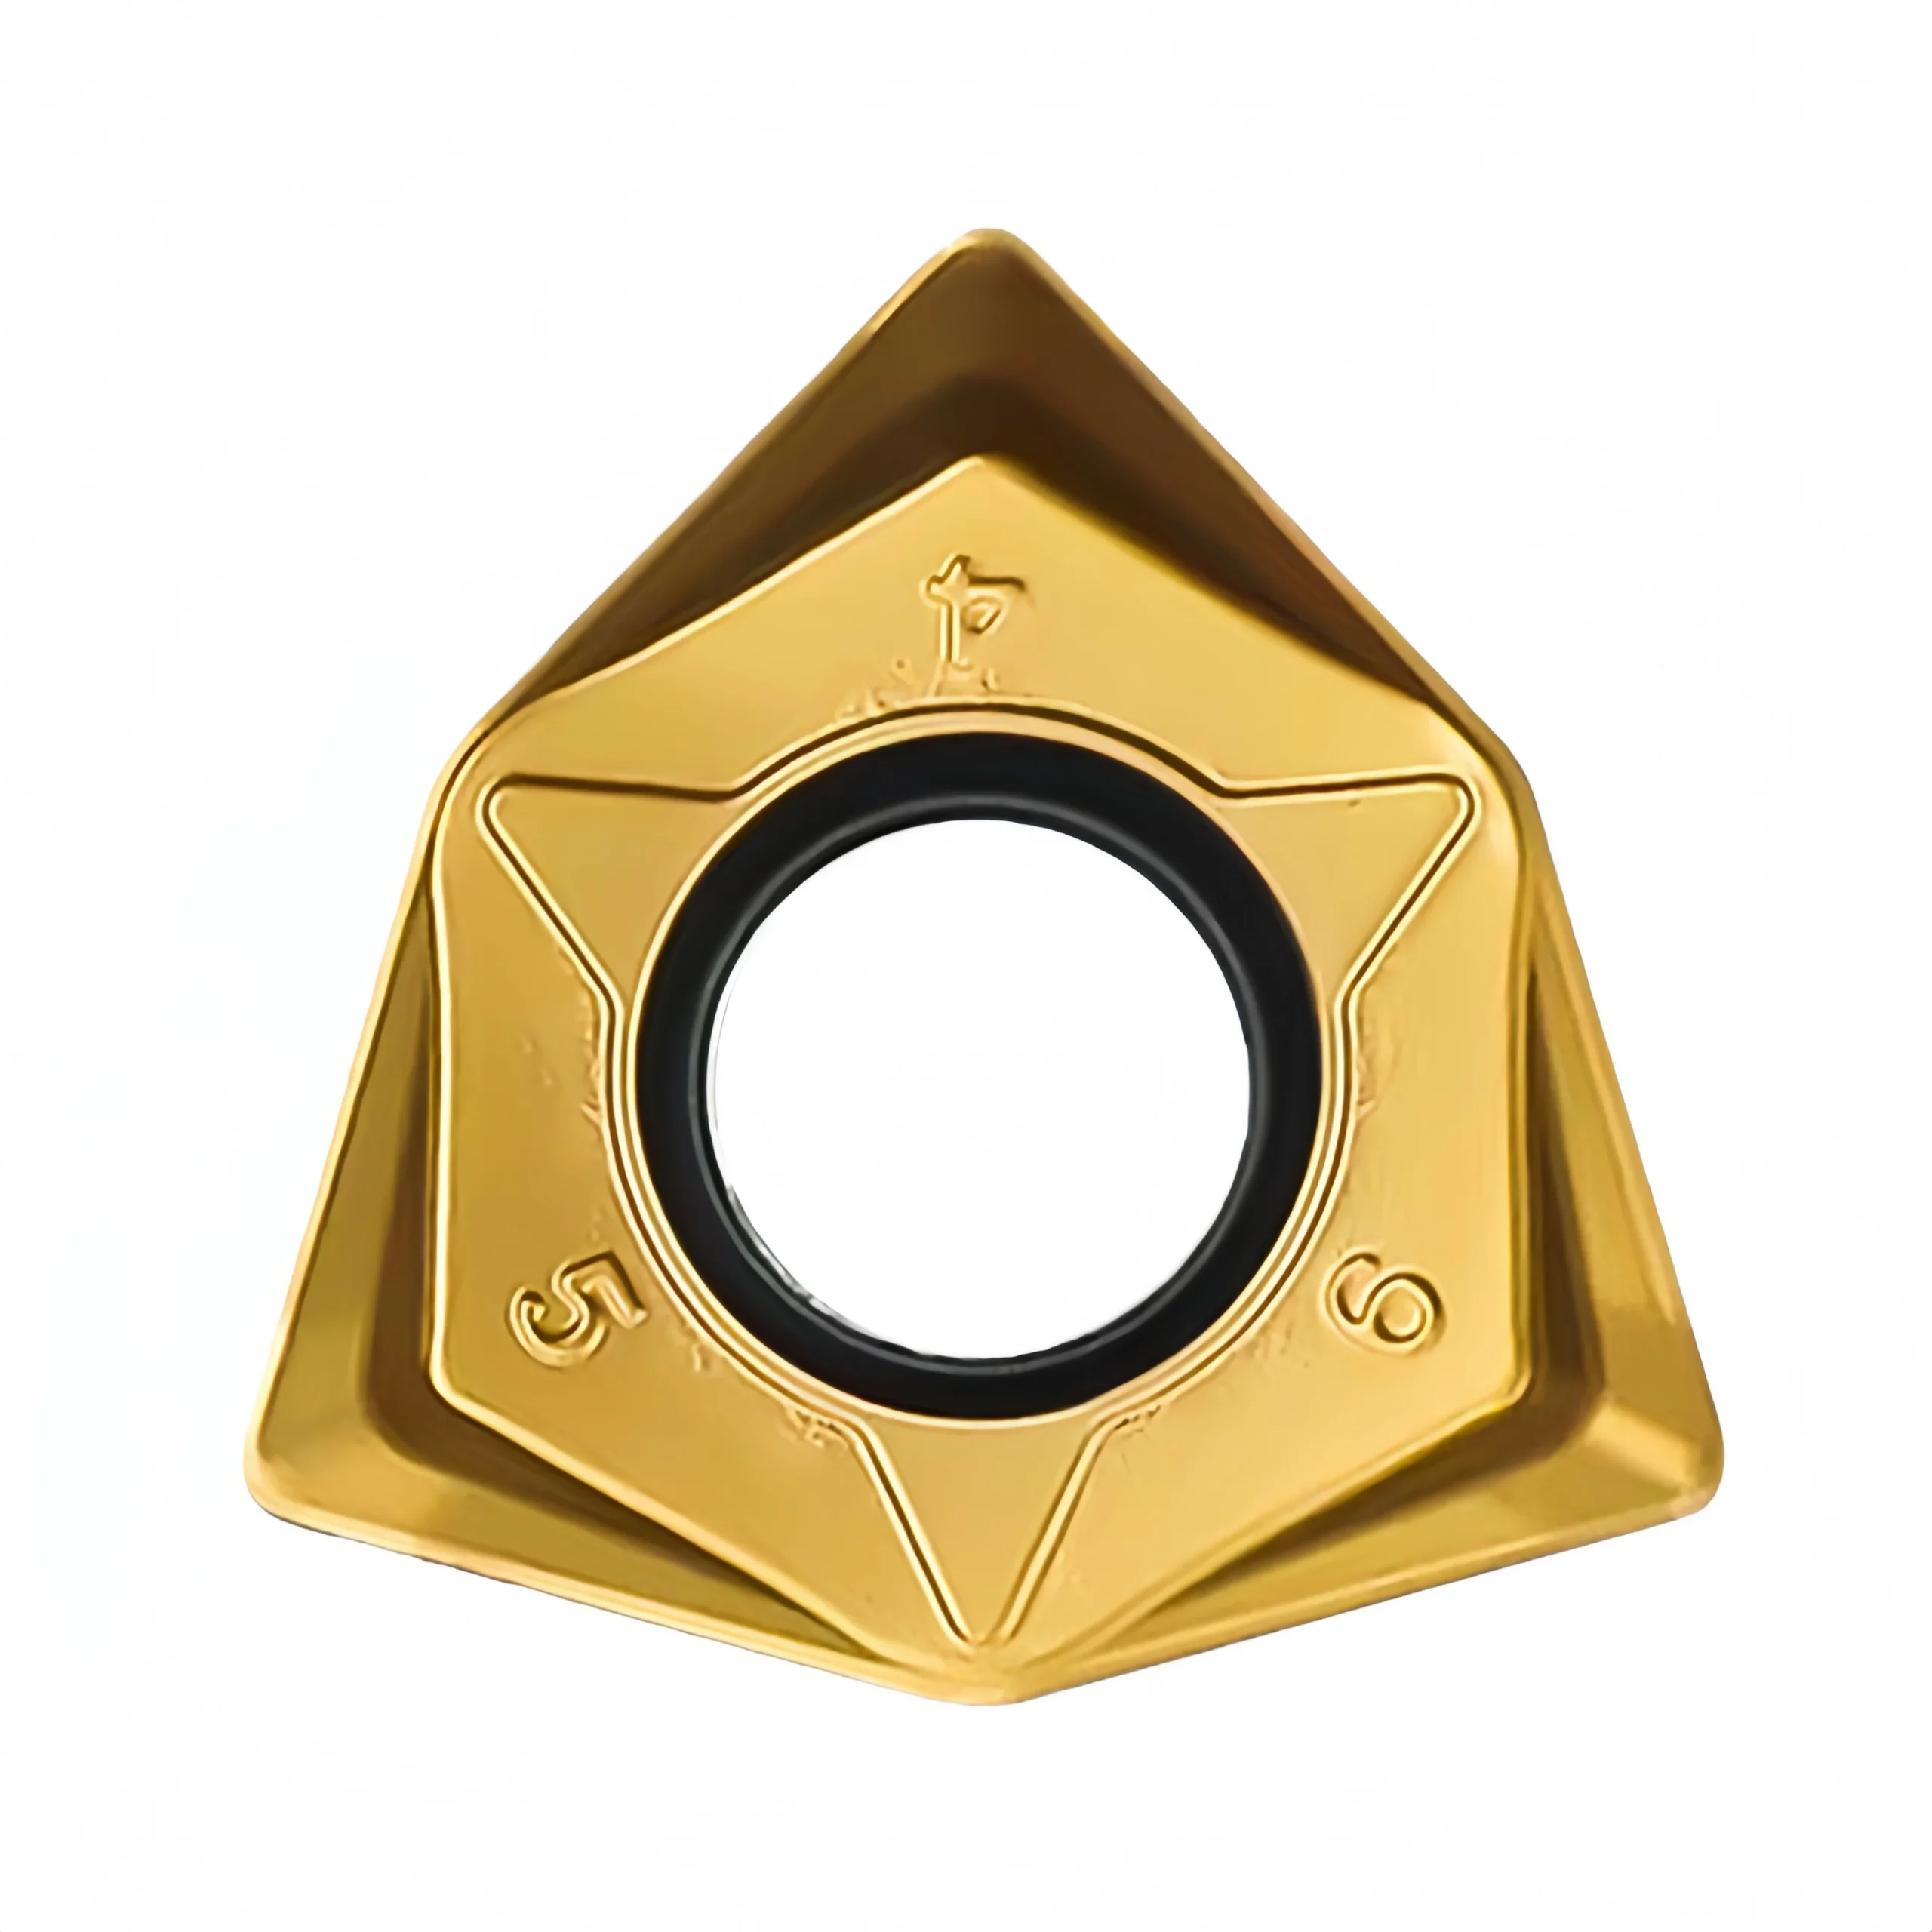
◆Machining Video
Machining demonstration; confirm the actual insert, cutter, workpiece and cutting parameters separately.
◆Specifications & Series
Three WNMU sizes are named in the supplied product description. No dimensioned drawing, complete grade codes or cutting data were provided for this exact HY series. The table distinguishes the listed models and the information needed to specify each one; do not treat the numeric code alone as a verified dimensional chart.
| Model Listed | Nominal Family | Confirm Before Ordering |
|---|---|---|
| WNMU 040304 | WNMU 04 | Full suffix, insert dimensions, corner geometry, grade and approved 04-size cutter pocket. |
| WNMU 060408 | WNMU 06 | Full suffix, insert dimensions, corner geometry, grade and approved 06-size cutter pocket. |
| WNMU 080608EN | WNMU 08, EN suffix | Complete geometry suffix, insert dimensions, grade and approved 08-size cutter pocket. |
◆Configuration to Confirm
| Selection Field | What to Confirm |
|---|---|
| Cutting system | Nominal 90° shoulder cutter; verify actual lead angle, tool overhang, seating and maximum axial depth with the cutter drawing. |
| Insert grade & coating | Carbide; verify substrate, PVD/CVD or other coating, chipbreaker and edge preparation by full SKU. |
| Workpiece group | Steel (ISO P), stainless steel (ISO M), cast iron (ISO K) or another material only with an approved grade and geometry. |
| Operation | Shoulder or side milling; check pocketing, slotting, ramping and entry limits against the complete cutter specification. |
| Wall & floor | Confirm corner geometry, tool deflection, step-down overlap and finish allowance for the required shoulder tolerance. |
◆How to Select the Insert
◆Starting Cutting Data
Select cutting speed (Vc), feed per tooth (fz), axial depth (ap) and radial engagement (ae) using the complete insert grade and shoulder-cutter recommendations. The original description provides no validated numerical range. A 90° shoulder cutter should not automatically use the chip-thinning feed multiplier of a low-entering-angle high-feed cutter.
◆Related Guide & Ordering
Read our Carbide Insert Types Guide for a family overview. Send the full WNMU and cutter-body codes to request the exact drawing, grade options and cutting data.
◆Carbide Insert Customization & OEM
Specify the insert around the machining operation, workpiece and holder. We can review standard replacements, application-specific geometry and private-label requirements using your insert designation, drawing or sample. Available grades, coatings, dimensions and order quantities are confirmed for each requested series.
Geometry & Chip Control
Review chipbreaker, rake, cutting-edge preparation, nose radius and corner design for the operation and workpiece. Confirm holder compatibility before approving a modified geometry.
Substrate & Coating
Select an available carbide grade and coating for the workpiece material, cutting conditions and desired balance of wear resistance and edge toughness.
Dimensions & OEM
Review insert size, thickness, locating and clamping features, tolerances, laser marking and private-label packaging against the approved specification.
◆Opzioni di personalizzazione
Use the fields below when sending an inquiry. The exact options depend on the insert family and are confirmed in the quotation or approved drawing.
| Specifiche | Details to Confirm |
|---|---|
| Insert Type | Turning, milling, threading, grooving or drilling insert; send the designation or drawing. |
| Size & Fit | Shape, size, thickness, inscribed circle or edge length, hole or clamping form, and holder model. |
| Geometria di taglio | Chipbreaker, nose or corner radius, edge preparation, cutting direction and application-specific profile. |
| Grade & Coating | Workpiece group and grade, carbide substrate, coating system and wet or dry cutting conditions. |
| Tolerance & Inspection | Critical dimensions, profile requirements, inspection method and any required report. |
| OEM Presentation | Insert or box marking, label content, packaging format and quantity per pack. |
◆How to Request a Custom Insert

Send your insert requirements through our contact form or review our OEM and private-label service.
◆Carbide Insert Quality Control

Insert quality depends on the approved grade, geometry, coating and dimensional specification. We review the requirements at order confirmation and align the inspection scope with the insert series and any customer drawing. Share critical dimensions or documentation needs before production so they can be included in the agreed inspection plan.
01 · Incoming Material
Confirm the specified carbide grade or material documentation against the order requirements.
02 · In-Process Checks
Review dimensions and cutting-edge features during production against the approved specification.
03 · Final Inspection
Check the agreed dimensions, appearance, edge condition, coating identification and marking as applicable.
04 · Packing Review
Verify the item code, quantity, labels and protective packing against the approved order.
◆Inspection & Documentation
Inspection points and acceptance criteria should be agreed for the ordered series. For custom inserts, the approved drawing takes priority over a generic catalogue description.
| Check Area | What to Confirm |
|---|---|
| Dimensions & Fit | Insert size, thickness, corner radius, clamping features and any drawing tolerances. |
| Geometria di taglio | Chipbreaker, edge preparation, usable corners and profile where applicable. |
| Grade & Coating | Approved grade and coating designation; any requested verification method. |
| Appearance & Packing | Visible edge damage, marking, item code, count and packing format. |
| Requested Records | Inspection report, material or coating documentation, sample approval or batch identification when agreed. |
◆Order & Delivery
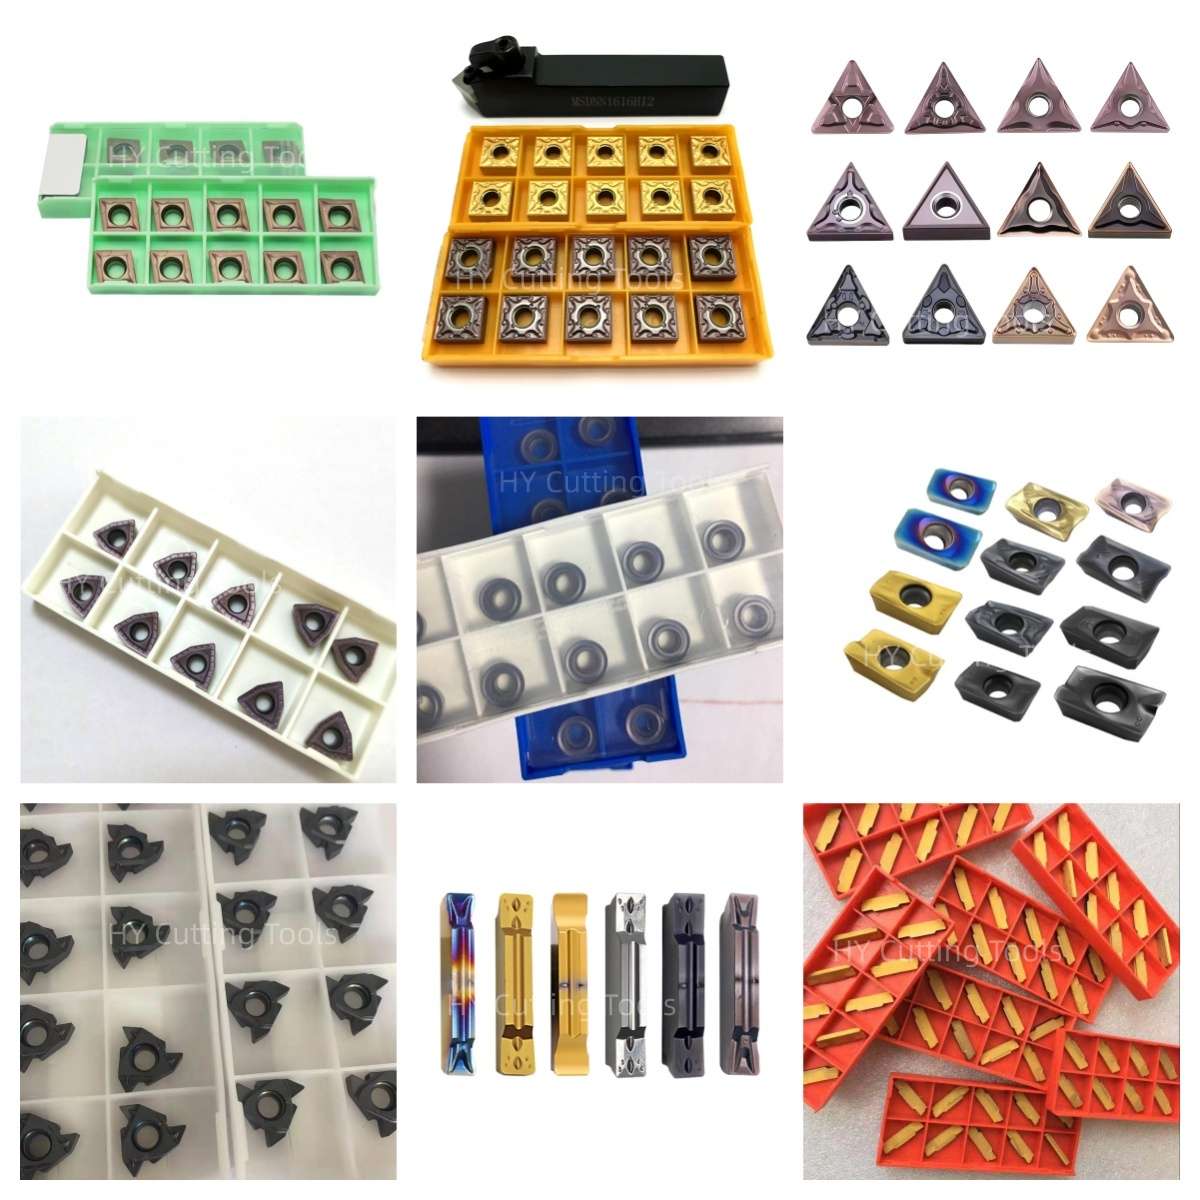

Share a line-by-line list of insert codes and quantities for a mixed-size quotation. Stock status, minimum quantity, sample requirements and production lead time are confirmed for each grade, coating and configuration.
Send your item list and quality requirements through our contact form for specification, availability and delivery confirmation.
◆Product FAQs
Are these 90° shoulder inserts also high-feed inserts?
This product title specifies 90° shoulder milling. Small-entering-angle high-feed milling relies on a different chip-thinning relationship and often uses shallower axial cuts. Choose speeds, feeds and depths from the exact WNMU insert and shoulder-cutter data rather than applying another high-feed system's settings.
Can WNMU 040304, 060408 and 080608EN fit the same cutter?
They are different size families. Verify the complete code against the cutter body's approved insert list and compare the pocket, seating surfaces, screw, corner form and specified tightening torque. A shared WNMU prefix does not establish interchangeability.
Does a 90° cutter guarantee an exact square shoulder?
The nominal entering angle describes the cutter geometry. Wall squareness and floor finish also depend on insert corner design, cutter runout, deflection, depth of cut and the machining setup. Use a finishing pass and measure the part when tolerances are tight.
How deep can these inserts cut?
Maximum axial depth varies by insert size, edge geometry and cutter body. The supplied description contains no verified ap limit for these three HY models. Request the matching cutter drawing and application data before programming a deep pass.
Which grade suits steel, stainless steel or cast iron?
Provide the exact workpiece grade and hardness, operation, coolant and cut stability. The carbide grade, coating and chipbreaker should be selected for ISO P, M or K as applicable; the WNMU size code alone does not identify material suitability.
How many usable edges does a WNMU insert have?
Some manufacturer's double-sided WNMU shoulder systems offer six usable edges, but confirm the actual indexing geometry and edge count for the complete insert and cutter being ordered. The supplied HY description does not document one edge count across all three sizes.
◆Ordering & OEM FAQs
What should I send for an insert replacement?
Send the current manufacturer's complete insert code and grade, box-label and both-face photos, cutter-body code, workpiece, cutting conditions, observed wear and required quantity. Validate pocket fit and cutting results with a sample.
Can I combine WNMU 04, 06 and 08 in one order?
Send a line-by-line list with the full code, grade and quantity for each model. Mixed-size availability, pack count, minimum quantity and dispatch date are confirmed for each item.
Can I request a different coating or edge geometry?
Provide the existing code or drawing, target material, operation, cutter body and expected volume. Available substrate, coating and edge options are confirmed through the approved specification and quotation.
Are OEM marking and private-label boxes available?
Send your marking text, artwork, box-label format, pack quantity and order volume. Confirm the sample presentation and delivery terms before production.
◆Guides & Technical References
Use our CNC Insert Selection Guide e Carbide Insert Types Guide for initial insert selection.
For a model-specific drawing or quotation, send the full WNMU and cutter-body codes with the required quantity.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.