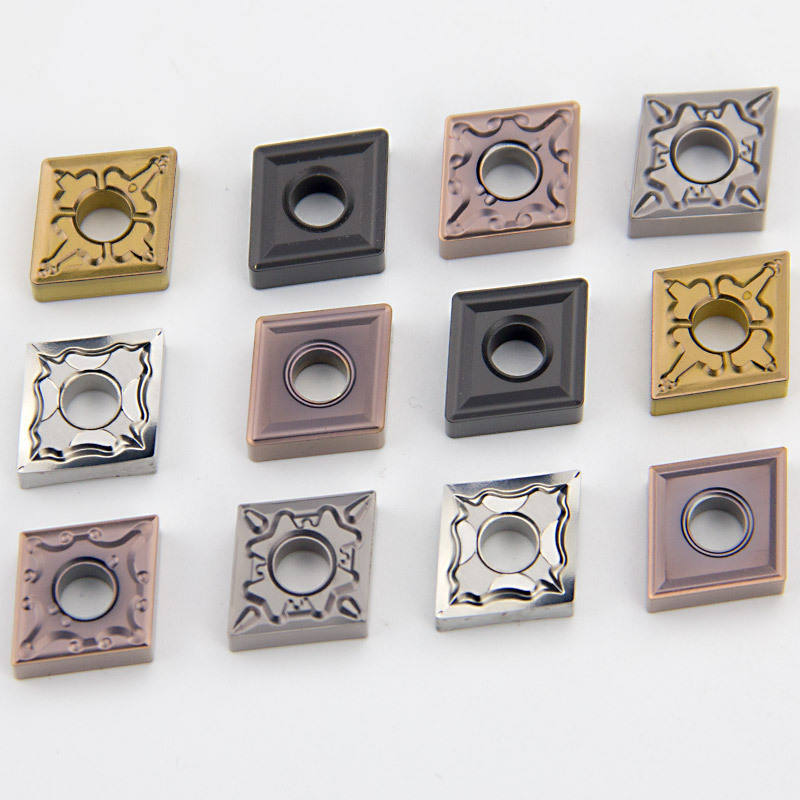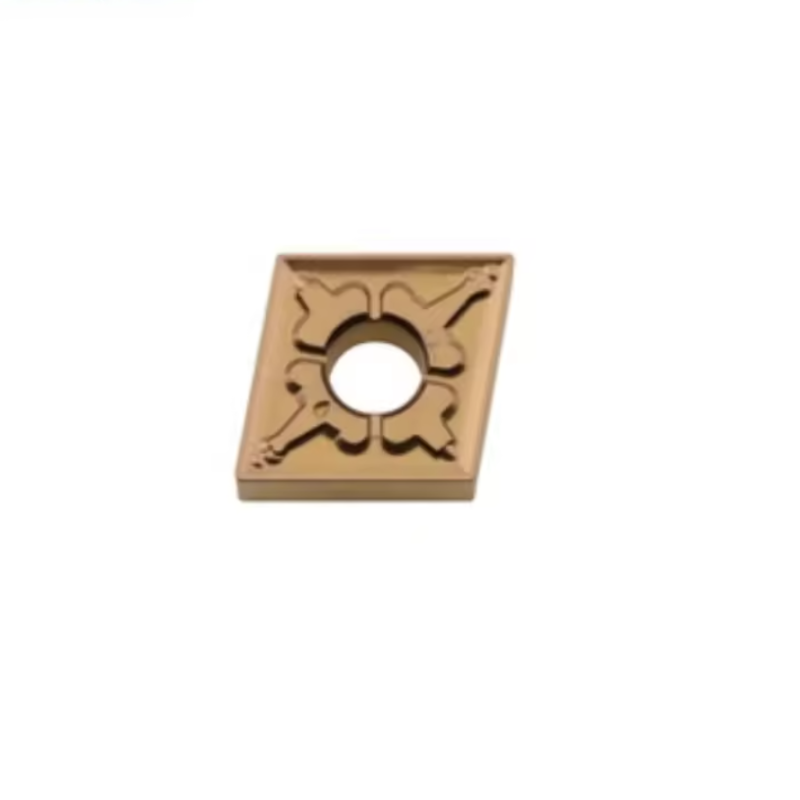

TNMG 160404/160408 R/L Cermet Turning Inserts for Steel Machining
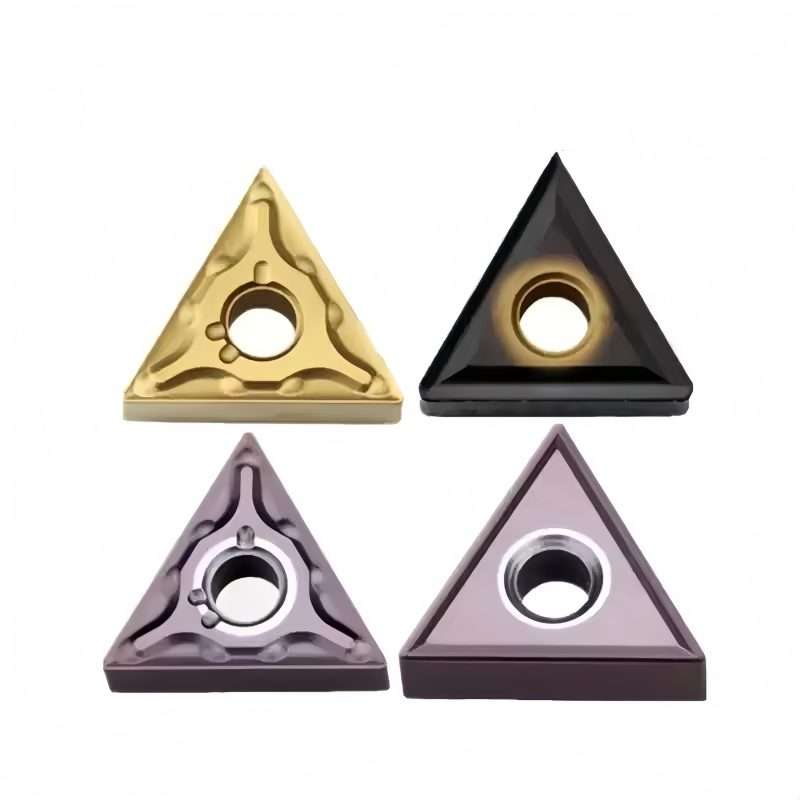
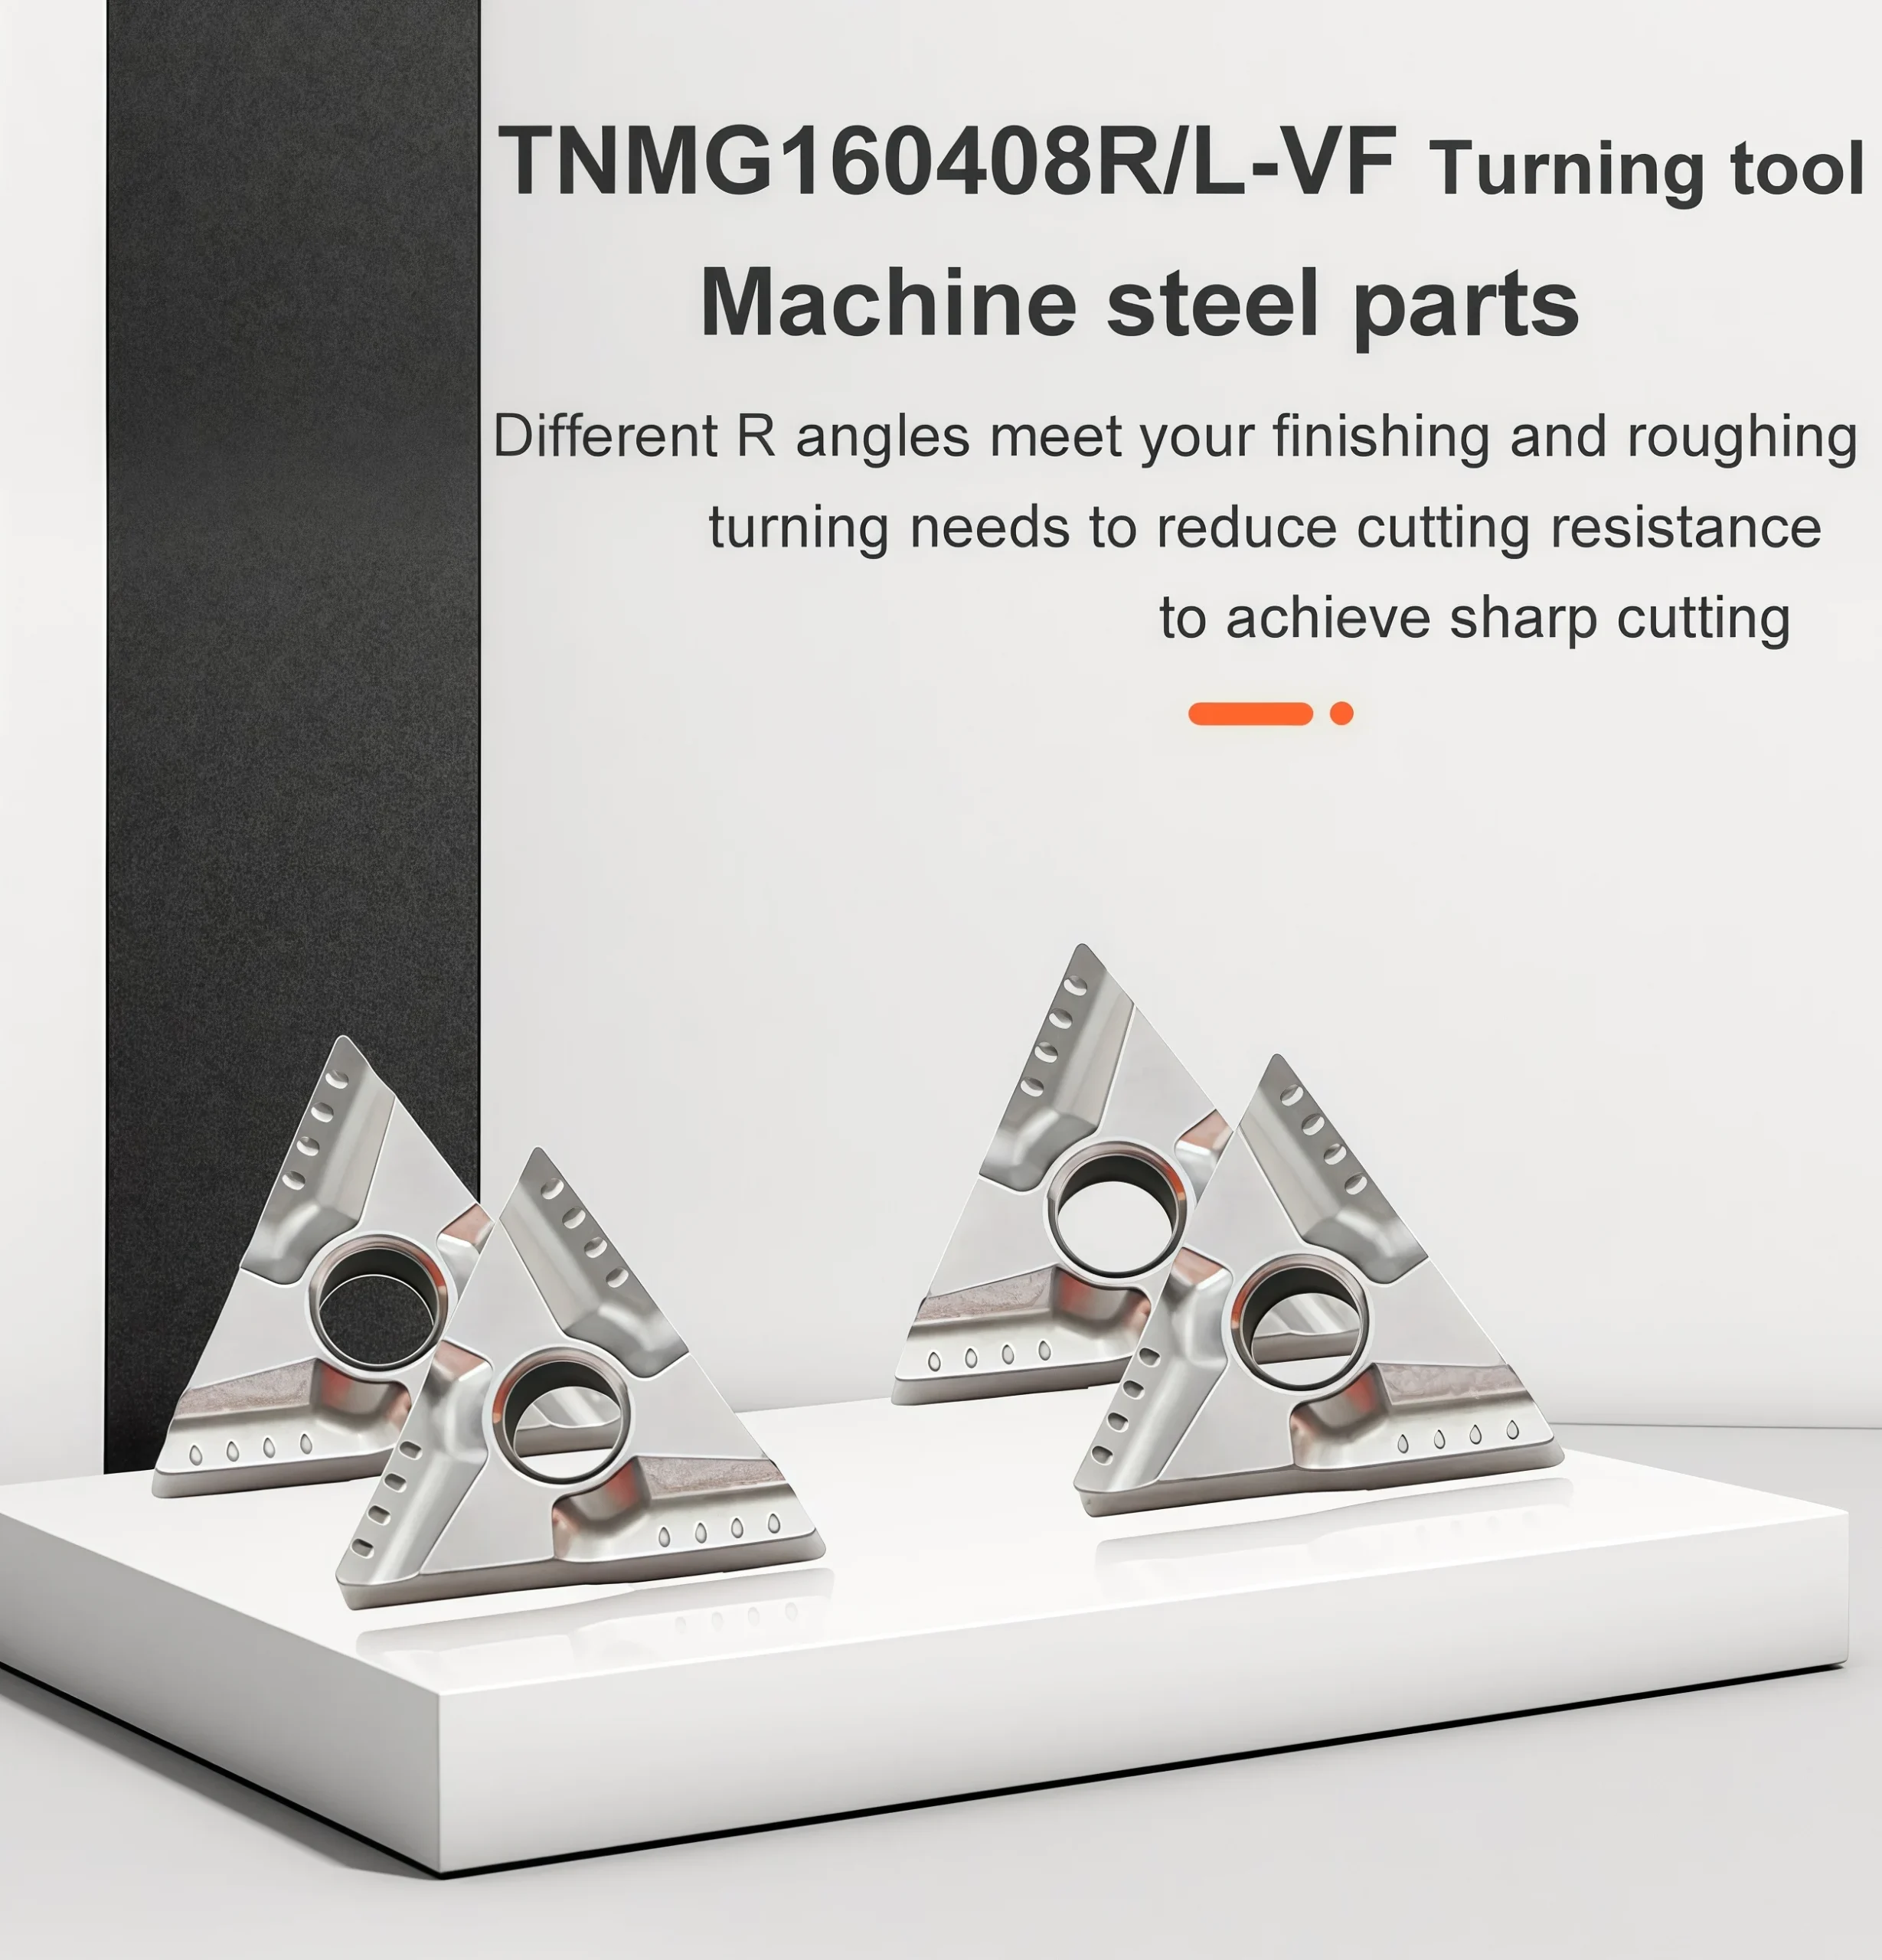
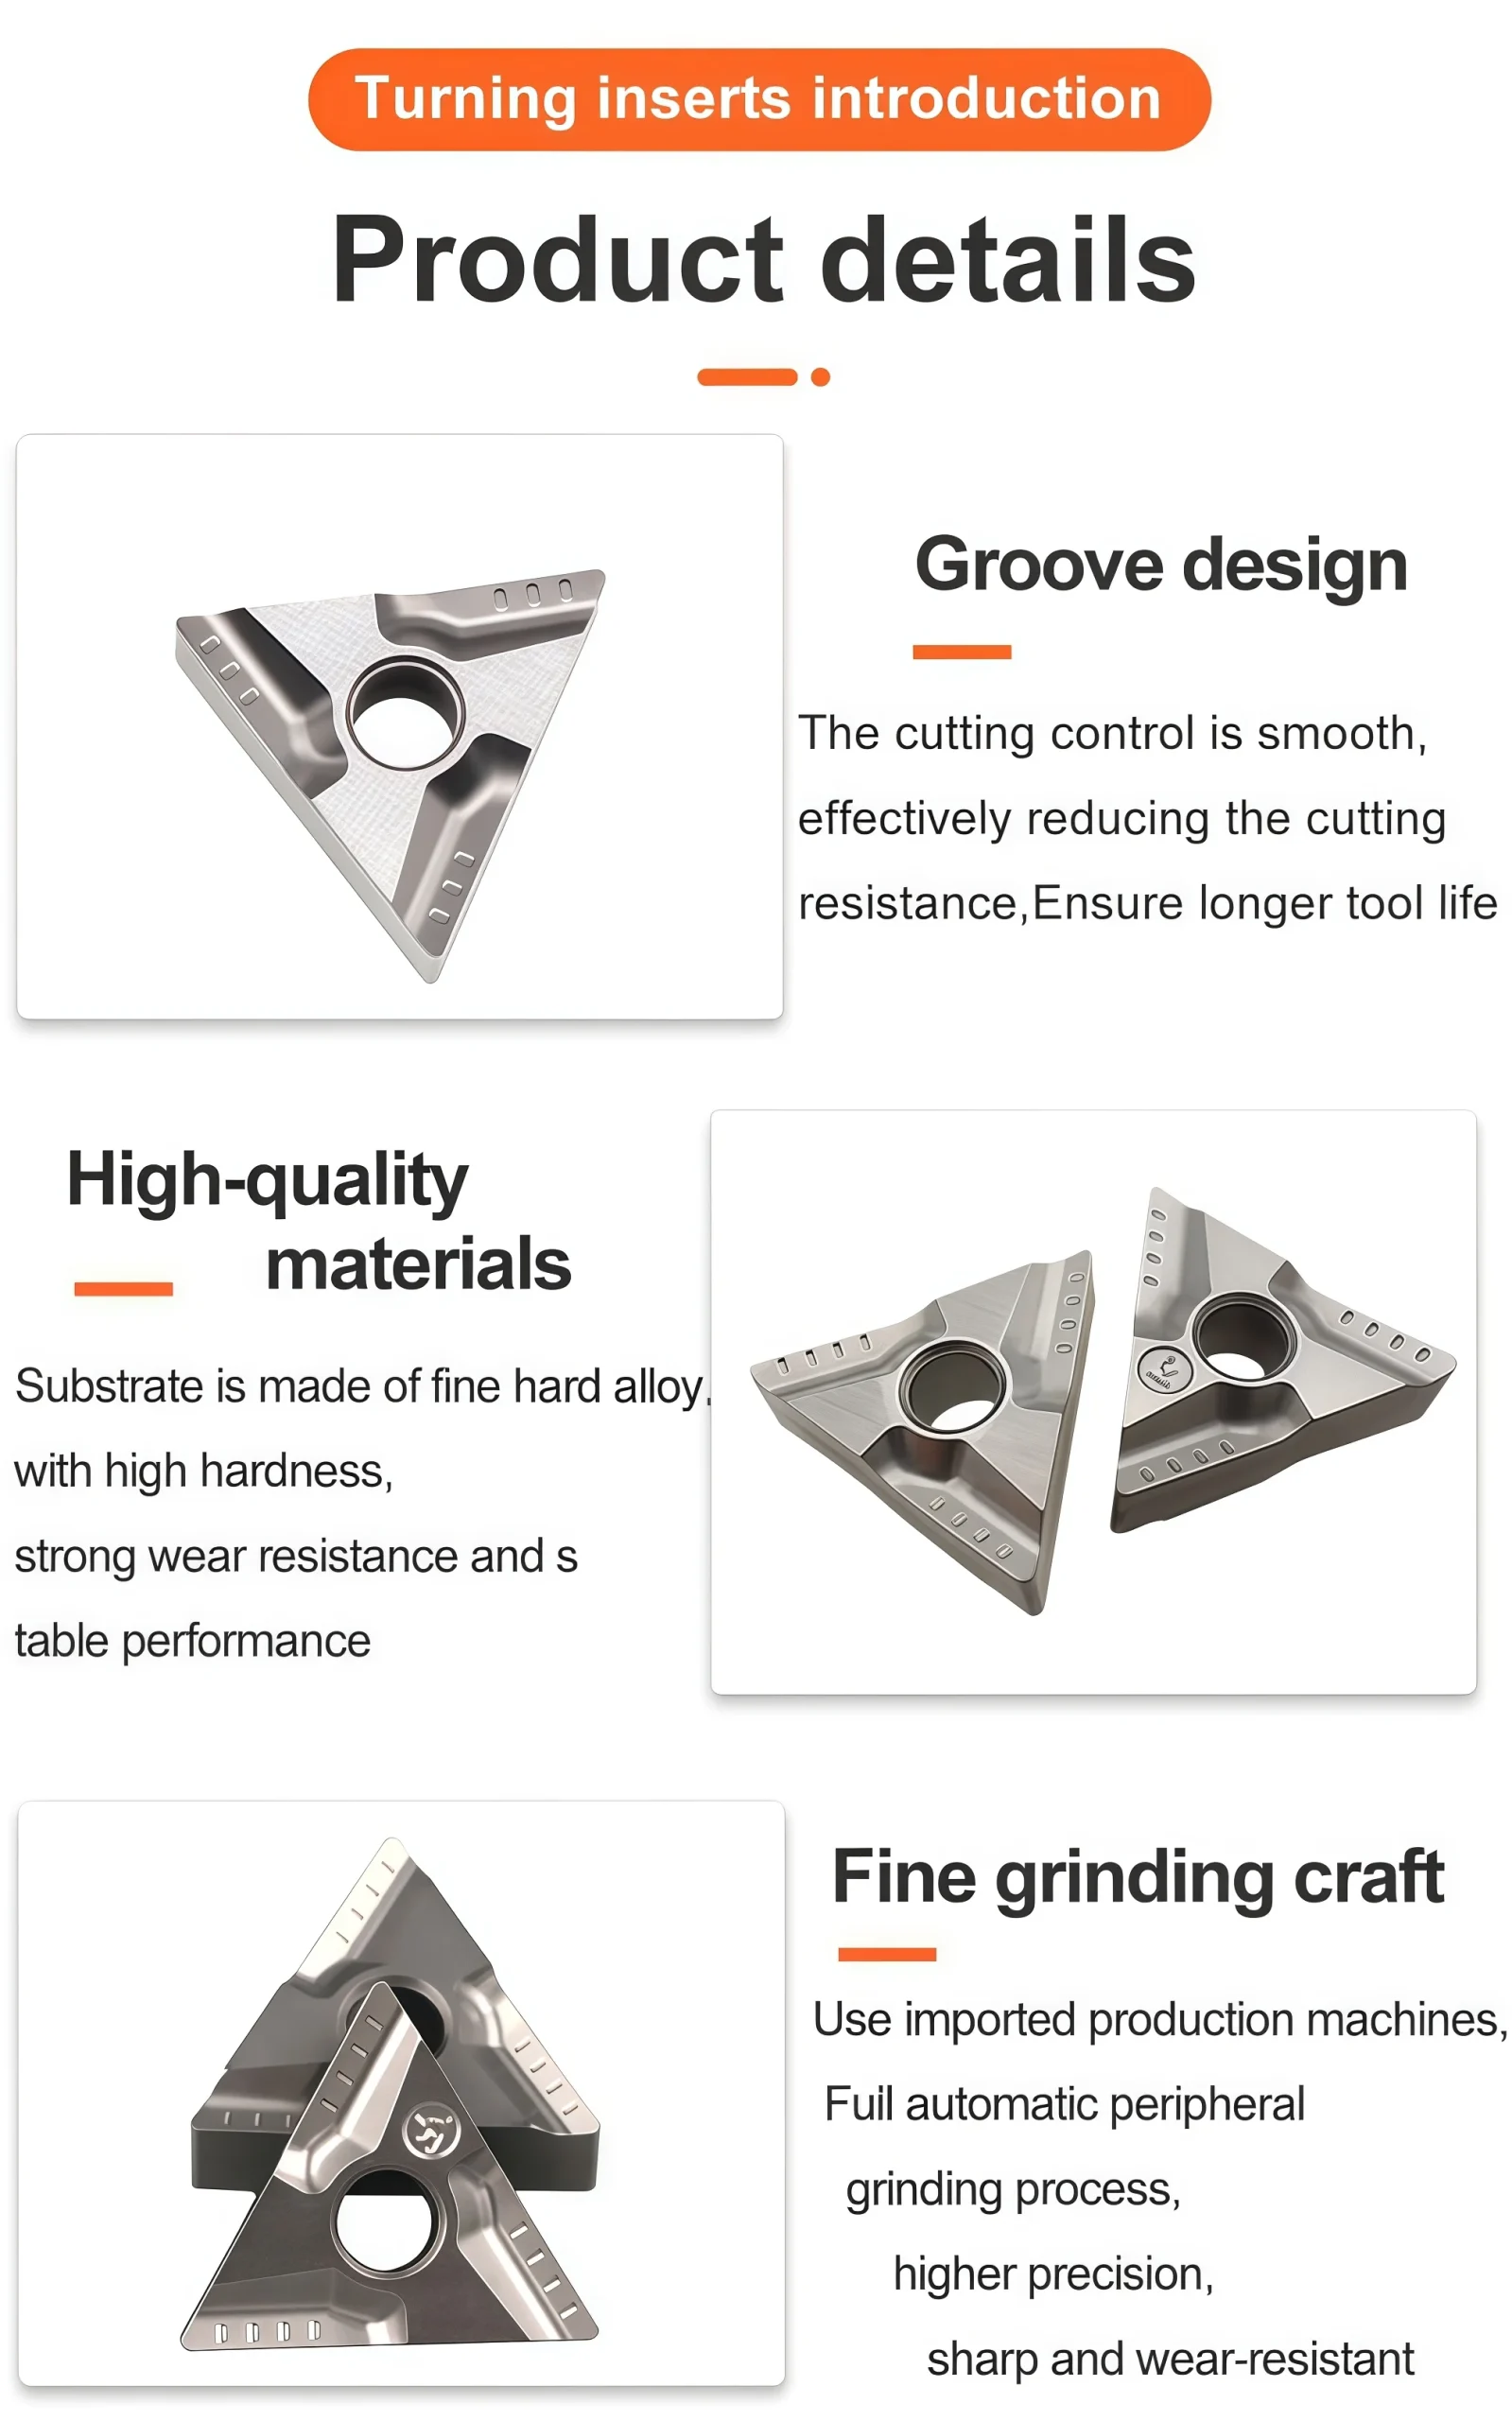
TNMG160404 and TNMG160408 R/L cermet inserts are designed for precision steel turning and profiling. Right- and left-hand geometries support different feed directions, while the cermet cutting material helps maintain consistent surface finishes in finishing and semi-finishing production.
Qualità costante
Consistent geometry across repeat orders.
Ordini flessibili
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
Standard e personalizzati
Standard sizes and custom configurations.
◆Panoramica del prodotto
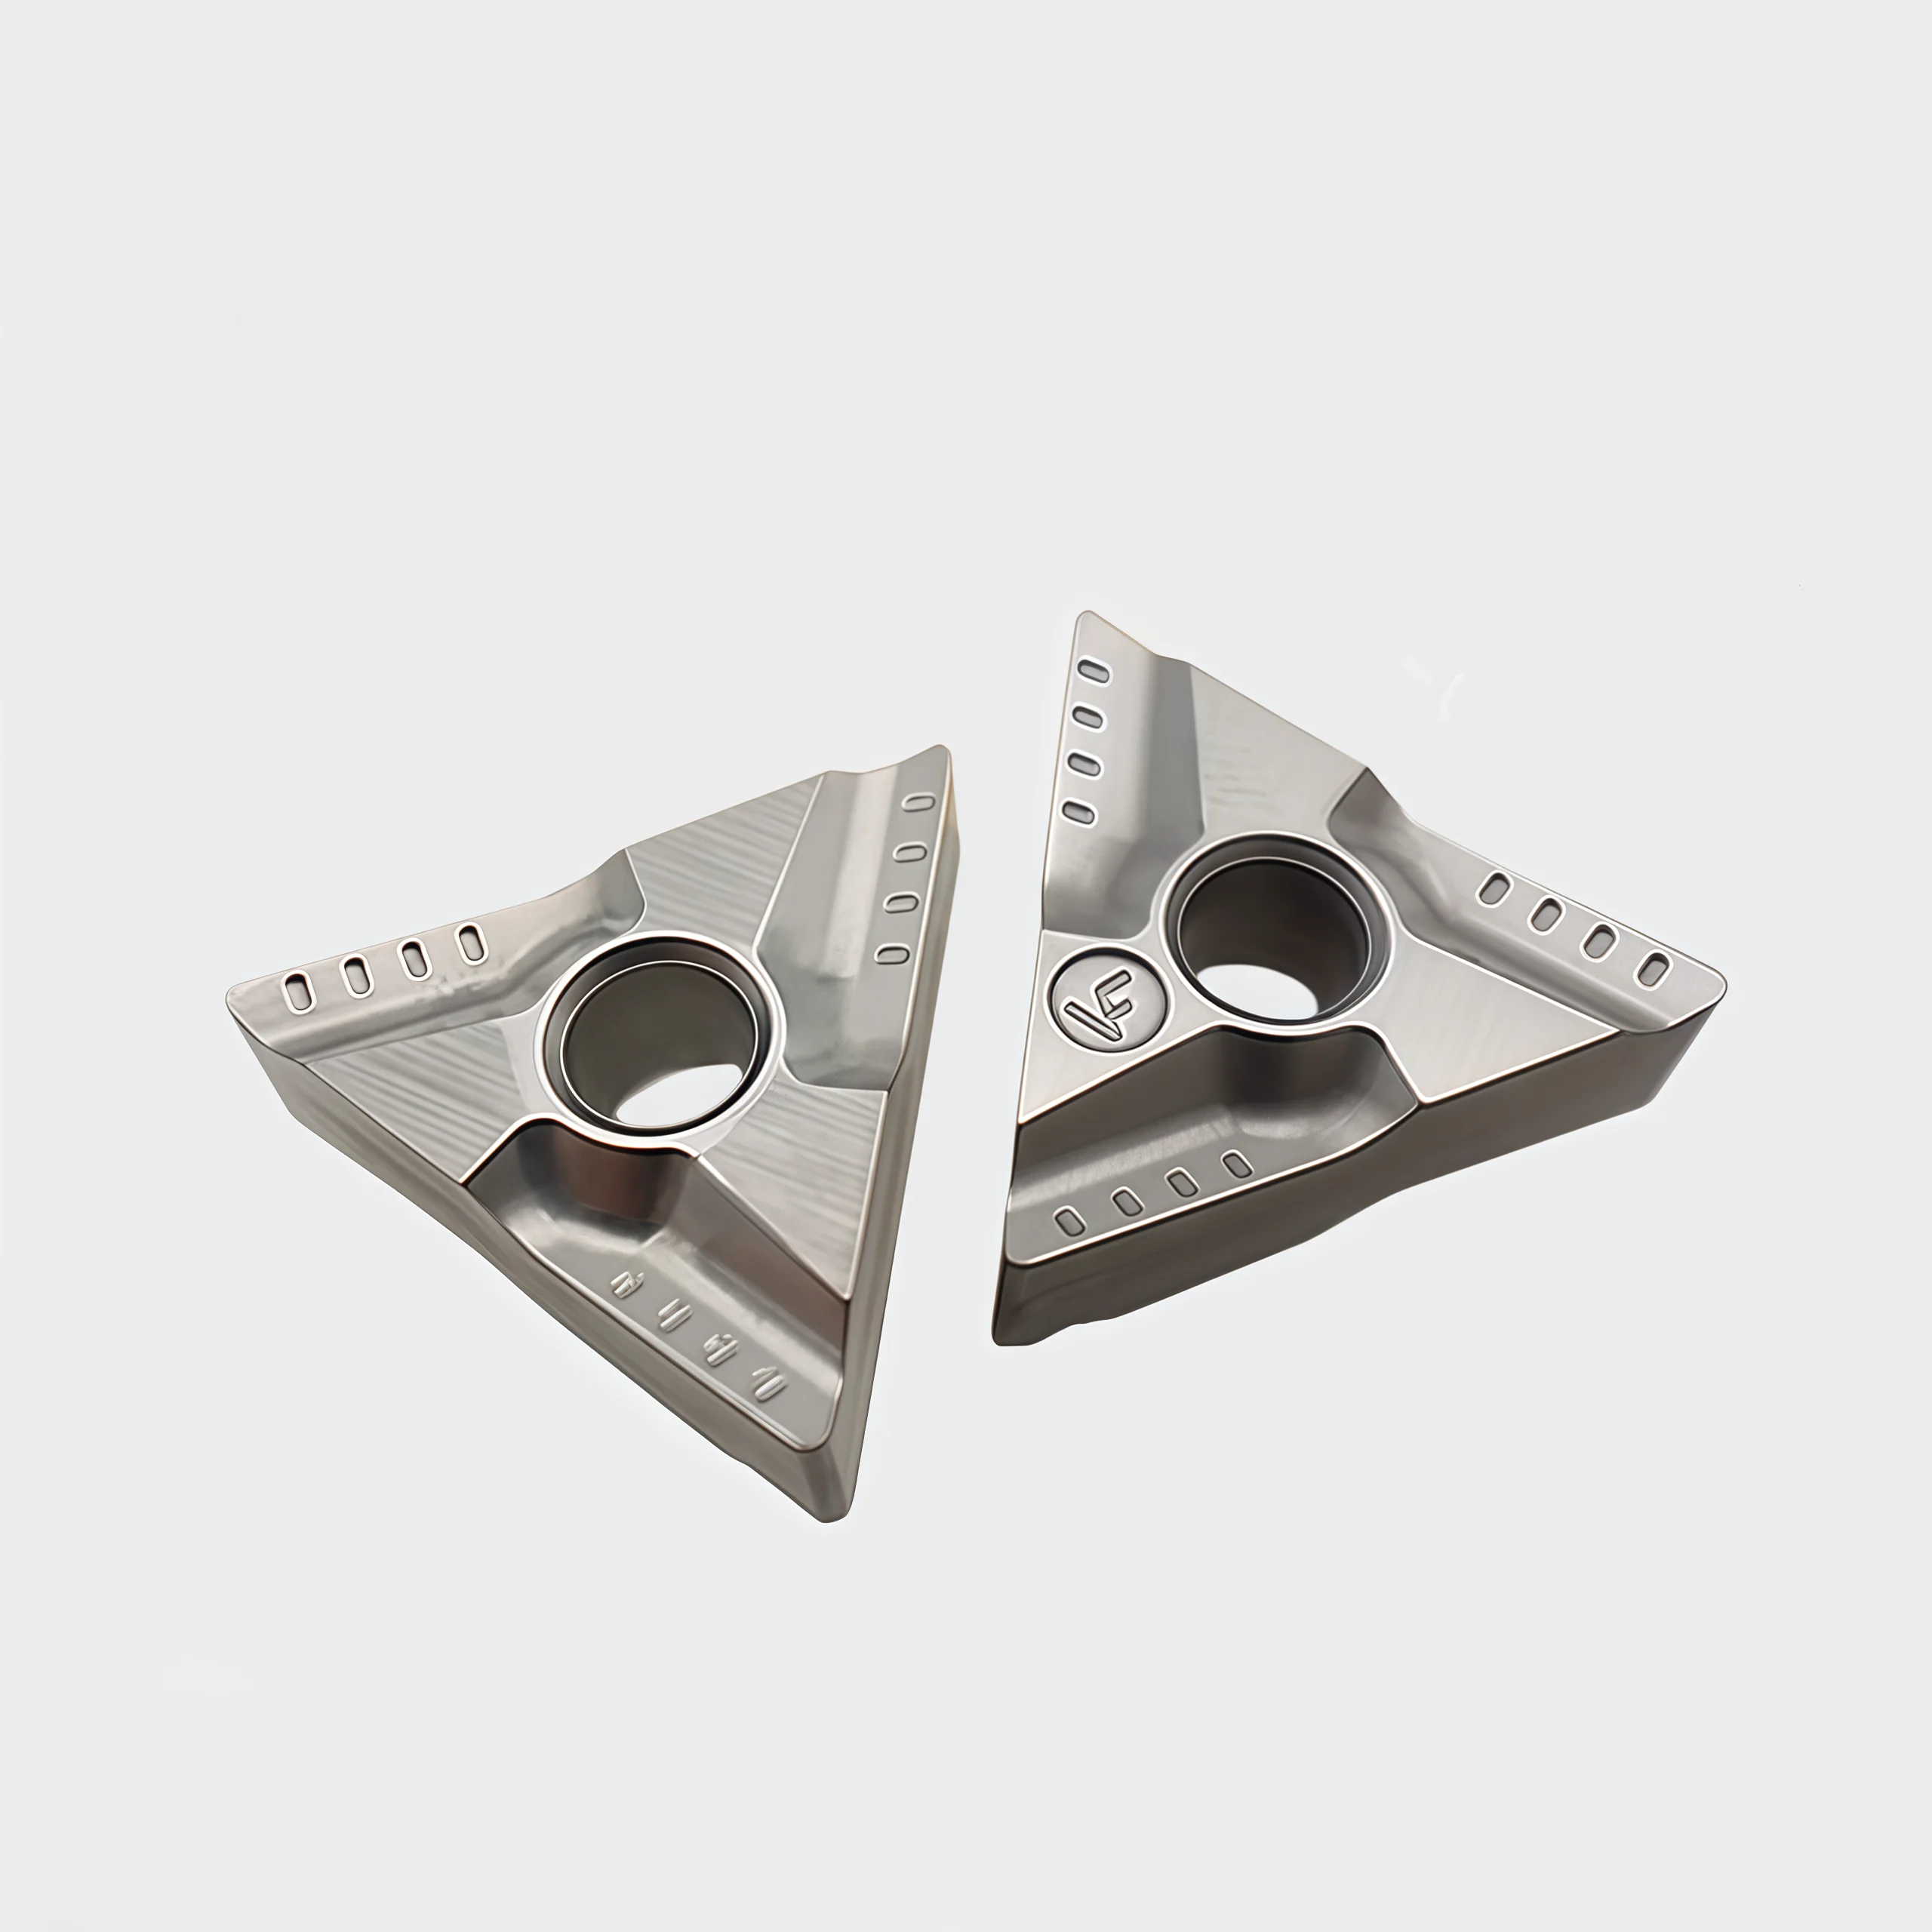
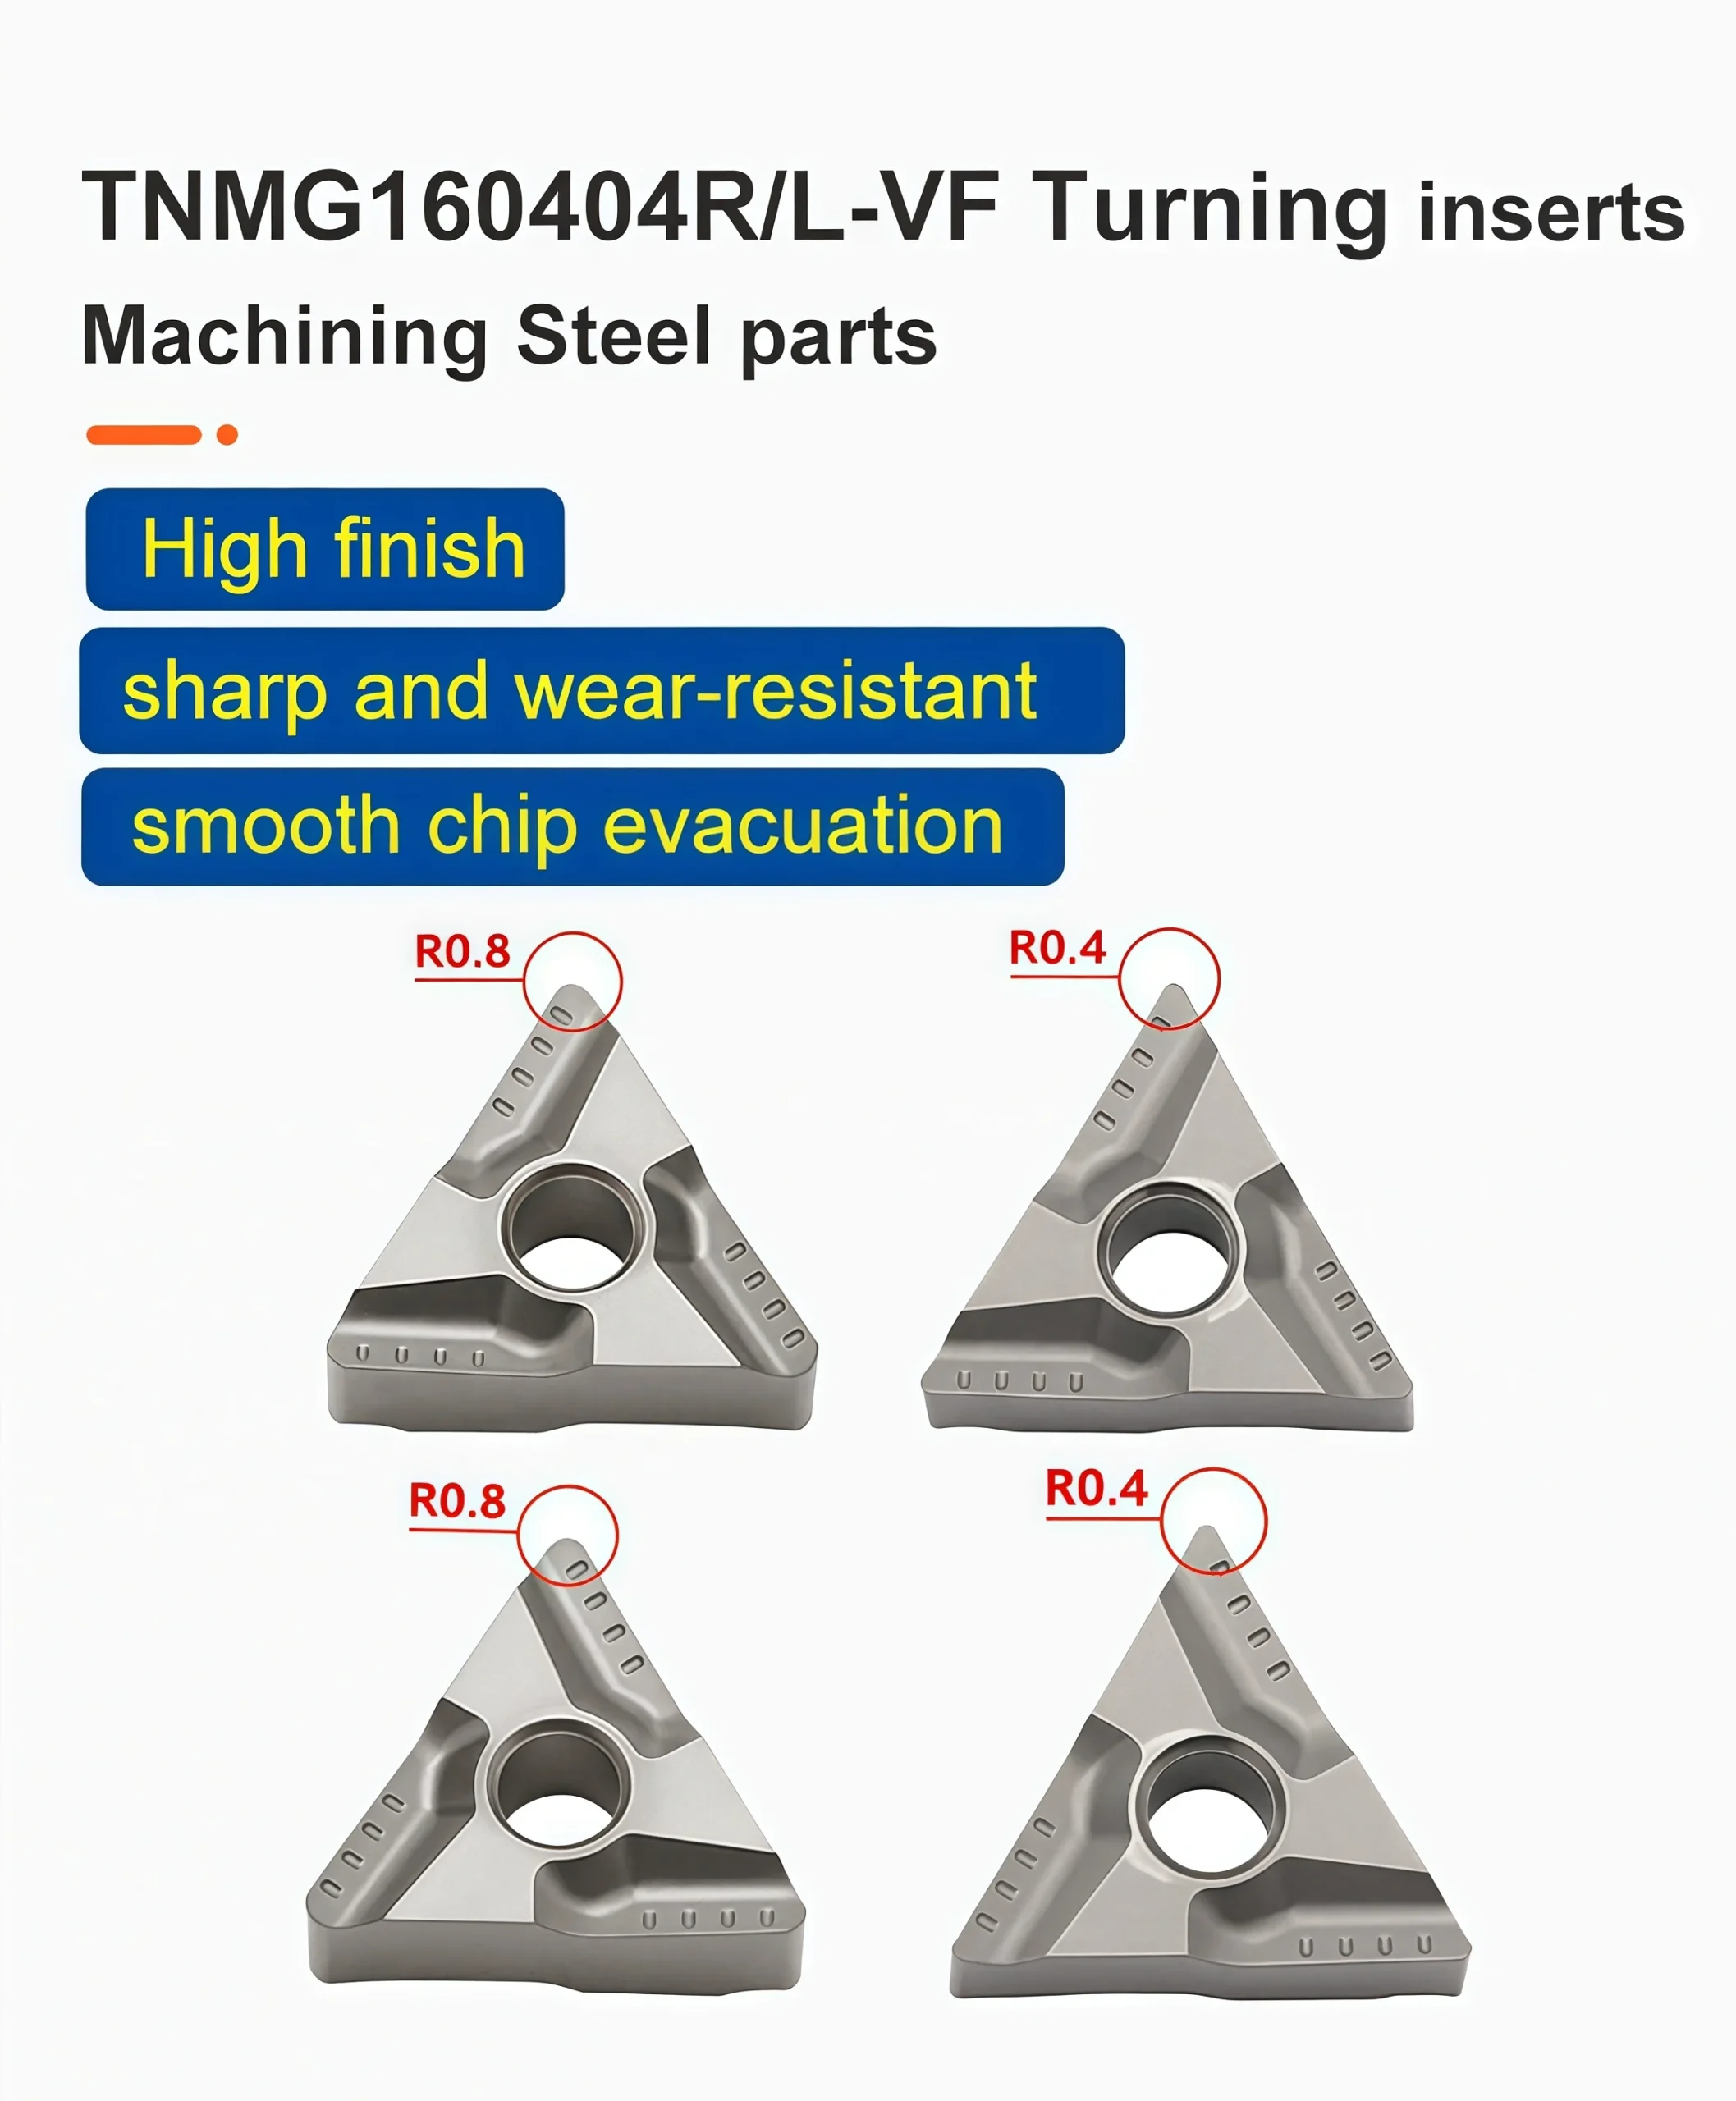
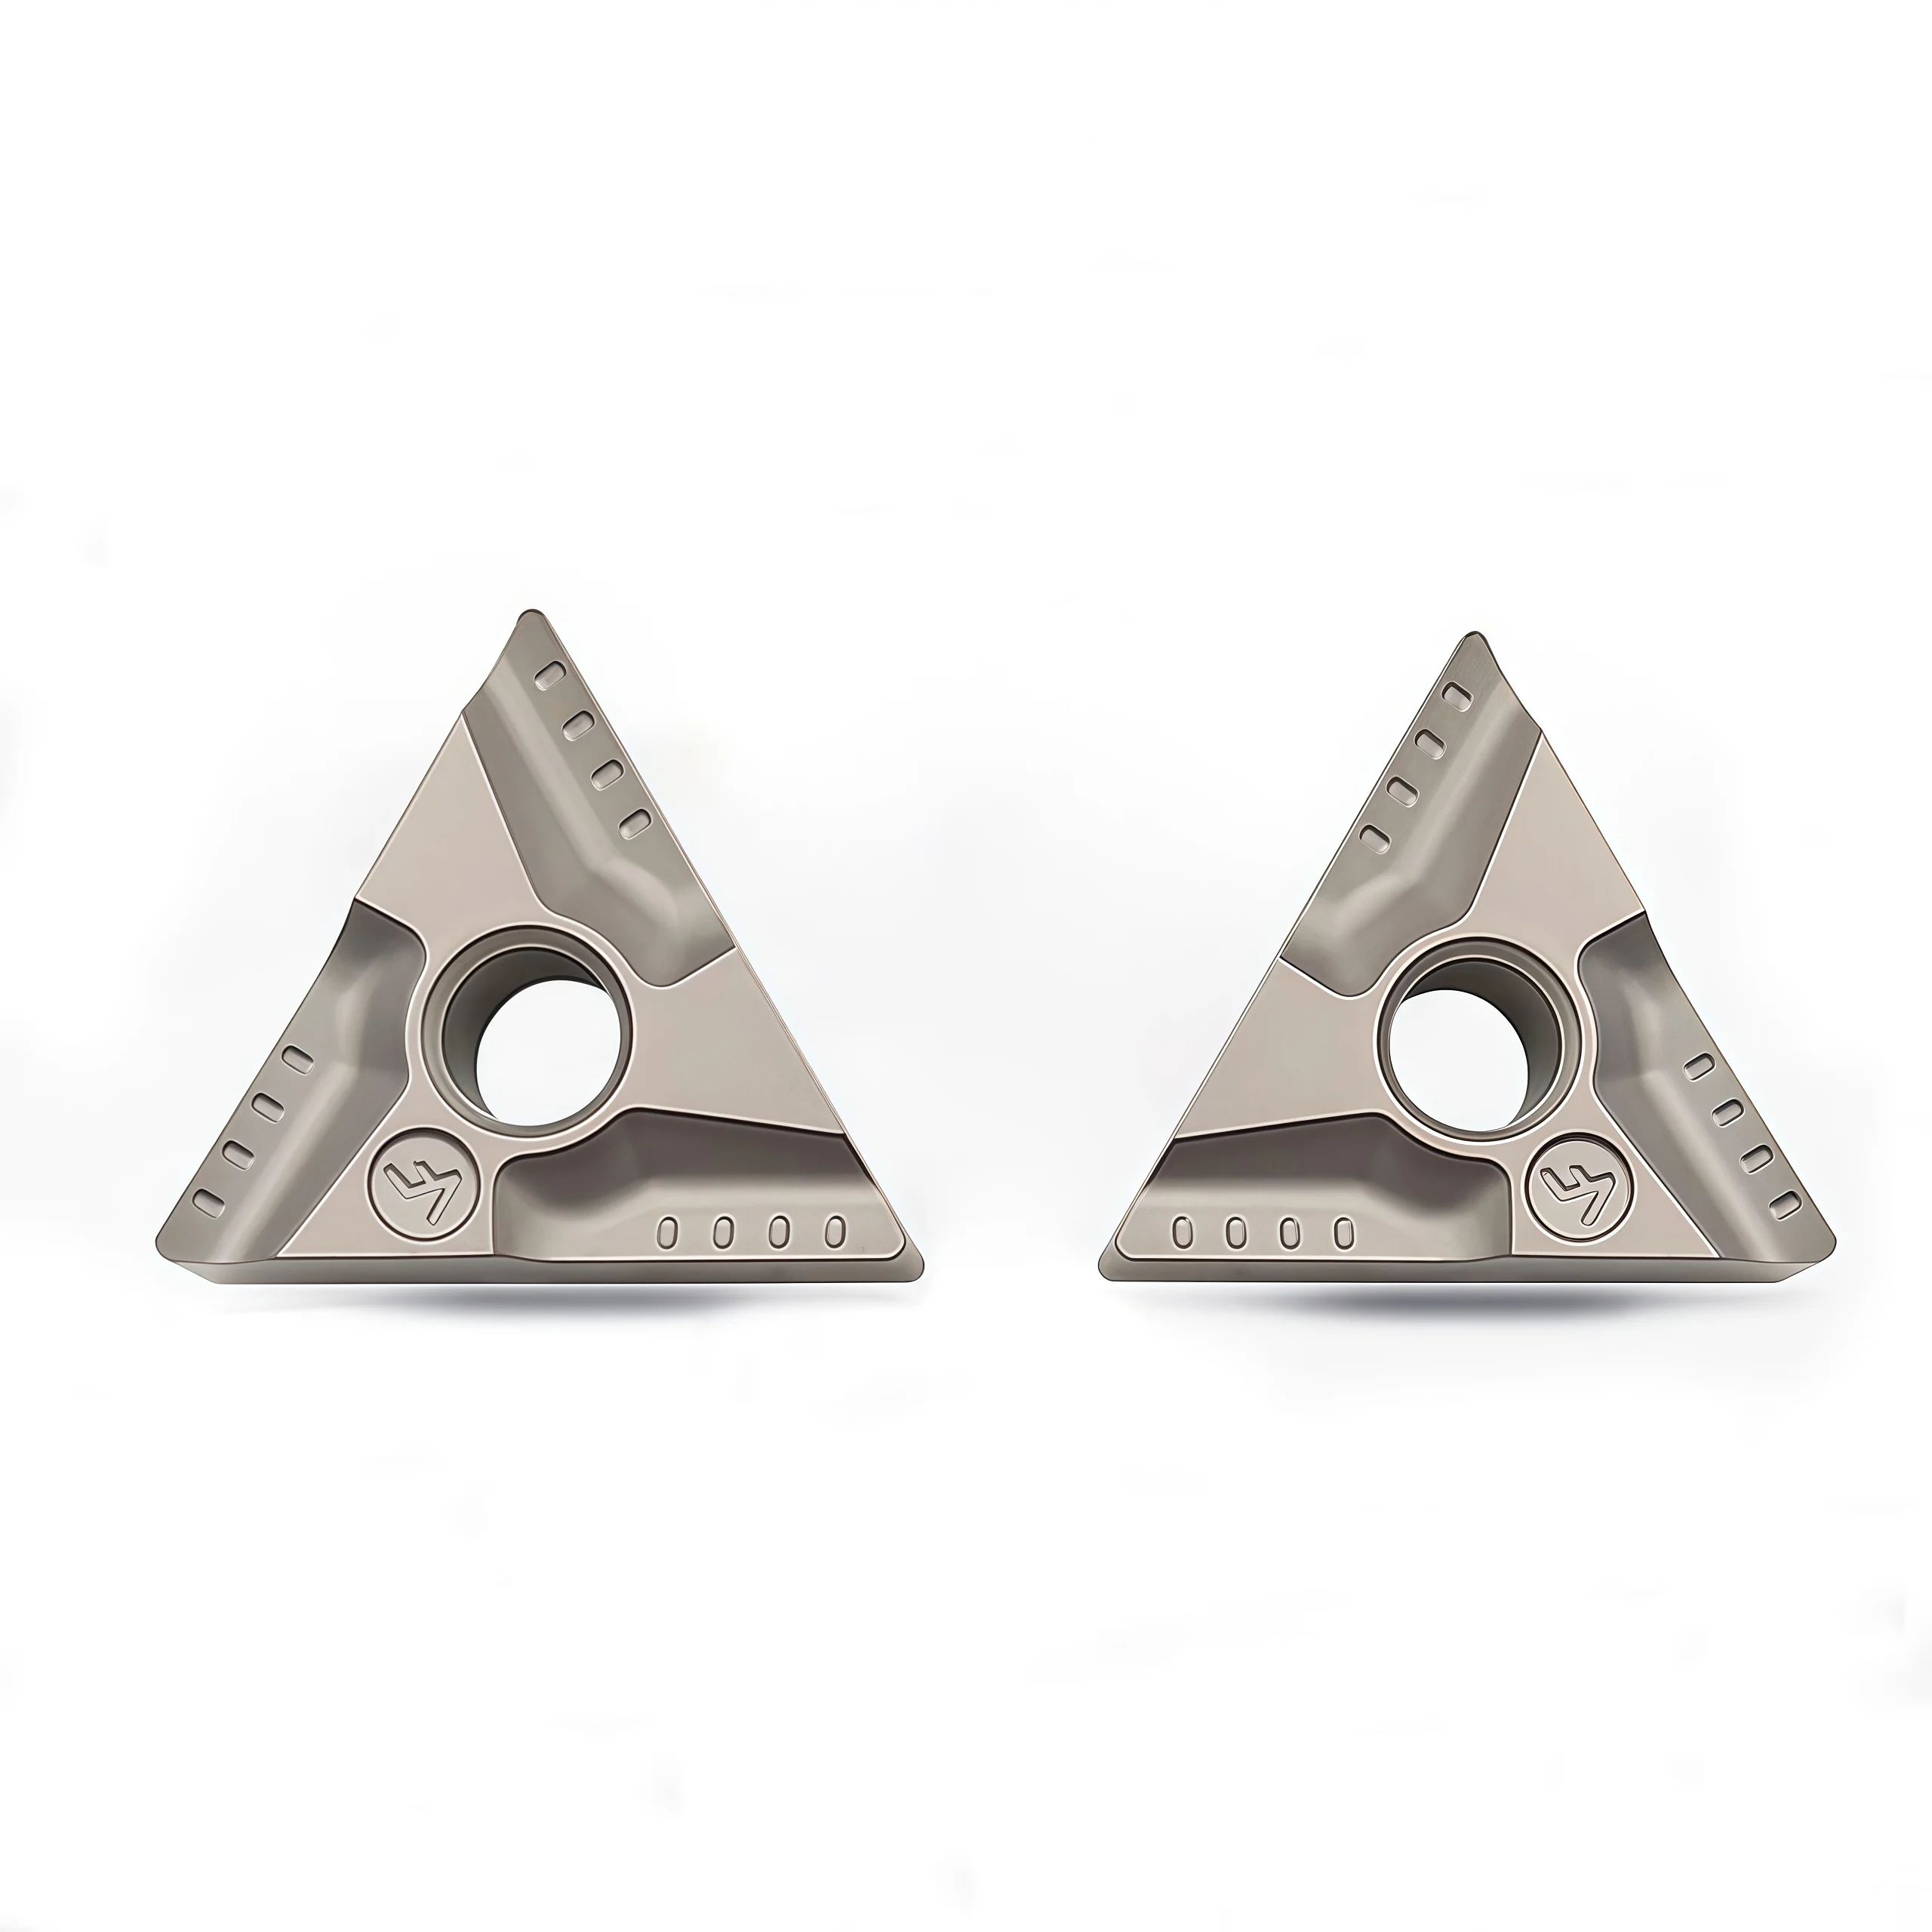
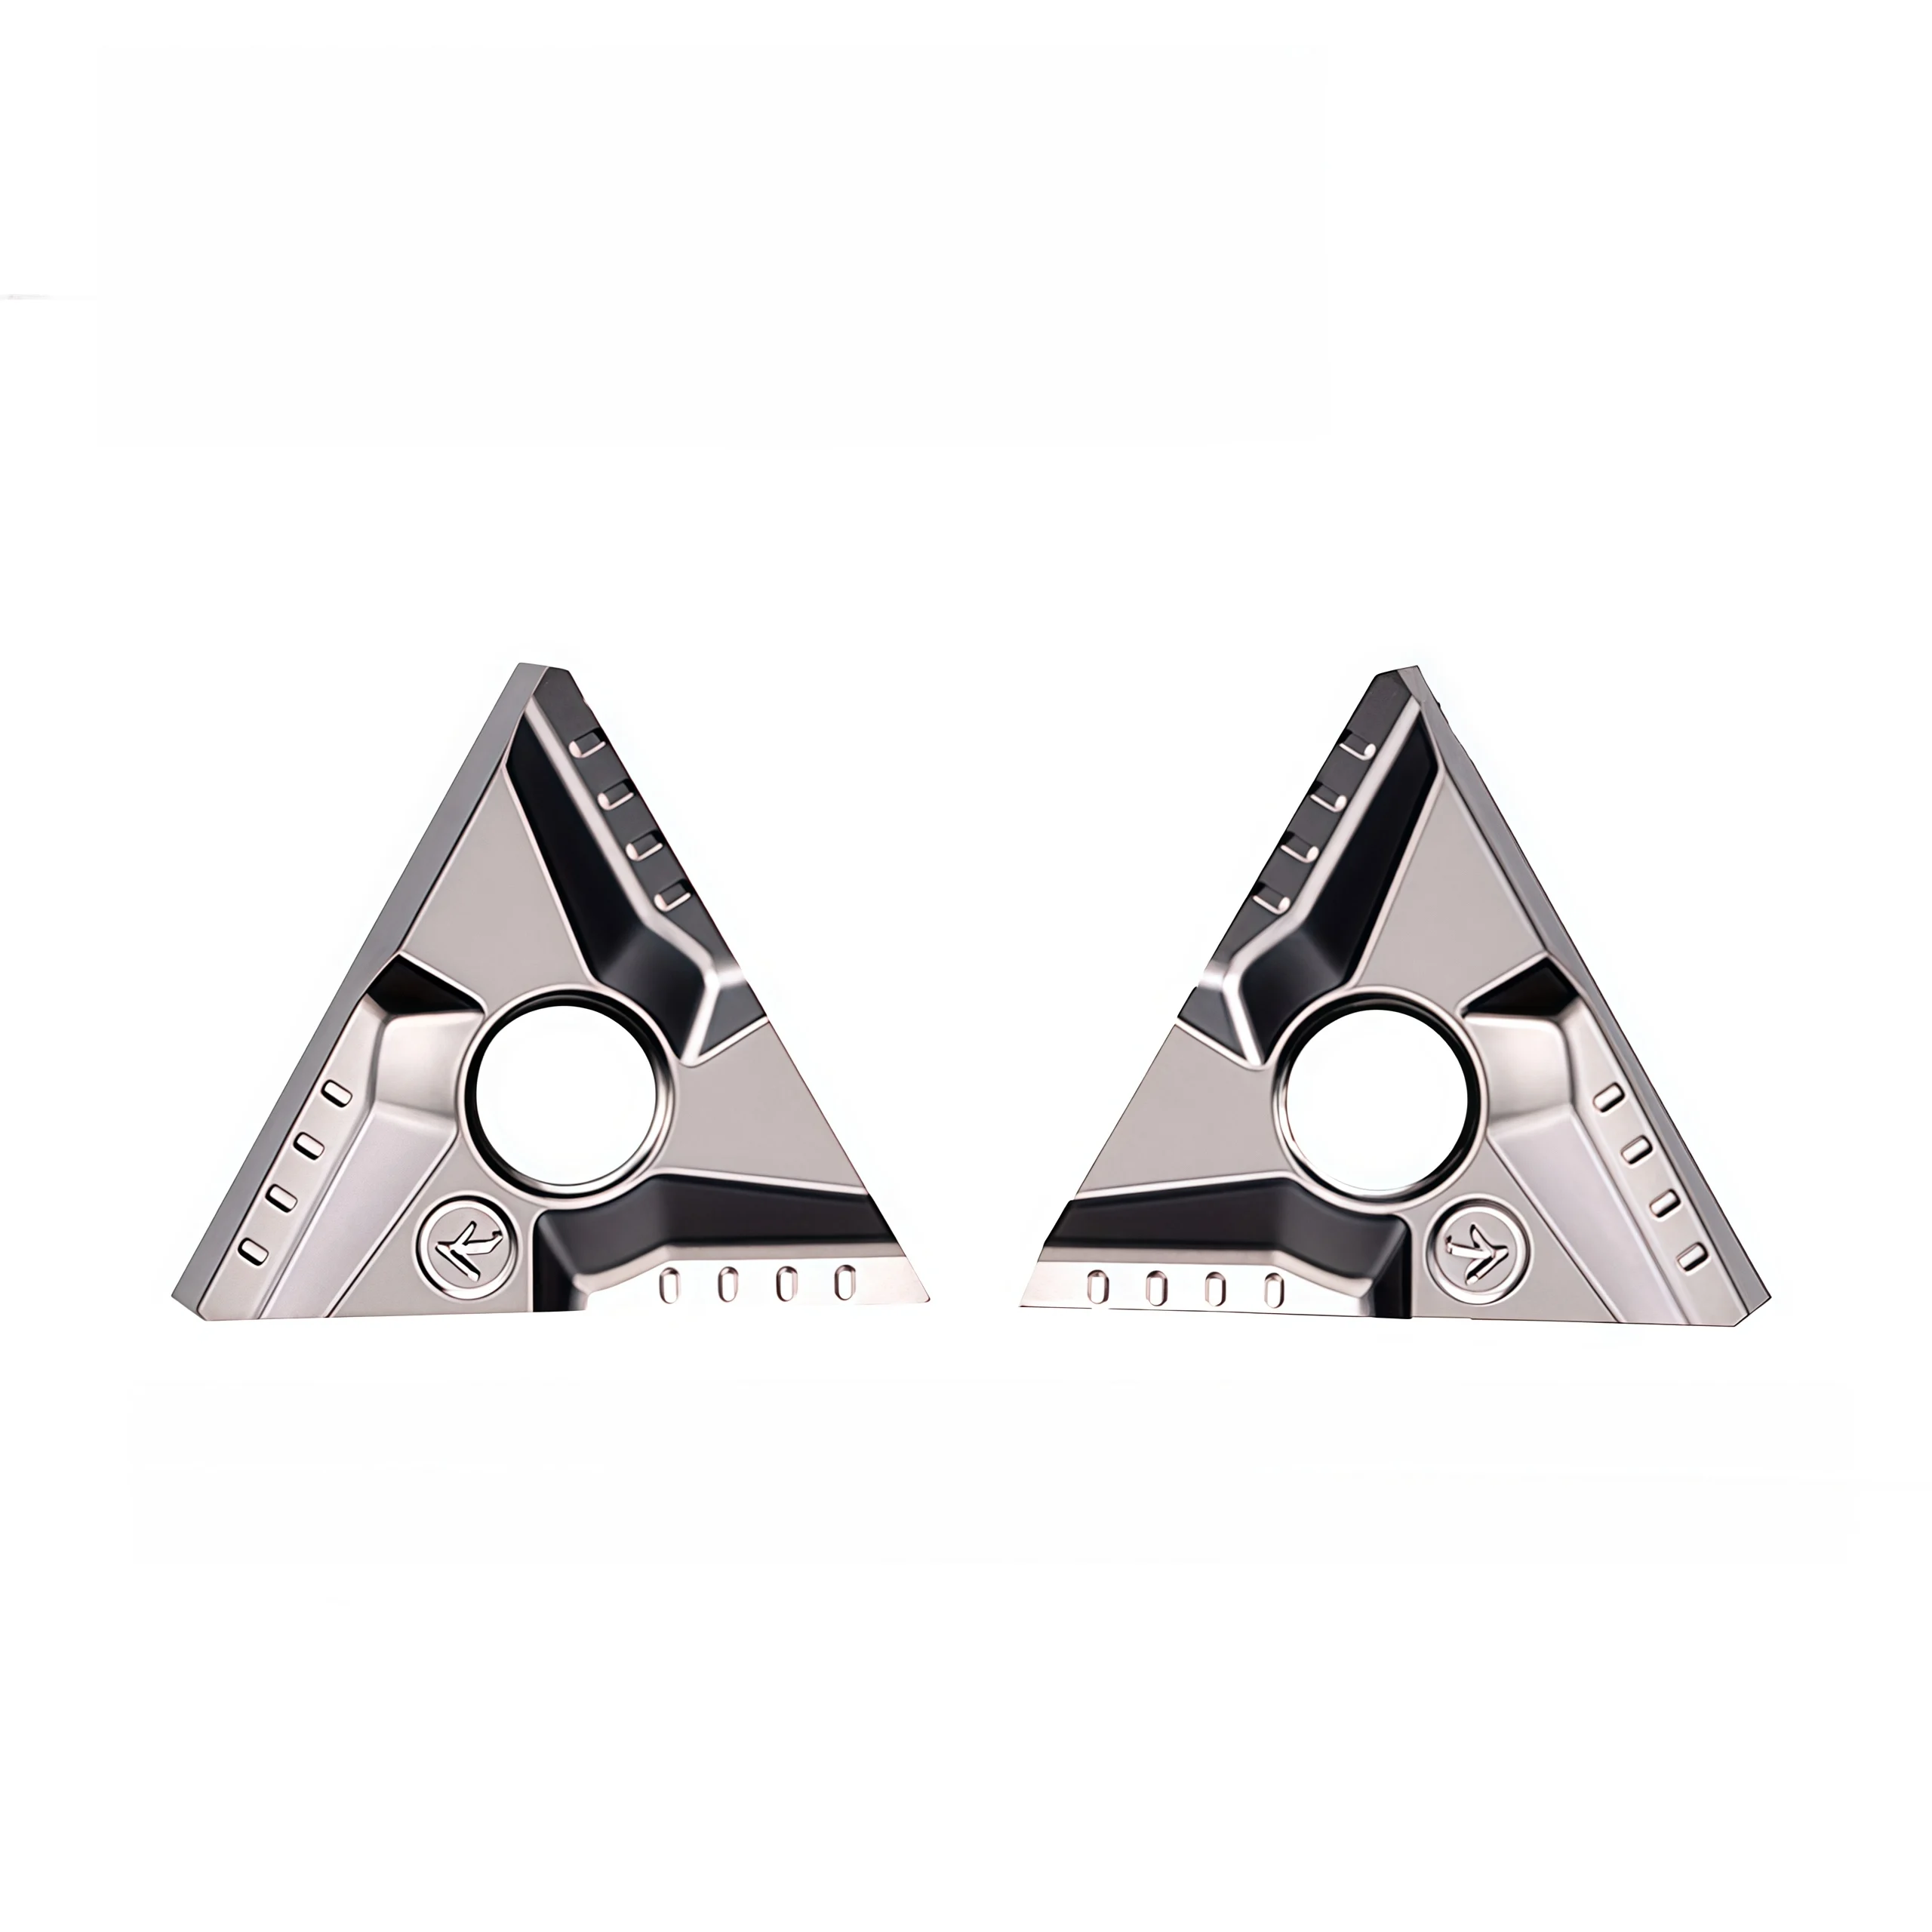
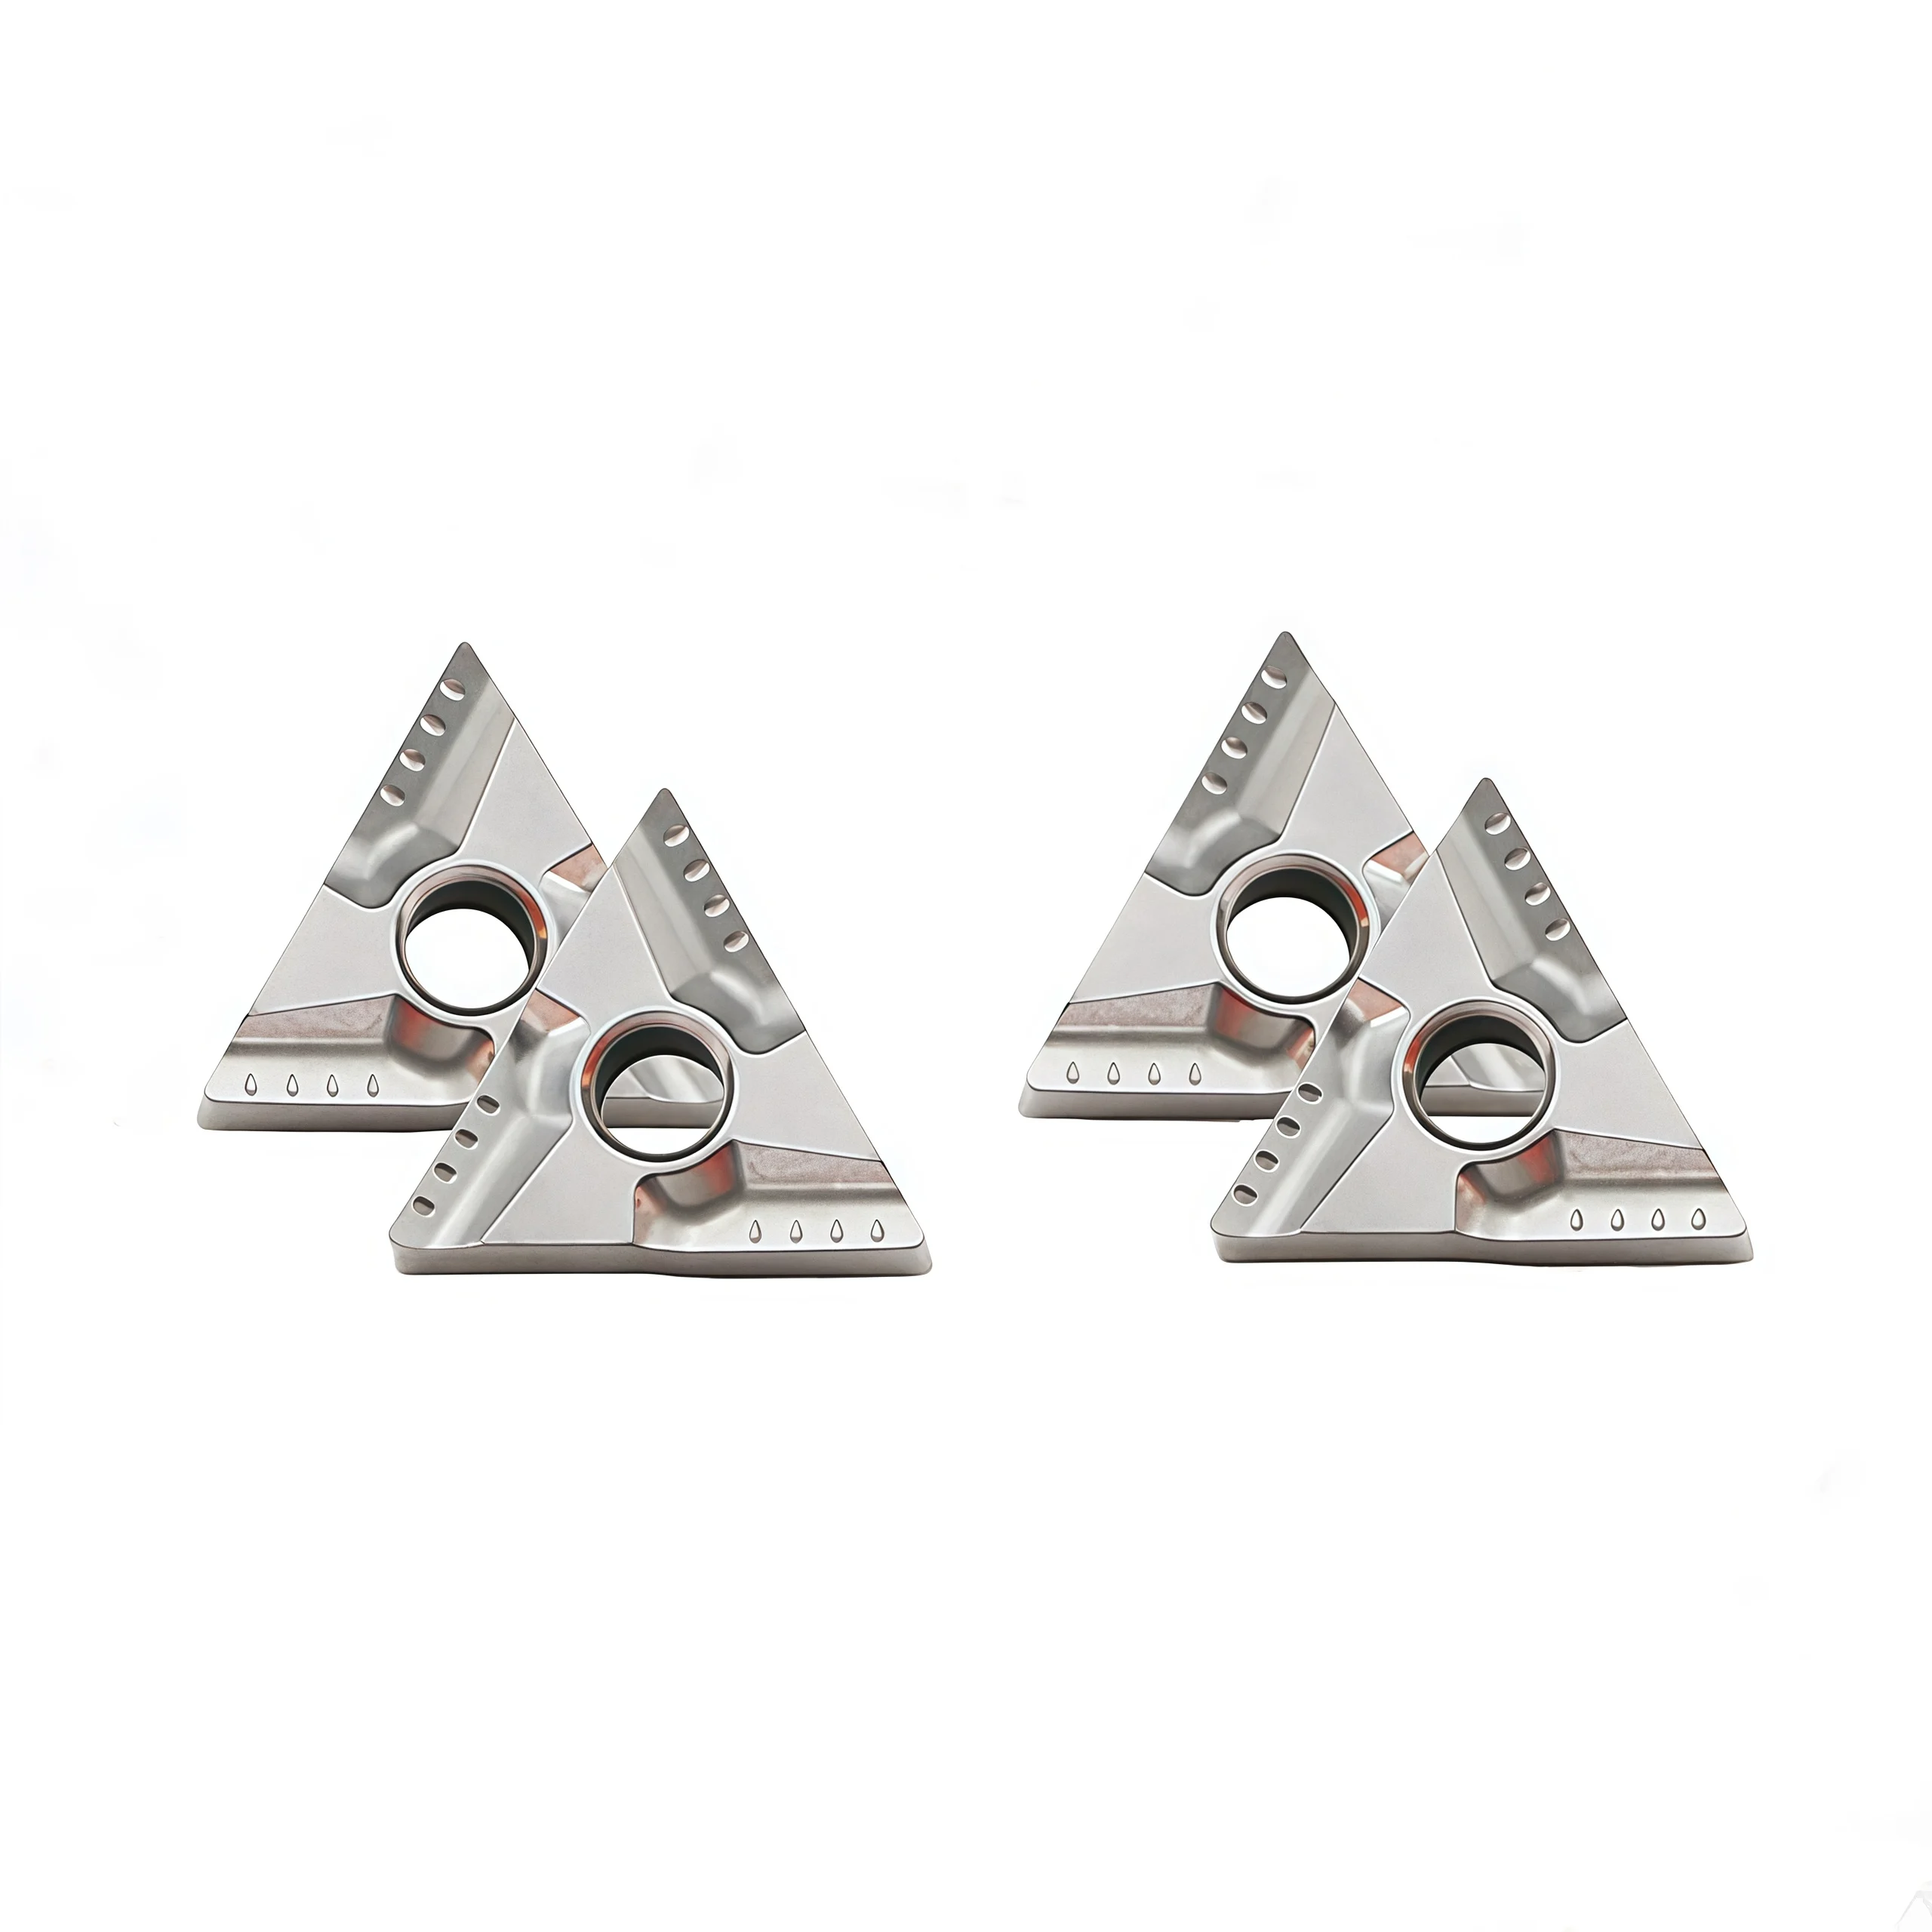
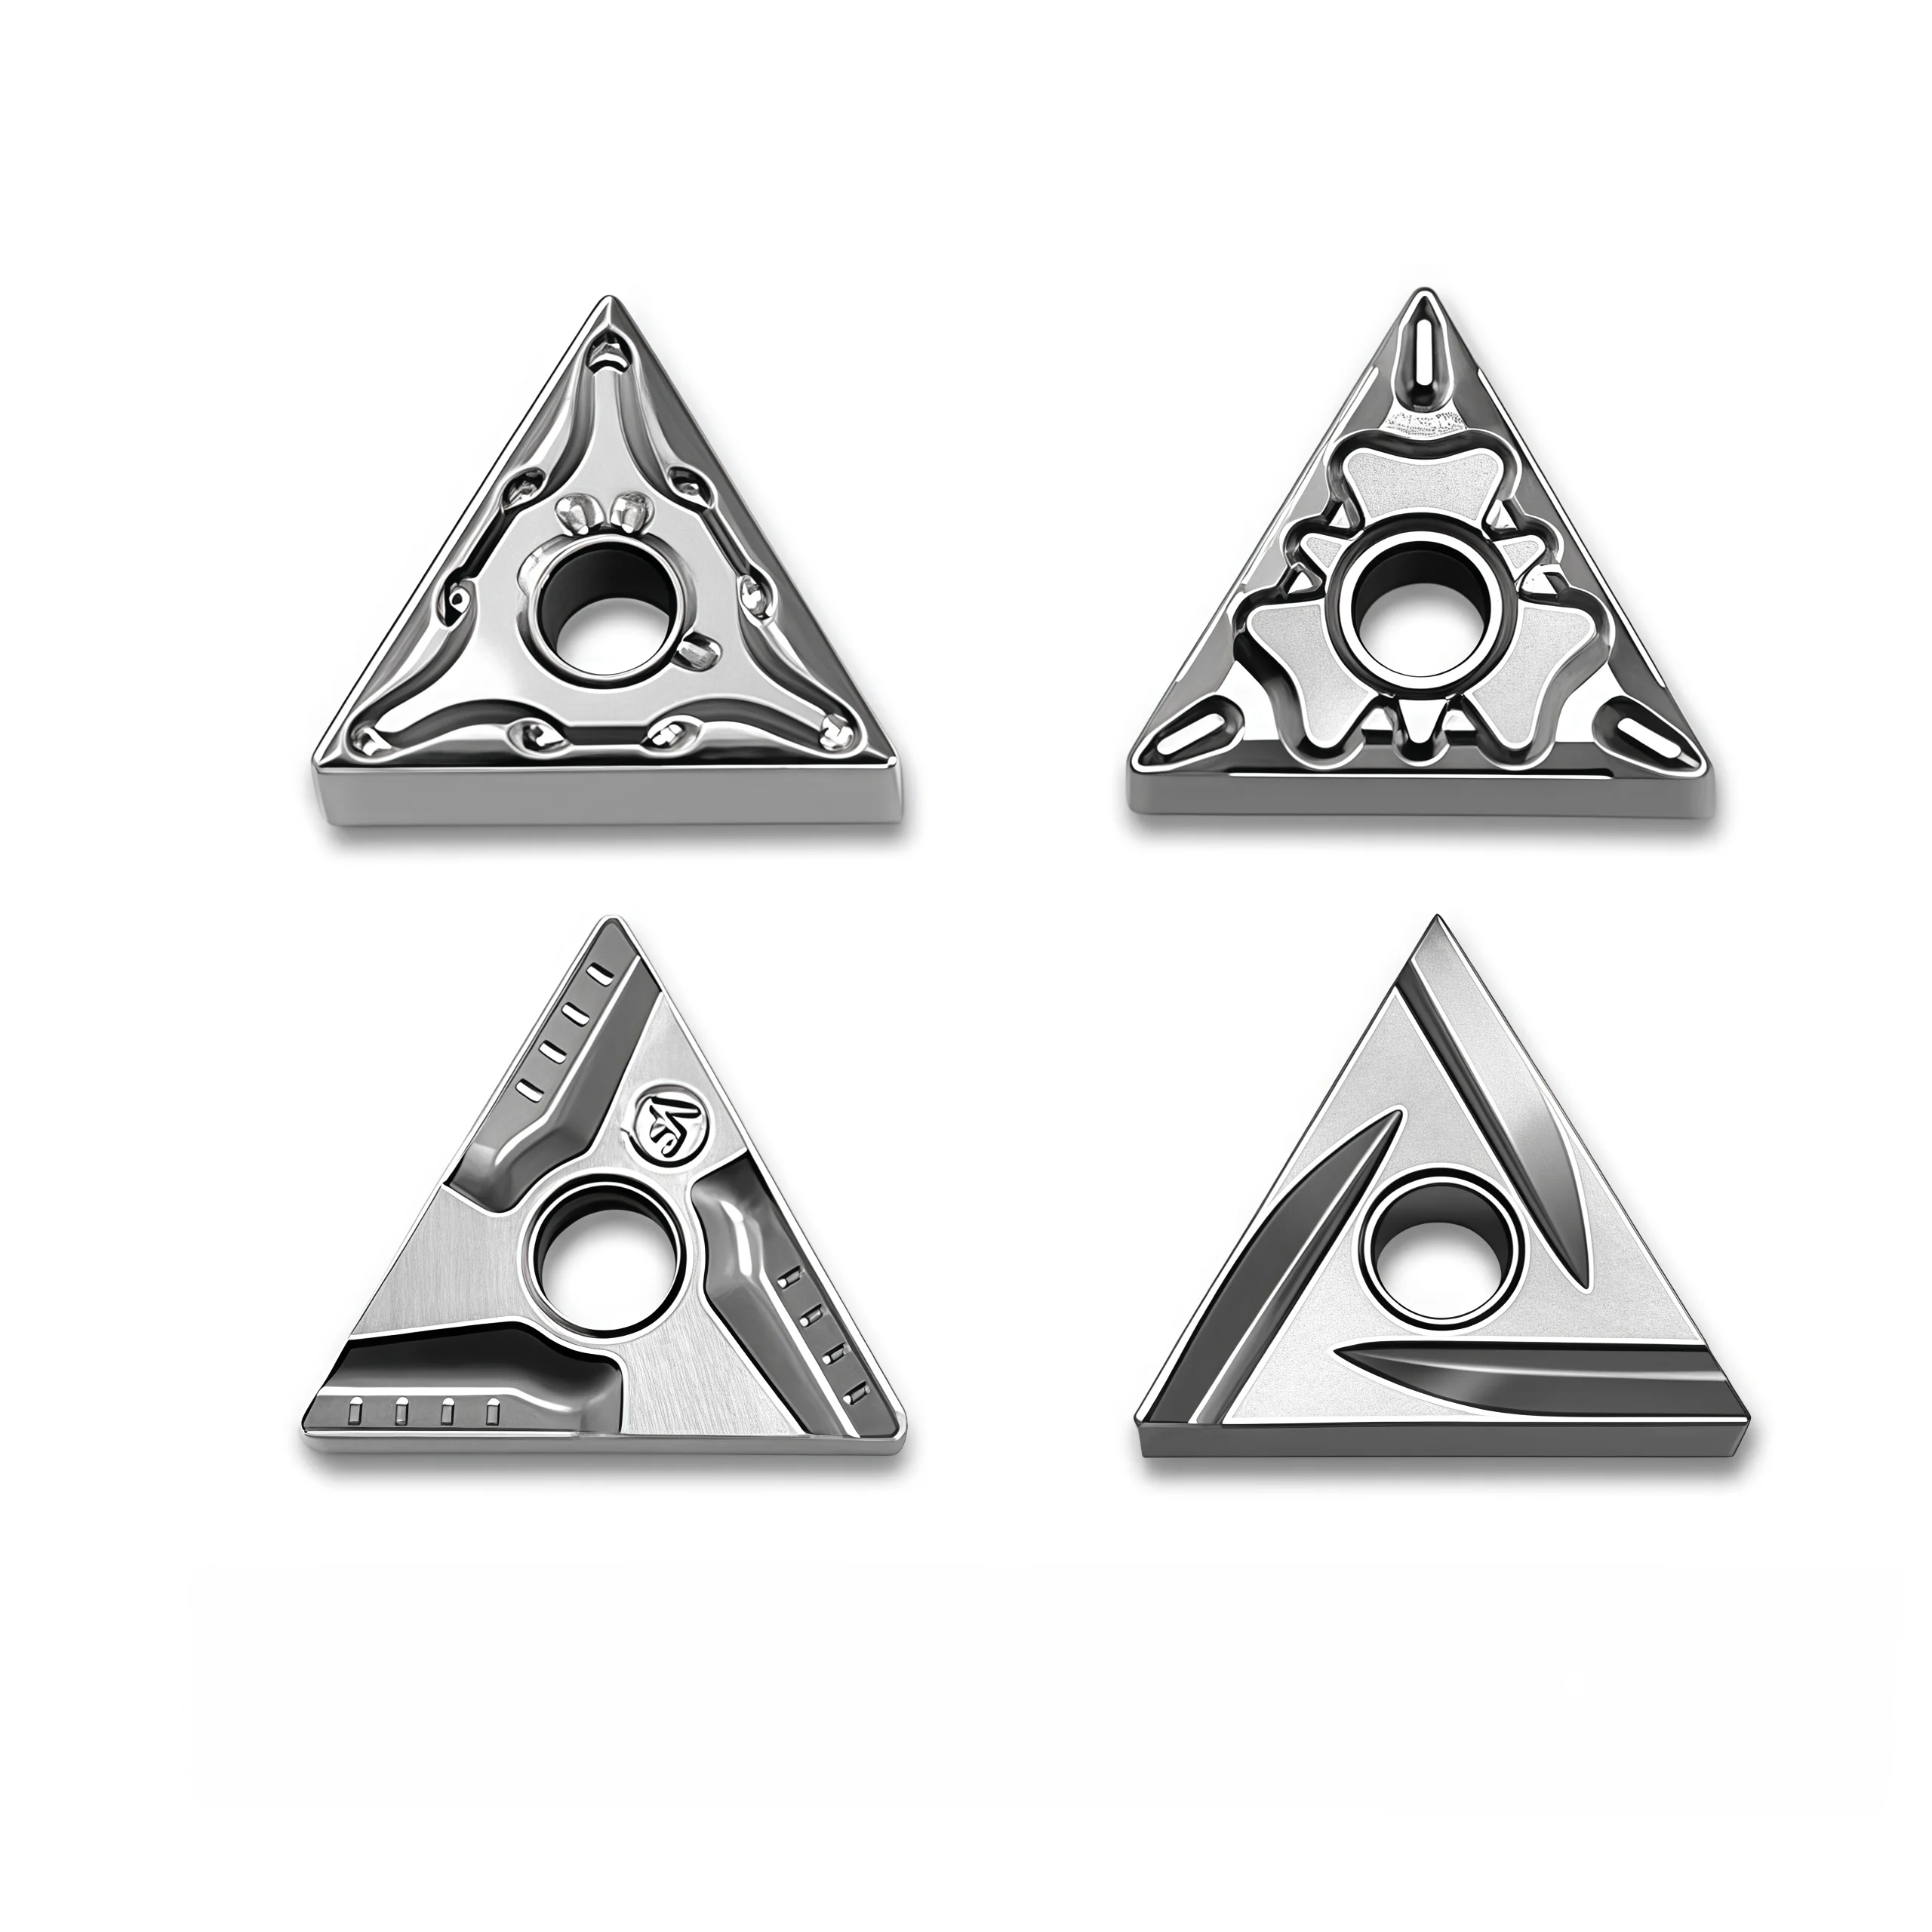
Il TNMG 160404/160408 R/L cermet inserts cover four handed configurations for finishing and light-to-medium turning of steel. Their 60° triangular, negative-clearance body fits compatible TNMG 1604 toolholders; the selected R or L cutting geometry must match the holder and feed direction.
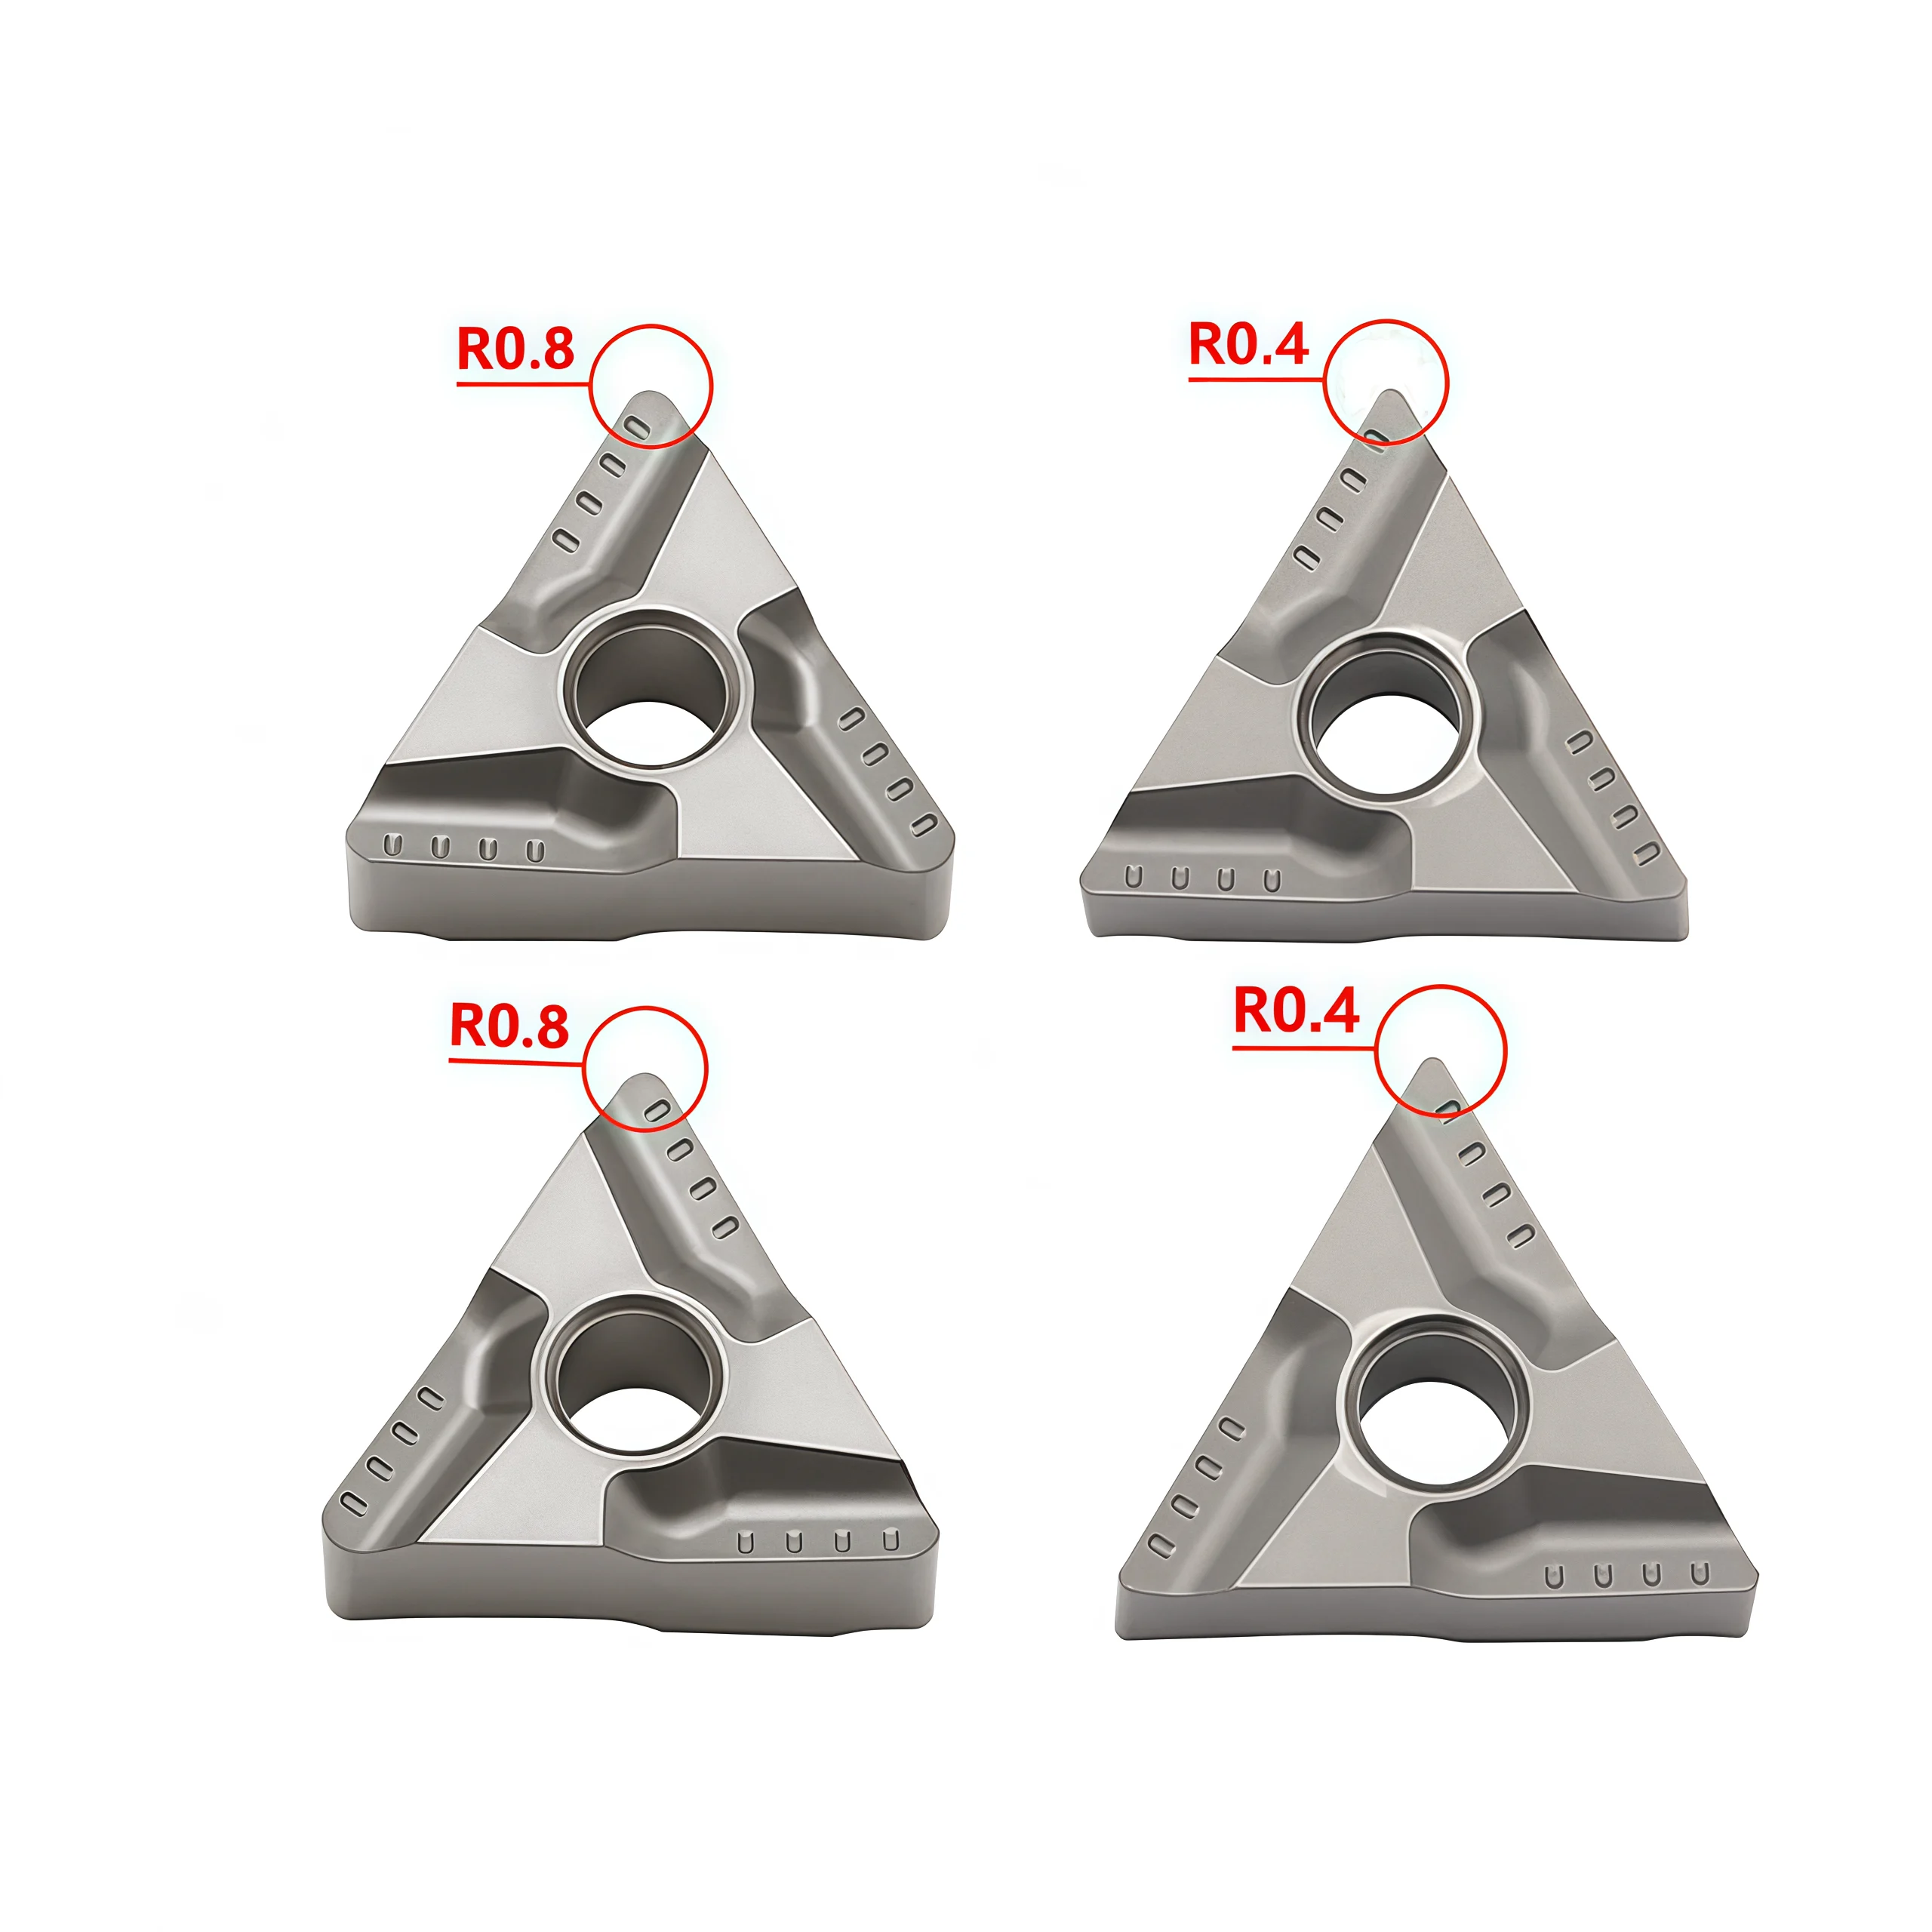
The 0.4 mm corner radius supports lighter finishing cuts, while the 0.8 mm radius gives additional corner support at suitable feeds. Select the cermet grade, coating and chipbreaker for the steel grade, workpiece hardness, cut continuity and desired surface finish.
The supplied page lists carbon and alloy steels as its primary applications. Availability of each R/L variant and any coated grade should be checked against the current item code before ordering.
Quick Procurement Summary
| Insert Family | TNMG 1604, 60° triangle | Substrate | Cermet |
|---|---|---|---|
| Listed Models | 160404R/L · 160408R/L | Nose Radius | 0.4 / 0.8 mm |
| Primary Workpiece | Carbon / low-alloy / suitable alloy steel | Main Operation | Finishing / light-to-medium turning |
| Order Reference | MOQ 10 pcs; 10 pcs / box as listed | Supply Check | R/L geometry, grade, coating and holder fit |
Grade, coating and pack quantity depend on the complete item code; confirm each requested configuration before ordering.
Key Turning Advantages
◆Choose the R/L Configuration
The R and L letters identify the handed cutting geometry specified on this range. They do not, by themselves, prove compatibility with every right- or left-hand holder. Match the complete insert suffix, holder model, clamping arrangement and intended feed direction.
| Modello | Nose Radius | Handed Geometry | Initial Selection |
|---|---|---|---|
| TNMG 160404R | 0.4 mm | R | Lighter finishing cuts |
| TNMG 160404L | 0.4 mm | L | Lighter finishing cuts |
| TNMG 160408R | 0.8 mm | R | Finishing / suitable semi-finishing |
| TNMG 160408L | 0.8 mm | L | Finishing / suitable semi-finishing |
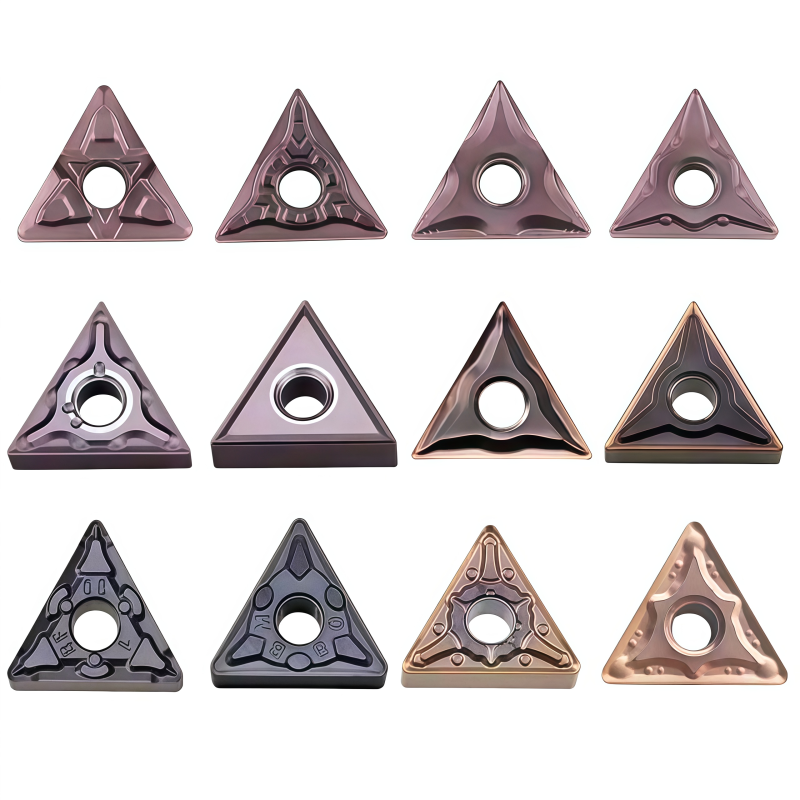
◆Product Images

Application & Ordering Check
For a recommendation, share the complete R/L code, holder model, steel grade and hardness, continuous or interrupted cut, finishing allowance, target finish, coolant, quantity and any existing grade you want to replace.
For a broader choice of insert shapes, view our carbide turning and milling insert range, or send your model list for a quotation.
◆Specifications & Size Chart
This range lists TNMG160404R/L and TNMG160408R/L cermet inserts. For TNMG 1604, published manufacturer catalogues show nominal IC 9.525 mm, thickness 4.76 mm and fixing hole 3.81 mm. The last two digits indicate the nominal 0.4 or 0.8 mm corner radius. Confirm the exact hand-specific geometry and product drawing for the ordered grade.
| Modello | Handed Geometry | IC (D)* | Thickness (S)* | Hole (D1)* | Nose Radius (rε) |
|---|---|---|---|---|---|
| TNMG 160404R | R | 9.525 mm | 4.76 mm | 3.81 mm | 0.4 mm |
| TNMG 160404L | L | 9.525 mm | 4.76 mm | 3.81 mm | 0.4 mm |
| TNMG 160408R | R | 9.525 mm | 4.76 mm | 3.81 mm | 0.8 mm |
| TNMG 160408L | L | 9.525 mm | 4.76 mm | 3.81 mm | 0.8 mm |
◆Material & Configuration
| Specifiche | Selection Detail |
|---|---|
| Substrate | Cermet; obtain the exact grade designation for the ordered item. |
| Primary workpiece | Carbon steel, low-alloy steel and suitable alloy steel, with hardness and cut conditions confirmed by grade. |
| Operation | Continuous finishing and appropriate light-to-medium turning. Heavy interruption or roughing requires a separately qualified grade and geometry. |
| R/L suffix | Hand-specific cutting geometry. Confirm the complete suffix, toolholder, approach angle and programmed feed direction. |
| Rivestimento | PVD and CVD are listed as range options. Verify the offered grade and coating for each model in the quotation. |
| Fornitura | MOQ 10 pieces and 10 pieces per box as standard references. Confirm stock, actual pack quantity and dispatch by full code. |
For stainless steel, aluminum, copper, cast iron or hardened steel, request a separate grade and application review; the TNMG size code alone does not establish suitability for these materials.
◆How to Select the Insert
Use our CNC Insert Selection Guide for additional holder, radius and grade checks.
◆Starting Cutting Data
Starting speed, feed and depth of cut depend on the complete cermet grade, chipbreaker, steel hardness and setup. Obtain the cutting-data range for the ordered code and actual workpiece. For turning, n = (1000 × Vc) / (π × D), where n is RPM, Vc is cutting speed in m/min and D is workpiece diameter at the cut in mm.
◆Related Series & Technical References
For other turning operations and materials, see our carbide turning and milling insert range. For a TNMG R/L dimensional drawing, grade-specific cutting data or quotation, send the full insert and holder codes with the steel grade and required quantity.
◆Carbide Insert Customization & OEM
Specify the insert around the machining operation, workpiece and holder. We can review standard replacements, application-specific geometry and private-label requirements using your insert designation, drawing or sample. Available grades, coatings, dimensions and order quantities are confirmed for each requested series.
Geometry & Chip Control
Review chipbreaker, rake, cutting-edge preparation, nose radius and corner design for the operation and workpiece. Confirm holder compatibility before approving a modified geometry.
Substrate & Coating
Select an available carbide grade and coating for the workpiece material, cutting conditions and desired balance of wear resistance and edge toughness.
Dimensions & OEM
Review insert size, thickness, locating and clamping features, tolerances, laser marking and private-label packaging against the approved specification.
◆Opzioni di personalizzazione
Use the fields below when sending an inquiry. The exact options depend on the insert family and are confirmed in the quotation or approved drawing.
| Specifiche | Details to Confirm |
|---|---|
| Insert Type | Turning, milling, threading, grooving or drilling insert; send the designation or drawing. |
| Size & Fit | Shape, size, thickness, inscribed circle or edge length, hole or clamping form, and holder model. |
| Geometria di taglio | Chipbreaker, nose or corner radius, edge preparation, cutting direction and application-specific profile. |
| Grade & Coating | Workpiece group and grade, carbide substrate, coating system and wet or dry cutting conditions. |
| Tolerance & Inspection | Critical dimensions, profile requirements, inspection method and any required report. |
| OEM Presentation | Insert or box marking, label content, packaging format and quantity per pack. |
◆How to Request a Custom Insert

Send your insert requirements through our contact form or review our OEM and private-label service.
◆Carbide Insert Quality Control

Insert quality depends on the approved grade, geometry, coating and dimensional specification. We review the requirements at order confirmation and align the inspection scope with the insert series and any customer drawing. Share critical dimensions or documentation needs before production so they can be included in the agreed inspection plan.
01 · Incoming Material
Confirm the specified carbide grade or material documentation against the order requirements.
02 · In-Process Checks
Review dimensions and cutting-edge features during production against the approved specification.
03 · Final Inspection
Check the agreed dimensions, appearance, edge condition, coating identification and marking as applicable.
04 · Packing Review
Verify the item code, quantity, labels and protective packing against the approved order.
◆Inspection & Documentation
Inspection points and acceptance criteria should be agreed for the ordered series. For custom inserts, the approved drawing takes priority over a generic catalogue description.
| Check Area | What to Confirm |
|---|---|
| Dimensions & Fit | Insert size, thickness, corner radius, clamping features and any drawing tolerances. |
| Geometria di taglio | Chipbreaker, edge preparation, usable corners and profile where applicable. |
| Grade & Coating | Approved grade and coating designation; any requested verification method. |
| Appearance & Packing | Visible edge damage, marking, item code, count and packing format. |
| Requested Records | Inspection report, material or coating documentation, sample approval or batch identification when agreed. |
◆Order & Delivery

Share a line-by-line list of insert codes and quantities for a mixed-size quotation. Stock status, minimum quantity, sample requirements and production lead time are confirmed for each grade, coating and configuration.
Send your item list and quality requirements through our contact form for specification, availability and delivery confirmation.
◆Product FAQs
What are these TNMG R/L cermet inserts designed to machine?
Their primary application is finishing and suitable light-to-medium turning of carbon, low-alloy and selected alloy steels. Select the exact cermet grade for the workpiece hardness, cut continuity and surface-finish target. Other materials need separate grade and application qualification.
What do R and L mean in the model number?
They distinguish handed cutting geometries offered in this range. Select the hand according to the supplier's insert drawing, holder model, edge engagement and planned feed direction. R or L in the insert code alone does not establish compatibility with every right- or left-hand toolholder.
What is the difference between 160404 and 160408?
They share the TNMG 1604 nominal body size, while the final two digits specify 0.4 mm and 0.8 mm corner radii. A 0.4 mm corner may suit lighter finishing and tighter profile access; a 0.8 mm corner gives additional support when feed, finish and setup rigidity allow.
Can I use these inserts for stainless steel or hardened steel?
Do not assume those materials are covered by a TNMG 1604 size designation. This selection is positioned for steel finishing. Request grade-specific application data and test the chosen insert if your workpiece falls outside the stated steel range.
What speed and feed should I use?
Use the cutting-data range for the complete cermet grade, chipbreaker and steel grade, accounting for hardness and cut continuity. A single speed or feed does not suit every R/L model. Start with a controlled trial on the actual machine.
Are PVD and CVD versions both available for every model?
PVD and CVD are listed as range options, but availability may differ by R/L model and grade. Confirm the exact coating process by complete ordering code rather than relying on the photograph or insert color.
◆Ordering & OEM FAQs
What should I provide for model matching?
Send the complete TNMG code, R/L hand, chipbreaker and grade, holder model, photographs of the insert and box label, steel grade and hardness, cutting conditions, finish requirement and quantity. Check holder fit and cutting results before substituting a different brand.
Can I order R and L models together?
Send a separate line for each radius, hand, grade and quantity. MOQ 10 pieces and 10 pieces per box are the listed references; confirm mixed-model availability, stock and lead time for each requested configuration.
Can I request samples before a larger order?
Provide the full code, holder, workpiece, proposed cutting parameters and evaluation criteria. Confirm sample availability, then compare edge wear, surface finish, dimensions and cost per accepted part under the same setup.
Are custom marking or private-label boxes available?
Send the desired insert or box marking, artwork, label text, pack quantity and estimated order volume for feasibility review. Confirm the approved configuration, minimum quantity and lead time in the quotation.
◆Guides & Technical References
Use the CNC Insert Selection Guide for shape, hand, radius, grade and holder checks. The Carbide Insert Types Guide covers related insert families.
For an R/L drawing, cermet grade sheet, cutting data or quotation, send the complete insert and holder codes with the steel grade and quantity.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.