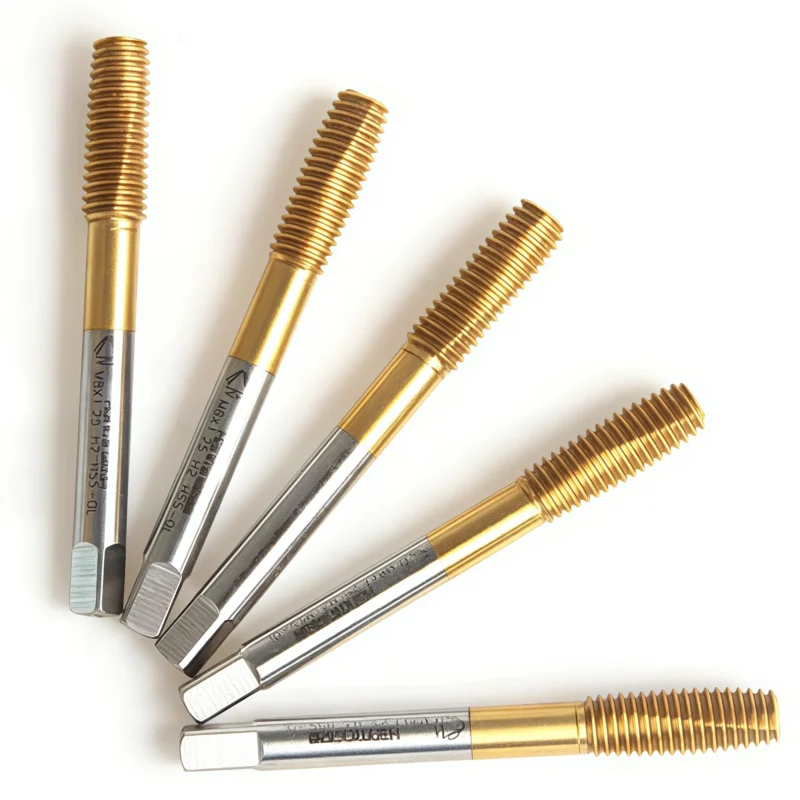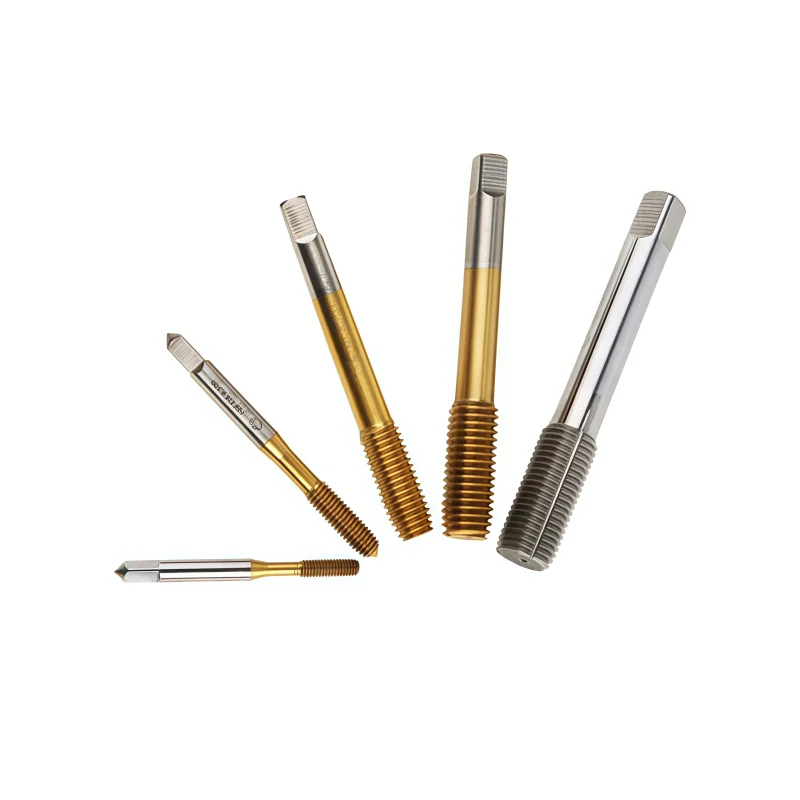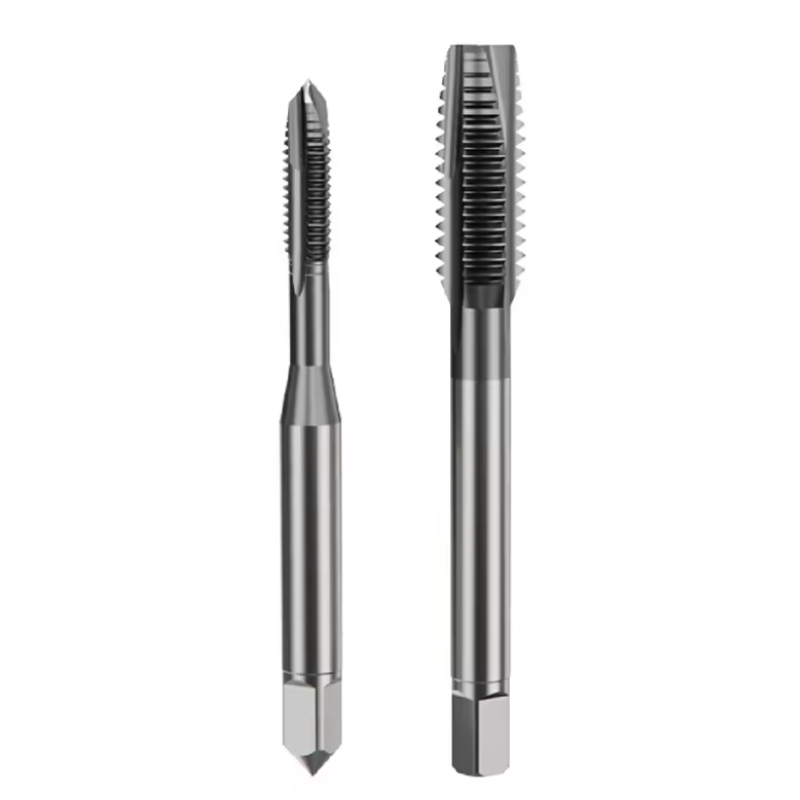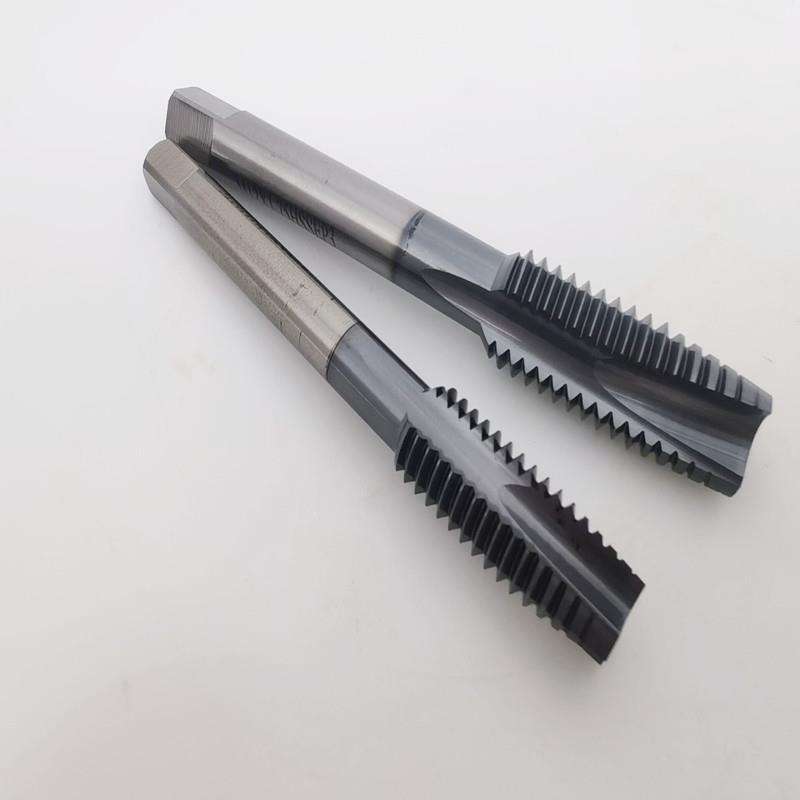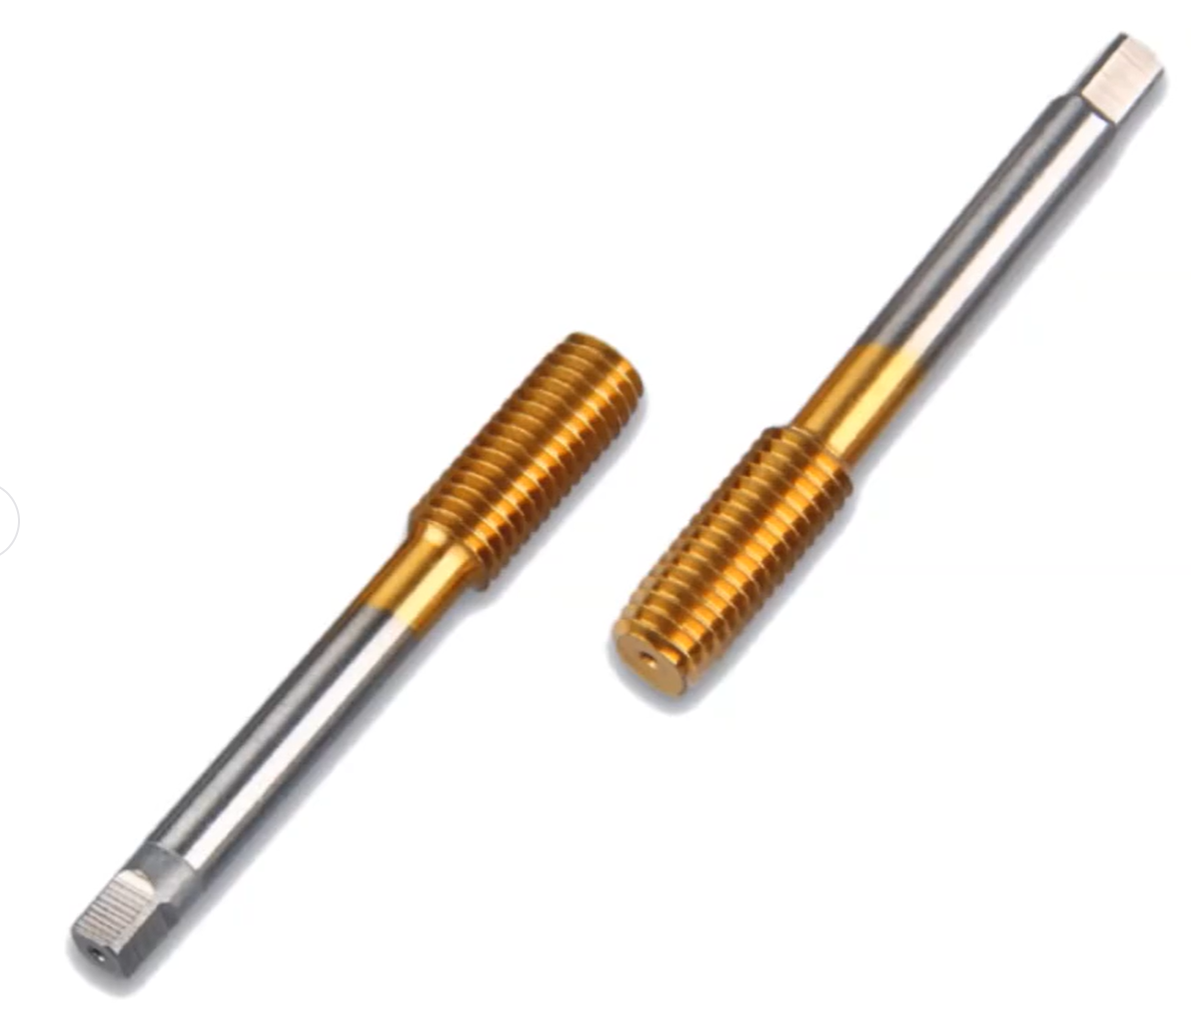


TiN-beschichtete HSS-E-Gewindeformer aus M35 für UNC- und UNF-Gewinde
TiN-coated M35 cobalt forming taps (roll taps) for chipless UNC and UNF threading in suitable ductile metals.
Spanlose Umformung
UNC & UNF
M35 Cobalt HSS
TiN Coated
M35 Cobalt UNC & UNF Thread Forming Taps
TiN-coated M35 cobalt thread forming taps, also called roll taps or fluteless taps, produce UNC and UNF internal threads by displacing ductile metal rather than cutting chips. These inch-size machine taps support blind- and through-hole applications when material, pre-hole size, lubrication and machine torque are correctly matched.
Thread forming process — general demonstration
Chipless Forming for Unified Inch Threads
Keine Späne
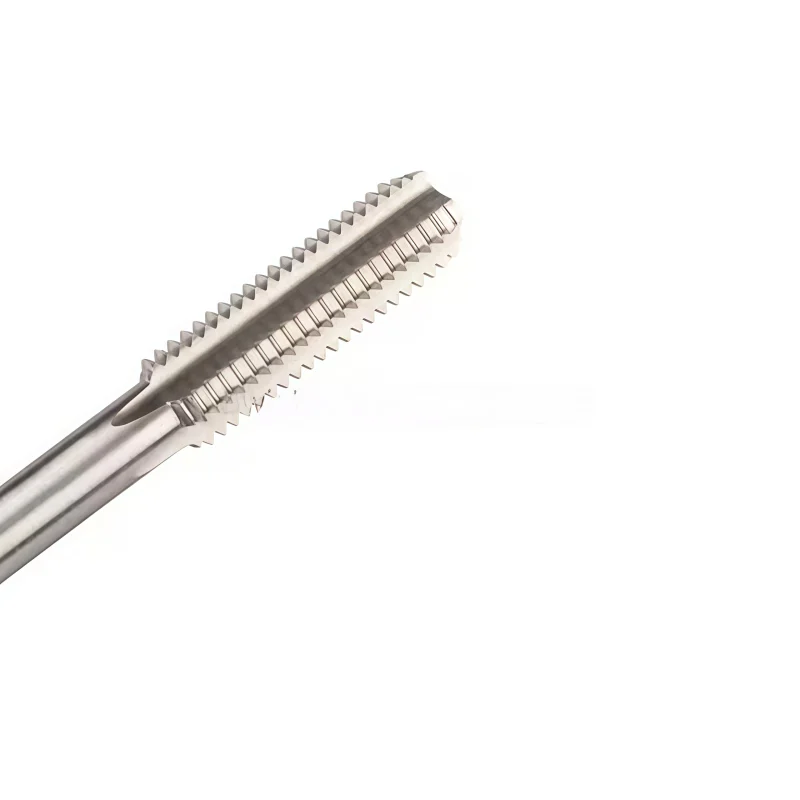
Forming lobes reshape the pre-drilled hole into an internal thread, eliminating cutting-chip evacuation.
M35 HSS-Co Substrate
Cobalt-alloyed high-speed steel supports hot hardness and wear resistance during repeat forming operations.
TiN-Coated Surface
Titanium nitride provides a hard, wear-resistant surface for suitably lubricated thread forming.
UNC & UNF Roll Tap Selection
Select the complete diameter, TPI and thread series. UNC coarse and UNF fine threads require different taps; availability and dimensional combinations vary by specification.
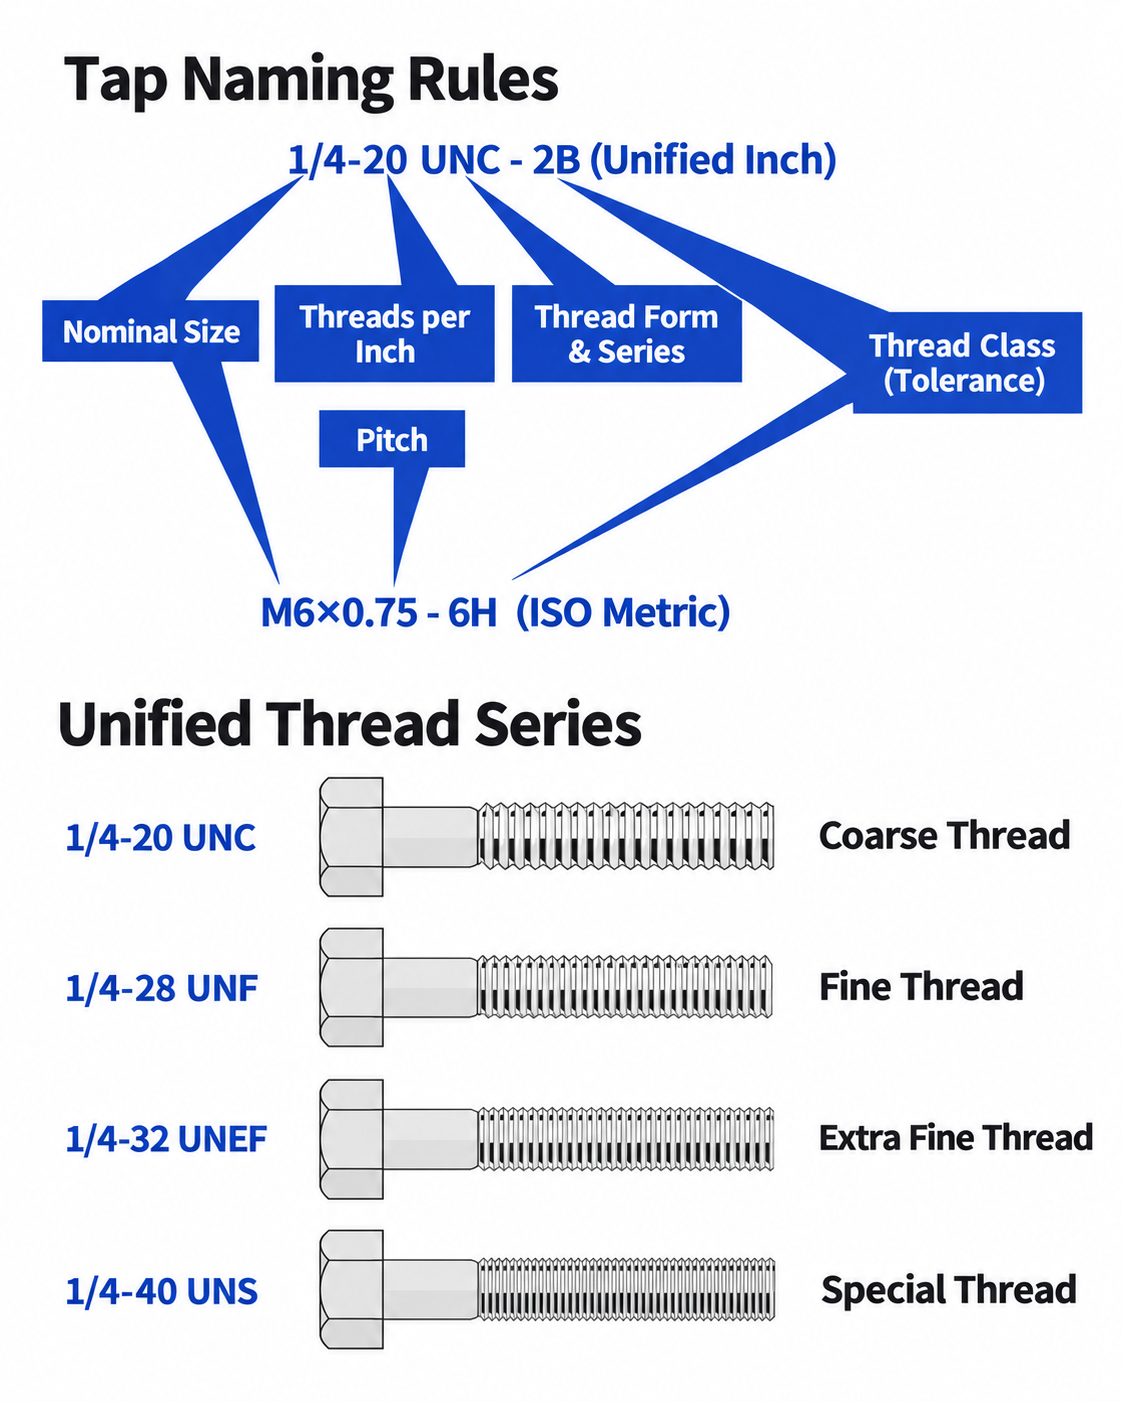
Chipless CNC Tapping Applications
For drawing-specified Unified threads in formable metals, including CNC production of:
- Housings, brackets and industrial equipment components.
- Automotive and general engineering parts with UNC or UNF threads.
- Blind- and through-hole components where cutting-chip removal is difficult.
Am besten geeignet für: Repeat inch-thread production in sufficiently ductile metals with controlled pre-hole size and lubrication.
Nicht ideal für: Brittle materials or setups without adequate torque, lubrication and pre-hole control.
Materials for Thread Forming
Ductile carbon steels, selected stainless steels, aluminum, copper and formable brass alloys can be reviewed for these HSS-Co forming taps. Suitability depends on the exact grade, hardness and ductility.

General material reference; not every listed material is suitable for roll tapping.
Pre-Hole, Lubrication & Machine Checks
- Thema: Match UNC or UNF, diameter, TPI and required tap limits.
- Pre-hole: Use a forming-tap drill size matched to material and thread requirements.
- Tiefe: Confirm forming length, chamfer allowance and blind-hole bottom clearance.
- Machine: Check available torque, holder fit, synchronized feed and suitable lubrication.
Forming taps require a different pre-hole size from cutting taps. An undersized hole increases torque; an oversized hole can leave insufficient thread formation.

TiN-Coated M35 Forming Tap Details


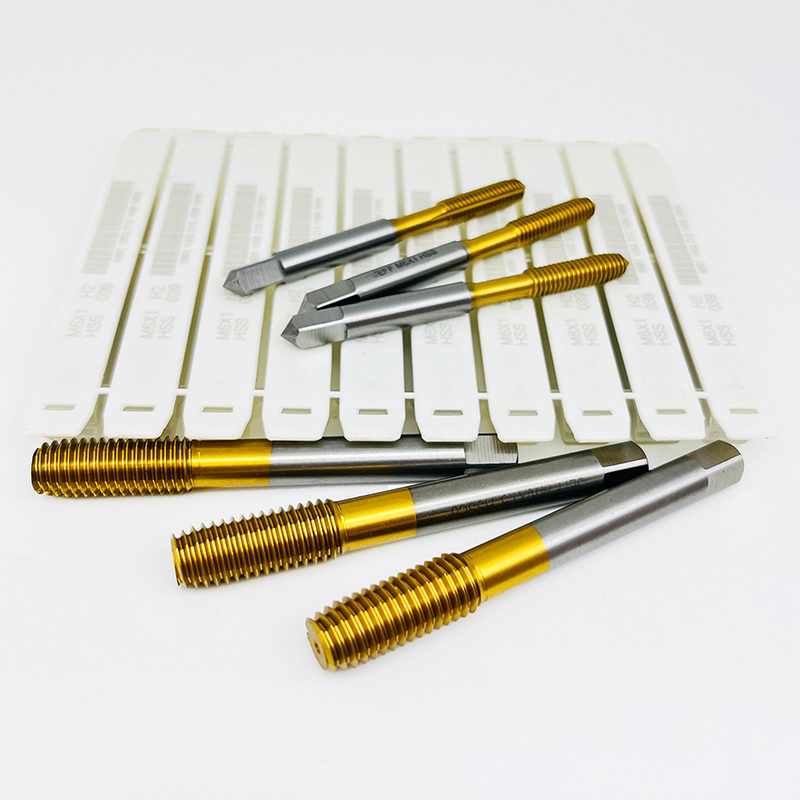
M35 UNC & UNF Forming Tap Sizes
Dimensional references for TiN-coated M35 cobalt thread forming taps, also called roll taps. Select the complete UNC or UNF designation, then check working length, shank and holder fit. Dimensional values are in millimeters unless stated otherwise.

UNC / UNF Inch-Size Roll Tap Chart

The supplied chart lists 42 specifications from #2-56 through 5/8-18. Confirm each diameter, TPI and thread-series combination before ordering.
| Spezifikation | Listed Range |
|---|---|
| Thread Series | UNC / UNF |
| Nominal Thread Diameter | 2.184–15.875 mm |
| Chart “Flute Length”* | 9.5–32 mm |
| Gesamtlänge | 44.5–102 mm |
| Schaft-Durchmesser | Ø2.8–Ø12.5 mm |
| Drive-Square Dimension | 2.24–10 mm |
“Flute Length” follows the supplied chart label. Confirm usable forming length separately; it does not establish full-thread depth or the presence of cutting flutes.
Benötigen Sie Informationen zu Größen, Preisen oder individuellen Optionen?
Send your UNC or UNF designation, material, required thread depth and quantity for specification confirmation and quotation.
UNC / UNF Forming Tap Selection Checks
- Thema: Match diameter, TPI, UNC or UNF series and specified tap limits.
- Material: Confirm grade, hardness and sufficient ductility for thread forming.
- Depth & fit: Check forming length, chamfer allowance, bottom clearance and holder dimensions.
- Machine: Verify available torque, alignment and suitable lubrication.
Confirm forming chamfer, lubrication grooves and coolant configuration where required; these are not defined by the thread designation.
Forming-Tap Drill Size & Pre-Hole Control
Roll taps generally require a larger, closely controlled pre-hole than equivalent cutting taps. Select the forming-tap drill diameter for the thread size, material and required thread formation. The nominal diameters in the chart are not drill-size recommendations.
Custom UNC & UNF Thread Forming Taps
Custom M35 cobalt roll taps can be reviewed for inch-thread production in suitable ductile metals.
- Thema: UNC / UNF size, TPI and specified tap limits.
- Forming geometry: Lobes, chamfer and lubrication grooves where required.
- Abmessungen: Forming length, reach, shank and drive square.
- Surface: TiN or alternative coatings, subject to application review.
Specifications, MOQ and lead time are confirmed with the quotation.
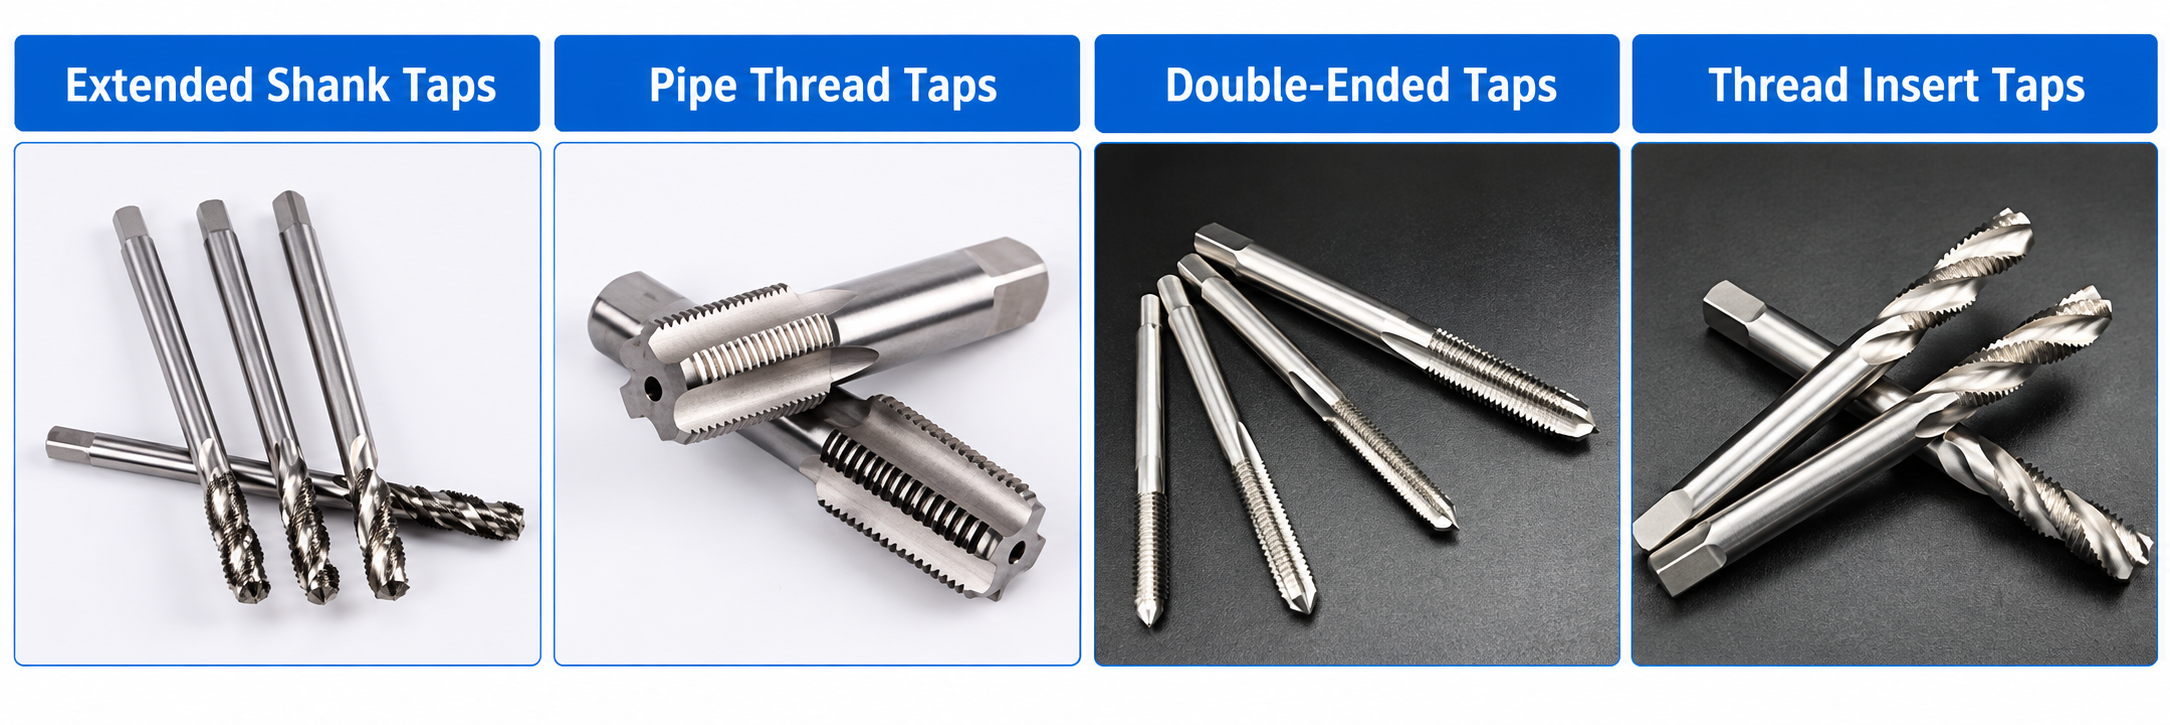
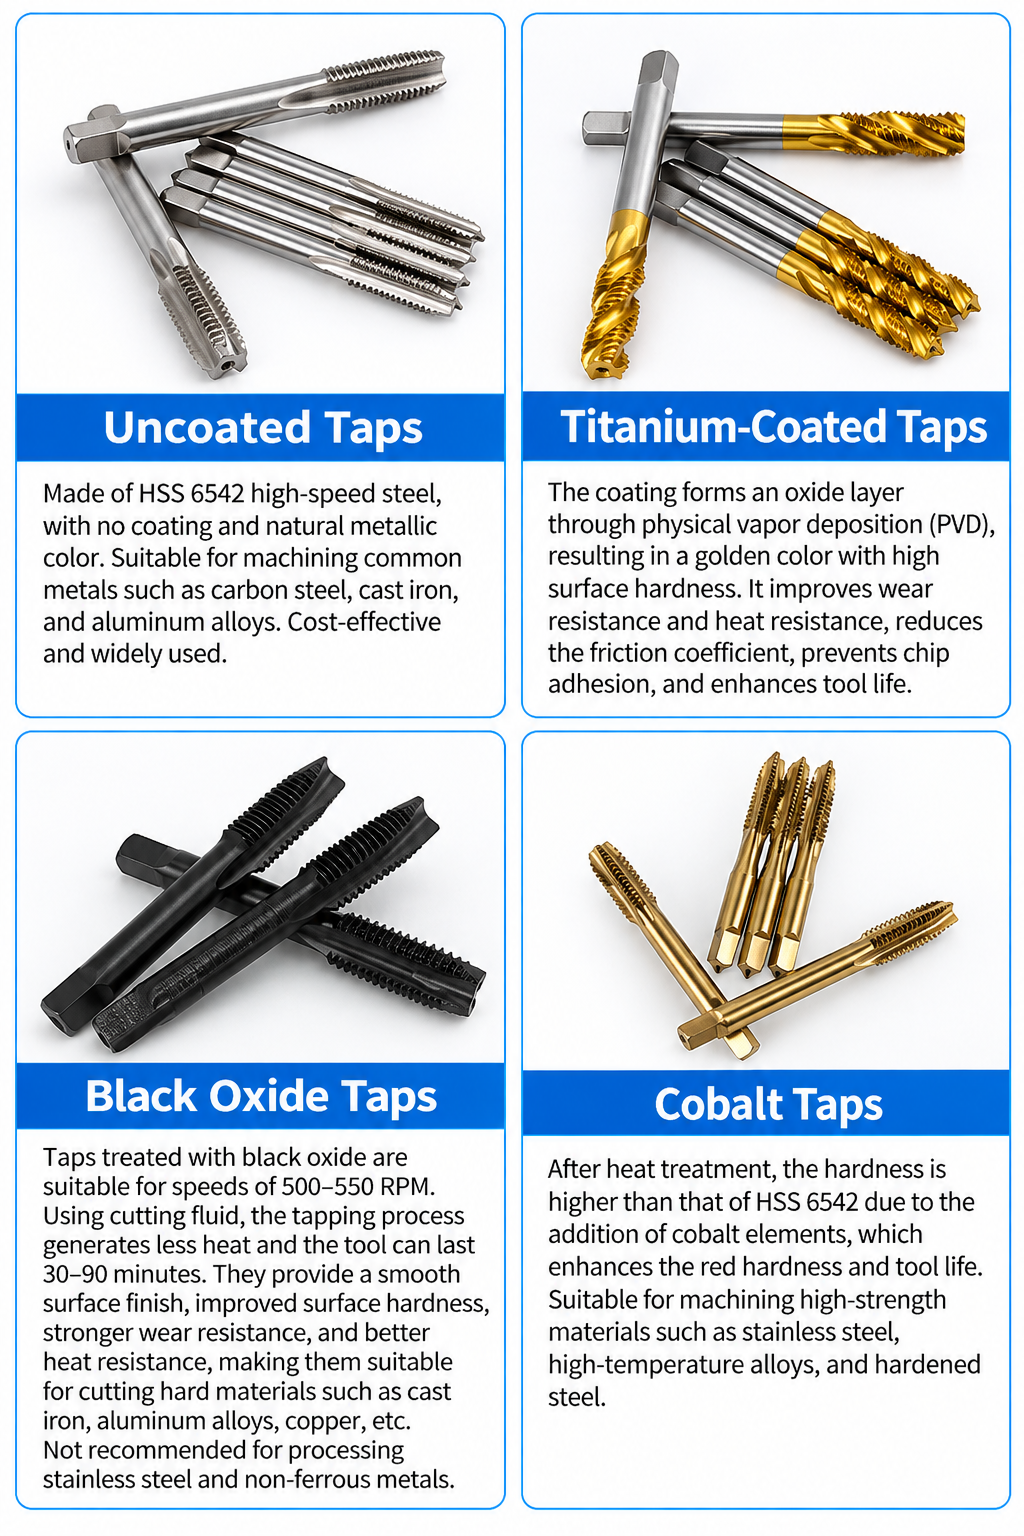
General range and coating references; options vary by forming-tap specification.
OEM & Private-Label Roll Taps
Distributor orders can include logo marking, thread codes, product labels and branded protective packaging.
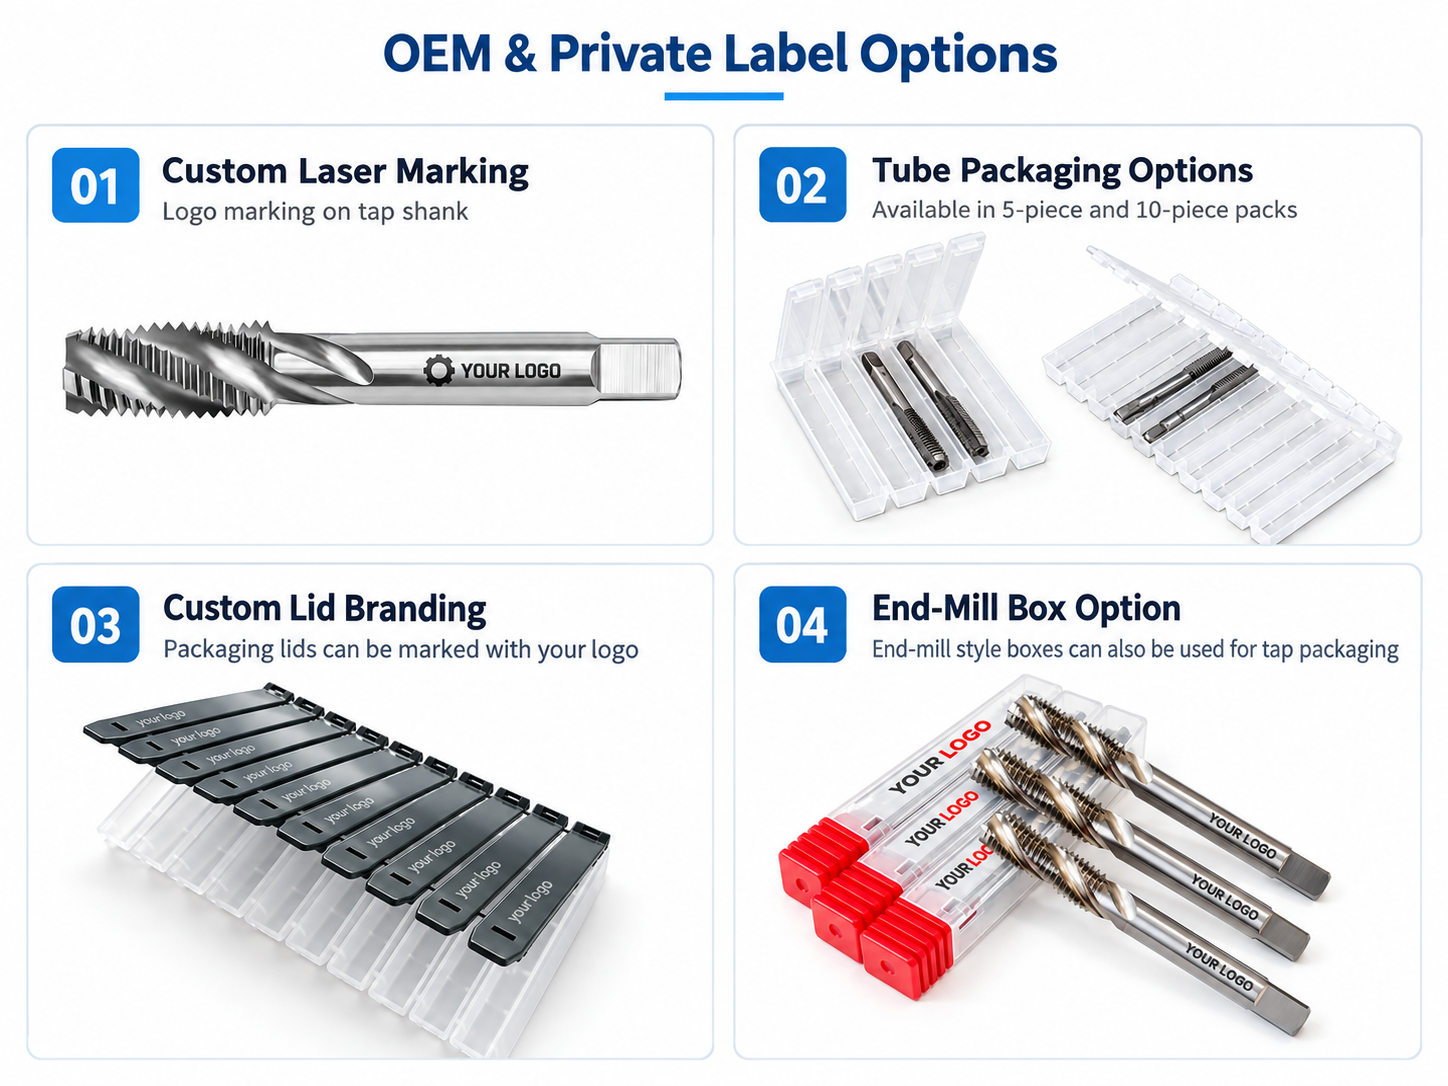
Marking depends on shank space; packaging follows approved artwork.
For a quotation: Specify thread size, TPI, tolerance, material, hardness, hole type, full-thread depth and quantity. Include pre-hole dimensions and OEM requirements where applicable.
M35 Forming Tap Quality & Inspection
Material, UNC / UNF forming geometry, dimensions and TiN coating condition are checked against confirmed specifications.

Wichtige Prüfpunkte
- Material: M35 cobalt HSS and agreed hardness requirements.
- Thema: UNC / UNF designation, TPI, profile and tap limits.
- Geometrie: Forming lobes, chamfer, surface condition and specified runout.
- Abmessungen: Forming length, overall length, shank and drive square.
Die erforderlichen Berichte und die Validierung der Probenfäden werden vor der Bestellung vereinbart.
Packaging & Identification
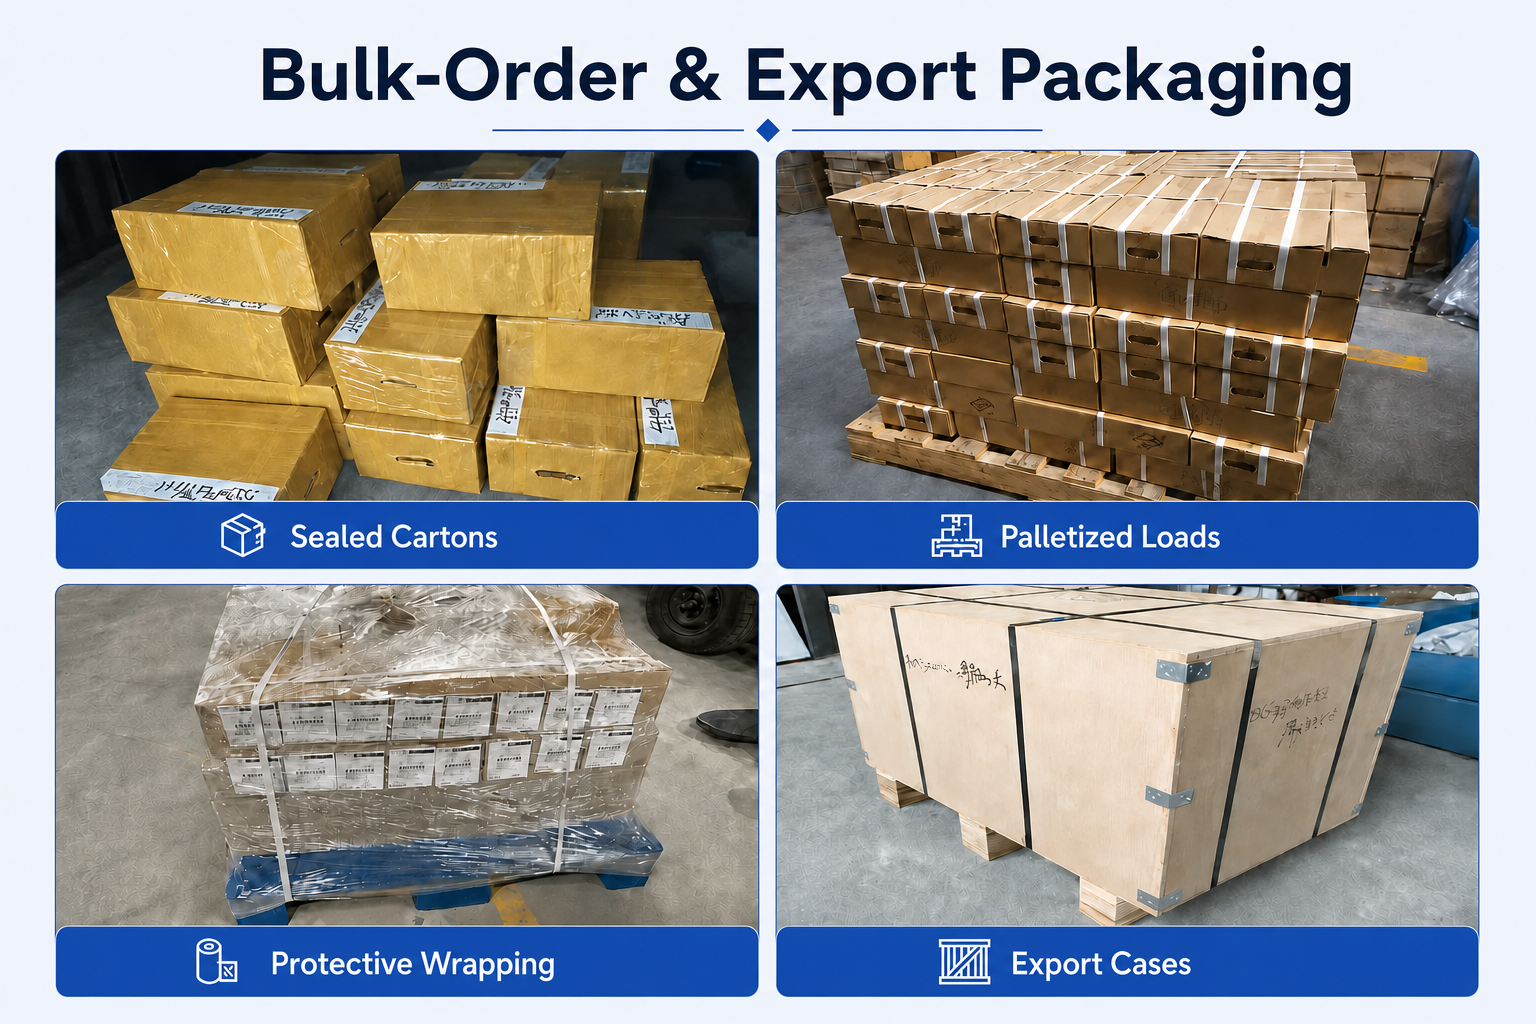
Individual protection helps prevent damage to forming surfaces. Labels identify thread size and order or batch references.

Lieferzeit und Exportversand
Standard-Wasserhähne: In der Regel 1–3 Werktage, vorbehaltlich der Verfügbarkeit.
Benutzerdefinierte Wasserhähne: Die Lieferzeit richtet sich nach den Spezifikationen, der Beschichtung und der Menge.
Die Exportverpackungs-, Fracht- und Zahlungsbedingungen werden bei der Bestellung bestätigt.

UNC & UNF Thread Forming Tap FAQs
Are thread forming taps, roll taps and fluteless taps the same?
Should I choose a forming tap or cutting tap for UNC / UNF threads?
Which UNC and UNF roll tap sizes are listed?
How do I select the drill size for a UNC or UNF forming tap?
Can M35 forming taps be used for aluminum, steel and stainless steel?
Can the same forming tap work in blind and through holes?
Do TiN-coated M35 roll taps still need lubrication?
Custom Roll Taps & Distributor Supply
Can UNC / UNF forming taps be customized for OEM orders?
Are sample and mixed-size forming tap orders available?
What details are needed for wholesale pricing and tool selection?
Katalog und Auswahlressourcen aufrufen
Benötigen Sie Informationen zu Größen, Preisen oder individuellen Optionen?
Senden Sie uns Ihre Spezifikationen und die gewünschte Menge, damit wir Ihnen ein Angebot unterbreiten können.
- Standardgrößen
- Kleine Probestellungen
- Verschiedene Größen
- OEM & Sonderanfertigungen
QR-Code anzeigen – Vertrieb über WeChat kontaktieren
Scannen Sie den QR-Code, um uns über WeChat zu kontaktieren.
Scannen Sie den QR-Code, um uns über WeChat zu kontaktieren.