
Deep-Hole Drilling in 20CrMoH: A Transmission Shaft Customer Case
Customer case · Custom carbide drills · Transmission shaft machining
Deep-hole drilling in 20CrMoH was the requirement for this transmission shaft project. The customer needed a drill for a blind hole, with particular attention to chip removal as drilling progressed.
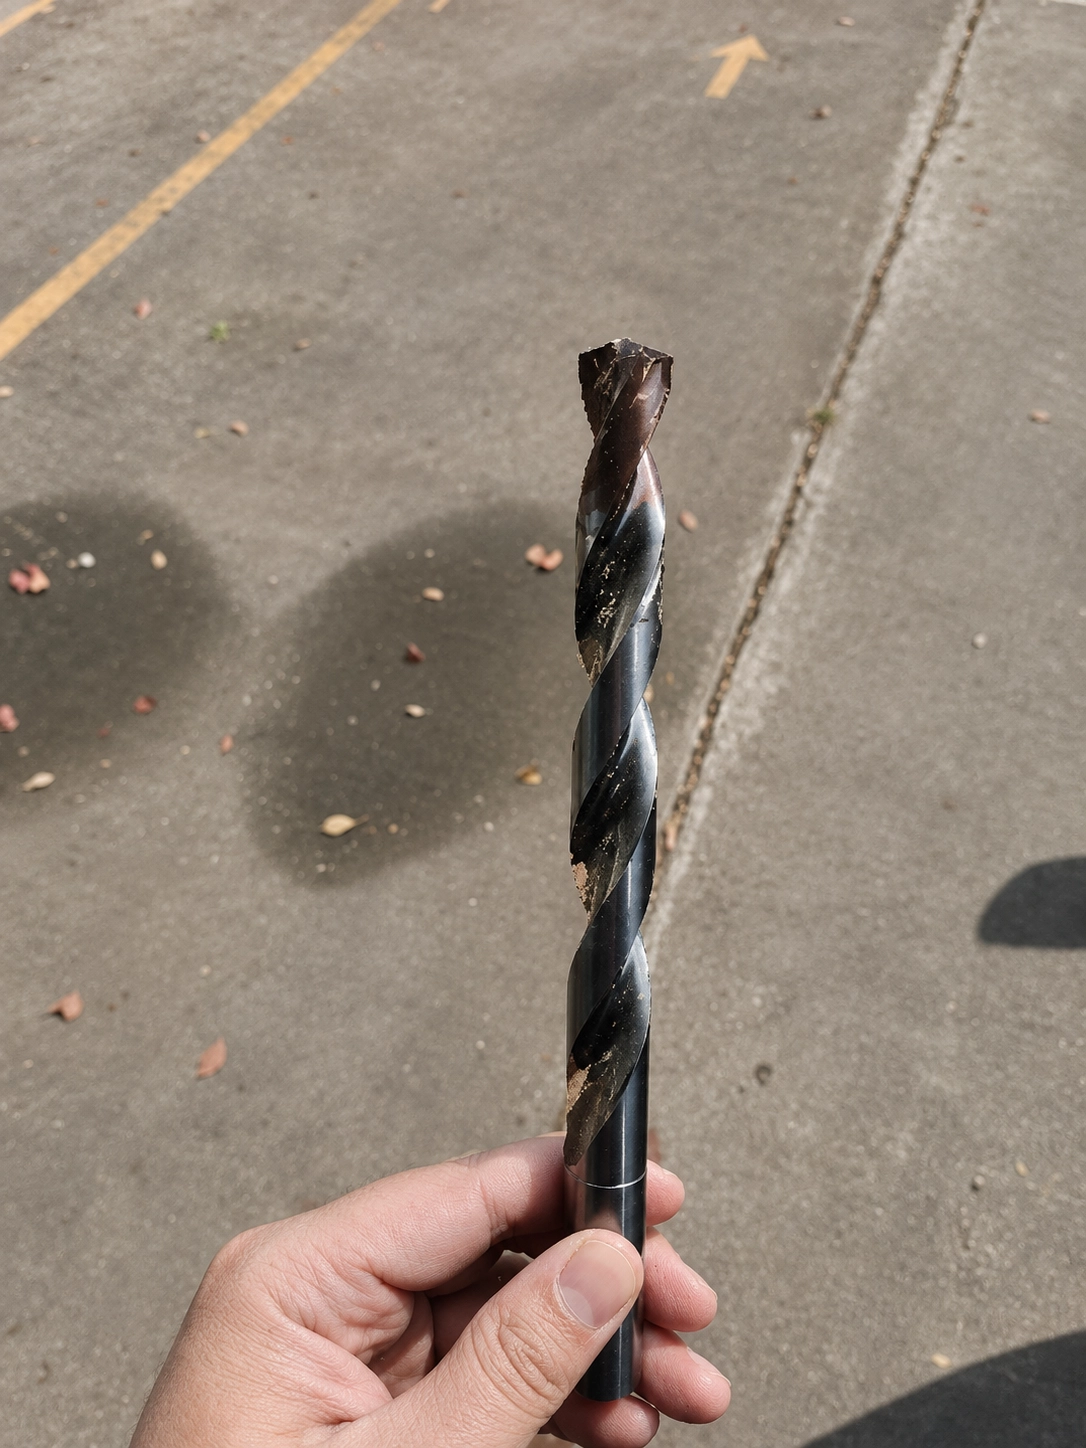
We supplied a custom through-coolant solid carbide drill for the application. The tool drawing, cutting-end detail and customer photographs are shown below, including the long drill after use.
If you are sourcing a similar drill, start with the required hole depth, access around the component and coolant supply available on the machine. These details help determine which tool configuration to review.
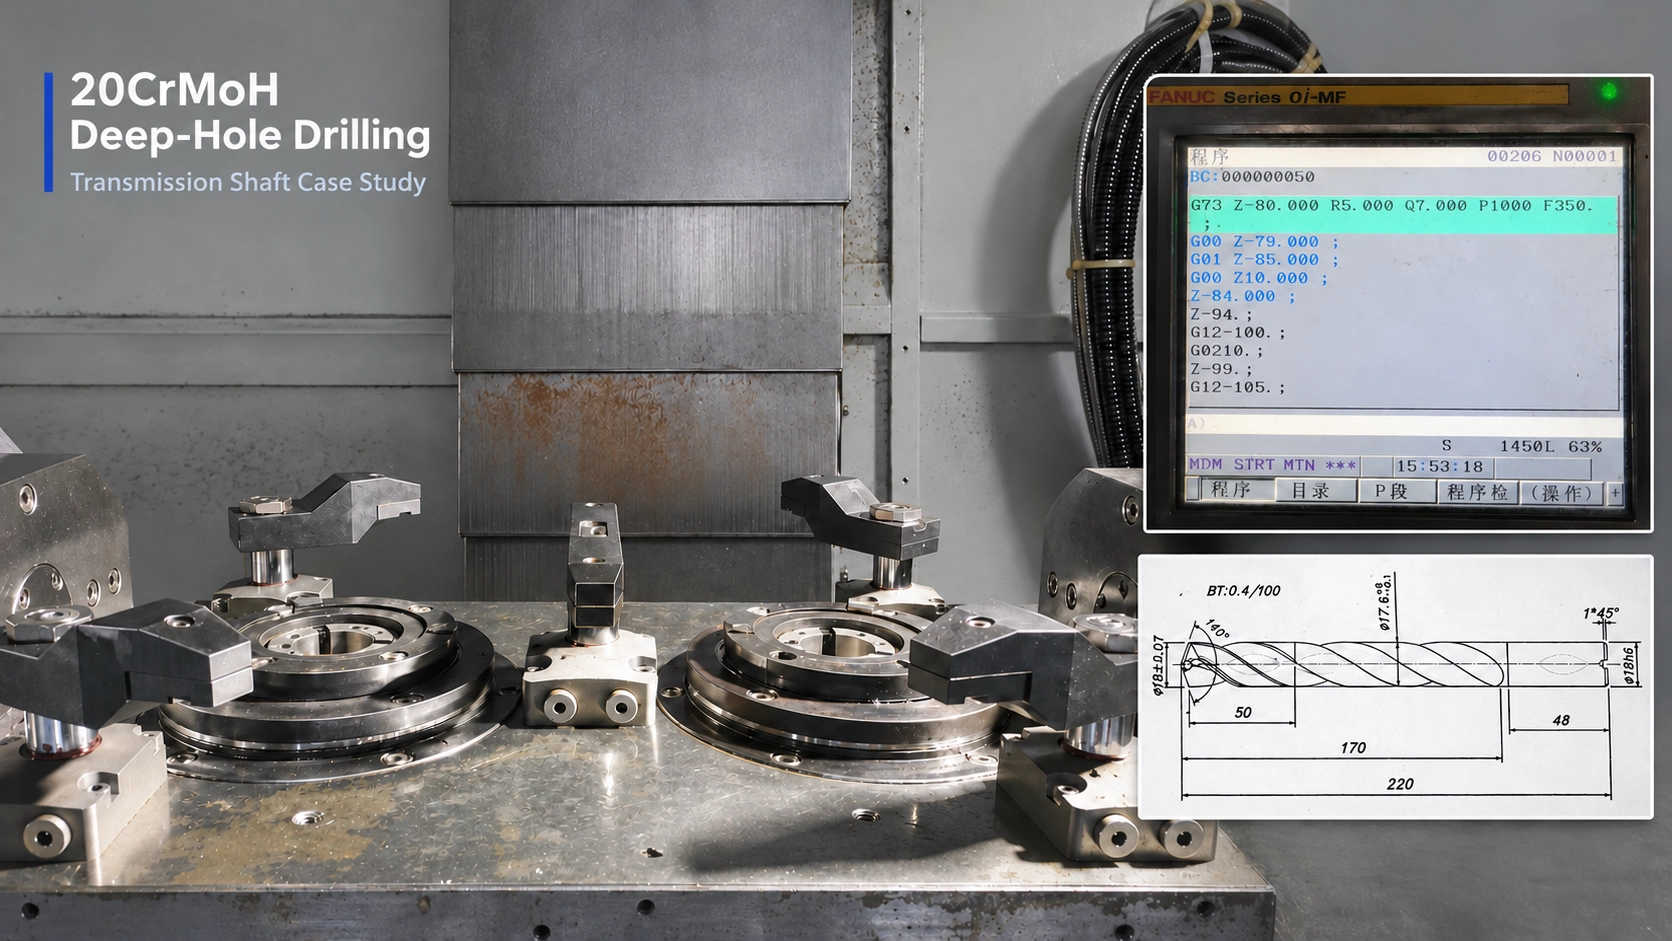
Case at a Glance
01 / APPLICATION
20CrMoH transmission shaft
Deep blind-hole drilling in an alloy-steel component.
02 / TOOLING
Custom through-coolant drill
Solid carbide construction with internal coolant outlets.
03 / FOCUS
Reach, chips and coolant
Tool dimensions considered alongside the machine setup.
Contents
Deep-Hole Drilling in 20CrMoH: The Customer’s Requirement
The aim was to reach the required depth and keep chips moving back out of the blind hole. The drill’s working length, flute space and coolant supply all needed consideration.
In blind-hole drilling, chips must return toward the entrance through the flutes. Long or congested chips can interfere with that movement. Chip formation, flute geometry, cutting conditions and coolant supply therefore need to be considered together.
For a replacement, check the complete hole requirement and the tool as it sits in the holder. Overall length does not tell you how much usable drilling depth or clearance is available.
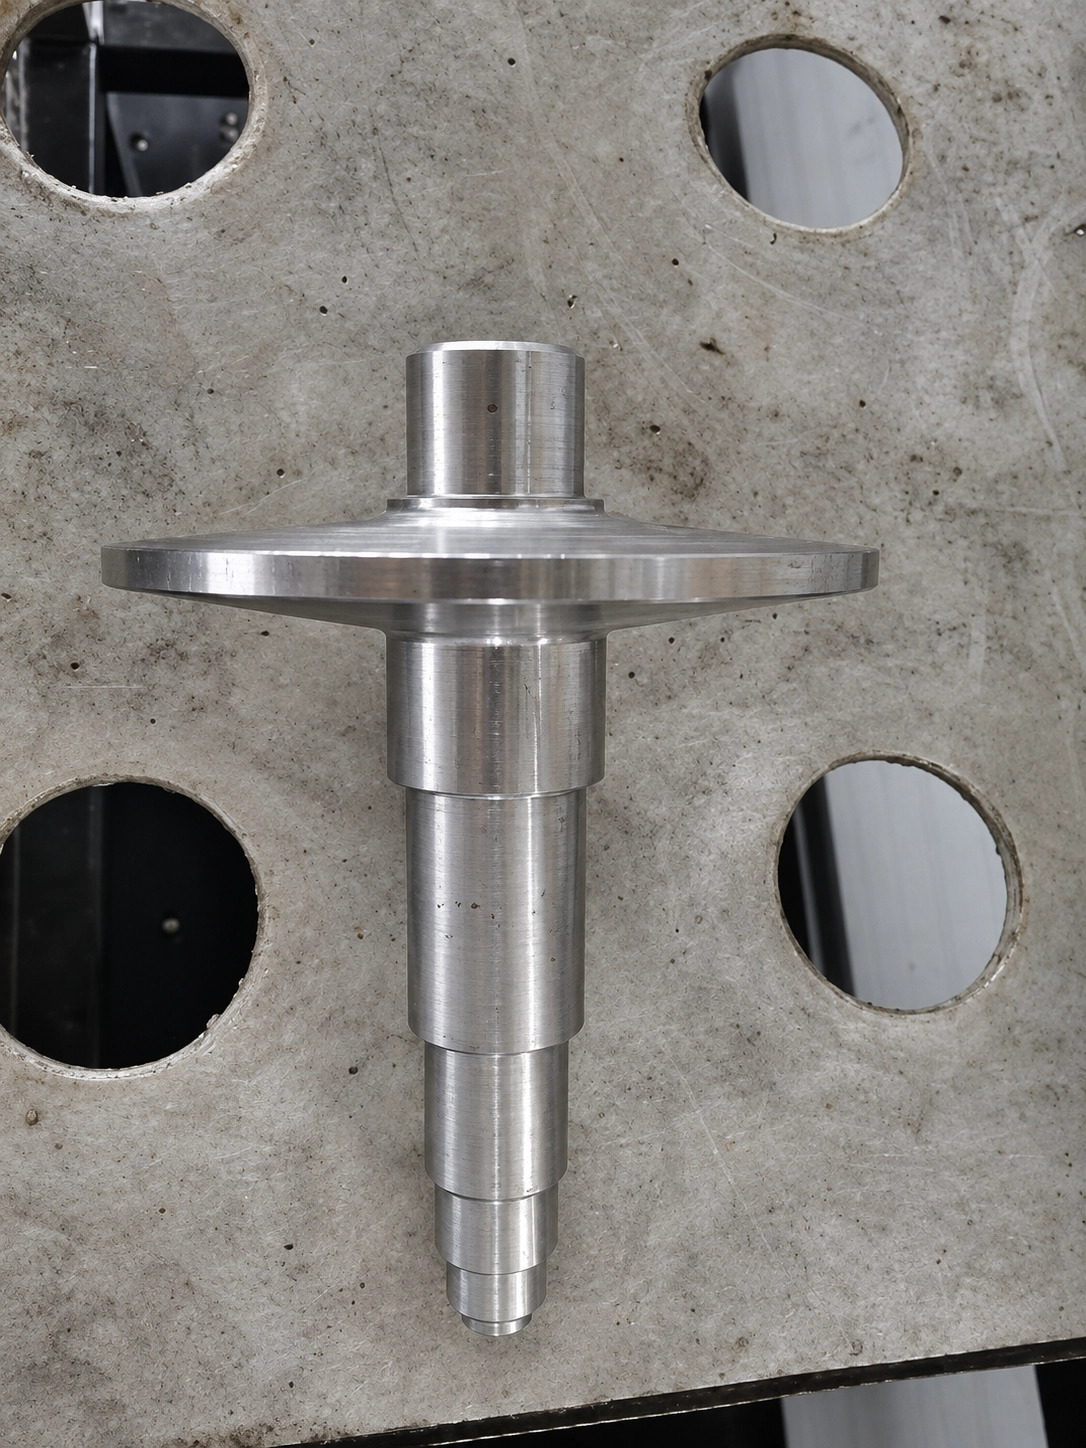
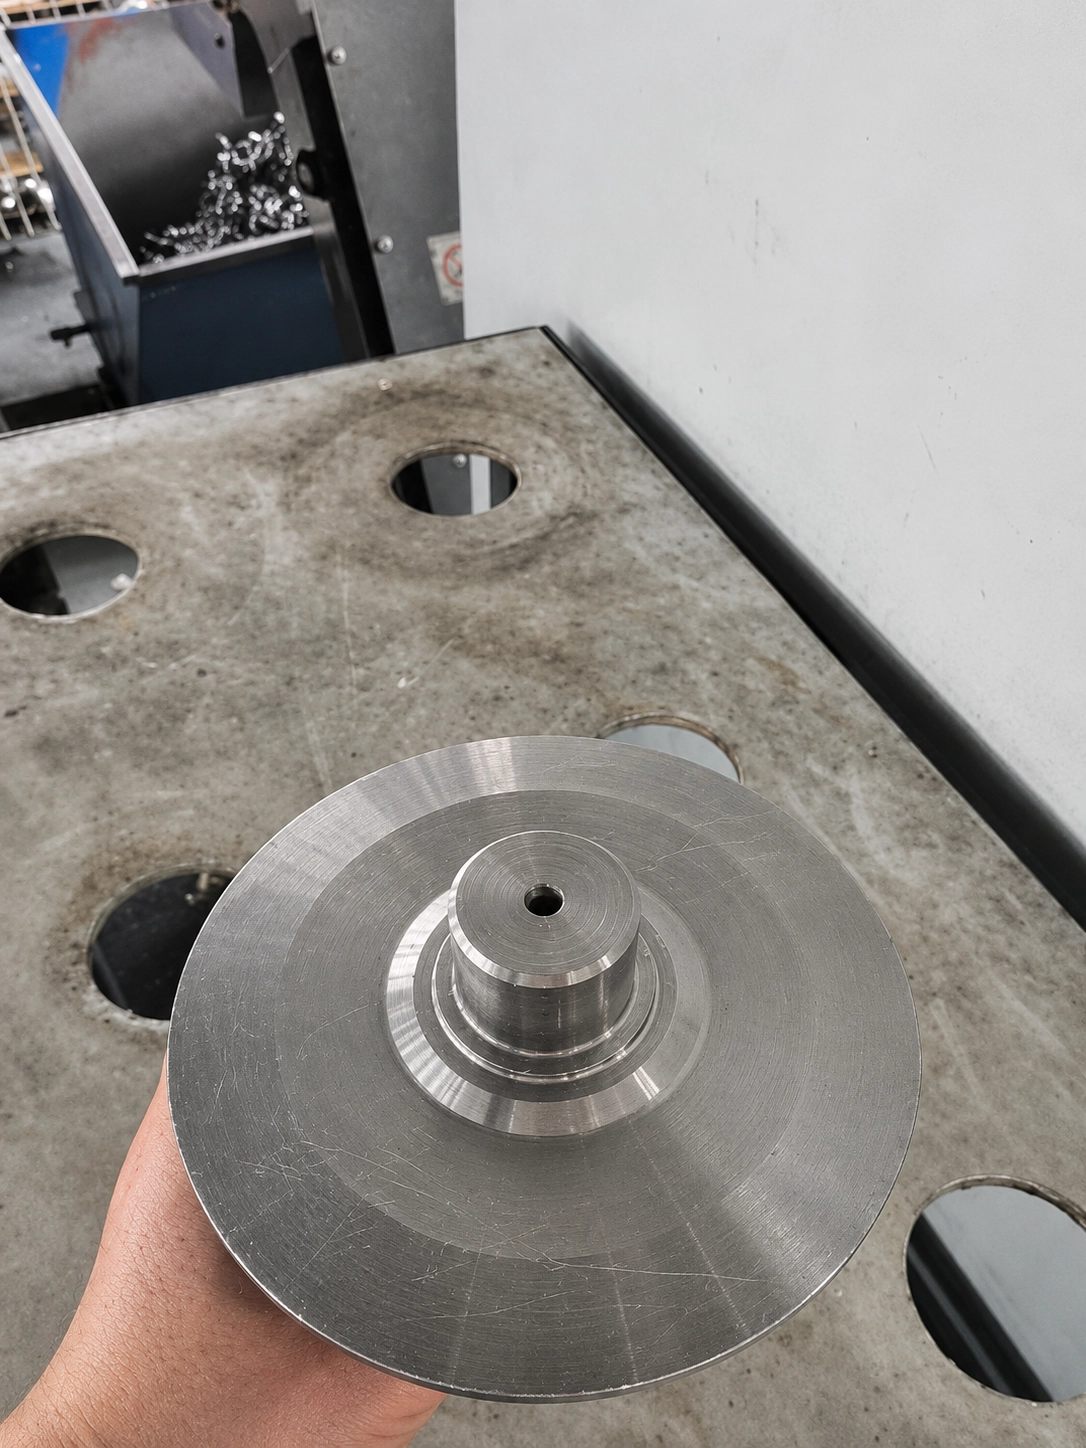
The Custom Through-Coolant Drill
The supplied solid carbide drill combines an extended helical-flute section with internal coolant outlets at the cutting end. The drawing records its dimensions; the close-up shows the point and outlets.

Three areas to review
Working length and access
Check flute length, usable reach, shank dimensions and projection from the holder. The shank and holder also need clearance around the component and fixture.
Coolant delivery
Through-tool passages bring cutting fluid toward the drill point to support cooling, lubrication and chip evacuation. Confirm that the machine and holder can supply coolant through the drill; include available pressure and flow if known.
Material condition
Tell us the material grade and its condition when drilled. If the part is heat-treated, include the hardness at this operation. This helps assess the carbide grade, geometry and coating.
The Drill in the Customer’s Workshop
The customer shared photographs of the machine and workholding arrangement for this project. The setup image shows the fixture layout and access area around the machining position.

Operating context
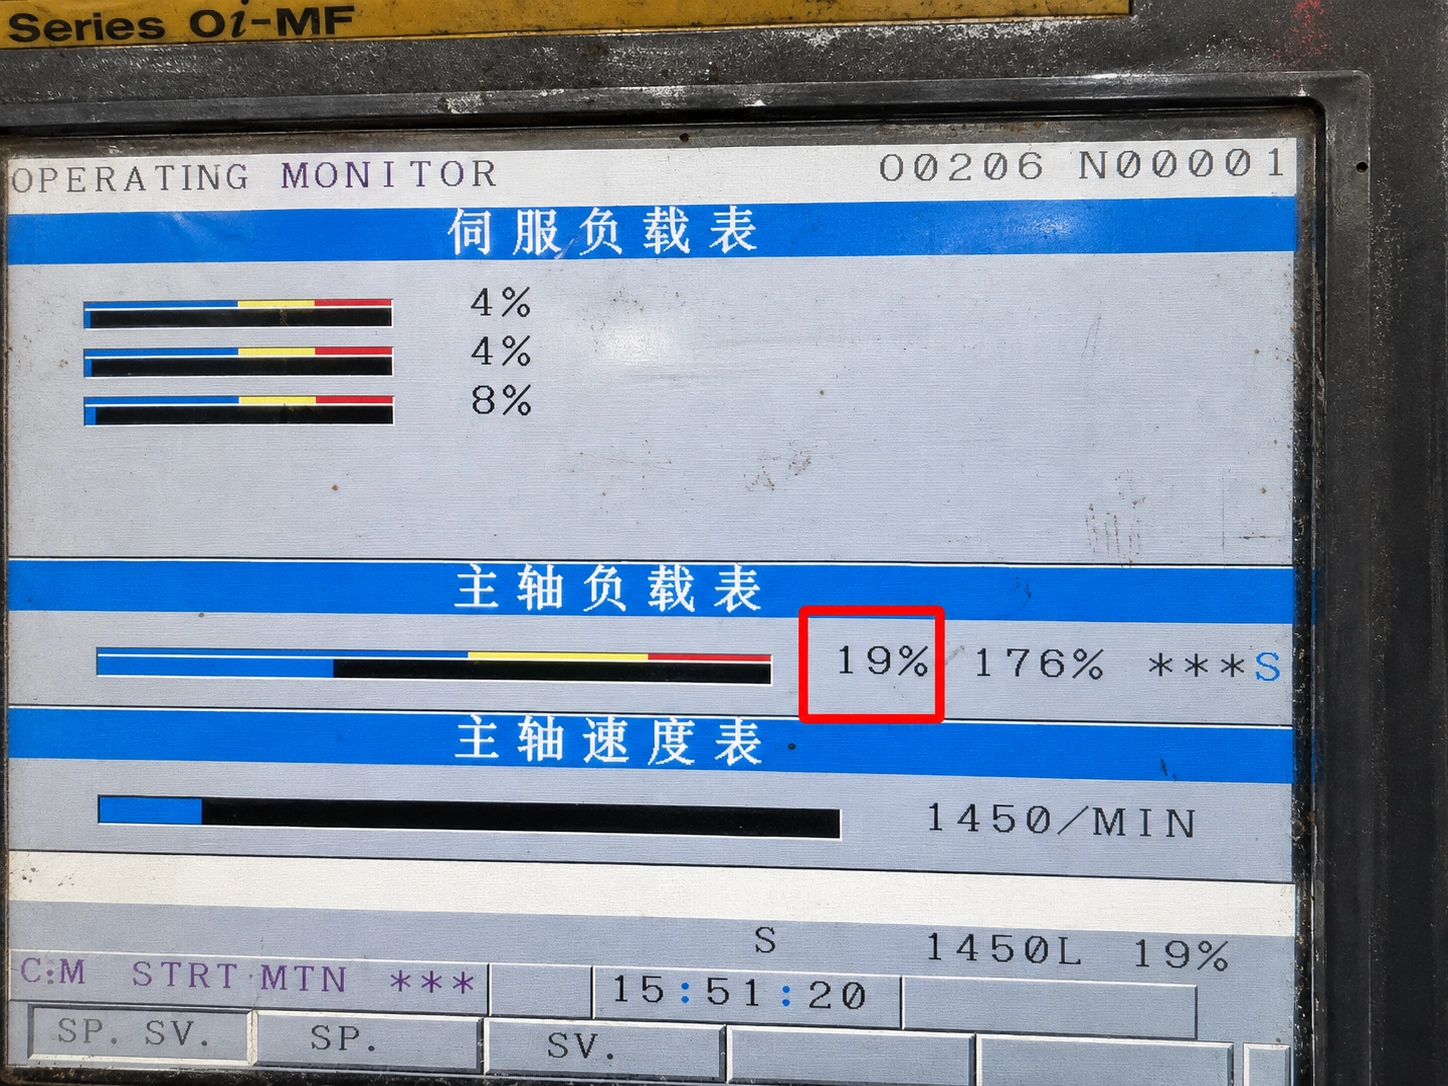
For a similar job, tell us at what depth chips begin to collect, the load changes or the cutting sound becomes different. Link any controller screenshots to that drilling stage, and include a photograph of the tool and chips if available. This gives us more to work with than a report that the drill “does not run well.”

Customer photographs after machining
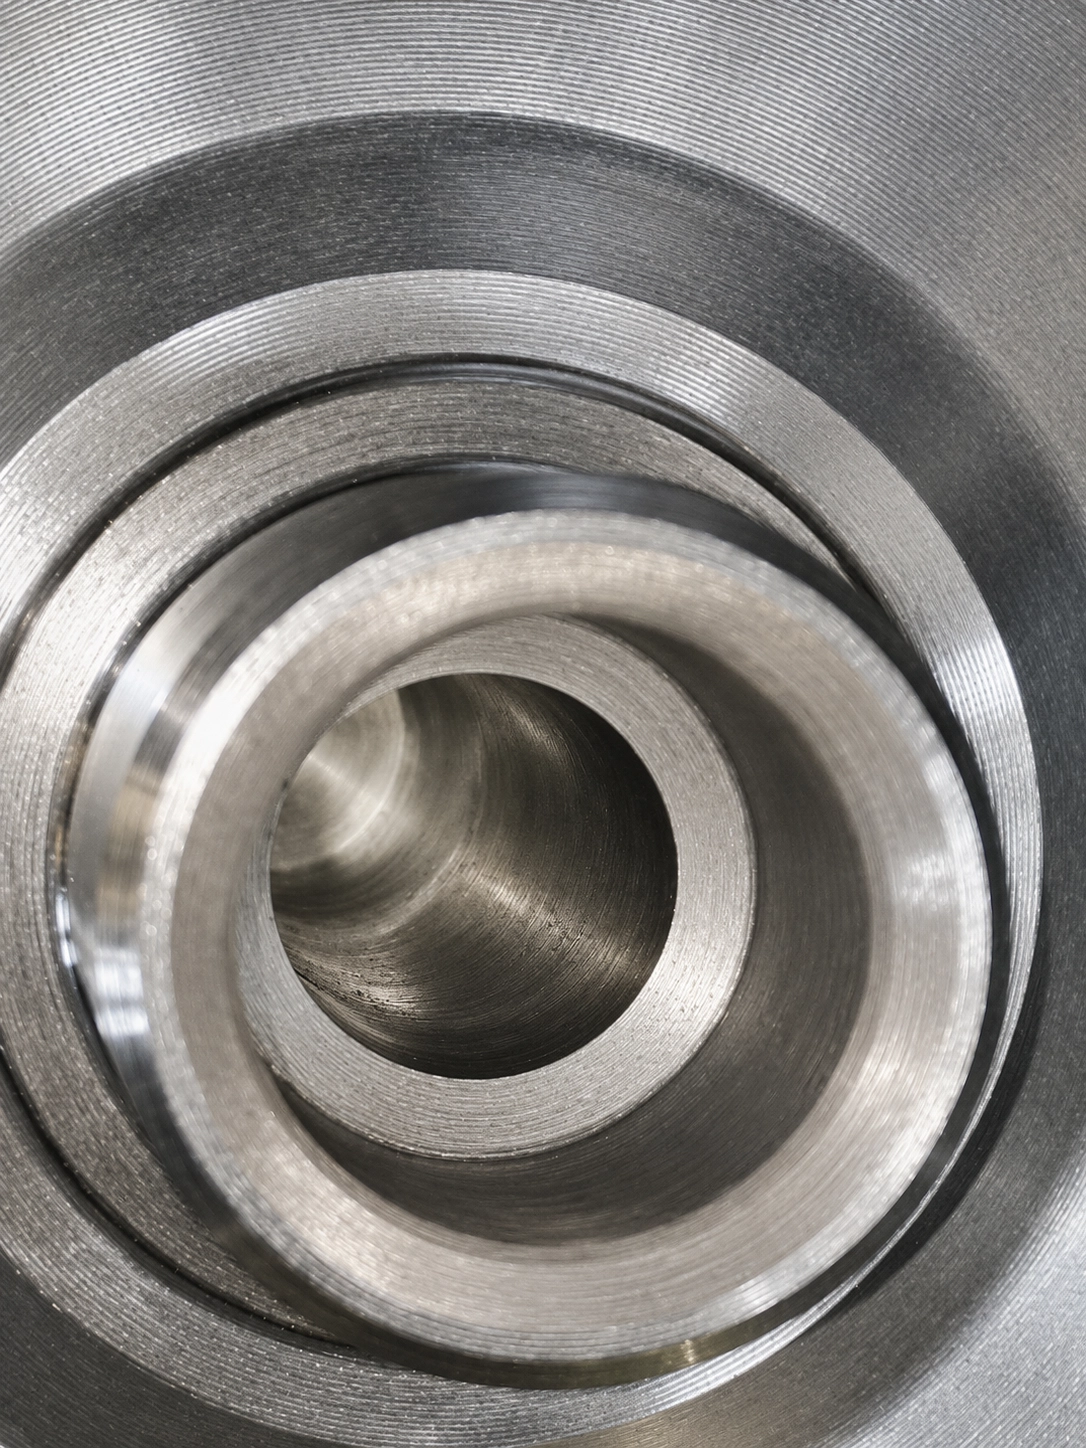
The customer sent the long-drill photograph after using the tool. It is shown alongside the internal view of the machined bore, so the tool condition and hole surface can be discussed together.
For a new trial, agree on the required hole checks before running the tool. Depending on the part drawing, these may include diameter, depth, position and surface finish. Keep the inspection results with the tool and setup photographs for follow-up.
What This Case Means for a Similar Project
For a similar deep-hole drilling in 20CrMoH project, compare the hole dimensions, material hardness and machine setup before choosing the drill. A similar-looking shaft may still require a different working length, coolant arrangement or cutting geometry.
Chips are difficult to remove
Send chip photographs and explain at what depth the problem appears.
The drill needs more reach
Mark the obstruction or clearance requirement on a section drawing.
The existing tool is unavailable
Provide its drawing or sample alongside the required hole details.
You do not need every technical detail before contacting us. Start with the information below, and we can discuss what else is needed.
- Part drawing, hole diameter and depth.
- Material and hardness, if known.
- Existing drill drawing, sample or photographs.
- Machine, holder and coolant arrangement.
- Problem to address and required quantity.
Questions About Similar Custom Drills
Could a standard drill work for my hole?
A standard through-coolant drill may be suitable if its usable drilling depth, cutting geometry and material range match the application. Custom tooling can be reviewed when dimensions or access requirements fall outside the standard options. Send the hole drawing and existing tool details so we can compare suitable configurations.
I only have the old drill. Can you work from it?
Yes. HY Cutting Tools can review an existing tool or physical sample when a complete drawing is unavailable. Key dimensions and application requirements are confirmed before a custom sample is prepared.
Can I order the same drill with a different length or shank?
Custom lengths and shank configurations can be reviewed. Send the dimensions that must remain fixed, together with the hole requirement and available holder clearance.
Can we test a small quantity first?
Yes. Tell us how many tools you would like for the trial. We will confirm the minimum quantity for the proposed design when quoting.
Will our part drawing remain confidential?
Yes. Customer drawings, specifications and custom-tool information are treated as confidential and used for quotation, production and quality control. Additional confidentiality requirements can also be discussed.
Discuss Your Deep-Hole Drilling Application
Need tooling for deep-hole drilling in 20CrMoH? Send us the part drawing, required hole dimensions and any existing drill details. Chip photographs and setup information can also help us review the application.
HY Cutting Tools can review the application and discuss suitable standard or custom through-coolant drilling options.