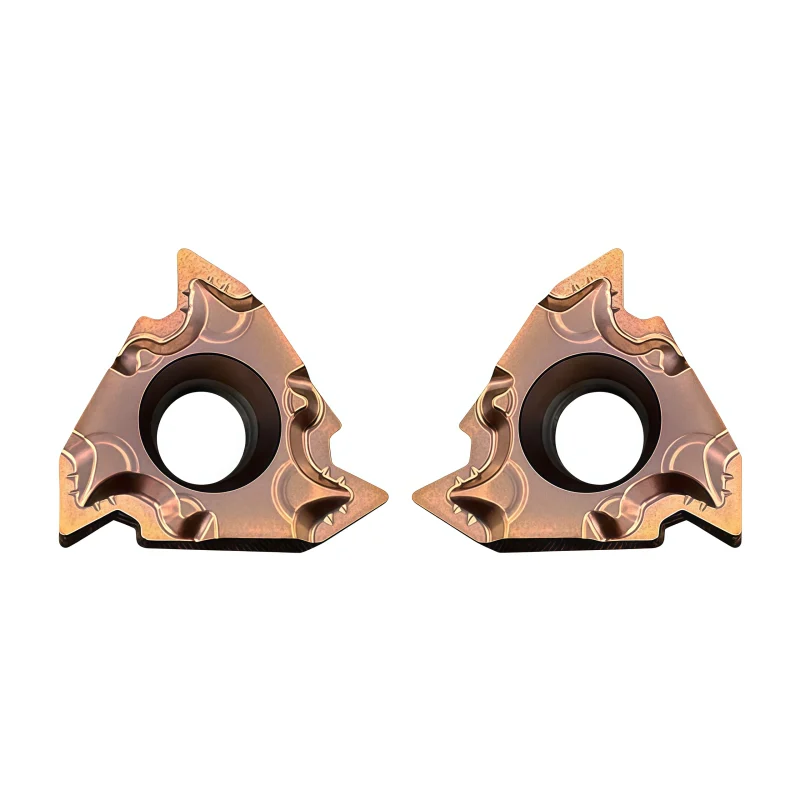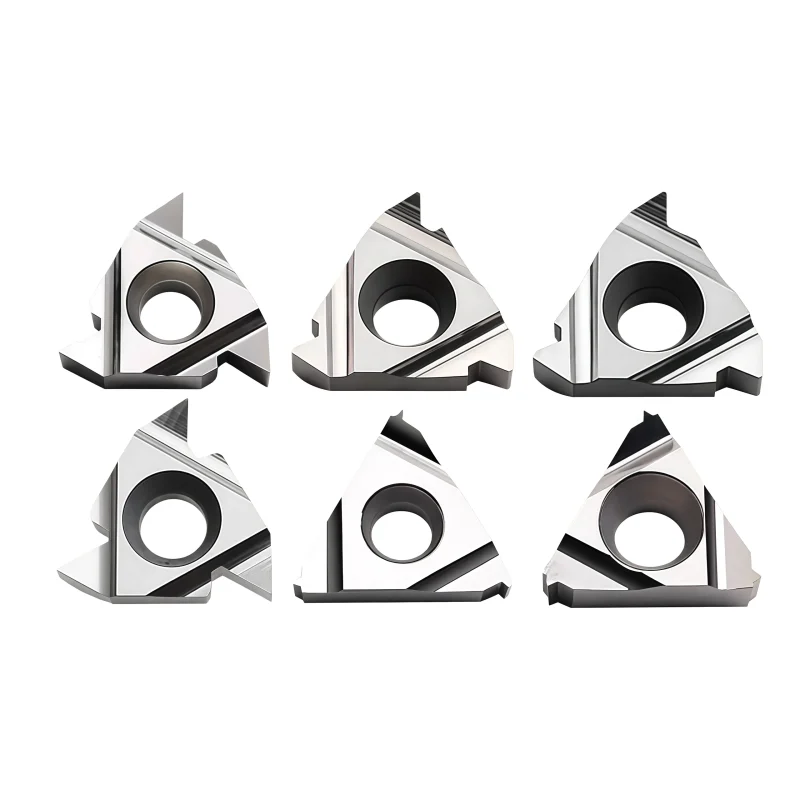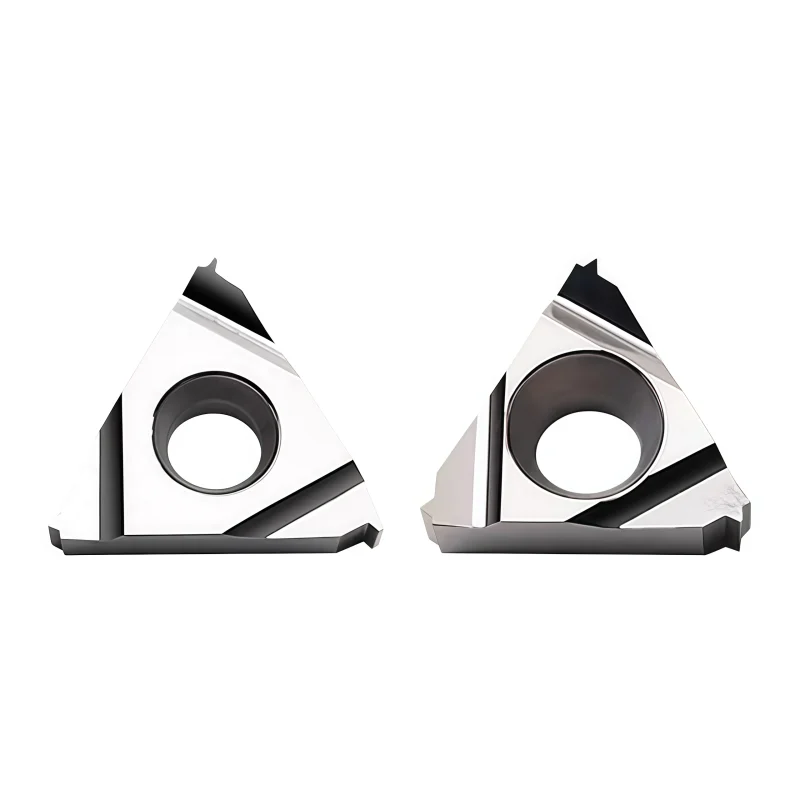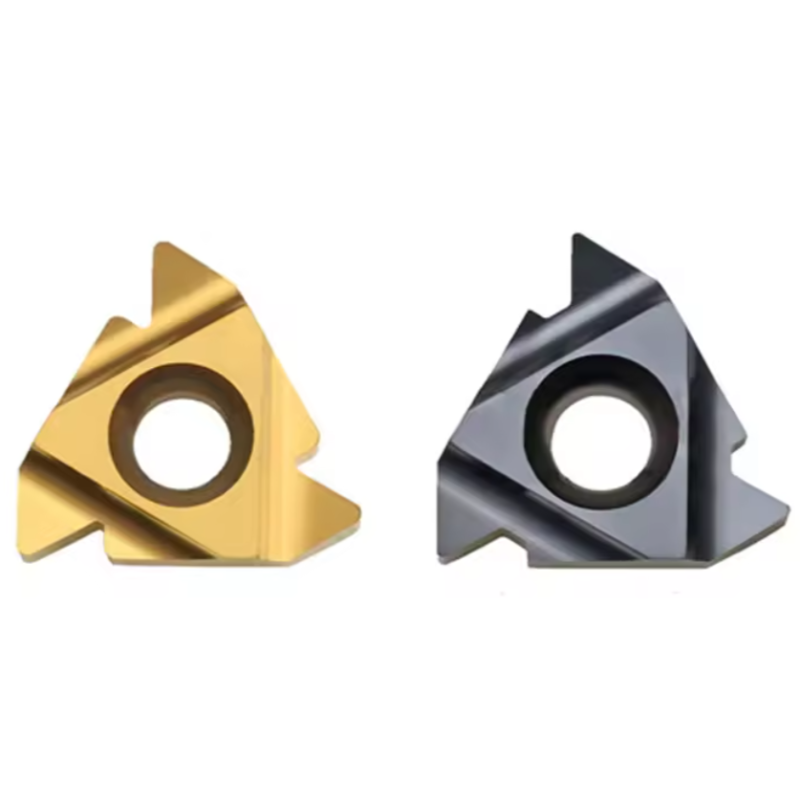
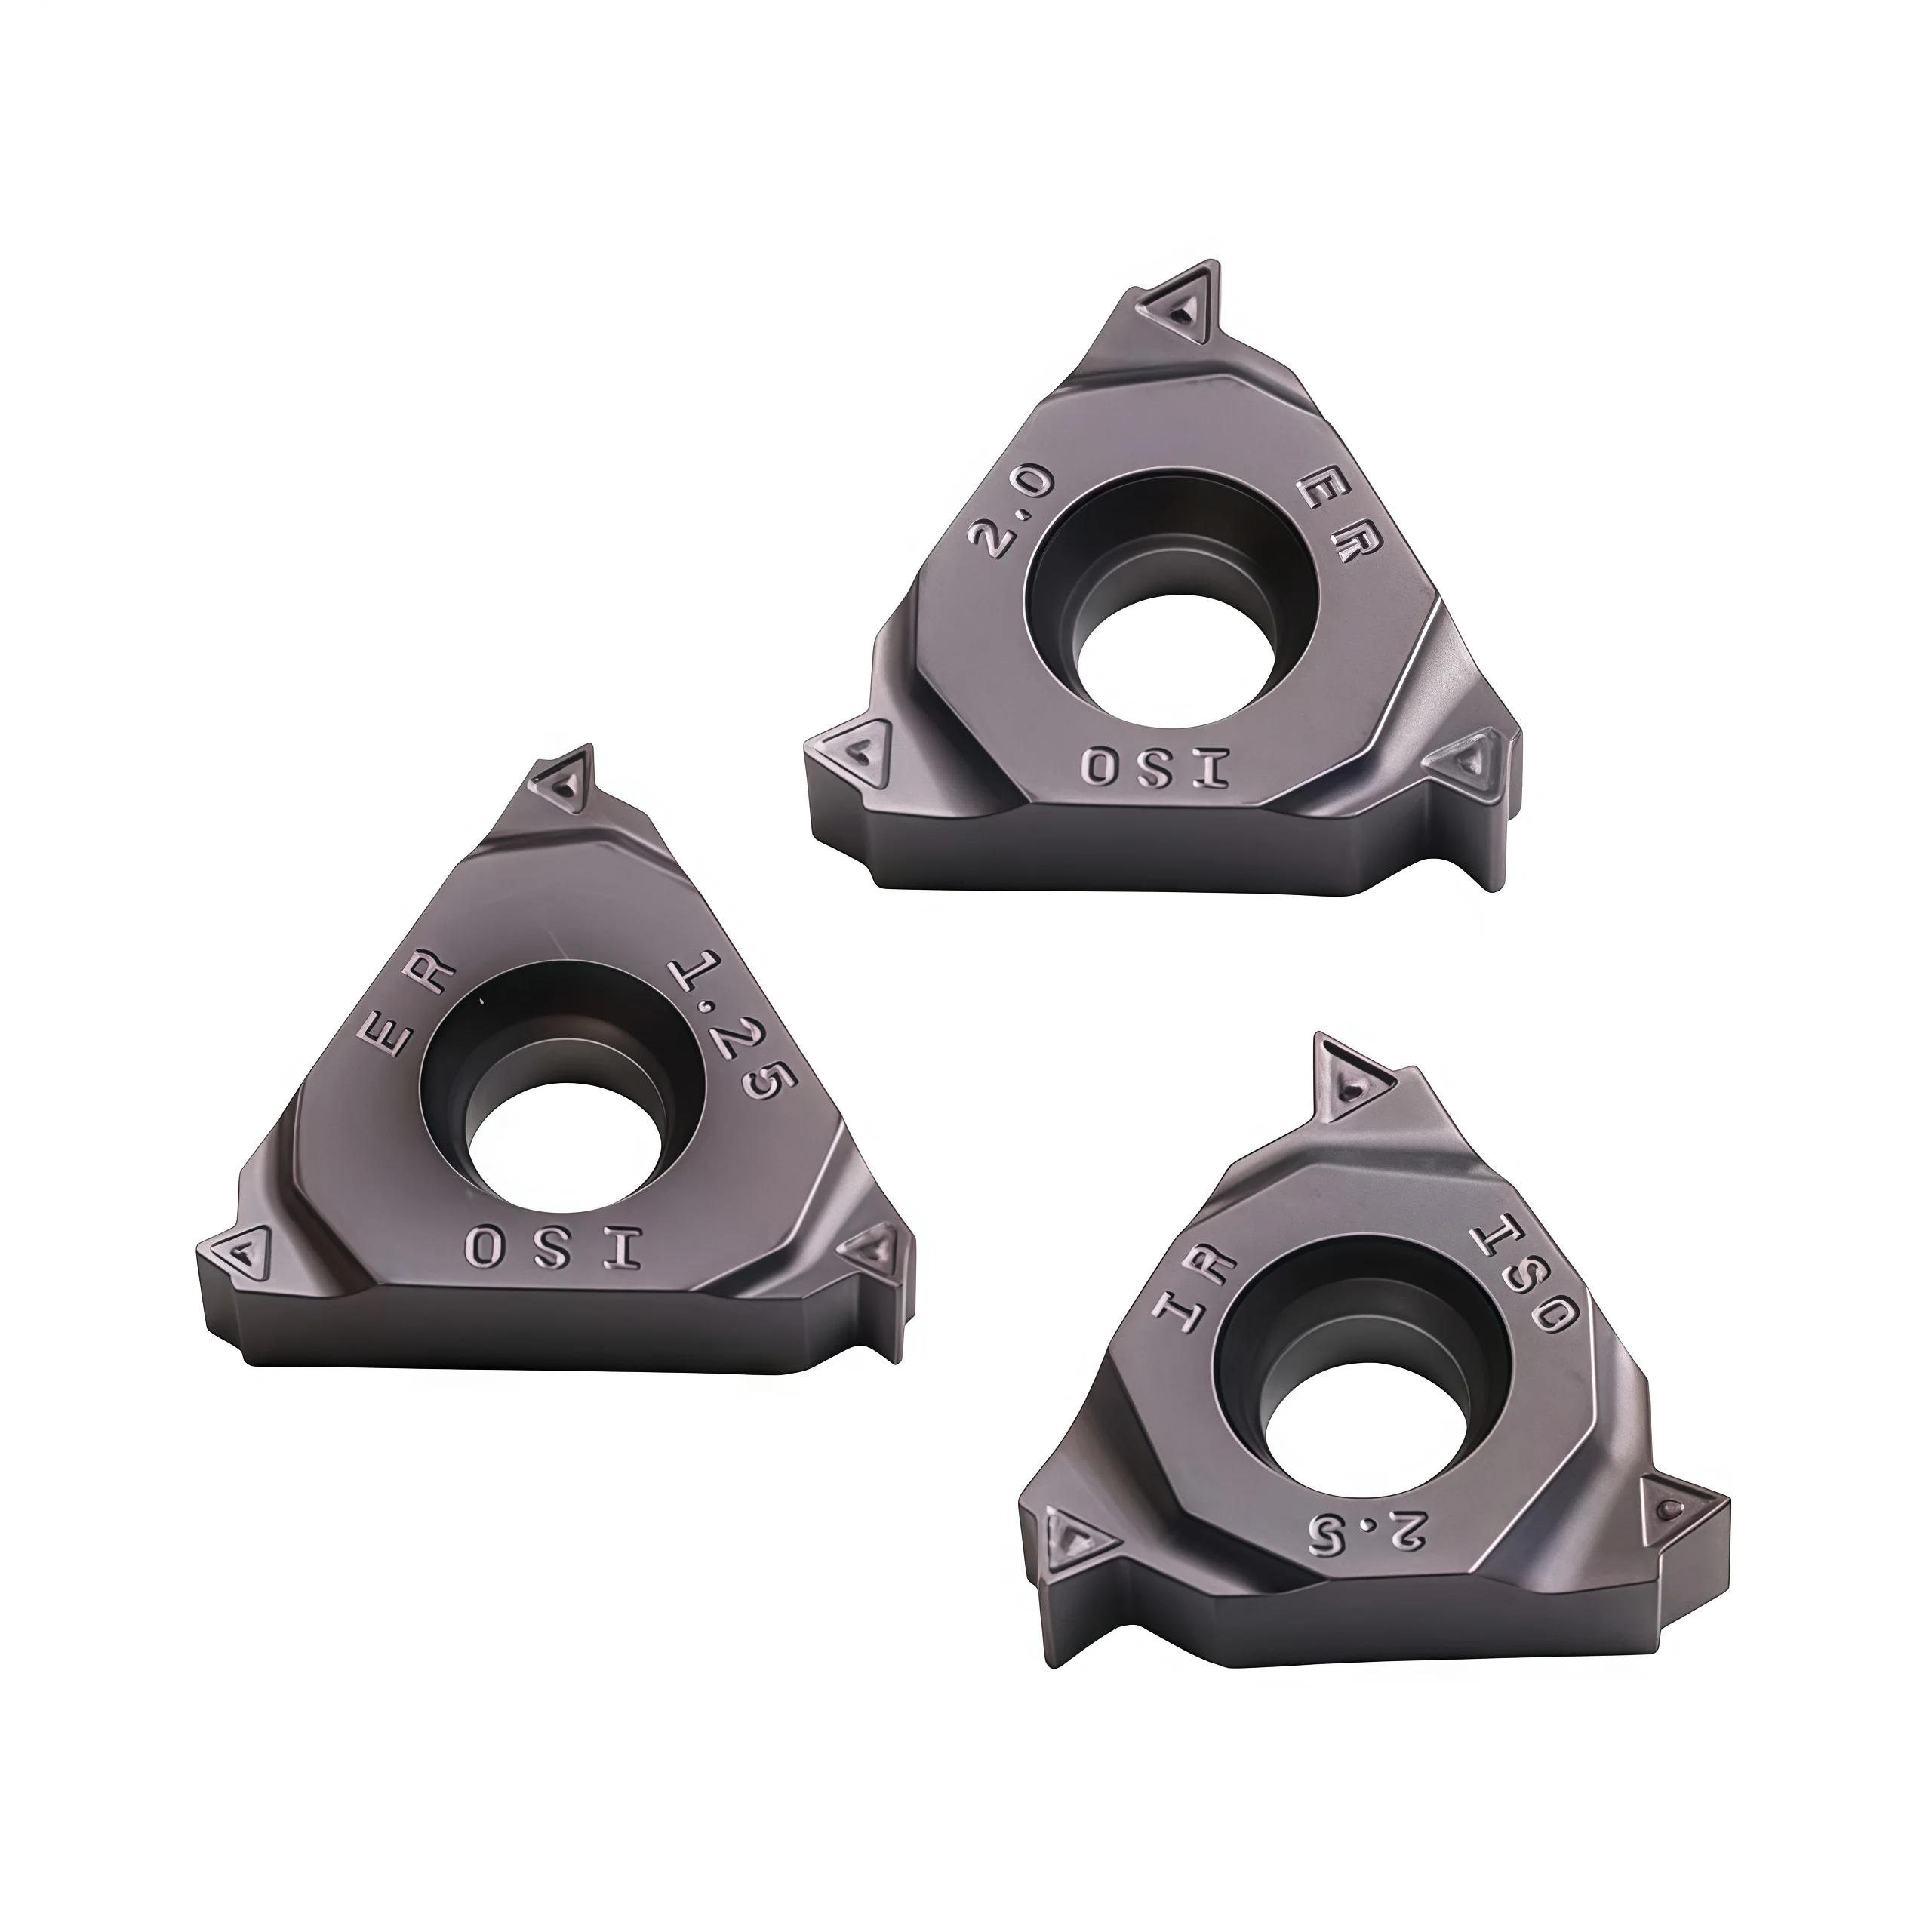



16IR/16ER ISO Carbide Threading Inserts for Metric Threads
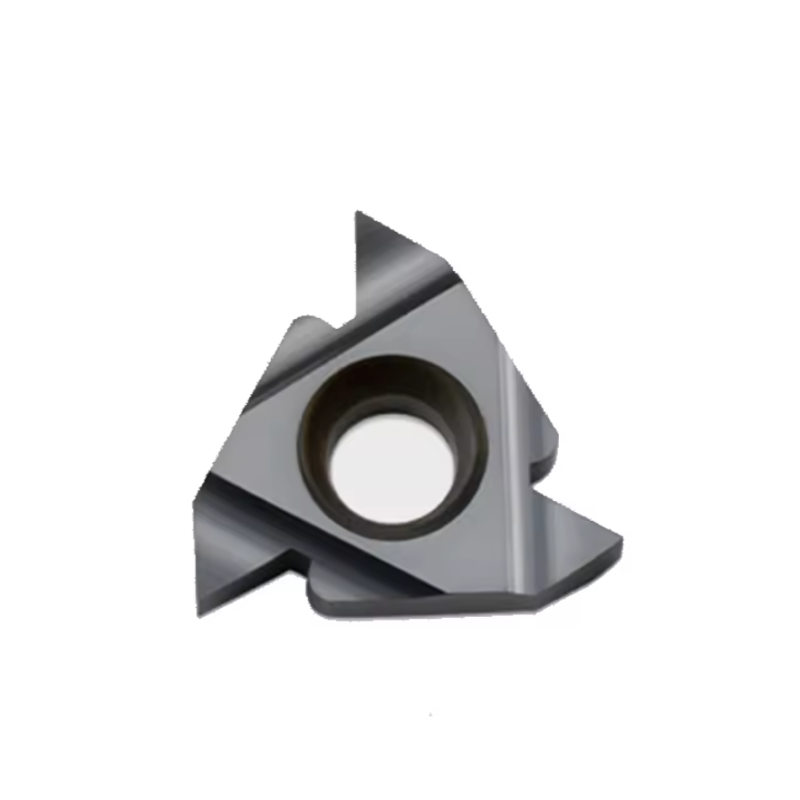
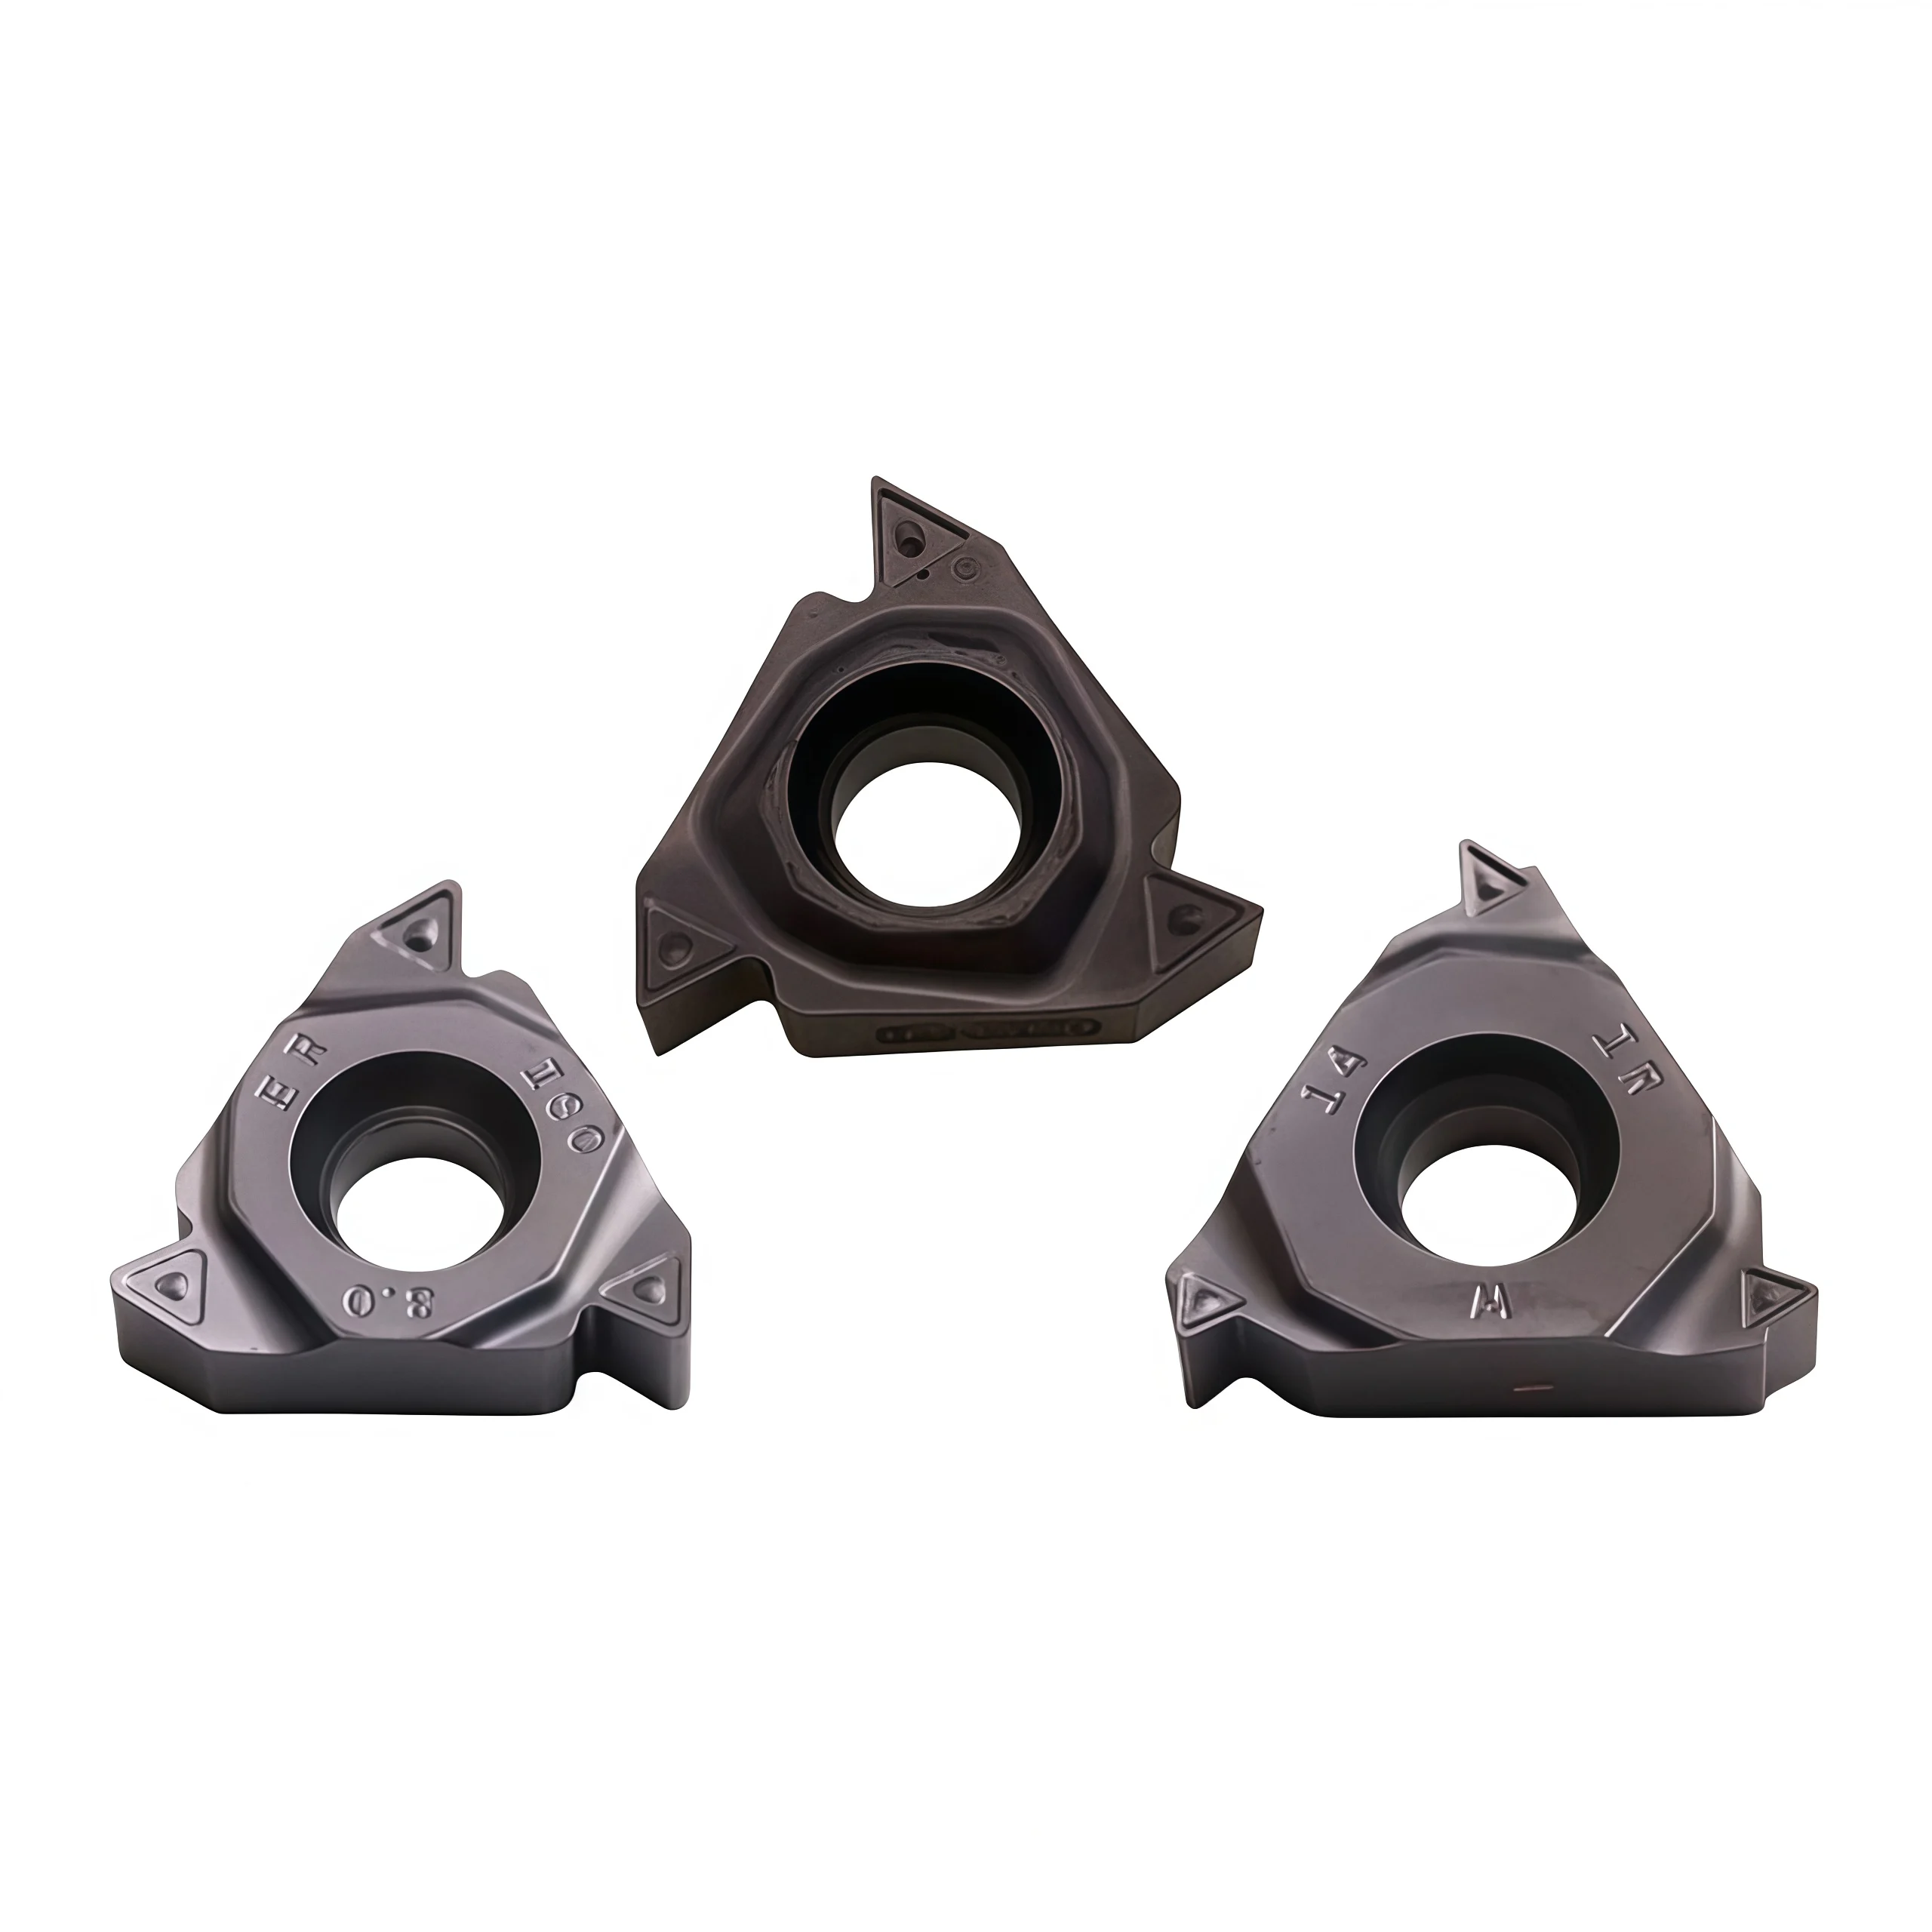
16IR and 16ER ISO carbide threading inserts provide a practical range for internal and external metric thread machining. Multiple pitch and grade options allow distributors to cover common customer requirements for steel, stainless steel and other grade-dependent materials. Precision profiles support consistent thread dimensions, surface quality and repeat-order interchangeability.
جودة متسقة
Consistent geometry across repeat orders.
الطلبات المرنة
Small batches and mixed sizes available.
OEM Support
Custom marking, labels and packaging.
قياسي ومخصص
Standard sizes and custom configurations.
◆16IR/16ER ISO Carbide Threading Inserts Overview
إن 16IR / 16ER ISO carbide threading insert range covers internal and external turning of 60° metric threads. The existing product information lists pitch-specific 1.0, 2.0 and 3.0 mm options. Select the complete full-profile insert designation for the required M or MF thread pitch; the cutting edge then forms the corresponding thread profile, including the crest when the blank diameter leaves suitable stock.
For steel, stainless steel or cast iron, match the verified carbide grade and coating to the workpiece and cutting conditions. Holder fit, insert hand, bore clearance for 16IR, infeed strategy and thread gauging all affect the finished result. Request the selected HY insert drawing and grade-specific cutting data before production.
◆Key Configurations
| Configuration | Selection Point |
|---|---|
| 16IR / 16ER | Internal / external thread turning; use the corresponding holder and check its hand. |
| Metric ISO profile | 60° pitch-specific full-profile option; confirm the complete M or MF thread designation. |
| Listed pitches | P = 1.0 / 2.0 / 3.0 mm in the existing description; confirm available 16IR and 16ER codes separately. |
| Grade / coating | Confirm by full item code. “AG55/60A” in the old copy does not establish an HY carbide grade or coating. |
◆Application Considerations
Pitch-specific crest: a verified ISO full-profile edge forms the thread crest for its stated pitch; leave suitable stock at the starting diameter.
Internal access: for 16IR, confirm minimum bore, boring-bar overhang, chip clearance and runout at the tool.
Material selection: choose a documented carbide grade and edge geometry for the exact steel, stainless or cast-iron workpiece.
Process control: use synchronized pitch feed, multiple infeed passes, an appropriate holder/shim setup and the specified thread gauge.
◆Original Product Images


◆Application & Ordering
Send the M or MF thread designation, pitch and tolerance, internal/external location, holder model, workpiece grade, thread diameter and length, required grade/coating and quantity. We can confirm the matching insert code, dimensions and availability.
See our CNC Insert Selection Guide or send an inquiry.
◆Specifications & Sizes
The original page lists 1.0, 2.0 and 3.0 mm pitches for 16IR/16ER ISO metric threading. It does not provide a verified HY size drawing or separate item codes for every combination. Confirm the exact configuration, insert dimensions, grade and holder before ordering.
| المعلمة | Specification / Confirmation |
|---|---|
| Insert family | 16IR internal / 16ER external carbide threading inserts; “16” refers to the insert-size family. |
| Thread form | 60° metric ISO, M or MF according to the workpiece drawing; pitch-specific full profile where confirmed by the complete code. |
| Pitches in source | P = 1.0 / 2.0 / 3.0 mm; verify each IR and ER stock code and grade individually. |
| Tool material | Carbide; request the actual grade, coating and edge preparation for the selected model. |
| Workpiece groups | Steel (ISO P), stainless steel (ISO M) or cast iron (ISO K), subject to the selected grade's application data. |
| Holder fit | Match insert pocket, clamp, right/left hand and shim/anvil; confirm minimum bore and bar clearance for 16IR. |
| Finished thread | Nominal diameter, pitch, tolerance class and inspection gauge are specified by the customer drawing. |
◆Pitch Selection
| Pitch option | Full-profile insert check | Single-start axial feed |
|---|---|---|
| 1.0 mm | Confirm 16IR or 16ER 1.0 ISO and crest geometry. | 1.0 mm/rev |
| 2.0 mm | Confirm 16IR or 16ER 2.0 ISO and crest geometry. | 2.0 mm/rev |
| 3.0 mm | Confirm 16IR or 16ER 3.0 ISO and crest geometry. | 3.0 mm/rev |
These feed values describe axial advance per spindle revolution for single-start threads. They are not radial depth of cut or cutting-speed recommendations. A full-profile edge typically reaches the final form over multiple infeed passes.
◆Cutting Data & Confirmation
Confirm the starting cutting speed, number of passes, infeed method, coolant and shim inclination from the exact carbide grade, workpiece, thread pitch and diameter. For internal threading, check bore clearance, bar rigidity and chip evacuation. Inspect the finished thread against the specified class and gauge.
For a model-specific size drawing and cutting data, send the insert designation, holder code and thread drawing.
◆Carbide Insert Customization & OEM
Specify the insert around the machining operation, workpiece and holder. We can review standard replacements, application-specific geometry and private-label requirements using your insert designation, drawing or sample. Available grades, coatings, dimensions and order quantities are confirmed for each requested series.
Geometry & Chip Control
Review chipbreaker, rake, cutting-edge preparation, nose radius and corner design for the operation and workpiece. Confirm holder compatibility before approving a modified geometry.
Substrate & Coating
Select an available carbide grade and coating for the workpiece material, cutting conditions and desired balance of wear resistance and edge toughness.
Dimensions & OEM
Review insert size, thickness, locating and clamping features, tolerances, laser marking and private-label packaging against the approved specification.
◆Customization Options
Use the fields below when sending an inquiry. The exact options depend on the insert family and are confirmed in the quotation or approved drawing.
| المواصفات | Details to Confirm |
|---|---|
| Insert Type | Turning, milling, threading, grooving or drilling insert; send the designation or drawing. |
| Size & Fit | Shape, size, thickness, inscribed circle or edge length, hole or clamping form, and holder model. |
| هندسة القطع | Chipbreaker, nose or corner radius, edge preparation, cutting direction and application-specific profile. |
| Grade & Coating | Workpiece group and grade, carbide substrate, coating system and wet or dry cutting conditions. |
| Tolerance & Inspection | Critical dimensions, profile requirements, inspection method and any required report. |
| OEM Presentation | Insert or box marking, label content, packaging format and quantity per pack. |
◆How to Request a Custom Insert

Send your insert requirements through our contact form or review our OEM and private-label service.
◆Carbide Insert Quality Control

Insert quality depends on the approved grade, geometry, coating and dimensional specification. We review the requirements at order confirmation and align the inspection scope with the insert series and any customer drawing. Share critical dimensions or documentation needs before production so they can be included in the agreed inspection plan.
01 · Incoming Material
Confirm the specified carbide grade or material documentation against the order requirements.
02 · In-Process Checks
Review dimensions and cutting-edge features during production against the approved specification.
03 · Final Inspection
Check the agreed dimensions, appearance, edge condition, coating identification and marking as applicable.
04 · Packing Review
Verify the item code, quantity, labels and protective packing against the approved order.
◆Inspection & Documentation
Inspection points and acceptance criteria should be agreed for the ordered series. For custom inserts, the approved drawing takes priority over a generic catalogue description.
| Check Area | What to Confirm |
|---|---|
| Dimensions & Fit | Insert size, thickness, corner radius, clamping features and any drawing tolerances. |
| هندسة القطع | Chipbreaker, edge preparation, usable corners and profile where applicable. |
| Grade & Coating | Approved grade and coating designation; any requested verification method. |
| Appearance & Packing | Visible edge damage, marking, item code, count and packing format. |
| Requested Records | Inspection report, material or coating documentation, sample approval or batch identification when agreed. |
◆Order & Delivery

Share a line-by-line list of insert codes and quantities for a mixed-size quotation. Stock status, minimum quantity, sample requirements and production lead time are confirmed for each grade, coating and configuration.
Send your item list and quality requirements through our contact form for specification, availability and delivery confirmation.
◆Product FAQs
What is the difference between 16IR and 16ER?
16IR is for internal thread turning and 16ER is for external thread turning. Check the corresponding holder, insert hand, clamping arrangement and shim. For 16IR, also verify the minimum bore and boring-bar clearance.
Which metric pitches are listed for this product?
The existing description lists 1.0, 2.0 and 3.0 mm. Confirm the complete 16IR or 16ER code, grade and current availability for each pitch; the thread's nominal diameter and tolerance come from your drawing.
What does a full-profile ISO metric insert do?
A pitch-specific full-profile insert forms the metric thread's flanks, root and crest when the blank diameter has suitable material for cresting. Select the insert for the exact pitch and gauge the finished thread to the drawing's tolerance class.
Is AG55/60A the grade of these inserts?
The original copy does not establish AG55/60A as a verified HY carbide grade. In manufacturer nomenclature, AG 60 can describe a 60° partial-profile geometry, separate from an ISO full-profile insert. Ask for the actual HY grade and coating on the complete item code.
Can one full-profile insert cut all three listed pitches?
No. A full-profile insert is pitch-specific. Use a separately confirmed 1.0, 2.0 or 3.0 ISO insert. A partial-profile 60° insert may cover a stated pitch range, but it does not form the thread crest.
How should feed and cutting speed be set?
For a single-start metric thread, synchronized axial feed per revolution equals the pitch. Reach the final thread depth over controlled infeed passes. Select cutting speed from the confirmed insert grade, workpiece material, diameter and holder setup.
◆Ordering & OEM FAQs
What information is needed to match a replacement insert?
Send the original complete insert and holder codes, clear marking or box-label photos, metric thread size and tolerance, workpiece material, cutting conditions and required quantity. Matching the 16IR or 16ER family name alone does not establish fit or grade equivalence.
Can I combine internal and external pitches in one inquiry?
Yes. Provide a separate line for each 16IR or 16ER code, pitch, grade and quantity. Availability, mixed-order packing, minimum quantity and dispatch timing are confirmed by item.
Are steel, stainless steel and cast iron covered by the same grade?
The product family can be quoted for these material groups, but grade suitability is specific to the complete insert code and cutting conditions. State the workpiece grade and operation so a suitable carbide grade and starting data can be confirmed.
Can I request OEM markings or samples?
Include the insert codes, quantity, trial application and requested marking or packaging artwork. Sample availability and OEM feasibility are confirmed with the specification and quotation.
◆Guides & Technical References
Review the CNC Insert Selection Guide for insert, grade and holder selection. Use the ordered model's drawing and cutting data for final setup.
For a model-specific drawing or quotation, send the thread and holder details.
Need Sizes, Pricing or Custom Options?
Send us the required tool type, sizes, quantities, workpiece material and any OEM or custom requirements. We will confirm suitable specifications, availability, lead time and quotation details.
Drawings, size lists and reference photos are welcome.