
Aluminum Sticking to End Mills: What to Check Before Changing the Tool
HY CUTTING TOOLS JOURNAL / BUYING GUIDE
What to Check Before Changing the Tool
Aluminum sticking to end mills often reaches a reseller as a simple request: “The cutter is loading up. Can you send a better one?” Before quoting another cutter, check the current tool, the alloy and the operation.
A practical guide for resellers, importers and purchasing teams handling customer complaints, comparing replacements and planning trial orders.
| What to Check | Quick Review |
|---|---|
| What Does the Customer’s Photo Actually Show? | Collect clear edge and flute photos, the tool code, and when the problem starts. |
| Confirm the Alloy and the Operation | Identify the aluminum grade, operation, depth and width of cut. |
| Check Lubrication and Chip Removal | Check fluid delivery and whether chips remain in the cut. |
| Review the Actual Cutting Data | Record spindle speed, feed rate, flute count, cutting engagement and tool projection. |
| Compare the Replacement Specification | If replacement is needed, compare dimensions, reach, geometry, surface finish and coating. |
| Agree on the Trial Before Expanding the Order | Define the test job and acceptance criteria before committing to a larger order. |
In this guide
CUSTOMER EVIDENCE
What Does the Customer’s Photo Actually Show?
A distant photo of the cutter rarely explains the complaint. Request close-ups of every cutting edge, the flute area and the affected part surface, along with the tool label or full model code.
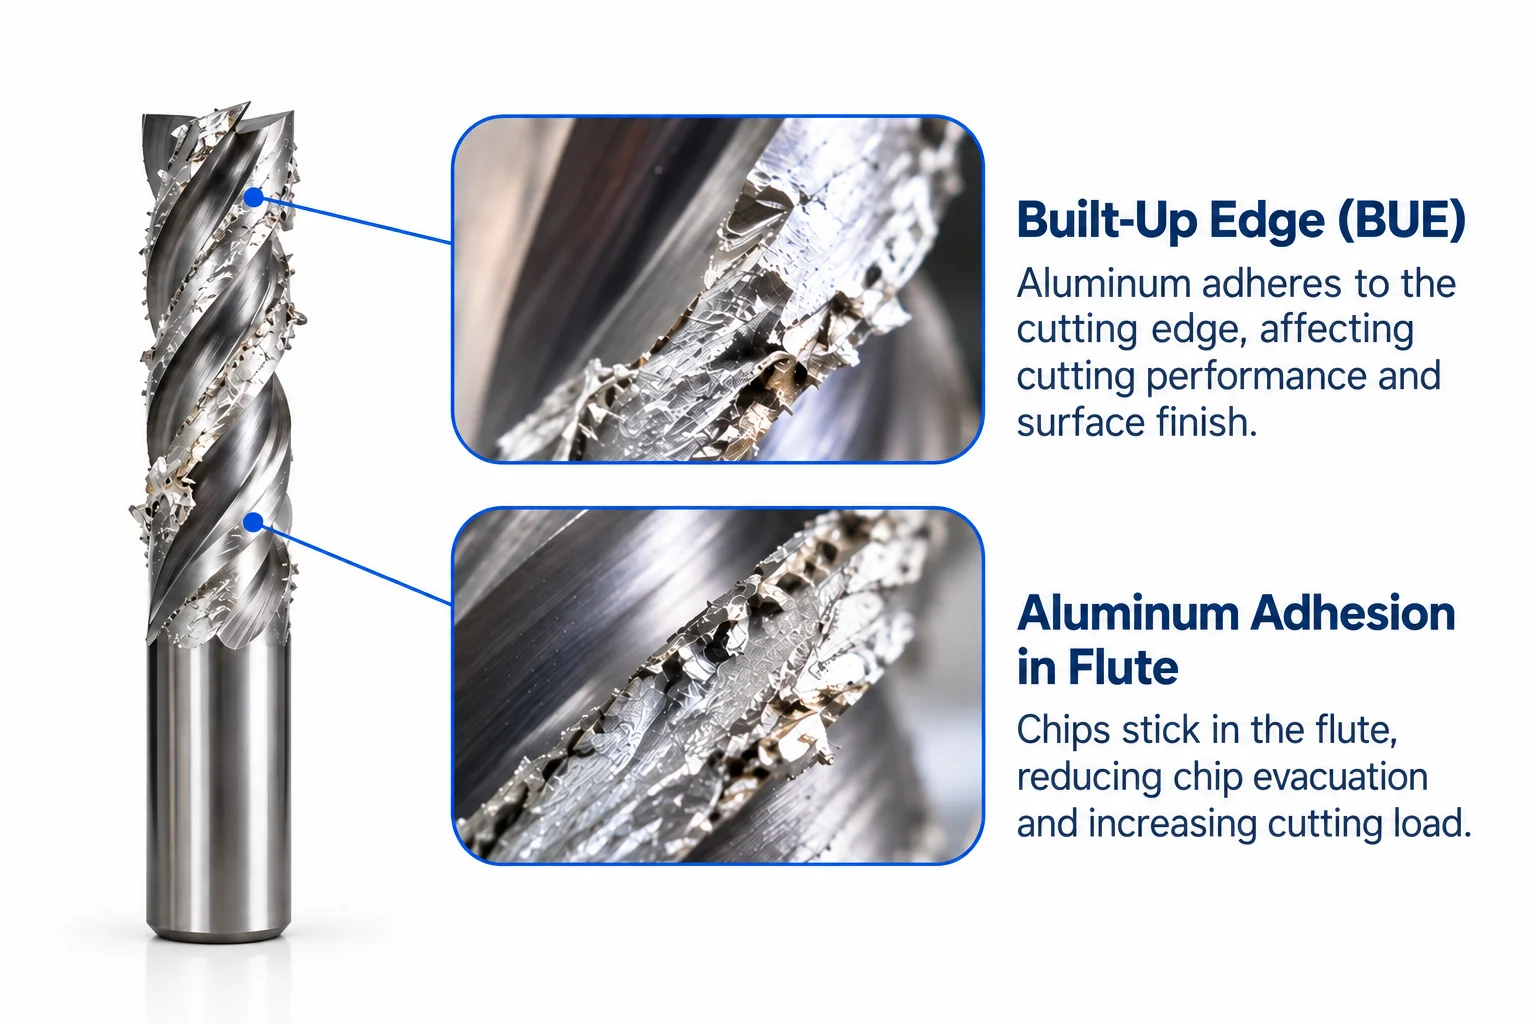
Timing helps narrow the review. Does the problem start on the first part, after several parts, at a particular depth, or after a material or setup change? Keep that answer with the photos.
Collect the cutting data before confirming tool selection or trial settings. Damaged tools should be removed from service.
| Customer reports | What to do with this information |
|---|---|
| Material stuck near the cutting edge |
Request: Close-ups of all active edges and the affected surface Review: Is this built-up edge, and what conditions need checking? |
| Flutes filling with chips |
Request: Flute photos and the location of the cut Review: Is chip packing occurring in this operation? |
| One edge damaged |
Request: Images showing every flute, plus holder and projection details Review: Does the damage pattern require a setup or loading review? |
| Finish deteriorates during a run |
Request: Accepted-part count, inspection results and failure timing Review: What changes between the first acceptable part and the complaint? |
Built-up edge is workpiece material adhering to the cutter’s rake face. Chip packing means chips are accumulating in the flutes. The two can occur together, but a rough surface or broken edge alone does not identify either problem.
For visual reference, see Seco’s end mill wear-pattern guide. It separates built-up edge, chipping and chip-evacuation damage rather than treating them as one failure.
A Reply You Can Send to the Customer
“Please send the tool code, close-up photos of the edges and flutes, and the aluminum grade and operation. These will help us review a replacement. We can follow up on the cutting settings before arranging the trial.”
APPLICATION
Confirm the Alloy and the Operation
“For aluminum” is a product category, not a complete application description. Ask for the exact alloy designation and whether the customer is machining wrought stock or a casting. Add silicon content if it is known and relevant.
The operation matters just as much: full-width slotting, pocketing, side milling or finishing. Include the depth and width of cut. A light side-milling job and a deep slot place different demands on chip evacuation.
- Minimum job description: alloy, operation and where the problem appears.
- Useful additions: feature drawing, required finish, tolerance and machining depth.
- If details are missing: write “to be confirmed” and request them from the operator before final selection.
Harvey Performance’s aluminum machining guide discusses material differences, geometry and chip evacuation. Those application details help a supplier narrow the candidate tool; the alloy name alone does not settle the choice.
CHIP CONTROL
Check Lubrication and Chip Removal
You can collect useful information without troubleshooting the machine yourself. Find out how cutting fluid or lubricant reaches the tool and whether chips remain in the cut. A short video can help if the customer is allowed to share it.
“We use coolant” leaves several questions open: what fluid, what concentration, what delivery method, and where does the nozzle aim? The operator should check fluid condition against the fluid supplier’s instructions and the tool’s application guidance.
If the complaint appears only in pockets, deep slots or corners, include that detail. It gives the supplier a reason to review chip space, tool engagement and fluid access before recommending a coating change.
Have the operator and tool supplier agree on lubrication and chip-removal conditions for that job. For a broader checklist, use our machining troubleshooting guide.
CUTTING CONDITIONS
Review the Actual Cutting Data
For the application review, collect actual spindle speed, feed rate, flute count, axial depth and radial width of cut. Include tool projection and any known runout or holder issue. Screenshots are useful when the units and job are clear.
If the operator has already changed the program, holder or cutting settings, send the before-and-after values and results. Catalog recommendations alone do not show what happened on the machine.
Reducing speed and feed together is not a universal response to aluminum sticking to end mills. Ask the supplier which setting to test first, why it is relevant to the observed failure, and how it fits the tool’s operating range.
Le Sandvik Coromant milling troubleshooting reference organizes corrective actions by failure mode. Use it to frame the review, then confirm instructions for the customer’s exact end mill and application.
Keep a short change log. Where practical, change one factor at a time; if the tool and process must change together, record both so the successful conditions can be repeated.
TOOL COMPARISON
Compare the Replacement Specification
“A better Ø8 three-flute aluminum end mill” is a starting point for a quote. Before offering it as a replacement, compare reach, chip space, edge preparation and recommended applications. Standard nominal dimensions make matching easier; they do not make every model interchangeable.
| Spécifications | What to do with this information |
|---|---|
| Dimensions and clearance |
Confirm: Cutting diameter, cutting length, shank, overall length, corner radius and neck Why it matters: The candidate must fit the feature, reach and holder. |
| Flute and edge design |
Confirm: Flute count, helix, chip space and edge preparation where specified Why it matters: Matching nominal dimensions does not establish matching performance. |
| Surface and coating |
Confirm: Uncoated or coated; which surfaces are polished; exact coating designation Why it matters: Compare the stated finish and coating, not the tool color. |
| Application range |
Confirm: Alloy, operation, engagement and lubricant recommendations Why it matters: Confirm the intended job before presenting the tool as a replacement. |
| Model and purchasing terms |
Confirm: Exact code, quantities by size, trial availability, lead time and reorder specification Why it matters: Tie the price and sample approval to an identifiable product. |
Uncoated and polished describe different things. One refers to coating; the other to surface finishing. The quotation should state which surfaces are polished and the coating designation, if any. Tool color is not a reliable coating specification.
When adhesion is the problem under review, DLC may be worth testing. OSG describes improved welding resistance and lubricity for its DLC-IGUSS-coated AE-VTS-N series. Use that as a product-specific example, then confirm the quoted tool’s own coating, geometry and application guidance.
Keep a suitable uncoated tool in the comparison, particularly if it already meets the customer’s quality requirements. Compare product ranges through our end mill series guide. For a coating-focused supplier review, see the DLC end mill sourcing guide.
Choose the Next Purchasing Step
- Specification still unclear: confirm the model and dimensions before approving a substitute. Label an initial quotation with the details still outstanding.
- Chip packing or setup concerns: send the evidence for application review before ordering a coating upgrade.
- A suitable alternative is identified: quote the exact model and arrange a customer trial. Keep any geometry and coating differences in the comparison record.
Describe the alternative as a candidate for testing until the customer approves it. If geometry and coating both change, the trial compares complete tools, not the coating alone.
COMPARE BEFORE YOU ORDER
Need a Replacement Candidate to Quote?
Send what you have, even if the application details are incomplete. HY Cutting Tools can review the product reference and quantities, then identify the information needed to compare options for a customer trial.
TRIAL AND REORDER
Agree on the Trial Before Expanding the Order
Start with the size involved in the complaint and a job the customer expects to repeat. Confirm trial quantities and delivery time before ordering the full size range. Record the alloy and operation covered by the test.
Agree on what counts as a pass: required finish and dimensions, accepted-part count or usable cutting length, and when to stop the test. “Looks better” needs an inspection result before it can support a repeat order.
| Record | What to do with this information |
|---|---|
| Part quality |
Compare: Required dimensions and finish using the same acceptance criteria Decision: Whether the candidate meets the customer’s requirement. |
| Usable run |
Compare: Accepted parts or cutting length before the agreed stopping point Decision: Whether the apparent improvement lasts beyond the first cuts. |
| Adhesion and edge condition |
Compare: Photos at comparable points in the run Decision: Whether the reported sticking problem changes. |
| Cost and interruptions |
Compare: Tool price per accepted part, tool-change time and relevant rework Decision: Whether the alternative justifies its purchase cost. |
Does the Higher Tool Price Pay Back?
Tool cost per accepted part = tool purchase cost ÷ accepted parts produced before the agreed stopping point.
For a trial involving several cutters, divide their total purchase cost by their total accepted output. Record machining time, tool-change time and rework separately. The result measures tooling cost; it is not the full production cost per part.
Use conditions approved for each exact tool. Where practical, begin within a common operating window and keep the job and setup comparable. If a candidate requires different settings, record them and treat the result as a tool-and-process comparison.
Where practical, repeat the trial with additional tools to check whether the result is repeatable. Keep the model code and lot reference if supplied; a successful single-tool trial is a starting point for approval, not a batch-consistency test.
Before placing the order, confirm MOQ per size or model, mixed-size conditions, available quantities, sample and repeat-order lead times, and the quality-claim procedure. Ask specifically whether each SKU has its own minimum quantity.
Carry the Approval Into the Reorder
Attach the approved model, dimensions, surface finish or coating and trial record to the reorder. Confirm availability and how specification changes will be communicated. Replenish the approved sizes according to demand; extend approval as further sizes and applications are tested.
BUYER QUESTIONS
Buying FAQ
Select a question to view the answer.
Does aluminum sticking to end mills mean the tools are defective?
Sticking alone is not enough to judge tool quality. Send the supplier close-up photos, the tool code and the cutting conditions before deciding whether to replace the tools or raise a quality claim.
If you still have the box or batch label, include a photo of it. That helps the supplier identify the tools involved.
Can I get a replacement quote with just a tool photo or model code?
Yes—you can use either to start the inquiry. Include the diameter, cutting length and quantity if you have them. Missing details can be checked before the order is confirmed.
For a replacement linked to a customer complaint, also tell us the aluminum grade, the operation and what went wrong. That helps us discuss a suitable option alongside the price.
Is the same diameter and flute count enough to choose a replacement?
It narrows the search, but cutting length, reach and flute geometry still need checking. Two 8 mm, three-flute cutters may fit the same holder without performing the same way.
Ask which model suits the customer’s operation, then test it on that job before buying more.
Should I recommend a DLC-coated end mill when my customer reports sticking?
DLC is worth considering when buildup or poor finish keeps recurring. Give us the alloy, operation and coolant details so we can review the proposed tool for that job.
If an uncoated tool already meets the customer’s requirements, there may be little reason to pay more. For a DLC trial, agree on what you want to improve—less buildup, better finish or a longer usable run.
Can I try a few sizes before placing a larger order?
Yes. HY Cutting Tools accepts mixed-size trial orders. Send the sizes and quantities you want, and we’ll confirm availability, the minimum quantity for each item, price and delivery time.
For a sticking complaint, start with the size the customer is using. Add other sizes if they represent jobs you also need to evaluate.
Is a higher-priced DLC tool worth buying over an uncoated one?
Compare the cost per accepted part, rather than the price of one cutter. Ask the customer to record how many acceptable parts each tool produces, along with tool changes and rework.
If the DLC tool costs more but gives no useful improvement on that job, the extra cost is hard to justify. If geometry also differs, compare the complete tools rather than treating the result as a coating-only test.
What should I include when reordering a tool that passed the trial?
Use the tested model code and full specification on the order, rather than writing only “same as the sample.” Keep the sample or batch reference so both sides can identify what was approved.
Include the quantity and required delivery date. If you need inspection records or batch identification, request them before ordering, and ask to be told about any proposed specification change.
READY TO INQUIRE
Prepare Your Supplier Inquiry
Use the checklist below to prepare a replacement or trial inquiry. Send what you have, and mark missing details “to be confirmed.”
INQUIRY CHECKLIST
Replacement & Trial Details
A message you can adapt
Our customer is seeing aluminum buildup on [tool model] while [operation] in [alloy]. We can send edge and flute photos and the cutting settings.
Could you suggest a replacement and quote [sizes / quantities]? Please include trial availability, MOQ and lead time.
PLAN THE REPLACEMENT ORDER
Compare the Next Tool Before Expanding the Order
Use the inquiry card to send the available information. HY Cutting Tools can review product options and quotation details, including the trial quantities and purchasing terms that need confirming.